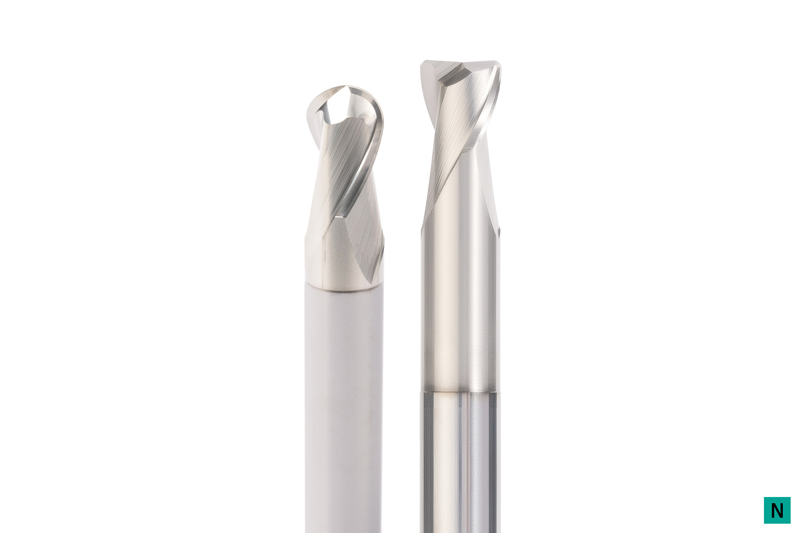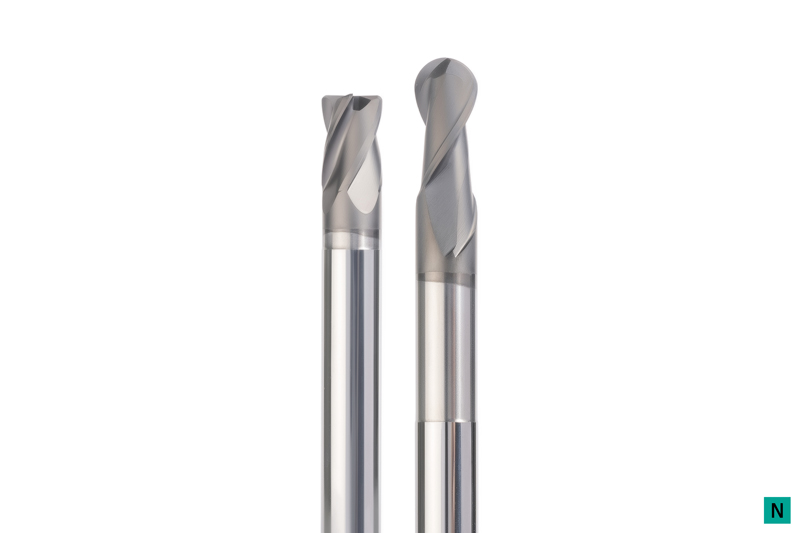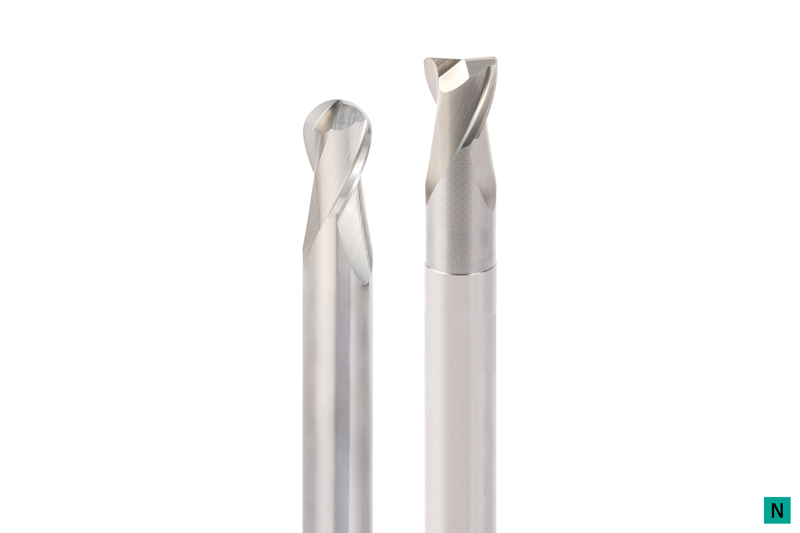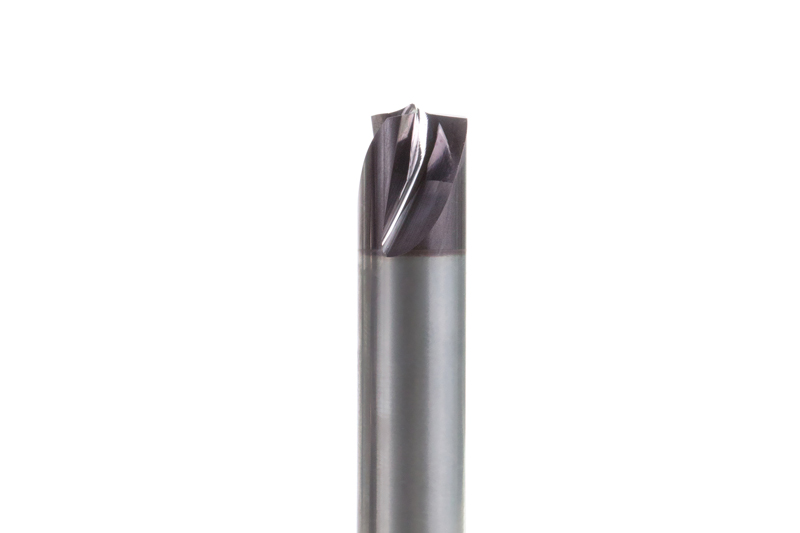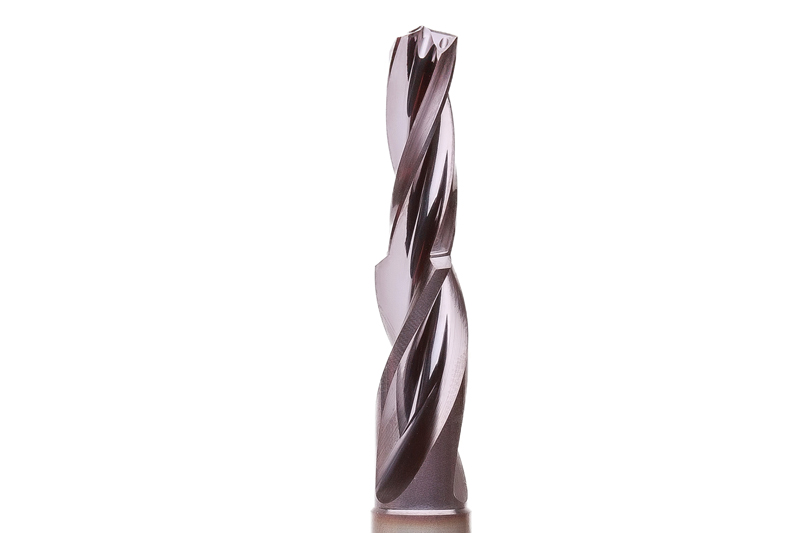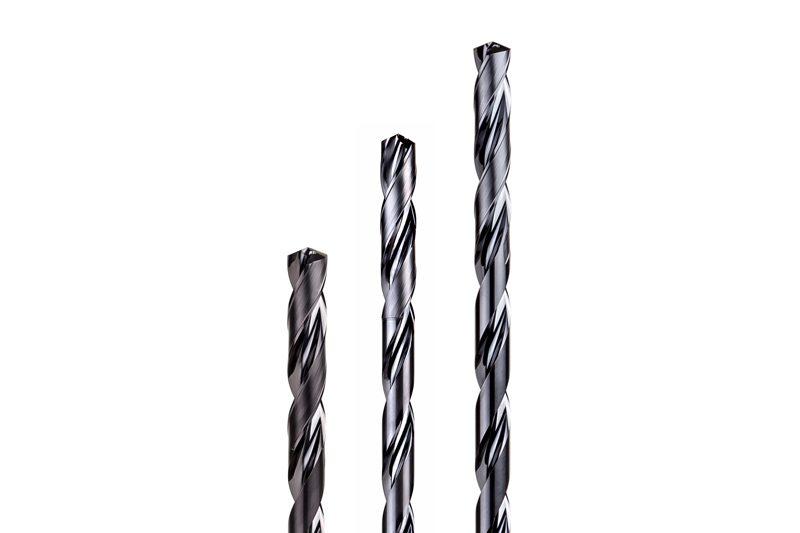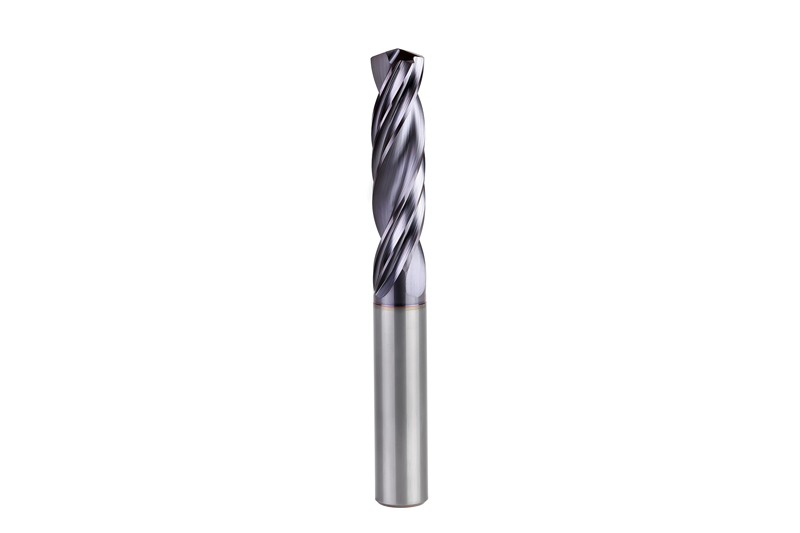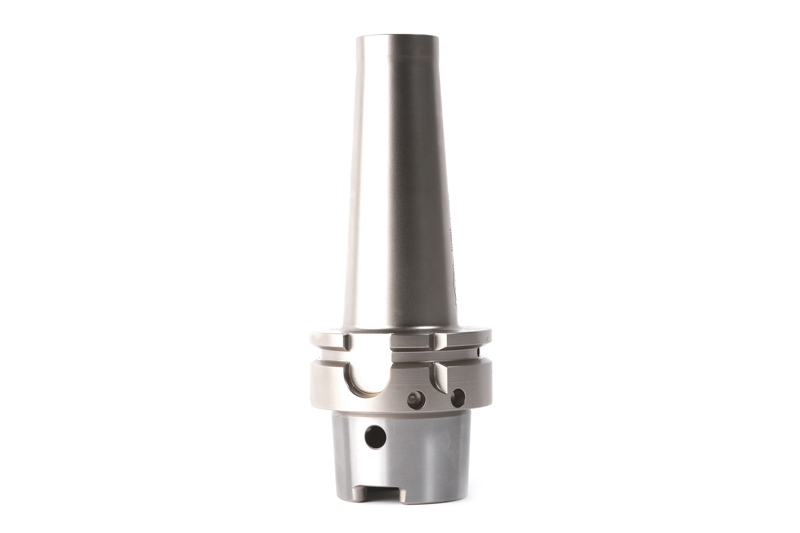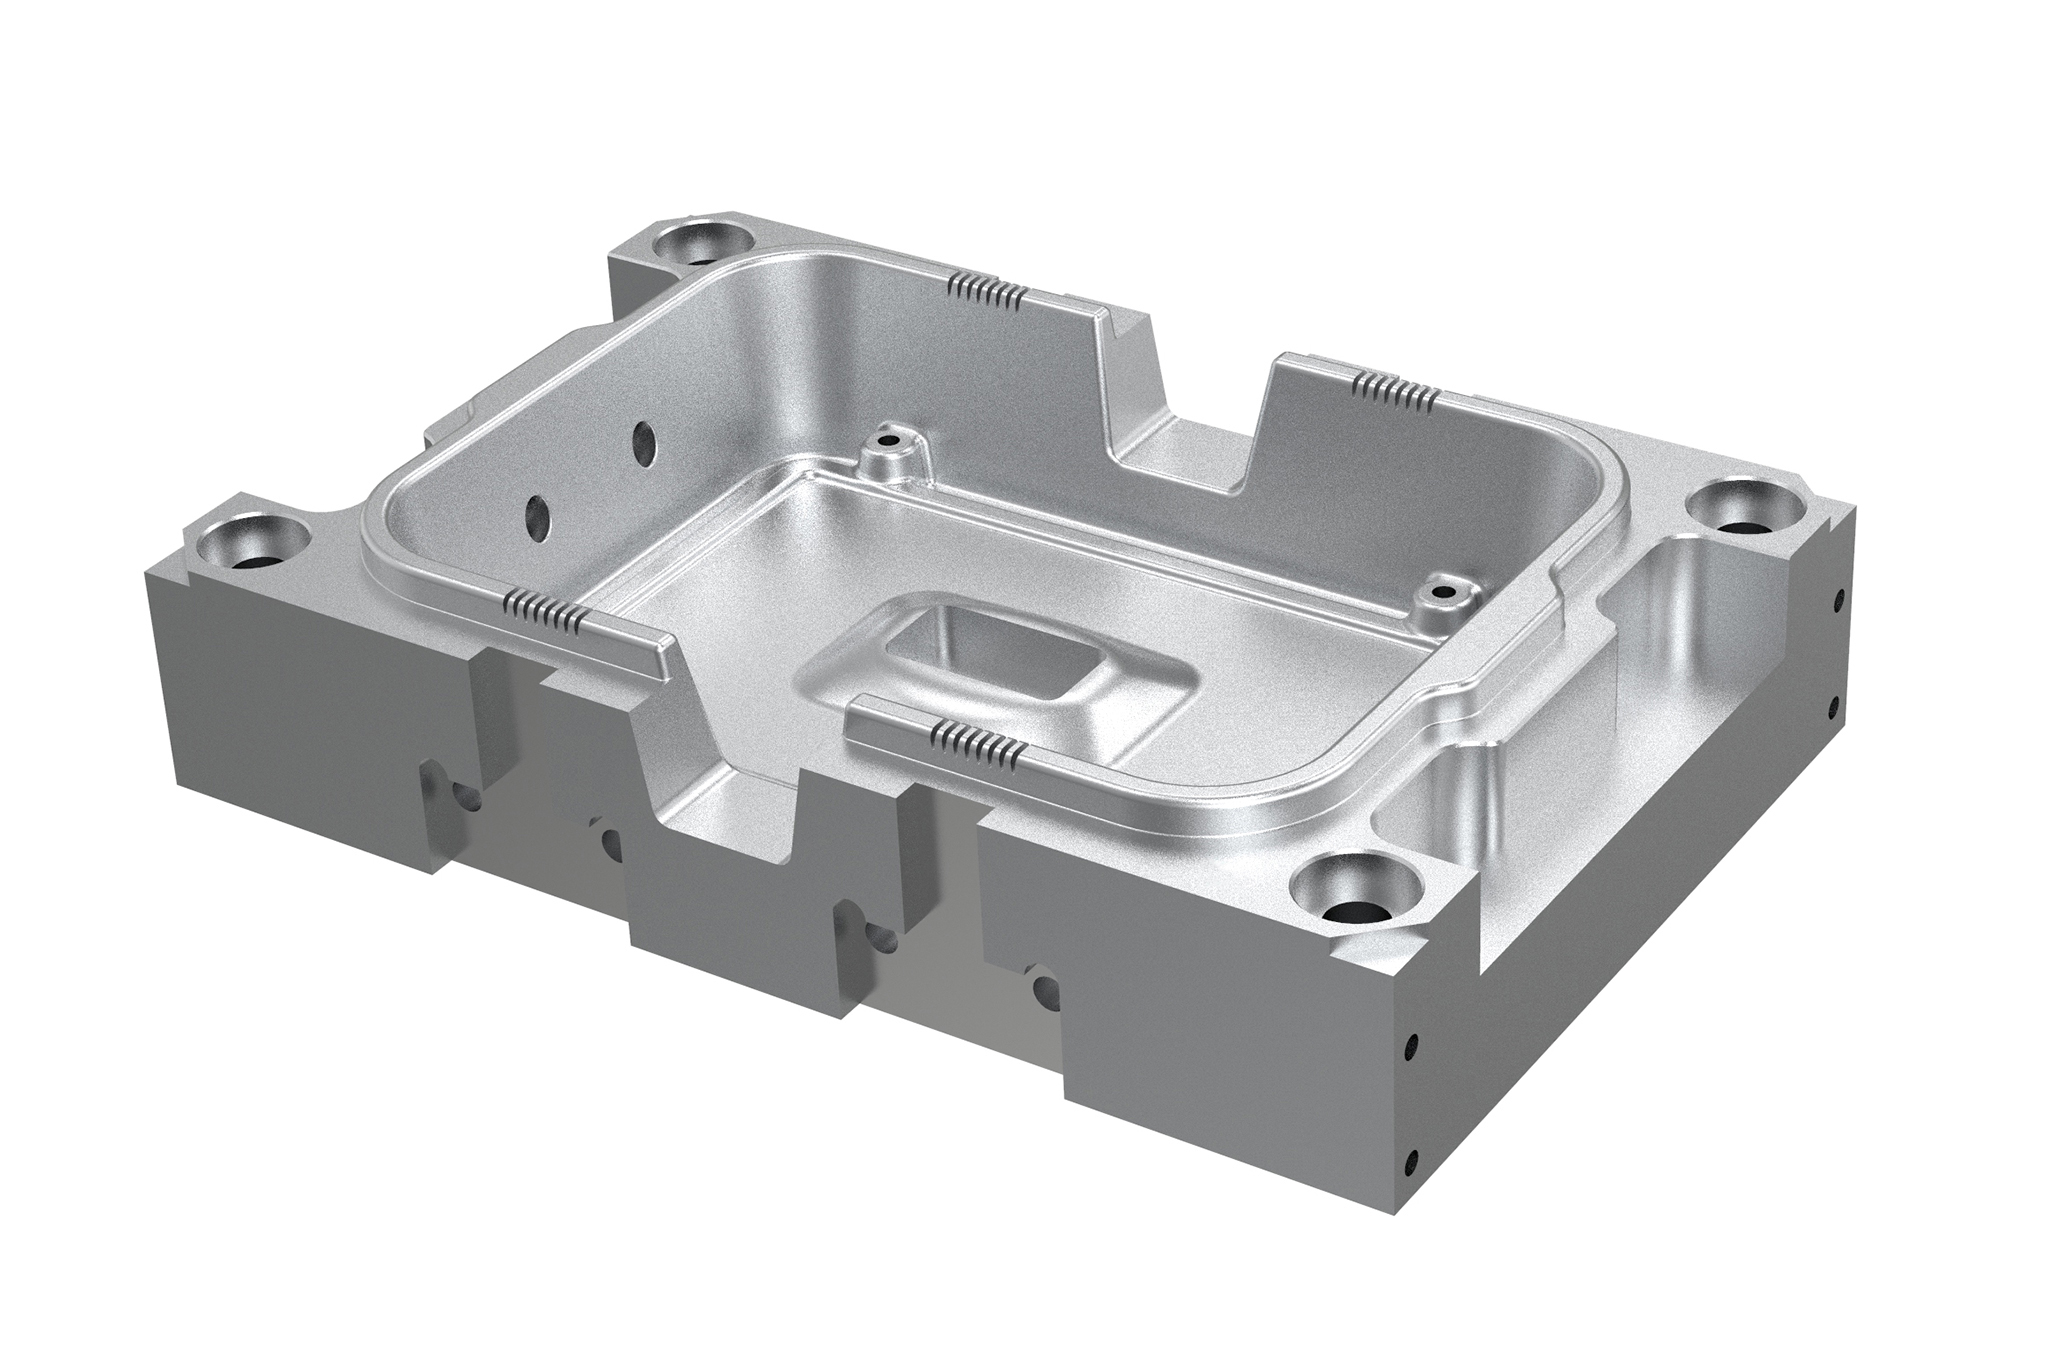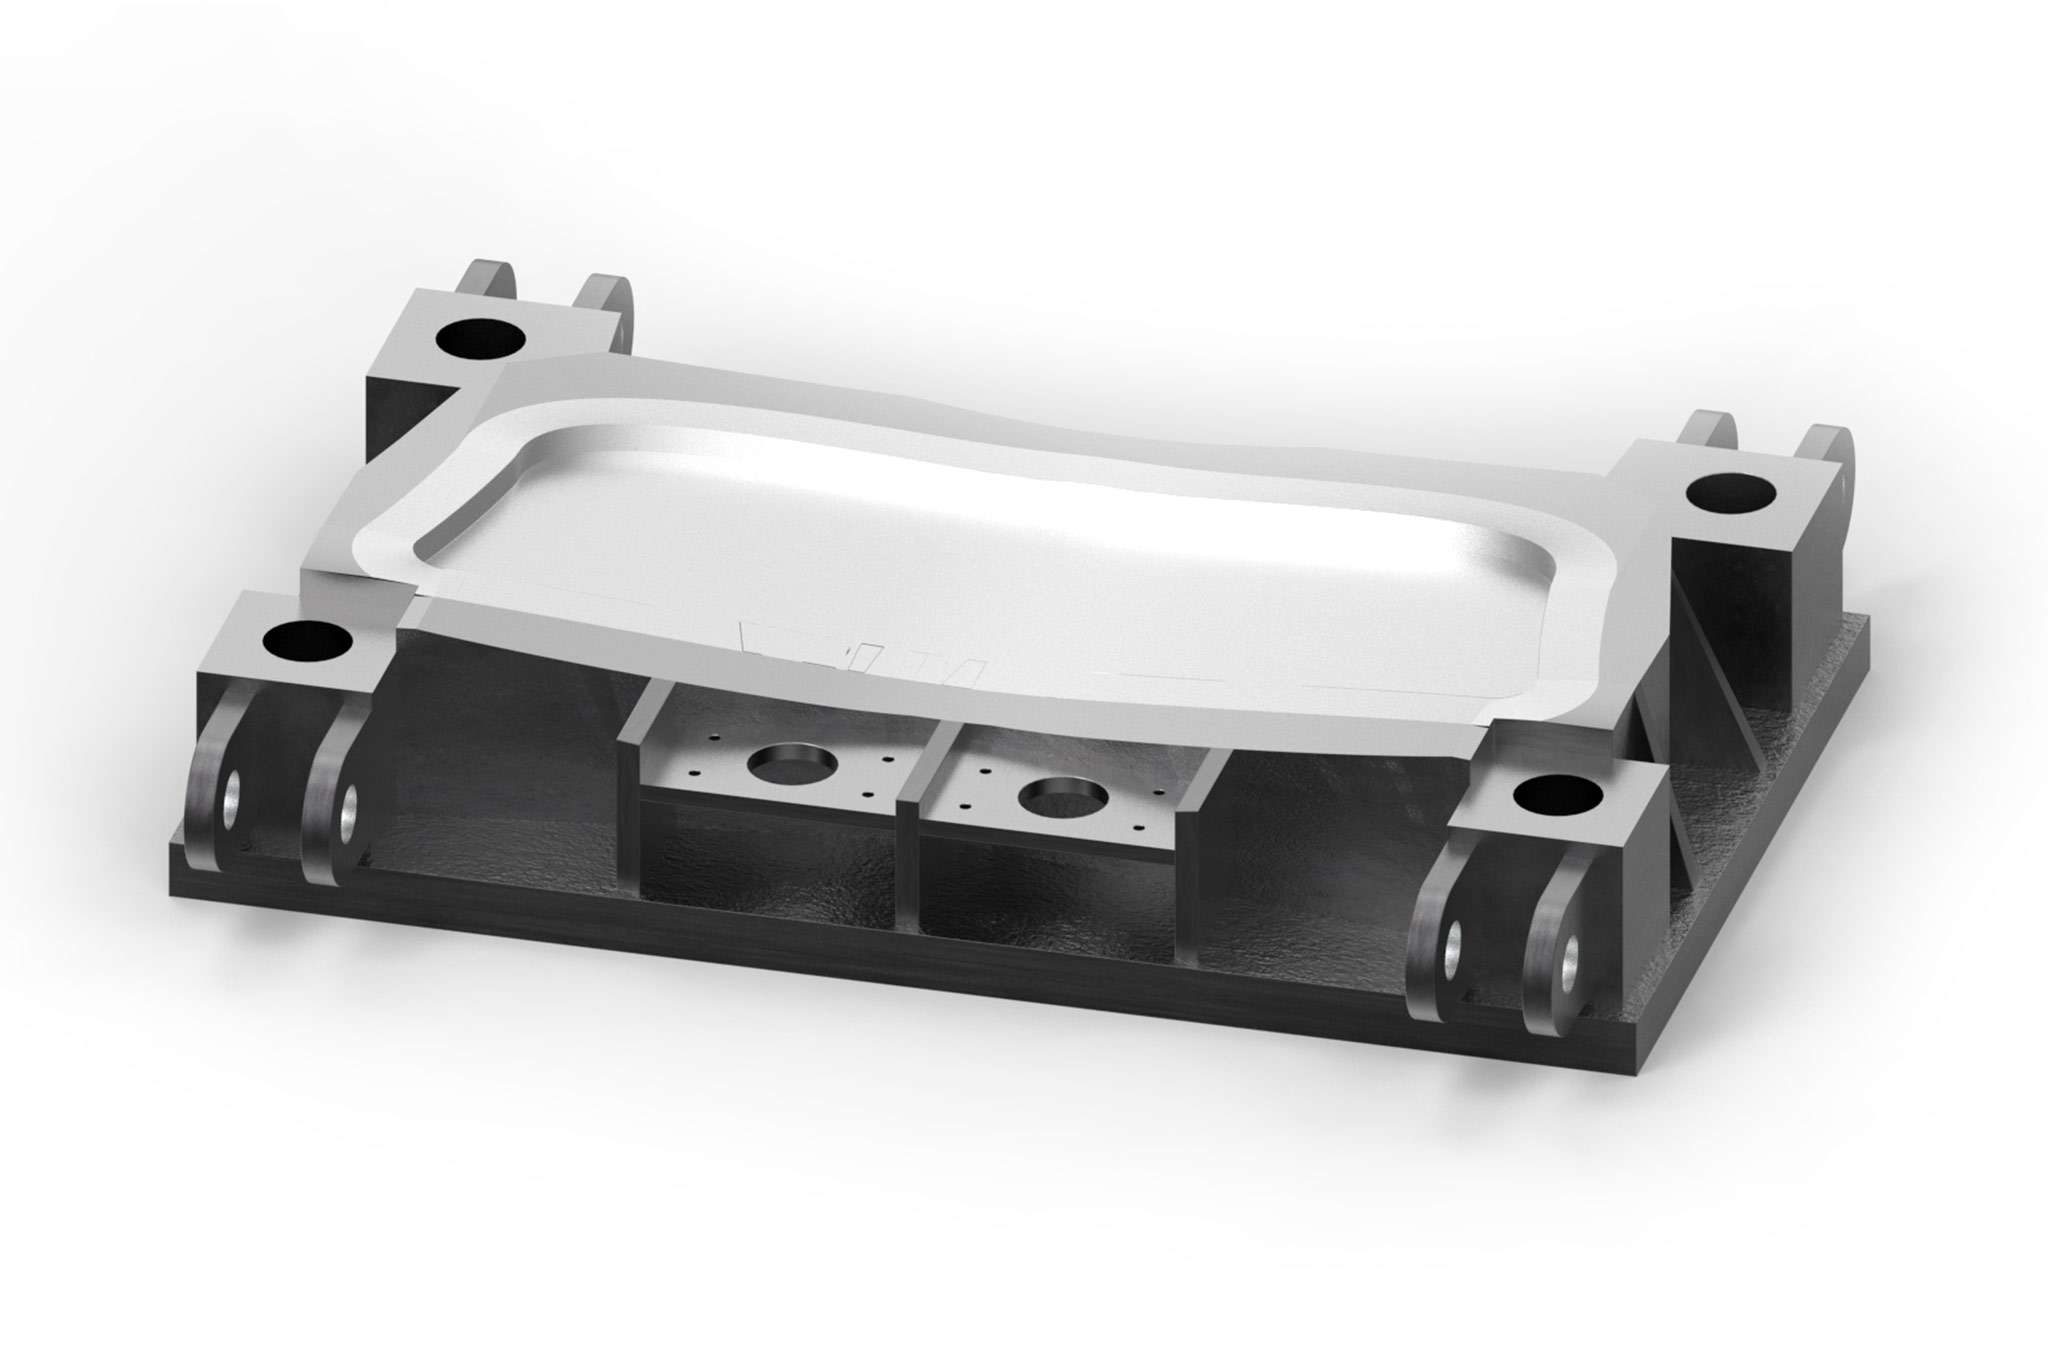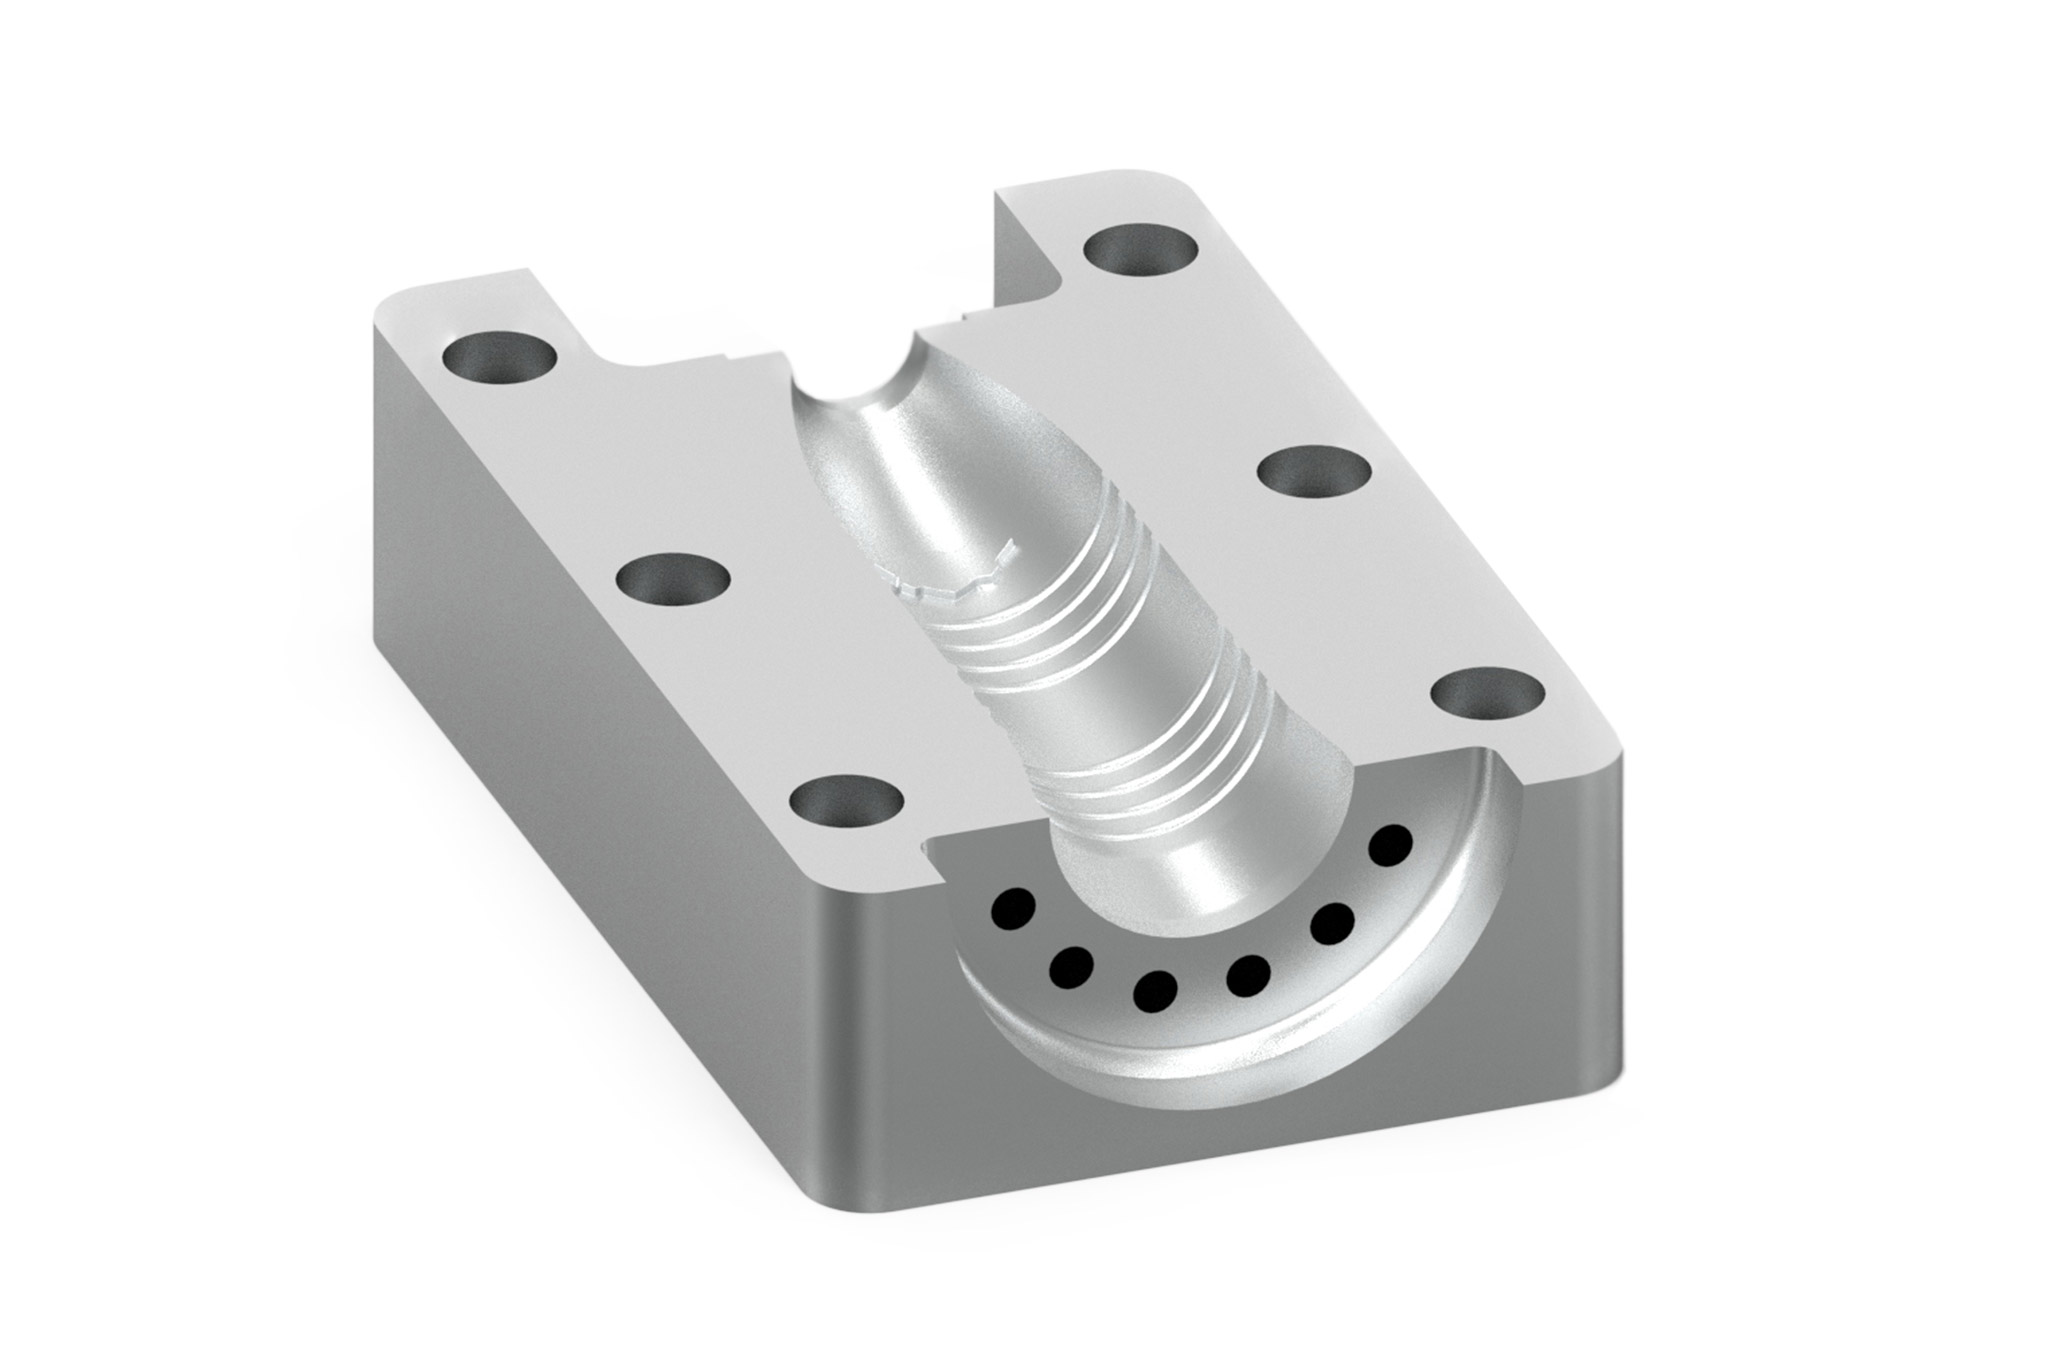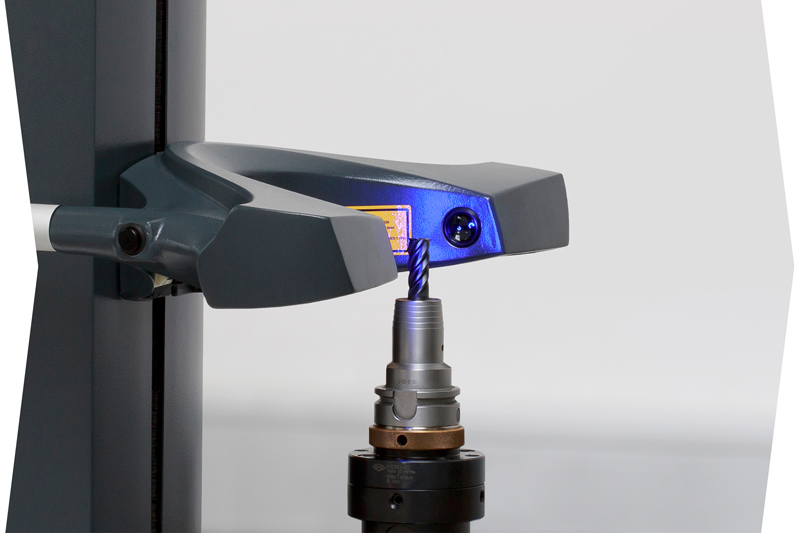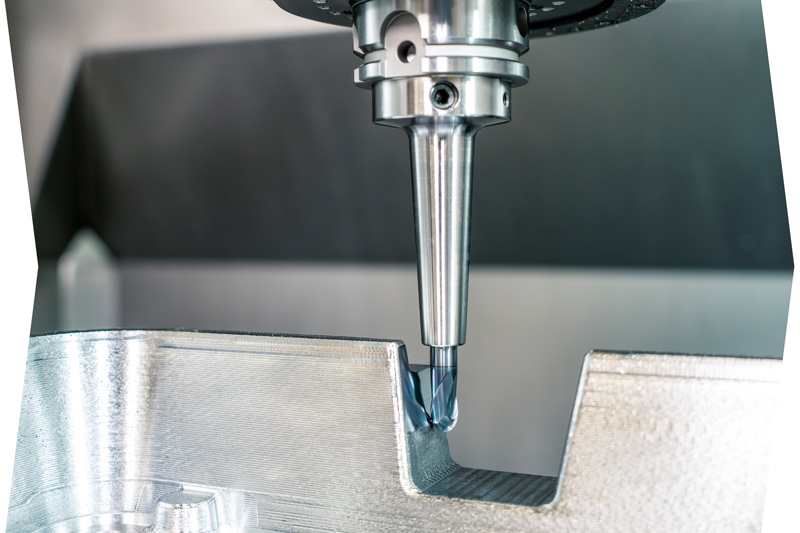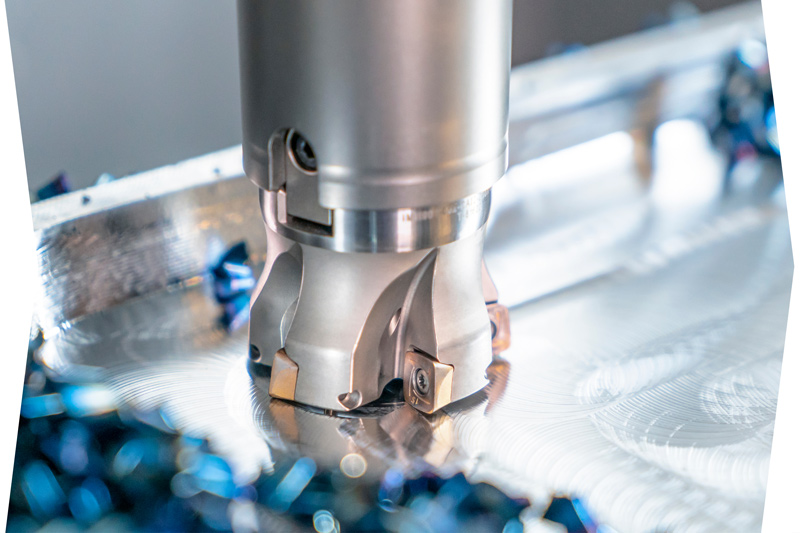
• MAPAL offers complete machining solutions for the die and mould industry.

Getting started in the die & mould sector

Die and mould makers expect high process and product expertise from their cutting tools manufacturer. This is because the tool life of the moulds to be created and the precision of the moulded parts are extremely important for competitiveness in mass production. Therefore, they require their tools to offer the highest levels of precision, a long tool life, and – above all – process reliability.
 

It is precisely these aspects that make MAPAL successful in sectors such as the automotive industry, machine engineering and the aerospace industry. Now the precision tool manufacturer is also offering efficient and economical solutions for the complete machining process in the die & mould sector. Versatile and precise high-performance tools and special tool holders with narrow contours and a precise radial run-out minimise polishing effort and reworking thanks to a constant surface finish in the milling process.

Tool range for mould making
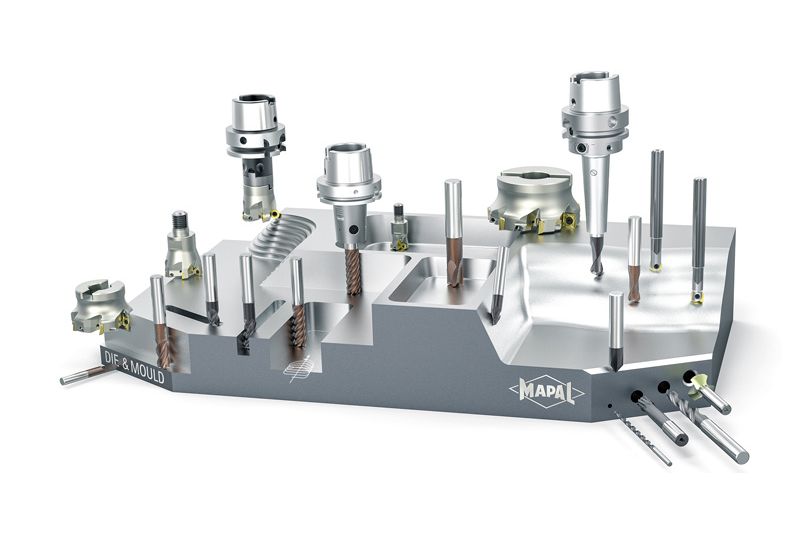
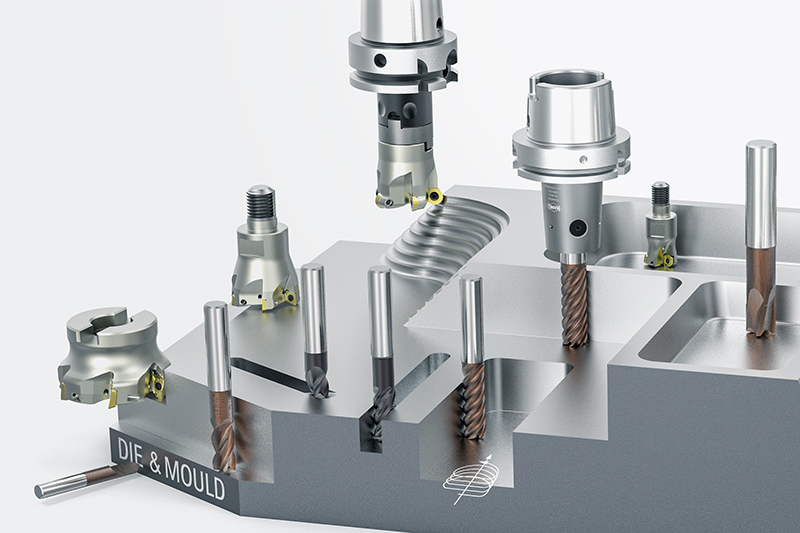
The picture shows the MAPAL tool range for mould making
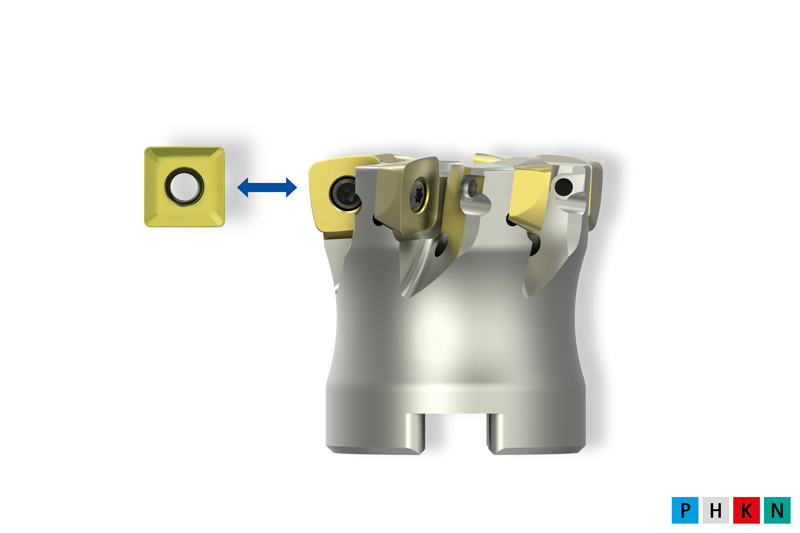
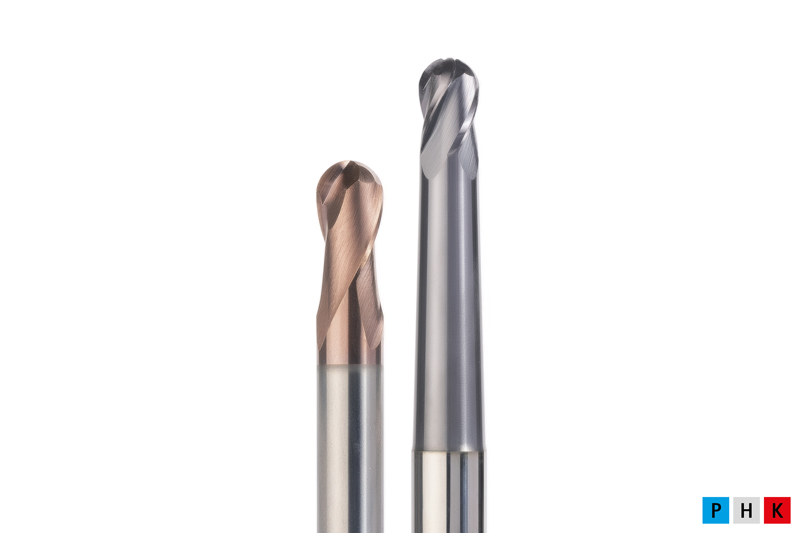
Solid carbide end mills
  • OptiMill-3D-BN

    Ball nose milling cutter
    • High-precision machining of 3D contours
    • ø range: 0.10 - 20.00 mm

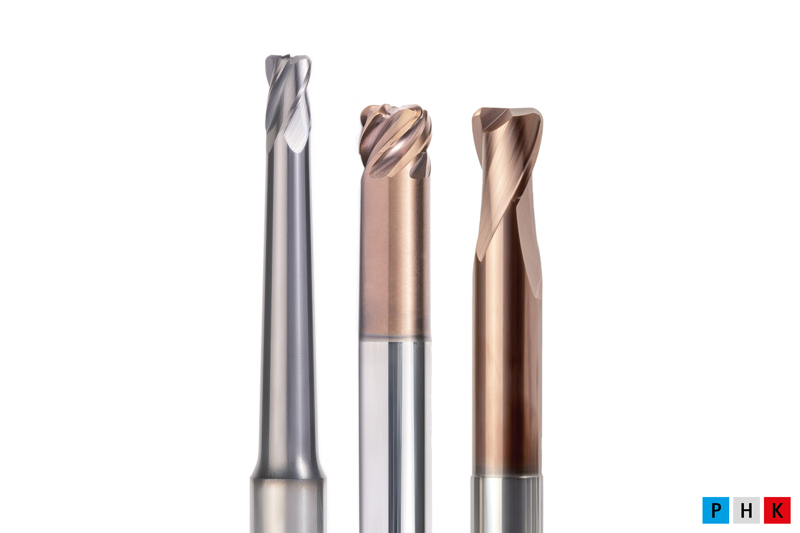
  • OptiMill-3D-CR

    Corner radius milling cutter
    • Milling with a very precise corner radius
    • ø range: 0.10 - 20.00 mm

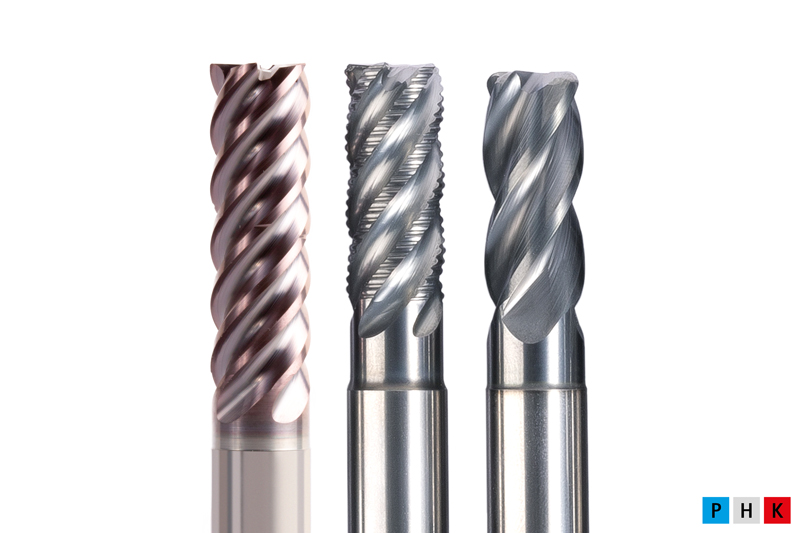
  • OptiMill Shoulder milling cutter

    Shoulder milling cutter
    • Ideal for roughing, finishing, trochoidal milling and milling pockets
    • ø range: 2.00 - 12.00 mm

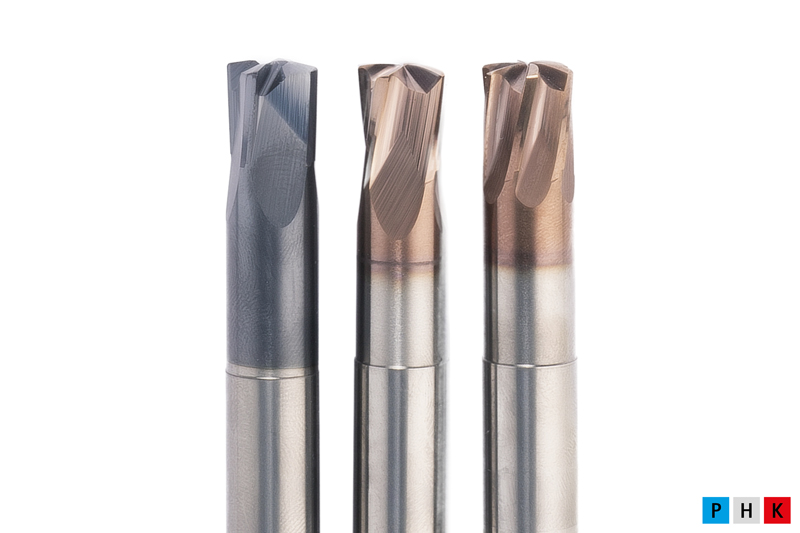
  • OptiMill-3D-HF

    High-feed milling cutter
    • Ideal for high-feed machining with a high material removal rate and high process reliability
    • ø range: 2.00 - 16.00 mm

  • OptiMill-3D-Alu

    Ball nose and corner radius cutters

    • High-precision machining of 3D contours
    • ø range: 1.00 - 20.00 mm

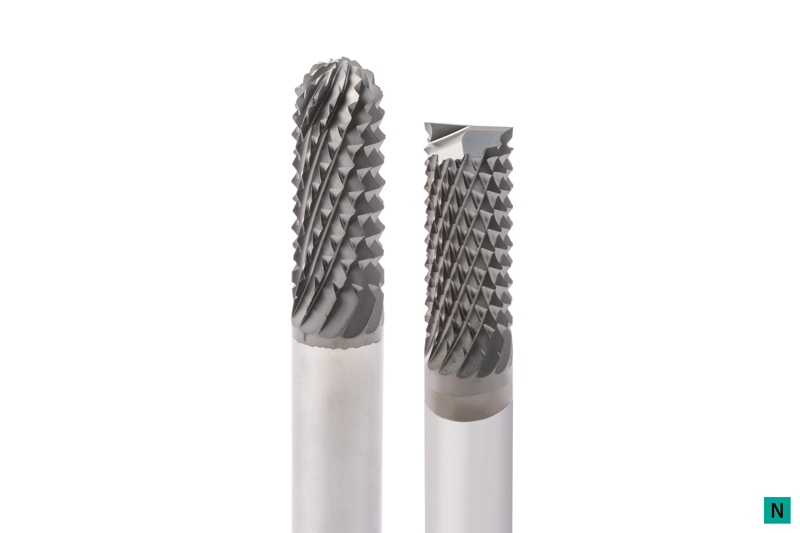
  • OptiMill-Graphite-MT

    Ball nose and shoulder milling cutter
    • Multi-tooth milling cutter for roughing graphite electrodes with high removal rates
    • ø range: 3.00 - 16.00 mm

  • OptiMill-3D-Graphite

    Ball nose and corner radius milling cutter
    • Suitable for machining of graphite electrodes
    • Different designs depending on the machining situation
    • ø range: 0.20 - 12.00 mm

  • OptiMill-3D-Copper

    Ball nose and corner radius milling cutter
    • Special geometry for machining copper electrodes and tough non-ferrous alloys
    • ø range: 0.10 - 20.00 mm

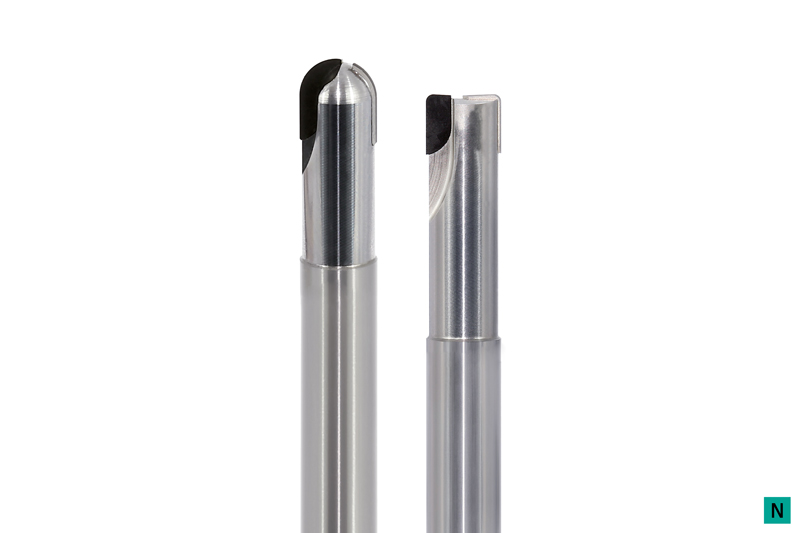
  • OptiMill-Diamond

    Ball nose, corner radius and shoulder milling cutter
    • PCD cutting edges for a long tool life
    • ø range: 3.00 - 12.00 mm

Milling cutters with indexable inserts
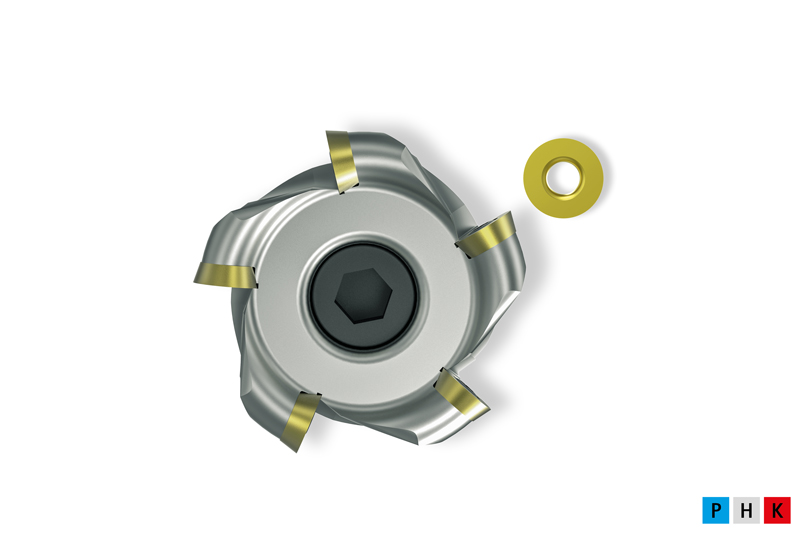
  • NeoMill-ISO-360

    Milling cutter with round inserts
    • Perfect for roughing and pre-finishing
    • ø range: 10.00 - 160.00 mm

  • NeoMill-3D-Finish

    Finishing milling cutter
    • Perfect for finishing 90° surfaces, face surfaces and contours
    • ø range: 16.00 - 42.00 mm

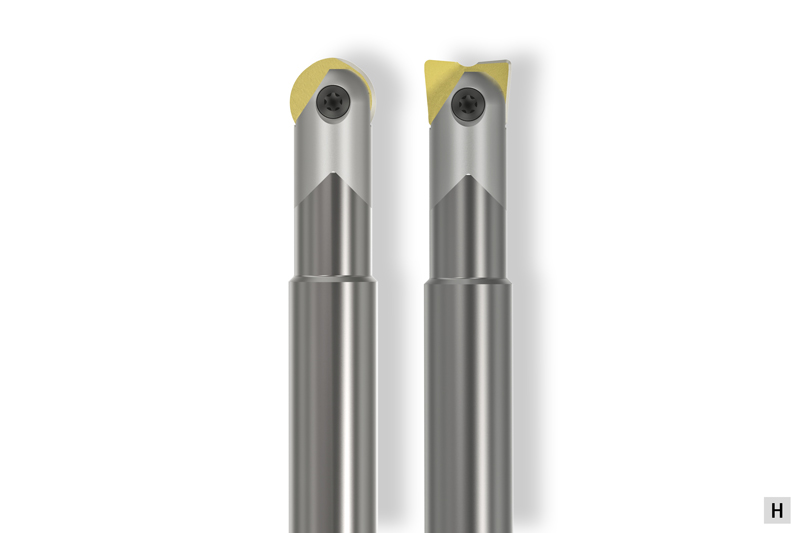
  • NeoMill-3D-Ballnose/-Torus

    Ball nose and corner radius milling cutter
    • One tool body with indexable insert for ball nose and corner radius milling for finishing and pre-finising
    • ø range: 8.00 - 32.00 mm

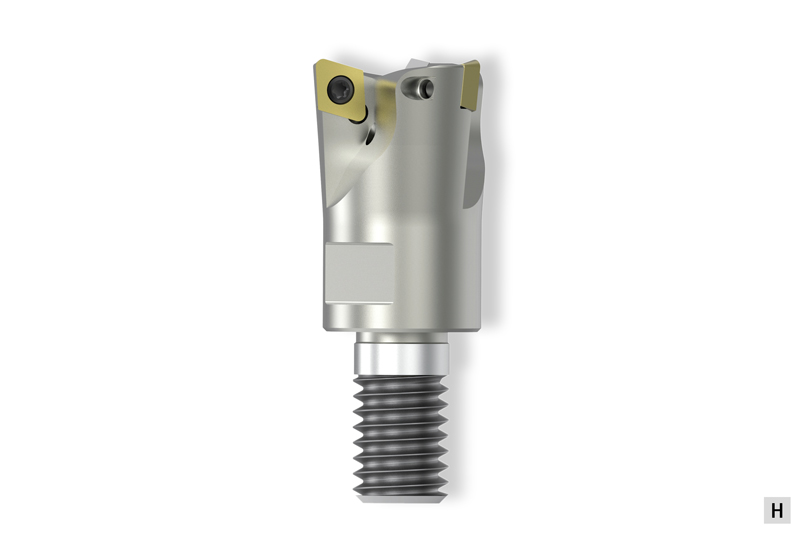
  • NeoMill-2/4-HiFeed90

    High-feed/90° shoulder milling cutter
    • Universal tool system to ensure maximum productivity
    • ø range: 16.00 - 200.00 mm

Drilling | Countersinking
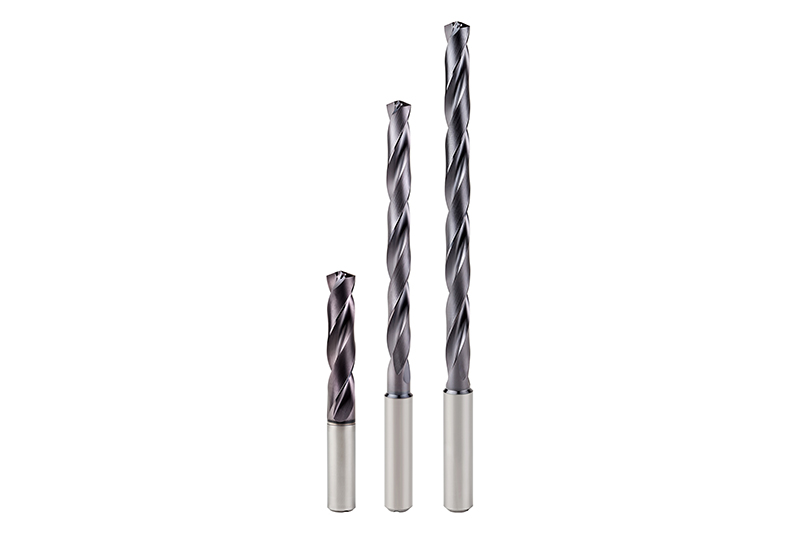
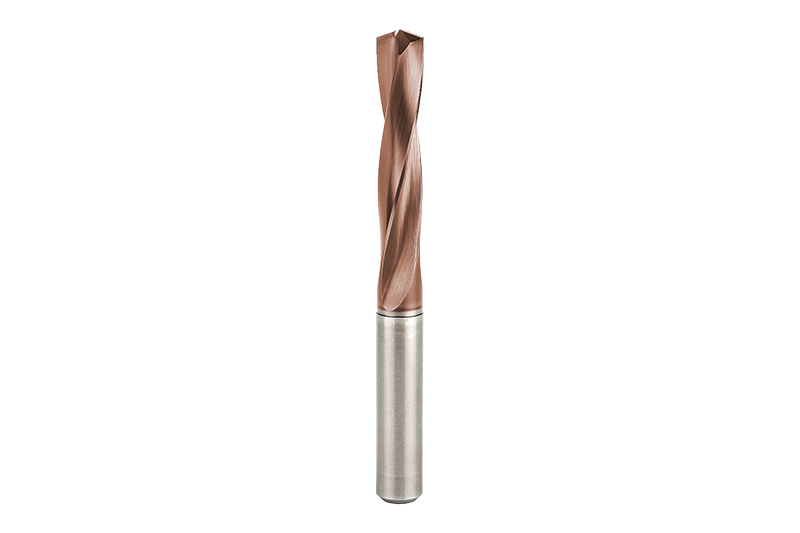
  • ECU-Drill-Steel

    Solid carbide drill  

    • Double-edge solid drill with a good price-to-performance ratio
    • Wide range of applications
    • Proven geometries for high precision and process reliability
    • Ø area: 1.00 – 20.00 mm

  • MEGA-Drill-Hardened

    High-performance solid carbide drill 

    • Double-edge solid drills with coating and geometry suitable for reliable machining of hardened workpiece material
    • New micro-geometry and macro-geometry
    • Ø area: 2.55 – 16.00 mm

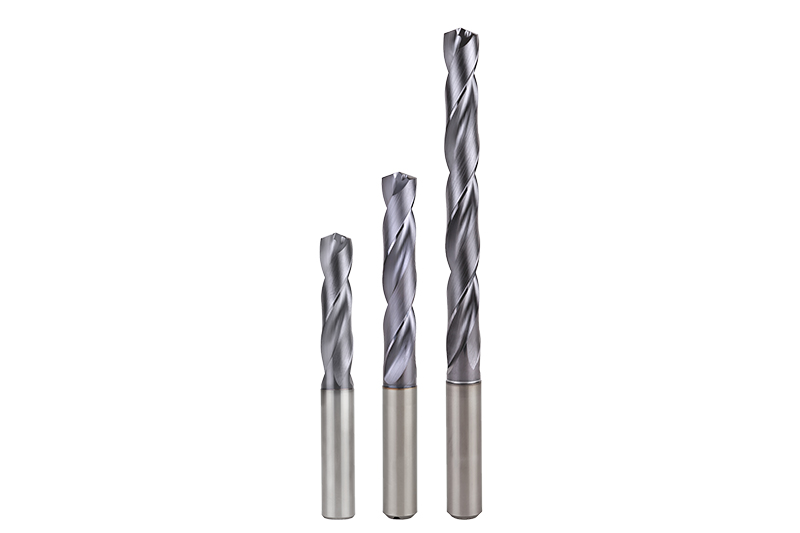
  • MEGA-Drill-Steel-Plus

    High-performance solid carbide drill 

    • Double-edge solid drills with coating and geometry suitable for steel machining
    • Optimised chip flute geometry and modified cutting-edge preparation
    • Ø area: 3.00 – 25.00 mm 

  • Tritan-Drill-Steel

    Triple-edge solid carbide drill 

    • Triple-edge solid drills for maximum feed
    • Self-centring chisel for challenging drilling situations
    • Specially adapted to steel machining
    • Ø area: 4.00 – 20.00 mm 

  • Tritan-Spot-Drill-Steel

    Pilot drill
    • Triple-edge pilot drill for demanding pilot drilling situations
    • Specially adapted to triple-edge drills
    • Ø area: 4.00 – 20.00 mm

  • Tritan-Step-Drill

    Triple-edge step drill
    • Triple-edge step drill with self-centring chisel
    • For machining threaded core holes without oscillating movement
    • Ø area: 4.25 – 14.15 mm

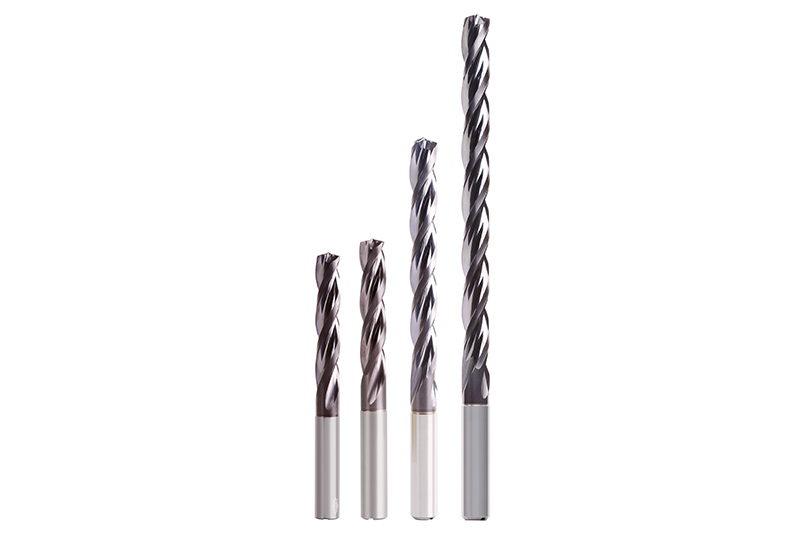
  • MEGA-Deep-Drill

    Deep drill
    • Process-reliable and efficient creation of deep bores up to 40xD
    • MEGA-Pilot-Drill
    • Ø area: 1.00 – 16.00 mm 

  • MEGA-Drill-Reamer

    Drill reamer
    • Two working steps – drilling and reaming – combined in a single tool
    • Optimised reaming cutting edge
    • Reduction of productive and non-productive times
    • Bore tolerance ≥ IT7
    • Ø area: 4.00 – 16.00 mm 

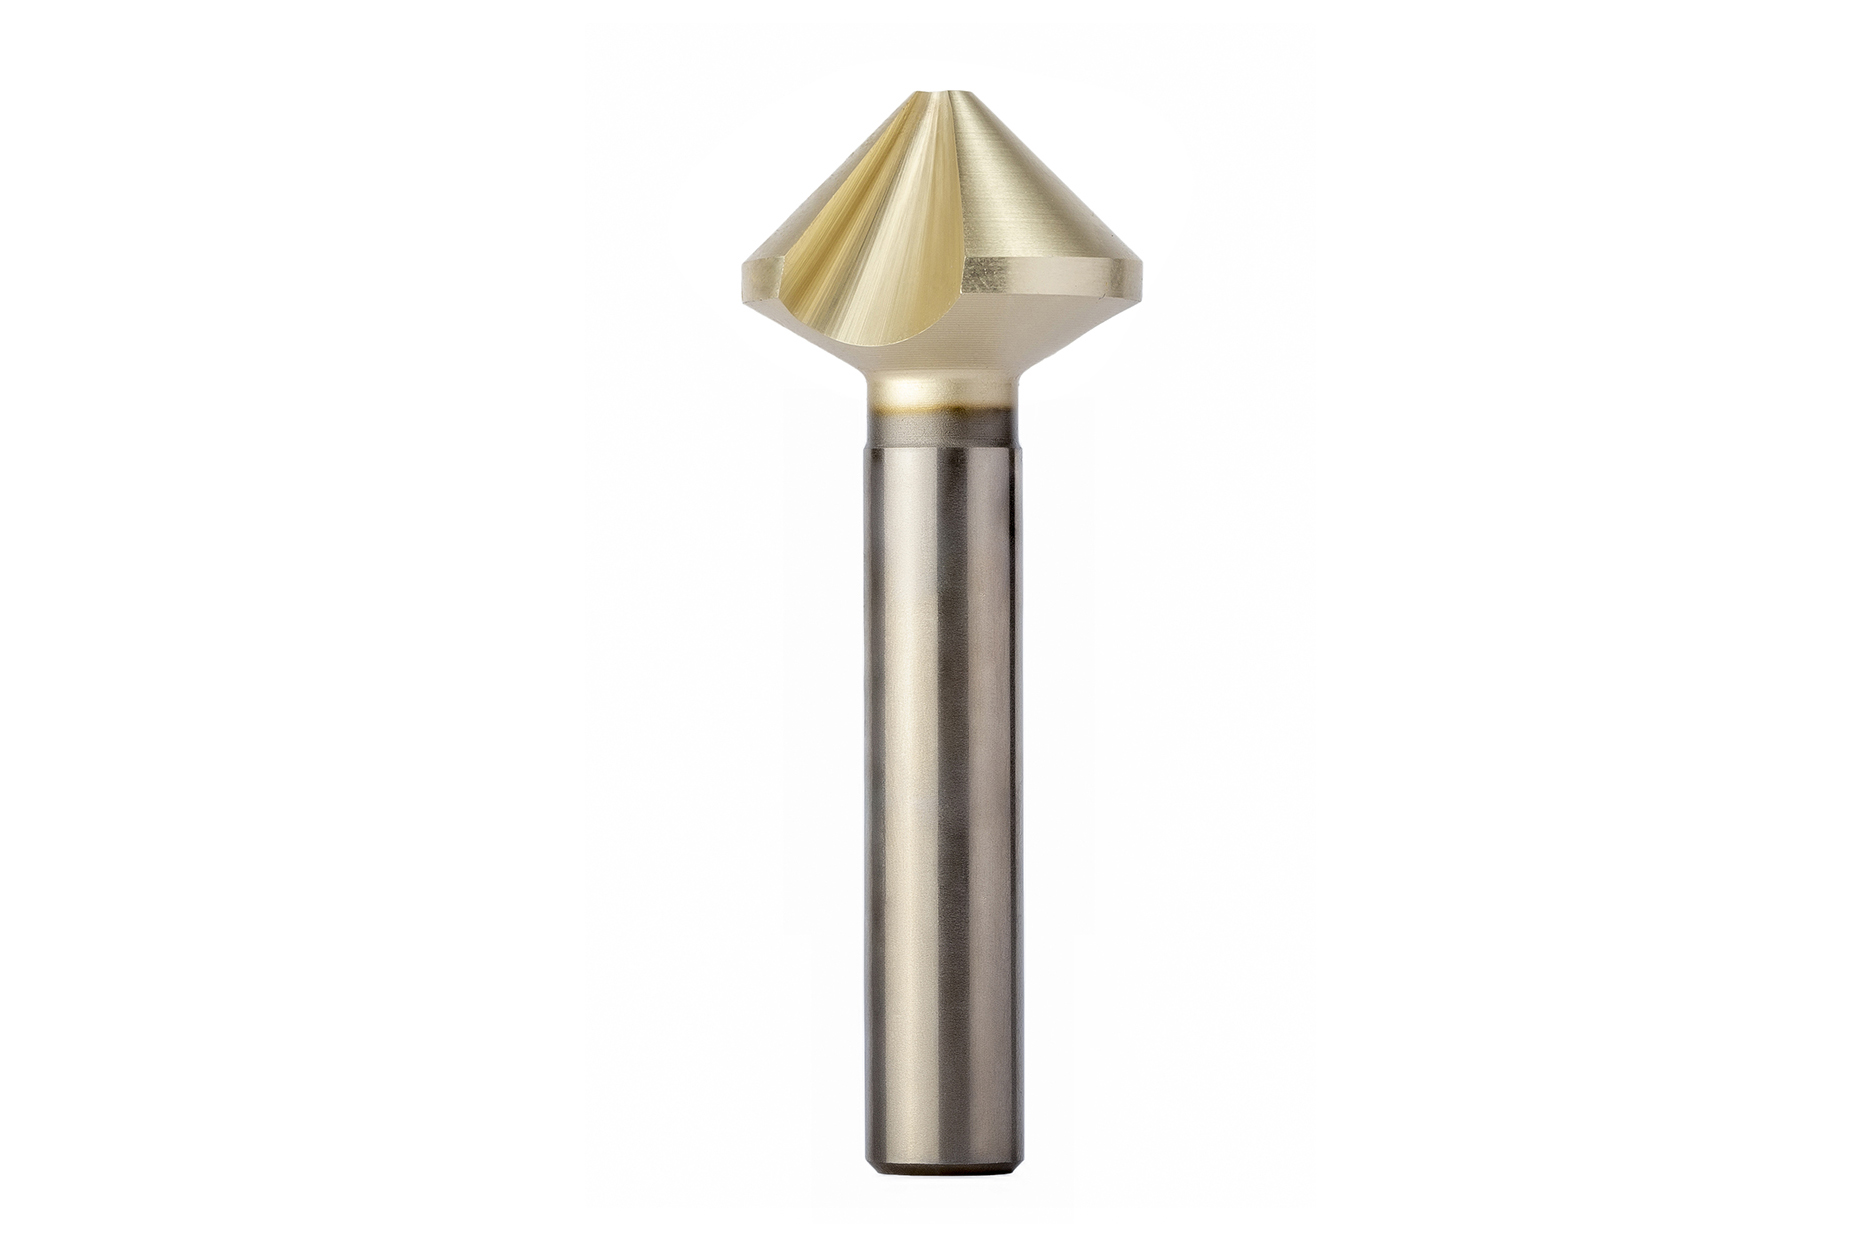
  • Precision countersink

    Countersink with unequal spacing
    • Extremely unequally spaced cutting edges
    • Higher degree of accuracy and improved surface values
    • Reduced axial and radial forces
    • Significantly less vibrations
    • Increased cutting parameters to ensure highest productivity
    • Ø area: 4.30 – 31.00 mm 

  • MEGA-Drill-Reamer-Pyramid

    Drill reamer with pyramid tip 

    • Spot drilling, drilling and reaming – all with one tool
    • Improved centring properties thanks to pyramid tip
    • Reduction of productive and non-productive times
    • Bore tolerance ≥ IT7
    • Ø area: 4.00 – 16.00 mm 

  • QTD indexable insert drill

    Solid drill with replaceable head system 

    • Cost-effective system with indexable inserts that can be swapped out
    • Force-locking and form-fit clamping system
    • Easy to handle
    • High degree of radial run-out accuracy
    • Ø area: 8.10 – 49.00 mm 

Reaming
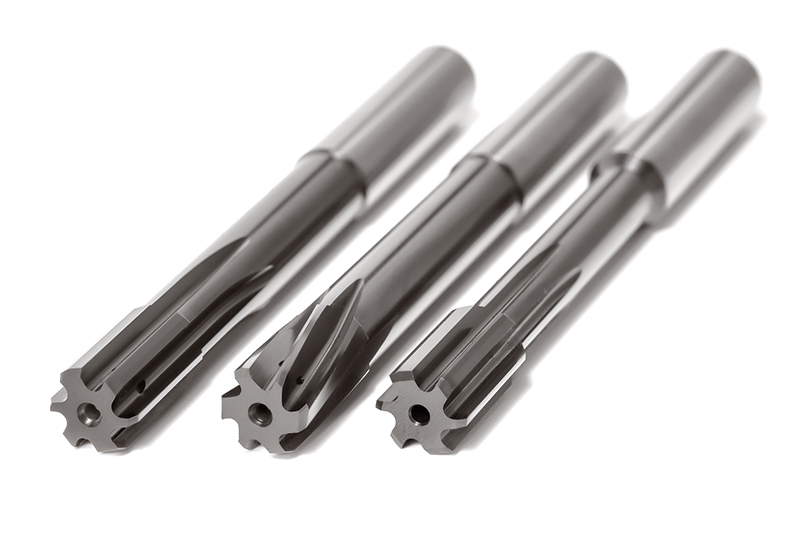
  • FixReam – FXR

    High-performance reamers with a cylindrical shank 

    • High-performance reamer made from solid carbide
    • Straight-fluted for through and blind bores
    • Left-hand fluted for through bores
    • Ø area: 3.00 – 20.00 mm 

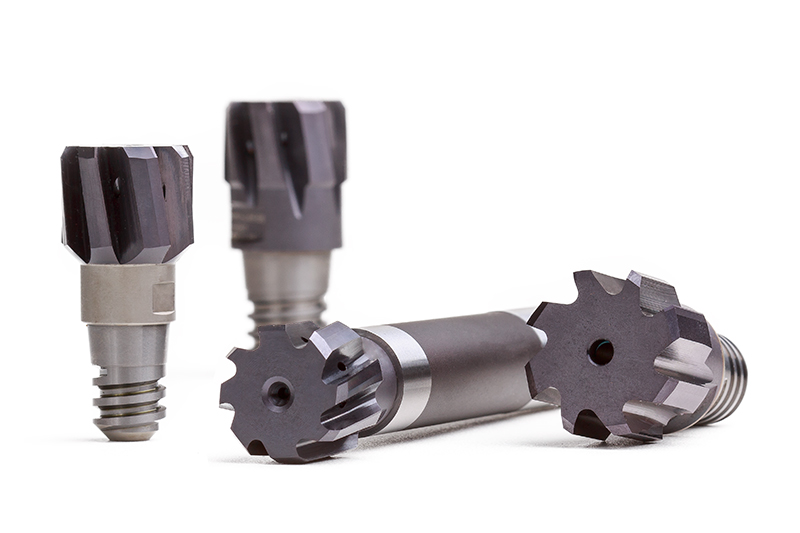
  • CPReam – CPR

    Replaceable head reamer 

    • Taper and face connection provide the greatest possible stability and rigidity
    • Highly precise radial run-out accuracy of 5 μm
    • Easy to handle
    • Ø area: 8.00 – 40.00 mm

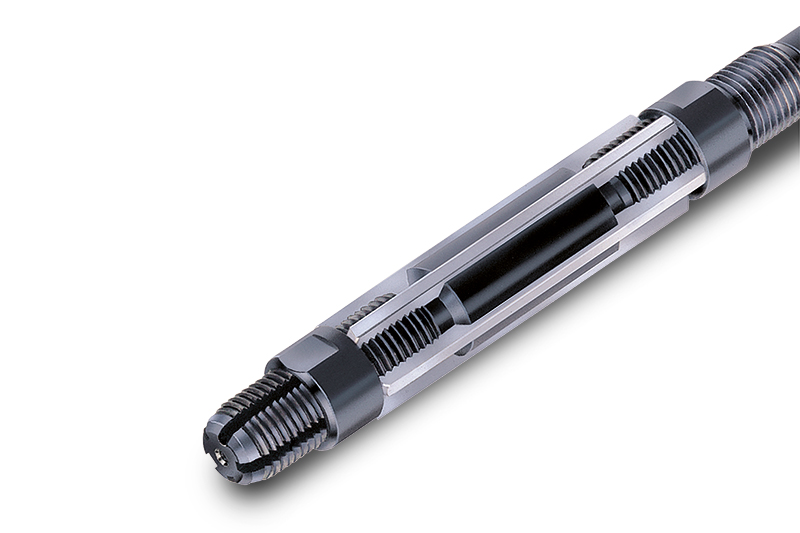
  • Quick adjustment reamer – WN 50

    Hand reamers 

    • Quick-adjust reamer with wide adjustment range
    • Especially suitable for repair work
    • Spare blade sets available
    • Ø area: 6.40 – 95.00 mm 

  • Guided tools

    Tools with guide pads 

    • Highest accuracy guaranteed with the MAPAL principle
    • Guide pads directly guide the tool into the bore
    • Precision-ground indexable inserts
    • High-precision adjustment for micrometre-precise bore machining

Clamping
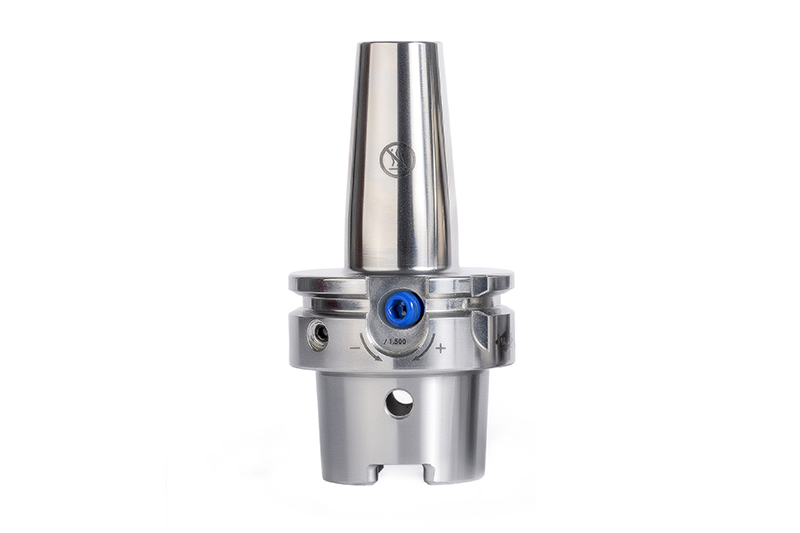
  • UNIQ DReaM Chuck, 4.5°

    Hydraulic chucks with a new design 

    • For reaming and drilling applications as well as for finishing during milling operations
    • This is achieved through an optimal interplay of geometric and functional properties
    • Outstanding surfaces as well as improved handling
    • Increasing productivity during the machining of contour-critical parts

    To the shop

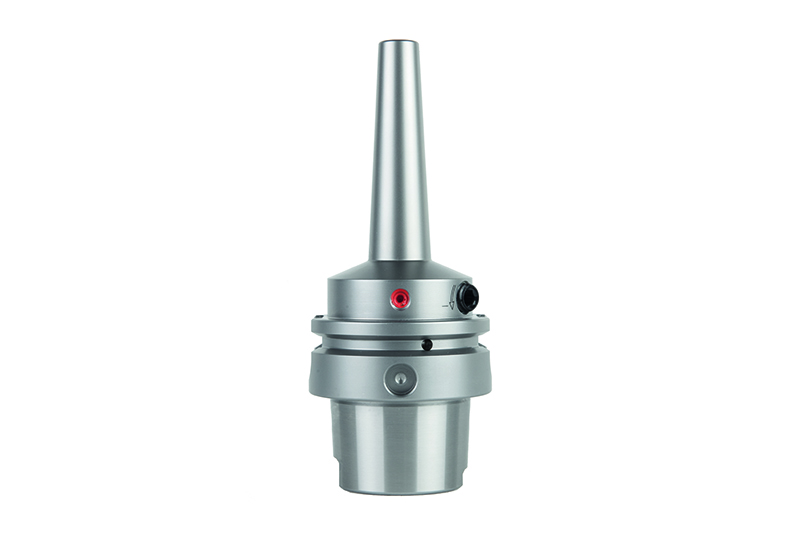
  • UNIQ Mill Chuck, HA

    Hydraulic chucks with a new design 

    • Hydraulic chuck for highly dynamic milling applications
    • This is achieved through an optimal interplay of geometric and functional properties
    • Excellent results when using tools with HA shanks
    • Process reliability – even on high-quality parts 

    To the shop

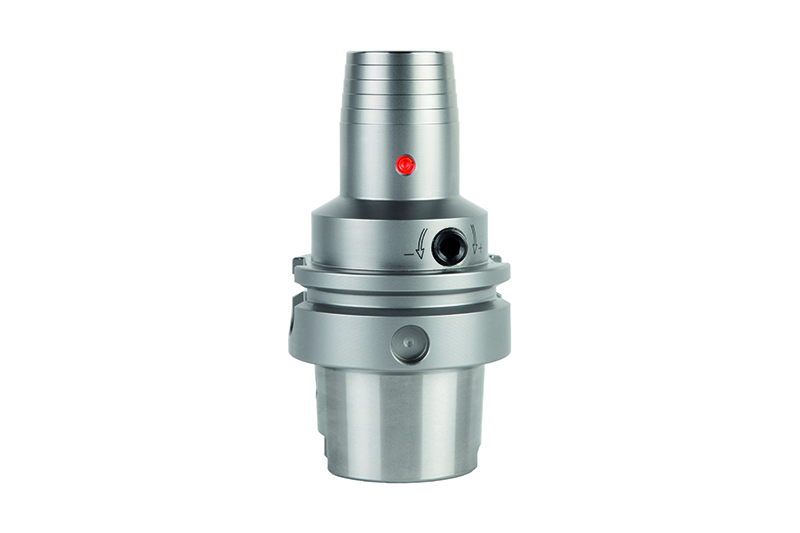
  • HighTorque Chuck HTC

    Hydraulic chuck 

    • High level of torque transmission
    • Ideal damping properties
    • Excellent rigidity of the entire system
    • Radial run-out accuracy < 3 μm
    • 3° slim design for use in contour-critical applications 


    To the shop

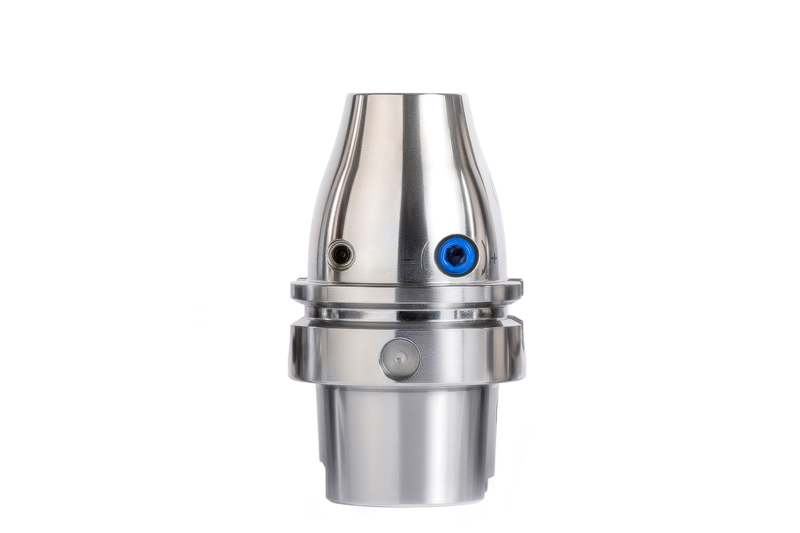
  • MAPAL HydroChuck MHC

    HydroChuck MHC

    Hydraulic chuck 

    • Excellent vibration dampening
    • High degree of radial run-out accuracy
    • Ultra-short and compact design for high rigidity


    To the shop

  • ThermoChuck MTC

    Shrink chuck 

    • Long tool life through the use of high-temperature tool steel 
    • High torque transmission and radial rigidity
    • Precision balanced as standard
    • MQL-suitable
    • With and without axial tool length adjustment 


    To the shop

  • MAPAL MillChuck

    Mill Chuck, System HB

    Side lock chuck
    • Easy to handle thanks to use of a differential screw
    • Maximum cost-effectiveness and precision
    • Axial tool positioning can be defined using spring system
    • Decentralised coolant outlets for maximum process reliability


    To the shop

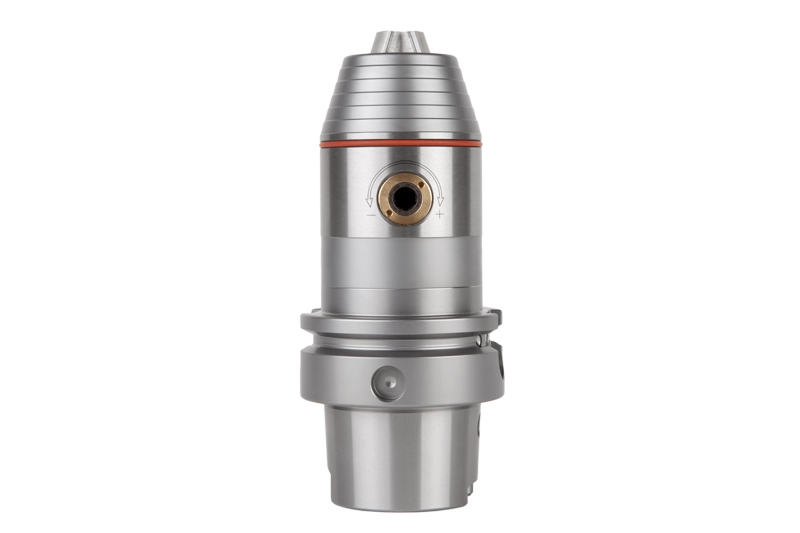
  • MAPAL Precision-DrillChuck MPC

    Precision-DrillChuck – MPC

    Precision drill chuck 

    • Simple construction, straightforward to handle
    • Safe clamping independent of direction of rotation
    • High degree of spindle speed strength
    • Modular design allows drill chuck heads to be used with all tool connections 

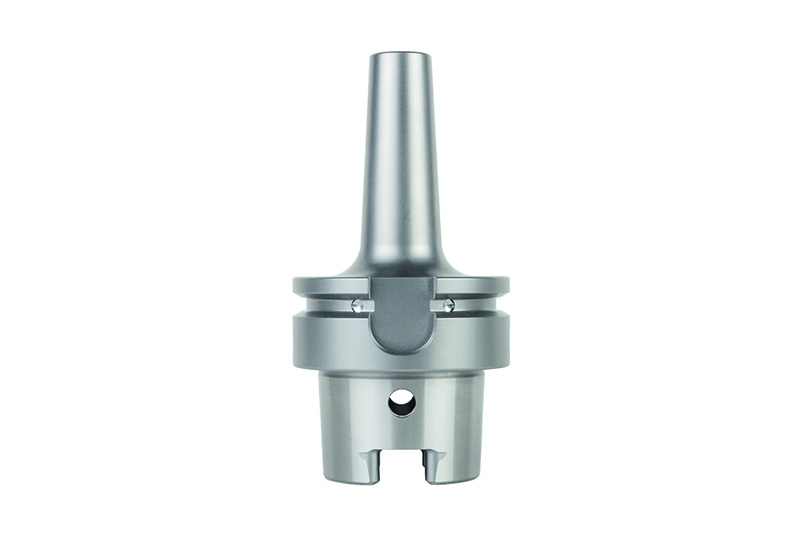
  • MAPAL slip-on reamer arbor

    Milling cutter arbor – MDA / MCA

    Milling cutter arbor 

    • Vibration-cancelling design (MDA) with vibration dampening system
    • Adapted to the rigidity of all common machine types
    • Smooth, stable running despite long projections delivers better surface finish
    • Milling cutter arbor (MCA) with large face connection for roughing and pre-finishing operations in large diameter ranges

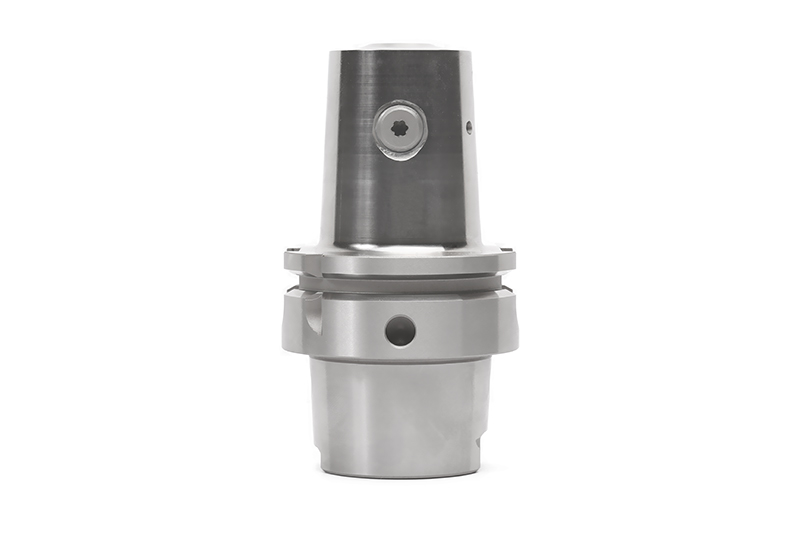
  • MAPAL MFS milling head holder

    MFS milling head holder

    Tool adapter for screw-in milling cutter 

    • Simple and fast clamping of screw-in milling cutters
    • Exact interaction of taper and face connection
    • Greatest possible stability and rigidity
    • Universally deployable for roughing and finishing operations

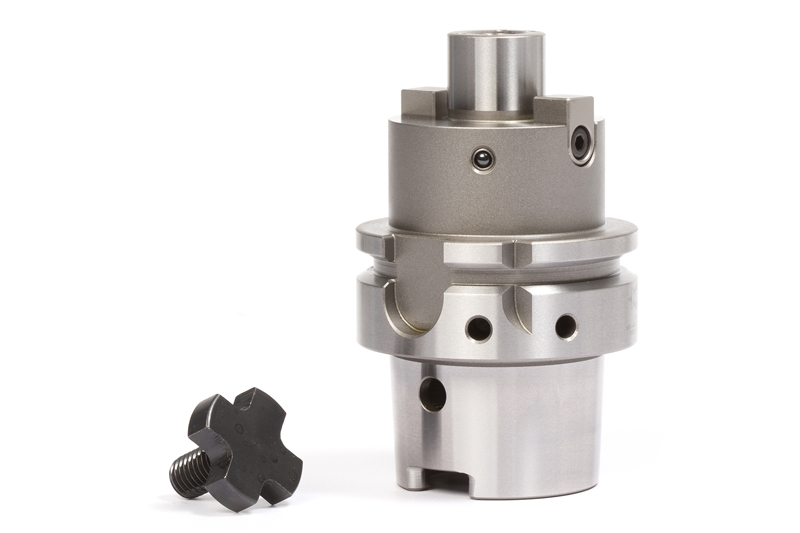
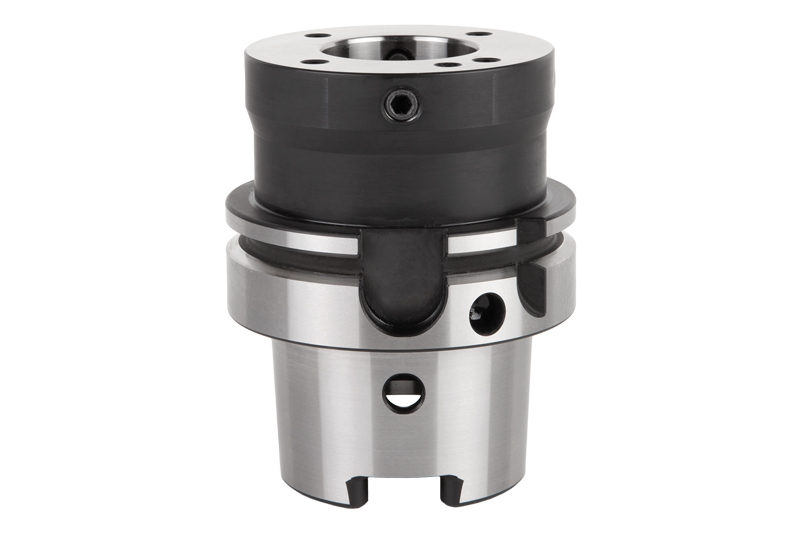
  • MAPAL HSK adapter

    Adapter

    Extensions, reducers and adapters 

    • Wide range of options for modular tool systems
    • Hydraulic extensions and tool extensions for thermal expanding chucks
    • HSK reducers and extensions
    • KS steep taper adapter


    To the shop


Components and workpiece material


From the unmachined to the finished part

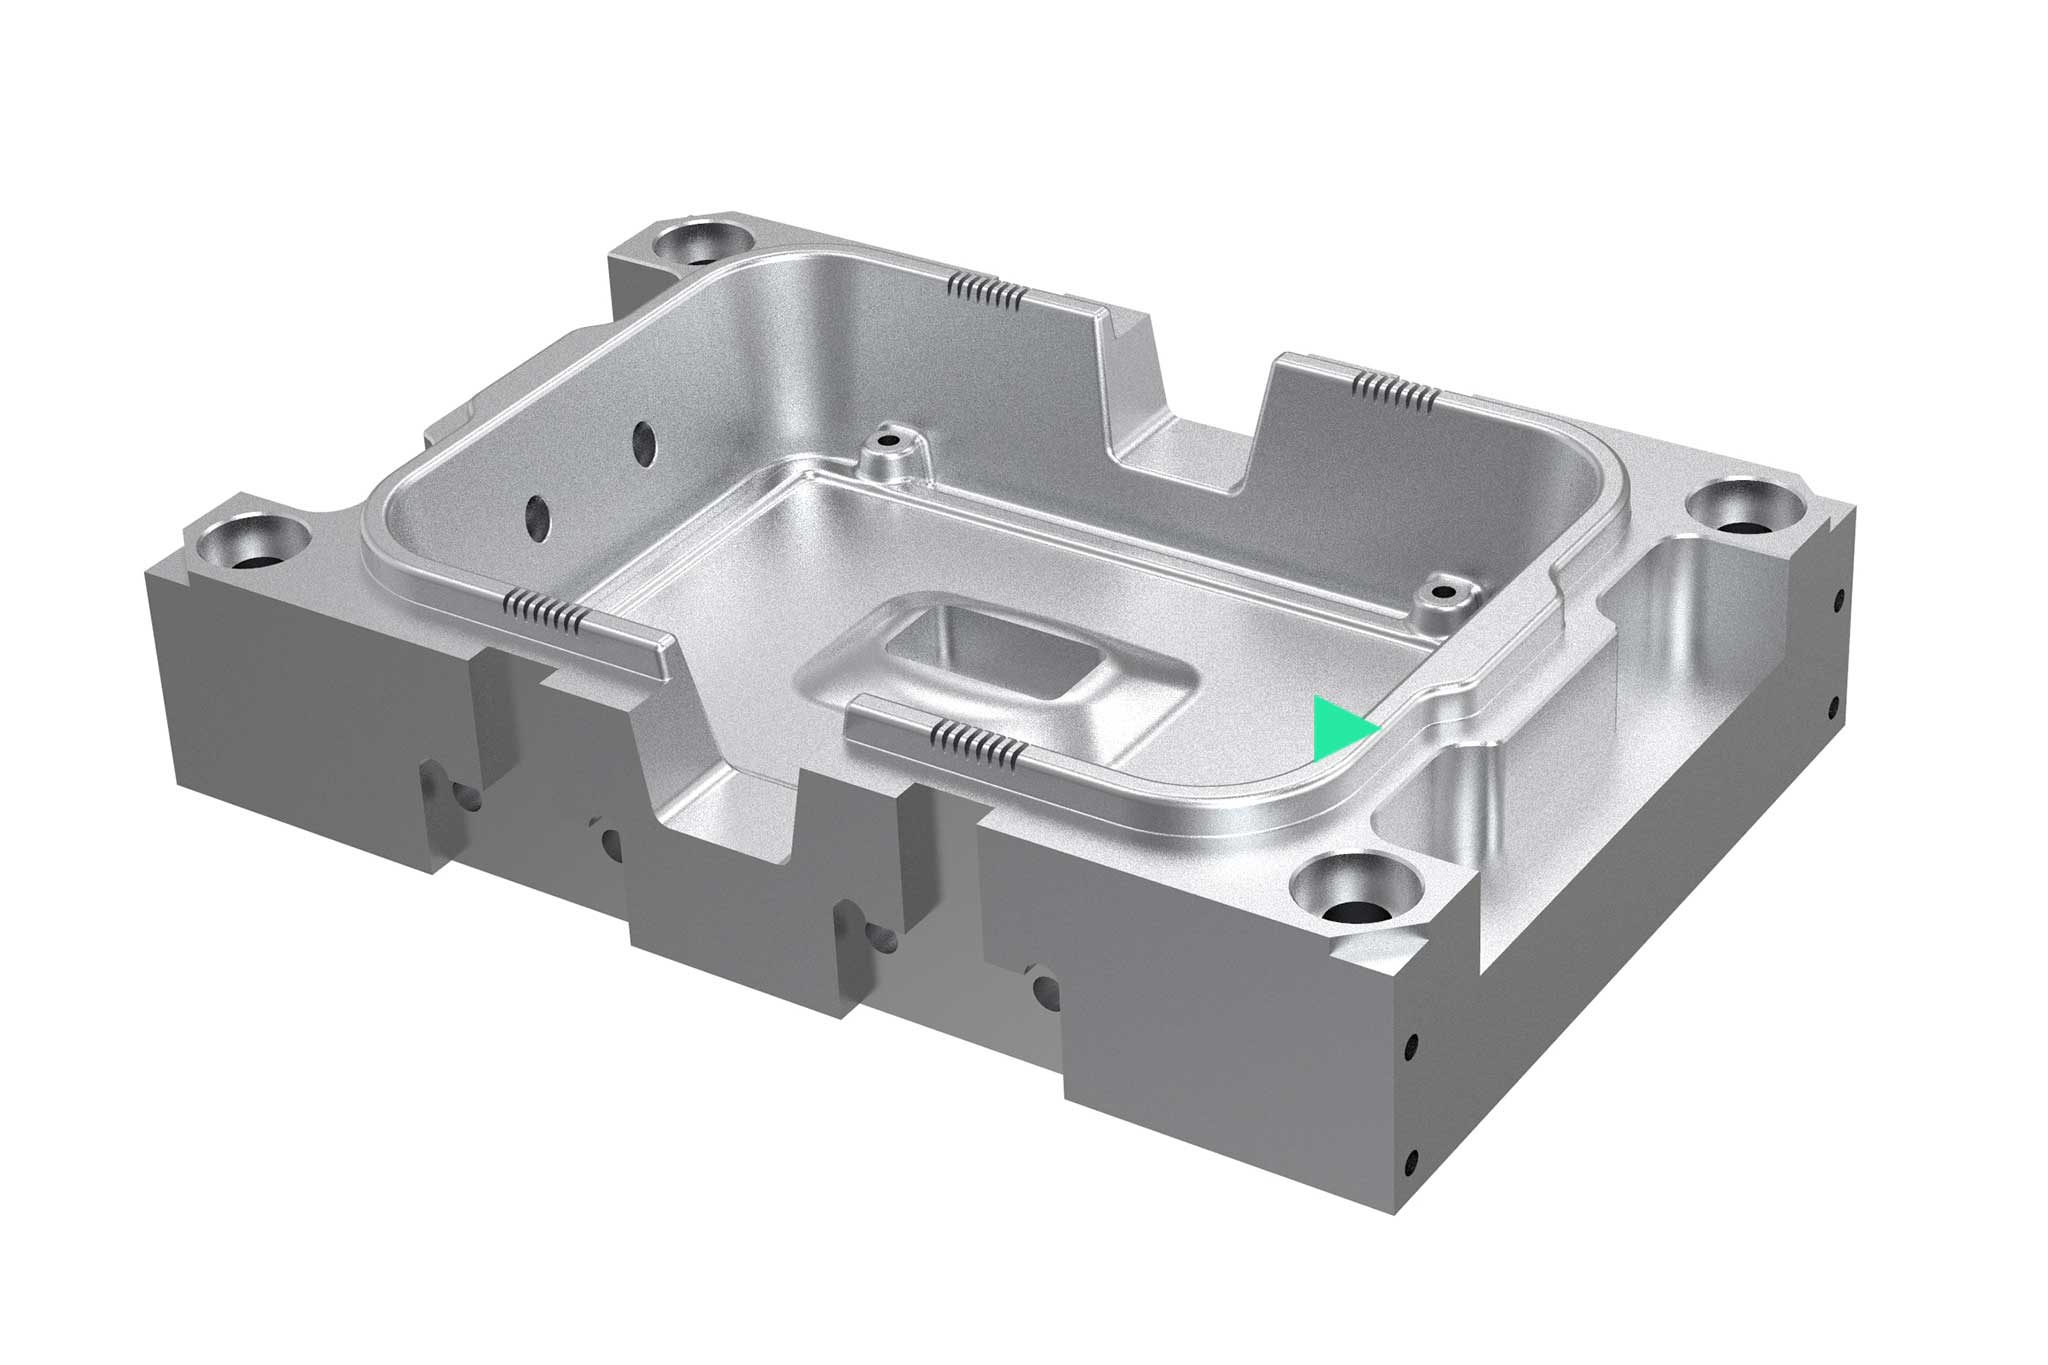
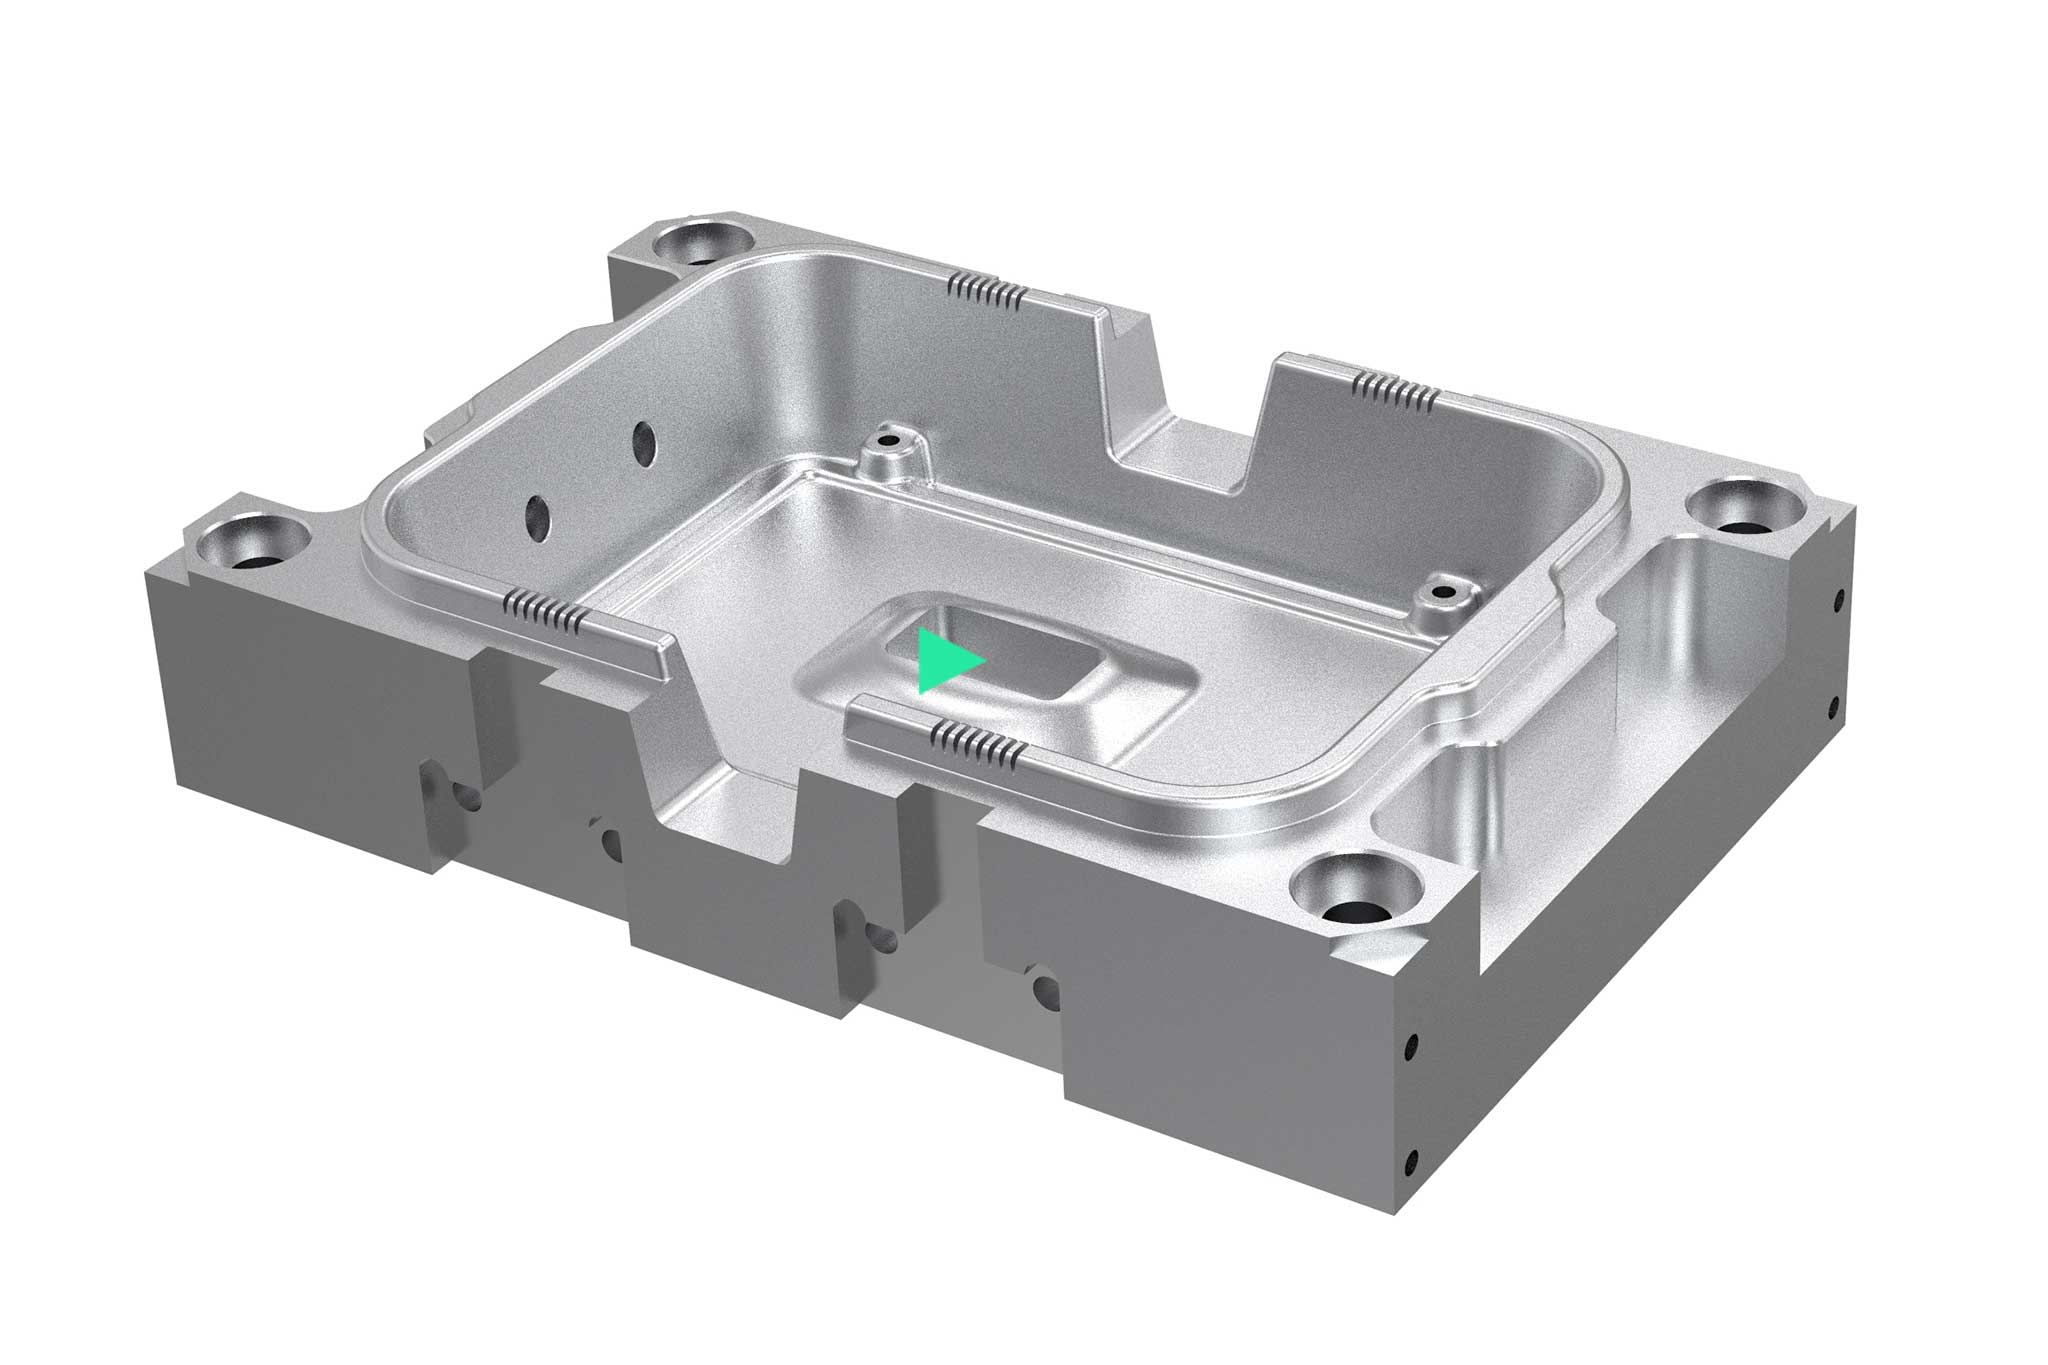
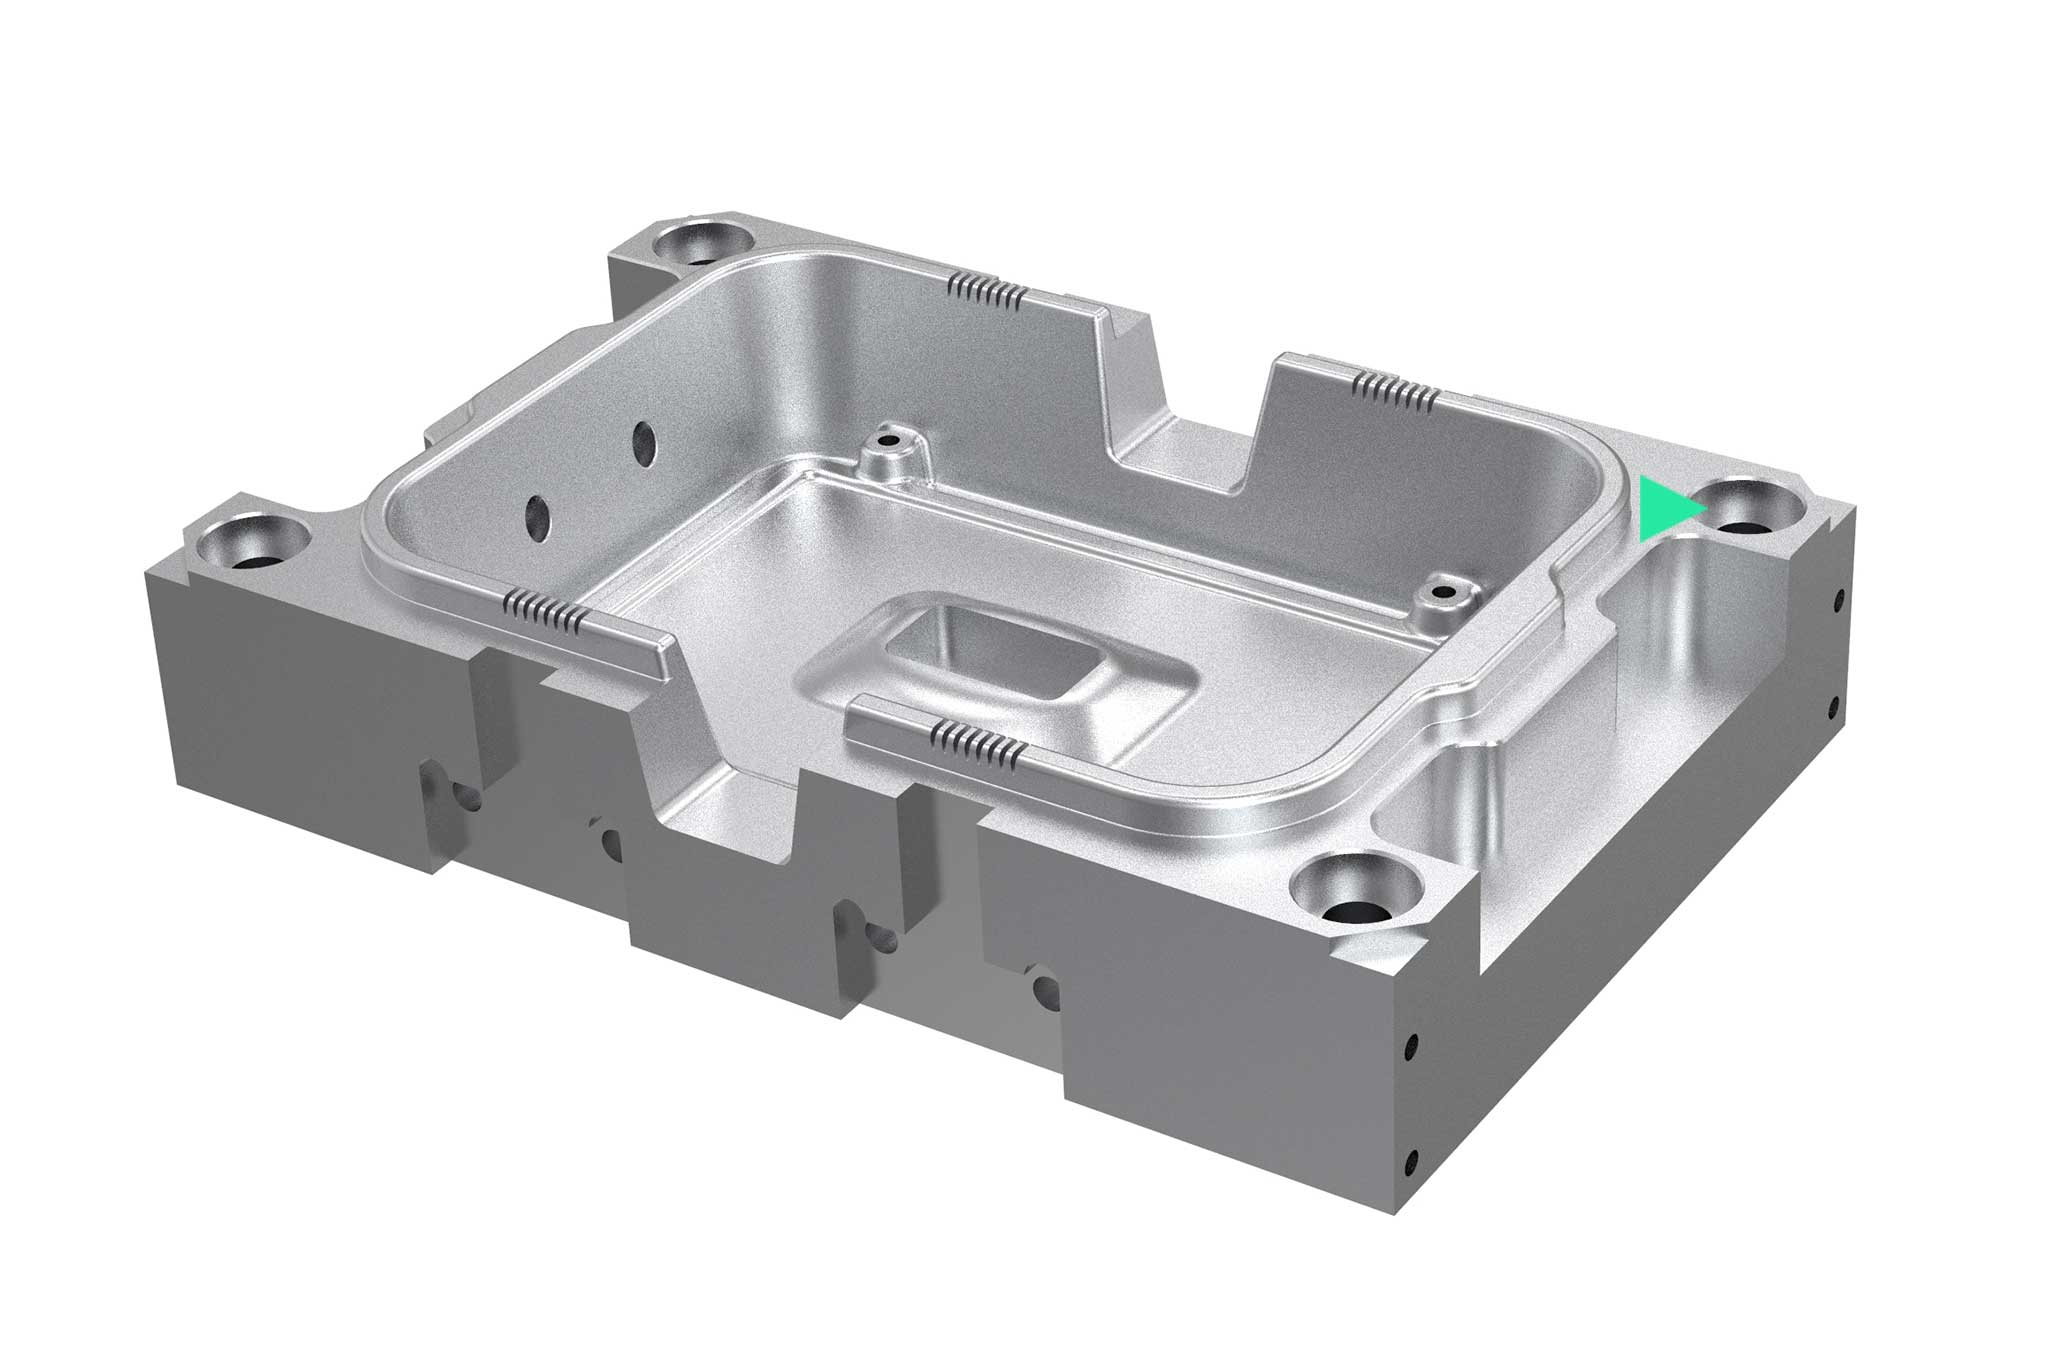
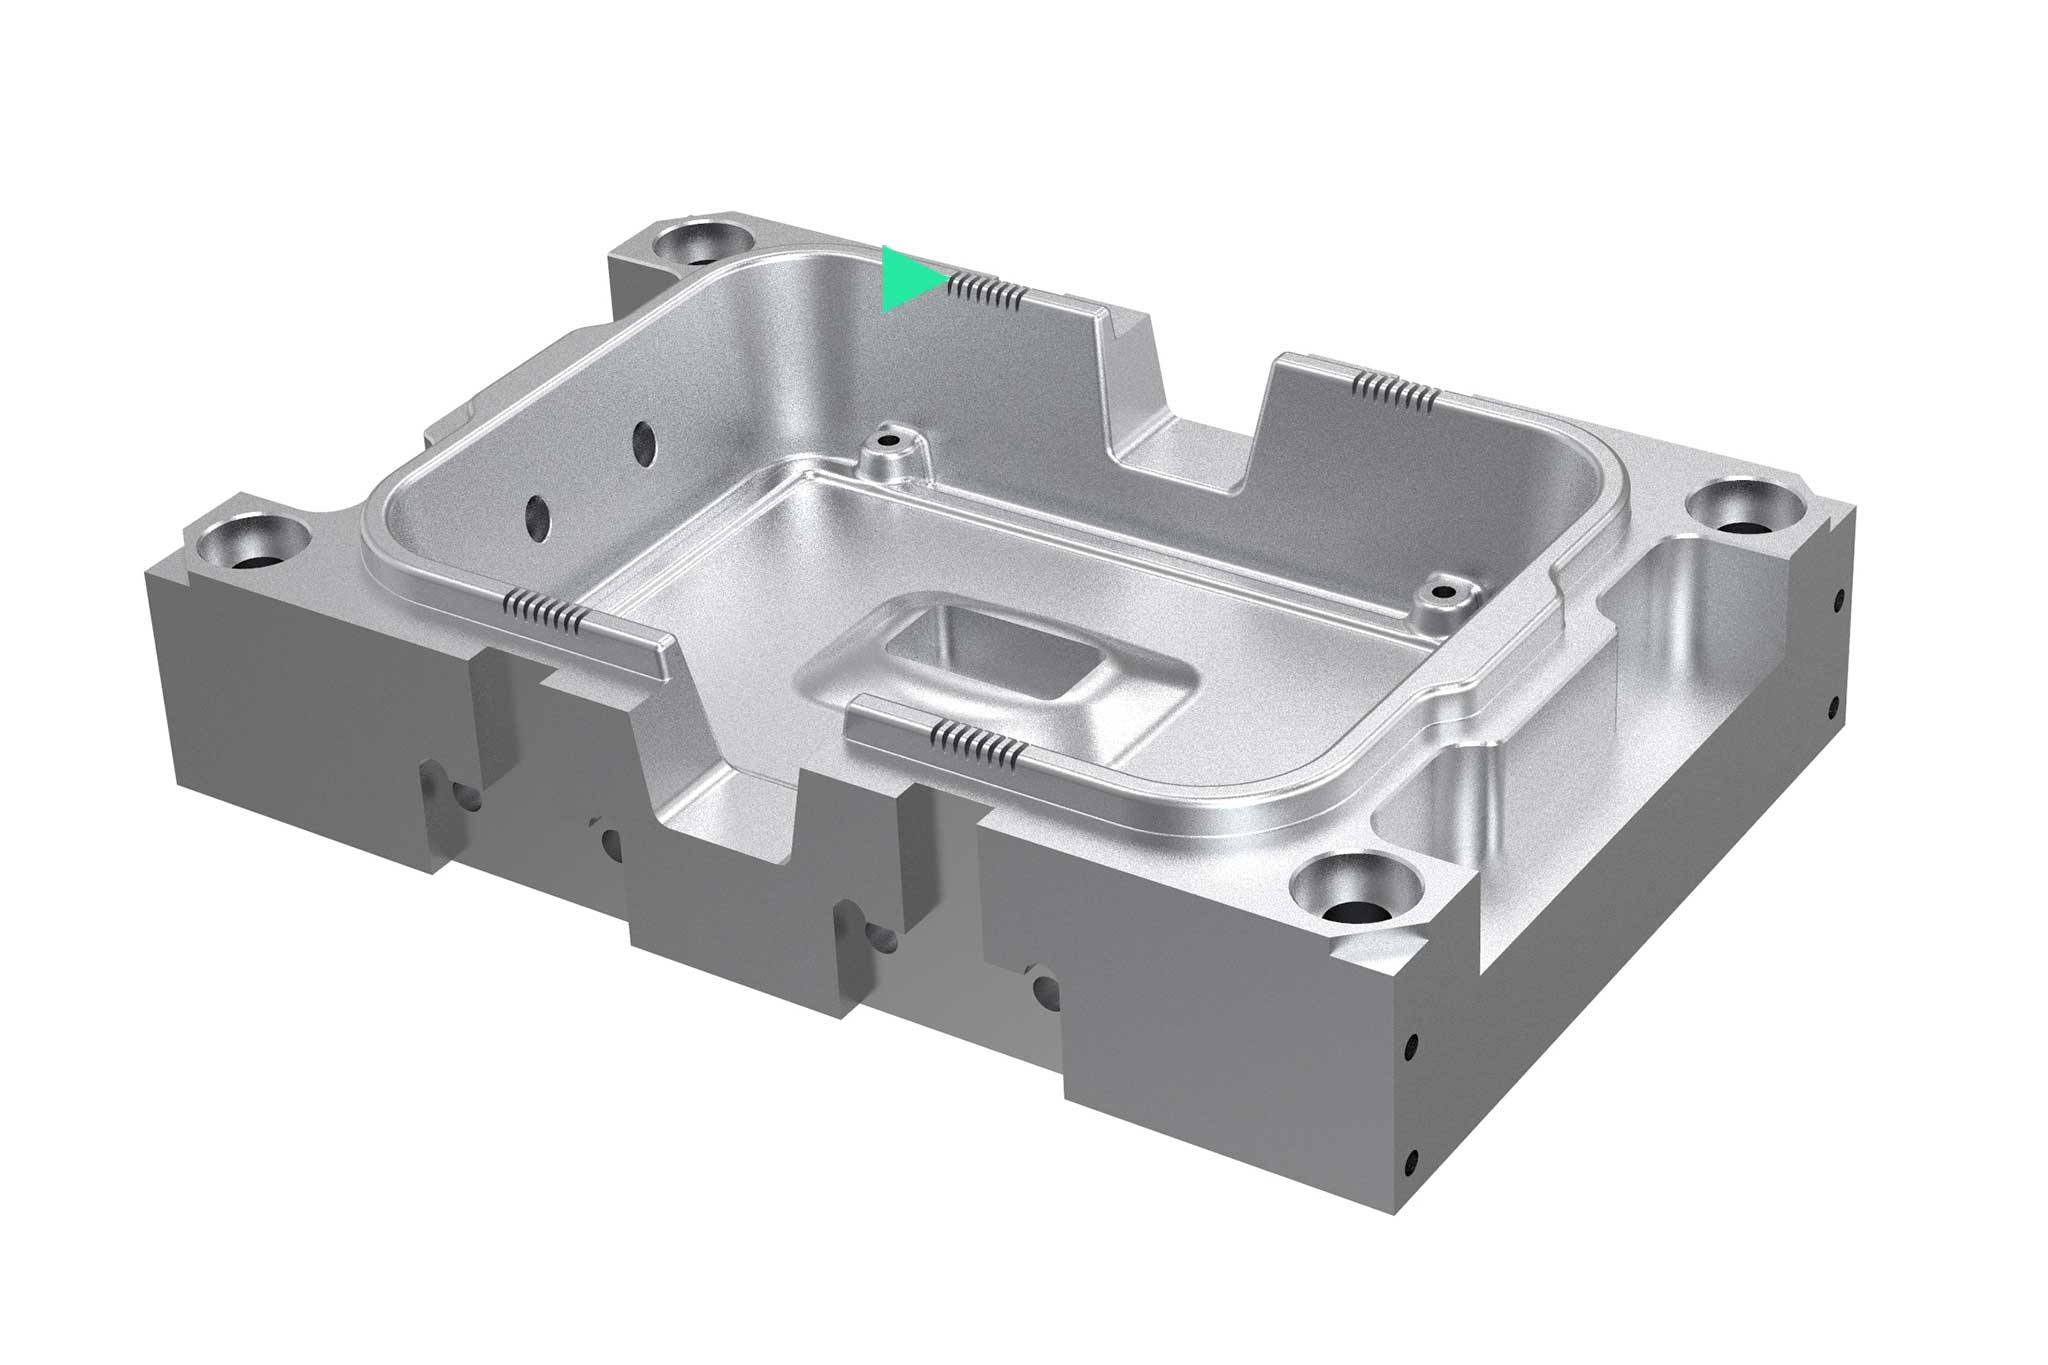
Find the right tool with just a few clicks: Depending on the machining, the specific operation and the tool requirement, you can quickly find the tool you want.
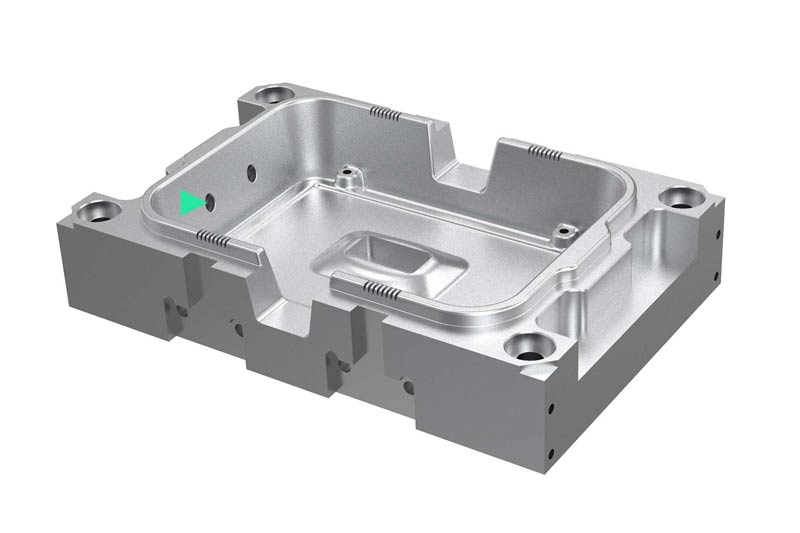
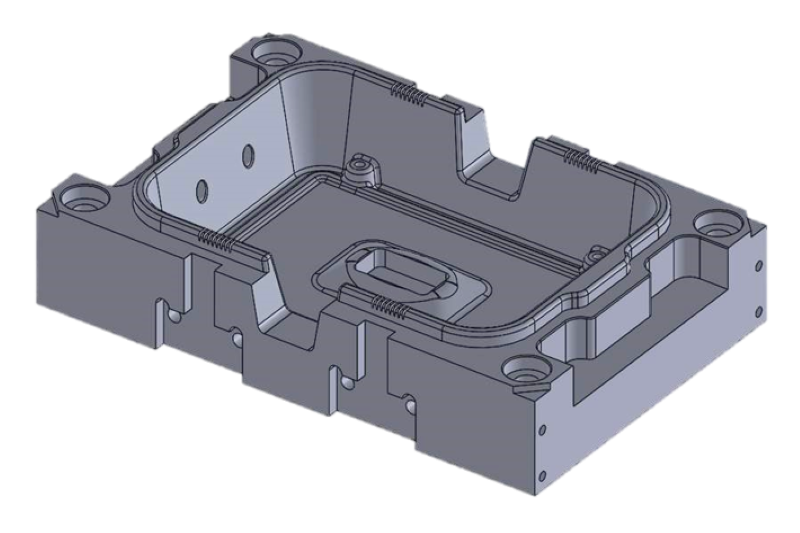
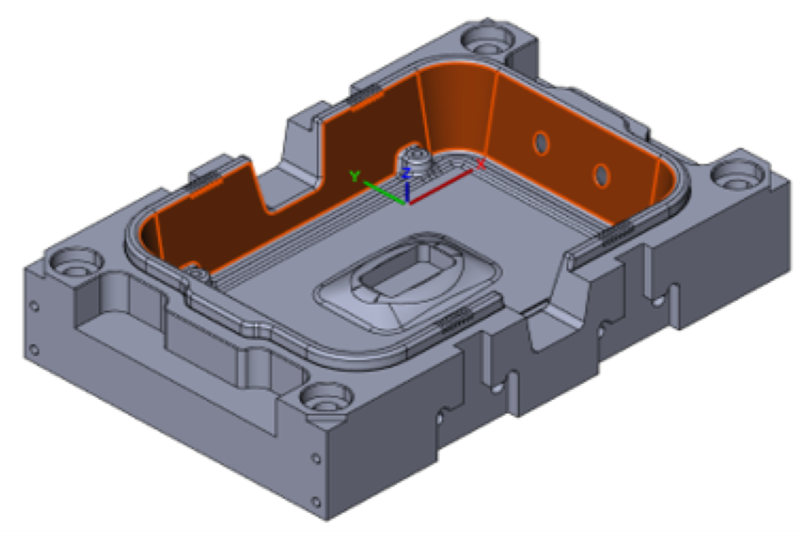
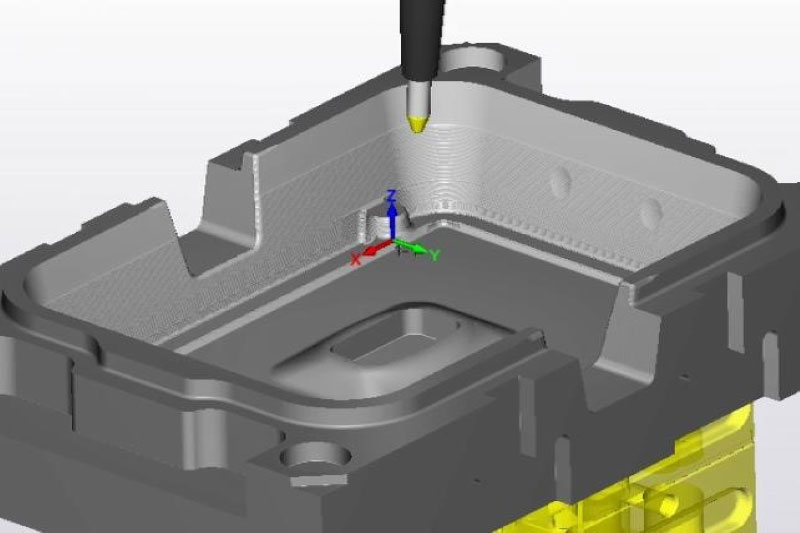
  • On a rendered example component, an operation is highlighted.
    1 / 8

    Superficies en 2D

    En esta categoría se incluyen los procesos de mecanizado ejecutados directamente en la máquina como el fresado plano, fresado de cajeras y paredes rectas. También el trabajo en geometrías complejas que se pueden programar con un software CAM.

    Acerca de la gama de productos del mecanizado de superficies en 2D
  • On a rendered example component, an operation is highlighted.
    2 / 8

    Superficies en 3D

    En los sectores de la fabricación de moldes y troqueles, los moldes complejos forman parte del día a día. El desarrollo continuo de las máquinas-herramienta y del software CAM mantienen en aumento el nivel del rendimiento y la productividad. Por eso, las herramientas usadas también deben cumplir siempre los requisitos de la última generación. Para alcanzar los mejores resultados, hay que analizar el proceso al comienzo del diseño.

    Acerca de la gama de productos del mecanizado de superficies en 3D
  • On a rendered example component, an operation is highlighted.
    3 / 8

    Cajeras abiertas

    Los insertos de molde representan también las tareas de mecanizado necesarias para el moldeo o diversos componentes. Cada vez más, los usuarios mecanizan las cajeras abiertas (mecanizado de volumen) con fresado trocoidal. Este sistema de mecanizado facilita que se mejoren los tiempos de mecanizado y prolonguen la duración de la herramienta.

    Acerca de la gama de productos del mecanizado de cajeras abiertas
  • On a rendered example component, an operation is highlighted.
    4 / 8

    Cajeras cerradas

    Las cajeras cerradas suelen fabricarse con desbastado a escala Z. Normalmente, se elige para ello el fresado de la entrada de mecanizado por medio de una rampa. La elección de la herramienta dependerá del grosor de las paredes y de la inclinación de moldeado del componente. La amplia gama de MAPAL de sistemas modulares también abarca el mecanizado de cajeras profundas de gran diámetro.

    Acerca de la gama de productos del mecanizado de cajeras cerradas
  • On a rendered example component, an operation is highlighted.
    5 / 8

    Fresado helicoidal

    Uno de los puntos importantes de los mecanizados de fresado es reducir el tiempo de mecanizado. Normalmente, con formas de herramienta específicas para el mecanizado se consigue eliminar el proceso de taladrado previo de las cajeras cerradas y redondas. En el fresado helicoidal se programan trayectorias de fresado con entradas helicoidales adecuadas para las dimensiones de las cajeras.

    Acerca de la gama de productos de fresado helicoidal
  • On a rendered example component, an operation is highlighted.
    6 / 8

    Superficies planas

    Tratar de lograr superficies planas es muy habitual en los distintos campos de la fabricación de moldes y troqueles: ya sea porque lo requiere el componente, la estrategia por medio del mecanizado de fresado correspondiente o por medio de los requisitos de superficies de cierre de molde, así como secciones y troquelados. Por tanto, la herramienta adecuada se elegirá en función del uso y de los requisitos.

    Acerca de la gama de productos del mecanizado de superficies planas
  • On a rendered example component, an operation is highlighted.
    7 / 8

    Paredes finas y nervaduras

    Los moldes de plástico por inyección y los moldes de fundición de presión suelen tener nervaduras y paredes finas. Por ejemplo, cada vez se fresan más nervaduras, porque dicho proceso es más rentable que el proceso EDM (electroerosión). Por norma general, se usan herramientas de metal duro largas o extralargas de diámetro pequeño. En estos casos, también se pueden emplear las soluciones específicas de cada cliente (RibCutter) correspondientes a la forma de la nervadura.

    Acerca de la gama de productos del mecanizado de paredes y nervaduras finas
  • On a rendered example component, an operation is highlighted.
    8 / 8

    Agujeros pequeños y grandes

    En los sectores de la fabricación de moldes y troqueles hay infinidad de procesos de taladrado en macizo: Por ejemplo, grandes perforaciones en columnas guía, perforaciones profundas para sistemas de refrigeración o perforaciones de gran precisión para pasadores expulsores. Para cada uno de los pasos de fabricación, MAPAL ofrece una amplia variedad de herramientas de taladrado y escariado.

    Acerca de la gama de productos del mecanizado de agujeros pequeños y grandes

Todo de un solo proveedor

  • 1. Planificación y adquisición

    Para una clara organización de las existencias de herramientas es importante también una gestión de compra optimizada.

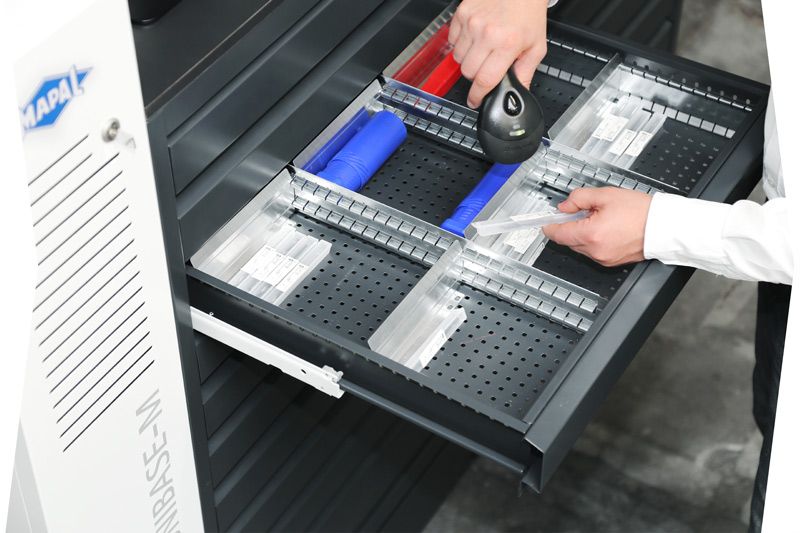
  • 2. Logística de herramientas

    Rentabilidad incluso en la periferia del mecanizado: los sistemas inteligentes de distribución reducen los tiempos improductivos de manera significativa.

  • 3. Ingeniería

    Los especialistas en mecanizado asisten en la ingeniería del proceso, por ejemplo, con simulaciones CAM, asesoramiento general y elaboración de estrategias rentables de mecanizado.

  • 4. Medición y ajuste

    Los dispositivos de ajuste y medición fiables impresionan por su precisión y fácil manejo durante el ajuste de las herramientas.

  • 5. Herramientas y técnica de sujeción

    Desde el husillo hasta la cuchilla: MAPAL ofrece un amplio catálogo de herramientas y técnica de sujeción para la fabricación de moldes y troqueles.

  • 6. Mecanizado

    Procesos de mecanizado eficientes y estrategias de mecanizado adaptadas al máximo nivel tecnológico.

  • 7. Digitalización y automatización

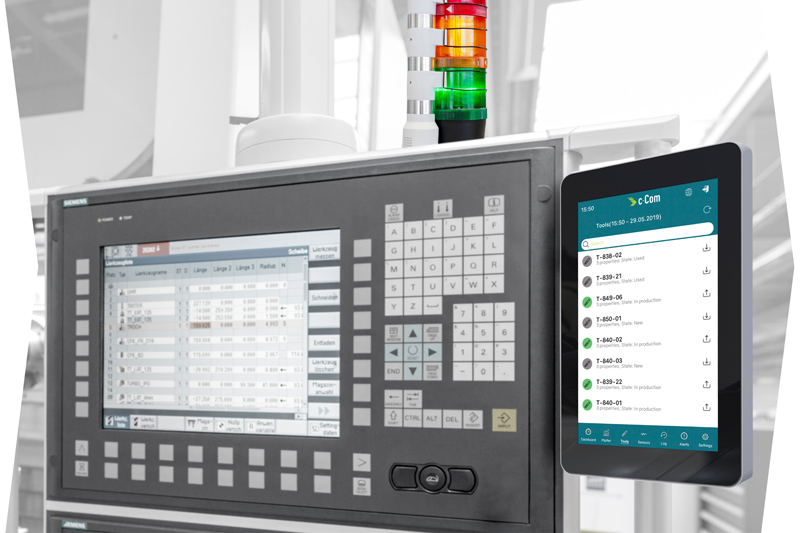
    Digitalización fácil y rápida: la c-Connect Box transmite digitalmente los datos de medición del dispositivo de ajuste a la máquina herramienta. Además, entre otras cuestiones, supervisa el estado de la máquina.

  • 8. Reacondicionamiento

    En muy poco tiempo los clientes reciben sus herramientas reacondicionadas en la calidad de fabricante. Si se solicita, también hay servicio de recogida y entrega.


Flujo de trabajo de ingeniería: de la teoría a la práctica

El reto de MAPAL es encontrar la solución perfecta para satisfacer las necesidades de los clientes. Aparte de las soluciones especiales de cada uno y una amplia gama estándar de productos, prestamos una gran variedad de servicios para organizar de forma óptima desde la concepción del producto hasta la última viruta del proceso al completo. Los clientes podrán confiar en la dilatada experiencia en el sector del mecanizado de este líder tecnológico.
  • 3D model of a workpiece from the die and mould making.

    1. Customer enquiry

    MAPAL sales representatives are directly available for individual enquiries. In a personal conversation with the customer, they sound out the specific requirements and the scope (complete or partial machining) and discuss the details directly on the 3D model of the component.

    The MAPAL die & mould team looks forward to your enquiry by ​​​​​​​Email and will contact you directly as soon as possible.

  • 3D model of a workpiece from the die and mould making.

    2. Project analysis

    On the basis of 3D models and machine data, the conversation partners analyse the manufacturing tasks and develop effective machining strategies.

    The project analysis consists of the following:​​​​​​​
    • Machining suggestions for all machining steps
    • Tool list
    • Process optimisation

  • 3. Process design

    Regardless of whether the focus is on flexibility or productivity: The machining specialists simulate the developed process on the basis of the 3D models and thus show potential for optimisation. They check and improve the machining parameters in CAM programming and thus ensure stable and economical production.

    The process design includes:​​​​​​​
    • Runtime analysis of the component
    • Technology data definition
    • CAM programming

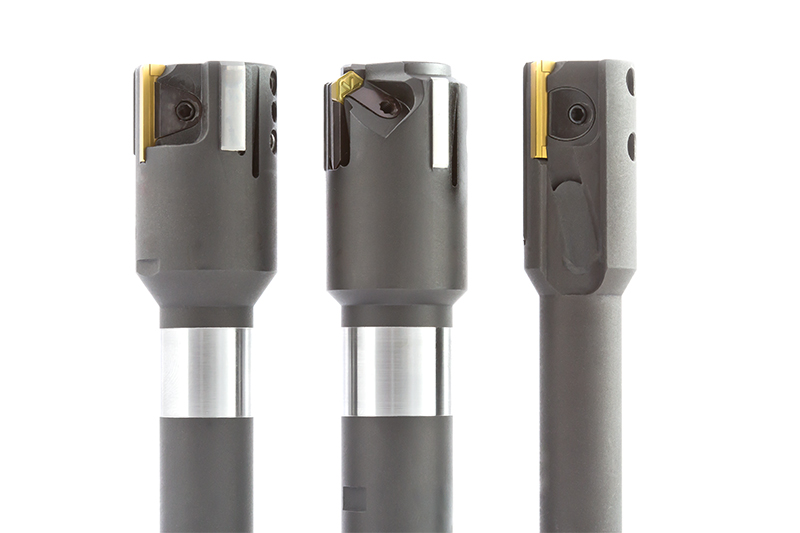
  • Overview of all MAPAL tool solutions for die and mould making in one workpiece.
    4. Tool solution

    The wide-ranging MAPAL standard range for the die & mould sector offers the ideal tool solution for every application. Customised solutions are available upon request.
    Advantages for the user:​​​​​​​
    • Broad standard range
    • Availability of tool data

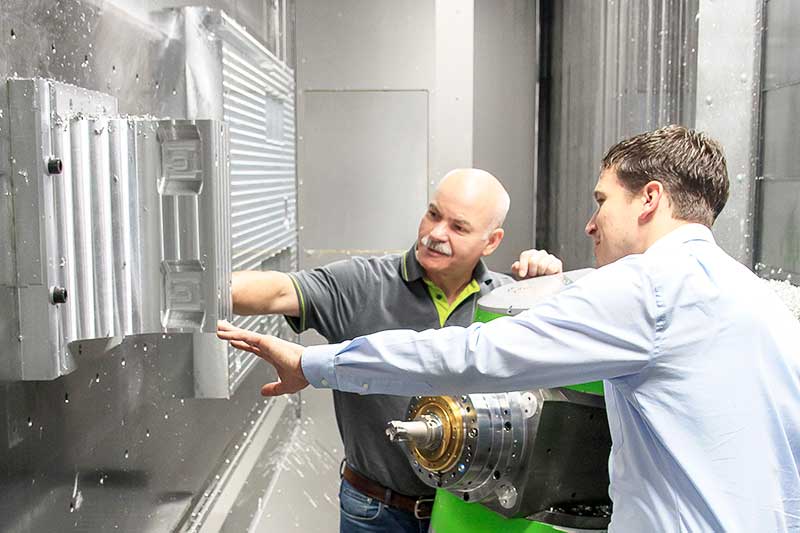
  •  The picture shows a technical advisor from MAPAL in conversation with a customer.

    5. Tool test and offer

    After discussing the machining task, MAPAL supports its customers in the selection of tools required in the process. This is the basis for a well-founded offer tailored to the respective application.

  • The picture shows documents for preparing offers on a table with three people.

    6. Cooperative partnership

    Even after mutual success, the specialists at MAPAL remain in close contact with the customer. Should optimisation potential arise over time or other tools turn out to be better, MAPAL will be happy to support you to further improve productivity and profitability.

    In order to ensure efficient production in the long term, MAPAL also offers comprehensive tool management options.
    ​​​​​​​
    Tool management options:

    • Dispensing systems
    • Regrinding service
    • Comprehensive product portfolio of adjustment and measuring devices


Weitere Artikel aus dem Bereich Formenbau


Unsere Fachhandelspartner

Zuständigkeit nach Postleitzahlen-Bereichen

  • 1 / 16

    PLZ 35

    FRITZ WEG GmbH & Co. KG
    Ahornweg 41
    35713 Eschenburg-Wissenbach

    Tel.: +49 2774 701-0
    Fax: +49 2774 701-39
    E-Mail: info@fritzweg.de
    Web: www.fritzweg.de

  • 2 / 16

    PLZ 44

    Jansen Schneidwerkzeuge Vertriebs GmbH
    Im Käsebrink 12
    58840 Plettenberg

    Tel.: +49 2391 9177-0
    Fax: +49 2391 9177-20
    E-Mail: info@j-s-v.com
    Web: www.j-s-v.com

  • 3 / 16

    PLZ 51

    Jansen Schneidwerkzeuge Vertriebs GmbH
    Im Käsebrink 12
    58840 Plettenberg

    Tel.: +49 2391 9177-0
    Fax: +49 2391 9177-20
    E-Mail: info@j-s-v.com
    Web: www.j-s-v.com

  • 4 / 16

    PLZ 56, 57

    FRITZ WEG GmbH & Co. KG
    Ahornweg 41
    35713 Eschenburg-Wissenbach

    Tel.: +49 2774 701-0
    Fax: +49 2774 701-39
    E-Mail: info@fritzweg.de
    Web: www.fritzweg.de

  • 5 / 16

    PLZ 58, 59

    Jansen Schneidwerkzeuge Vertriebs GmbH
    Im Käsebrink 12
    58840 Plettenberg

    Tel.: +49 2391 9177-0
    Fax: +49 2391 9177-20
    E-Mail: info@j-s-v.com
    Web: www.j-s-v.com

  • 6 / 16

    PLZ 60, 61

    Heinrich Meier GmbH
    Herrenwaag 31
    75417 Mühlacker

    Tel.: +49 7041 9530-0
    Fax: +49 7041 9530-30
    E-Mail: info@heinrich-meier.de
    Web: www.heinrich-meier.de

  • 7 / 16

    PLZ 63 - 69

    Heinrich Meier GmbH
    Herrenwaag 31
    75417 Mühlacker

    Tel.: +49 7041 9530-0
    Fax: +49 7041 9530-30
    E-Mail: info@heinrich-meier.de
    Web: www.heinrich-meier.de

  • 8 / 16

    PLZ 70 - 73

    Dieter Schätzle GmbH & Co. KG
    Präzisionswerkzeuge
    Unter Haßlen 12
    78532 Tuttlingen

    Tel.: +49 7462 9465-0
    Fax: +49 7462 9465-50
    E-Mail: info@schaetzle-werkzeuge.de
    Web:​​​​​​​ www.schaetzle-werkzeuge.de

  • 9 / 16

    PLZ 74, 75

    Heinrich Meier GmbH
    Herrenwaag 31
    75417 Mühlacker

    Tel.: +49 7041 9530-0
    Fax: +49 7041 9530-30
    E-Mail: info@heinrich-meier.de
    Web: www.heinrich-meier.de

  • 10 / 16

    PLZ 76 - 79

    Dieter Schätzle GmbH & Co. KG
    Präzisionswerkzeuge
    Unter Haßlen 12
    78532 Tuttlingen

    Tel.: +49 7462 9465-0
    Fax: +49 7462 9465-50
    E-Mail: info@schaetzle-werkzeuge.de
    Web:​​​​​​​ www.schaetzle-werkzeuge.de

  • 11 / 16

    PLZ 80 - 87

    AB1-Tools e.K.
    Goethering 45
    91732 Merkendorf

    Tel.: +49 9826 333-2241
    Fax: +49 9826 333-3691
    E-Mail: info@ab1-tools.com
    Web: www.ab1-tools.com

  • 12 / 16

    PLZ 88, 89

    Dieter Schätzle GmbH & Co. KG
    Präzisionswerkzeuge
    Unter Haßlen 12
    78532 Tuttlingen

    Tel.: +49 7462 9465-0
    Fax: +49 7462 9465-50
    E-Mail: info@schaetzle-werkzeuge.de
    Web:​​​​​​​ www.schaetzle-werkzeuge.de

  • 13 / 16

    PLZ 90 - 97

    AB1-Tools e.K.
    Goethering 45
    91732 Merkendorf

    Tel: +49 9826 333-2241
    Fax: +49 9826 333-3691
    E-Mail: info@ab1-tools.com
    Web: www.ab1-tools.com

  • 14 / 16

    Dänemark

    EDECO TOOL APS 
    Naverland 2
    2600 Glostrup
    Danmark

    Tel.: +45 7060 2029
    E-Mail: info@edeco.dk
    Web: www.edeco.dk

  • 15 / 16

    Italien

    TEKNOS S.r.l.
    Via A. Pigafetta, 2
    35011 Campodarsego (PD)
    Italia

    Tel.: +39 049 8877061
    E-Mail: info@teknositalia.it
    Web: www.teknositalia.it

  • 16 / 16

    Portugal

    Álamo-Ferramentas Unipessoal Lda
    Rua da ETAR, Lote 9
    Zona Industrial de Oiã
    3770-059 Oiã
    ​​​​​​​
    Tel.: +351 234 728-193
    E-Mail: geral@alamo-ferramentas.com
    ​​​​​
    Web: www.alamo-ferramentas.com