Drei Fräser für die Zerspanung

New innovative solutions for the HPR400 system

More productivity and process reliability with four new solutions for the HPR400 system

複雑な加工工程や高い品質要求には、効 果的で精密、そして使いやすい仕上げ加 工システムが求められます。MAPALは、 大径の高生産性リーマ加工に対応する HPR400およびHPR400 Plusによって、 まさにこれ の要求に応えています。多 刃ツールシステムには、HPR400は1枚 刃、HPR400 Plusは4枚刃のインサートを 使用。現 でお客様自身で交換できる利点 があり、高精度なインサート座により、最大 限の加工精度を確保。
MAPALは、3つの新しいソリューションを 通じて、車両製造業や油圧・空圧機器分野 のお客様に対し、要求の厳しい加工用途に 対応する未来志向のツールを提供していま す。
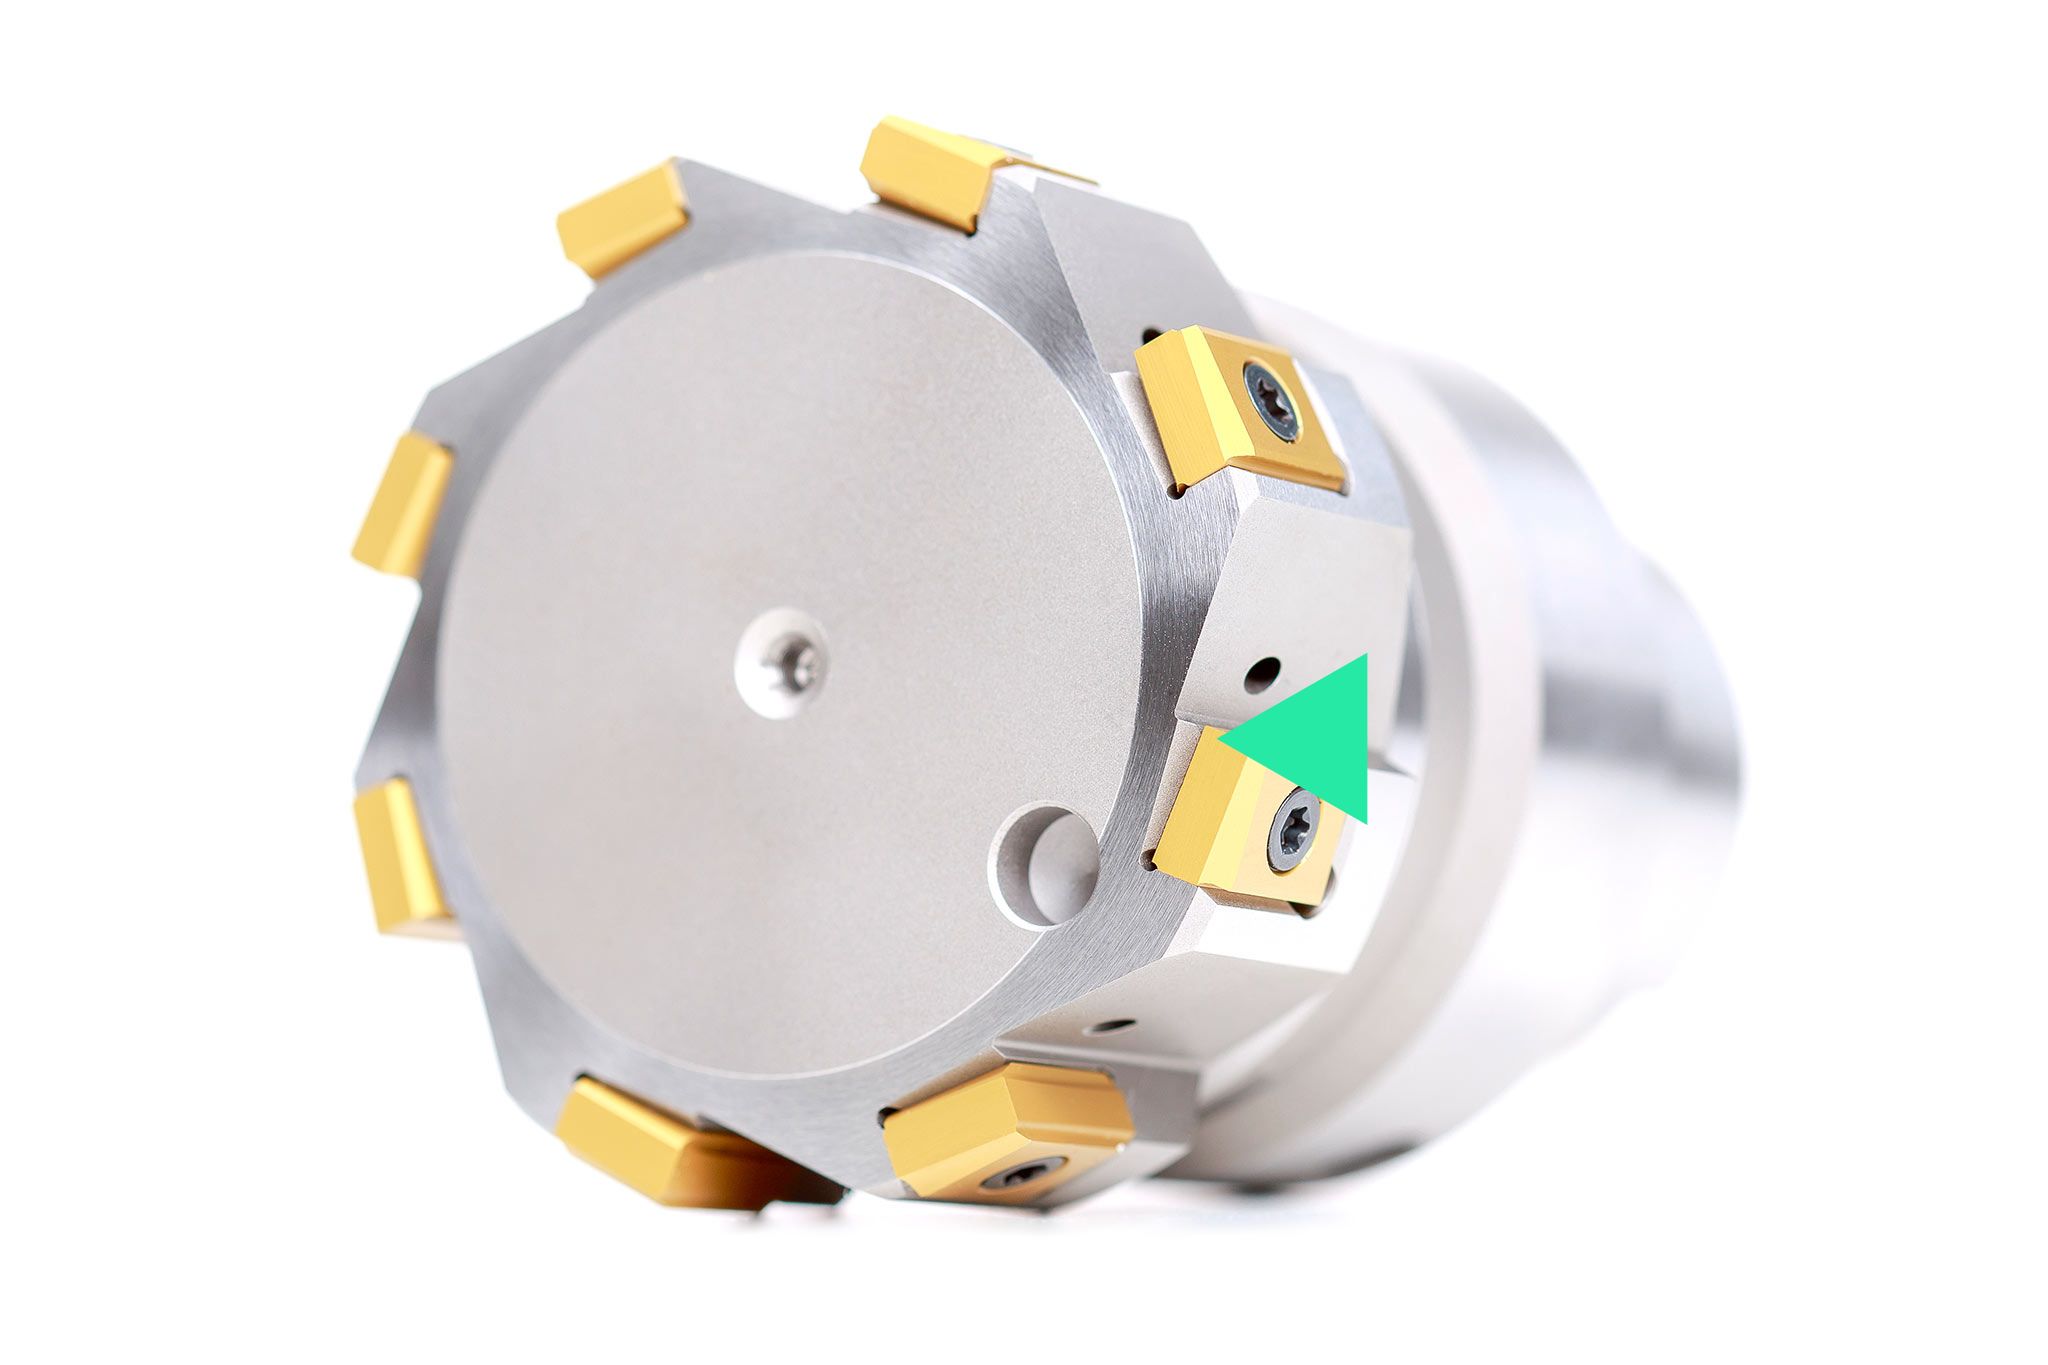
  • Photo of the HPR400 system with plug & play cutting system.
    1 / 4

    プラグ & プレイの刃先システム

    • 刃先交換時の調整不要
    • マシンのダウンタイムを短縮
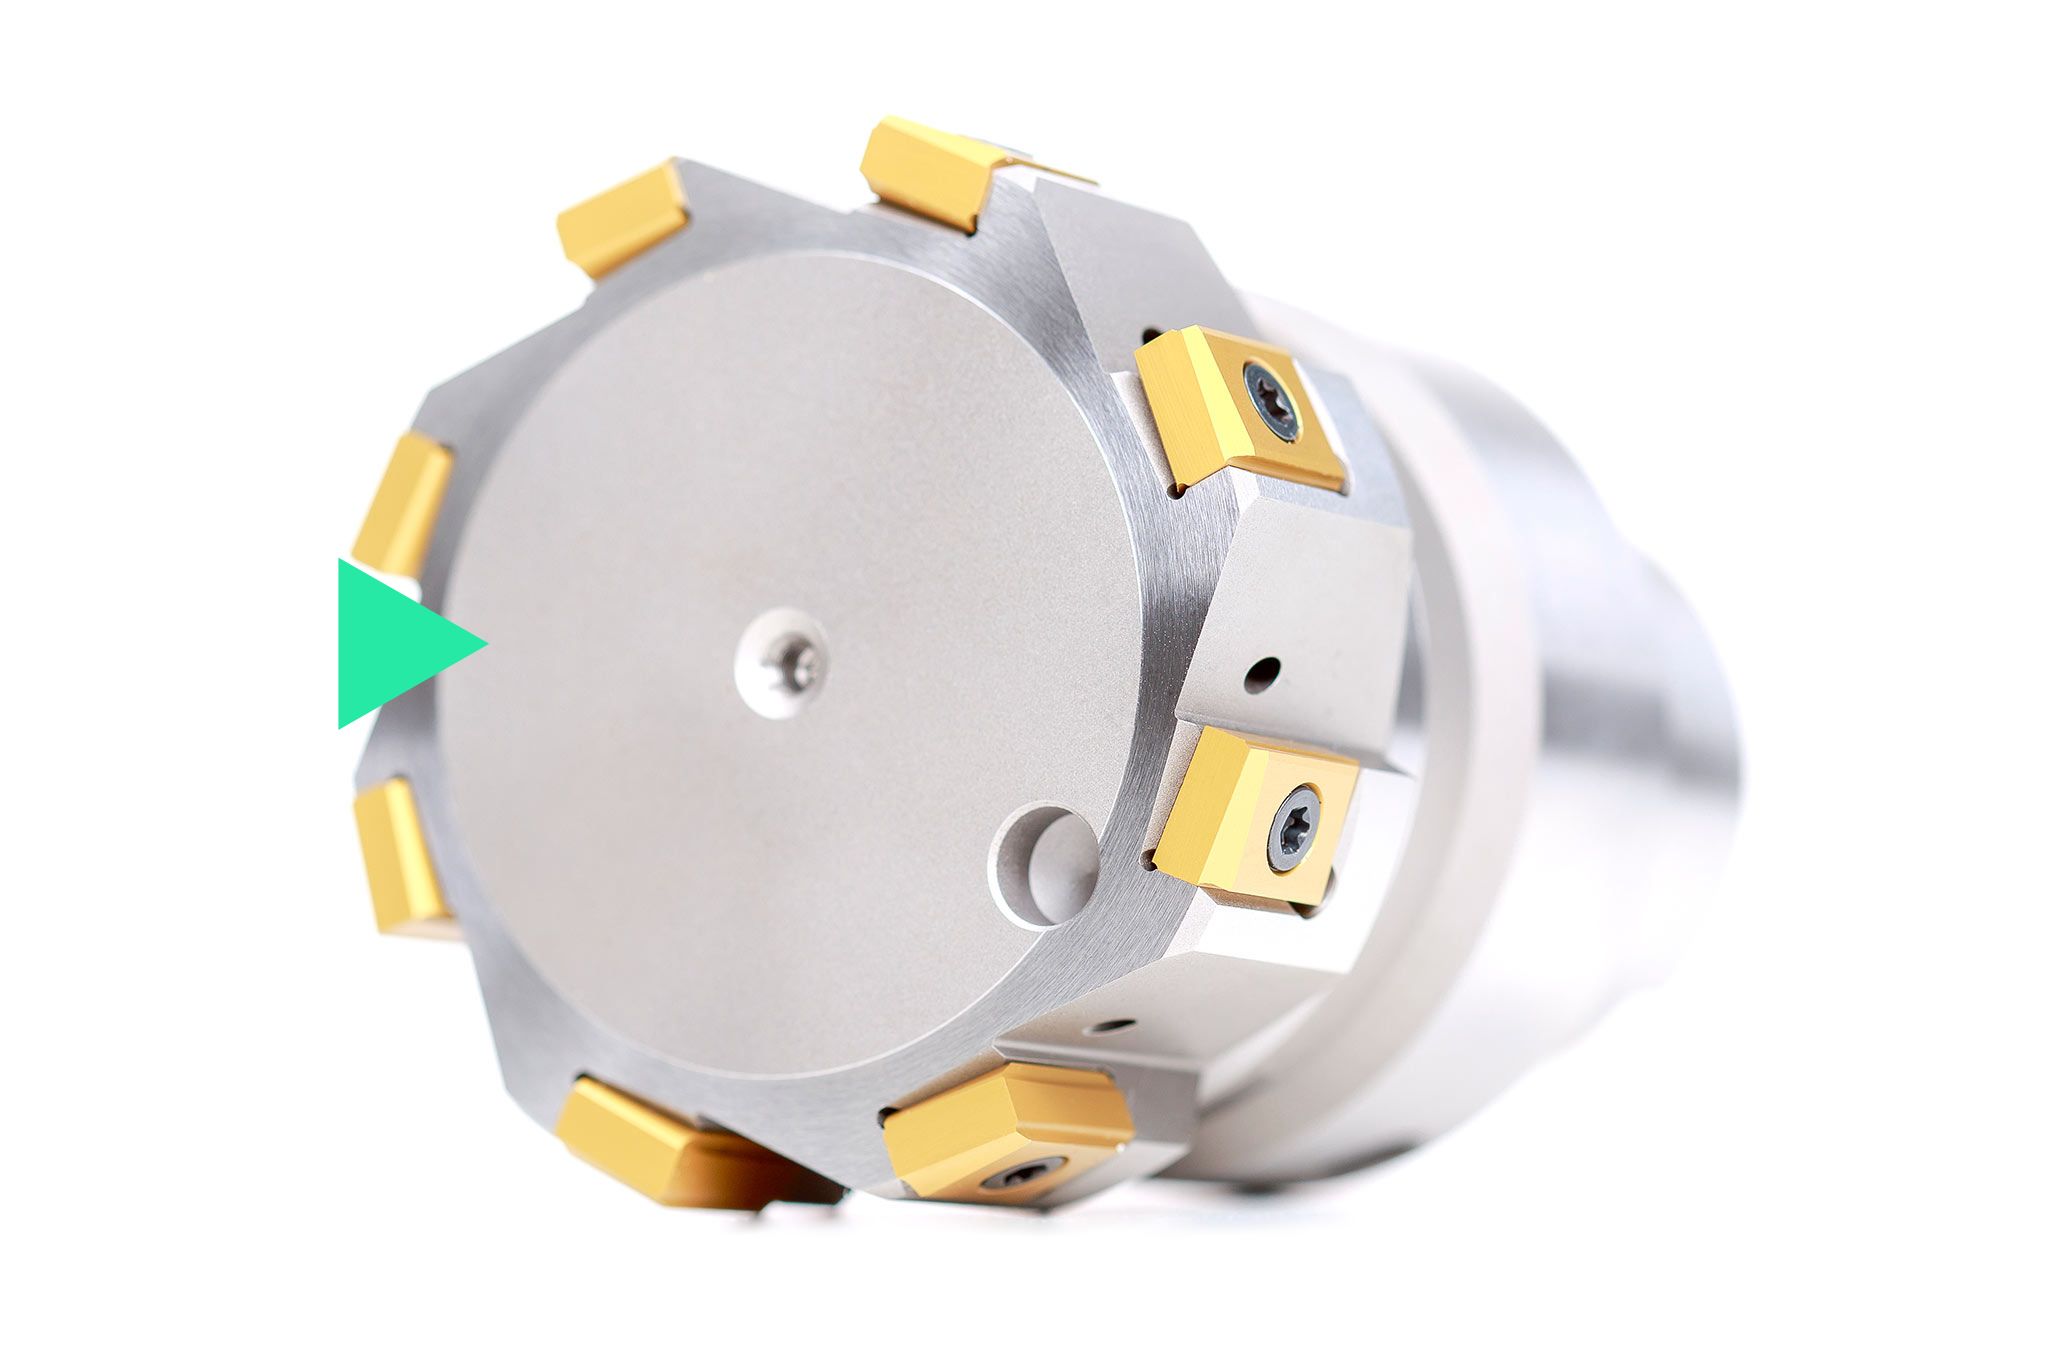
  • Photo of the HPR400 system with multi-edge design.
    2 / 4

    多刃仕様

    • 高い切削速度と送り速度を実現
    • 短縮されたサイクルタイムと 安定した品質
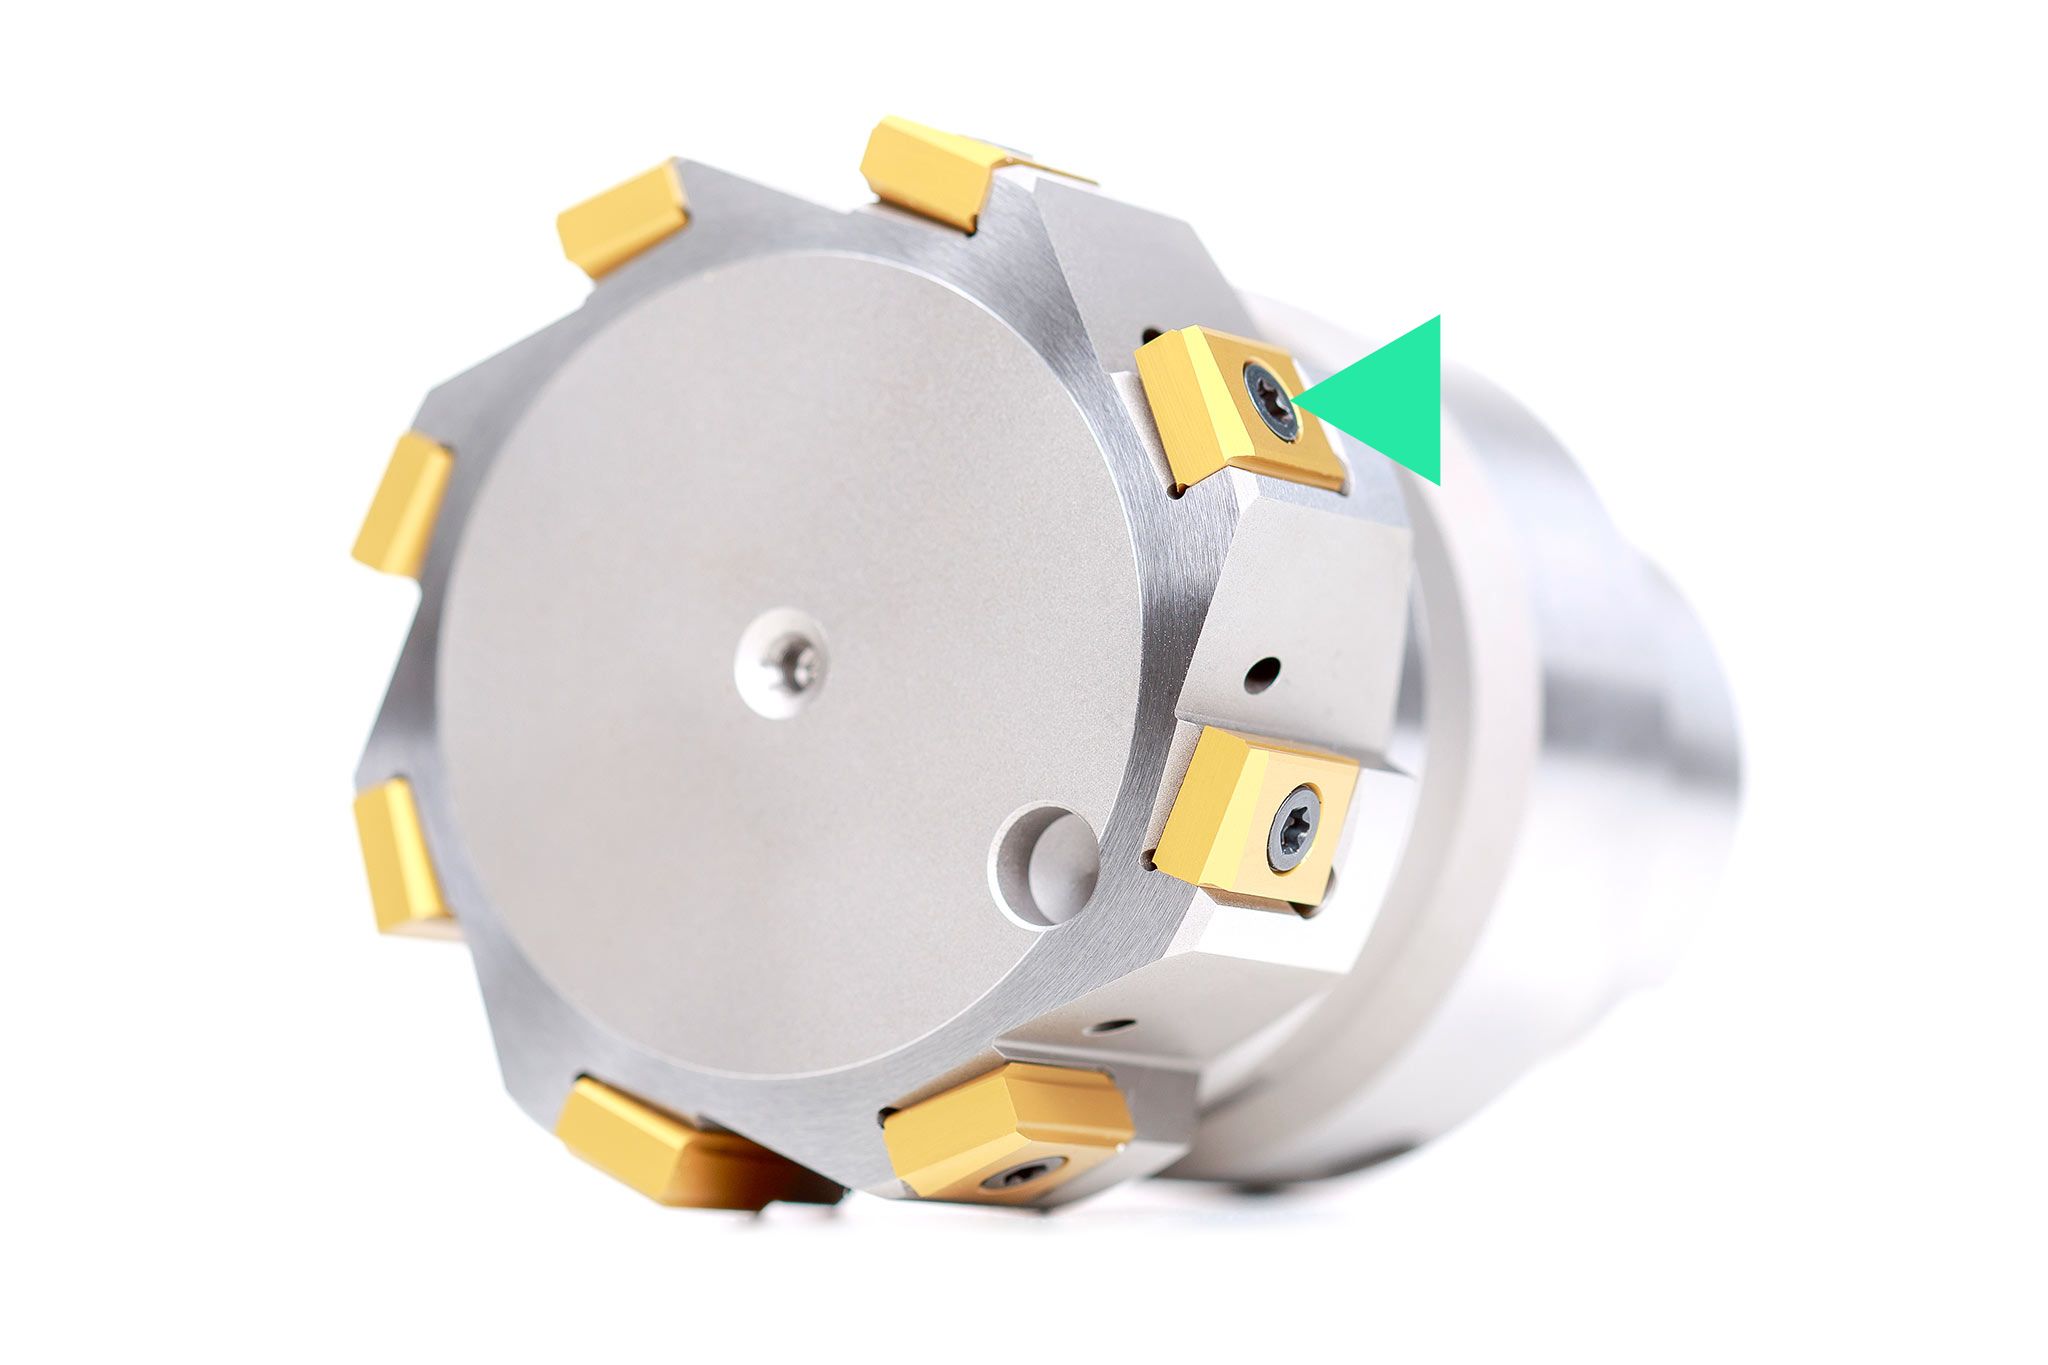
  • Photo of the HPR400 system with customizable tool configuration.
    3 / 4

    調整可能なツール構成

    • 加工内容に応じた柔軟な設計
    • 他のツールシステムとの 組み合わせも可能
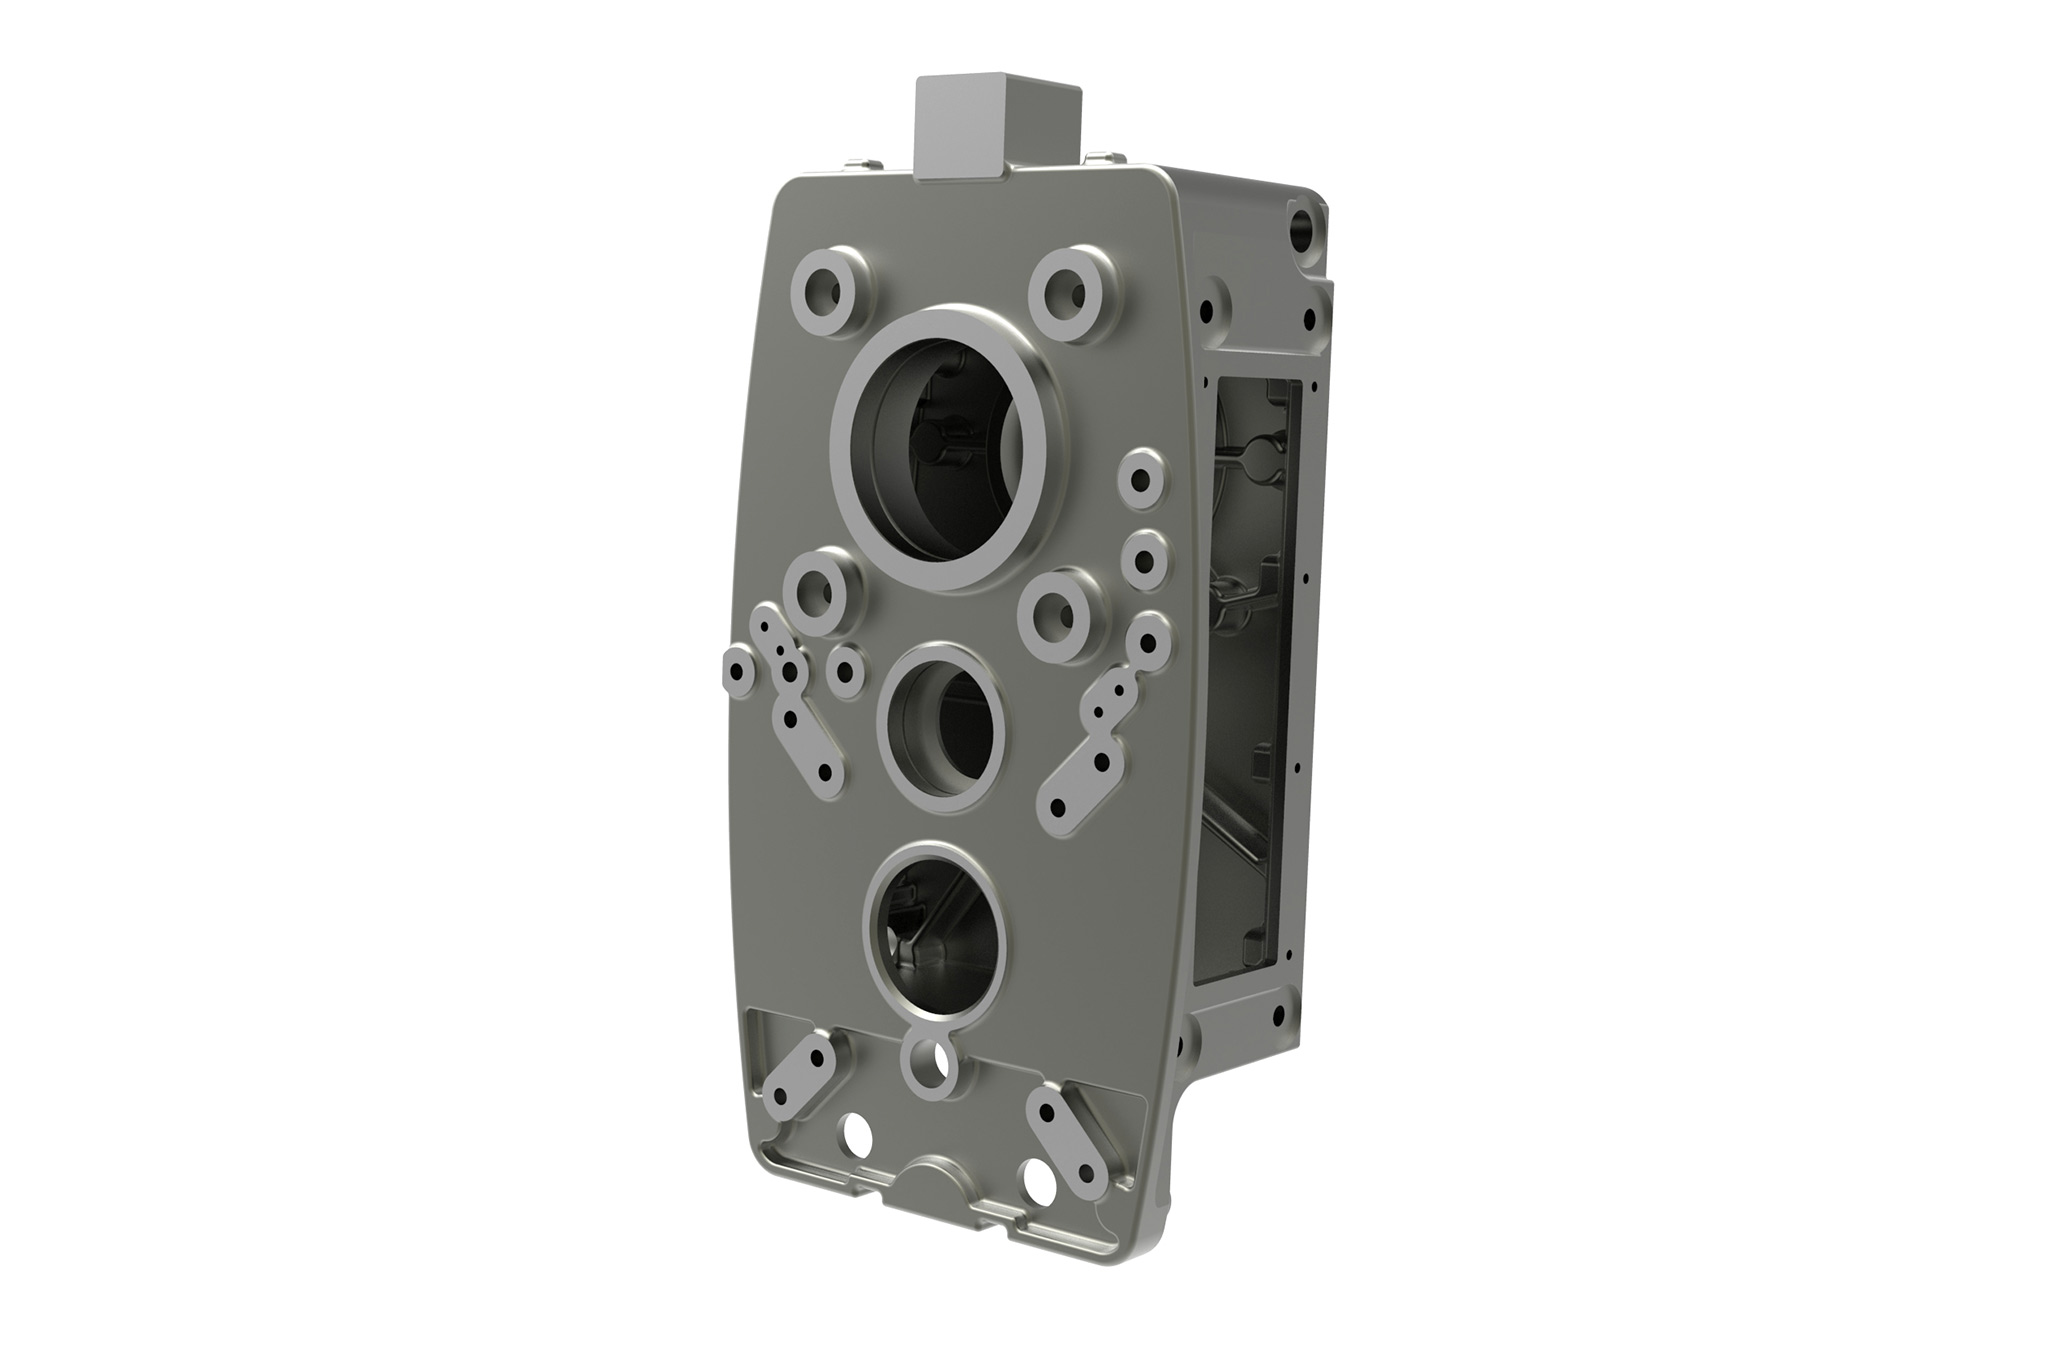
  • Photo of the HPR400 system.
    4 / 4

    HPR400 system

    • HPR400 for the highest precision
    • HPR400 plus for maximum cost-effectiveness
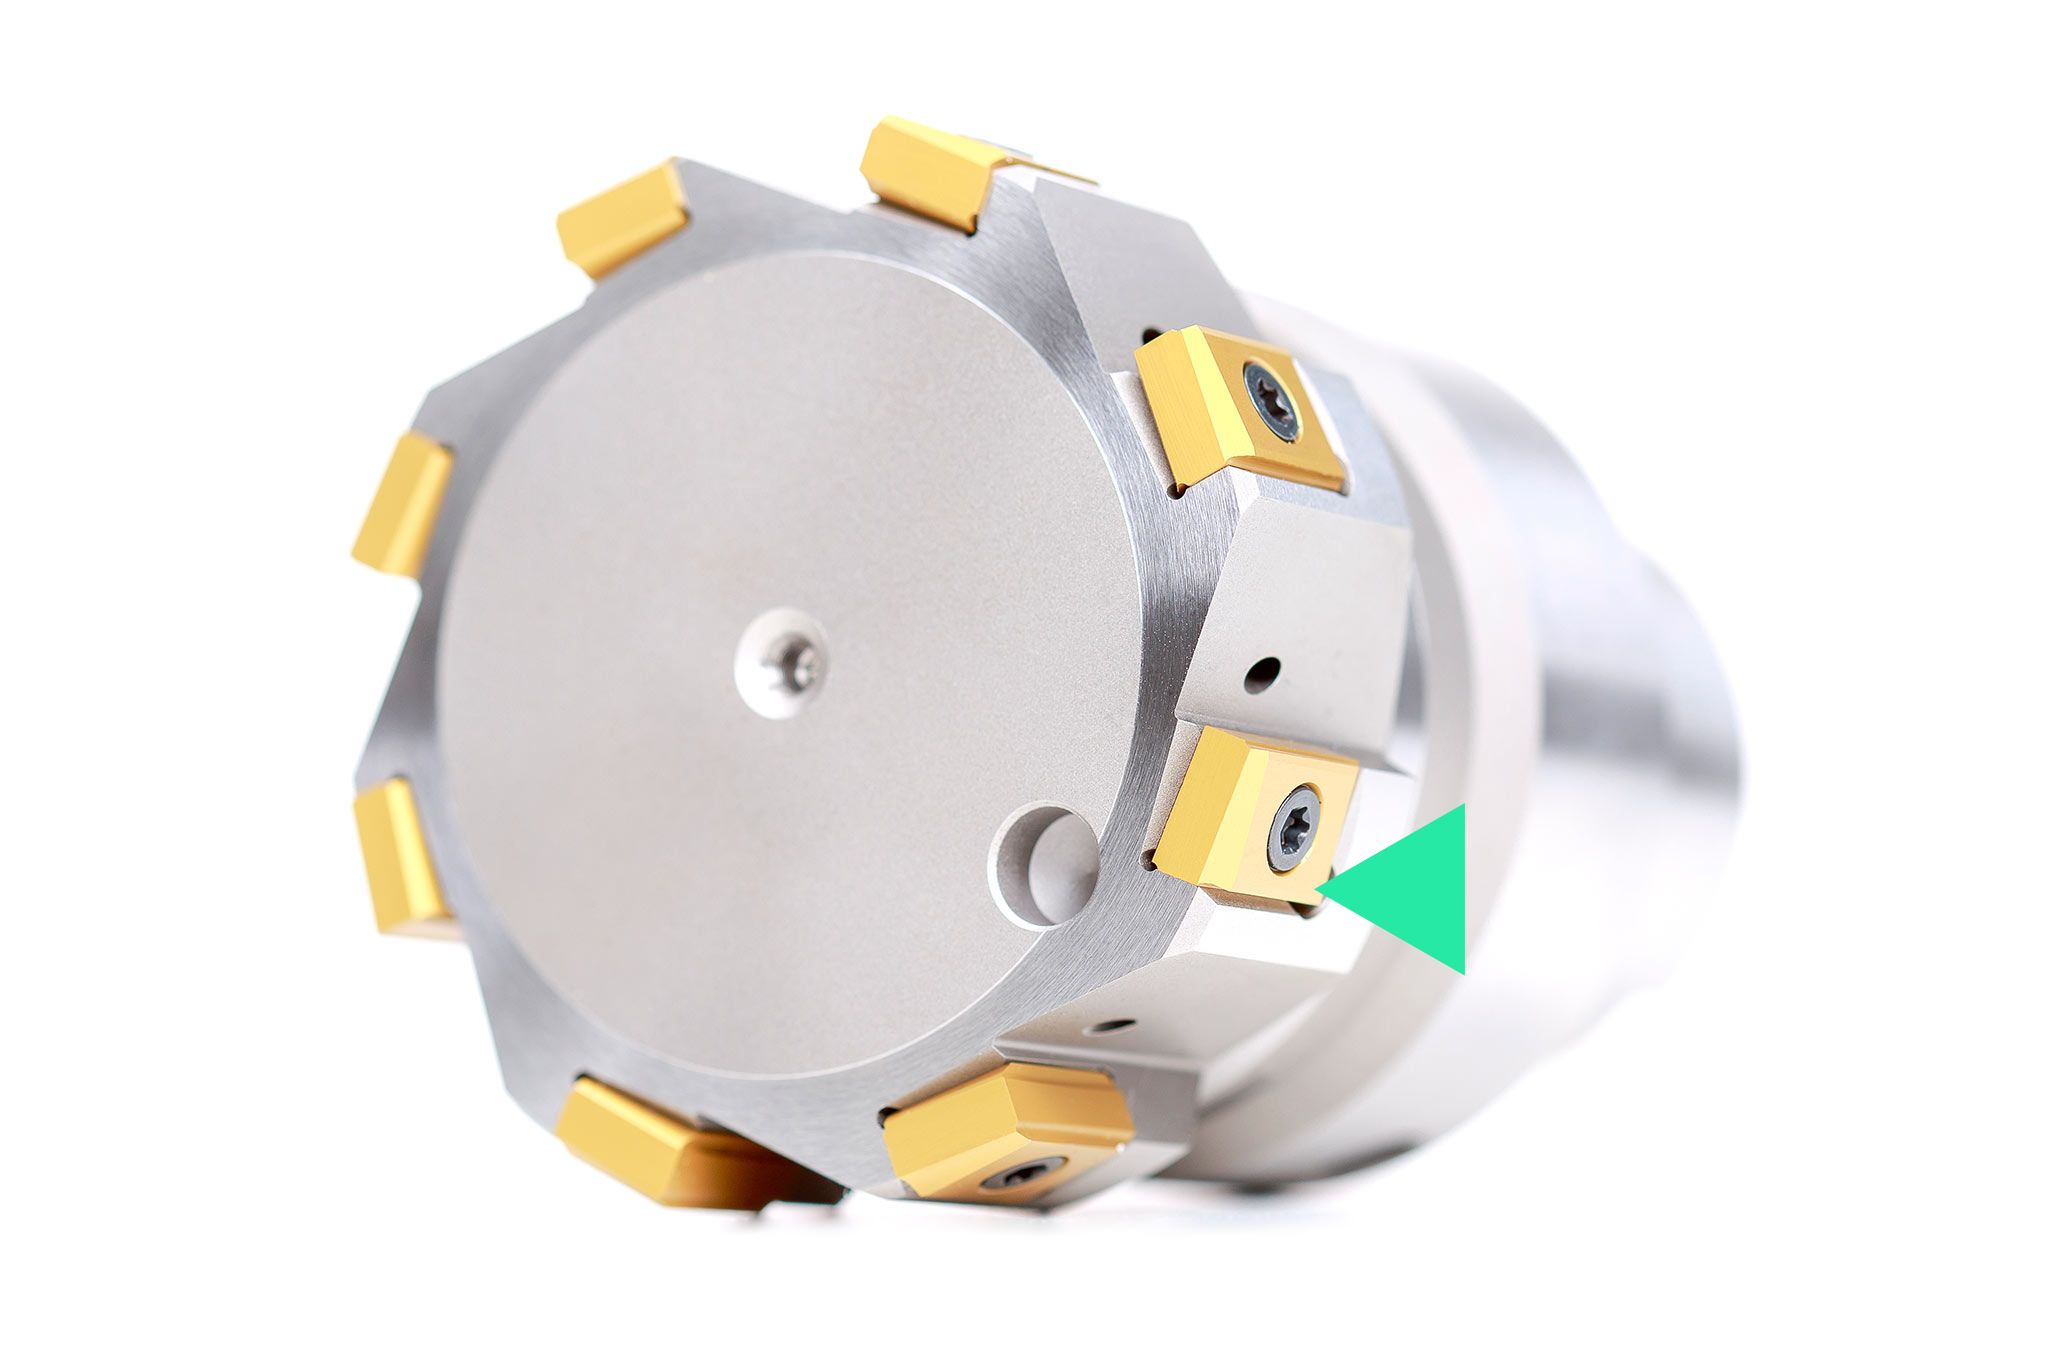
Four new solutions for practical use

  • The photo shows the one-lock solution.

    One-shot solution

    The combination tool with an ISO leading stage and HPR400 plus system enables the finishing of bores with high stock allowances (up to 6 mm) in a single step. The ISO part handles the main machining duties, while the HPR400 plus system takes care of finishing – with short cycle times and no setting effort required.

  • The picture shows the HPR400 plus for planing grooves.

    HPR400 plus for face grooves

    The new solution with indexable inserts with two usable cutting edges was designed for bores with specific base contours. It offers high stability and reliability and is particularly economical – ideal for steering knuckles and bearing bores with clearance at the bottom of the bore.

  • The photo shows the HPR400 with PCD cutting edges for stator housings.

    HPR400 with PCD inserts for stator housings

    MAPAL supplies a solution for finishing stator bores in electric motors with a higher number of cutting edges and no setting effort required. The result: high machining speed, low effort and high output – for high productivity.