

Automotive – constant velocity joints
New PcBN cutting materials for maximum efficiency in the hard machining of constant velocity joints
Machining hardened components places the highest demands on cutting material, tool geometry and process design – especially for safety-critical components such as drive joints. With new PcBN cutting materials and an optimised tool design, MAPAL takes the e–ciency of machining these key components to a new level. Longer tool life, shorter machining times and reduced unit costs make production much more cost-e‘ective.

Drive joints are highly stressed components whose ball tracks are hard-milled to the highest
precision. In the same way, the requirements for form, surface finish and tool performance are extremely high. Here, the cutting material and cutting edge preparation have a clear influence on tool life, performance and surface quality.
precision. In the same way, the requirements for form, surface finish and tool performance are extremely high. Here, the cutting material and cutting edge preparation have a clear influence on tool life, performance and surface quality.
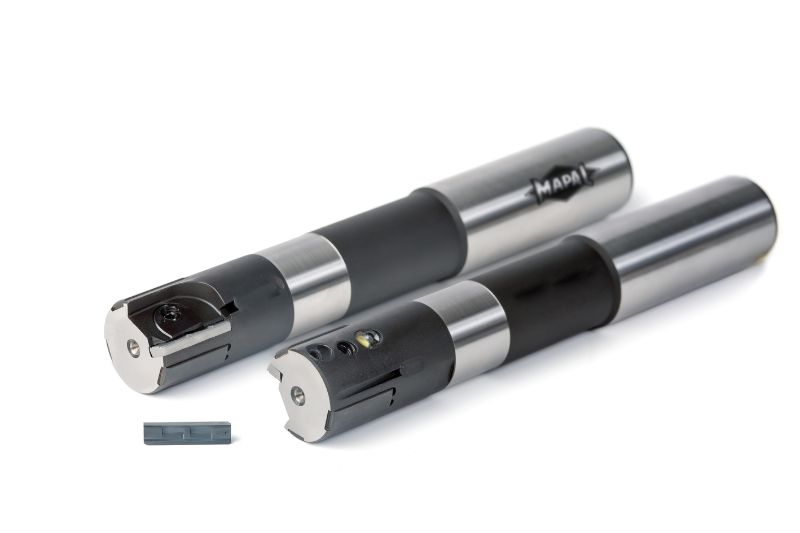
In response to the specific requirements of hard milling constant velocity joints, MAPAL has developed new PcBN cutting materials specifically tailored to the applications in the inner race (ball hub) and outer race (outer housing), enabling more efficient hard machining. Compared with the previous solutions, the new FU240 (outer race) and FU290 (inner race) cutting materials achieve upwards of 30% more workpieces per tool at cutting speeds of 180 m/min and a feed per tooth of between 0.07 and 0.10 mm.
In addition, MAPAL has revised the tool design of its ball track milling cutters and introduced
a new five-bladed design that reduces machining time by around 20% compared with four-bladed tools. With annual production volumes of up to 15 million components, this results in significant potential for reducing unit costs.
a new five-bladed design that reduces machining time by around 20% compared with four-bladed tools. With annual production volumes of up to 15 million components, this results in significant potential for reducing unit costs.

MAPAL is also introducing new PcBN cutting materials for the hard turning of drive joints. FP240 is designed for continuous cutting applications, such as on the shank of the outer race, while the ductile FP260 cutting material is used for interrupted cuts on the inner race or cage. Depending on the application, tool life can be increased by more than 40%.

The combination of application-optimised cutting materials and adapted tool design delivers lasting productivity gains and improves cost efficiency when machining hardened drive joints.
-
 1 / 5
New PcBN cutting materials
- Upwards of 30% more workpieces per tool
-
2 / 5
Component-specific cutting material selection
- Optimised for inner race, outer race and ball cage
-
3 / 5
Optimised cutting edge preparation
- Highest surface quality of the ball tracks
-
4 / 5
Five-bladed milling cutter design
- Up to 20% shorter machining time
-
5 / 5
Perfectly coordinated tool concept
- Reduced unit costs in series production




/OptiMill-HPC-Pocket-Bearbeitungen-800x533-2-.png)


