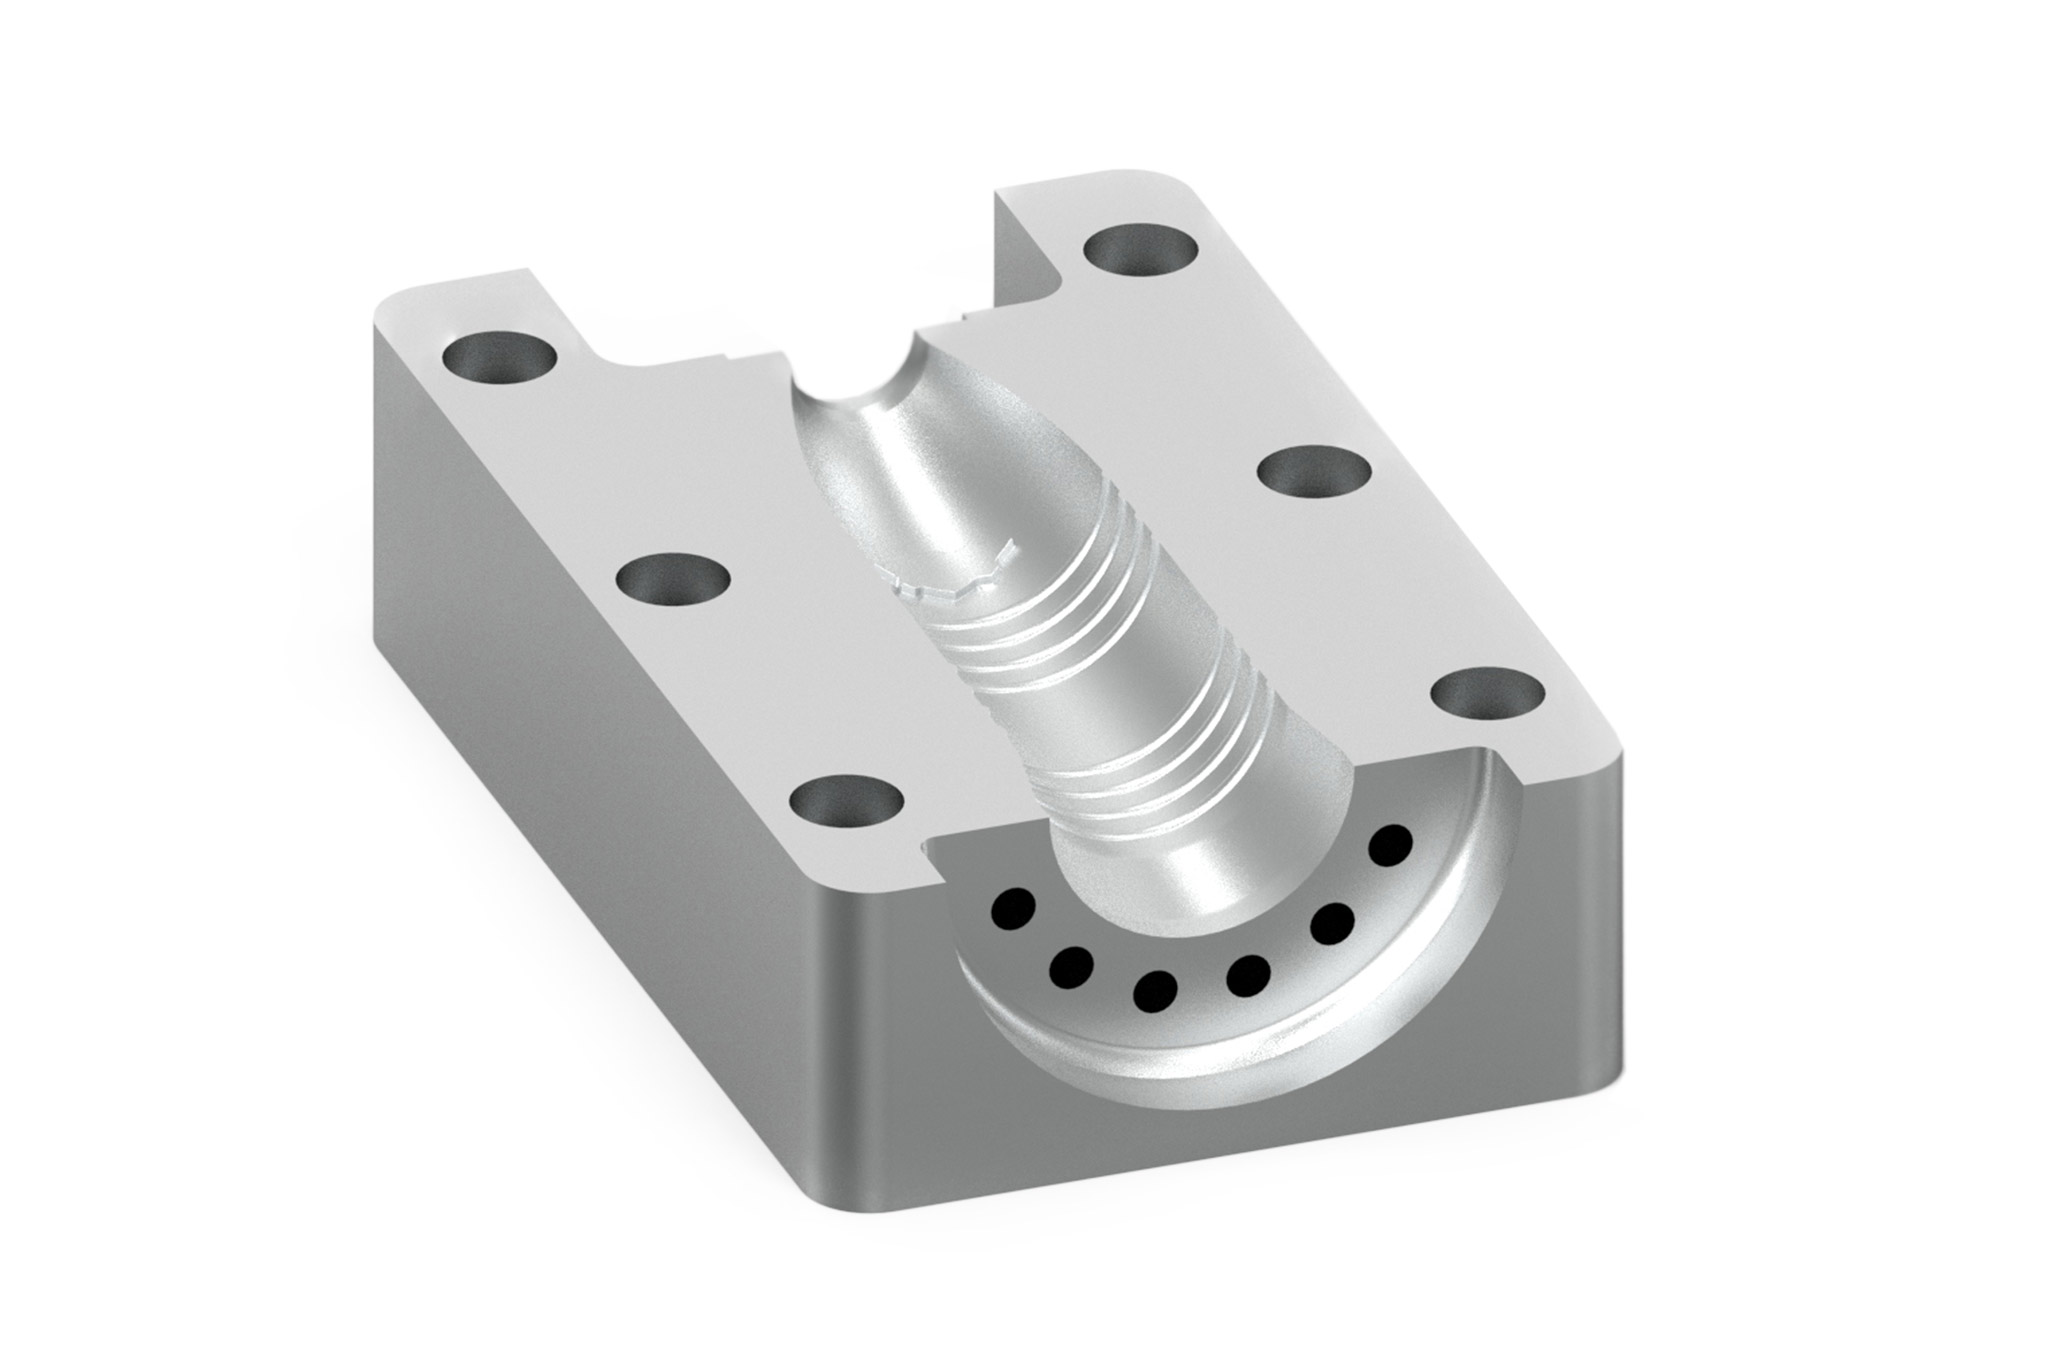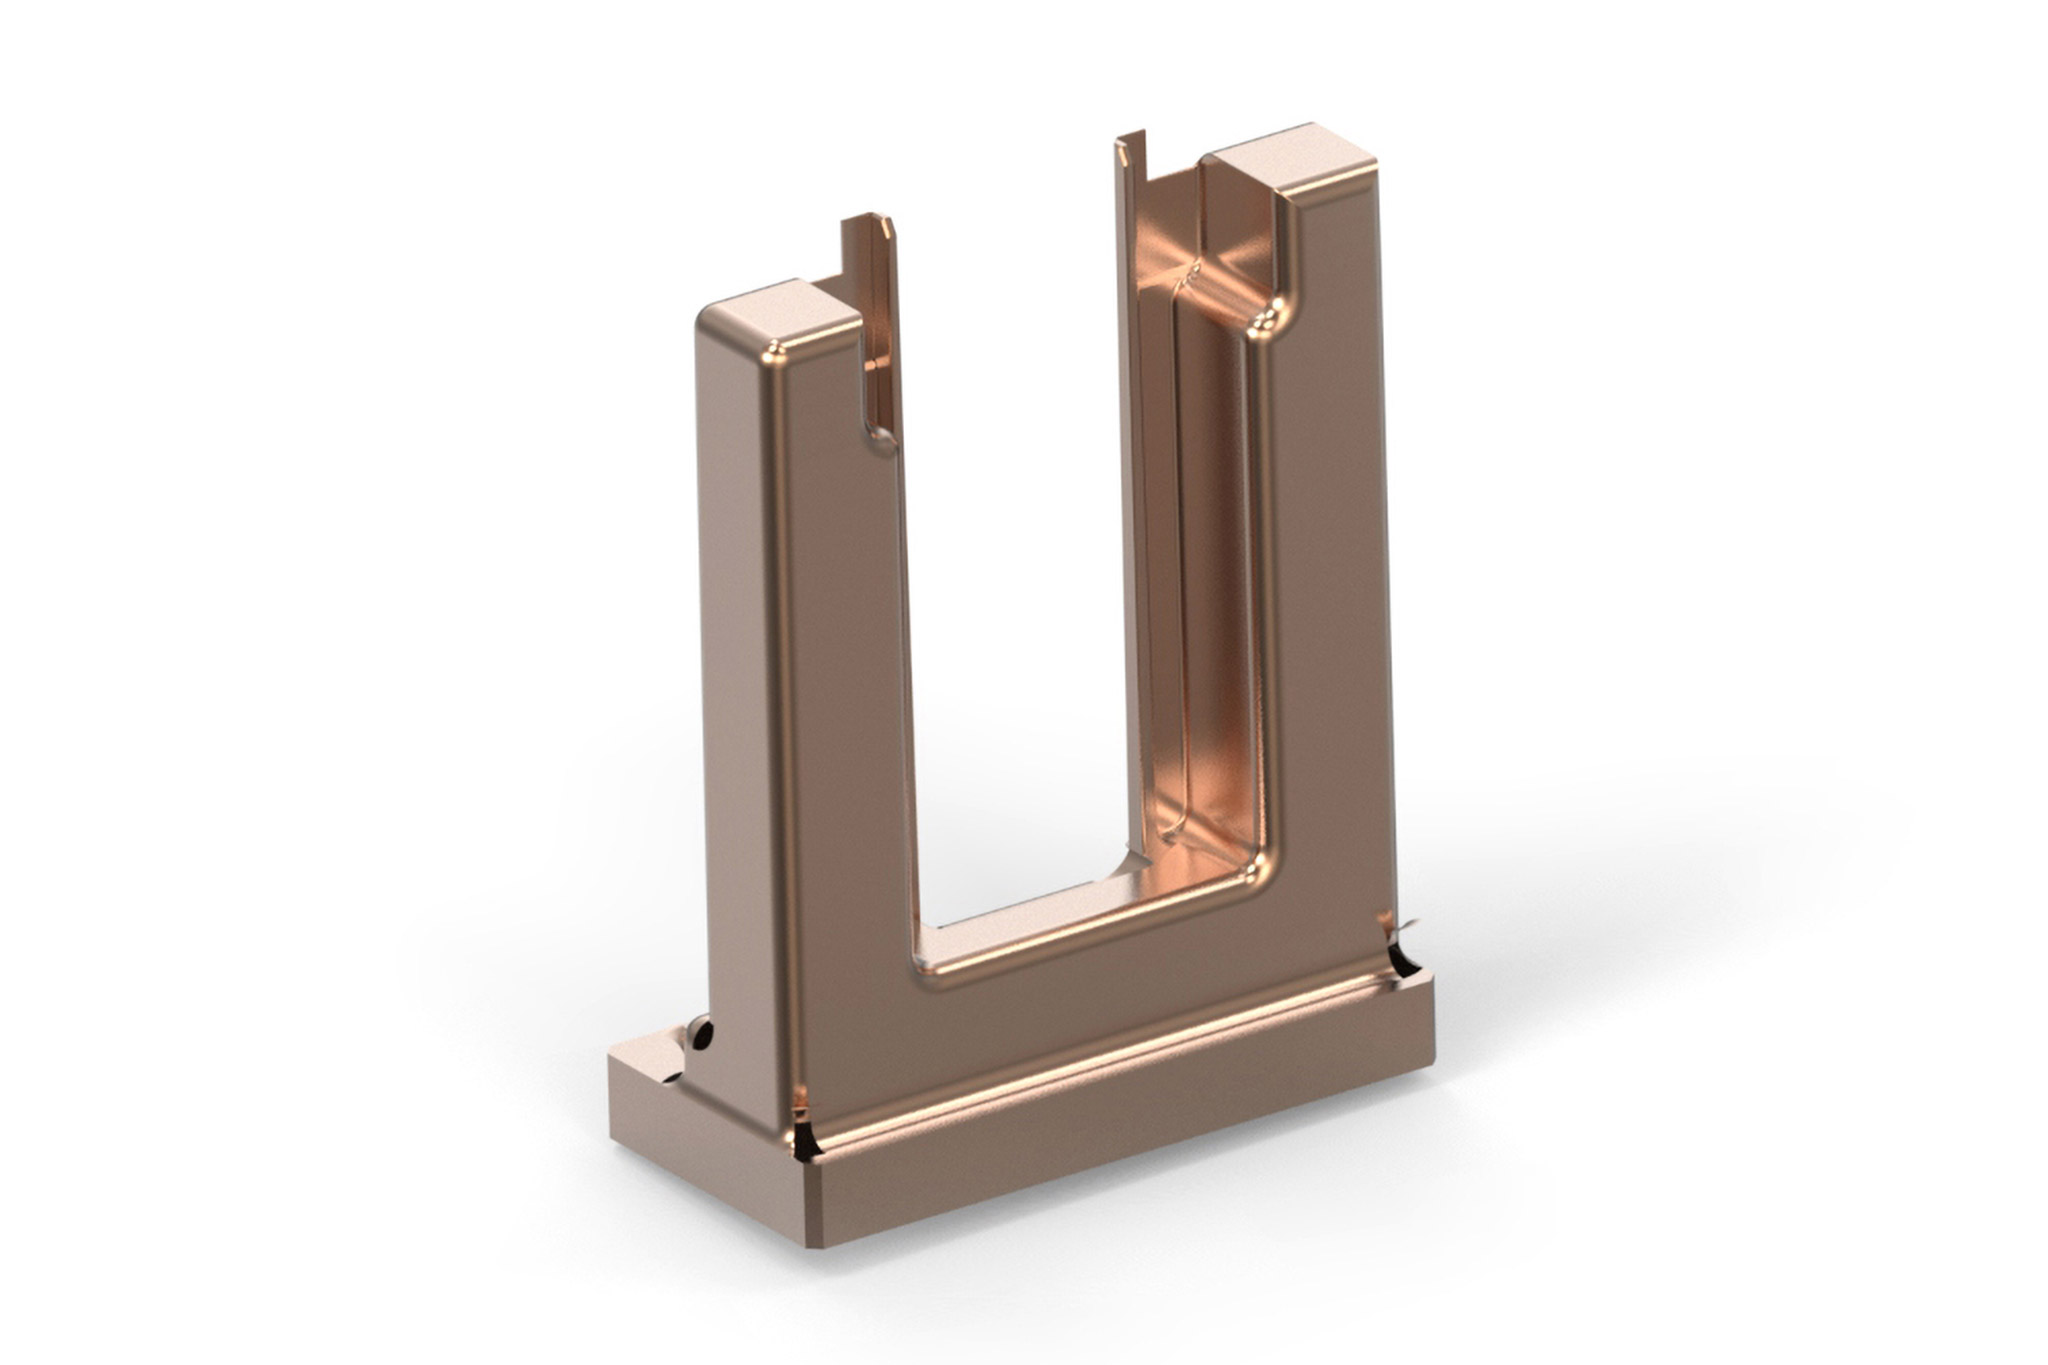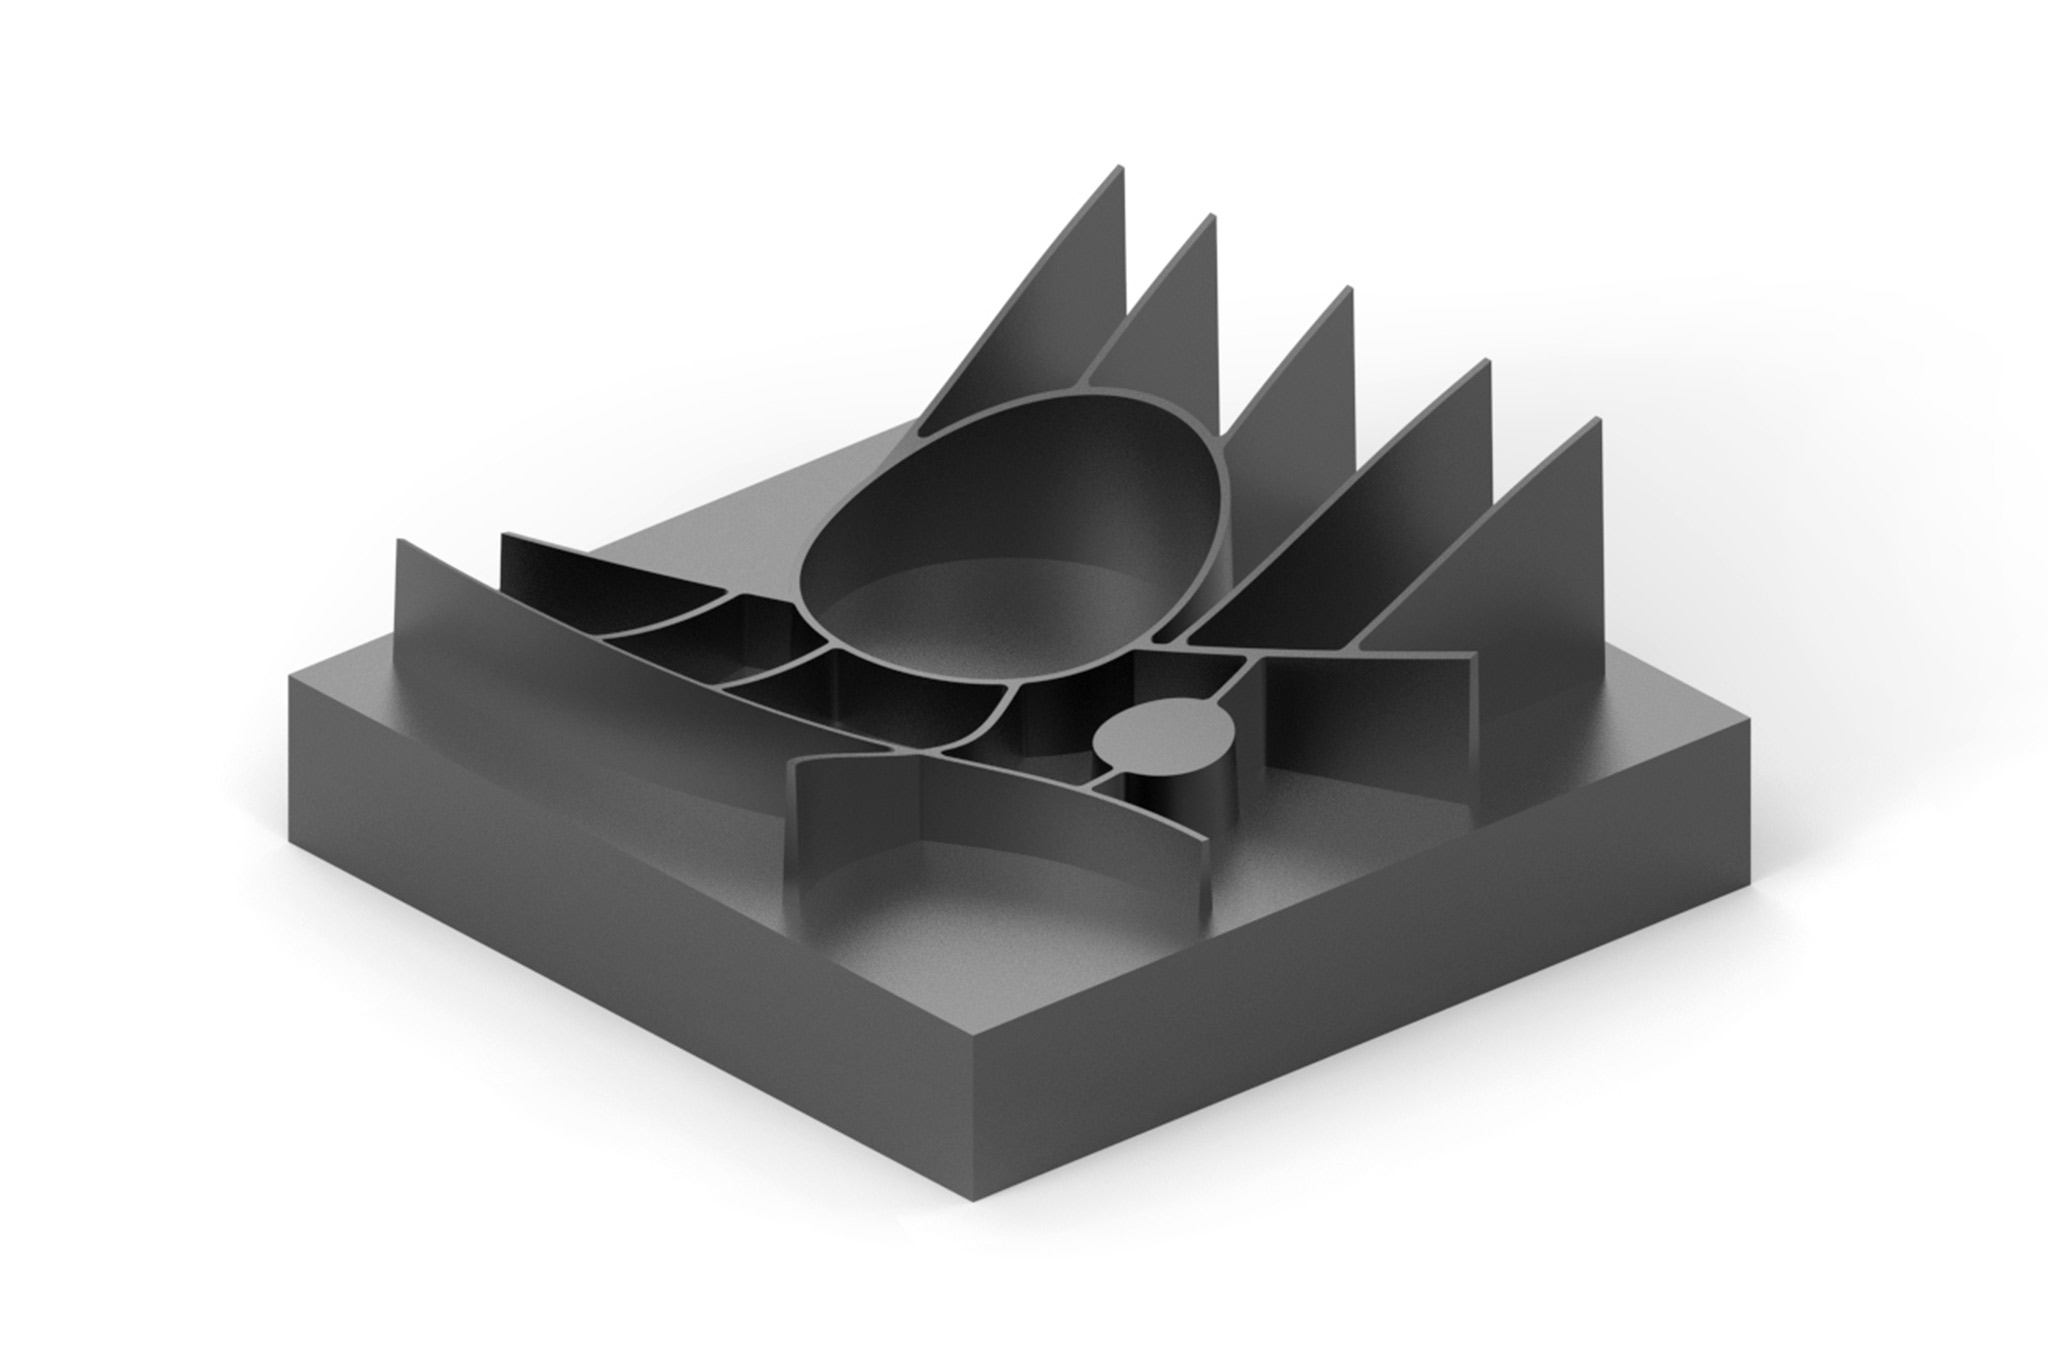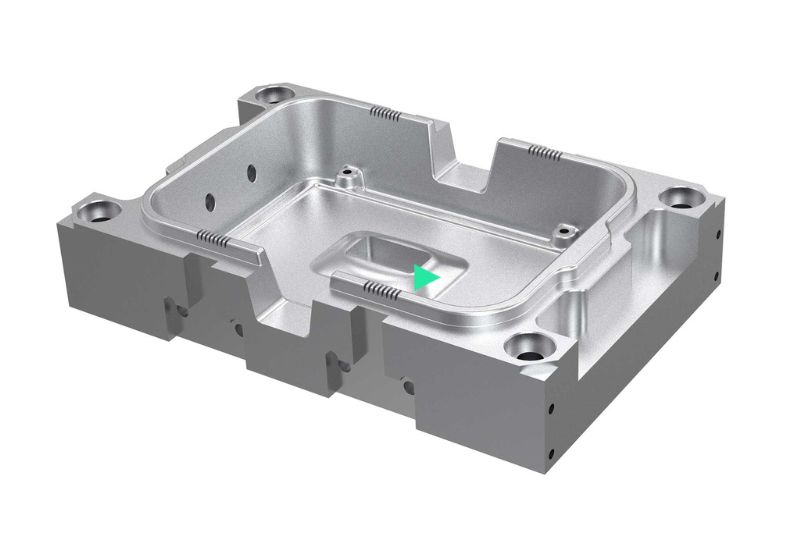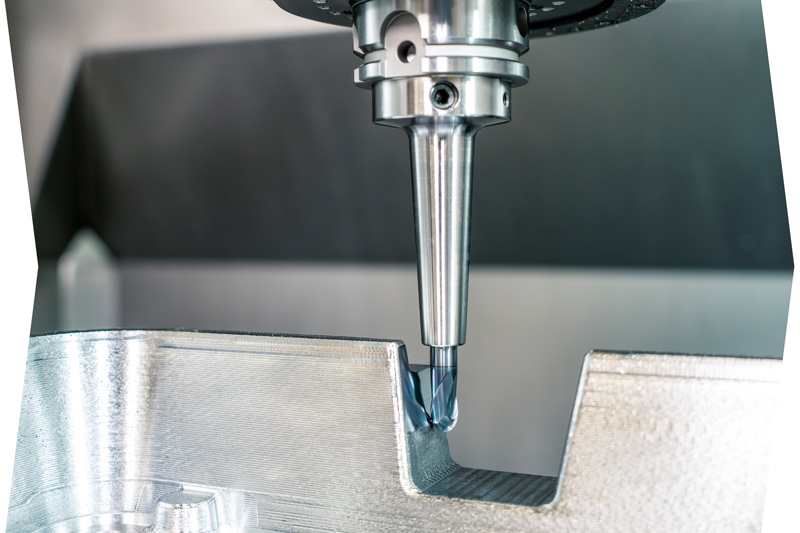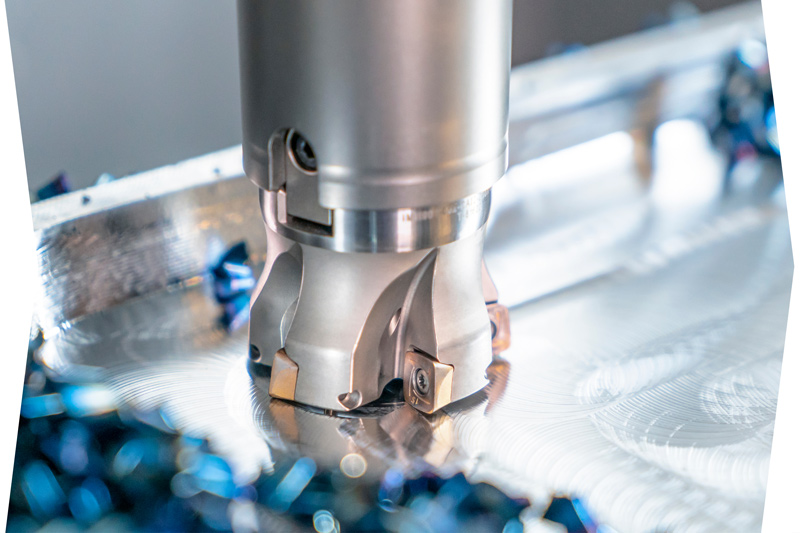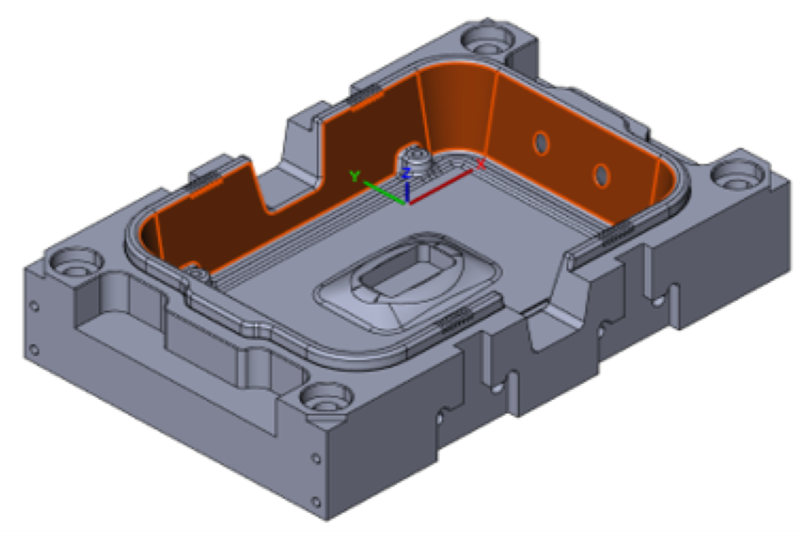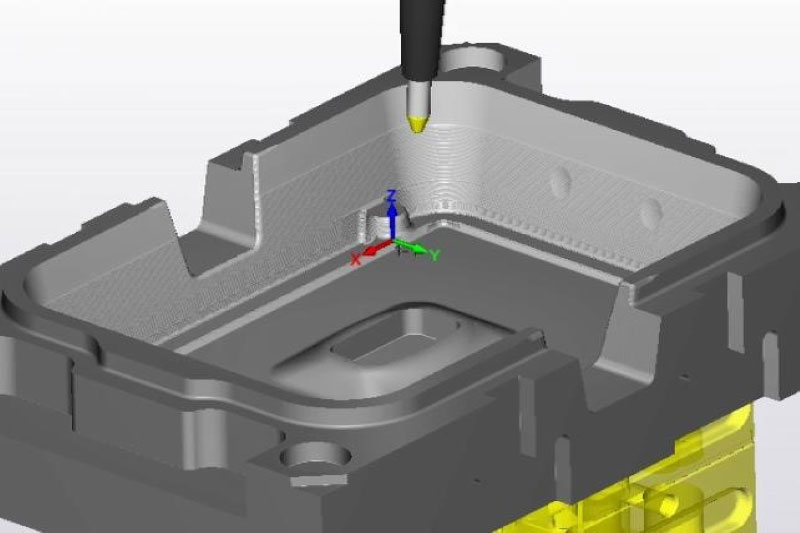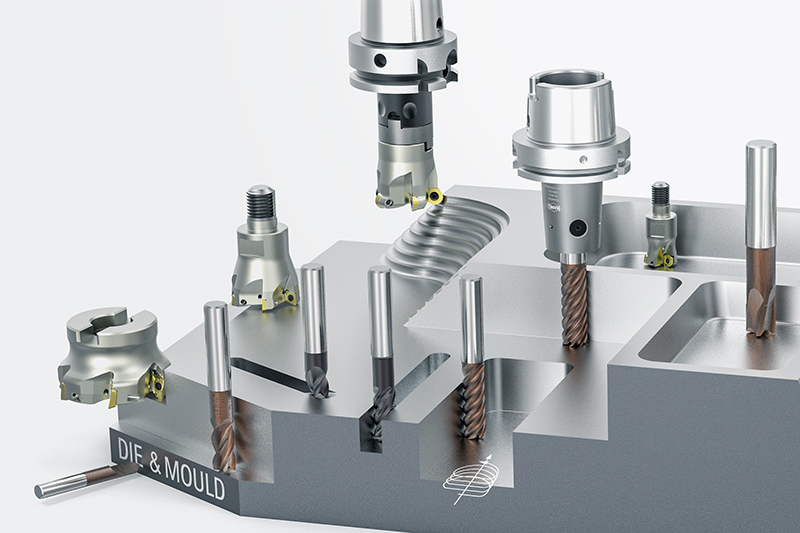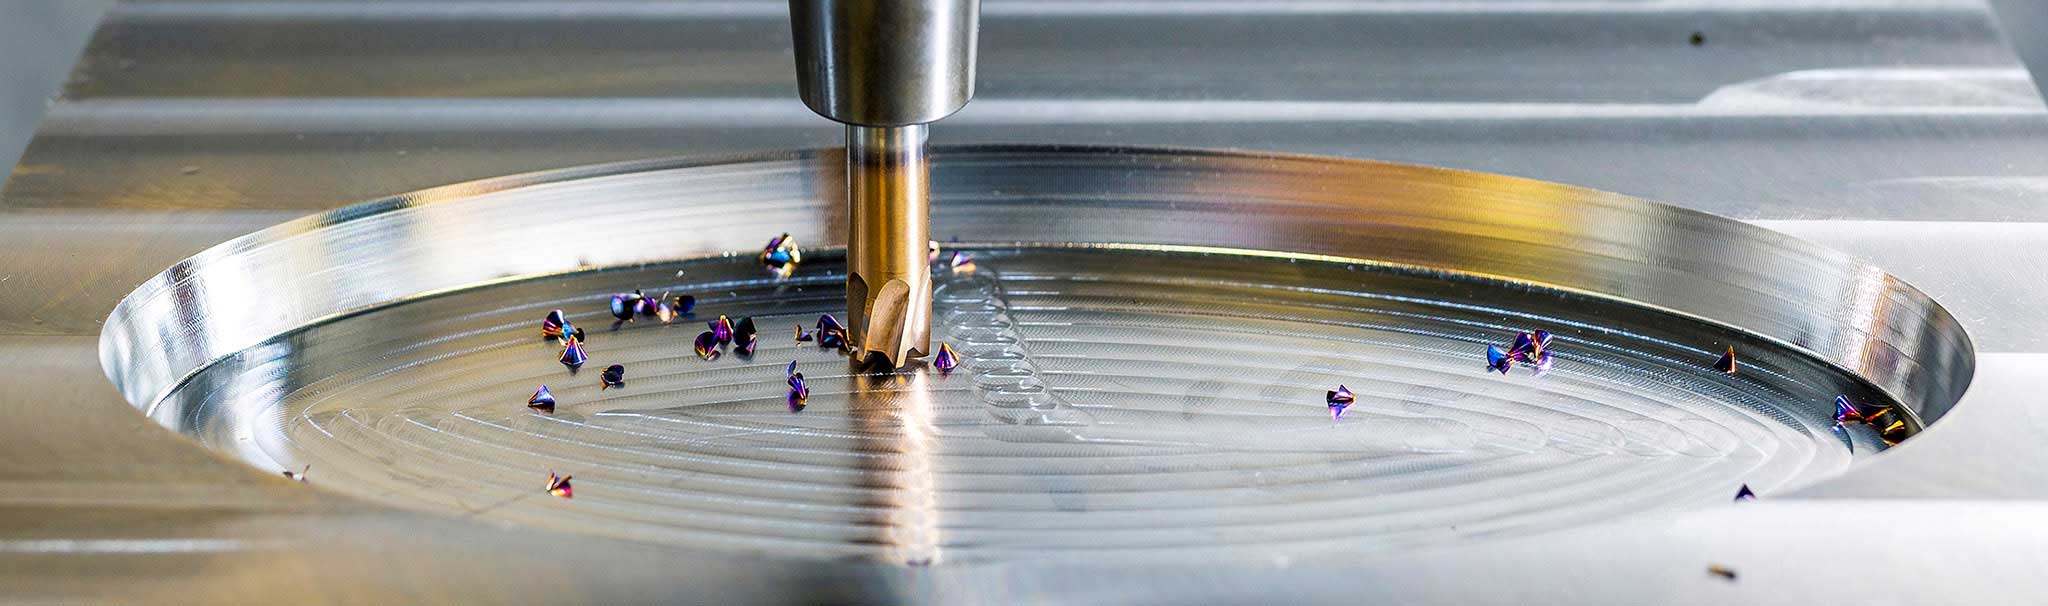
• MAPAL offers complete machining solutions for the die and mould industry.

Démarrer dans la fabrication des moules et des matrices

Les moulistes attendent un haut niveau de compétence de la part des fabricants d'outils d'usinage. En effet, la durée de vie des moules à fabriquer et la précision des composants moulés sont vitales pour se démarquer de la concurrence au niveau de la production en masse. L'on exige des outils qu'ils soient hautement précis, particulièrement durables et, le plus important, sûrs.
 

Ce sont précisément ces aspects qui sont à la base de la popularité de MAPAL dans divers secteurs, dont l'industrie automobile, le génie mécanique et l'industrie aérospatiale. Il est donc logique que le fabricant d'outils de précision propose désormais des solutions efficaces et économiques pour l'usinage complet de moules et de matrices. Les outils haute performance précis et polyvalents ainsi que les porte-outils spéciaux avec contours fins et concentricité précise réduisent les opérations de polissage et le réusinage au minimum grâce à une qualité de surface constante lors du fraisage. Ils permettent de réaliser des économies substantielles tout au long du processus.

Programme d'outils pour la fabrication de moules
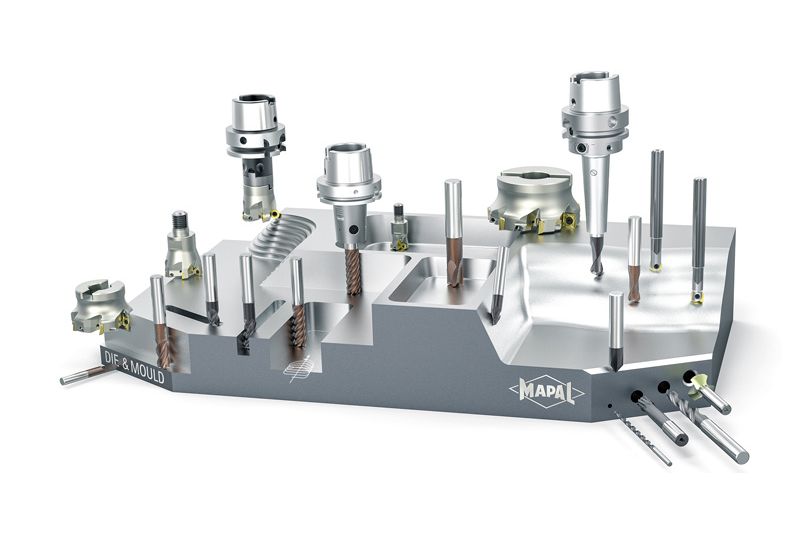
The picture shows the MAPAL tool range for mould making

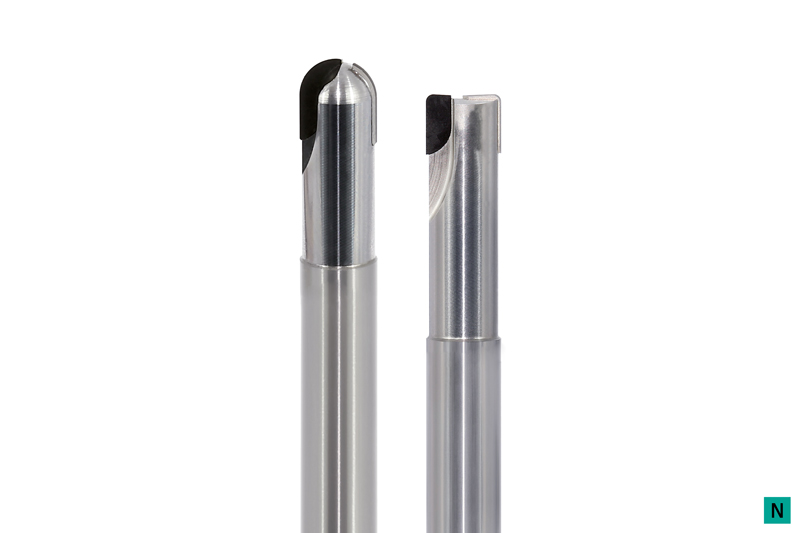
Fraises en carbure monobloc
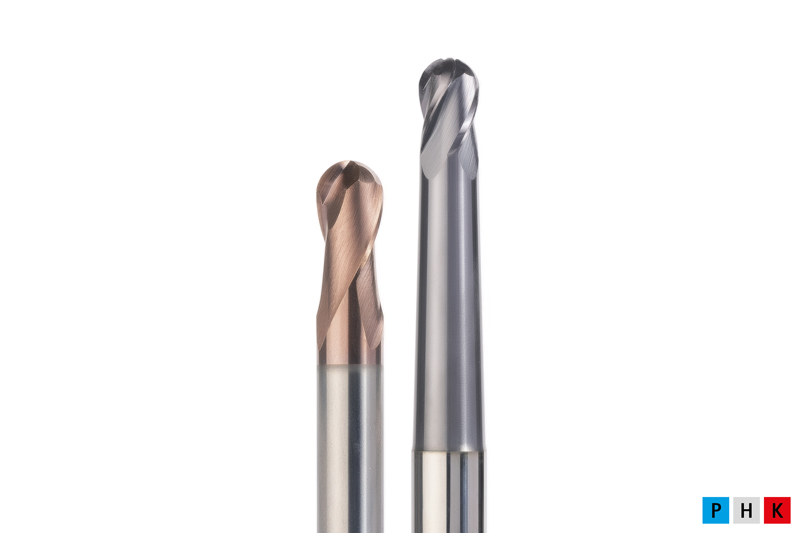
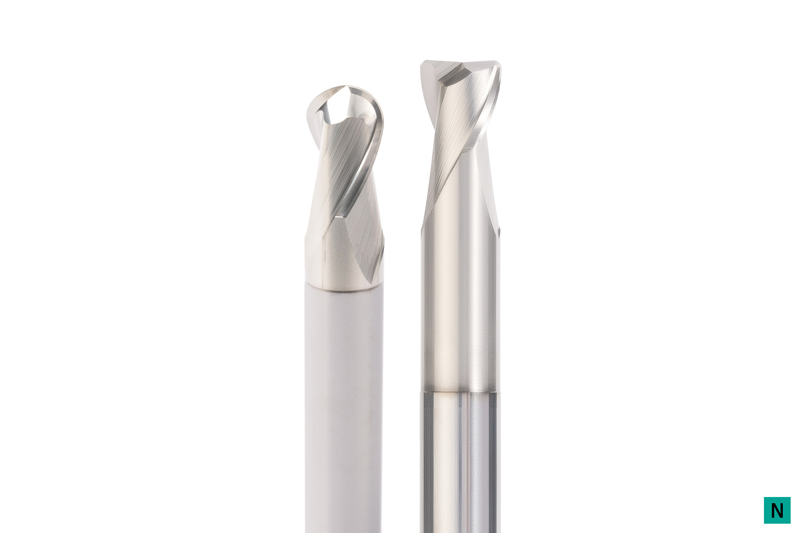
  • OptiMill-3D-BN

    Fraises hémisphériques
    • Usinage hautement précis de contours 3D
    • Plage ø : 0,10 - 20,00 mm

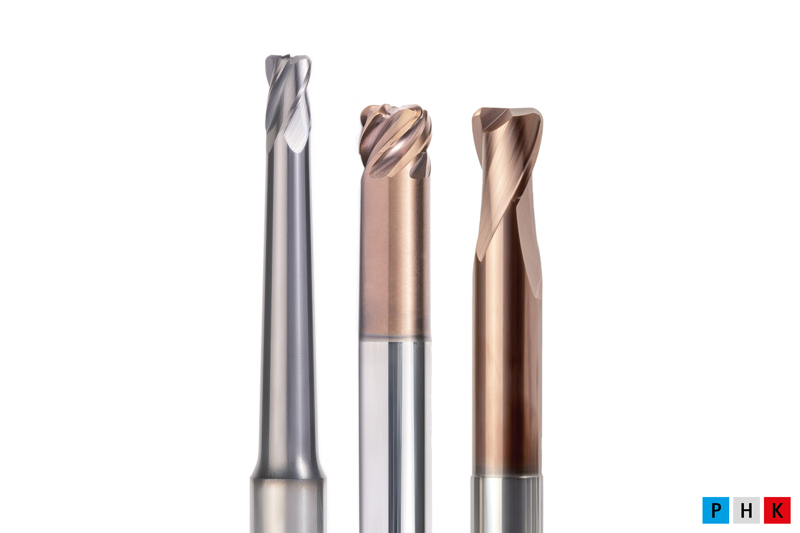
  • OptiMill-3D-CR

    Fraises rayonnées
    • Fraisage avec rayon de raccordement hautement précis
    • Plage ø : 0,10 - 20,00 mm

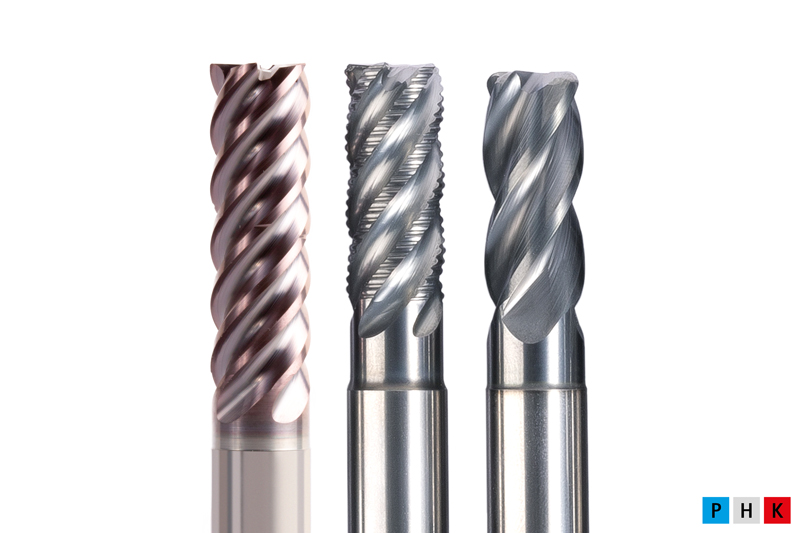
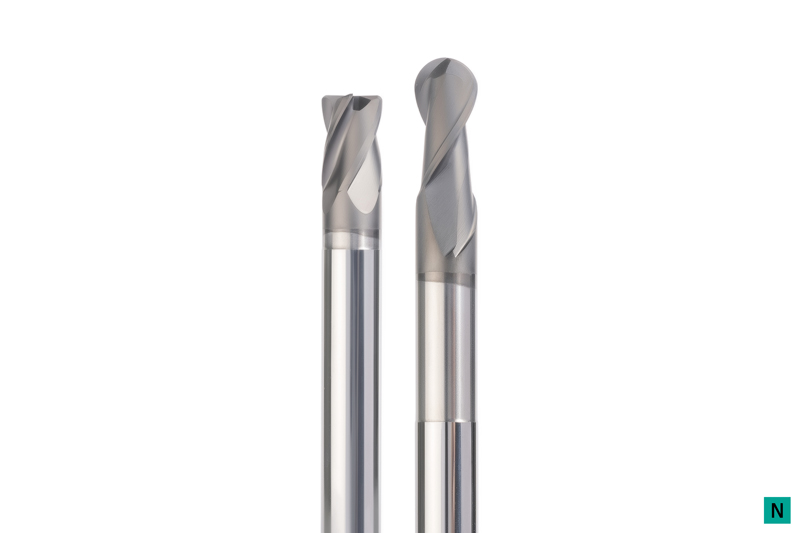
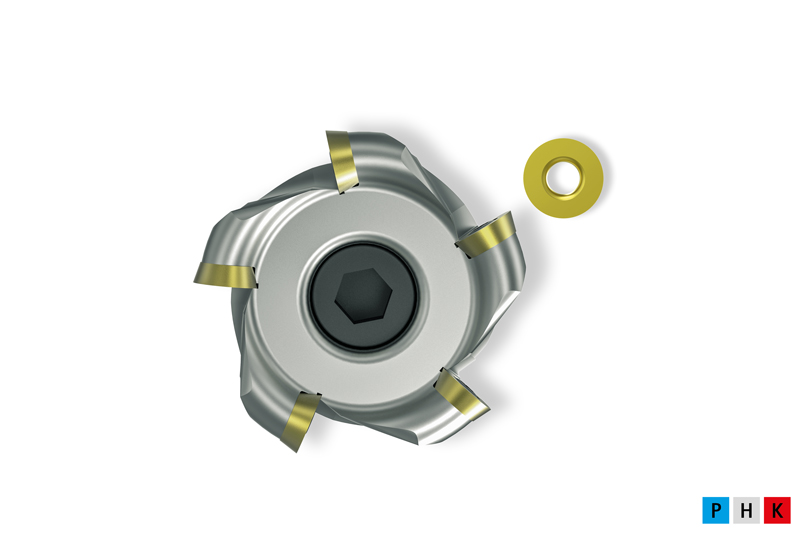
  • OptiMill Fraises à dresser

    Fraises à dresser
    • Idéales pour l'ébauche, la finition, le fraisage trochoïdal et le fraisage de poches
    • Plage ø : 2,00 - 12,00 mm

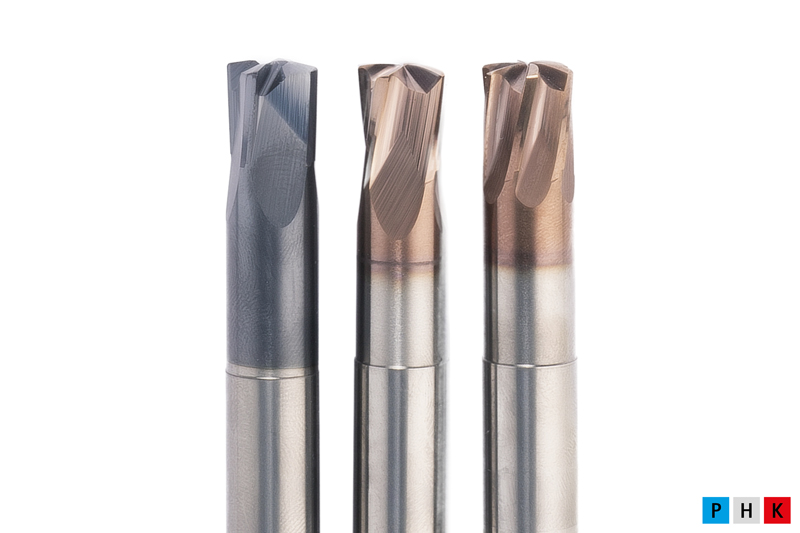
  • OptiMill-3D-HF

    Fraises à grande avance
    • Idéales pour l'usinage grande avance avec un volume d'enlèvement de copeaux élevé pour une fiabilité des processus accrue
    • Plage ø : 2,00 - 16,00 mm

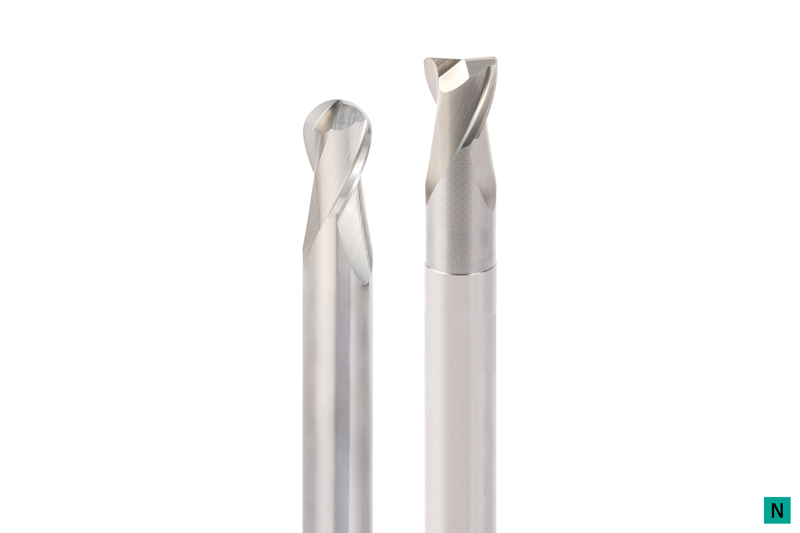
  • OptiMill-3D-Alu

    Fraises rayonnées/hémisphériques
    • Usinage hautement précis de contours 3D
    • Plage ø : 1,00 - 20,00 mm

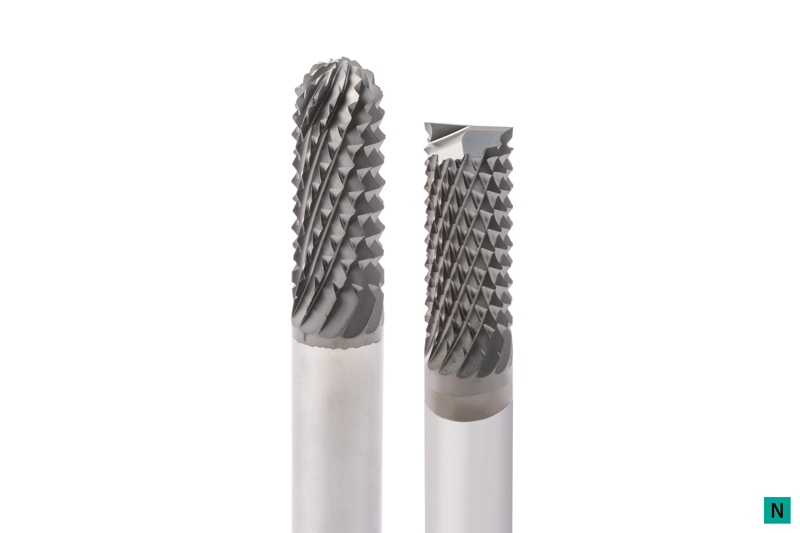
  • OptiMill-Graphite-MT

    Fraises à dresser et hémisphériques
    • Fraises multidents d'ébauche pour un taux d'enlèvement élevé avec les électrodes en graphite
    • Plage ø : 3,00 - 16,00 mm

  • OptiMill-3D-Graphite

    Fraises rayonnées/hémisphériques
    • Adaptées pour l'usinage d'électrodes en graphite
    • Différents modèles selon la situation d'usinage
    • Plage ø : 0,20 - 12,00 mm

  • OptiMill-3D-Copper

    Fraises rayonnées/hémisphériques
    • Géométrie spéciale pour l'usinage d'électrodes en cuivre et d'alliages non ferreux durs
    • Plage ø : 0,10 - 20,00 mm

  • OptiMill-Diamond

    Fraises à dresser, rayonnées, hémisphériques
    • Coupes PCD pour une durée de vie élevée
    • Plage ø : 3,00 - 12,00 mm

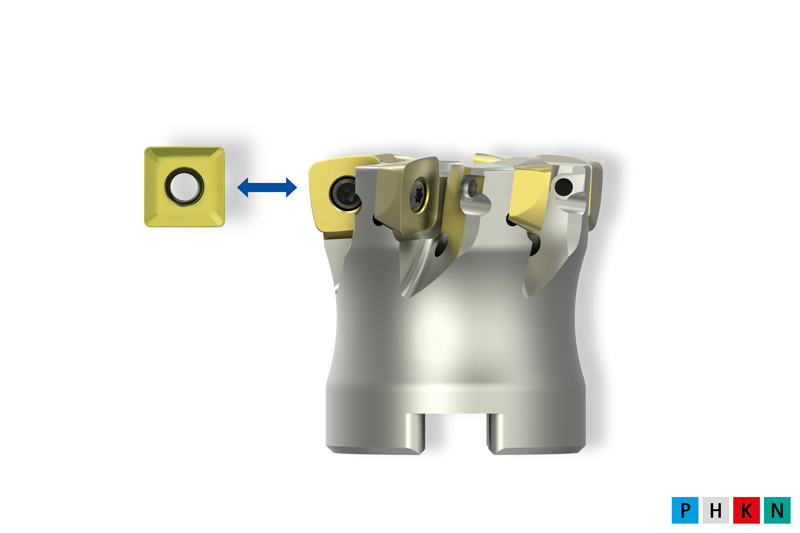
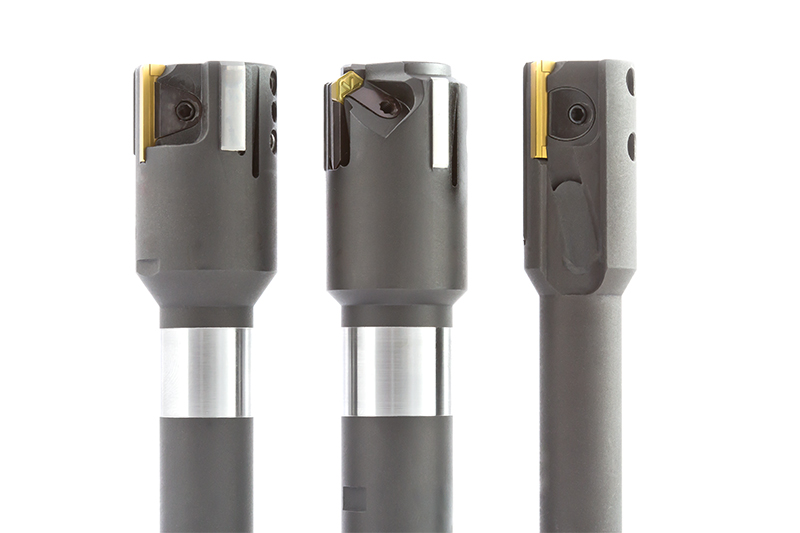
Fraises à plaquettes amovibles
  • NeoMill-ISO-360

    Fraises à plaquettes rondes
    • Idéales pour l'ébauche et la semi-finition
    • Plage ø : 10,00 - 160,00 mm

  • NeoMill-3D-Finish

    Fraises de finition
    • Idéales pour la finition des surfaces angulaires, des surfaces planes et des contours
    • Plage ø : 16,00 - 42,00 mm

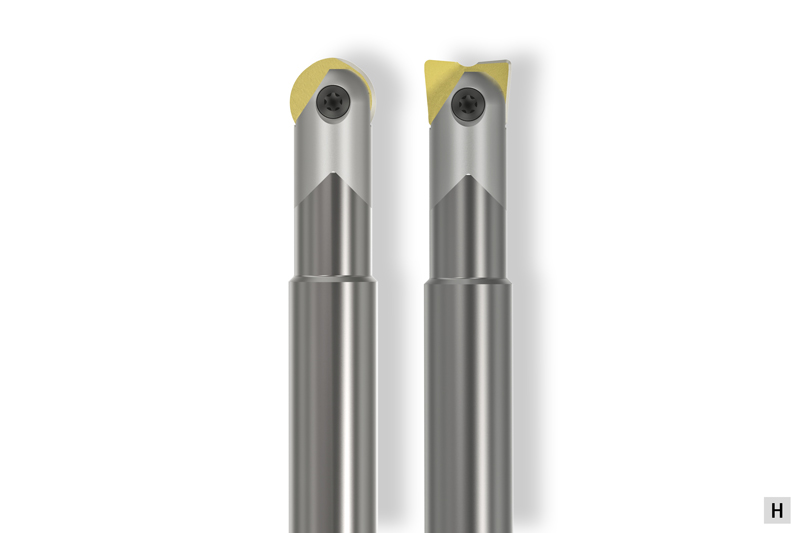
  • NeoMill-3D-Ballnose/-Torus

    Fraises rayonnées/hémisphériques
    • Un corps de base avec plaquette de coupe pour la finition et la semi-finition
    • Plage ø : 8,00 - 32,00 mm

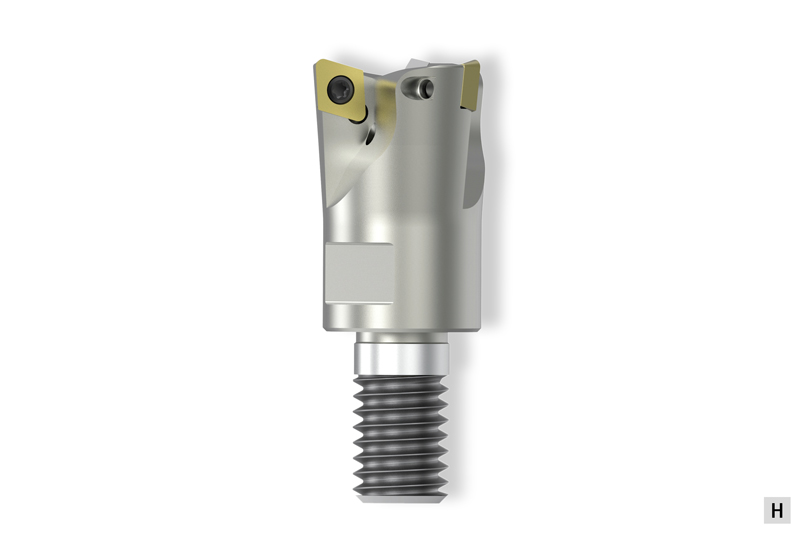
  • NeoMill-2/4-HiFeed90

    Fraises à dresser/grande avance
    • Système d'outil universel pour une productivité maximale
    • Plage de ø : 16,00 - 200,00 mm

Perçage | Chanfreinage
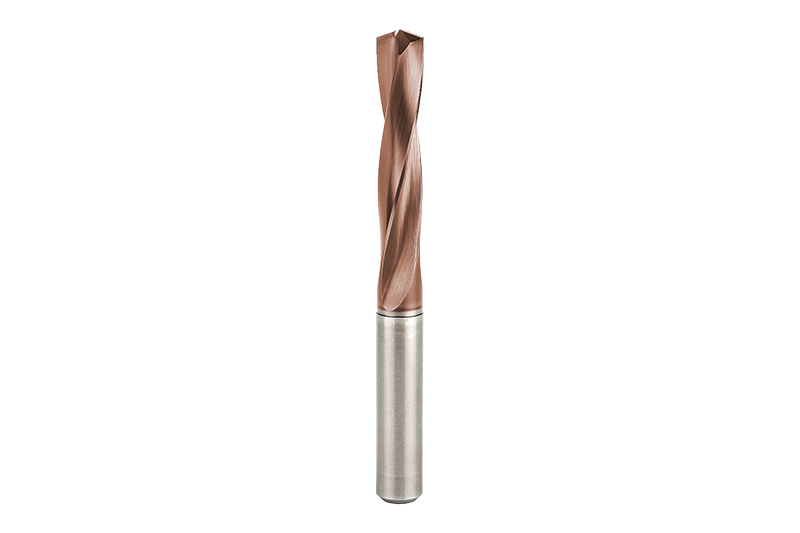
  • ECU-Drill-Steel

    Foret en carbure monobloc  

    • Foret à deux arêtes de coupe avec un très bon rapport qualité-prix
    • Vaste gamme d'applications
    • Géométrie éprouvée pour un niveau élevé de précision et de fiabilité des processus
    • Plage de ø : 1,00 – 20,00 mm 

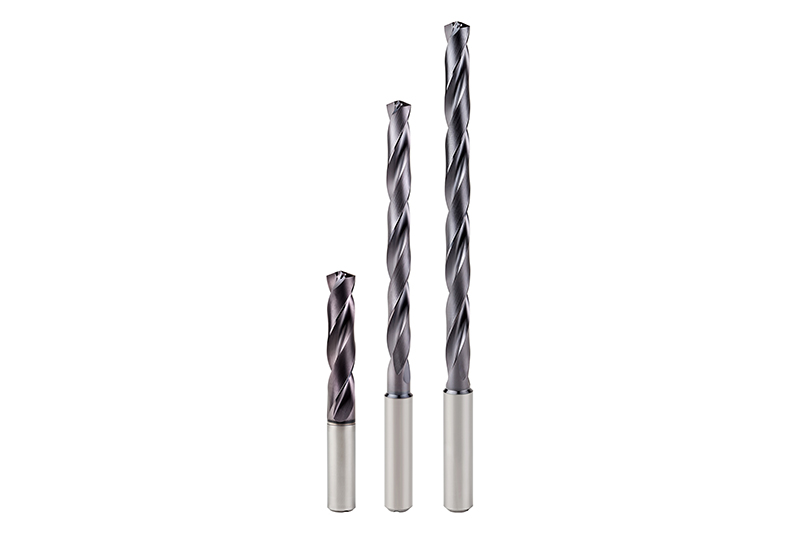
  • MEGA-Drill-Hardened

    Foret en carbure monobloc ultra-puissant 

    • Foret à deux arêtes de coupe avec revêtement et géométrie adaptés pour l'usinage fiable des matériaux durcis
    • Nouvelle micro et macro géométrie
    • Plage de ø : 2,55 – 16,00 mm 

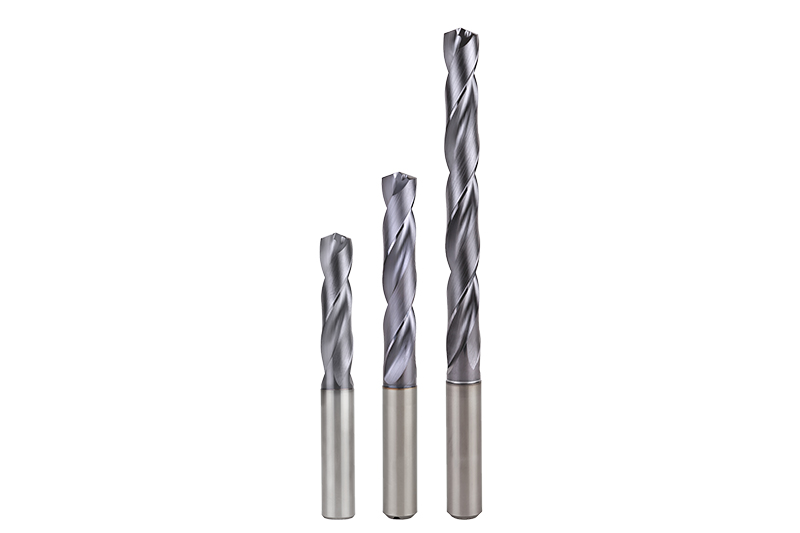
  • MEGA-Drill-Steel-Plus

    Foret en carbure monobloc ultra-puissant 

    • Foret à deux arêtes de coupe avec revêtement et géométrie adaptés pour l'usinage de l'acier
    • Géométrie de la goujure optimisée et préparation d’arêtes de coupe modifiées
    • Plage de ø : 3,00 – 25,00 mm

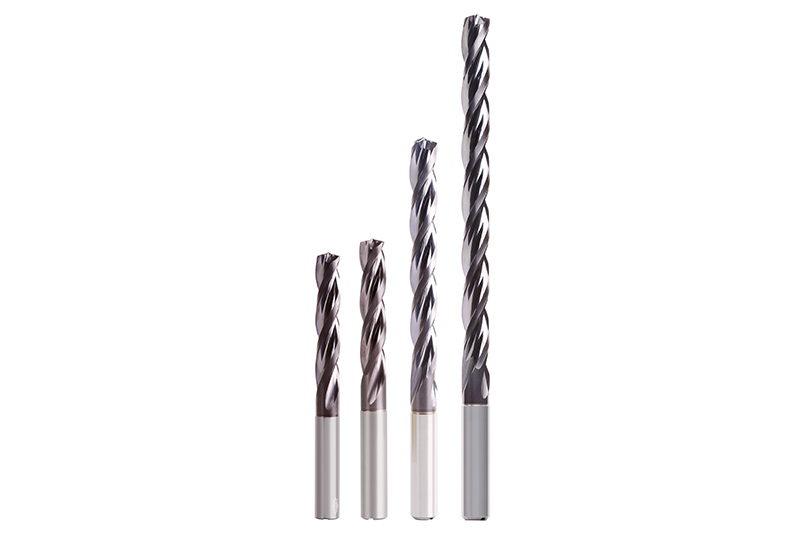
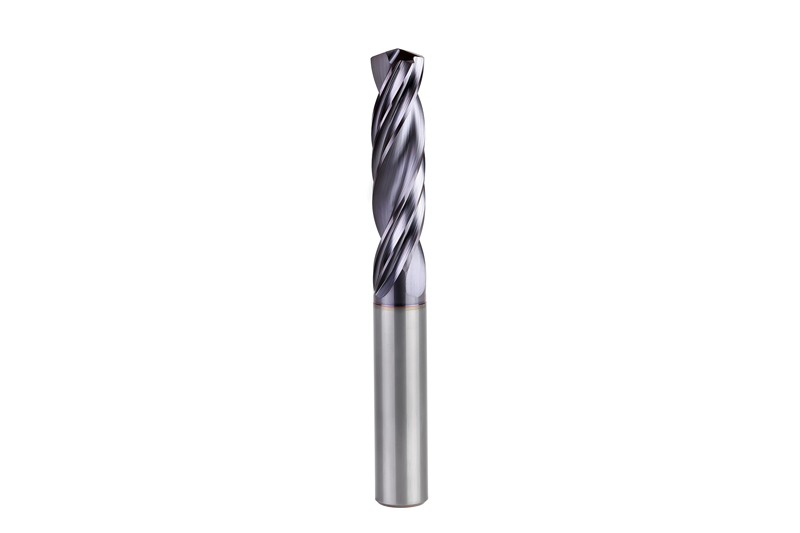
  • Tritan-Drill-Steel

    Forets en carbure monobloc à trois arêtes de coupe 

    • Foret à trois arêtes de coupe pour une avance maximale
    • Arête transversale autocentrée pour les situations de perçage difficiles
    • Spécialement développé pour l'usinage de l'acier
    • Plage de ø : 4,00 – 20,00 mm 

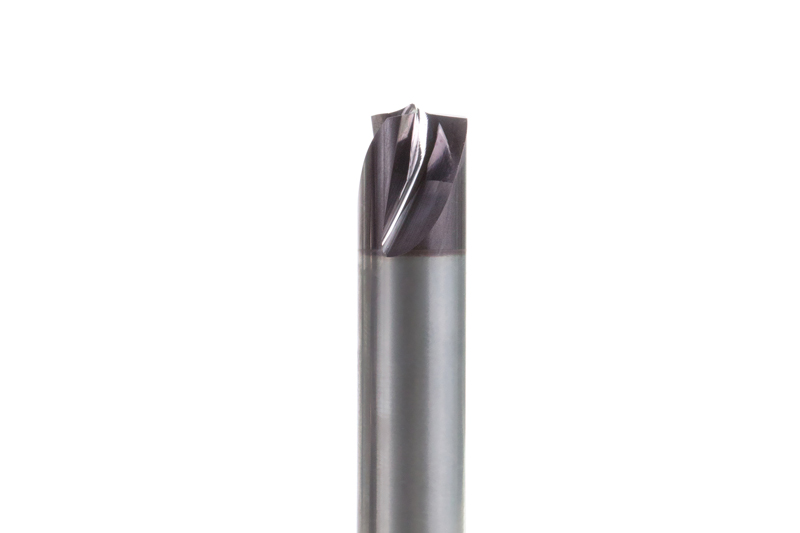
  • Tritan-Spot-Drill-Steel

    Foret à pointer
    • Foret à pointer à trois arêtes de coupe pour les situations de centrage exigeantes
    • Spécialement adapté aux forets à trois arêtes de coupe
    • Plage de ø : 4,00 – 20,00 mm

  • Wiertło stopniowe Tritan

    Wiertło stopniowe trójostrzowe
    • Wiertło stopniowe trójostrzowe z samocentrującym ścinem
    • Obróbka otworów z gwintem wewnętrznym bez ruchu oscylującego
    • Zakres ø: 4,25 - 14,15 mm

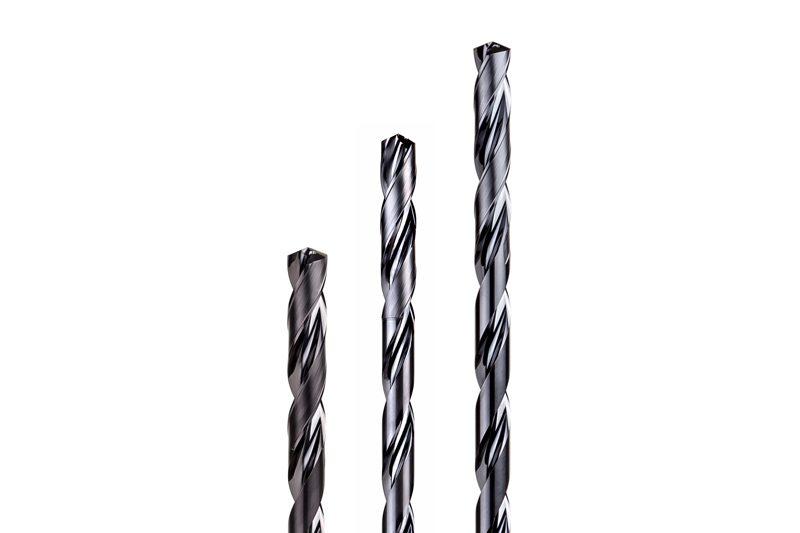
  • Wiertło MEGA-Deep-Drill

    Wiertła głębokie
    • Niezawodna i wydajna obróbka głębokich otworów do 40xD
    • Wiertło pilotowe MEGA-Pilot-Drill
    • Zakres ø: 1,00 - 16,00 mm

  • MEGA-Drill-Reamer

    Wiertło-rozwiertak do rozwiercania
    • Dwie operacje – wiercenie i rozwiercanie – w jednym narzędziu
    • Zoptymalizowane ostrze rozwiercające
    • Skrócenie czasów głównej i dodatkowej obróbki
    • Tolerancja otworu ≥ IT7
    • Zakres ø: 4,00–16,00 mm

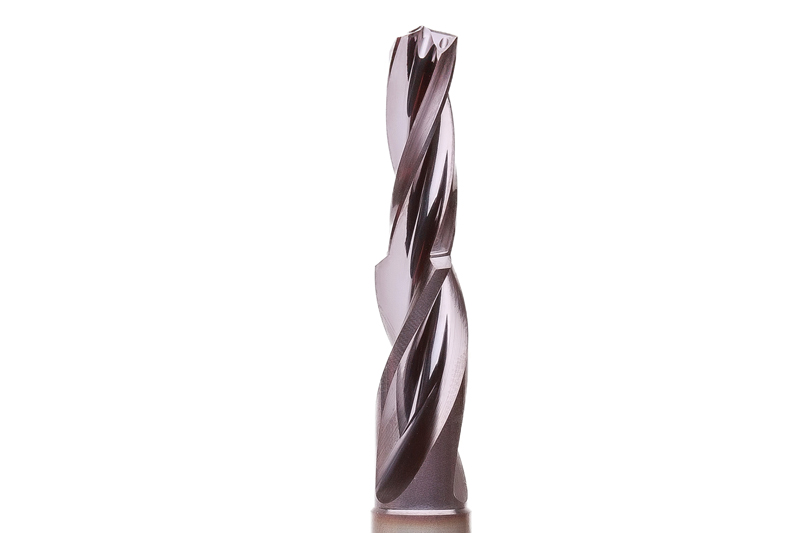
  • Precyzyjne wiertło stożkowe

    Precyzyjne wiertło stożkowe z nierównomiernym podziałem
    • Niezwykle nierównomierny podział ostrzy
    • Wyższa dokładność i lepsze właściwości powierzchni
    • Zmniejszone siły osiowe i promieniowe
    • Znacznie mniej wibracji
    • Zwiększone parametry skrawania dla najwyższej wydajności
    • Zakres ø: 4,30–31,00 mm

  • Wiertło MEGA-Drill-Reamer-Pyramid

    Wiertło-rozwiertak z końcówką piramidalną

    • Nawiercanie, wiercenie i rozwiercanie jednym narzędziem
    • Ulepszone właściwości centrowania dzięki końcówce piramidalnej
    • Skrócenie czasu operacji głównych i dodatkowych
    • Tolerancja otworu ≥ IT7
    • zakres ø: 4,00 – 16,00 mm

  • Wiertło z płytką skrawającą QTD

    Wiercenie w pełnym materiale z systemem wymiennych głowic

    • Ekonomiczny system z wymiennymi płytkami skrawającymi
    • System mocowania siłowego i kształtowego
    • Łatwa obsługa
    • Wysoka dokładność koncentryczności
    • Zakres ø: 8,10–49,00 mm

Rozwiercanie
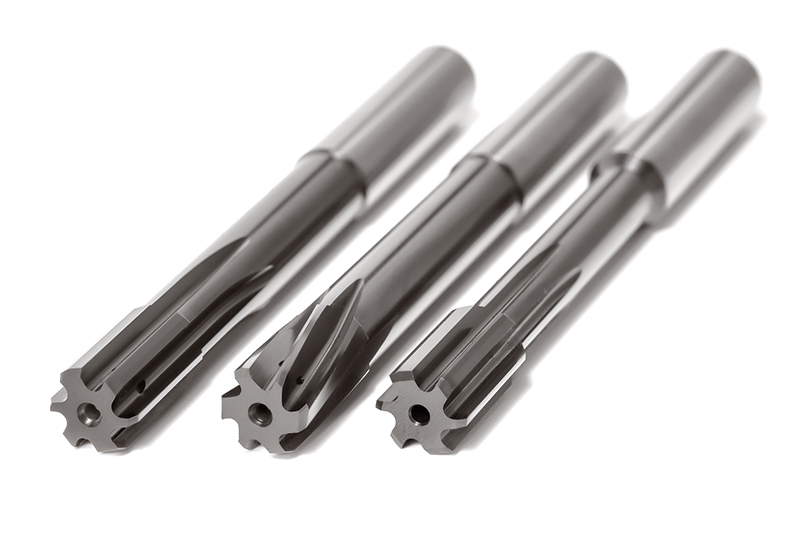
  • FixReam – FXR

    • Wysokowydajne wytrychowce z węglika spiekanego
    • Proste rowki do otworów przelotowych i podstawowych
    • Lewoskrętne rowki do otworów przelotowych
    • zakres ø: 3,00–20,00 mm

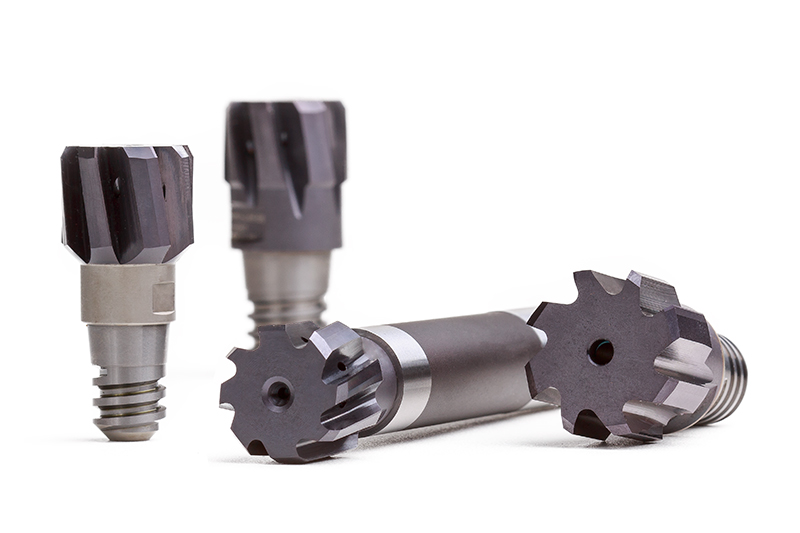
  • CPReam – CPR

    Wiertło z wymienną głowicą

    • Najwyższa możliwa stabilność i sztywność dzięki stożkowi i płaskiej powierzchni przylegania
    • Wysoka precyzja koncentryczności wynosząca 5 μm
    • Łatwa obsługa
    • Zakres ø: 8,00–40,00 mm

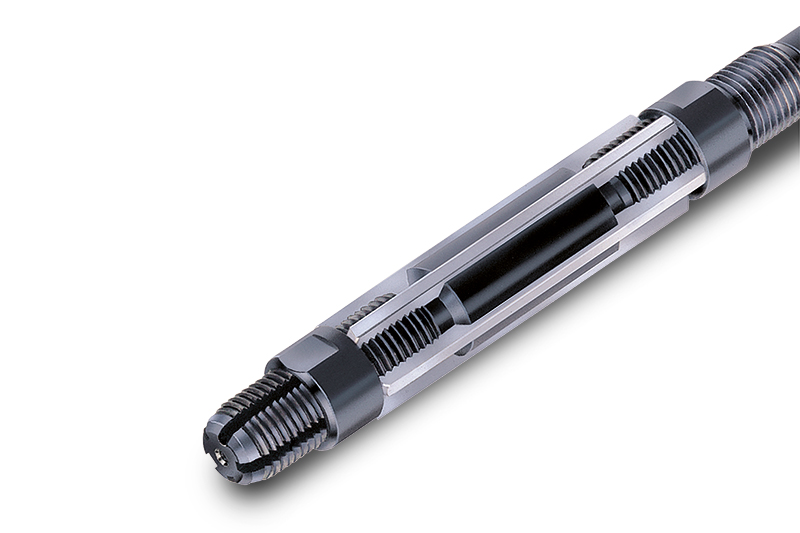
  • Wiertło z szybką regulacją – WN 50

    Ręczny rozwiertak

    • Szybko regulowany rozwiertak o dużym zakresie regulacji
    • Szczególnie nadaje się do prac naprawczych
    • Dostępne zestawy ostrzy zamiennych
    • zakres ø: 6,40 - 95,00 mm

  • Narzędzia prowadzone listwami

    Narzędzia z listwami prowadzącymi

    • Najwyższa dokładność dzięki koncepcji MAPAL
    • Bezpośrednie prowadzenie w otworze dzięki listwom prowadzącym
    • Precyzyjnie szlifowane płytki
    • Wysoka dokładność regulacji zapewniająca obróbkę otworów z dokładnością do μm

Technika mocowania
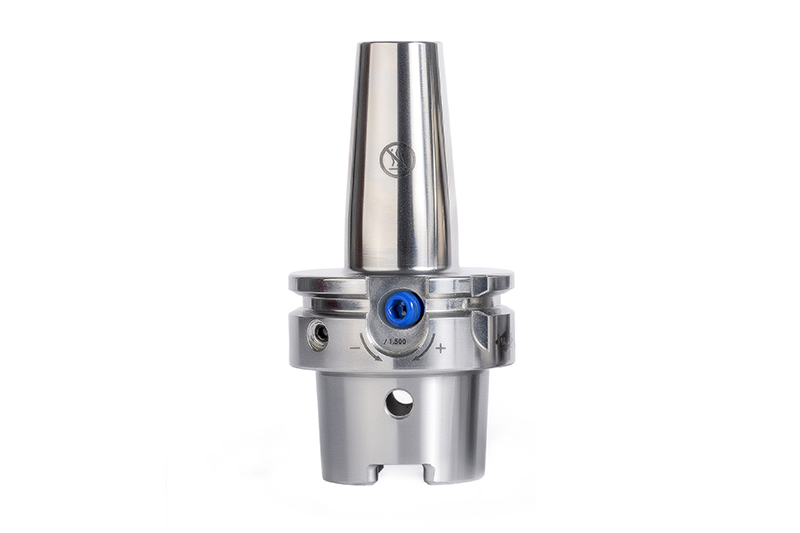
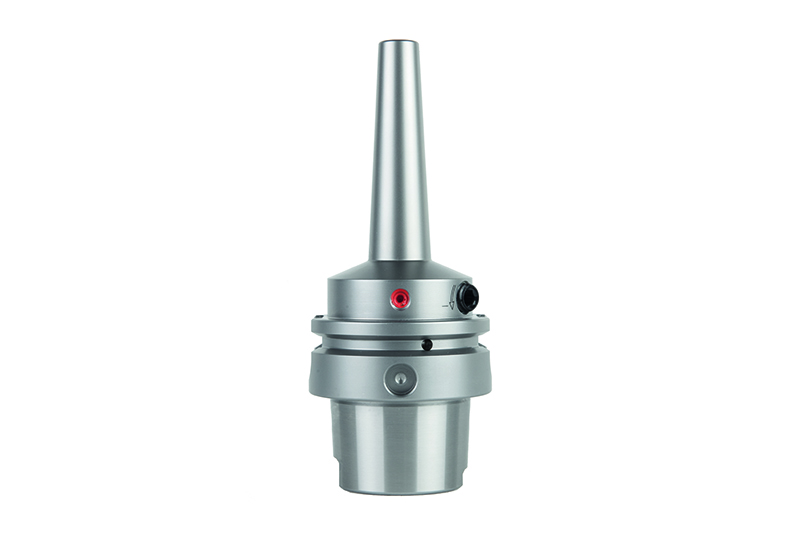
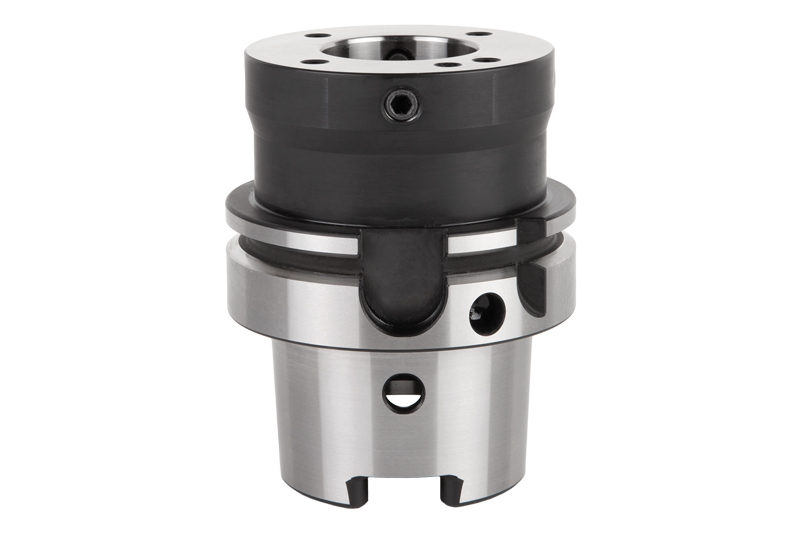
  • Uchwyt UNIQ DReaM, 4,5°

    Uchwyt hydrauliczny w nowej konstrukcji

    • Do zastosowań związanych z frezowaniem i wierceniem oraz do wykańczania podczas operacji frezowania
    • Optymalne połączenie właściwości geometrycznych i funkcjonalnych
    • Doskonała powierzchnia przy jednoczesnej poprawie obsługi
    • Maksymalna elastyczność i wydajność podczas obróbki elementów o krytycznych konturach

    Bezpośrednio do sklepu

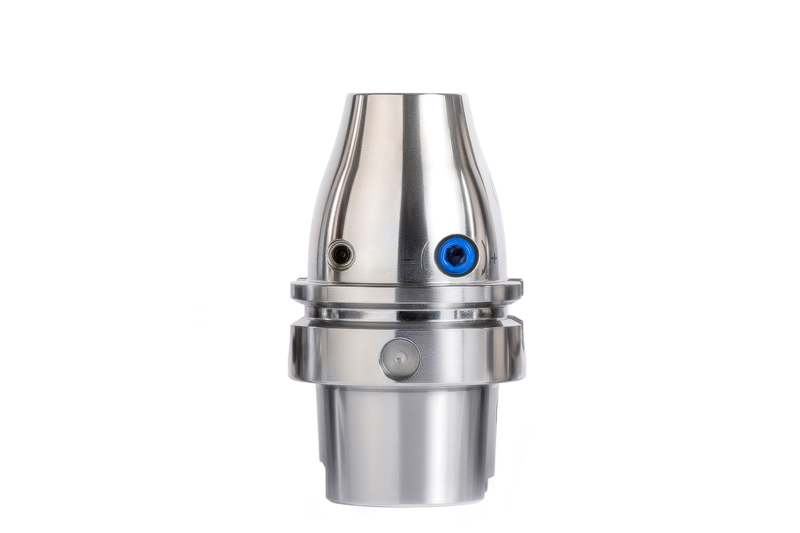
  • UNIQ Mill Chuck, HA

    Uchwyt hydroekspansyjny w nowej konstrukcji

    • Uchwyt hydroekspansyjny do wysoce dynamicznych zastosowań frezarskich
    • Optymalne współdziałanie właściwości geometrycznych i funkcjonalnych
    • Doskonałe wyniki przy stosowaniu narzędzi z chwytem HA
    • Najwyższe bezpieczeństwo procesu nawet w przypadku elementów o wysokiej jakości

    Przejdź bezpośrednio do sklepu

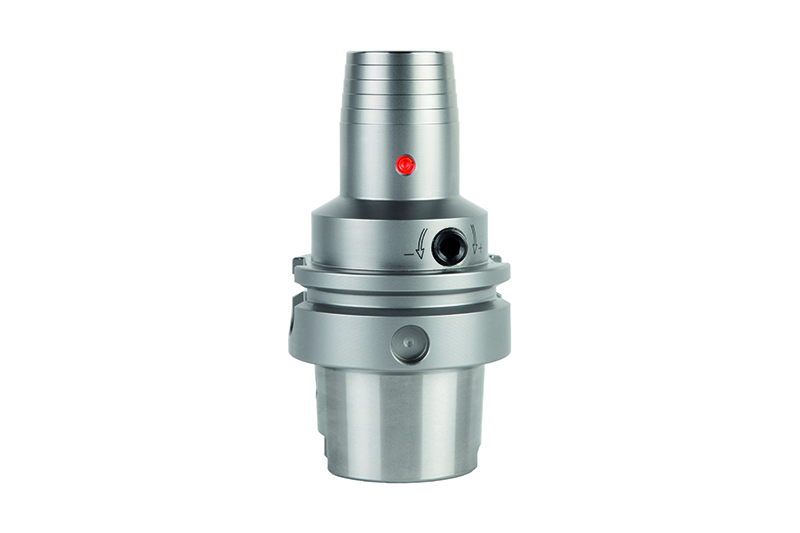
  • Uchwyt HighTorque HTC

    Uchwyt hydrauliczny

    • Wysokie przenoszenie momentu obrotowego
    • Idealne właściwości tłumiące
    • Doskonała sztywność całego systemu
    • Dokładność koncentryczności < 3 µm
    • Smukła konstrukcja 3° do zastosowań, w których kontur ma kluczowe znaczenie


    Przejdź bezpośrednio do sklepu

  • MAPAL HydroChuck MHC

    HydroChuck MHC

    Uchwyt hydrauliczny

    • Doskonałe tłumienie drgań
    • Wysoka dokładność koncentryczności
    • Ultra krótka wersja o kompaktowej konstrukcji zapewniającej wysoką sztywność


    Przejdź bezpośrednio do sklepu

  • Uchwyt termiczny MTC

    Tuleje skurczowe

    • Długa żywotność dzięki zastosowaniu stali narzędziowej o wysokiej odporności na temperaturę
    • Wysokie przenoszenie momentu obrotowego i sztywność promieniowa
    • Standardowo precyzyjnie wyważone
    • Odpowiednie do MMS
    • Z regulacją osiową długości narzędzia lub bez

    Przejdź bezpośrednio do sklepu

  • MAPAL MillChuck

    Uchwyt frezarski, system HB

    Oprawka mechaniczna
    • Łatwa obsługa dzięki śrubie różnicowej
    • Najwyższa ekonomiczność i precyzja
    • Zdefiniowane osiowe pozycjonowanie narzędzia dzięki systemowi sprężynowemu
    • Zdecentralizowane wyloty chłodziwa dla maksymalnego bezpieczeństwa procesu


    Przejdź bezpośrednio do sklepu

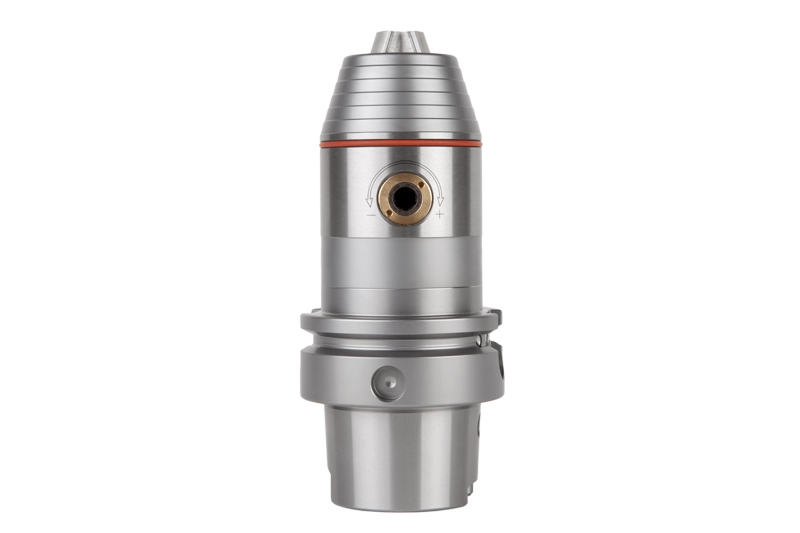
  • MAPAL Precision-DrillChuck MPC

    Precision-DrillChuck – MPC

    Precyzyjne uchwyty wiertarskie

    • Prosta konstrukcja i łatwa obsługa
    • Bezpieczeństwo mocowania niezależne od kierunku obrotów
    • Wysoka odporność na prędkości obrotowe
    • Modułowa konstrukcja umożliwia stosowanie głowic uchwytów wiertarskich we wszystkich interfejsach narzędziowych

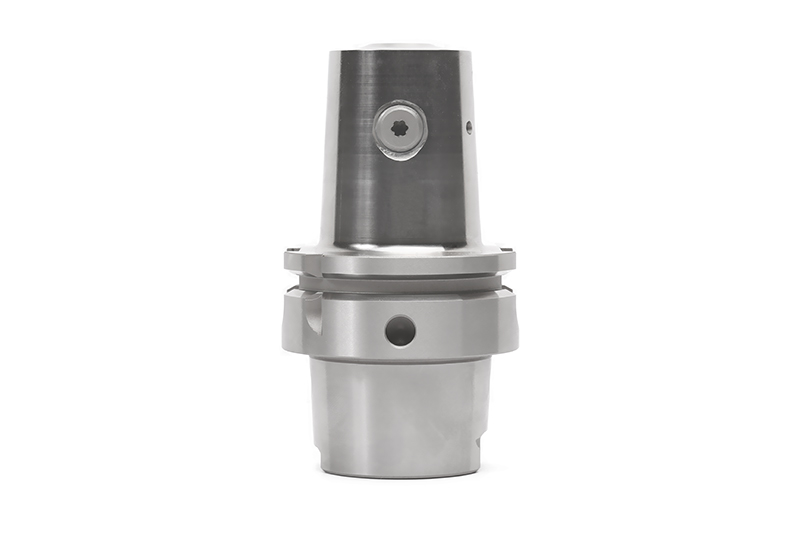
  • MAPAL slip-on reamer arbor

    Trzpień frezarki nasadowej – MDA / MCA

    Trzpień frezów nasadowych

    • Wersja z tłumieniem drgań (MDA) z systemem eliminacji drgań
    • Dostosowany do sztywności wszystkich popularnych typów maszyn
    • Cicha, stabilna praca pomimo długiego wysięgu dla lepszej jakości powierzchni
    • Trzpień do frezów nasadowych (MCA) ze zwiększoną powierzchnią czołową do operacji zgrubnych i wstępnych w dużych zakresach średnic

  • MAPAL MFS milling head holder

    Uchwyt frezarki MFS

    Uchwyt narzędziowy do frezów wkręcanych

    • Łatwe i szybkie mocowanie frezów wkręcanych
    • Precyzyjna współpraca stożka i płaszczyzny przylegania
    • Najwyższy poziom stabilności i sztywności
    • Uniwersalne zastosowanie do operacji zgrubnych i wykańczających

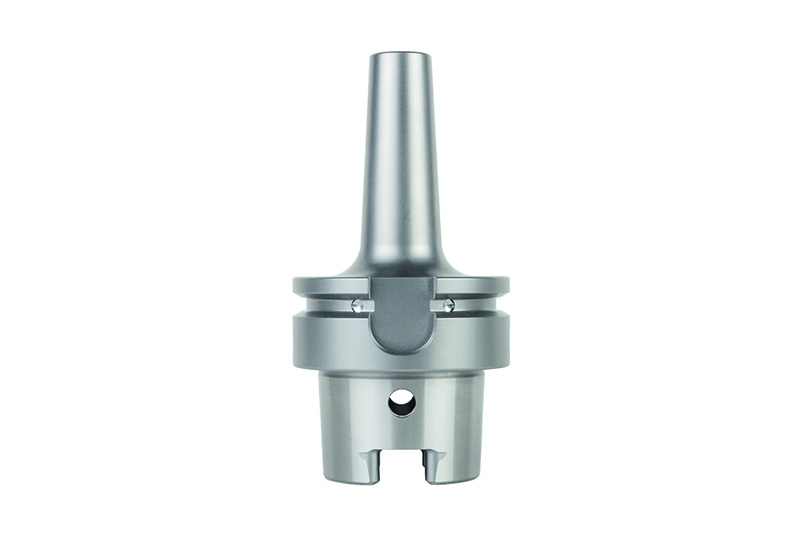
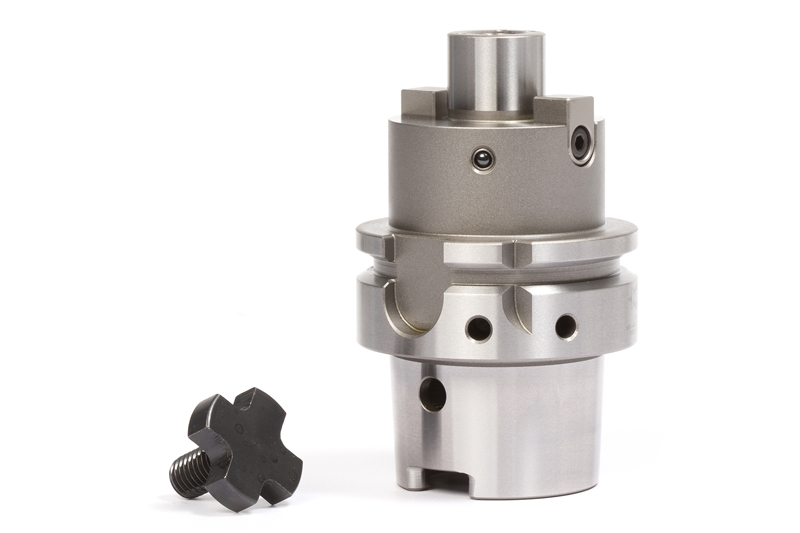
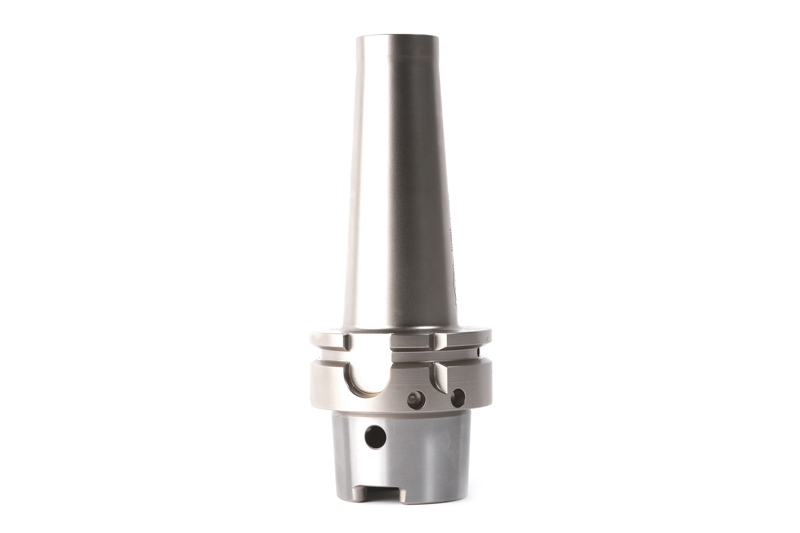
  • MAPAL HSK adapter

    Adapter

    Przedłużki, reduktory i adaptery

    • Różnorodne możliwości dla modułowych systemów narzędziowych
    • Przedłużki hydrauliczne i skurczowe
    • Reduktory i przedłużki HSK
    • Adaptery stożkowe KS


    Przejdź bezpośrednio do sklepu


Komponenty i materiały

Od surowca do gotowego elementu

Kilka kliknięć wystarczy, aby znaleźć odpowiednie Narzędzie: w zależności od obróbki, konkretnej operacji i wymagań dotyczących narzędzia, szybko znajdziesz pożądane Narzędzie.
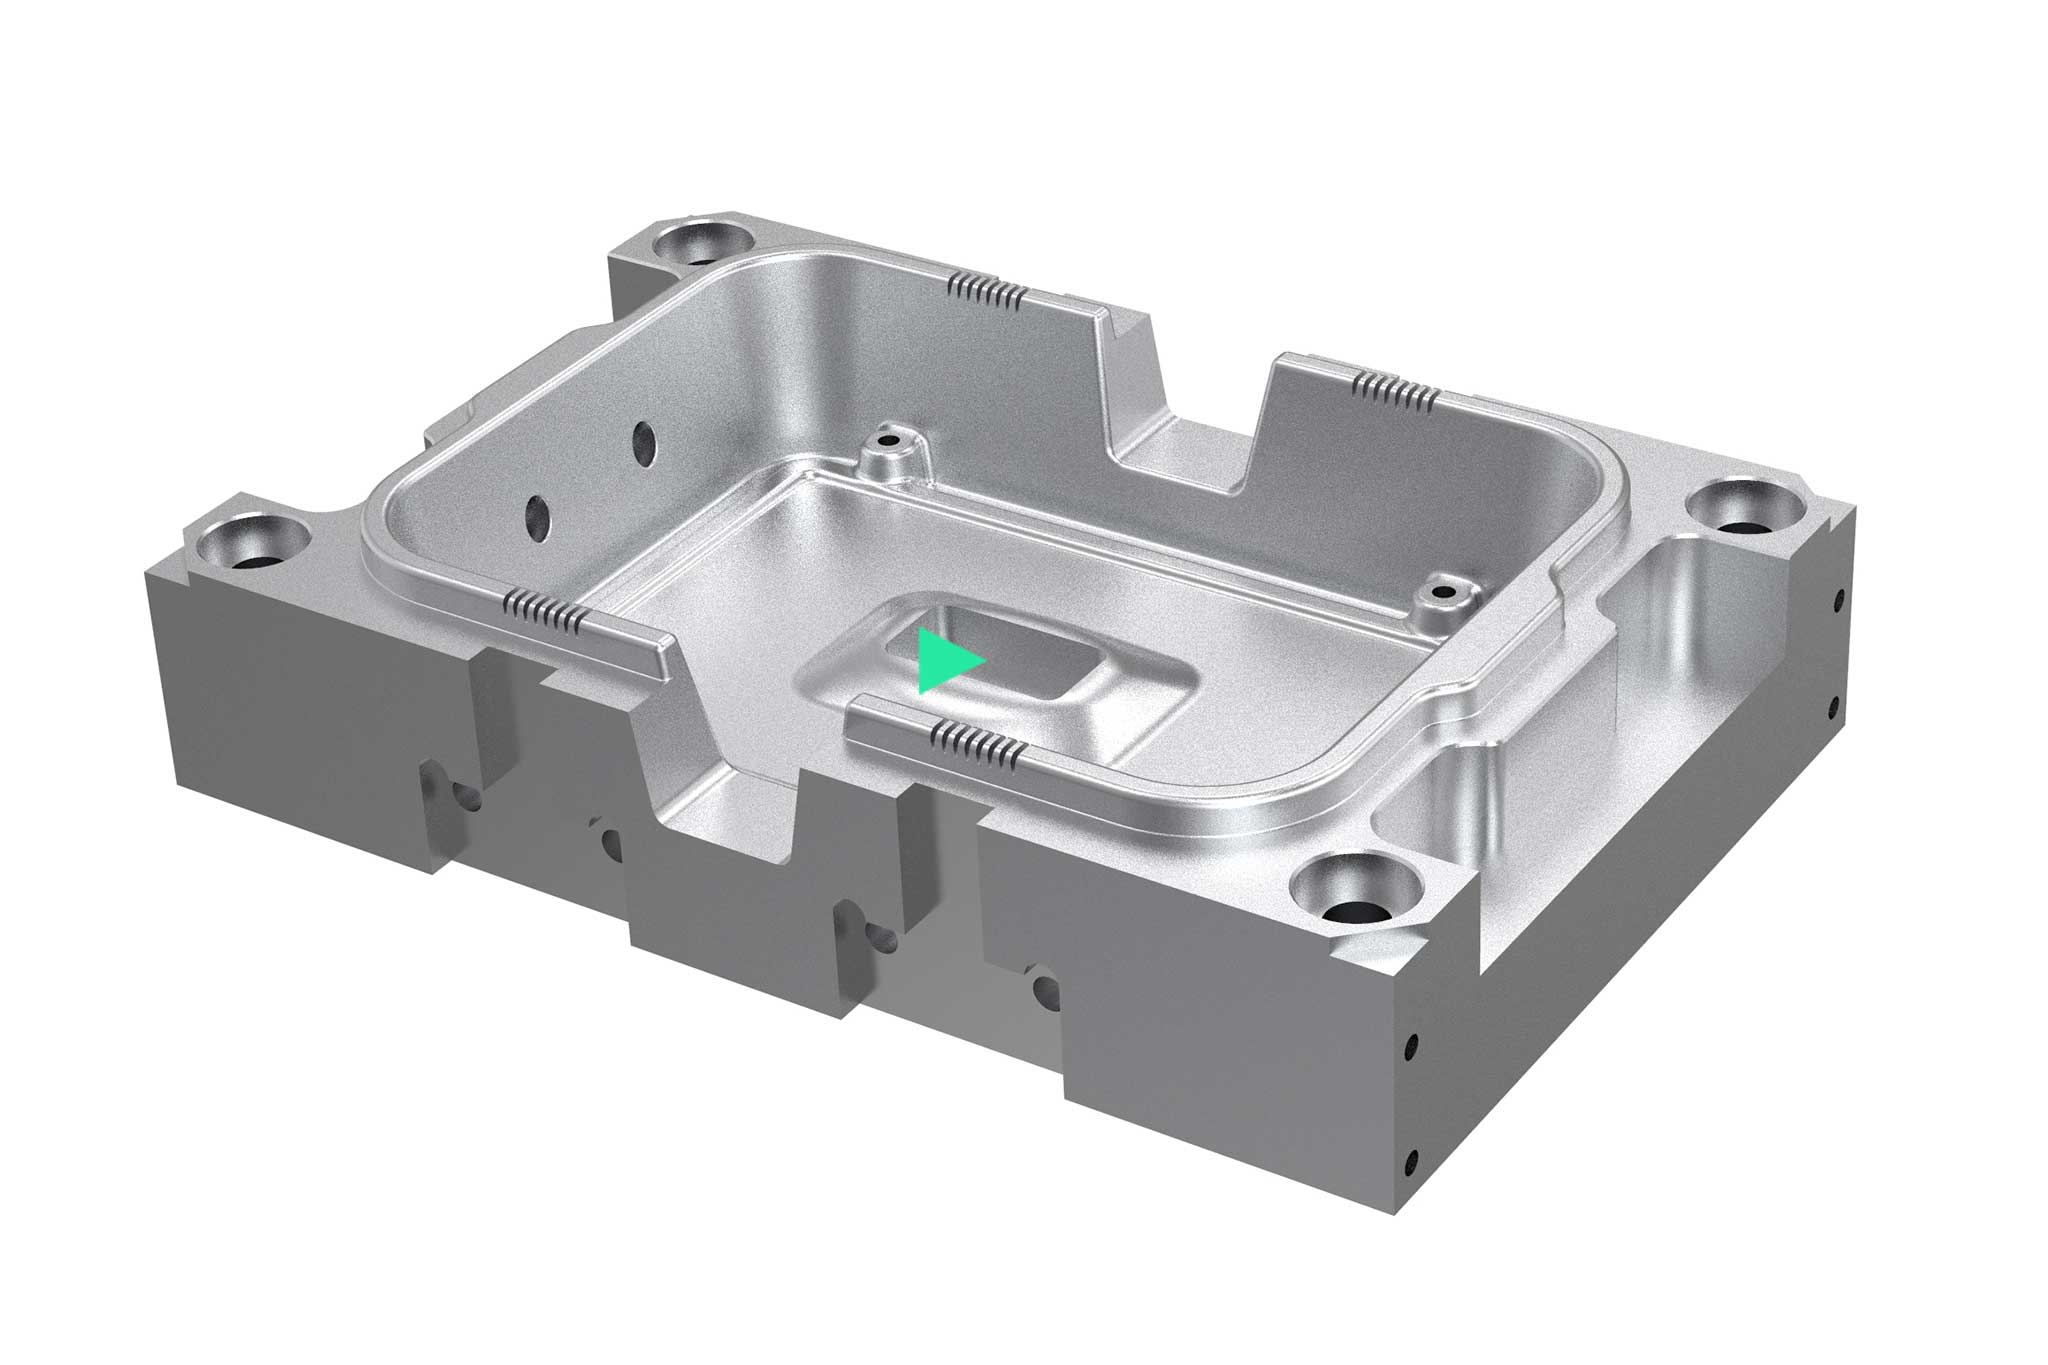
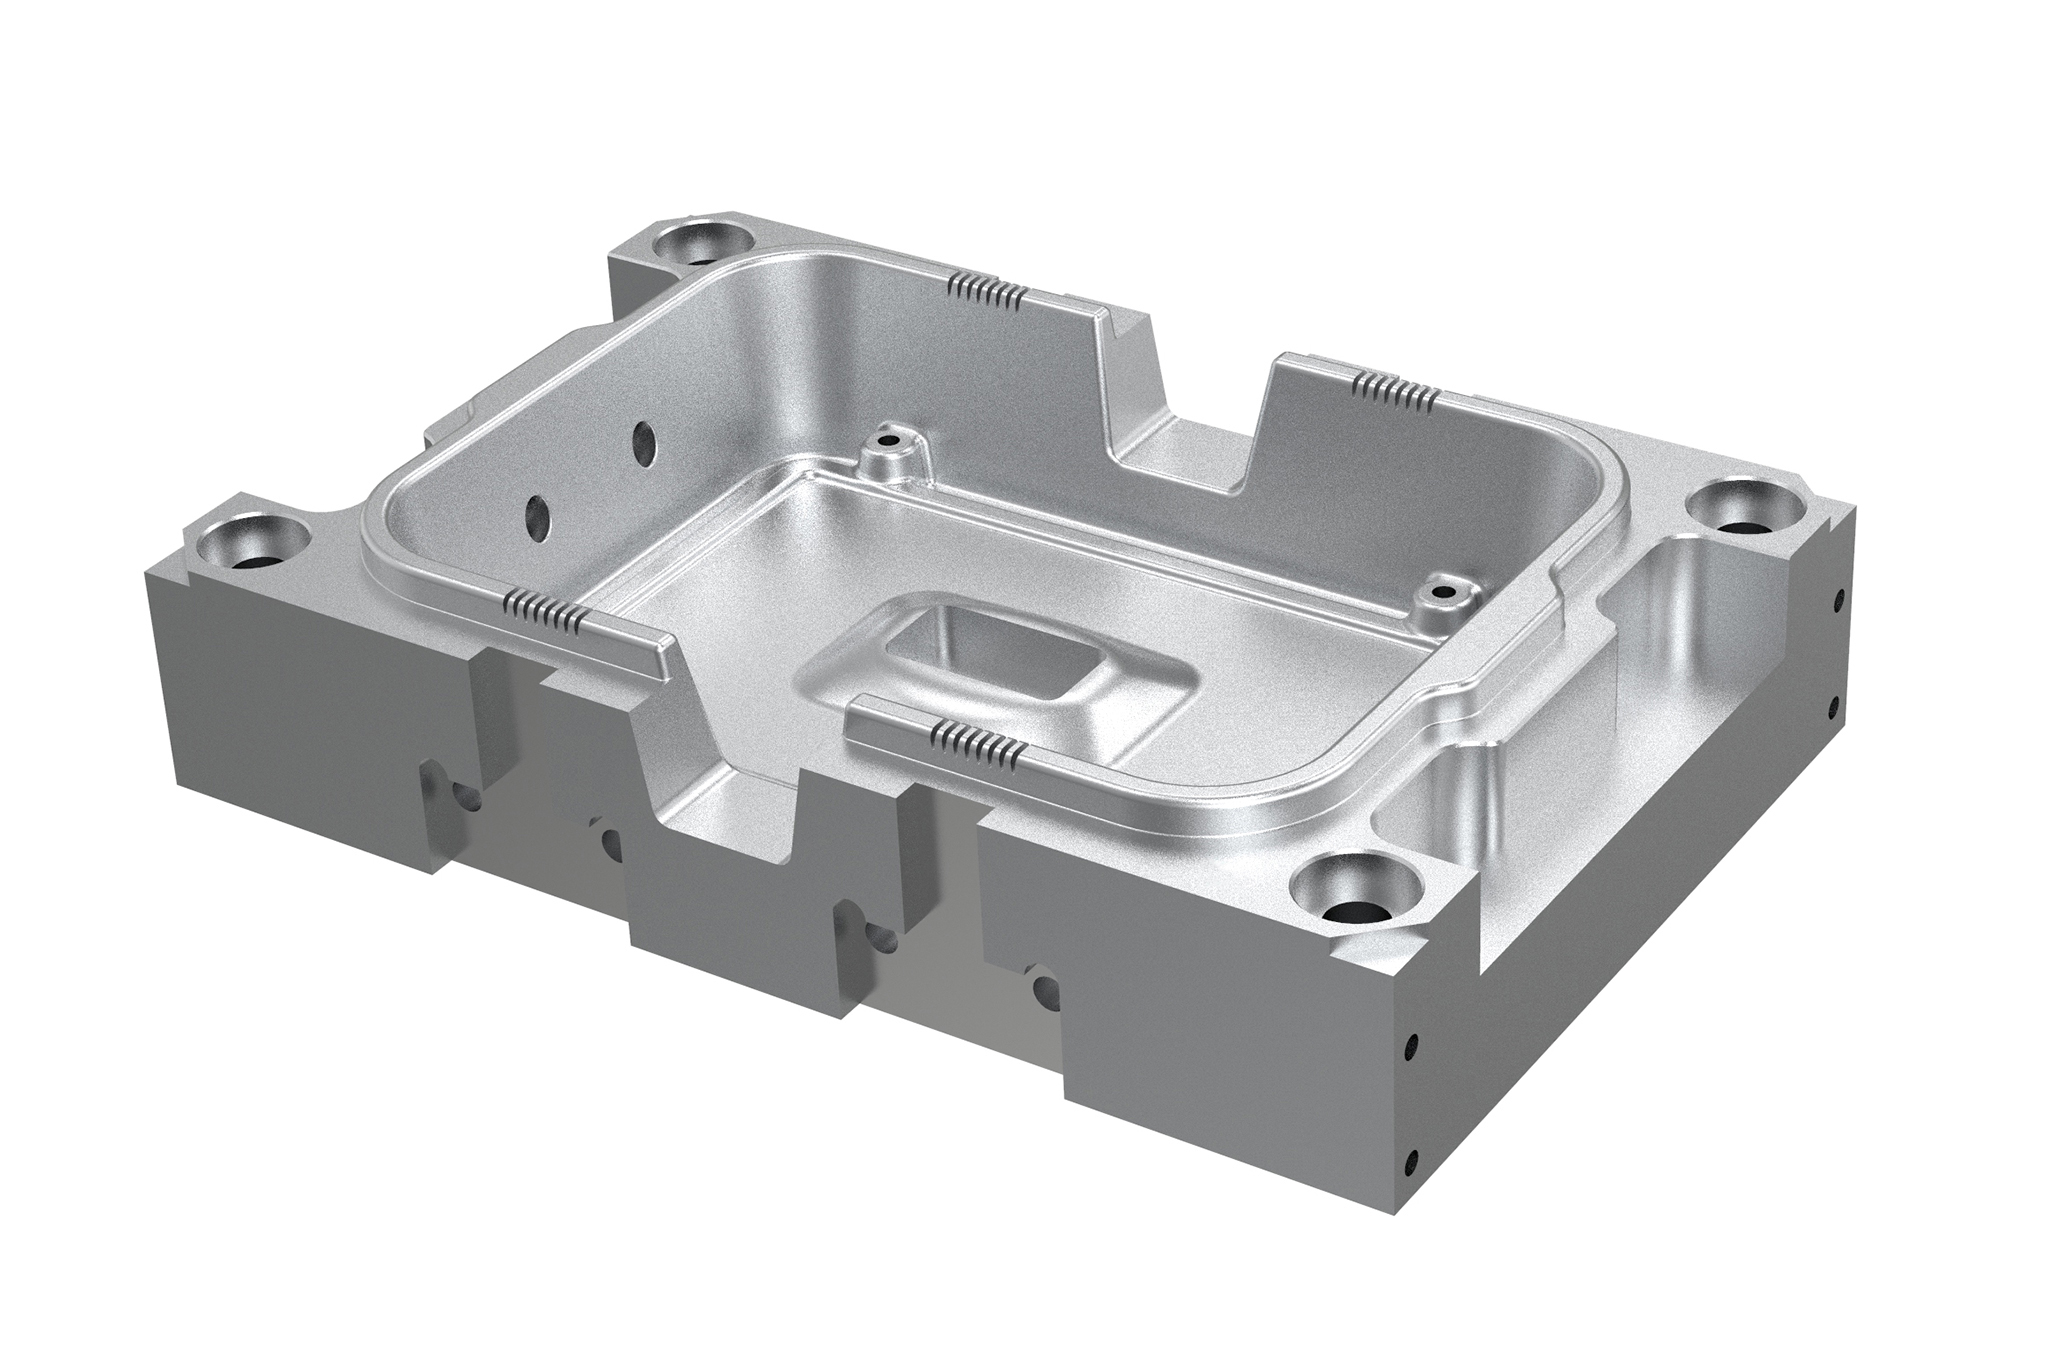
  • On a rendered example component, an operation is highlighted.
    1 / 8

    Powierzchnie 2D

    Do tej kategorii należą z jednej strony procesy obróbki wykonywane bezpośrednio na maszynie, takie jak frezowanie płaskie, frezowanie kieszeni i prostych ścianek. Z drugiej strony są to również operacje dotyczące złożonych geometrii, które są programowane za pomocą oprogramowania CAM.

    Do programu produktów do obróbki powierzchni 2D
  • On a rendered example component, an operation is highlighted.
    2 / 8

    Powierzchnie 3D

    W produkcji narzędzi i form codziennością jest wytwarzanie coraz bardziej złożonych kształtów. Ciągły rozwój obrabiarek i oprogramowania CAM podnosi wydajność i produktywność na coraz wyższy poziom. W związku z tym również stosowane narzędzia muszą być zawsze zgodne z najnowszym stanem techniki. Aby osiągnąć optymalne wyniki, na początku projektowania przeprowadza się analizę procesu.
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
  • On a rendered example component, an operation is highlighted.
    3 / 8

    Otwarte kieszenie

    Wkładki formujące mają również zadania obróbcze, które są niezbędne do odlewania lub różnych elementów montażowych. Otwarte kieszenie (obróbka obwodowa) są coraz częściej obrabiane przez użytkowników za pomocą frezowania trochoidalnego. Ta metoda obróbki pomaga zoptymalizować czas obróbki i wydłużyć żywotność narzędzi.
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​​​​​​
    ​​
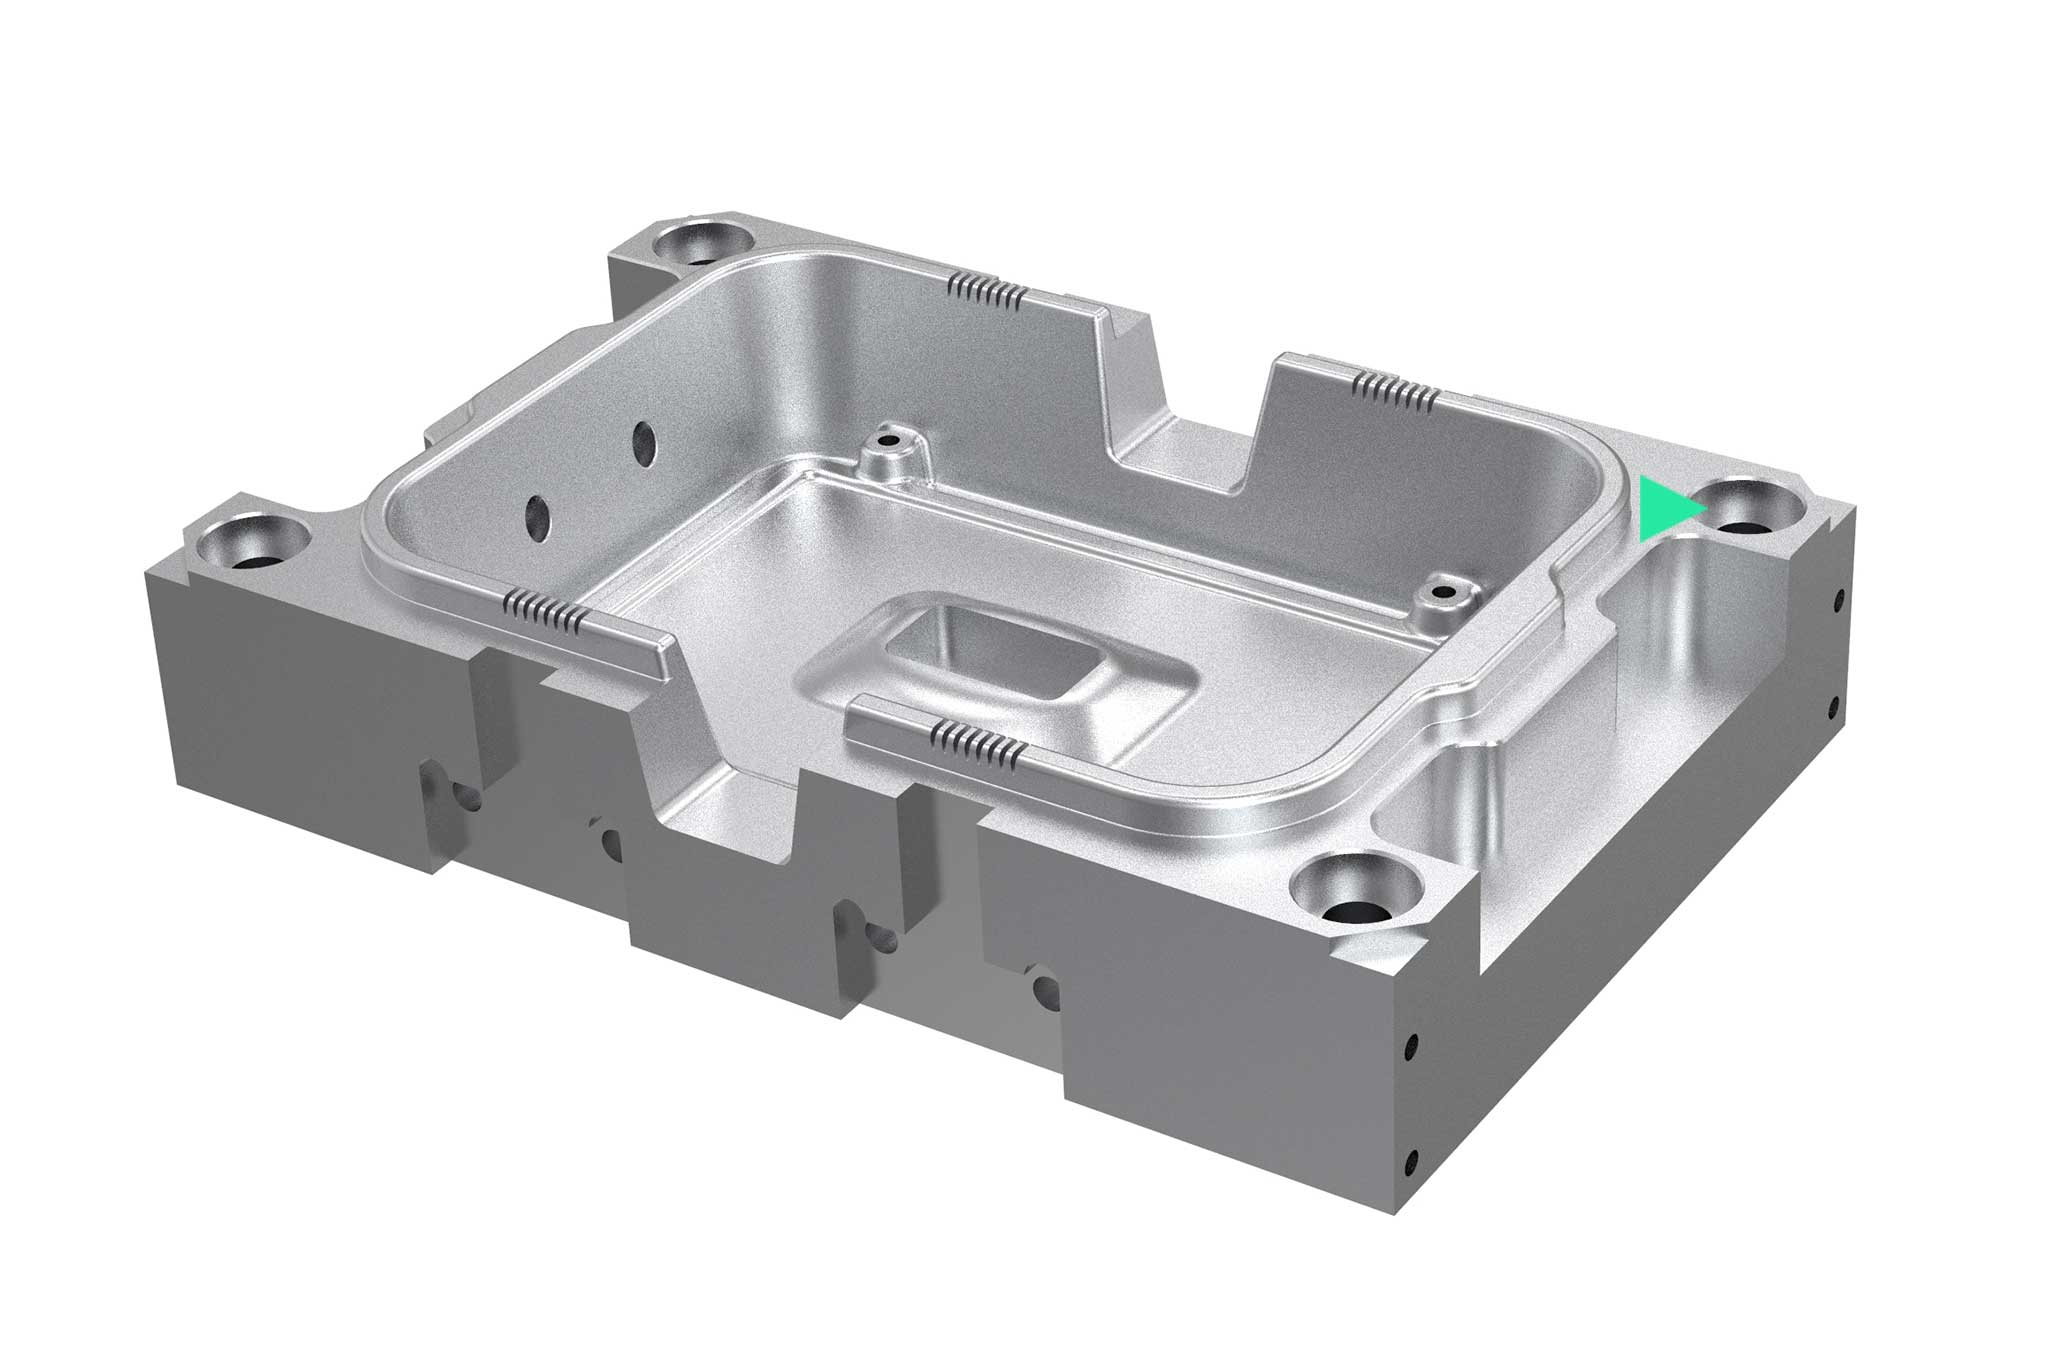
  • On a rendered example component, an operation is highlighted.
    4 / 8

    Zamknięte kieszenie

    Produkcja zamkniętych kieszeni odbywa się zazwyczaj poprzez obróbkę zgrubną w płaszczyznach Z. Często podczas frezowania wybiera się wejście w obróbkę poprzez rampę. Wybór narzędzia zależy od głębokości ścianek i kąta skosu, jaki ma zostać utworzony na elemencie. Szeroka oferta modułowych systemów MAPAL obejmuje również obróbkę głębokich kieszeni o dużych średnicach.

    Do programu produktów do obróbki zamkniętych kieszeni
  • On a rendered example component, an operation is highlighted.
    5 / 8

    Helix milling

    A major focus in milling operations is on reducing the machining time. With specific tool geometries for machining closed, round pockets, it is often possible to eliminate the pre-drilling process. With helix milling, milling paths are programmed with helical entrances that are suitable for pocket dimensions.

    Go to the helix milling product range
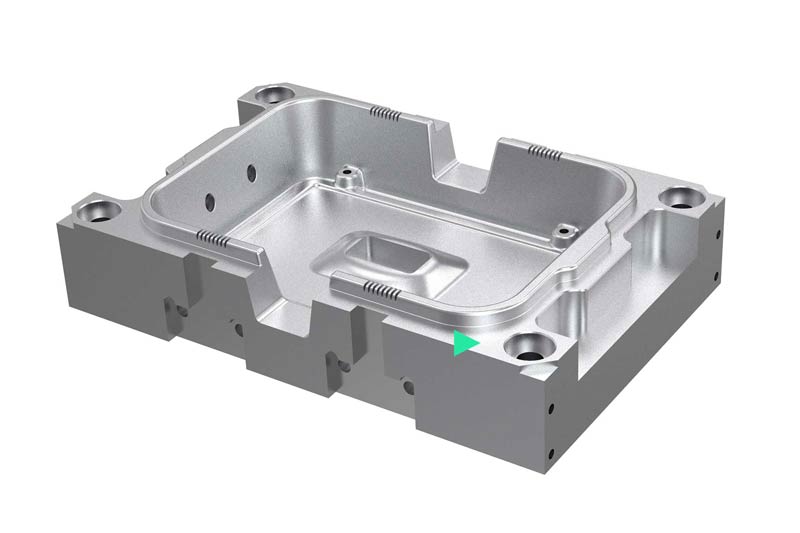
  • On a rendered example component, an operation is highlighted.
    6 / 8

    Even surfaces

    Operations to create even surfaces occur very frequently and in different areas in the die & mould sector: It could be component-related, strategy-related due to the respective milling process or due to requirements for mould closing surfaces as well as sections and cutting dies. The right tool is then selected depending on the application and requirements.

    Go to the product range for machining even surfaces
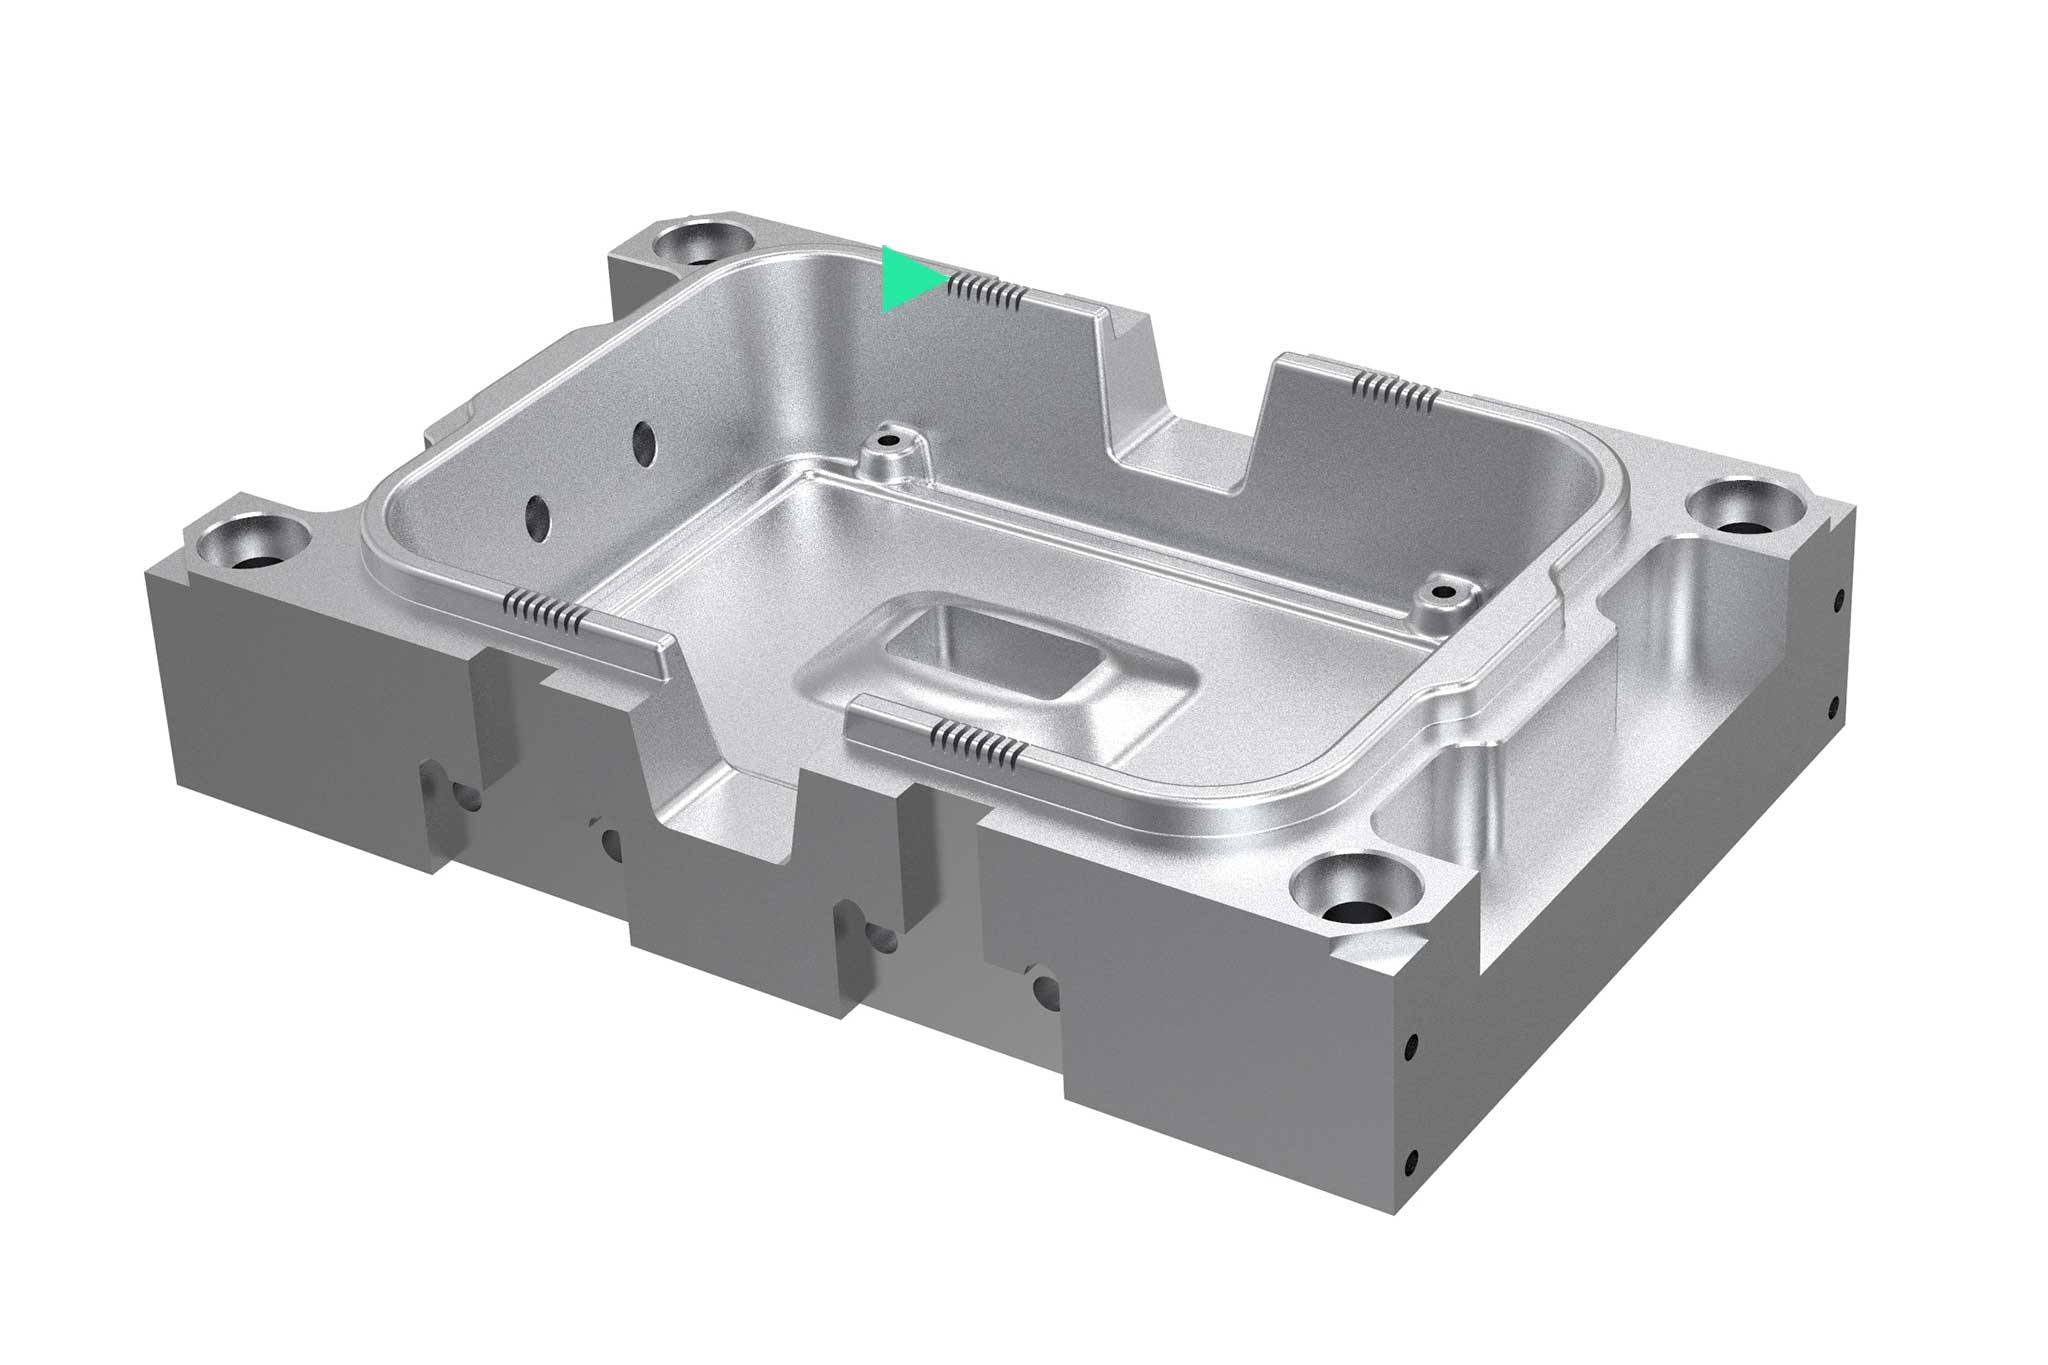
  • On a rendered example component, an operation is highlighted.
    7 / 8

    Cienkie ścianki i żebra

    Formy do wtrysku tworzyw sztucznych i formy do odlewania ciśnieniowego często mają żebra i cienkie ścianki. Na przykład żebra są coraz częściej frezowane, ponieważ proces ten jest tańszy niż proces EDM (erozja iskrowa). Zazwyczaj stosuje się długie lub bardzo długie narzędzia z węglika spiekanego o małych średnicach. Możliwe są również rozwiązania dostosowane do indywidualnych potrzeb klienta (RibCutter), dopasowane do kształtu żeberek.
    ​​​​​​​
    ​​​​​​​Do asortymentu produktów do obróbki cienkich ścianek i żeberek
  • On a rendered example component, an operation is highlighted.
    8 / 8

    Małe i duże otwory

    W produkcji narzędzi i form istnieje szeroki zakres operacji wiercenia pełnego: od dużych otworów dla kolumn prowadzących, przez głębokie otwory dla układu chłodzenia, aż po wysoce precyzyjne otwory dla sworzni wyrzutnika. MAPAL oferuje szeroki asortyment narzędzi do wiercenia i wytaczania dla poszczególnych etapów produkcji.
    ​​​​​​​
    ​​​​​​​Do asortymentu produktów do obróbki małych i dużych otworów
Wszystko z jednej ręki
  • 1. Planning and purchasing

    Optimised purchasing management is important for a clear organisation of the tool stock.

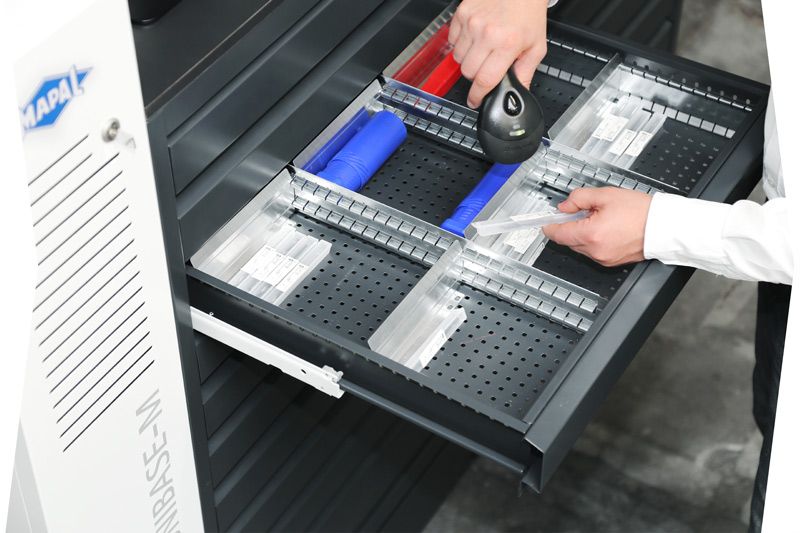
  • 2. Tool logistics

    Cost-effectiveness even in the periphery of machining: Intelligent dispensing systems significantly reduce non-productive times.

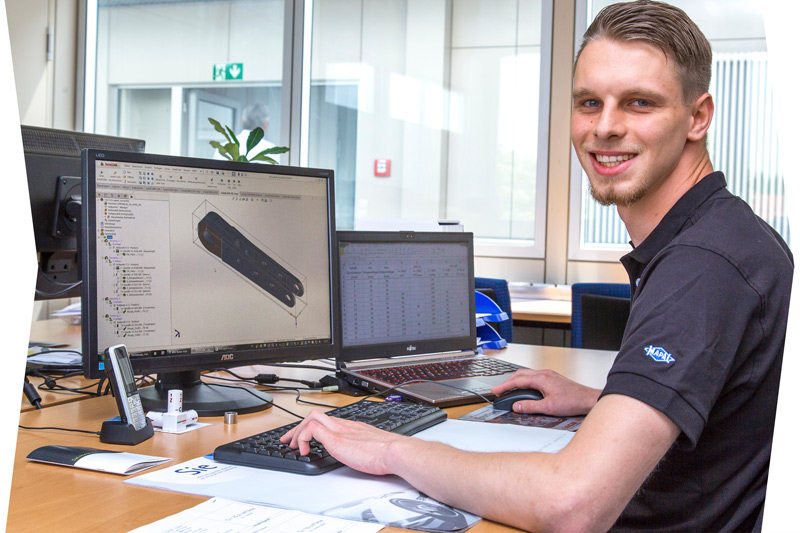
  • 3. Engineering

    The machining specialists provide support with process engineering, e.g. in the form of CAM simulations, general advice and the development of economic machining strategies.

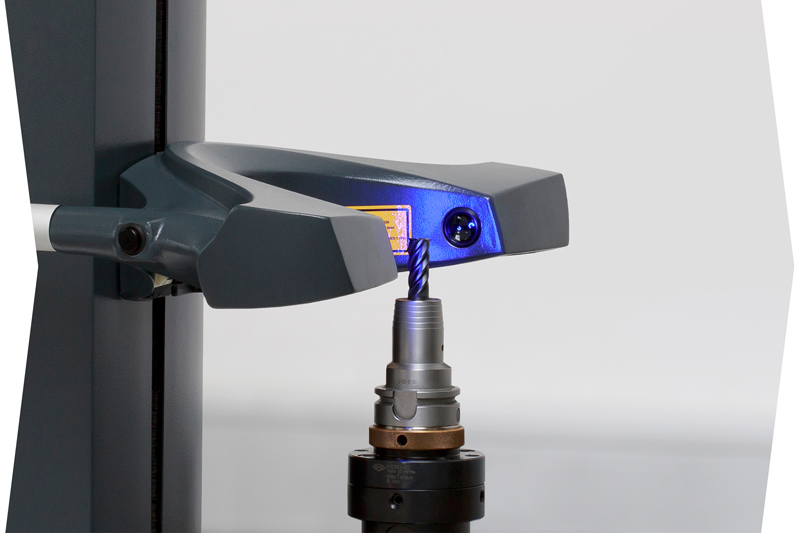
  • 4. Measuring and setting

    Reliable setting and measuring devices are convincing due to their accuracy and user-friendly operation when setting the tools.

  • 5. Tools and clamping technology

    From the spindle to the cutting edge – MAPAL offers a wide range of tools and clamping technology for the die & mould sector.

  • 6. Machining

    Efficient machining processes and customised machining strategies at the highest technological level.

  • 7. Digitisation and automation

    Quick and easy digitisation: The c-Connect Box digitally transmits measurement data from the setting fixture to the machine tool. It also monitors the machine status among other things.

  • 8. Reconditioning

    Customers receive their reconditioned tools back in manufacturer quality within a very short time. Also available with pick-up and delivery service upon request.


Engineering Workflow - From theory to practice
Finding the perfect solution for the customer is MAPAL’s main goal. In addition to individual custom solutions and a broad standard product portfolio, comprehensive services are available to optimally design the entire process from the product idea to the chip. Customers can rely on the technology leader’s many years of experience in machining.
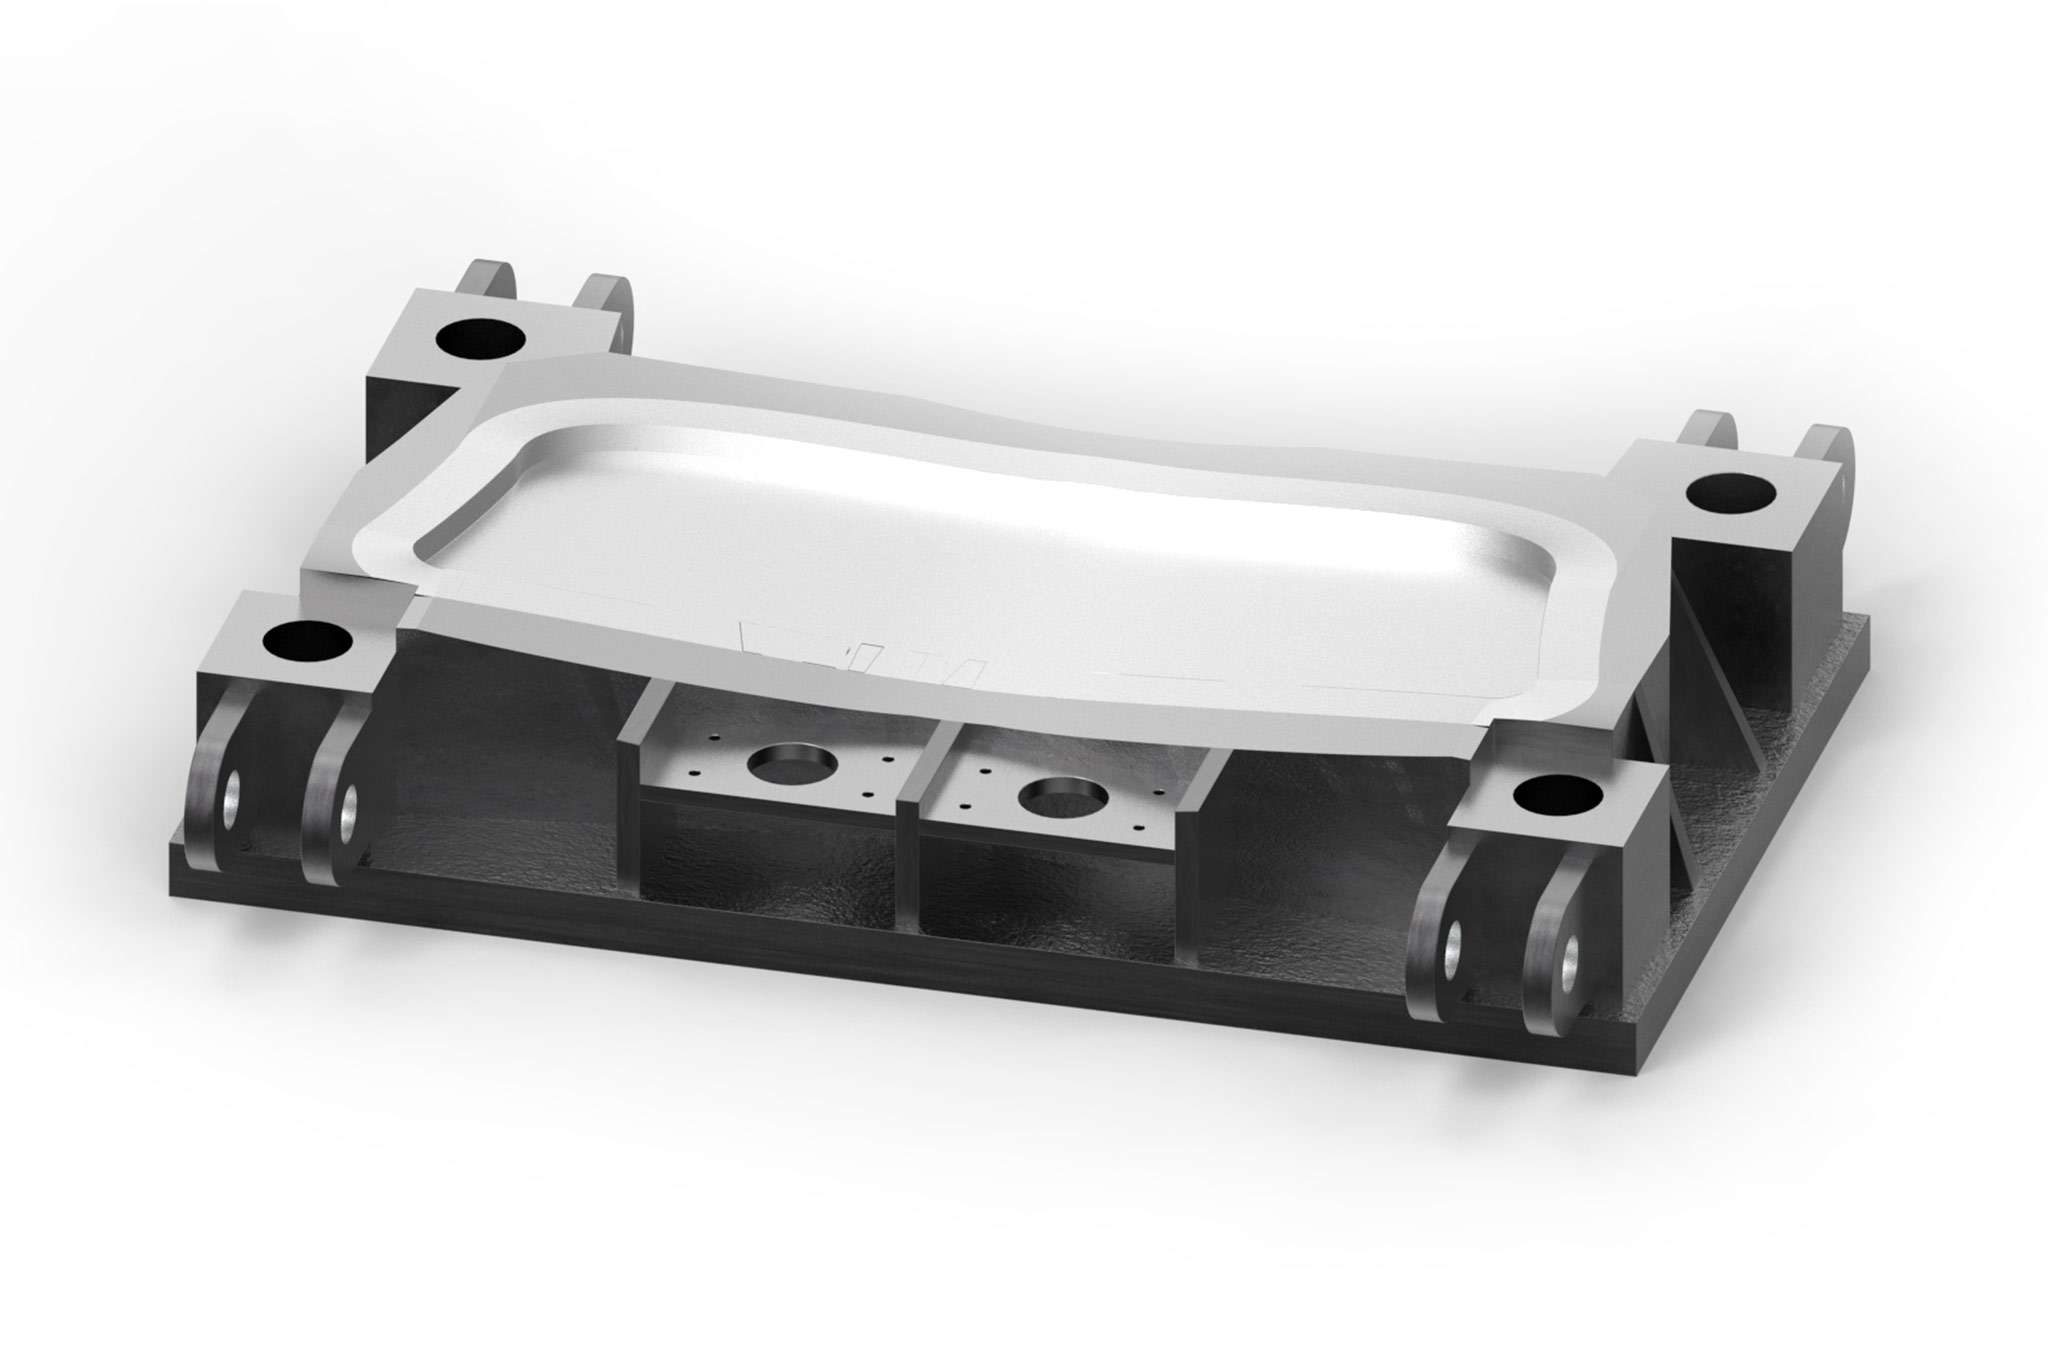
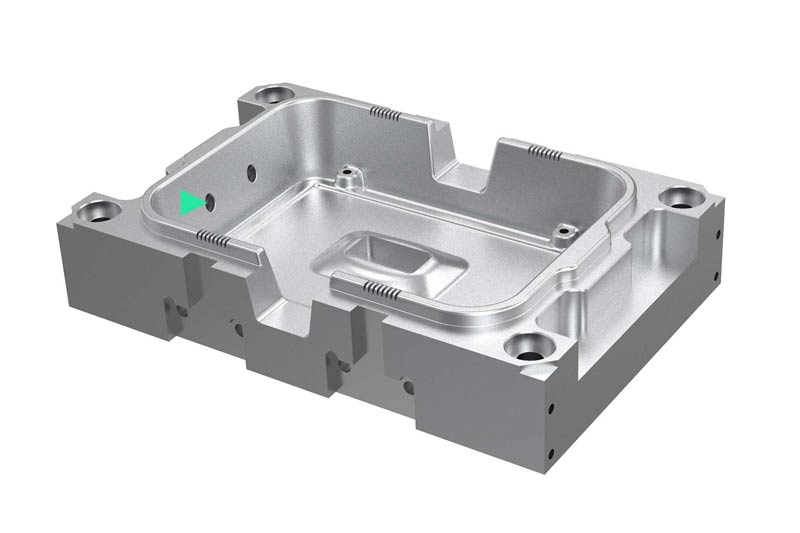
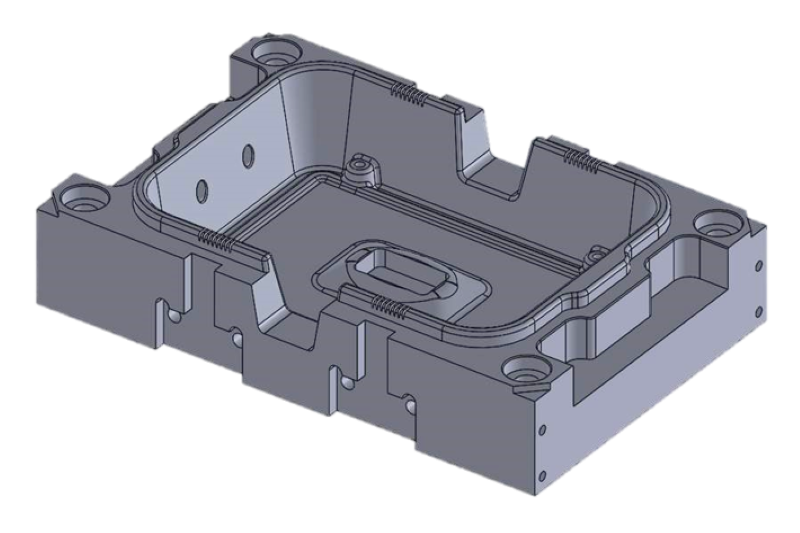
  • 3D model of a workpiece from the die and mould making.

    1. Customer enquiry

    MAPAL sales representatives are directly available for individual enquiries. In a personal conversation with the customer, they sound out the specific requirements and the scope (complete or partial machining) and discuss the details directly on the 3D model of the component.

    The MAPAL die & mould team looks forward to your enquiry by ​​​​​​​Email and will contact you directly as soon as possible.

  • 3D model of a workpiece from the die and mould making.

    2. Project analysis

    On the basis of 3D models and machine data, the conversation partners analyse the manufacturing tasks and develop effective machining strategies.

    The project analysis consists of the following:​​​​​​​
    • Machining suggestions for all machining steps
    • Tool list
    • Process optimisation

  • 3. Process design

    Regardless of whether the focus is on flexibility or productivity: The machining specialists simulate the developed process on the basis of the 3D models and thus show potential for optimisation. They check and improve the machining parameters in CAM programming and thus ensure stable and economical production.

    The process design includes:​​​​​​​
    • Runtime analysis of the component
    • Technology data definition
    • CAM programming

  • Overview of all MAPAL tool solutions for die and mould making in one workpiece.

    4. Tool solution

    The wide-ranging MAPAL standard range for the die & mould sector offers the ideal tool solution for every application. Customised solutions are available upon request.

    Advantages for the user:​​​​​​​
    • Broad standard range
    • Availability of tool data

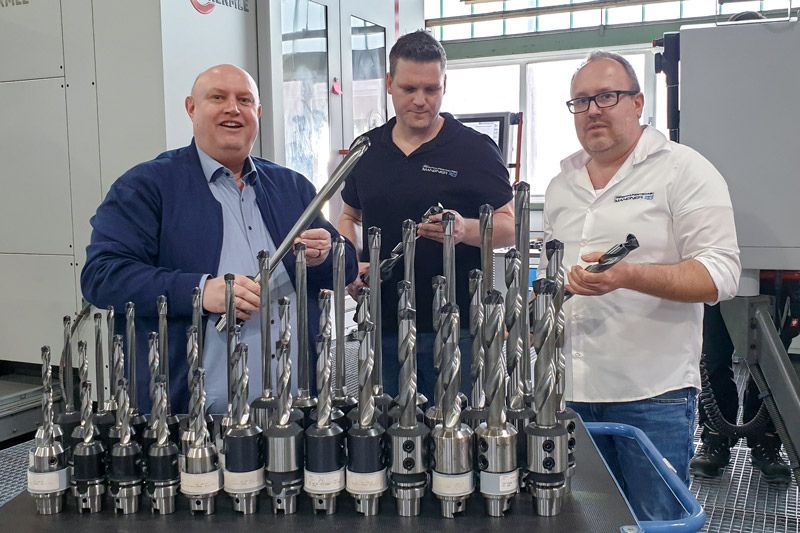
  •  The picture shows a technical advisor from MAPAL in conversation with a customer.

    5. Tool test and offer

    After discussing the machining task, MAPAL supports its customers in the selection of tools required in the process. This is the basis for a well-founded offer tailored to the respective application.

  • The picture shows documents for preparing offers on a table with three people.

    6. Cooperative partnership

    Even after mutual success, the specialists at MAPAL remain in close contact with the customer. Should optimisation potential arise over time or other tools turn out to be better, MAPAL will be happy to support you to further improve productivity and profitability.

    In order to ensure efficient production in the long term, MAPAL also offers comprehensive tool management options.
    ​​​​​​​
    Tool management options:

    • Dispensing systems
    • Regrinding service
    • Comprehensive product portfolio of adjustment and measuring devices


Further items about the die&mould area


Our retail partners

Responsibility according to postcode areas

  • 1 / 16

    Postcode 35

    FRITZ WEG GmbH & Co. KG
    Ahornweg 41
    35713 Eschenburg-Wissenbach

    Phone: +49 2774 701-0
    Fax: +49 2774 701-39
    Email: info@fritzweg.de
    Web: www.fritzweg.de

  • 2 / 16

    Postcode 44

    Jansen Schneidwerkzeuge Vertriebs GmbH
    Im Käsebrink 12
    58840 Plettenberg

    Phone: +49 2391 9177-0
    Fax: +49 2391 9177-20
    Email: info@j-s-v.com
    Web: www.j-s-v.com

  • 3 / 16

    Postcode 51

    Jansen Schneidwerkzeuge Vertriebs GmbH
    Im Käsebrink 12
    58840 Plettenberg

    Phone: +49 2391 9177-0
    Fax: +49 2391 9177-20
    Email: info@j-s-v.com
    Web: www.j-s-v.com

  • 4 / 16

    Postcode 56, 57

    FRITZ WEG GmbH & Co. KG
    Ahornweg 41
    35713 Eschenburg-Wissenbach

    Phone: +49 2774 701-0
    Fax: +49 2774 701-39
    Email: info@fritzweg.de
    Web: www.fritzweg.de

  • 5 / 16

    Postcode 58, 59

    Jansen Schneidwerkzeuge Vertriebs GmbH
    Im Käsebrink 12
    58840 Plettenberg

    Phone: +49 2391 9177-0
    Fax: +49 2391 9177-20
    Email: info@j-s-v.com
    Web: www.j-s-v.com

  • 6 / 16

    Postcode 60, 61

    Heinrich Meier GmbH
    Herrenwaag 31
    75417 Mühlacker

    Phone: +49 7041 9530-0
    Fax: +49 7041 9530-30
    Email: info@heinrich-meier.de
    Web: www.heinrich-meier.de

  • 7 / 16

    Postcode 63 - 69

    Heinrich Meier GmbH
    Herrenwaag 31
    75417 Mühlacker

    Phone: +49 7041 9530-0
    Fax: +49 7041 9530-30
    Email: info@heinrich-meier.de
    Web: www.heinrich-meier.de

  • 8 / 16

    Postcode 70 - 73

    Dieter Schätzle GmbH & Co. KG
    Präzisionswerkzeuge
    Unter Haßlen 12
    78532 Tuttlingen

    Phone: +49 7462 9465-0
    Fax: +49 7462 9465-50
    Email: info@schaetzle-werkzeuge.de
    Web:​​​​​​​ www.schaetzle-werkzeuge.de

  • 9 / 16

    Postcode 74, 75

    Heinrich Meier GmbH
    Herrenwaag 31
    75417 Mühlacker

    Phone: +49 7041 9530-0
    Fax: +49 7041 9530-30
    Email: info@heinrich-meier.de
    Web: www.heinrich-meier.de

  • 10 / 16

    Postcode 76 - 79

    Dieter Schätzle GmbH & Co. KG
    Präzisionswerkzeuge
    Unter Haßlen 12
    78532 Tuttlingen

    Phone: +49 7462 9465-0
    Fax: +49 7462 9465-50
    Email: info@schaetzle-werkzeuge.de
    Web:​​​​​​​ www.schaetzle-werkzeuge.de

  • 11 / 16

    Postcode 80 - 87

    AB1-Tools e.K.
    Goethering 45
    91732 Merkendorf

    Phone: +49 9826 333-2241
    Fax: +49 9826 333-3691
    Email: info@ab1-tools.com
    Web: www.ab1-tools.com

  • 12 / 16

    Postcode 88, 89

    Dieter Schätzle GmbH & Co. KG
    Präzisionswerkzeuge
    Unter Haßlen 12
    78532 Tuttlingen

    Phone: +49 7462 9465-0
    Fax: +49 7462 9465-50
    Email: info@schaetzle-werkzeuge.de
    Web:​​​​​​​ www.schaetzle-werkzeuge.de

  • 13 / 16

    Postcode 90 - 97

    AB1-Tools e.K.
    Goethering 45
    91732 Merkendorf

    Phone: +49 9826 333-2241
    Fax: +49 9826 333-3691
    Email: info@ab1-tools.com
    Web: www.ab1-tools.com

  • 14 / 16

    Danmark

    EDECO TOOL APS 
    Naverland 2
    2600 Glostrup
    Danmark

    Phone: +45 7060 2029
    Email: info@edeco.dk
    Web: www.edeco.dk

  • 15 / 16

    Italy

    TEKNOS S.r.l.
    Via A. Pigafetta, 2
    35011 Campodarsego (PD)
    Italia

    Phone: +39 049 8877061
    Email: info@teknositalia.it
    Web: www.teknositalia.it

  • 16 / 16

    Portugal

    Álamo-Ferramentas Unipessoal Lda
    Rua da ETAR, Lote 9
    Zona Industrial de Oiã
    3770-059 Oiã
    ​​​​​​​​​​​​​​
    Phone: +351 234 728-193
    Email: geral@alamo-ferramentas.com