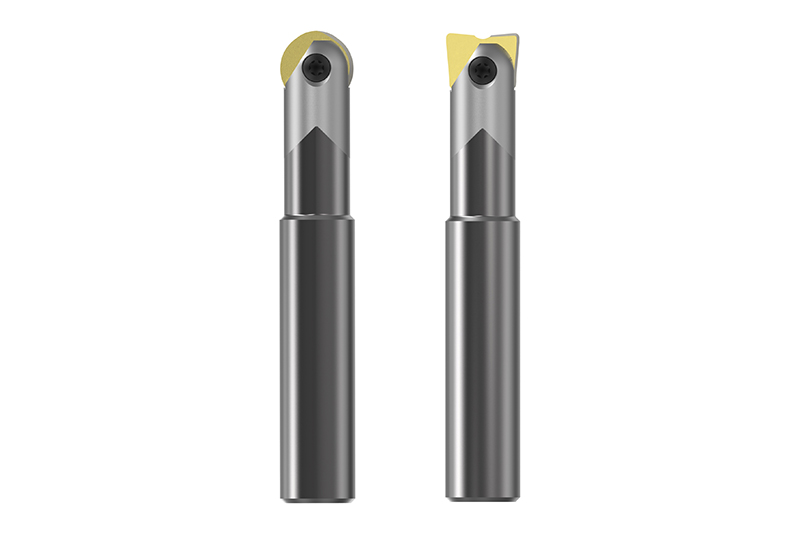
Usinagem de superfícies planas
Operações para criar superfícies planas ocorrem com muita frequência e em diferentes áreas na fabricação de moldes e matrizes: Seja relacionado ao componente, seja relacionado à estratégia devido à respectiva operação de fresagem ou devido às exigências de superfícies de fechamento do molde, bem como de cortes e matrizes de corte. A seleção da ferramenta apropriada é realizada, então, de acordo com a aplicação e a exigência.
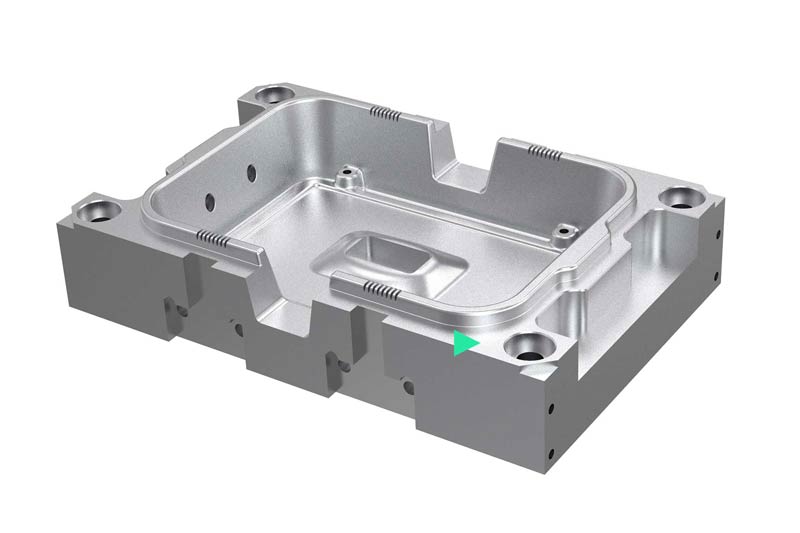
Visão geral das ferramentas para as seguintes etapas de usinagem:
Schruppen
Die Schruppoperation ist für den Großteil des Zerspanungsvolumens verantwortlich. Spezielle Frässtrategien wie die Hochvorschubbearbeitung oder das trochoide Fräsen können die Bearbeitungszeit reduzieren und somit die Wirtschaftlichkeit steigern. Neben Werkzeugen mit Wendeschneidplatten und Vollhartmetallfräsern kommen Hochleistungsfräser mit spezieller Schruppgeometrie zum Einsatz.
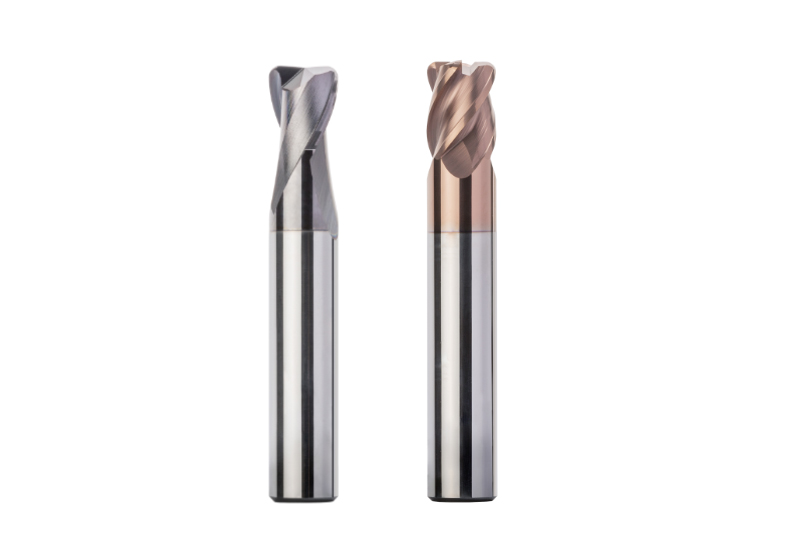
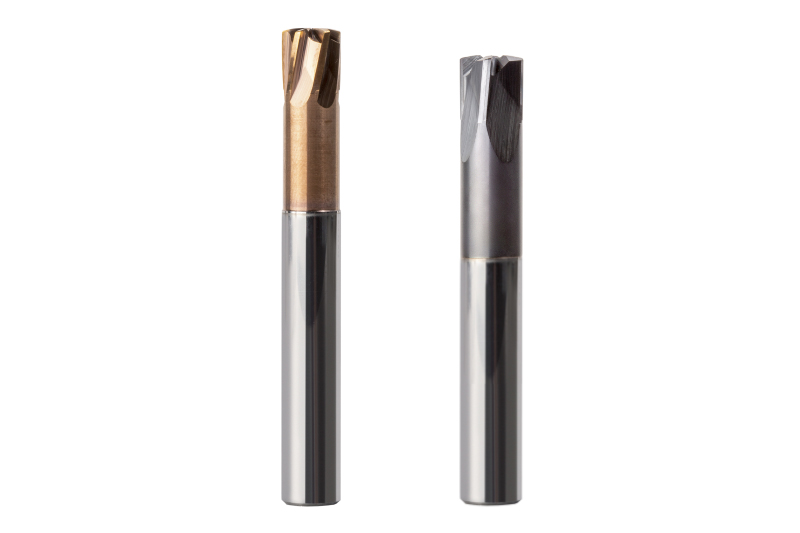
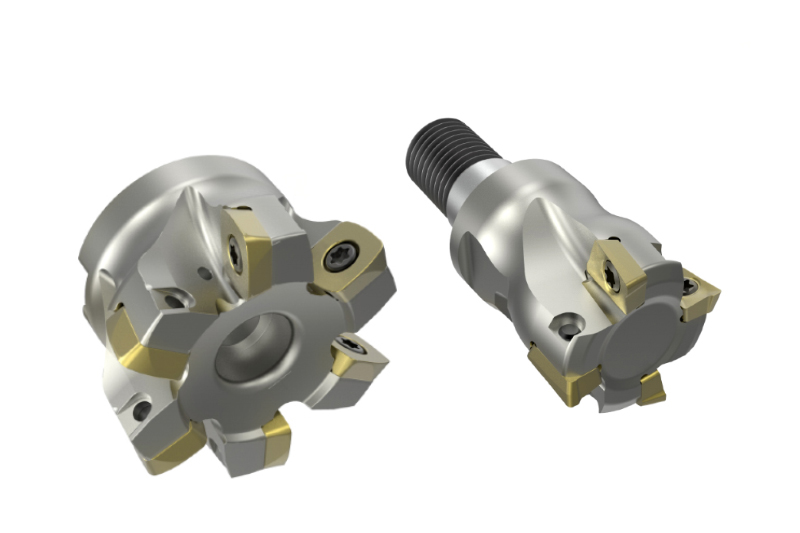
Residual material roughing
After roughing, in a second machining step, users machine the residual material, especially in corners and cavities, removing material as constantly as possible. Usually tools with corner radius or high-feed milling cutters are used. In some cases a ball cutter can be used to remove the residual material in corners.
Pre-finishing
If there are high demands on dimensional accuracy and surface finish, semi-finishing is recommended before finishing. With pre-finishing, machining approaches the final mould profile. The aim is to obtain a residual material that is as constant as possible in order to enable fast finishing with high demands on the surface quality. The stock removal after roughing is approx. 0.5-1 mm for hardened materials and 0.03-0.5 mm for soft materials. After pre-finishing, the constant stock removal is 0.05-0.1 mm for hardened materials or 0.1-0.3 mm for soft materials.
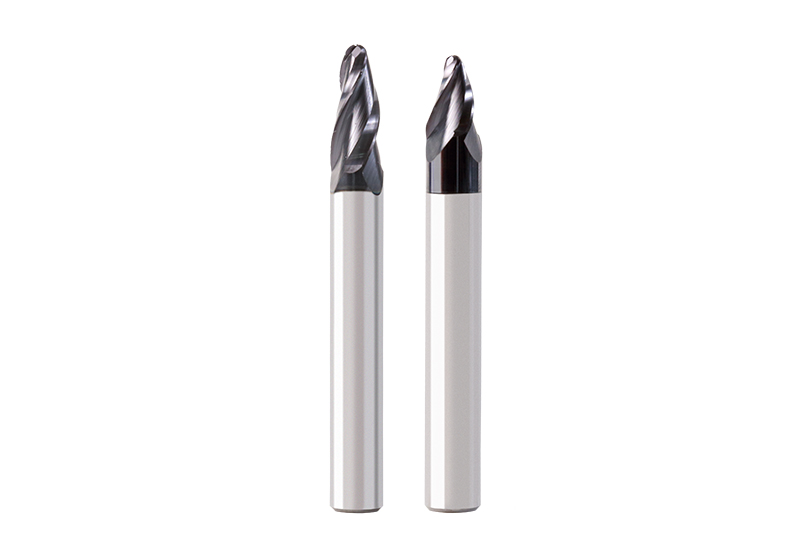
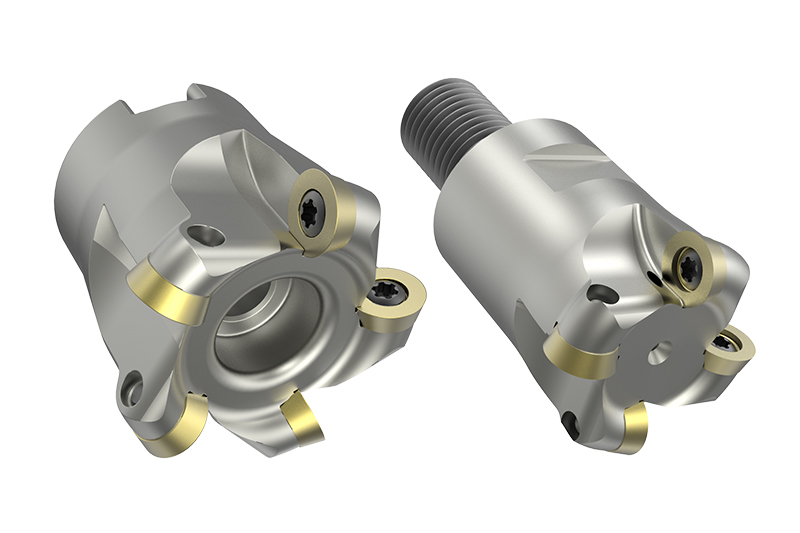
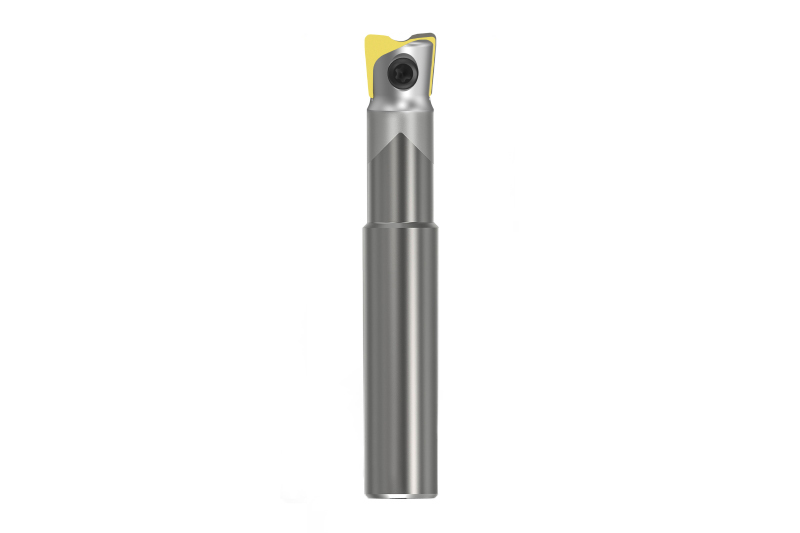
精加工
精加工去除剩余的加工余量以达到最终形状。在半精加工后,淬硬材料的加工余量为 0.05-0.1 mm,软质材料的加工余量为 0.1-0.3 mm。球形和/或圆角铣刀是首选刀具,具体取决于工件的最终轮廓。