
05.05.2025
Turnkey mit 78 passenden Tools
Zusammenarbeit der CHIRON Group und von MAPAL in den USA
Customer proximity is key
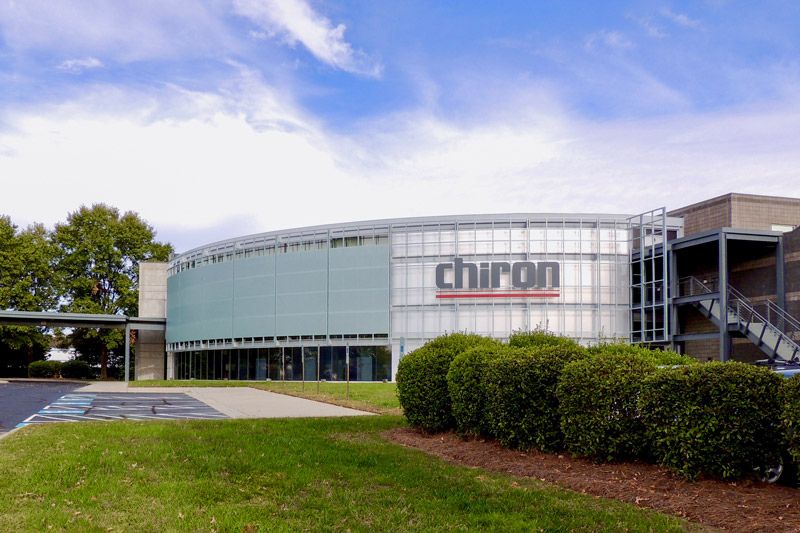
CHIRON Group has been active in the United States since 1993, with a modern factory opening in Charlotte in 2001. The 7,000-square-meter plant employs 100 employees focused on adapting German-built machines to meet the needs of the American industry. From fine-tuning hydraulic systems to developing advanced automation and turnkey solutions, the focus is on delivering precision and efficiency. These machines are designed for efficient production of specific components and are delivered to customers fully equipped with software, clamping fixtures, and tools—ready for immediate operation.
Like CHIRON Group, MAPAL also operates in the United States with two sites located in Port Huron, Michigan, and Fountain Inn, South Carolina. The precision tool makers and technology partners from Aalen/Germany recognised at an early stage that customer proximity was essential in the American market. This insight led to the establishment of MAPAL’s first international subsidiary in 1977. It began in New Jersey with the reconditioning of MAPAL tools. As MAPAL expanded into the automotive industry in the following years, business grew significantly. It soon became clear that the small factory was no longer sufficient. The next logical step involved setting up a manufacturing site closer to key automotive customers. MAPAL opened its production site in Port Huron in 1995 with a focus on manufacturing and reconditioning of high-precision tooling, such as reamers with guide pads. Through its proximity to Detroit, the company was able to provide faster response times and comprehensive technical support to customers.
By consolidating technical knowledge within its international Centres of Competence, MAPAL expanded its know-how and expertise in the manufacturing sector. In 2019, the precision tool maker expanded further by opening a second factory in the southern region. The Fountain Inn site enhanced sales, service, and manufacturing capabilities, complemented by a state-of-the-art aerospace test centre. Today, MAPAL Inc. manufactures solid carbide and PCD tools at both sites using technology and processes that adhere to the MAPAL Group’s global standards. The tools include drills with one or more diameters, form cutters, reamers, and tools for composite machining – all of which are also reconditioned in-house.
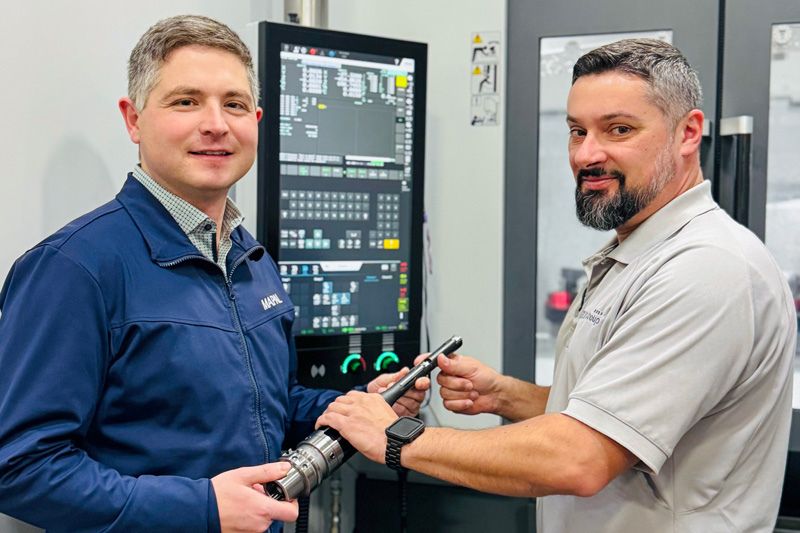
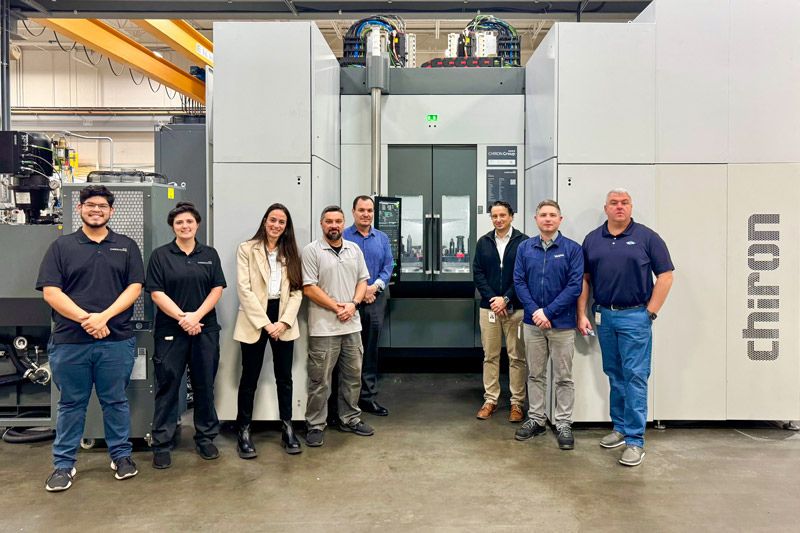
CHIRON Group and MAPAL have been cooperating in North America for nearly as long as the machine tool builder has been present in the region. As a trusted OEM supplier, MAPAL has supported CHIRON Group’s work across the automotive, aerospace, and medical technology industries, as well as their suppliers. “To offer our customers the best solutions, we need reliable partners – a quality MAPAL has consistently demonstrated,” says Jesus Flores, Lead Project Engineer at CHIRON Group in Charlotte.
Anspruchsvolles Bauteil
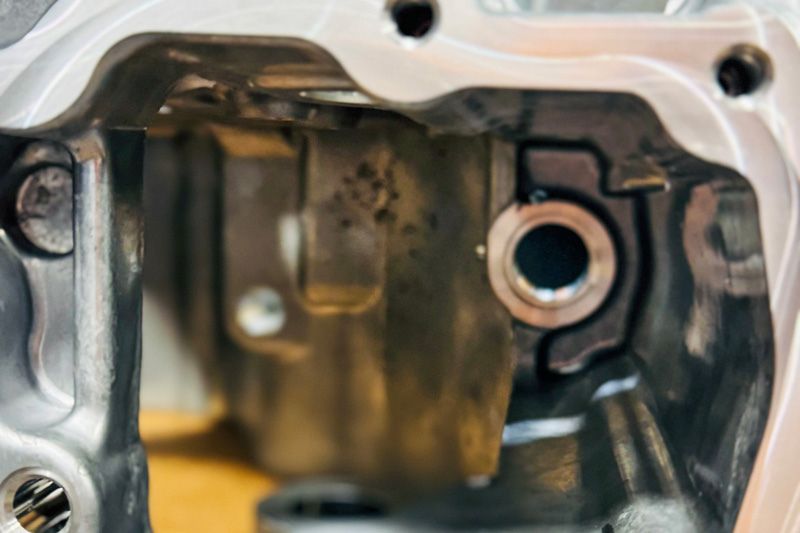
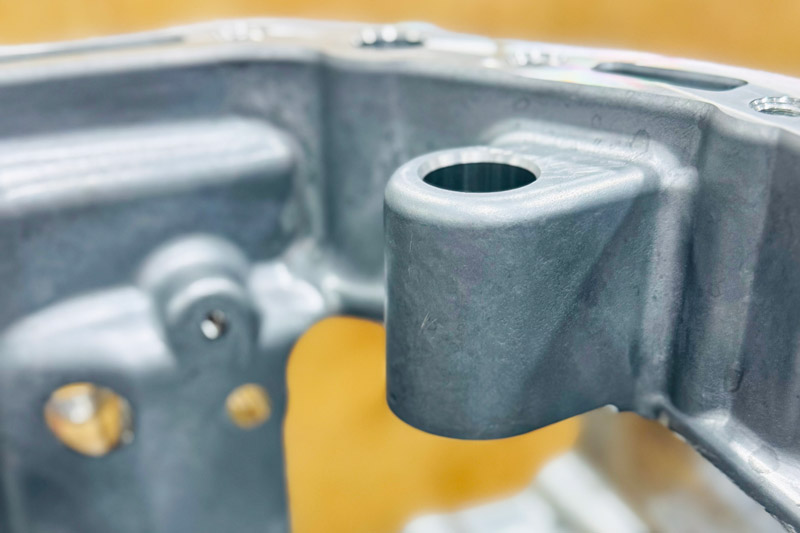
Auch beim jüngsten Projekt, einer Turnkey-Maschine für einen Truck-Hersteller, kommen sämtliche eingesetzten Werkzeuge sowie die Prozessauslegung von MAPAL. Bei dem zu produzierenden Bauteil handelt es sich um ein vorderes Getriebegehäuse für einen großen LKW-Dieselmotor. Um einen reibungslosen Start zu gewährleisten, unterstützte MAPAL den Kunden vor Ort in der Anlaufphase und beschleunigte die Bereitstellung optimierter Werkzeuge, sodass das Projekt vom ersten Tag an nach Plan lief.
Das hochkomplexe Bauteil mit zahlreichen Bohrungen und komplizierten Formen wird aus Druckgussaluminium A380 gefertigt. Der Endkunde plant, davon 120.000 Stück pro Jahr zu fertigen. Bei einer voraussichtlichen Produktionslaufzeit von sechs bis acht Jahren könnte die Gesamtstückzahl an eine Million Teile herankommen, bevor eventuell eine Designmodifikation ansteht.
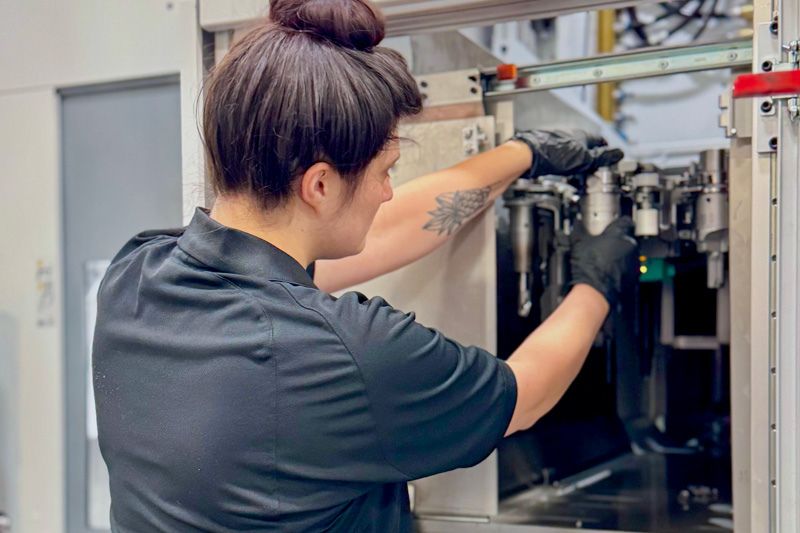
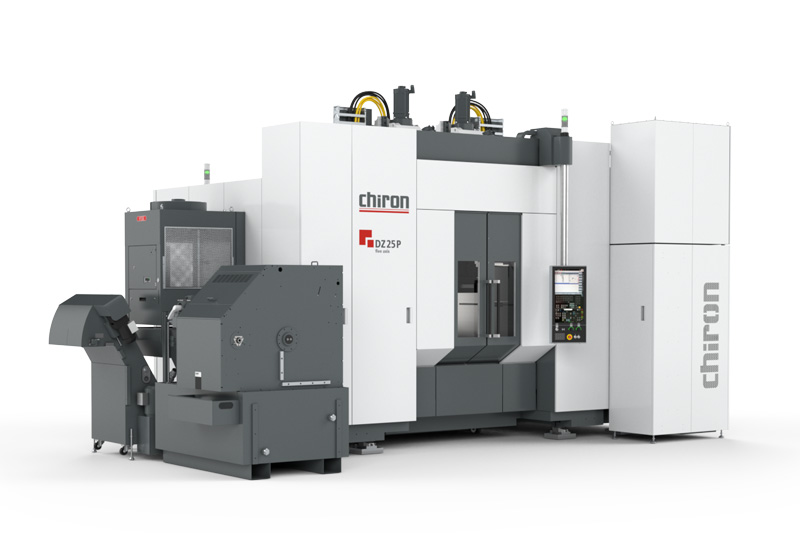
Die hohen Stückzahlen, in denen das Getriebegehäuse produziert werden soll, verlangen nach einer sehr effizienten Fertigung. Für diese Aufgabe wurde das doppelspindlige Bearbeitungszentrum DZ 25 P five axis gewählt, das die CHIRON Group speziell für die hochproduktive Bearbeitung großvolumiger Bauteile entwickelt hat.
Aufgrund der enormen Steifigkeit der Maschine sind hohe Dynamik und Präzision bei sehr hohen Achsbeschleunigungen und schnellen Eilgängen gewährleistet. Im geräumigen Arbeitsraum können zwei der 600 x 600 x 450 mm großen Bauteile gleichzeitig bearbeitet werden. In einem ersten Arbeitsschritt wird das Werkstück im angelieferten Zustand aufgespannt, um zunächst die Vorbearbeitung durchzuführen und so Spannungen aus dem Bauteil zu lösen. Dabei werden auch gleich Bearbeitungen mit mittlerer Toleranzgröße erledigt. Die exakte Bearbeitung von Passungsbohrungen und Flächen zum Referenzpunkt erfolgt in einer weiteren Aufspannung.
Two-thirds custom tools
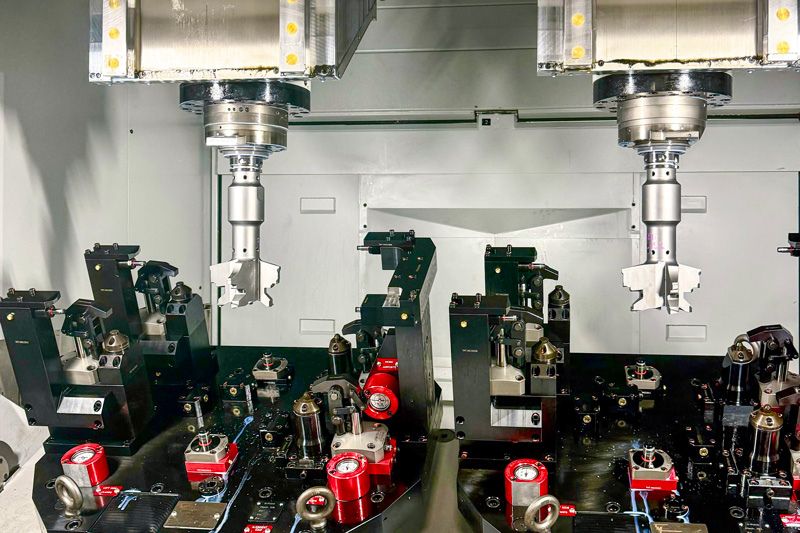
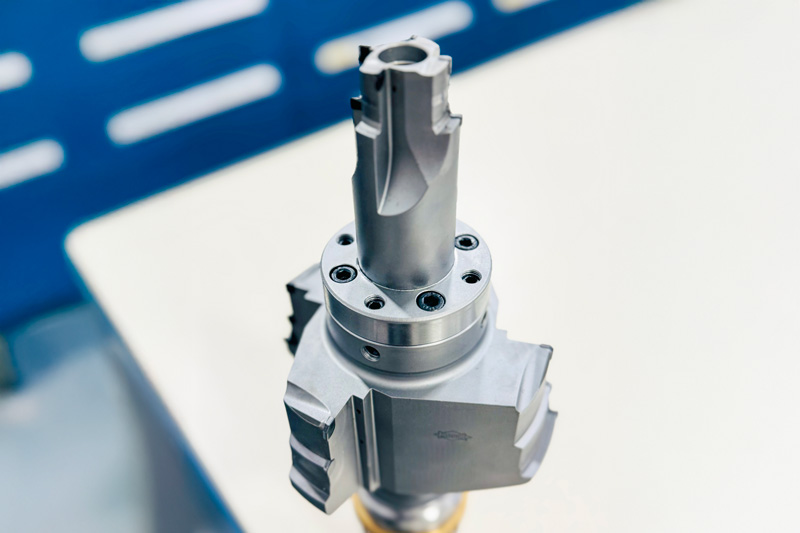
The tools supplied by MAPAL play a key role. 78 tools have been provided, with two-thirds being custom-made and precisely designed to the corresponding machining step with special geometries and dimensions. In many cases, the complexity of the tools is a direct result of the component design or the selected machining strategy. Among them, 33 of the tools are PCD tools, while the remaining 45 use carbide cutting edges.
Whenever possible, multiple machining steps have been combined into a single tool, allowing the machining of various diameters in one operation. “Cycle times are reduced with these custom tools”, explains Jesus Flores. “In this way, we save multiple tool changes every time, which improves both the machining times and precision.” Besides speed, the components require a high level of precision and quality that surpass typical automotive industry standards.
Proactive support
Kontakt
Kathrin Rehor Public Relations Kathrin.Rehor@mapal.com Tel.: +49 7361 585 3342


