12.07.2023
Milling instead of drilling
An alternative for long-chipping aluminium materials
Replacing a drill by a milling cutter to drill bores into a workpiece is a suggestion that takes some getting used to and initially causes many manufacturers to frown. However, the technology change makes sense for some parts, especially in the field of e-mobility. MAPAL shows that this not only allows greater process reliability, but even shorter machining times.
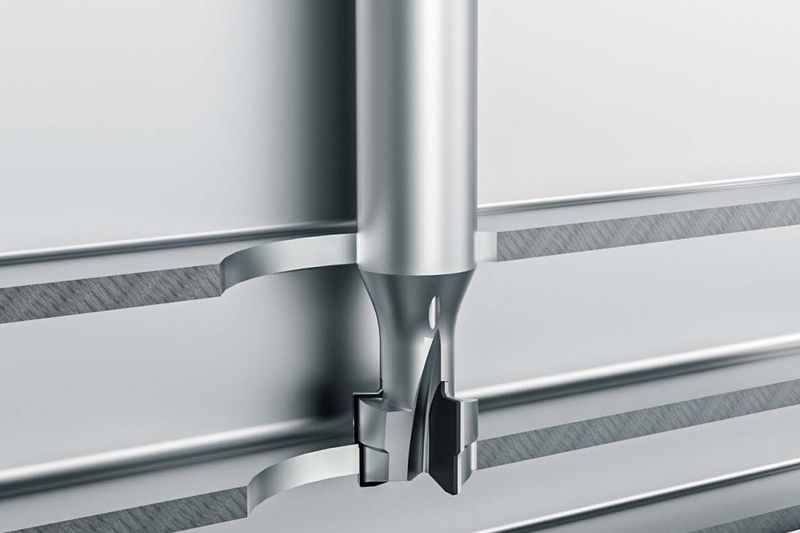
The fastest way to drill a bore is using a suitable drill. A milling cutter with a smaller diameter that enters the material circularly covers a significantly longer distance during machining, which results in a higher cycle time. However, certain materials can cause non-productive times that cancel out the drill’s time advantage.
During the course of the transformation to e-mobility, welded designs or structural parts are to be machined that consist of long-chipping aluminium. Battery housings, for example, are often made from extruded profiles that contain either no silicon at all or only a very small amount. That makes chip breaking more difficult and leads to nests of chips that can get stuck in the machine or on the tool. The same problem comes up when machining chassis parts made of forged aluminium, where manufacturers also struggle with long chips. If they settle on the shank of the tool, an automatic tool change may no longer be possible. Chip clusters cause disruptions that have an adverse effect on the machining time.
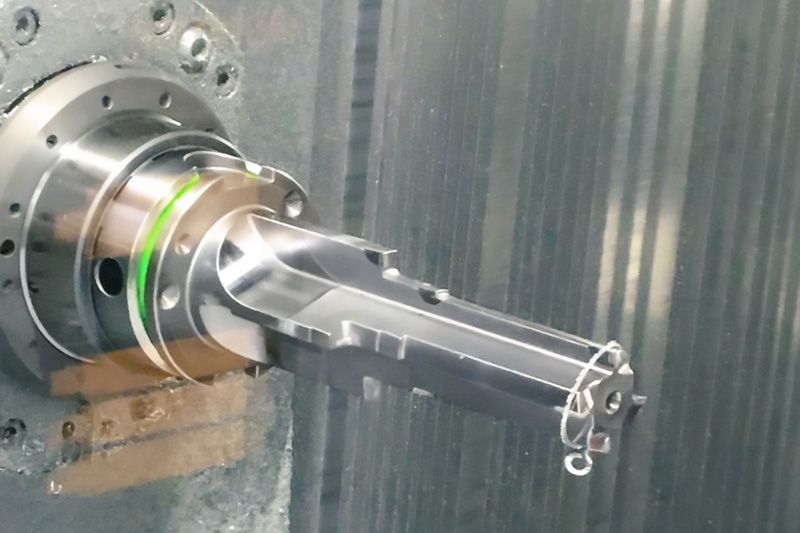
Speziell beim Vollbohren oder bei bestimmten Aufbohroperationen kann sich auch ein Grat bilden, der herausgedrückt wird und sich als Ring um das Werkzeug wickelt. „Diese Ringe sammeln sich an der Werkzeugschneide und können Werkstück und Werkzeug beschädigen“, bestätigt Leander Bolz, Vertriebsleiter PKD-Werkzeuge.
Grundsätzlich können Bohrer zwar mit Spanbrechern versehen werden, doch beeinträchtigen diese meist die Standzeit des Werkzeugs. Zudem ist bei den verwendeten Materialien nicht immer sichergestellt, dass der Spanbrecher seine Aufgabe zuverlässig erfüllt. Aluminium mit geringem Siliziumgehalt kann je nach Lagerzustand, Guss oder Charge andere Eigenschaften zeigen, was sich auch in unterschiedlicher Spanbildung zeigt. So wird in der Praxis oft die Aufmaßsituation der Vorbearbeitung geändert. Während bei einem Bohrwerkzeug mitunter Platten oder ganze Werkzeuge ausgetauscht werden müssen, lässt sich das Aufmaß mit einem Fräser über die gefahrenen Bahnen leicht reduzieren oder erhöhen.
Milling brings flexibility
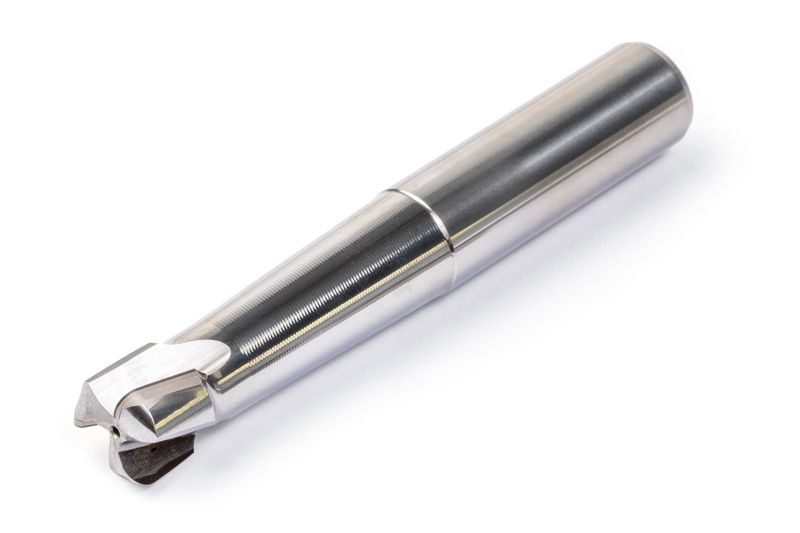
The milling strategy also demonstrates its flexibility when bores with different diameters are required. A single milling cutter can be used for this. For larger bores, it eliminates the need to replace one or even two drills for pre-machining. MAPAL favours using the milling cutter for the materials in question since it is possible to save time, particularly during pre-machining, which outweigh the initial performance disadvantages compared to drilling. For certain workpieces, the milling cutter is superior from the outset, for example when there is a risk of deformation due to drilling thin walls of structural parts or when bores with a very specific roughness are required in chassis technology.
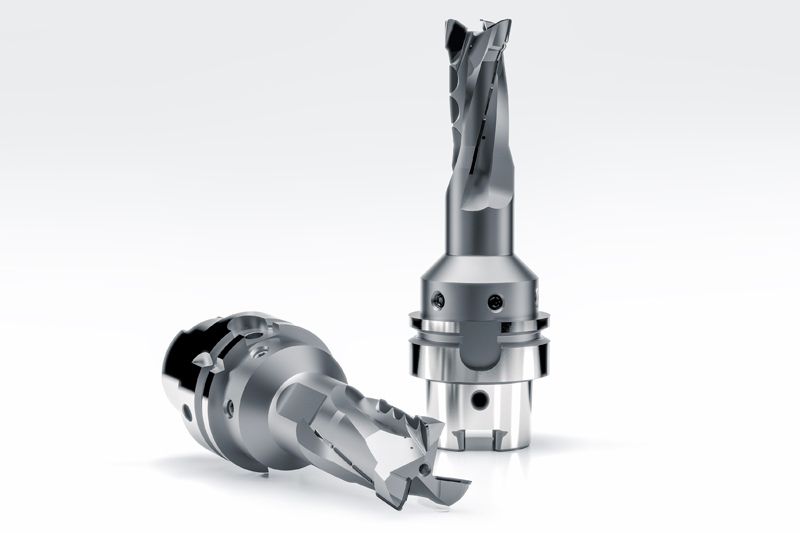
Combination tools further reduce the cycle time, as Leander Bolz explains: “If the milling operation sits at the front of the tool and the fine machining behind it, the bore can be created completely in one pass.” With various geometries to choose from, the tools are adapted to the respective machining operation. MAPAL offers SPM milling cutters (Structural Part Machining) with PCD cutting edges for machining aluminium. These very sturdily designed high-volume milling cutters were originally developed for the aerospace industry to machine material from solid.
Contact
Kathrin Rehor Public Relations Kathrin.Rehor@mapal.com Phone: +49 7361 585 3342