NeoMill® milling cutters combine productivity and cost-effectiveness
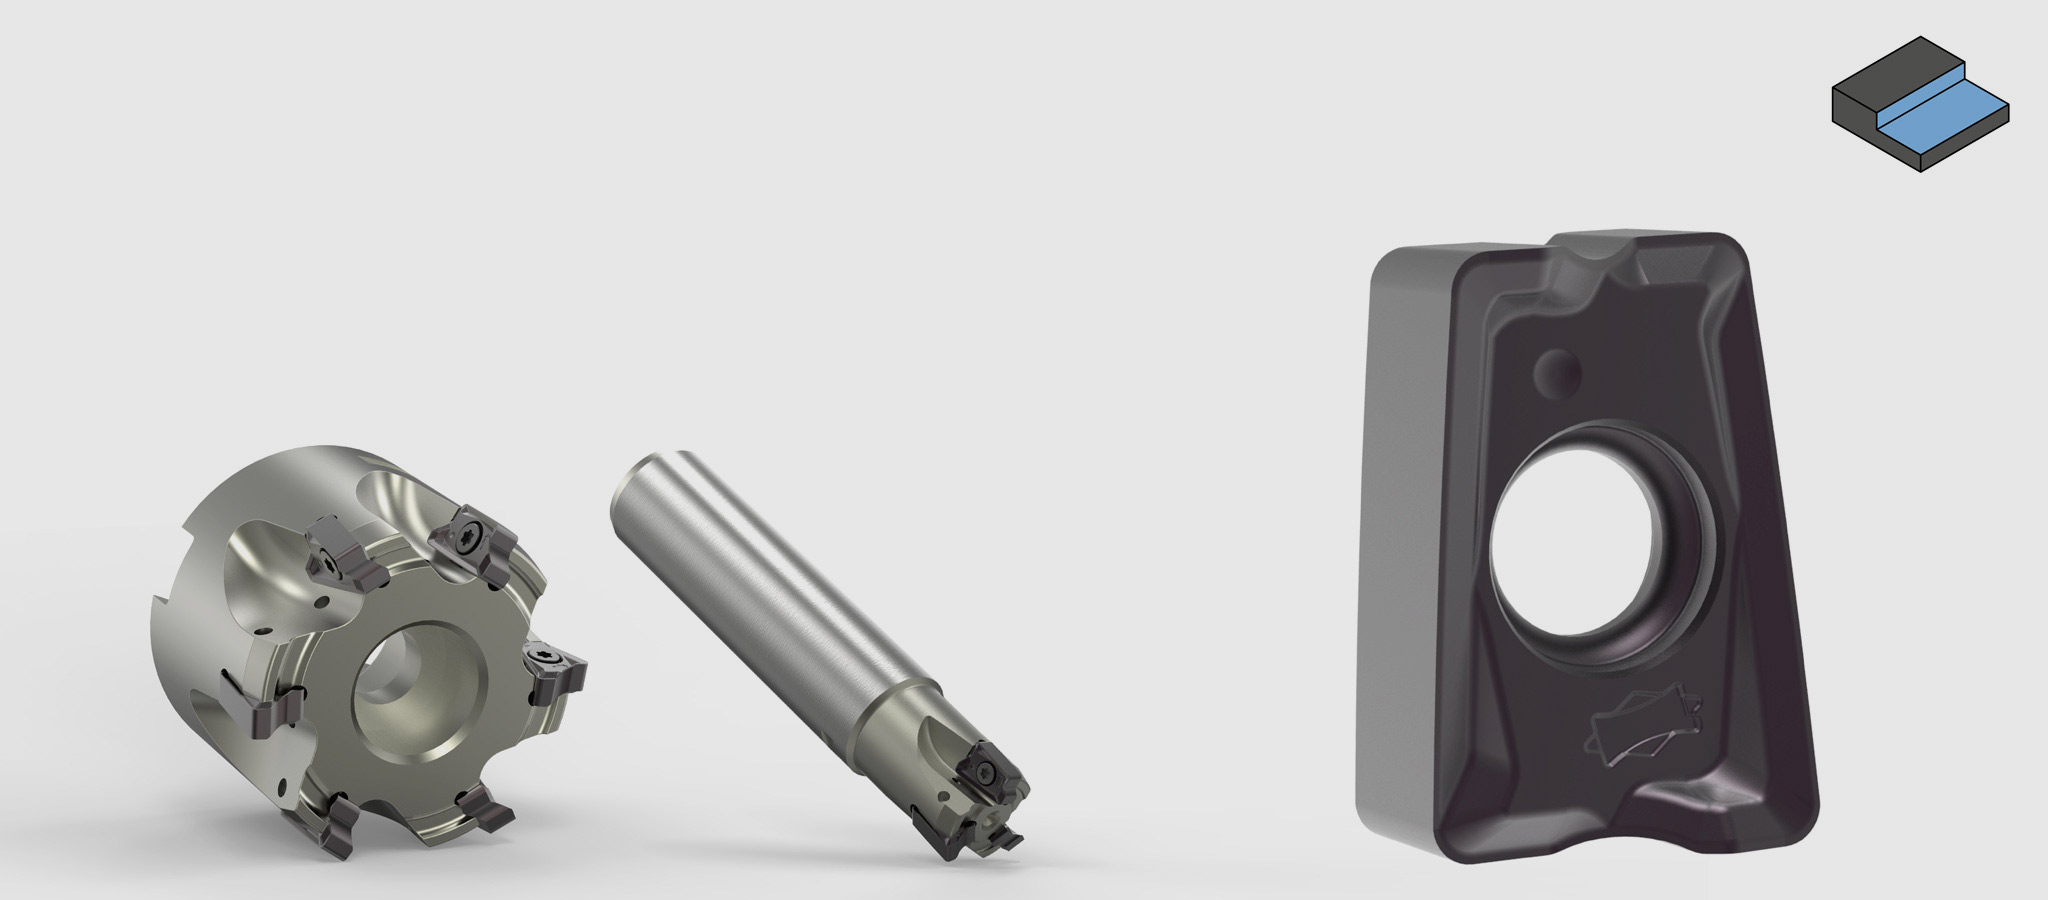
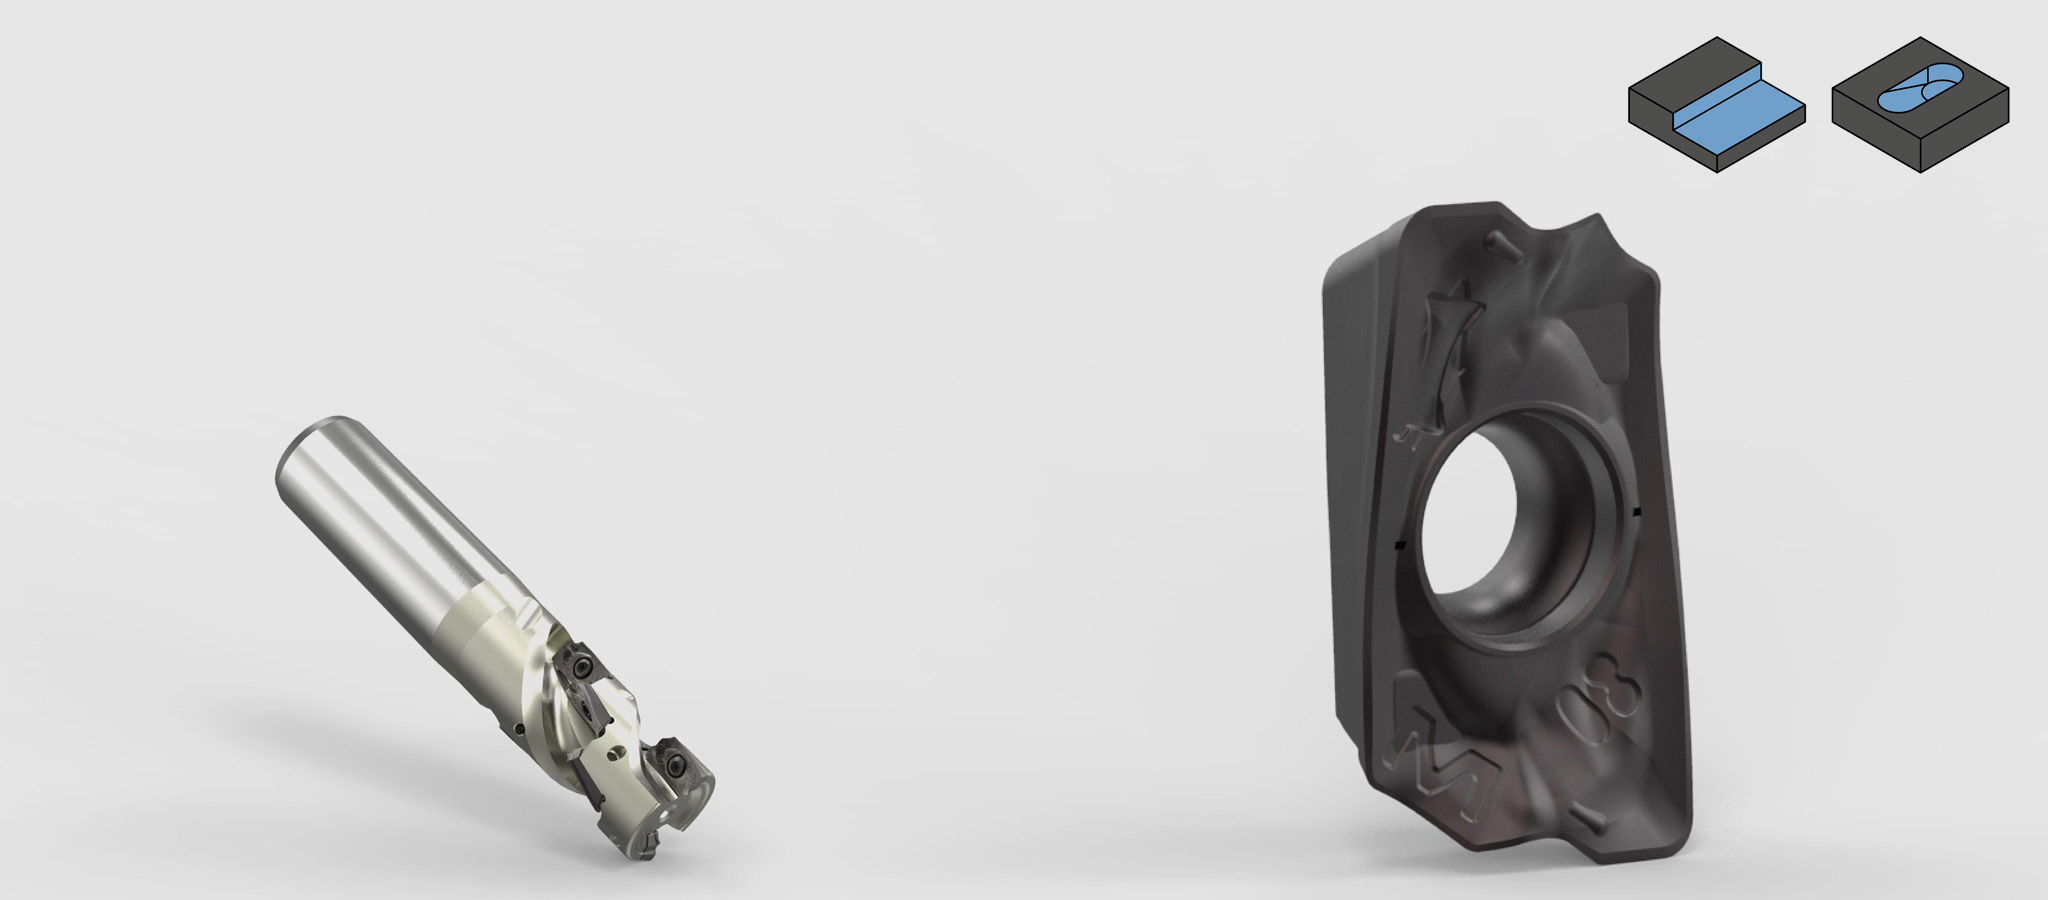
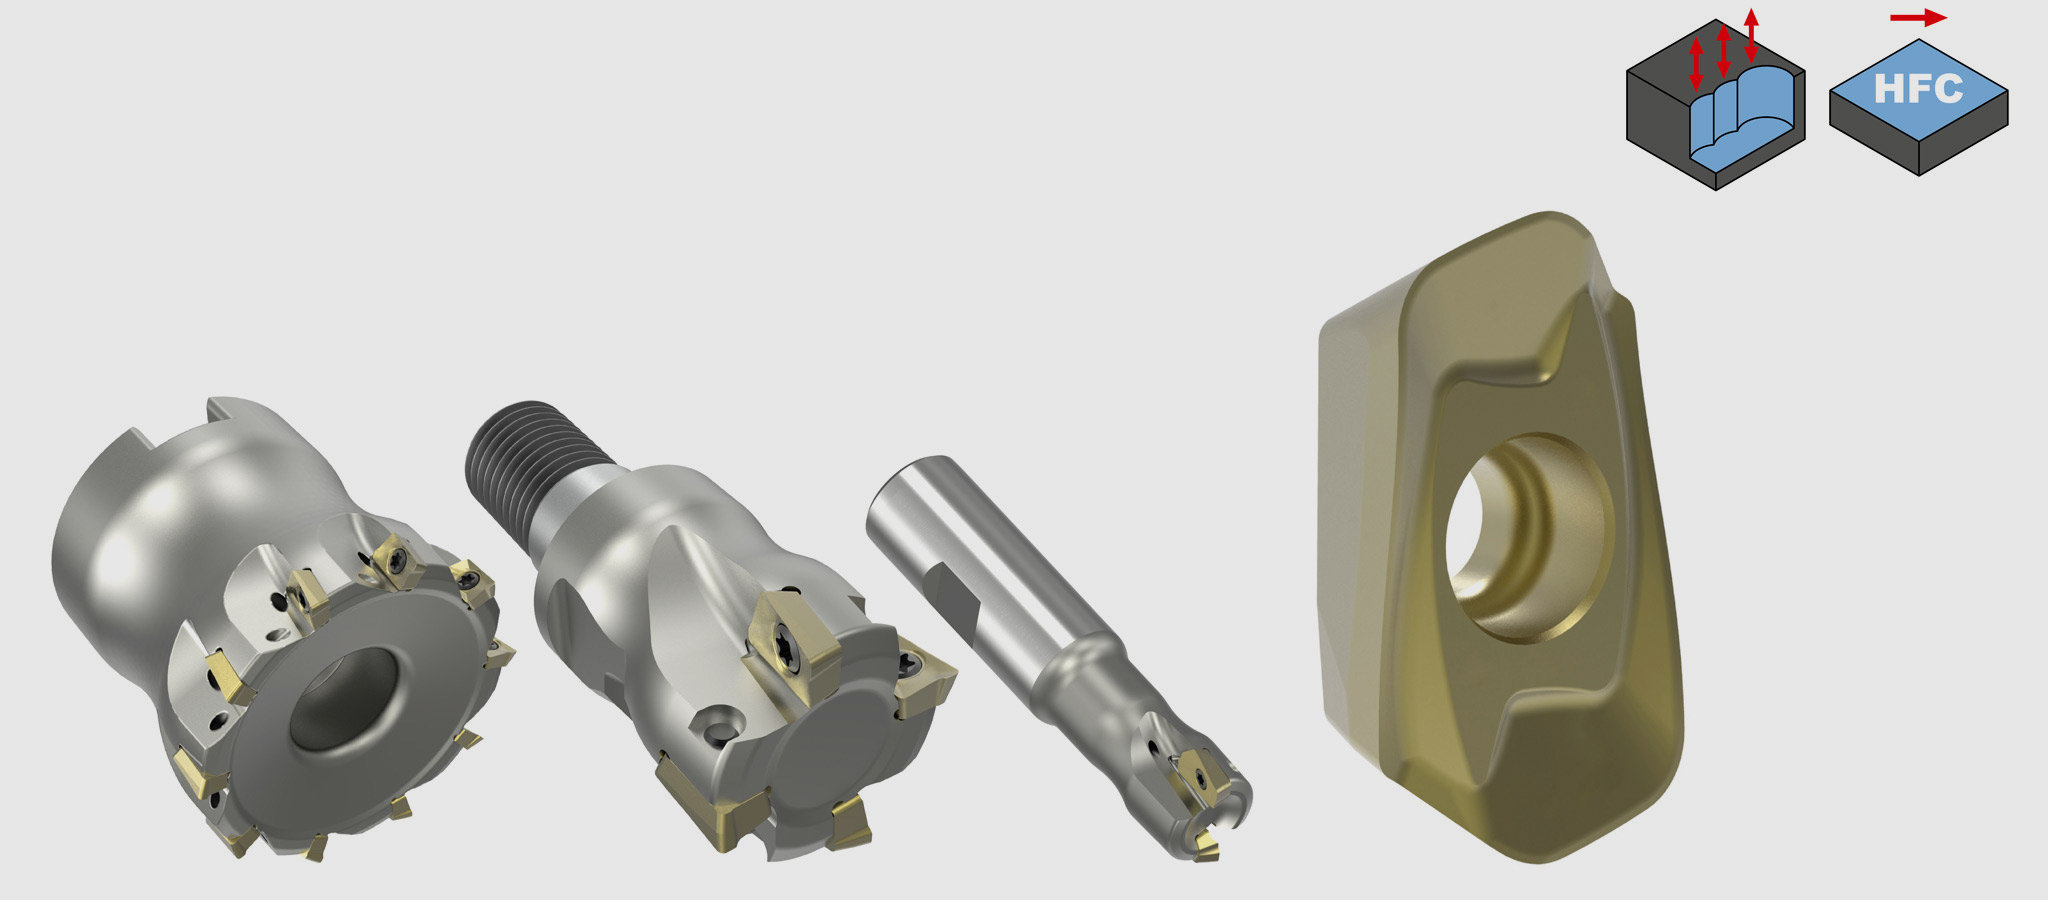
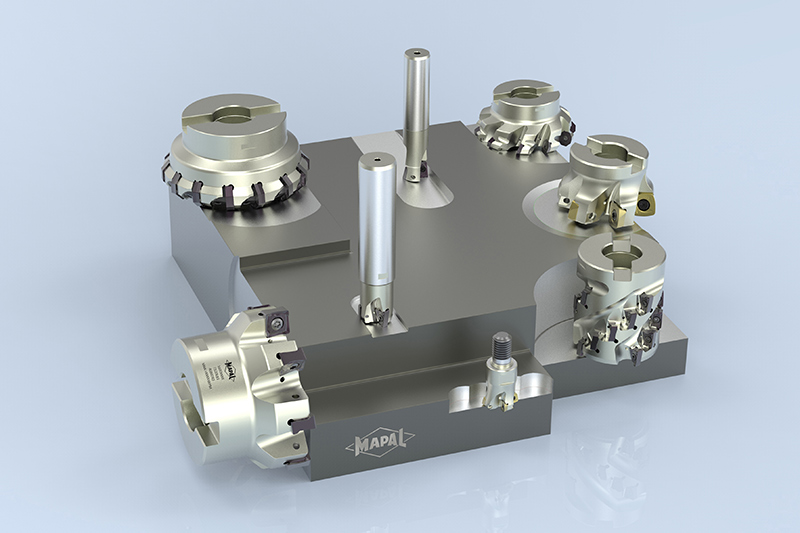
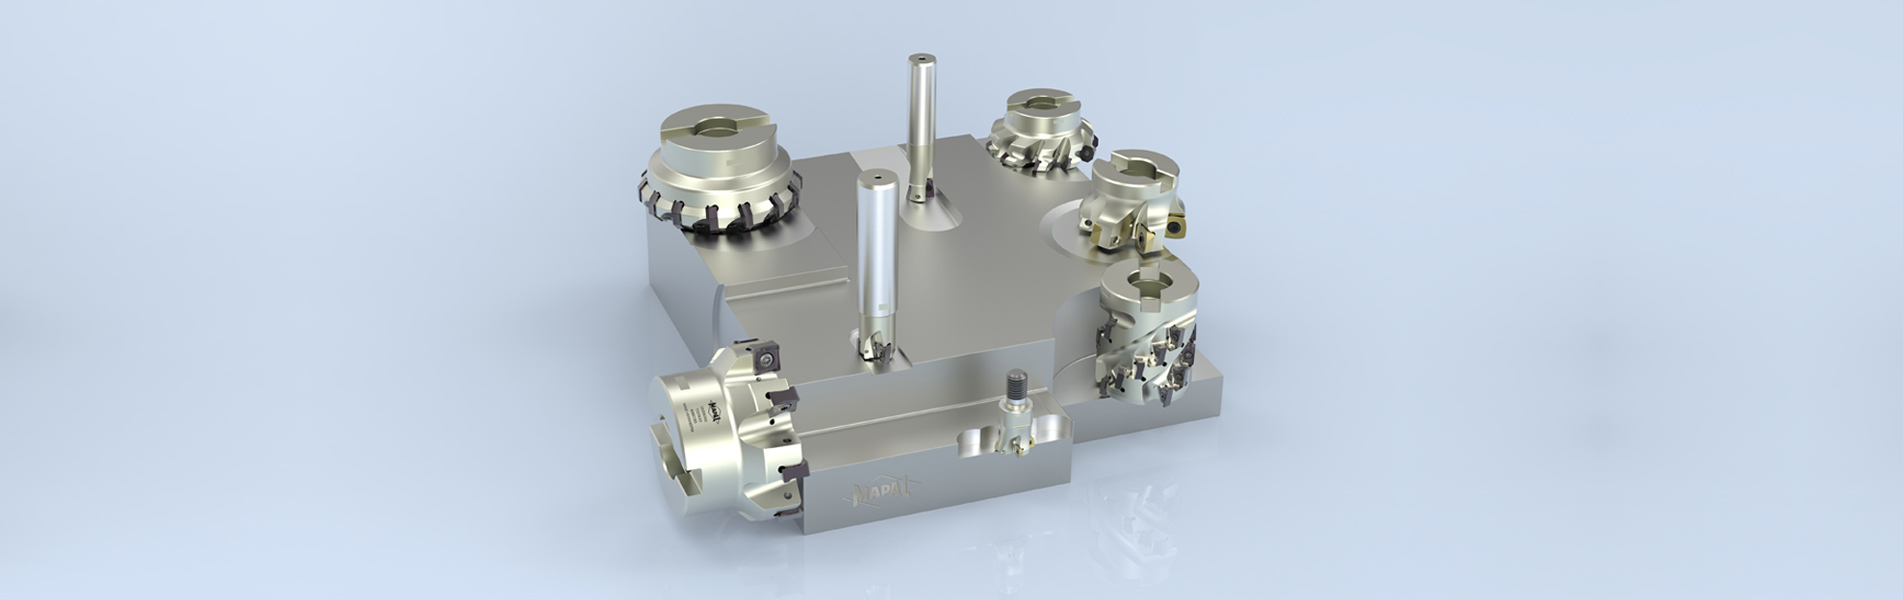
The radial NeoMill® standard milling cutter programme by MAPAL with its face, shoulder, slot, shell end face and high-feed milling cutters stands for maximum productivity and cost-effectiveness, especially in series production. The development was based on many years of experience with custom tools, which the industry uses to produce large quantities very efficiently with consistent quality.​
UNIQ Mill Chuck & UNIQ DReaM Chuck 4,5° recebem prémio de design 

Trabalhar no mundo de TI

Juntos, definiremos o rumo para o futuro. Apostamos numa abordagem humana, visão alargada e numa organização bem estruturada. Tudo isto constitui a base para uma perspetiva prospetiva e fiável, assim como para a qualidade dos nossos produtos e serviços. Como empregador e parceiro tecnológico, isto é algo de que sempre nos orgulhámos. Agora queremos crescer ainda mais – consigo na equipa.

Não é apenas um importante impulsor da digitalização – mas também escreve de raiz com cada linha de código. Isso faz de si um elemento perfeito para a nossa equipa: Porque colocámos a digitalização no centro das nossas competências e serviços. Trabalhamos internacionalmente, em equipas ágeis e com as mais recentes ferramentas e estruturas. Isto resulta em projetos desafiantes e oportunidades de desenvolvimento para si – para si connosco.
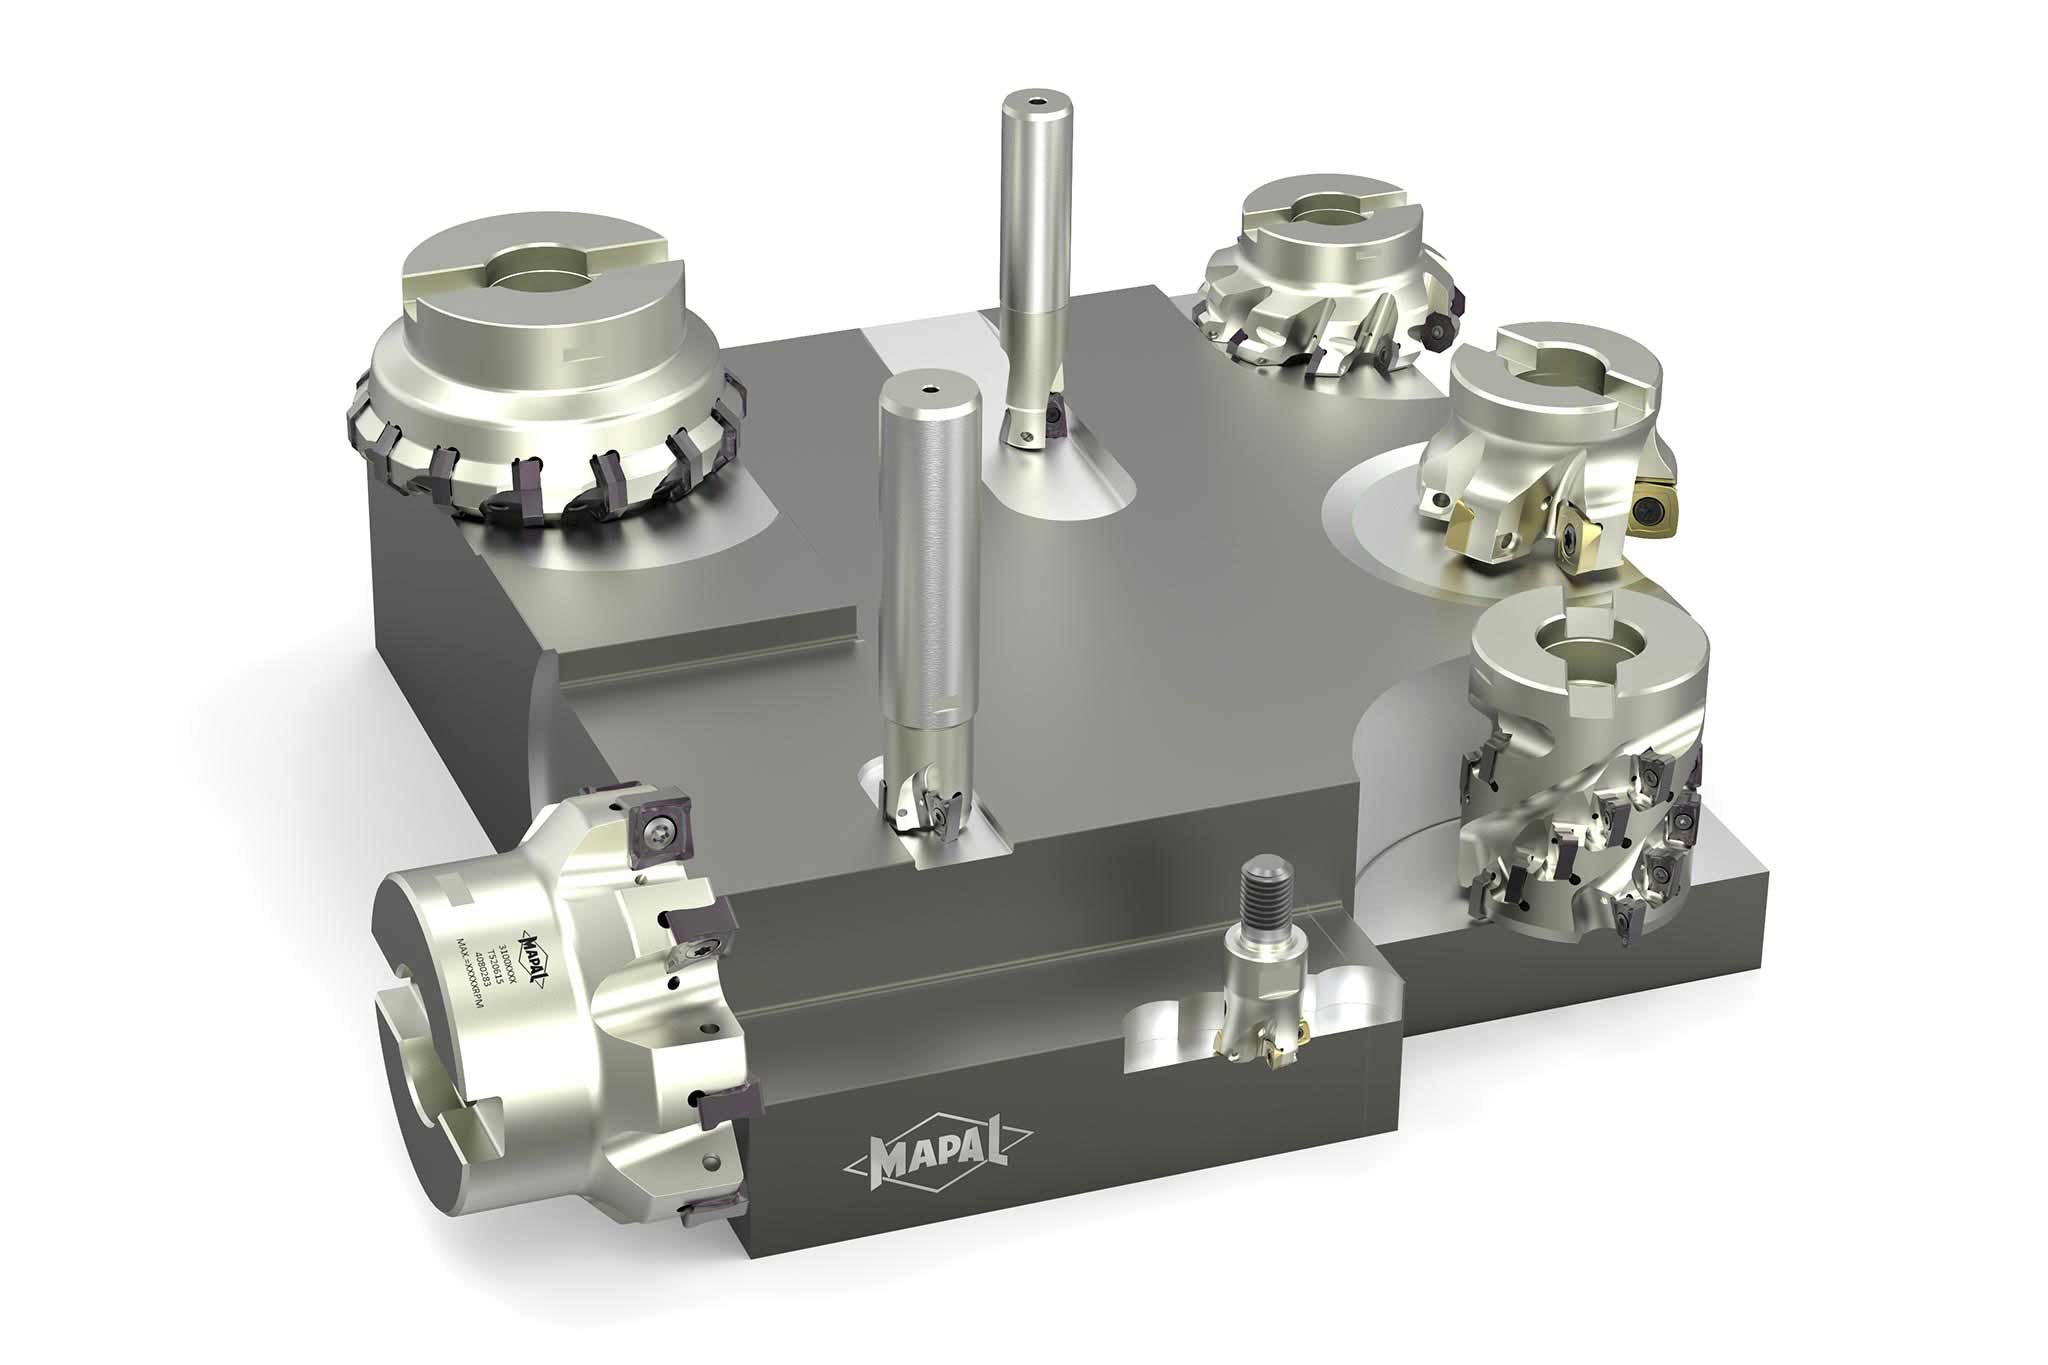

O programa de fresagem radial standard NeoMill da MAPAL.

AT A GLANCE

  • Milling cutter range with compacted radial indexable inserts

  • Face, shoulder, slot and shell end face milling cutters
  • For roughing and medium machining with one tool
  • Positive and negative indexable inserts made from different PVD and CVD cutting materials
     

ADVANTAGES

  • Indexable inserts for maximum efficiency also in difficult machining conditions
  • Very high surface quality due to indexable inserts with wiper component
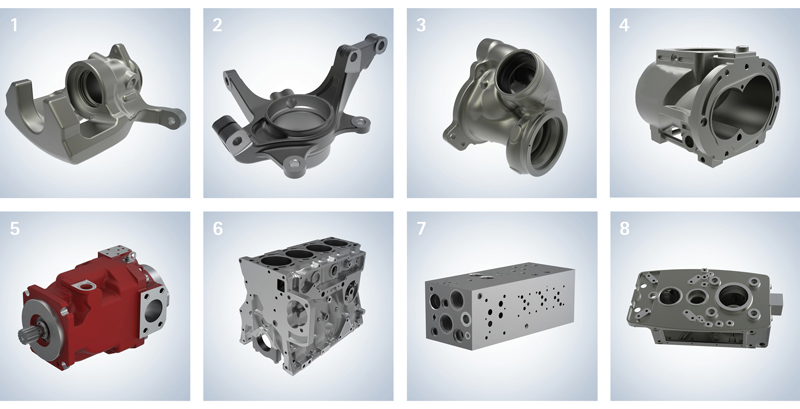
  • For all applications in cast iron, steel and stainless steel, as well as heat-resistant cast steel (turbocharger materials)
  • High cutting volume

NeoMill® standard programme

For all milling cutters, MAPAL offers a wide range of indexable inserts – each in a positive and a negative design. In addition, there are cutting edges with a wiper portion, which achieve good surface qualities even without being set. 

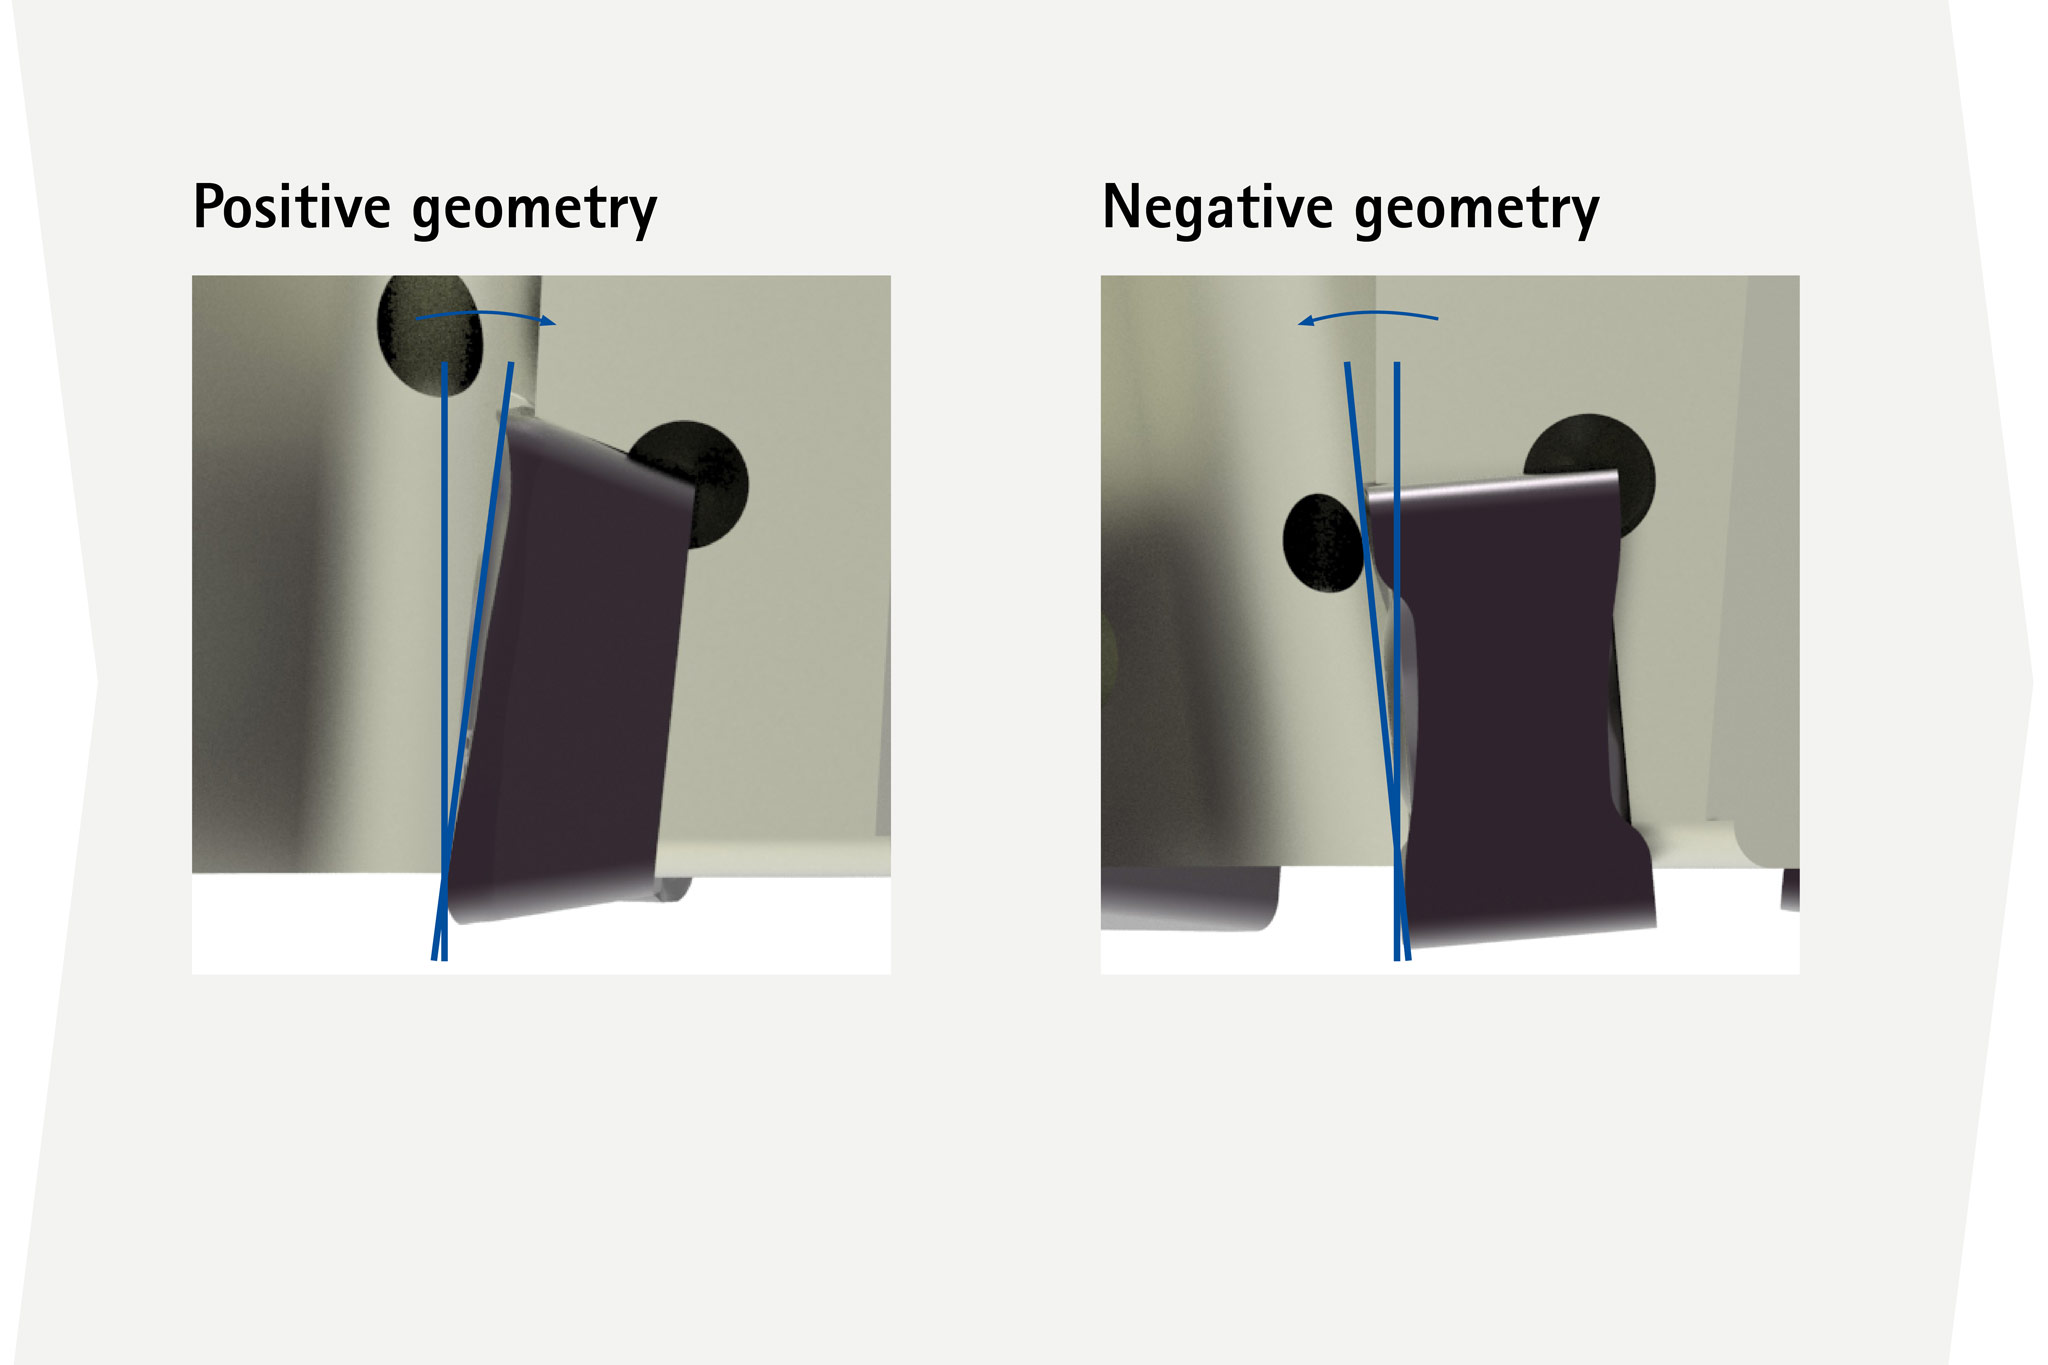
The negative inserts do not have a clearance angle and can therefore be designed with cutting edges on the contact surface. If the basic shape is the same, negative inserts thus have double the number of cutting edges compared with their positive counterparts. In combination with the high tool life of the indexable inserts, this makes the negative indexable inserts particularly cost-effective.


Applications


Selection steps for the NeoMill® milling cutter
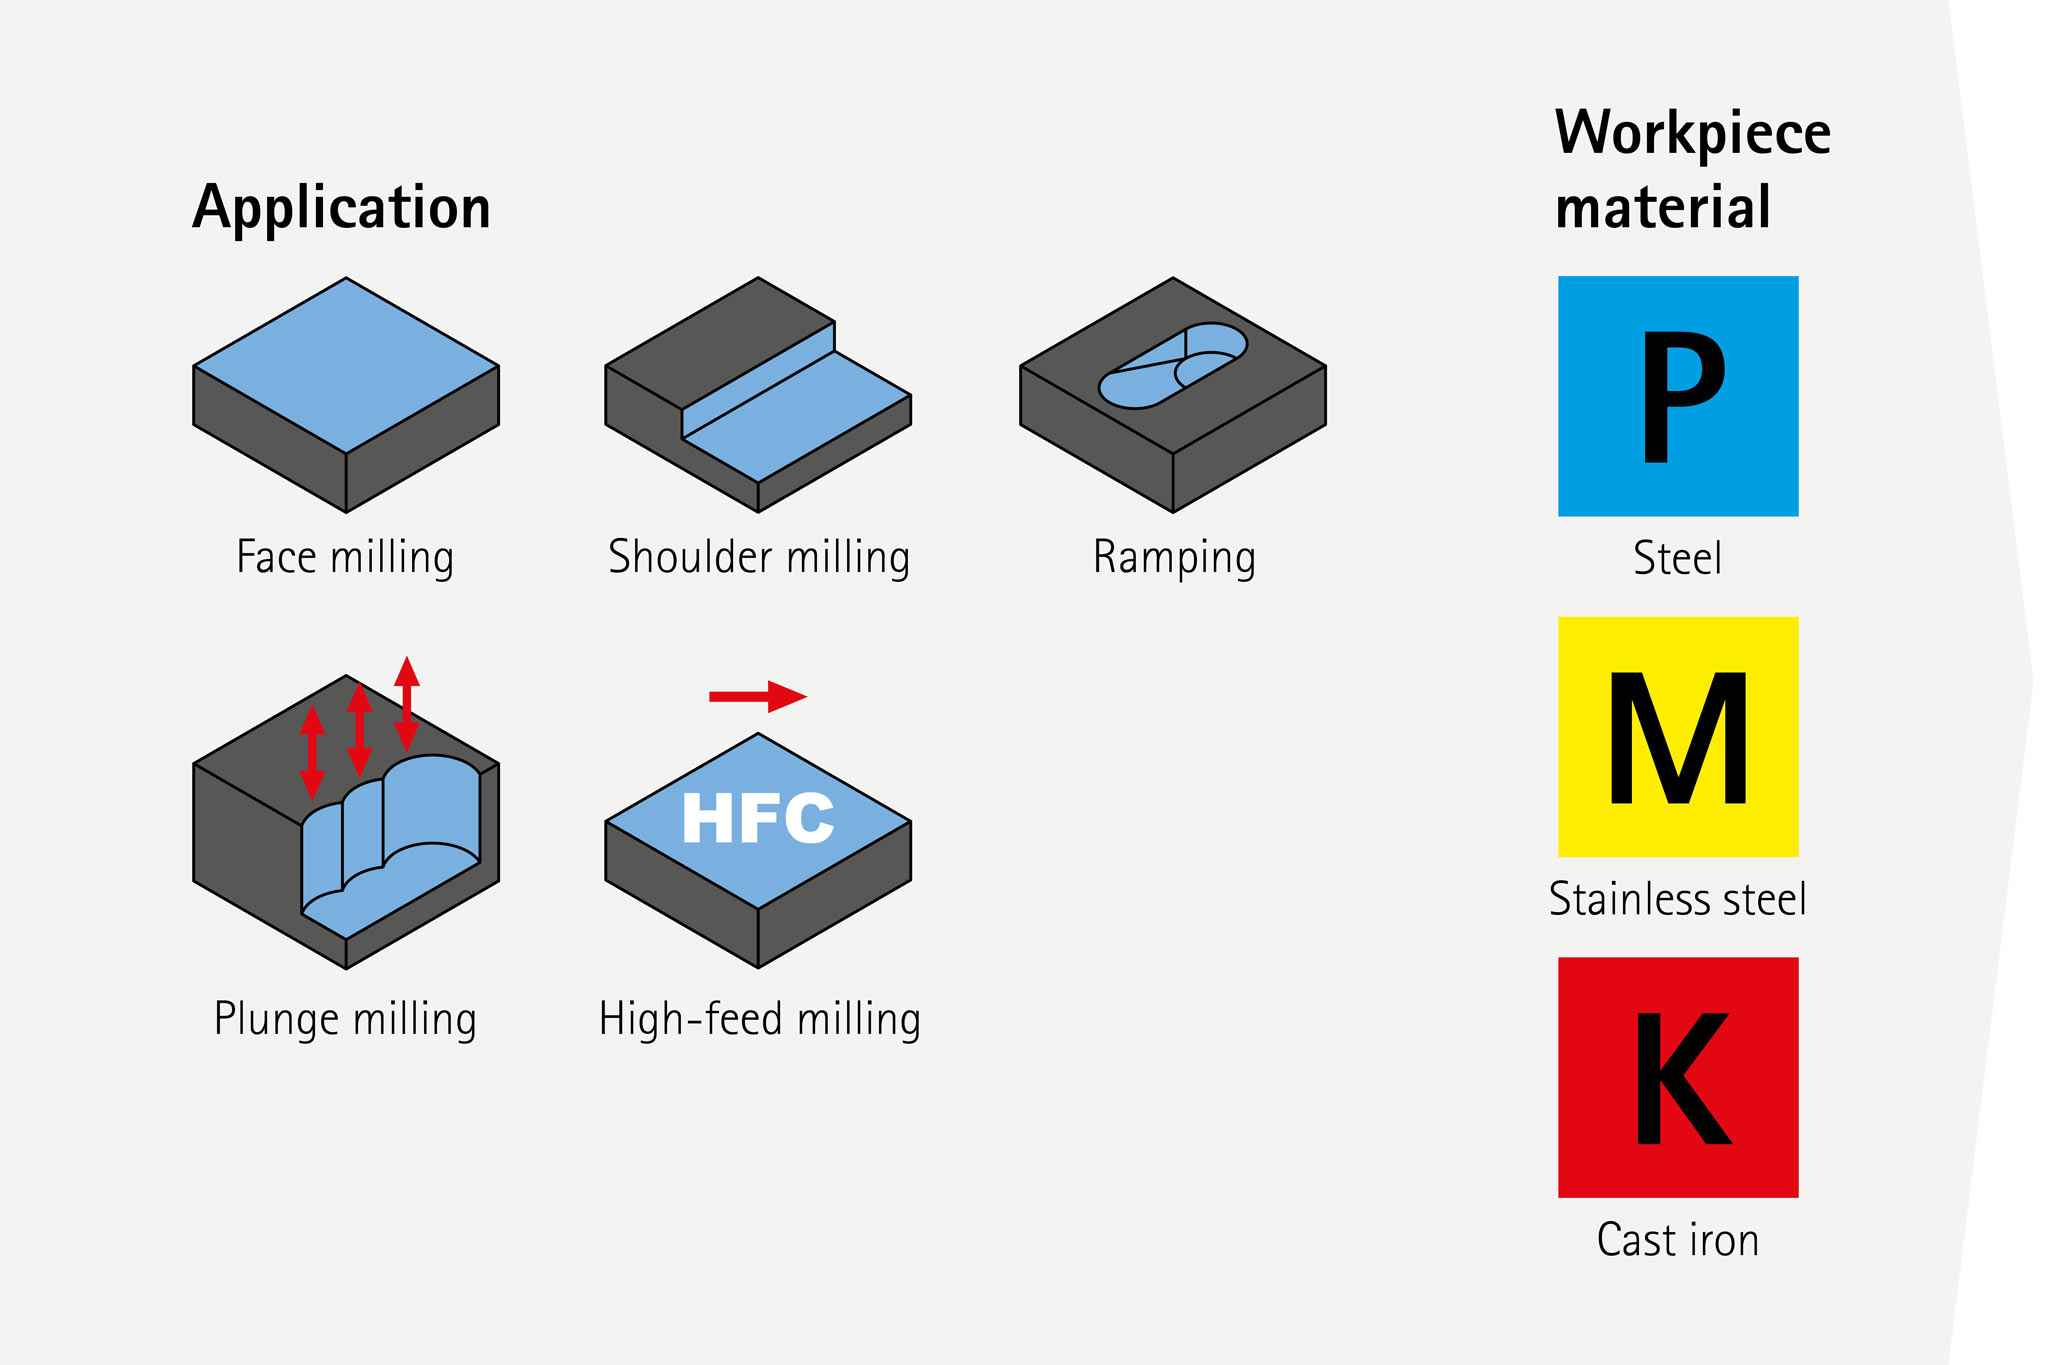
As a technology partner, MAPAL supports the selection and optimum use of the NeoMill® milling cutters with knowledge of tooling and processing.​​​​​​​.

  • 1. Component application and workpiece material

    Selection of application & workpiece material:

    Application
    Face milling, Shoulder milling, Ramping, Plunge milling, High-feed milling​​​​​​​
    Workpiece material:
    Steel, Stainless steel, Cast iron​​​​​​​


  • 2. Machining conditions

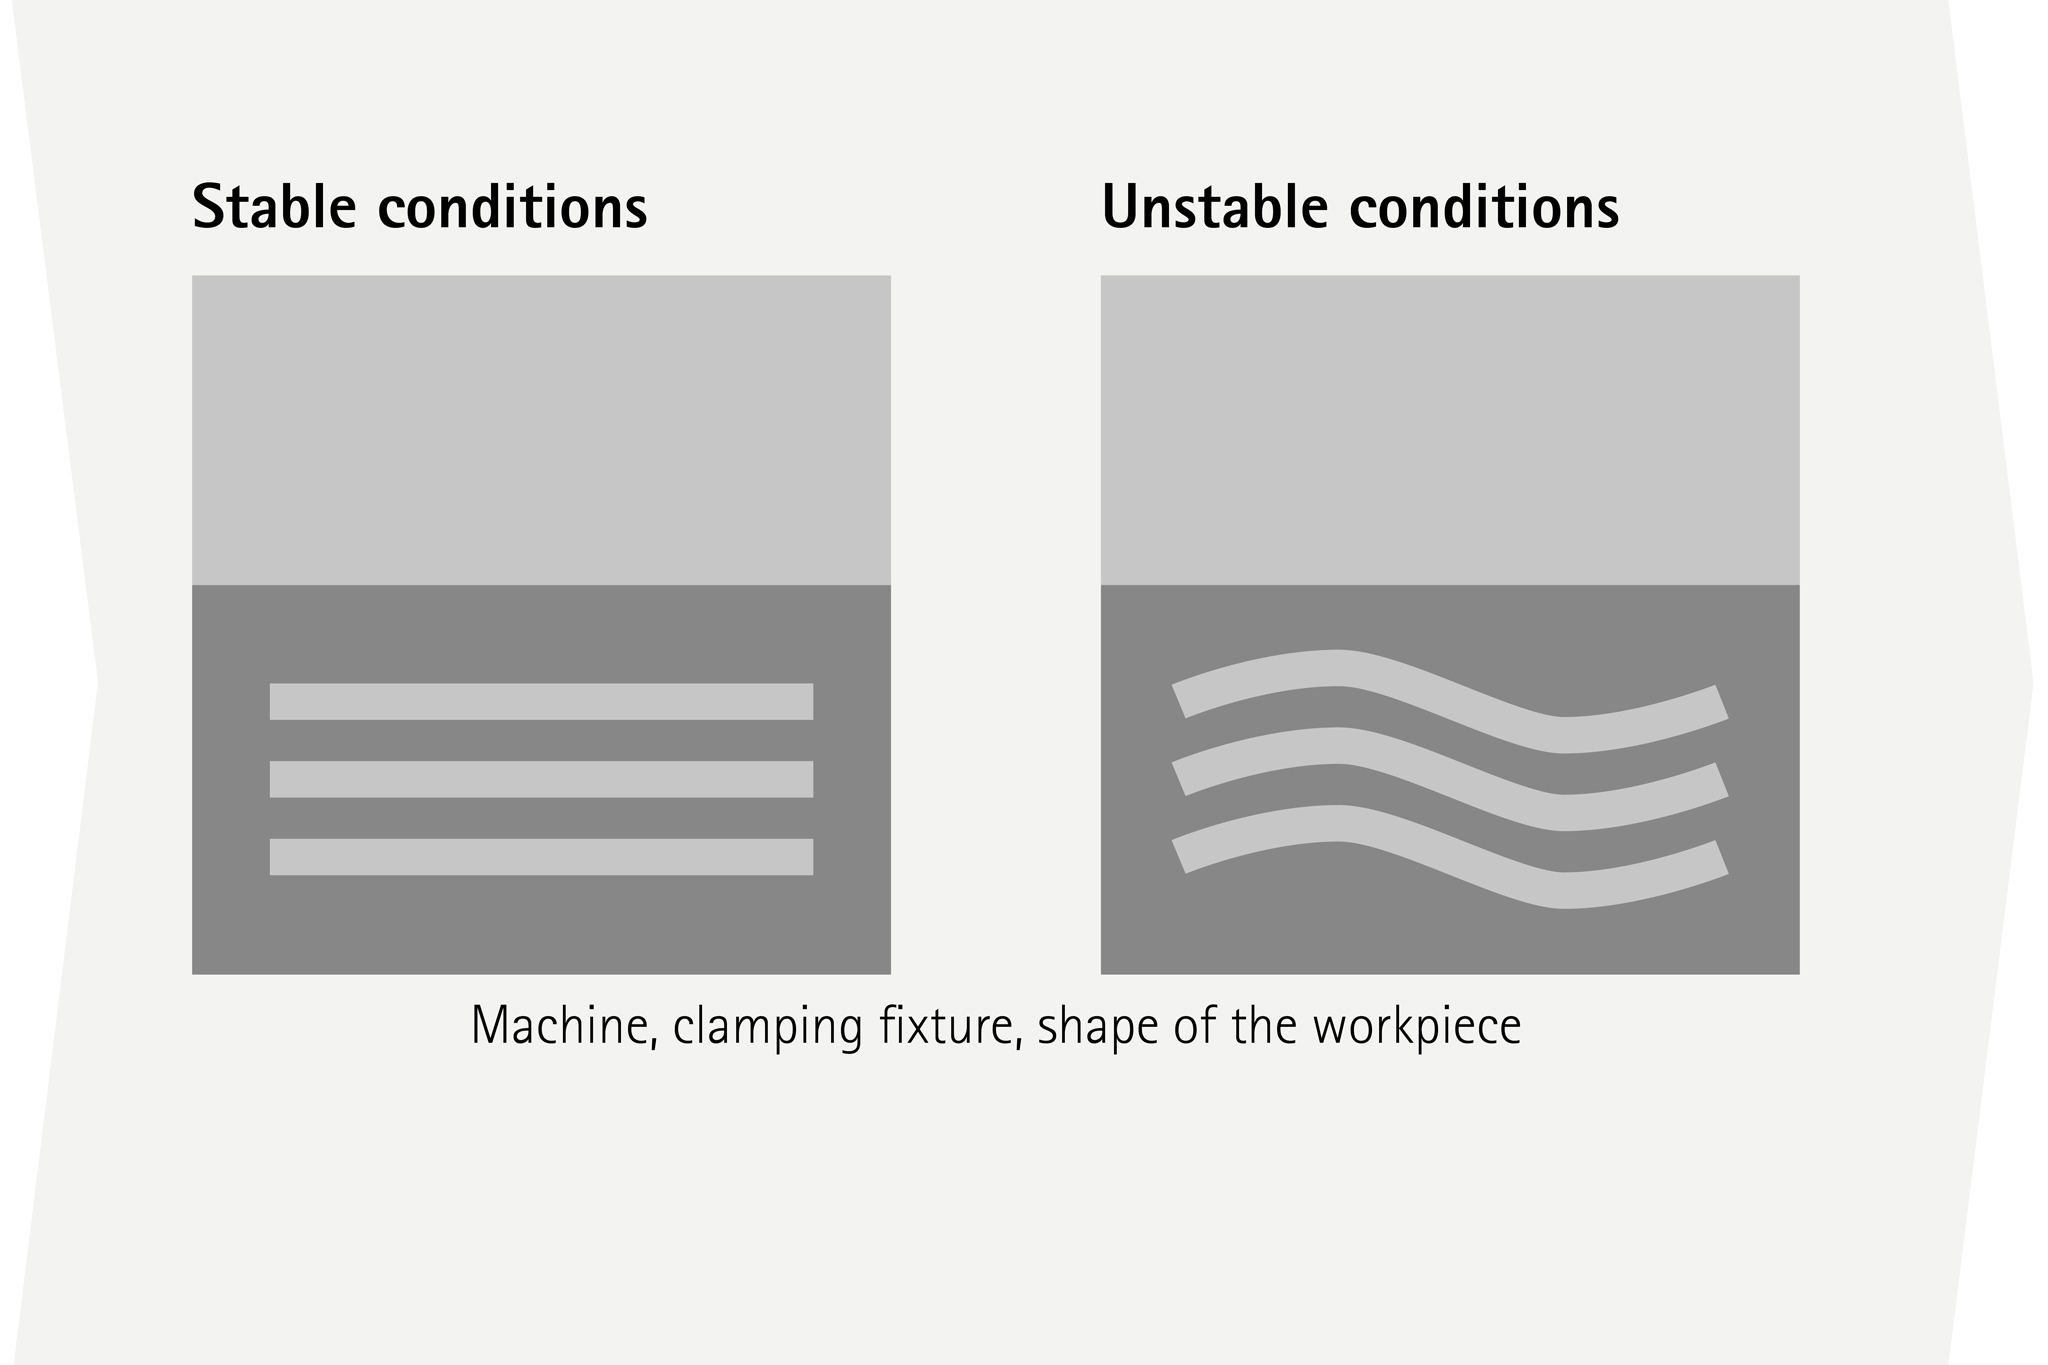
    The machine, clamping fixture and shape of the workpiece influence the machining conditions:

    • Interrupted cut
    • Low cutting width
    • Dry machining
    • Very heavy interrupted cut
    • Vibration-prone
    • Wet machining (thermal shock)

  • 3. Insert geometry / insert form

    Positive rake angle and low cutting forces are decisive in unstable conditions

    Negative rake angle: Particularly cost-effective due to double-sided use and high edge stability

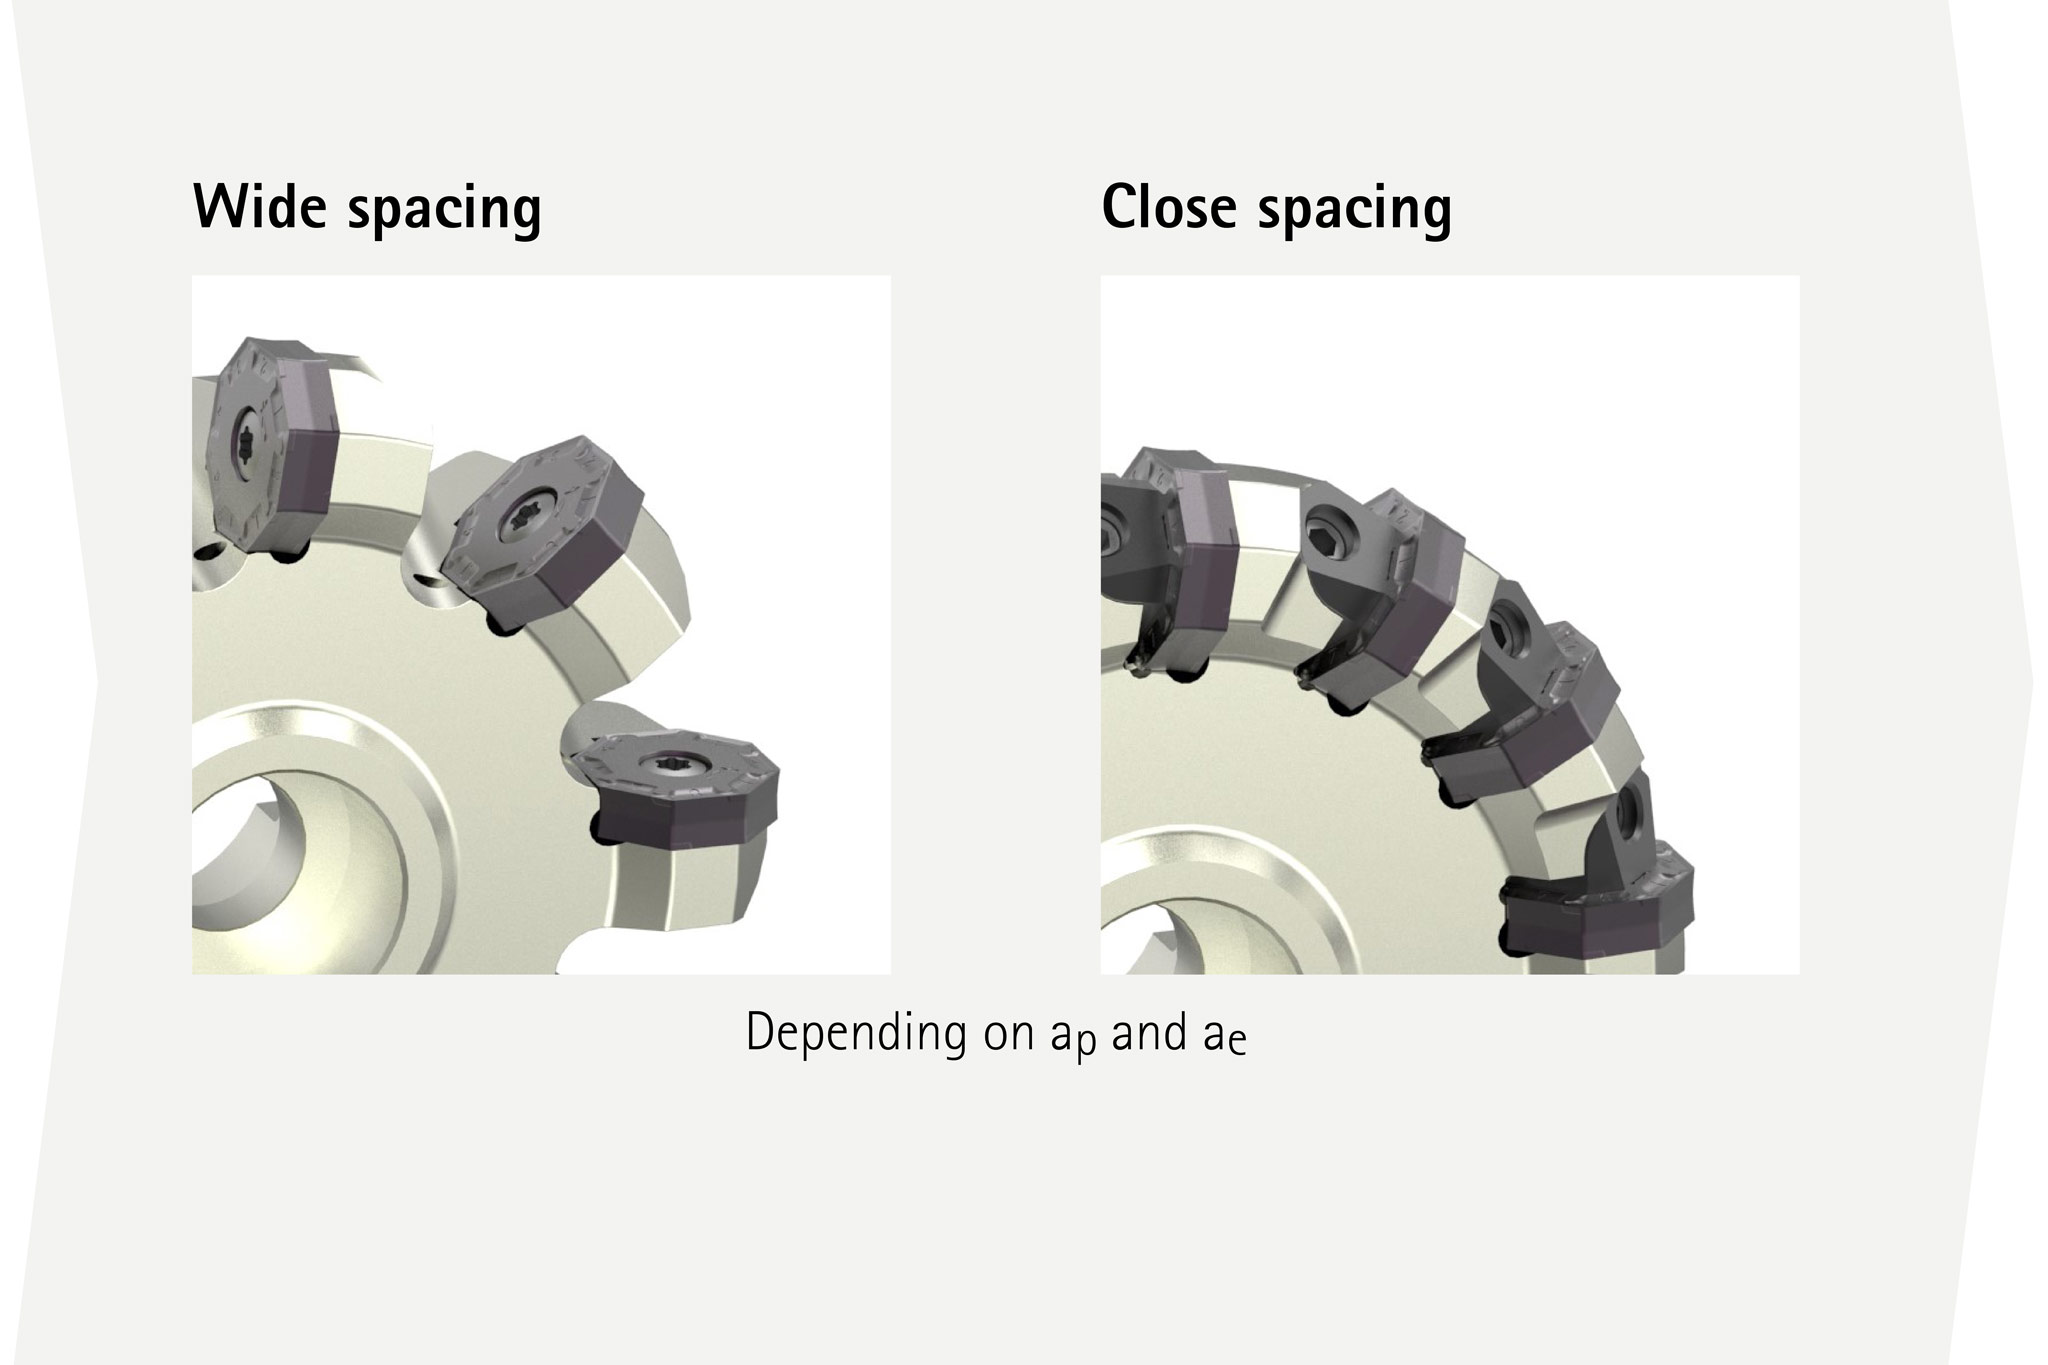
  • 4. Number of cutting edges / spacing

    Number of cutting edges and spacing depends on ap and ae

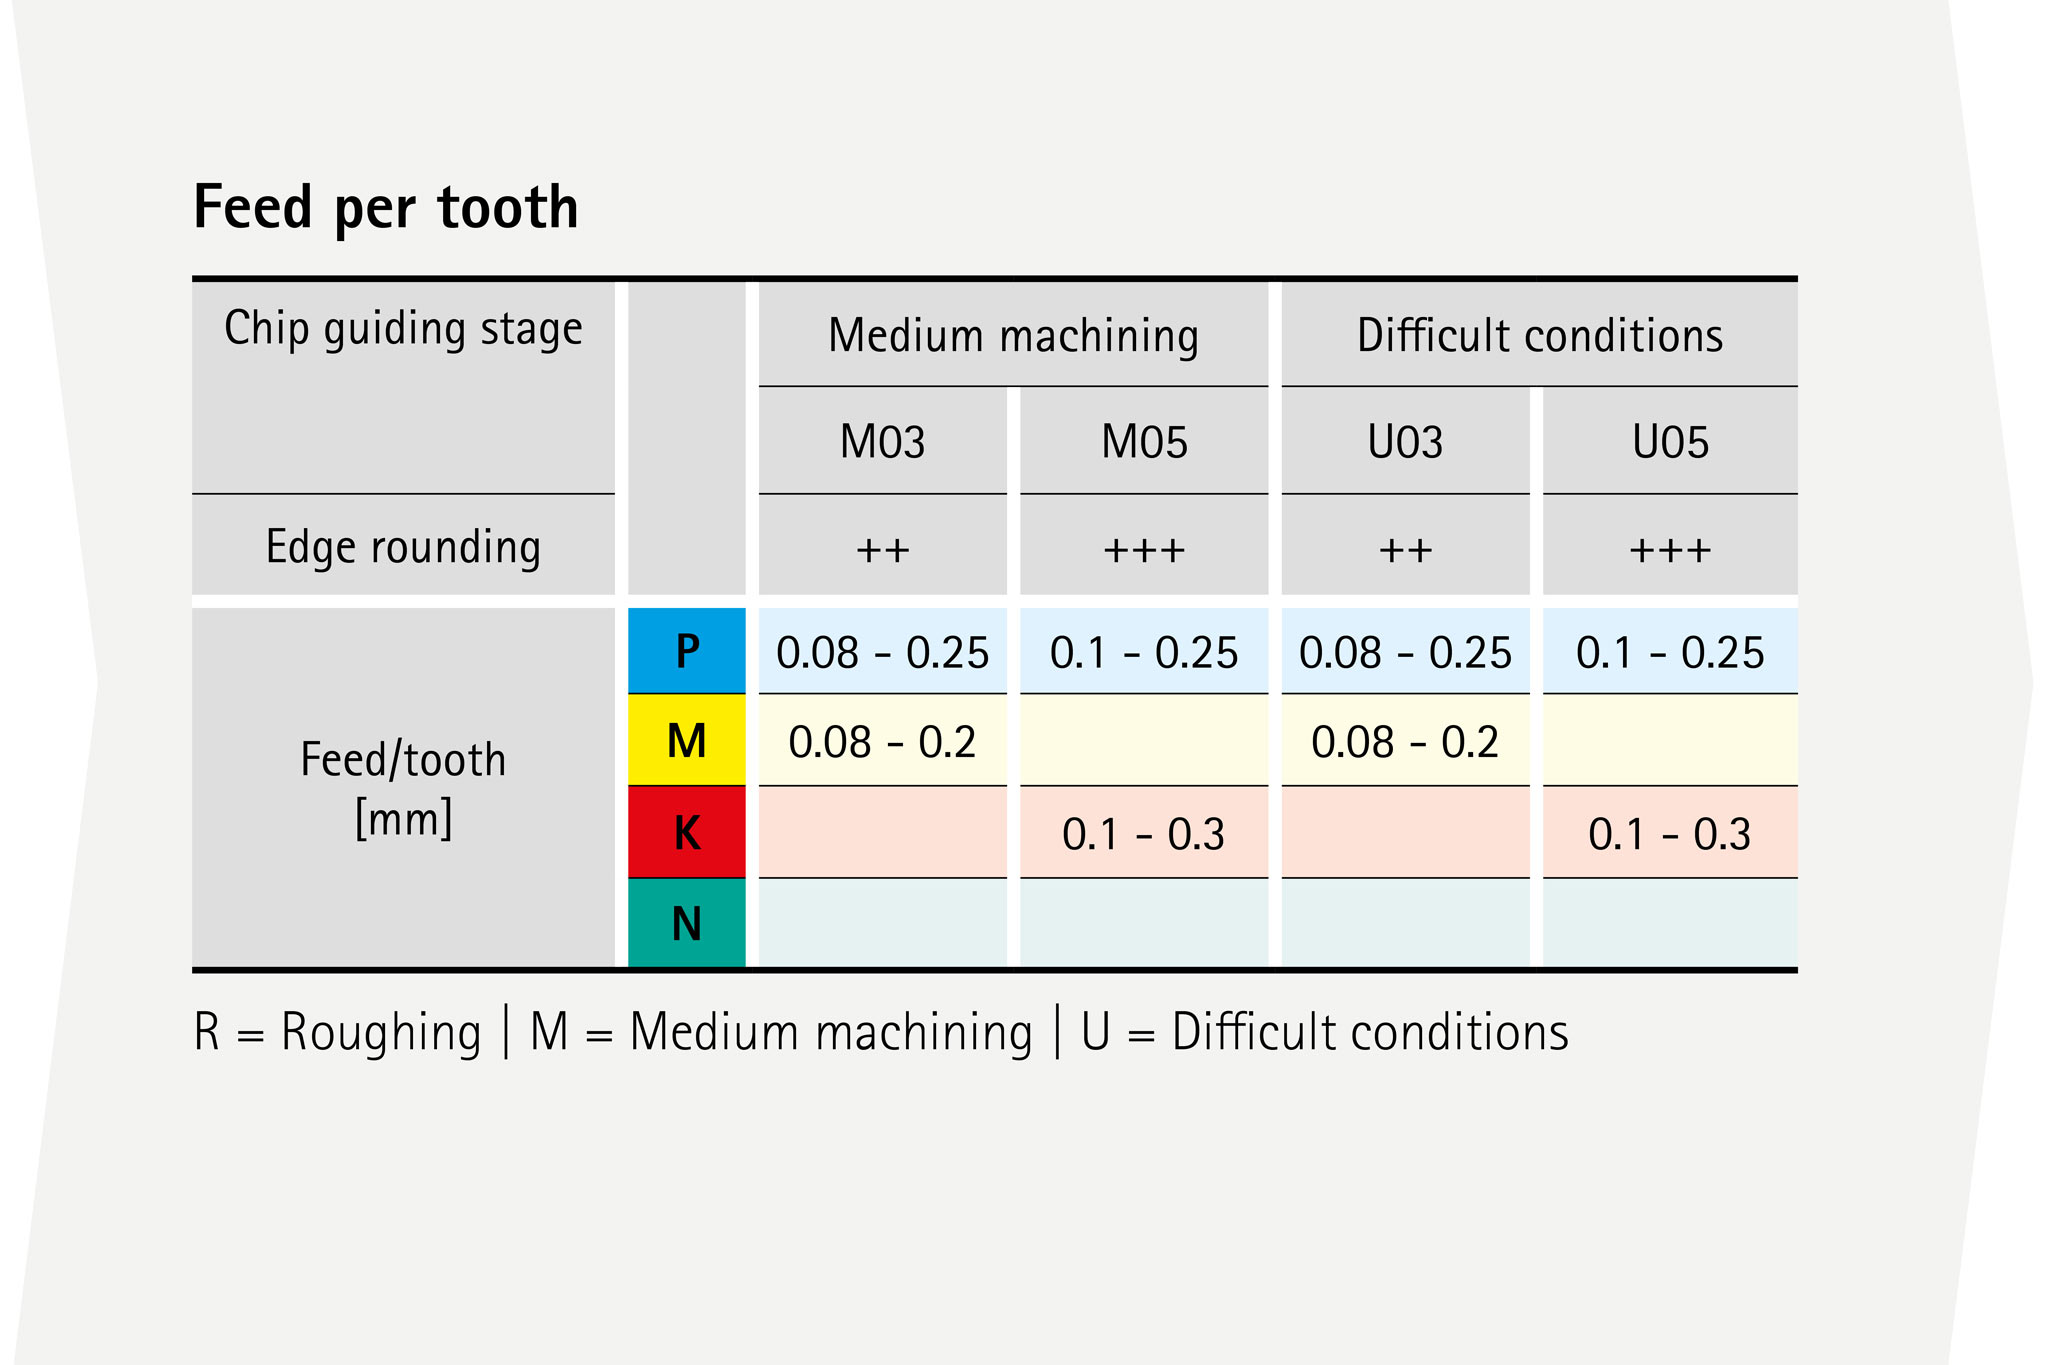
  • 5. Cutting edge design

    Cutting edge design depends on the workpiece material and application
    R = Roughing
    M = Medium machining
    U = Difficult conditions

  • 6. Fräsverhältnis ae / Ø

    Das Verhältnis von Fräserdurchmesser zur Schneidenbreite

    Das Verhältnis von Fräserdurchmesser zur Schneidenbreite ae sollte ae = 70% Dc oder ae < 25% Dc betragen

  • 7. Frässtrategie

    Einfahren mit einem Radius

    Mit Radius einfahren hält den Span im Austritt dünn, reduziert Vibrationen und ergibt beste Standzeiten

  • 8. Kalkulatorische Ermittlung der Prozessparameter

    Prozessrelevante Berechnungen

    • Schnittkraftberechnung

    • Leistung und Drehmoment
    • Vorlagen für Versuchsberichte
    • Wirtschaftlichkeitsberechnung


Innovative und prozesssichere Zerspanungslösungen erfordern ein ganzheitliches Prozessverständnis

  • Fräsanwendung & Aufspannung

    Bauteilanforderungen und Spannkonzept

  • Bearbeitungs-
    strategie

    Werkzeugauswahl und Auslegung der Frässtrategie

  • Steigerung der Produktivität

    Analyse und Optimierung der Schnittparameter und Taktzeit

  • Standard-
    programm

    Ab Lager verfügbare Werkzeuge und Wendeschneidplatten

  • Prozess-
    sicherheit & Wirtschaft-
    lichkeit

    Unterstützung beim Einsatz im Prozess 

  • Partnerschaftliche Zusammenarbeit

    Enger Kontakt und Optimierungspotentiale verbessern
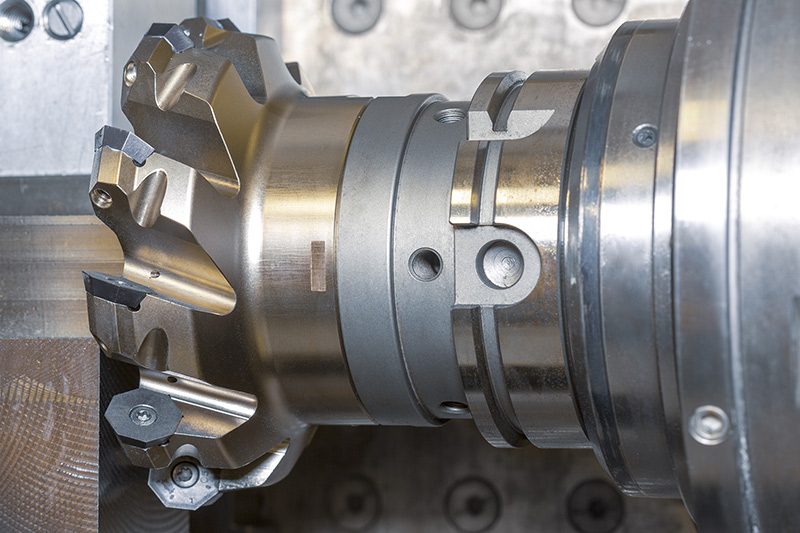

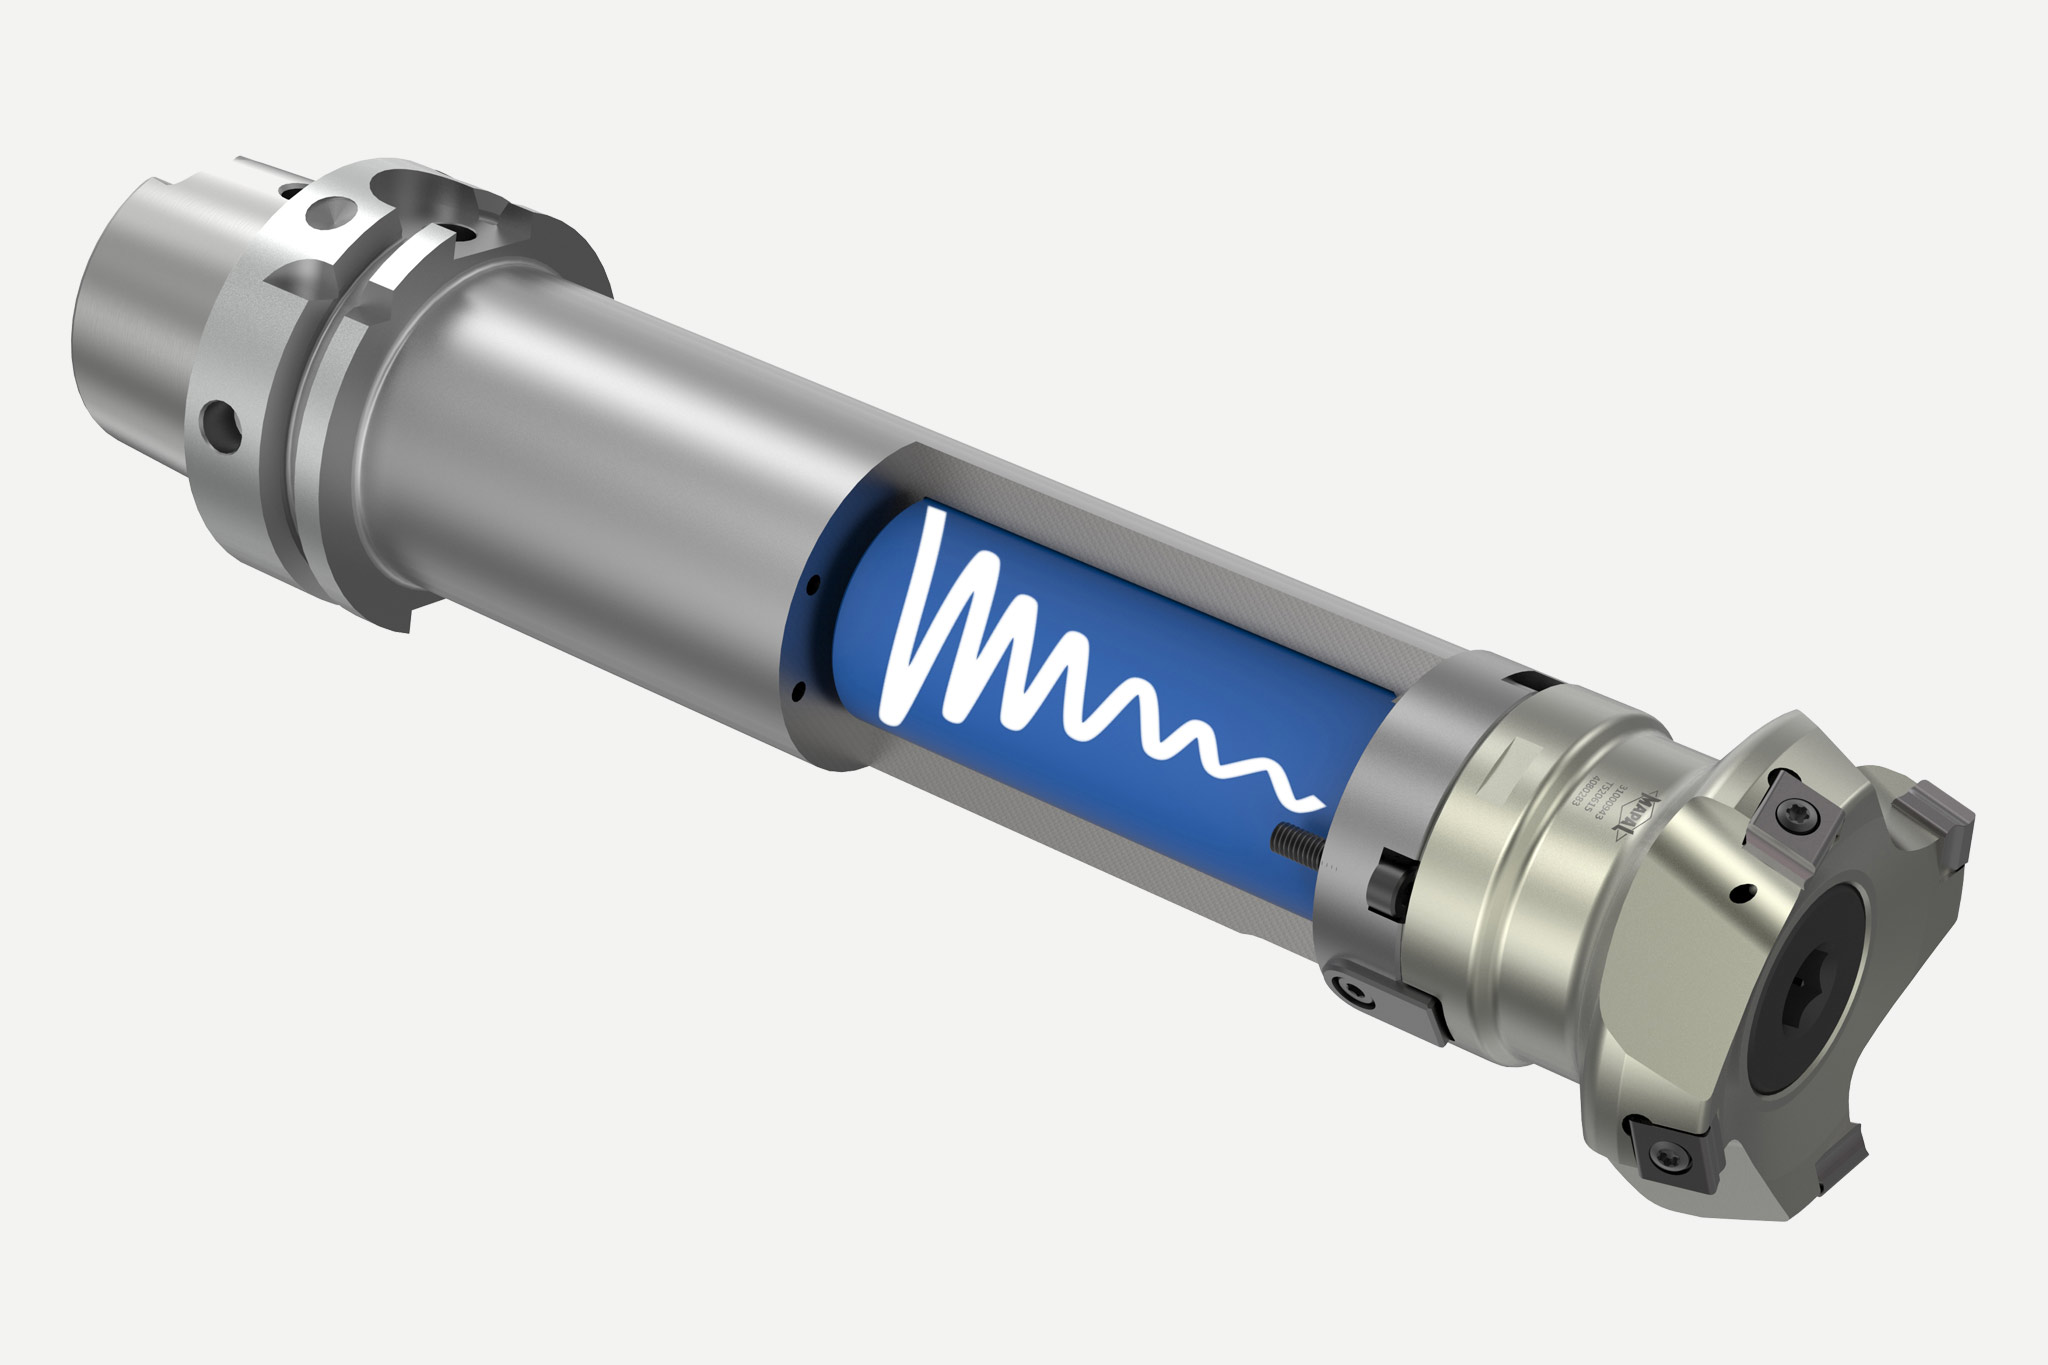
Vibrationen vermeiden durch Schwingungsdämpfungssysteme
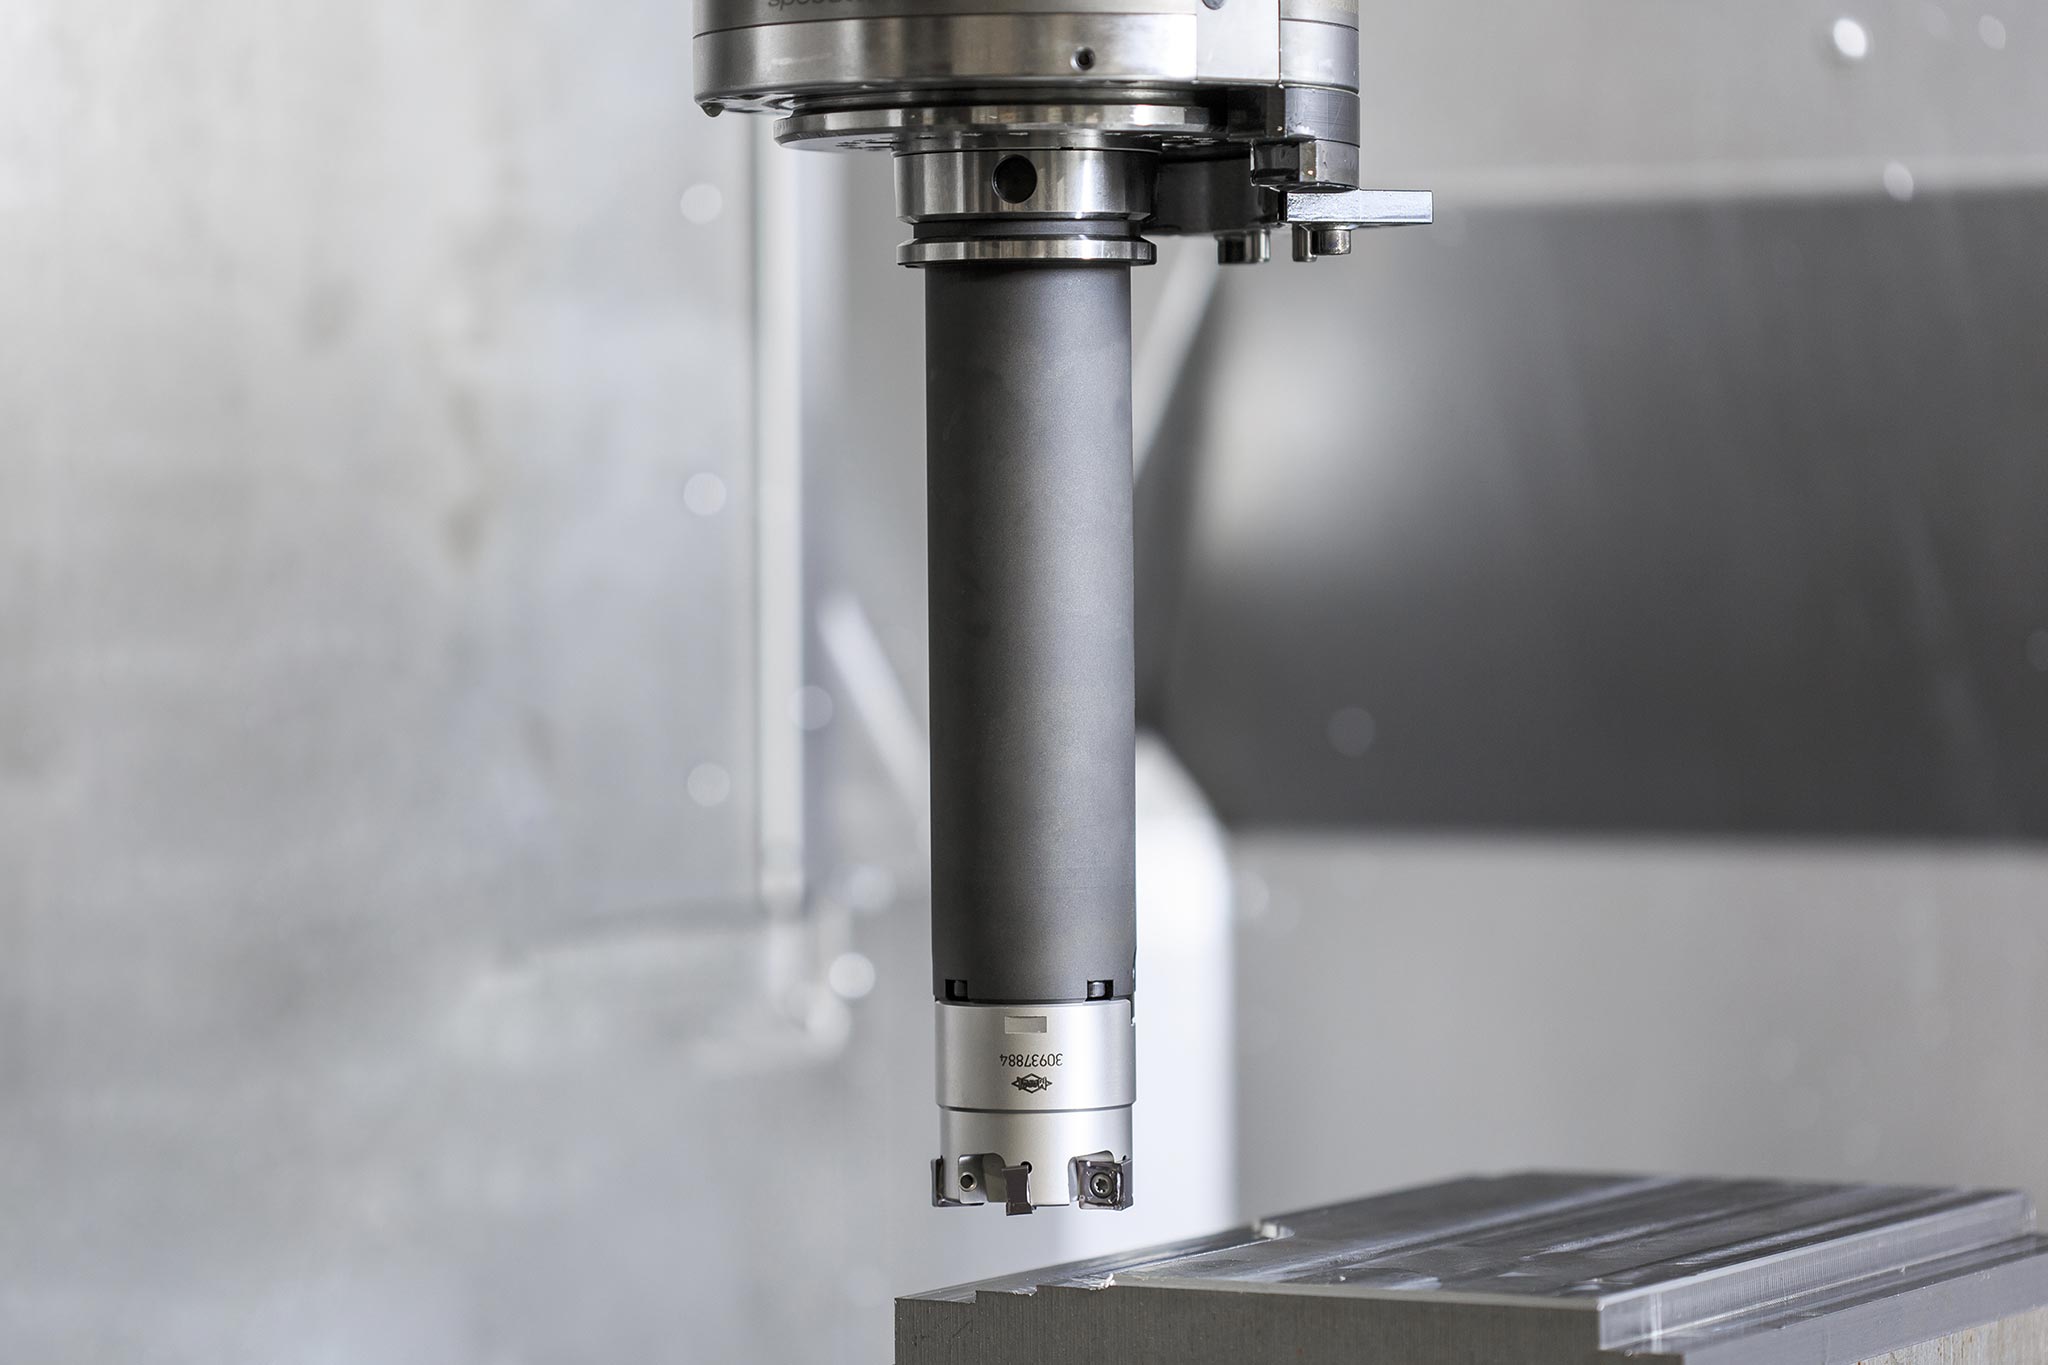
  • Herausforderungen beim Fräsen

    • Doppelte Auskraglänge entspricht 8x höherer Auslenkung, dies führt zu Schwingungen und erhöhter Geräuschentwicklung
    • Überbeanspruchung des Werkzeuges und der Maschinenspindel
    • Lange Bearbeitungszeiten durch Reduktion der Schnittparameter

  • MAPAL Lösungen

    • In sich geschlossenes System aus Schwermetallkern, Federpaket und Öllagerung
    • Werkzeugaufnahme mit Innenkühlung
    • Plug & Play: Keine Einstellung des Schwingungstilgungssystems in der Werkzeugaufnahme notwendig
    • Schwingungsdämpfungssystem sowohl im Standardbereich als auch bei kundenspezifischen Lösungen

    Mehrwert für Kunden

    • Einsparung bis zu 50% durch erhöhtes Zeitspanvolumen
    • Bis zu 60% bessere Oberflächengüten
    • Prozesssicherheit durch Vermeidung von Schneidkantenausbrüchen


Die perfekte Lösung für Ihre Fräsanwendung

Sie benötigen einen Fräser mit dem Sie ein hohes Zerspanvolumen erreichen und Ihre Standzeit erhöhen können? Dann haben wir für Sie, mit unserem NeoMill-Fräsprogramm die perfekte Lösung. 


Ihr direkter Kontakt

Heiko Rup, Produktmanager bei MAPAL.

Ansprechpartner

Heiko Rup Product and Application Management heiko.rup@mapal.com Phone: +49 7361 585 3034