11.05.2023
A strategy for battery frames
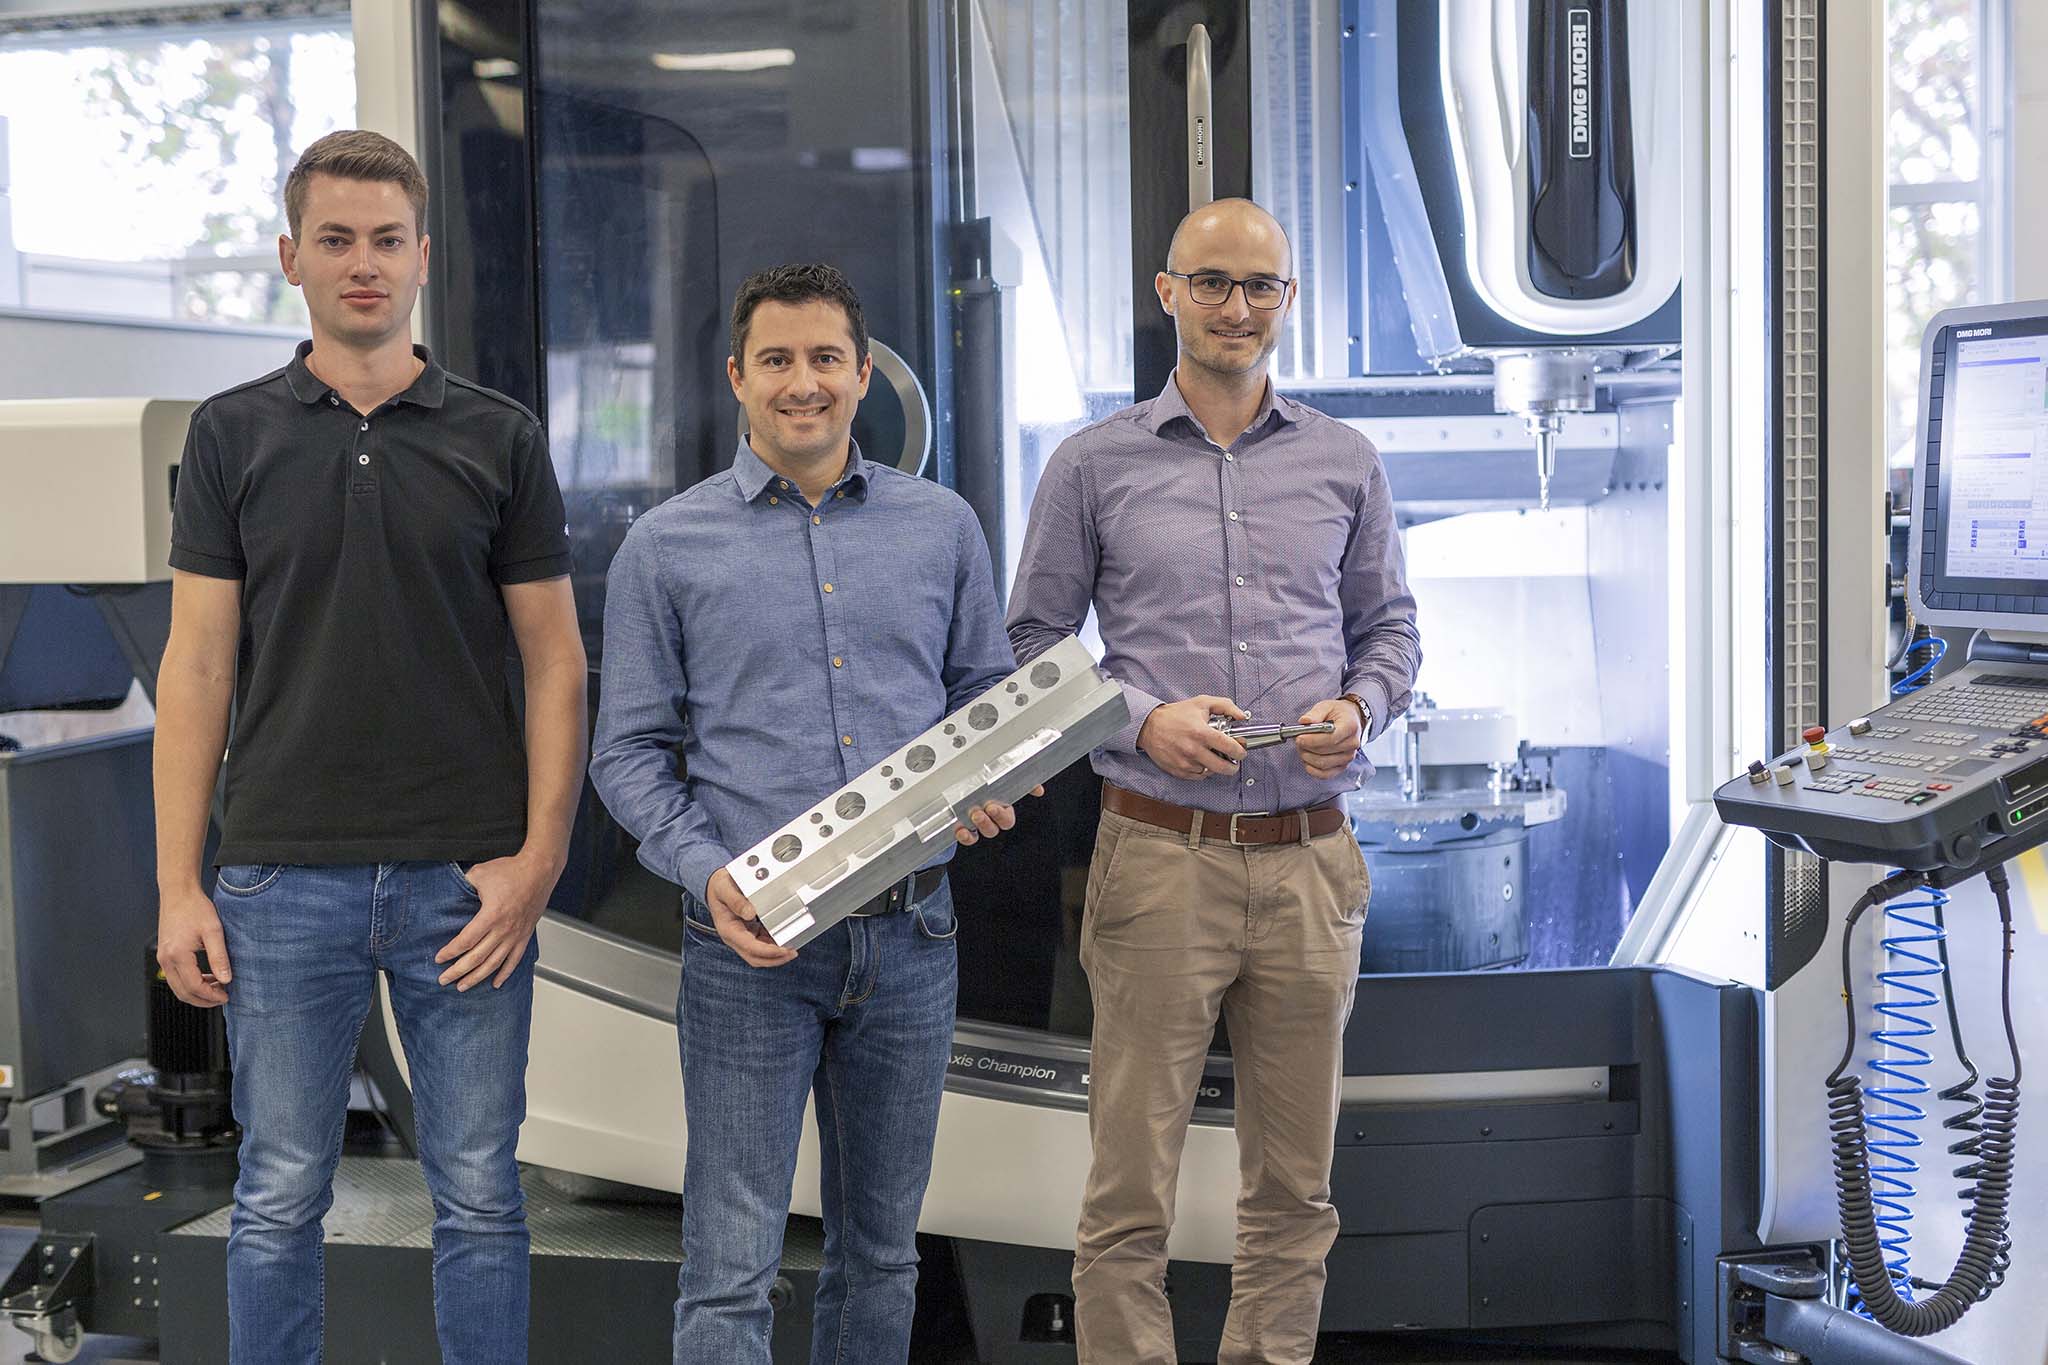
The complete machining of parts has to be well thought out, every step coordinated with the next. This is the only way to attain reliable and cost-effective manufacturing with perfect results. To provide customers with such sophisticated strategies, MAPAL has defined focus components on electric cars and worked out the optimal machining strategy for them. The battery frame is one of these components.
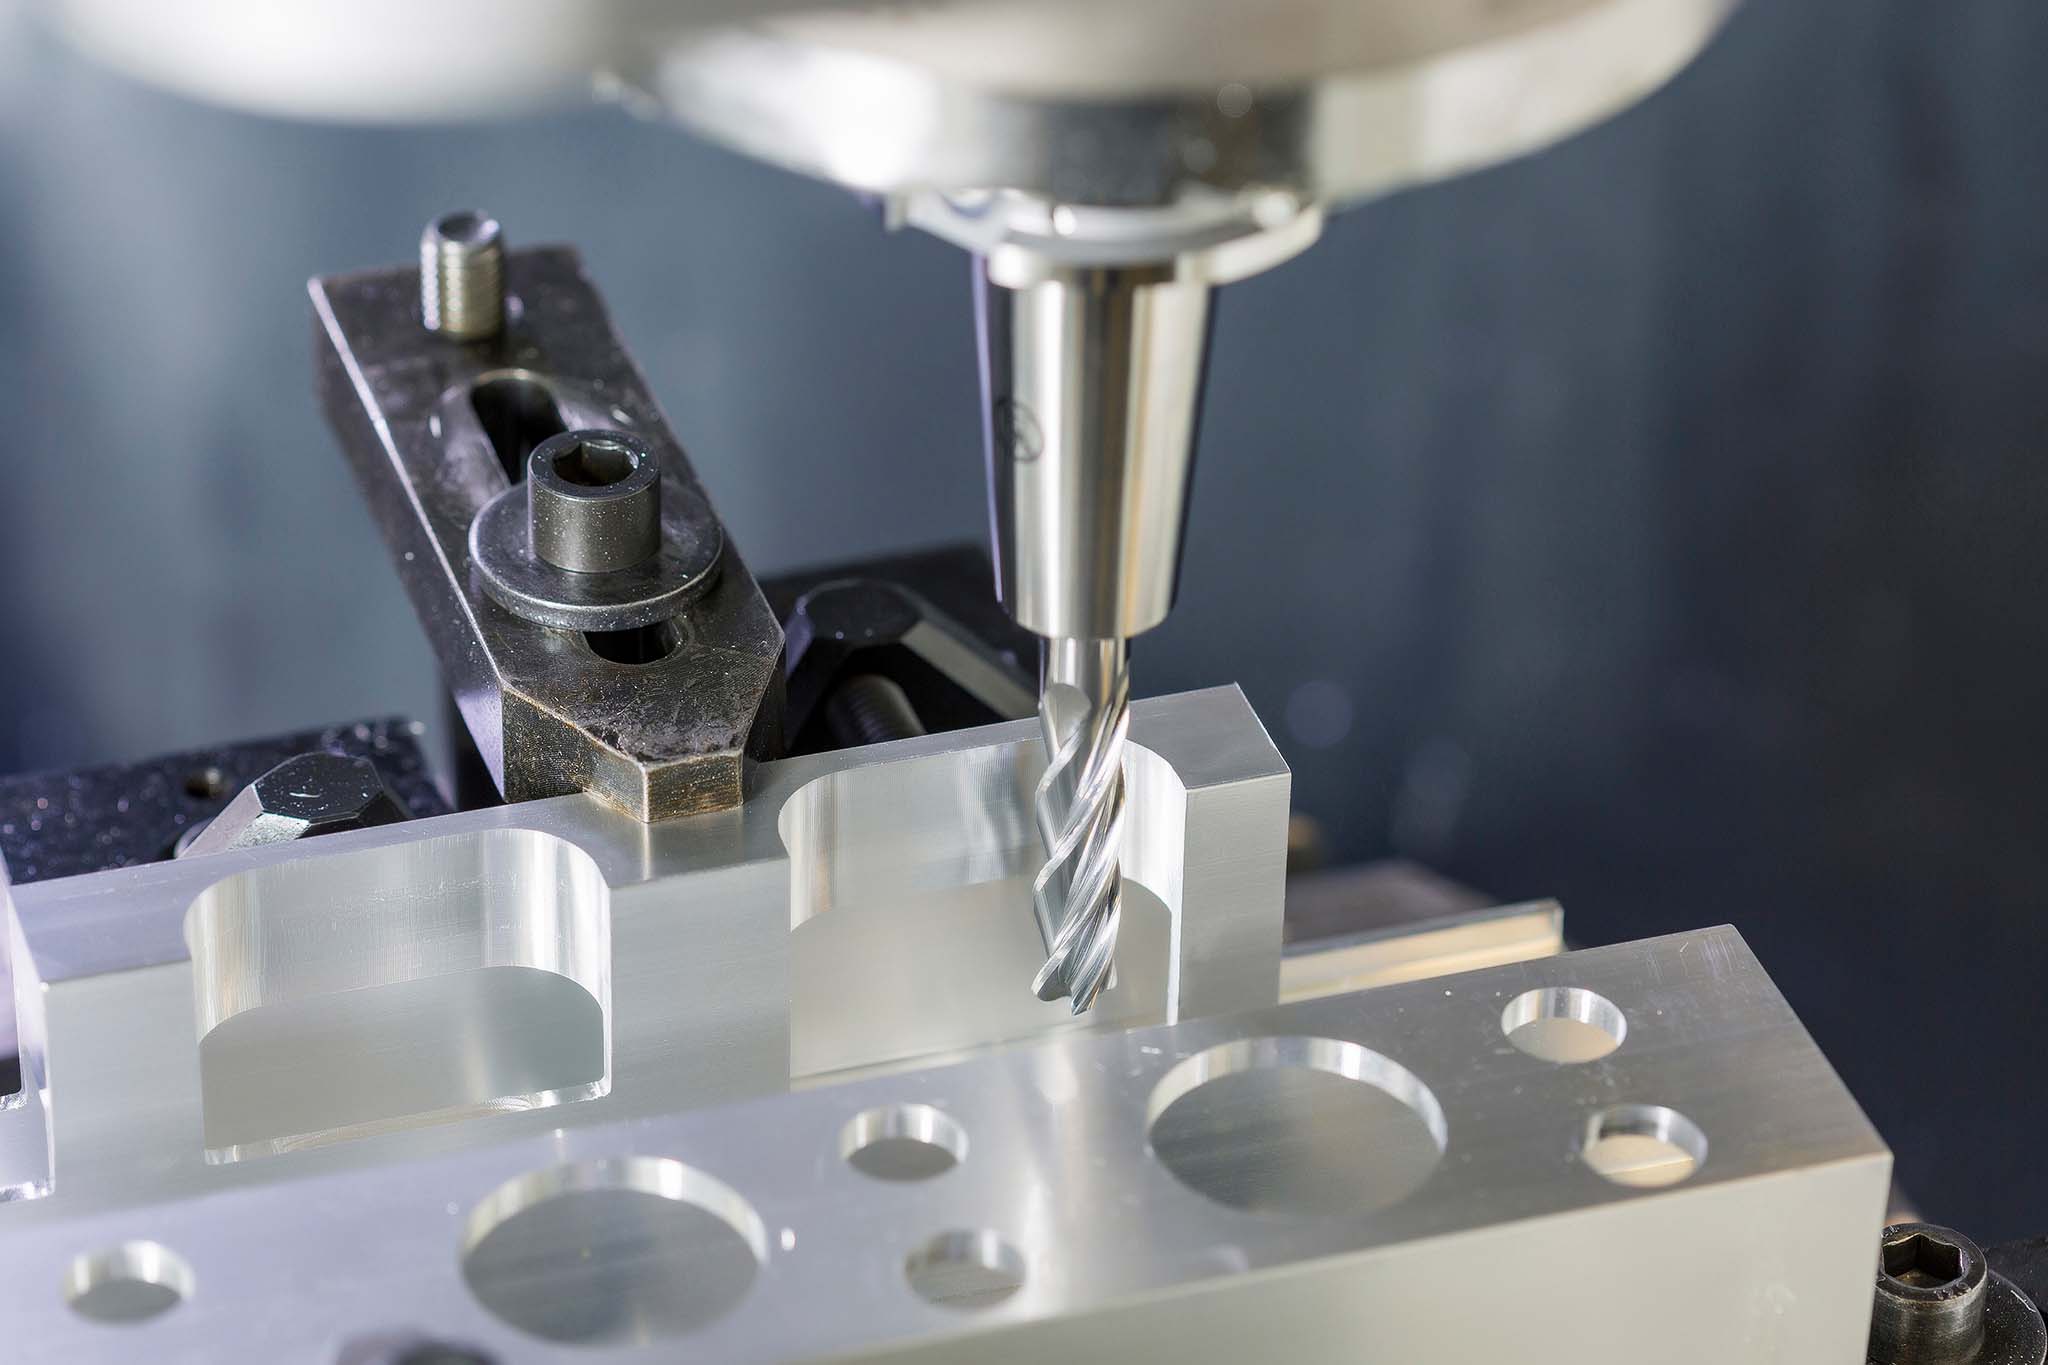
Als herausfordernd bei der Zerspanung zeigen sich am Bauteil unter anderem gestufte Bohrungen, Bohrungen mit unterschiedlichen Durchmessern durch mehrere Layer, gefräste Taschen mit verschiedenen Abmessungen, Absätze und hohe Anforderungen an die erzeugte Oberfläche.
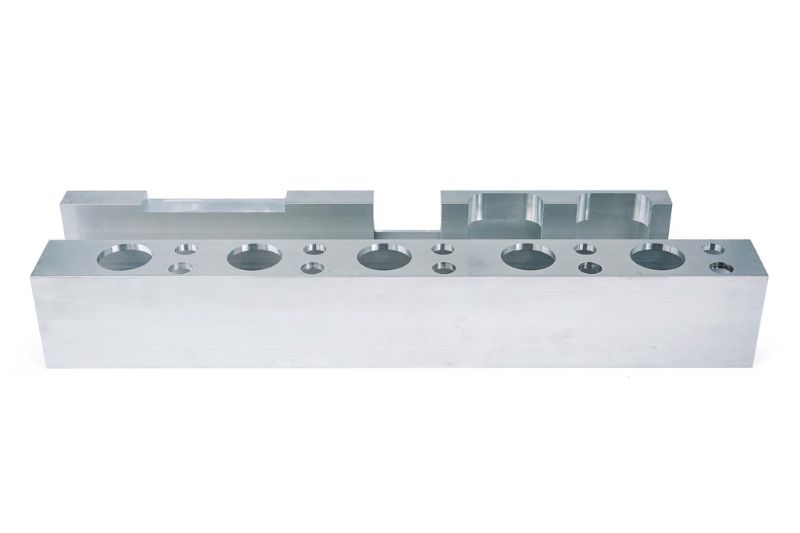
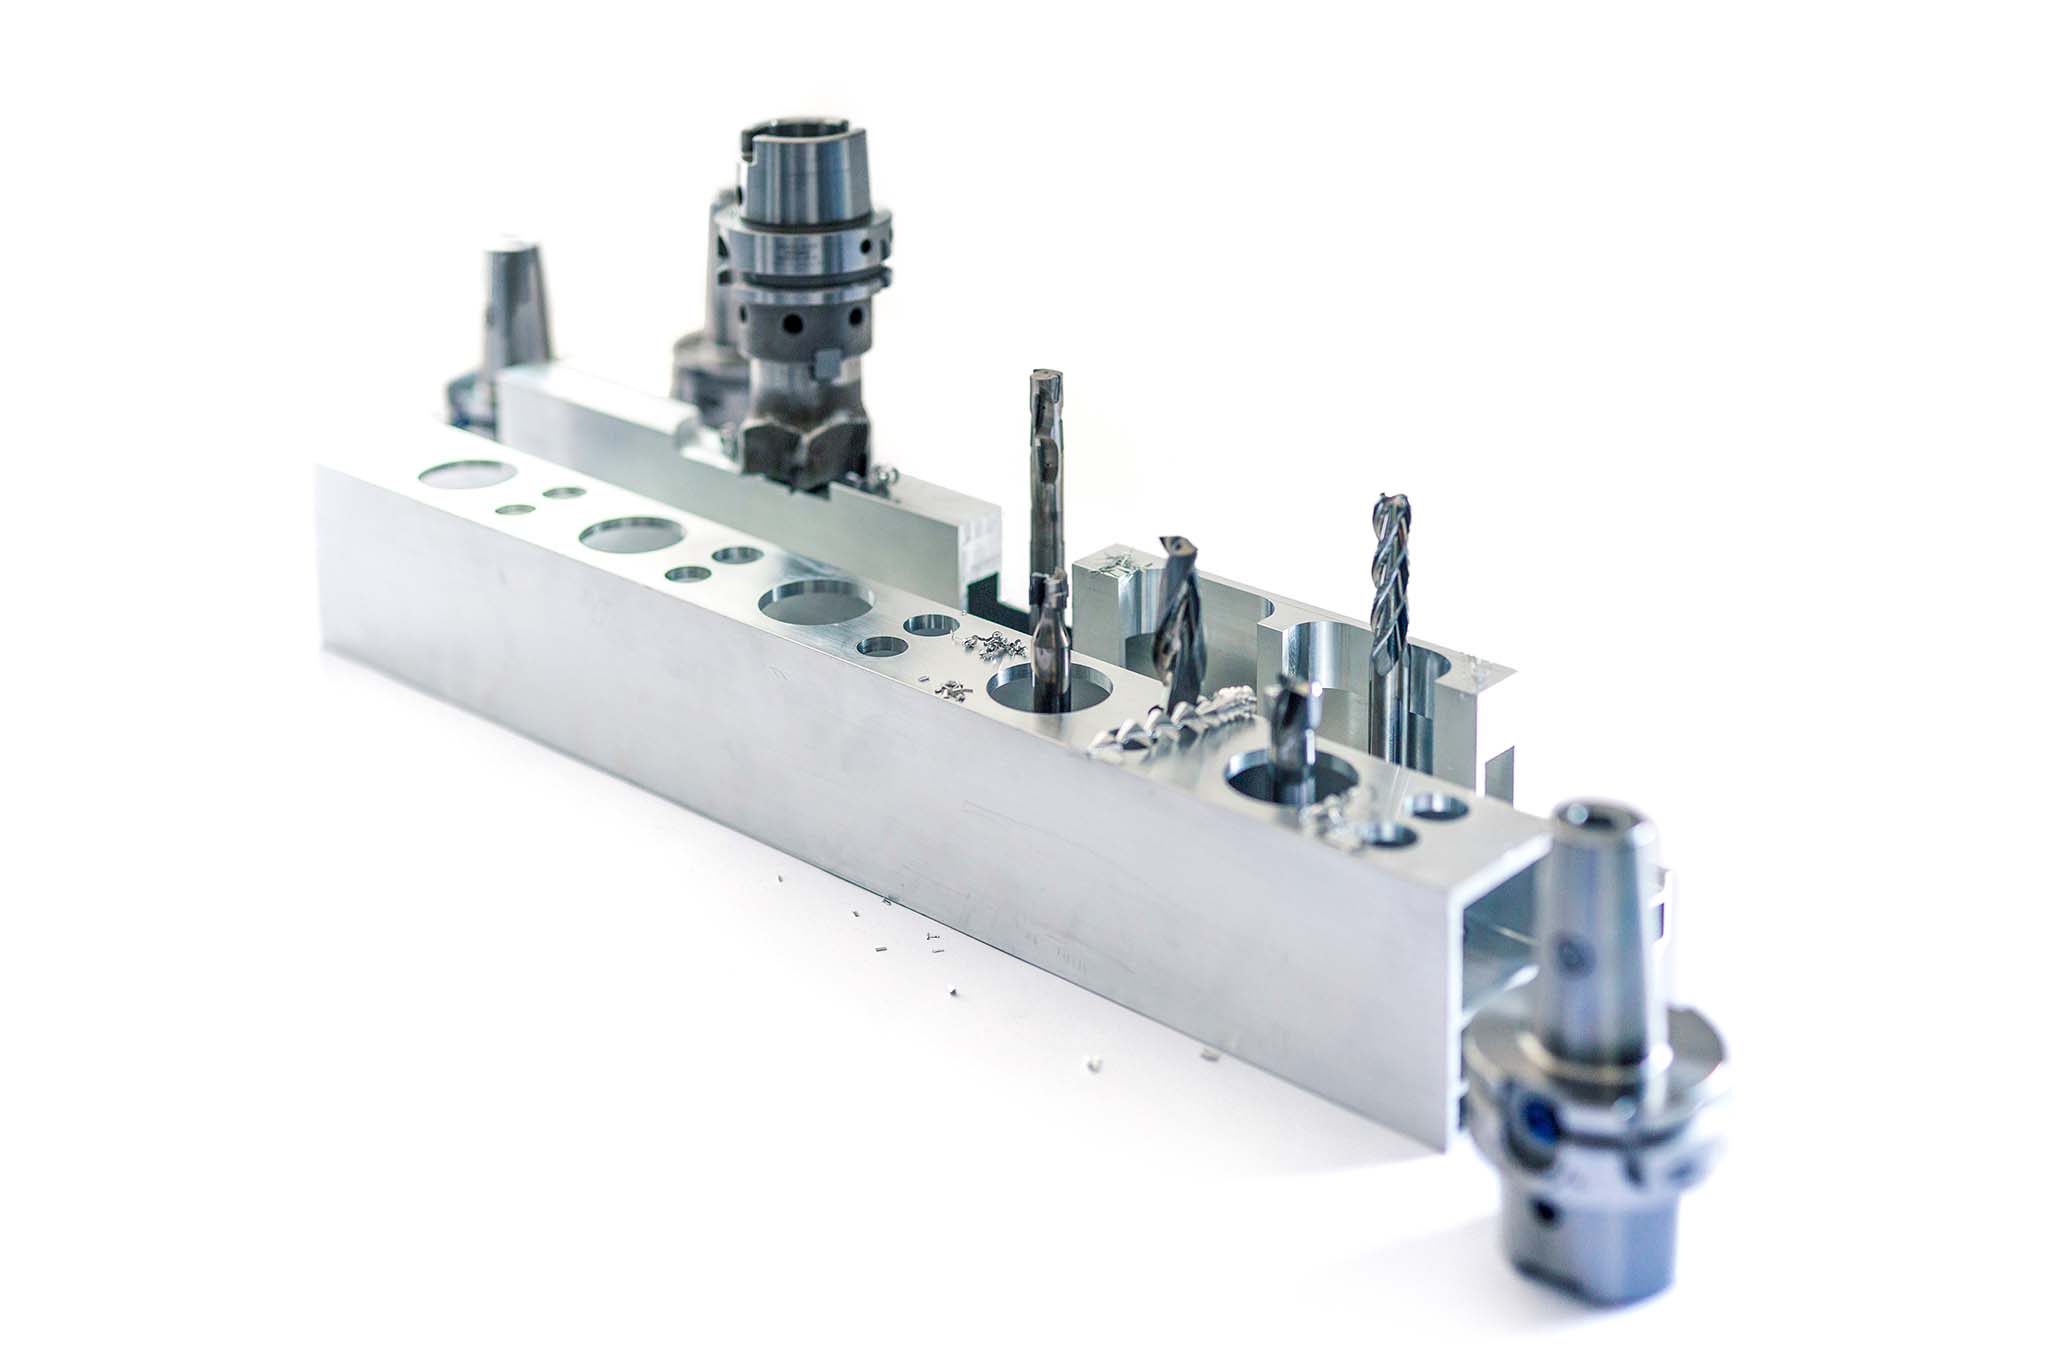
「私たちは、何よりも最適に設計されたフライスを使用して、これらの課題を克服します」と Kucher 氏は言います。 フレーム部分のほとんどの穴にフライス加工が使用されています。 直径と加工深さに応じて、専門家がそれぞれのケースでドリルを使用するかフライス加工を行うかを決定します。 「穴のフライス加工のサイクル時間は若干長くなりますが、この場合、フライス加工には、失われた時間を補って余りある決定的な利点があります。」 以前は、アルミニウム部品の穴あけ中に発生する長い切りくずが、お客様にとって非常に問題となることがよくありました。 「フレーム部品の内側から長い切りくずを除去することは、プロセスにリスクをもたらしました」と Kucher 氏は言います。 短い切りくずは簡単に除去できます。 また、ドリル加工よりもフライス加工はバリの発生が大幅に少なくなります。 また、ツールをチェンジする必要もありません。径の異なる複数の穴を 1 種類のフライス工具で簡単に加工できます。
このメリットは、穴が上面の穴入口よりも下面の径の方が大きい場合に特に顕著になります。 「これは、フライスの逆刃を使用すると効果的に行うことができます」と Kucher 氏は言います。 別の方法としては、ワークピースを再クランプして、ドリルで下面から穴を加工することになります。 MAPAL の特別に設計された PCD フライスは、スピンドル速度 16,000 rpm、切削速度 650 m/min、送り 0.063 mm で穴を加工します。
Optimal surfaces with the OptiMill-SPM-Finish
MAPAL recommends the OptiMill-SPM-Finish for roughing shoulders, pockets and slots as well as finishing pockets. “It achieves an optimal surface finish and works stably even in corners with large wrapping and high loads”, Kucher says of the tool. Because the chip spaces are polished, chip removal functions perfectly. The special feature of this tool is that the user can finish large depths in a single pass. This saves time, making it particularly cost-effective. When finishing the battery frame, a surface finish of up to Rz = 1 µm is achieved. During roughing, it operates at a spindle speed of 10,981 rpm, a cutting speed of 414 m/min and feed rates between 0.12 and 0.22 mm. The same spindle and cutting speeds are achieved during finishing with a feed of 0.075 mm.
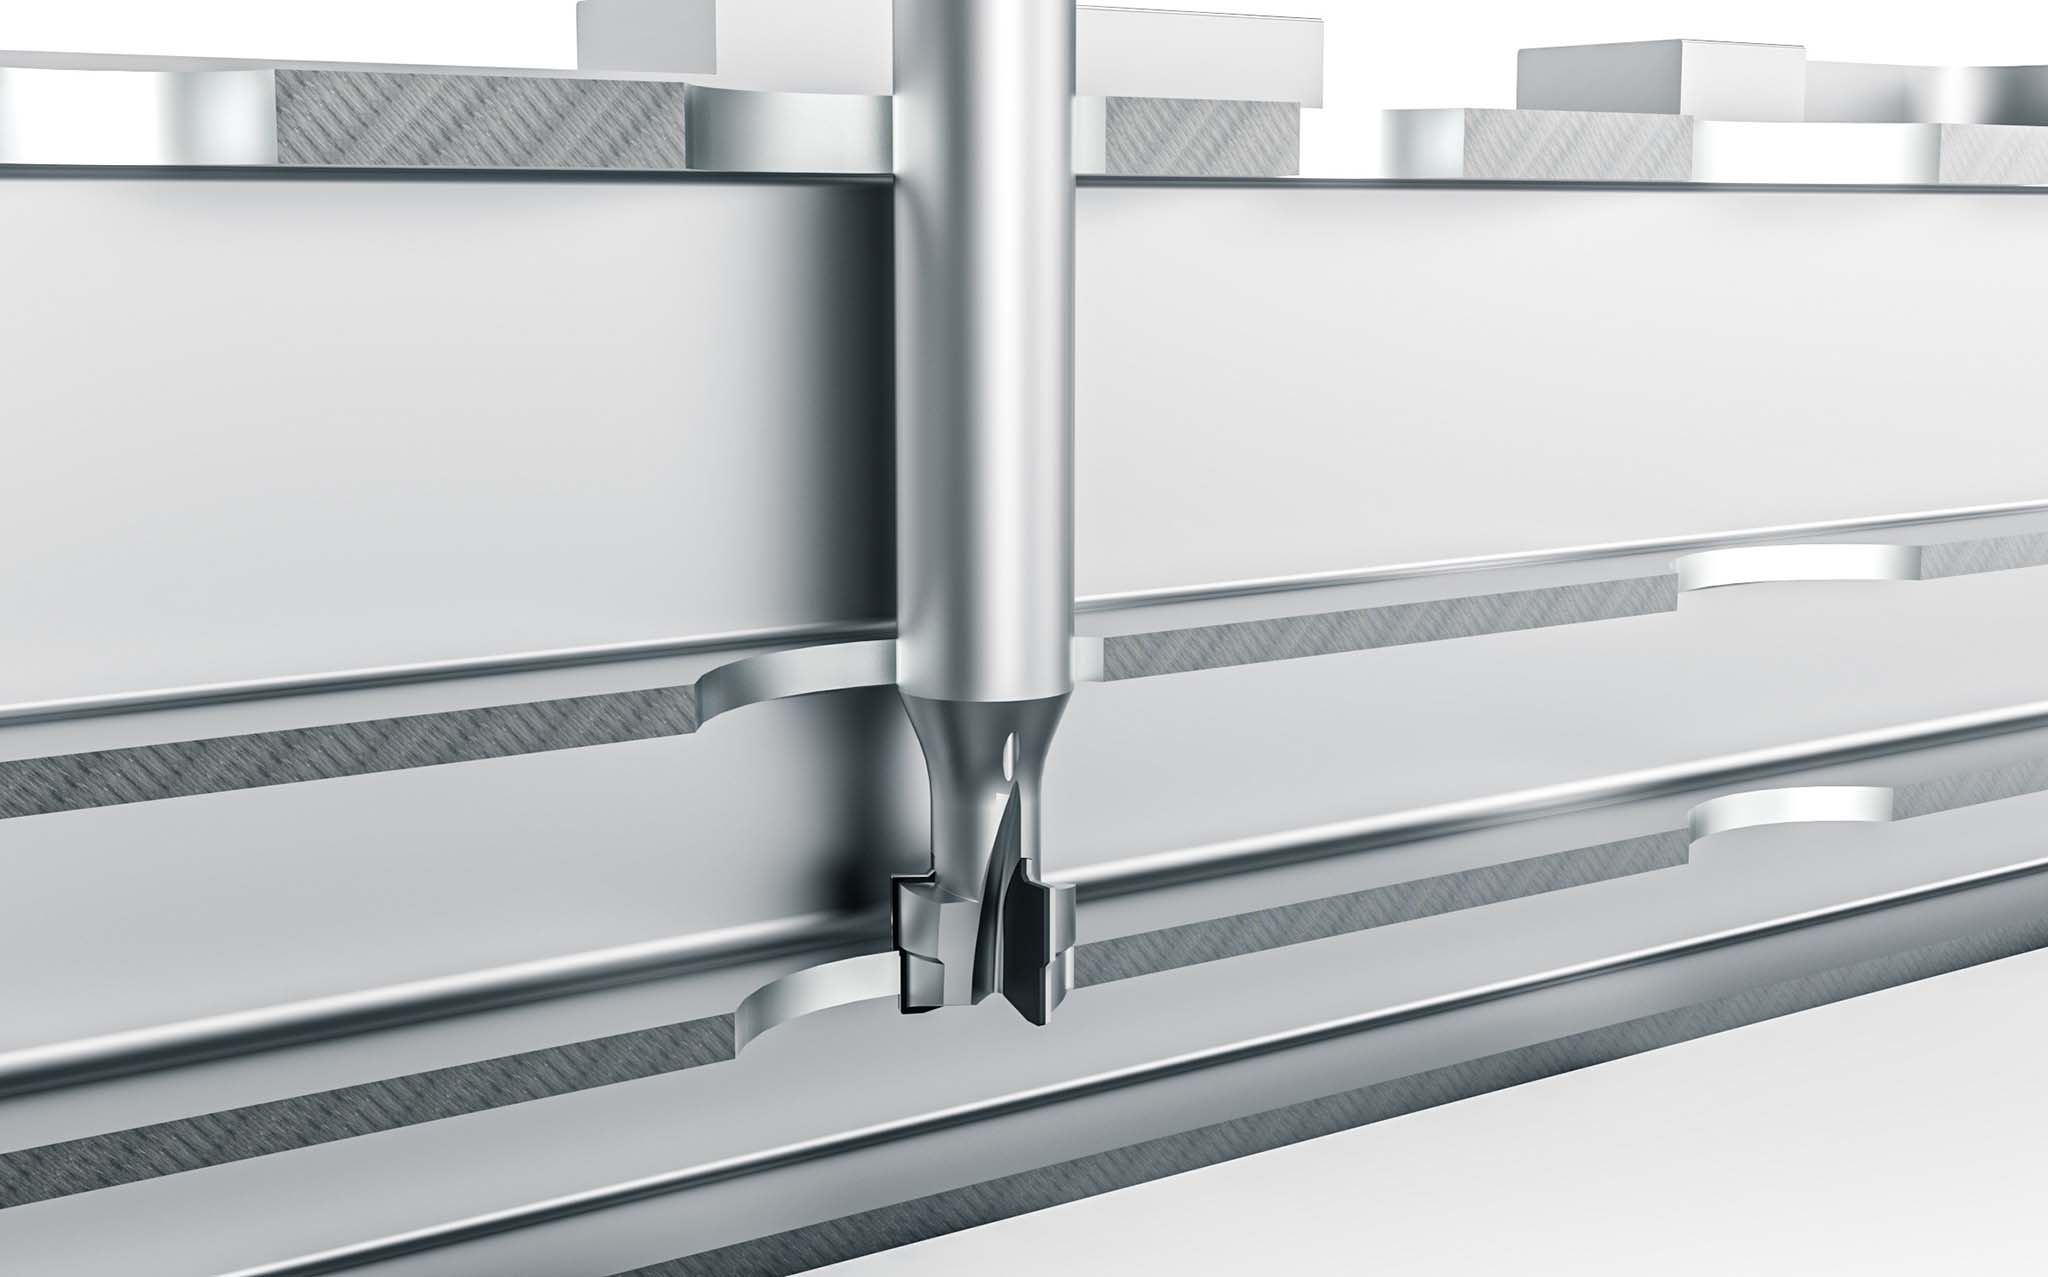
In total, seven tools are used during the generic process, including six milling cutters: besides the OptiMill-SPM-Finish, amongst others the recently introduced FaceMill-Diamond-ES. In order to attain a perfectly harmonised system, all of the tools with cylindrical shanks are clamped in the new UNIQ chucks in the generic process.
“We can now offer our clients an all-round package to meet the challenges of machining battery frames, which includes PCD and solid carbide tools, chucks, and the corresponding process. For this we adapt the generic process for our customers based on their concrete situation”, Kucher explains.
Contact
Kathrin Rehor Public Relations Kathrin.Rehor@mapal.com Phone: +49 7361 585 3342