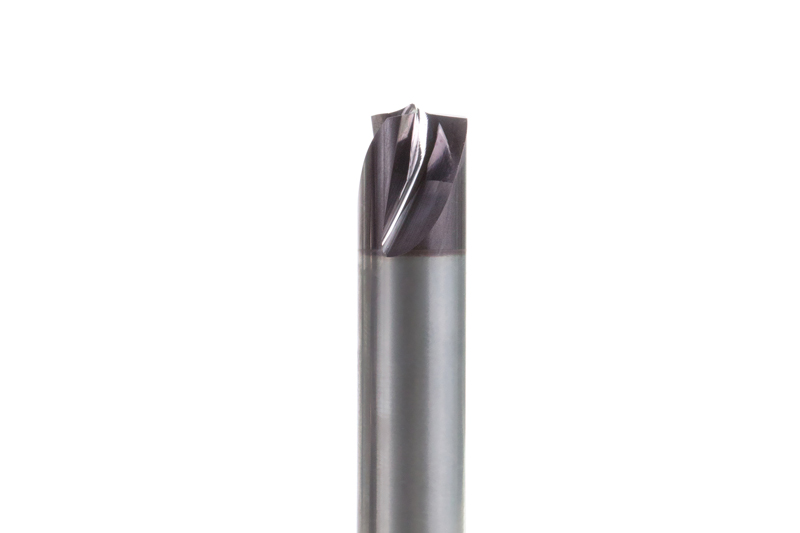
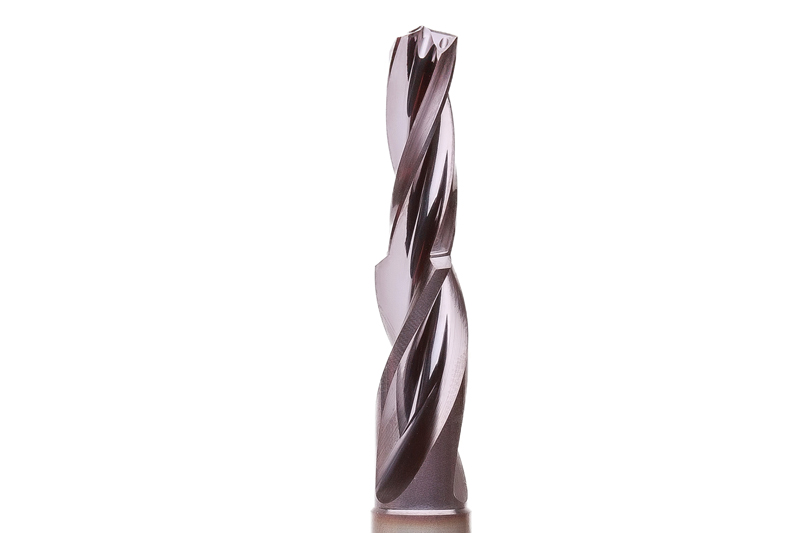
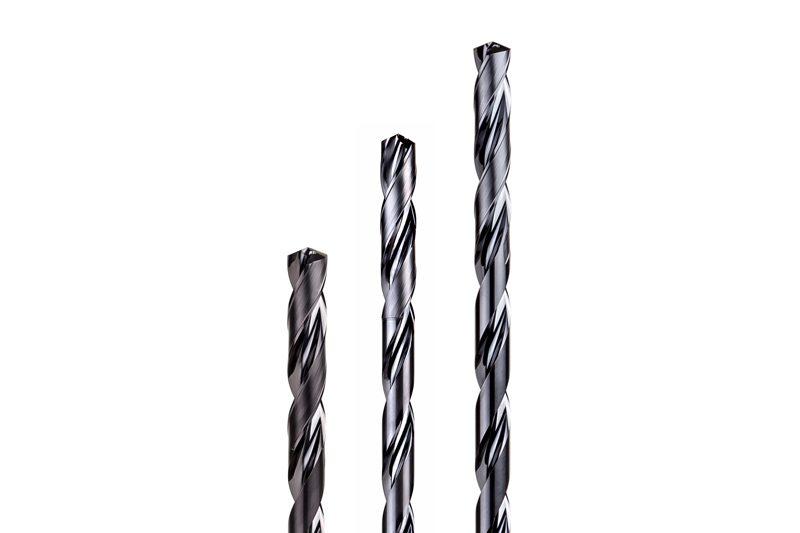
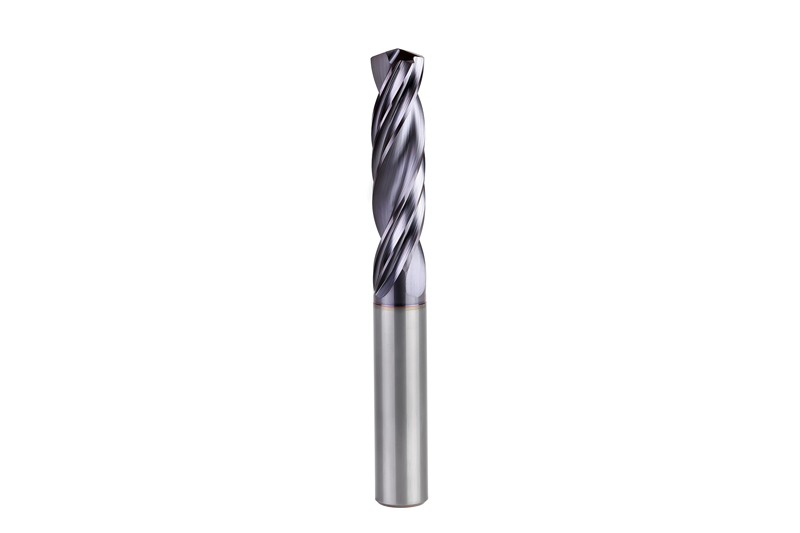
Fresas inteiriças de metal duro
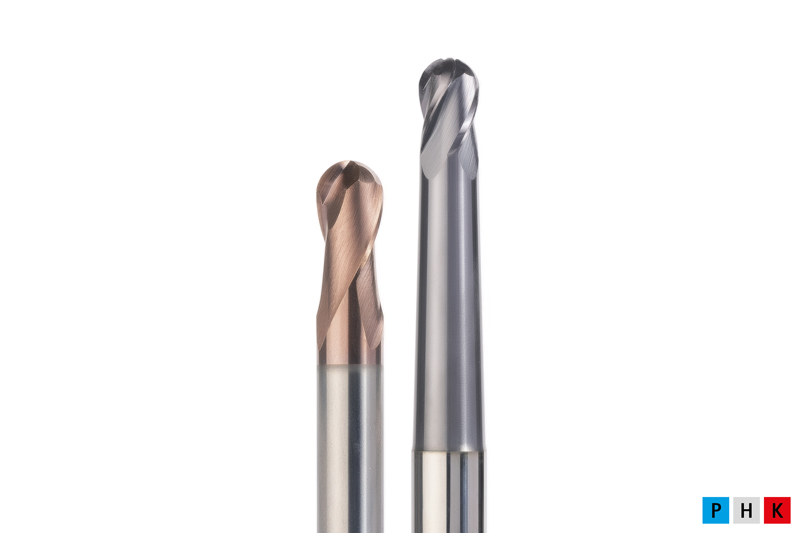
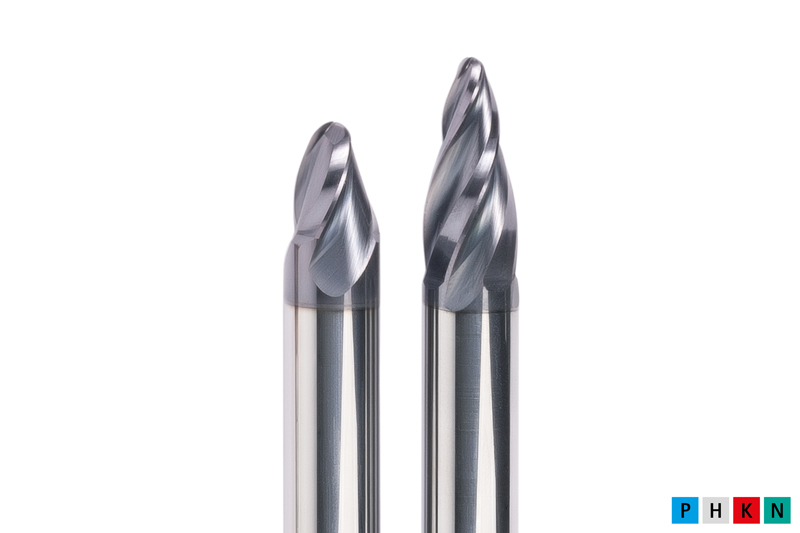
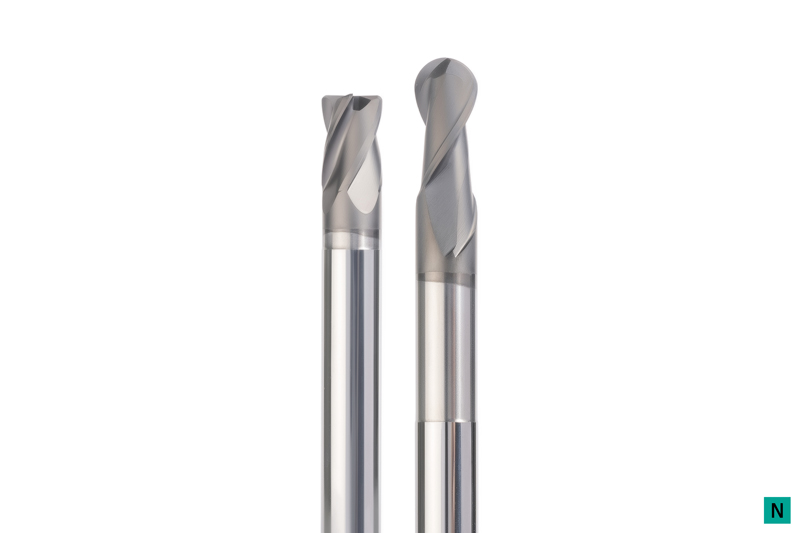
OptiMill-3D-BN
Fresa esférica metal duro Usinagem de contornos 3D com alta precisão Gama ø: 0,10 - 20,00 mm
OptiMill-3D-CR
Fresas com raio da canto Fresamento com alta precisão em raio de canto Gama ø: 0,10 - 20,00 mm
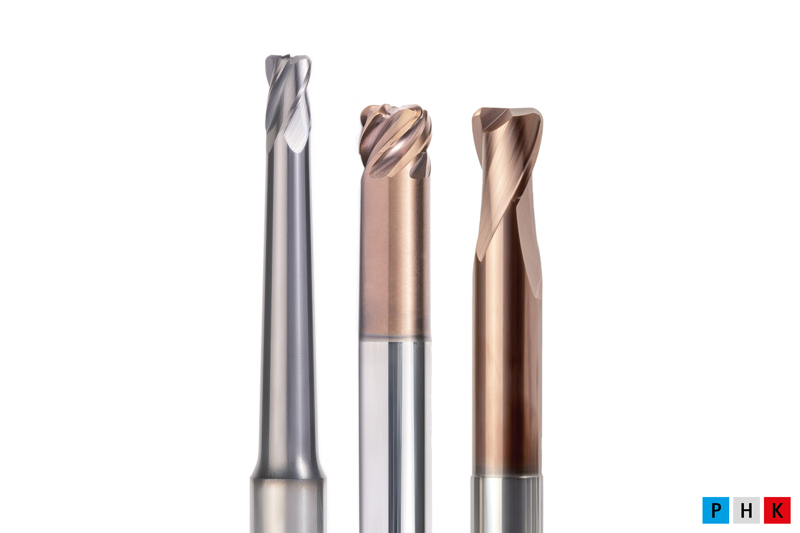
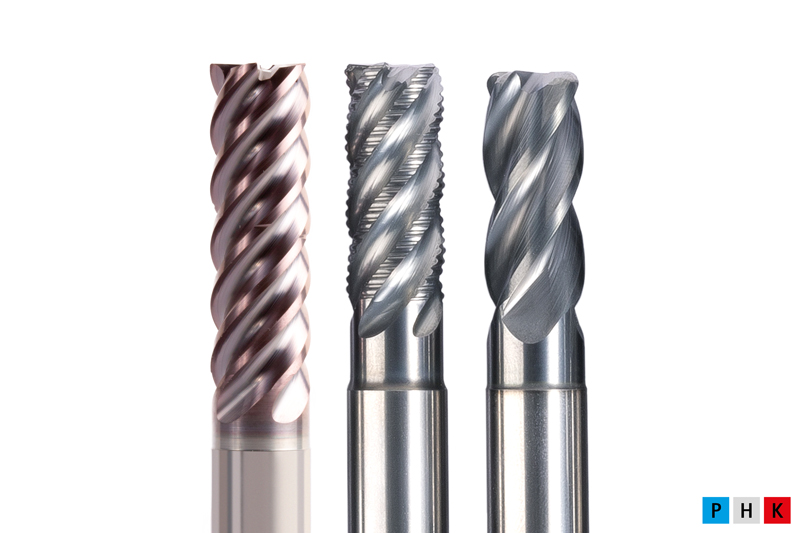
OptiMill Fresa de esquadrejamento
Fresa de esquadrejamento Ideal para desbaste, acabamento e fresamento trocoidal de bolsões Gama ø: 2,00 - 12,00 mm
OptiMill-3D-CS
Kreisradiusfräser
Schlichten von komplexen Freiformflächen und komplizierten Werkstückgeometrien ø-Bereich: 2,00 - 12,00 mm
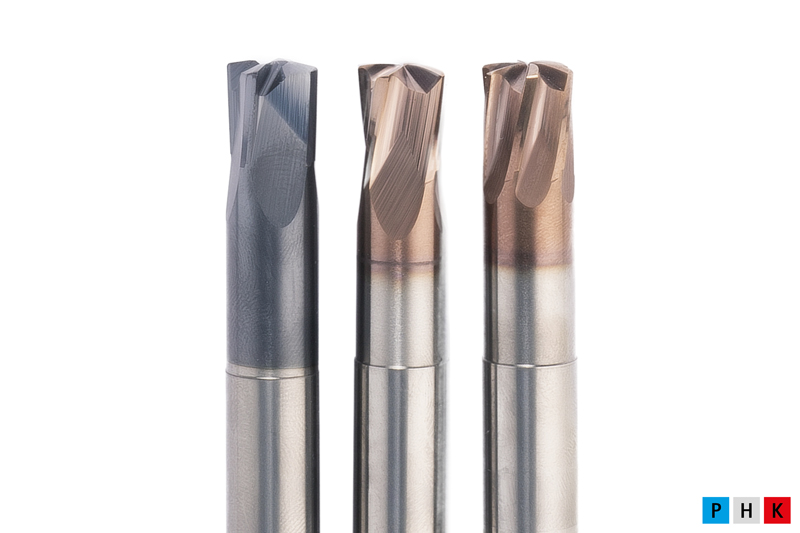
OptiMill-3D-HF
Fresas de alto avanço Ideal para usinagem de alto avanço com grande taxa de remoção do material e alta confiabilidade do processo Gama ø: 2,00 - 16,00 mm
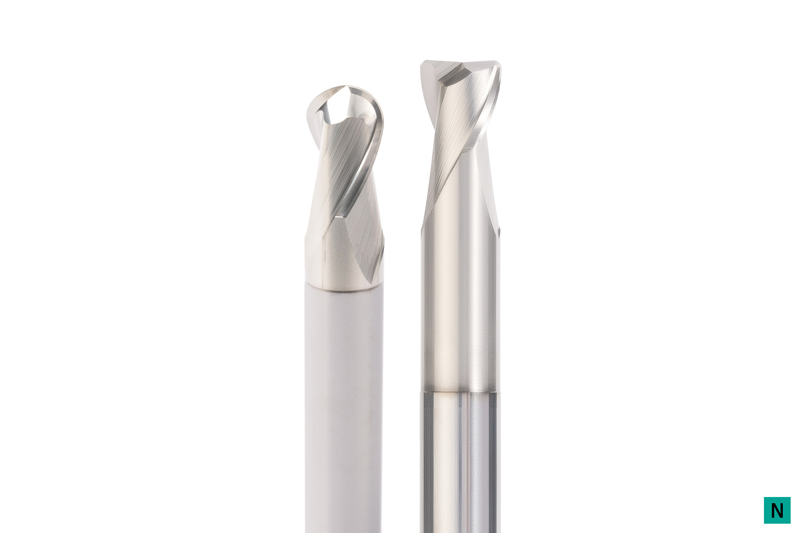
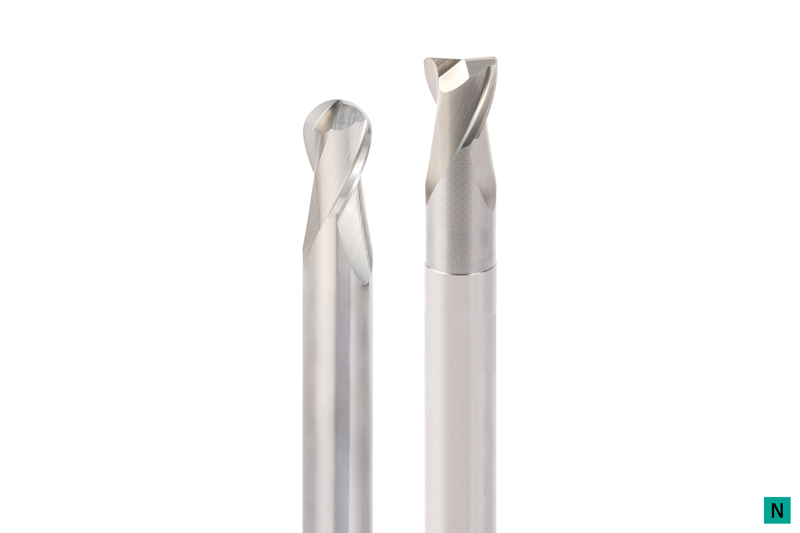
OptiMill-3D-Alu
Fresa esférica e fresa com raio de canto Usinagem de alta precisão de contornos 3D Gama ø: 1,00 - 20,00 mm
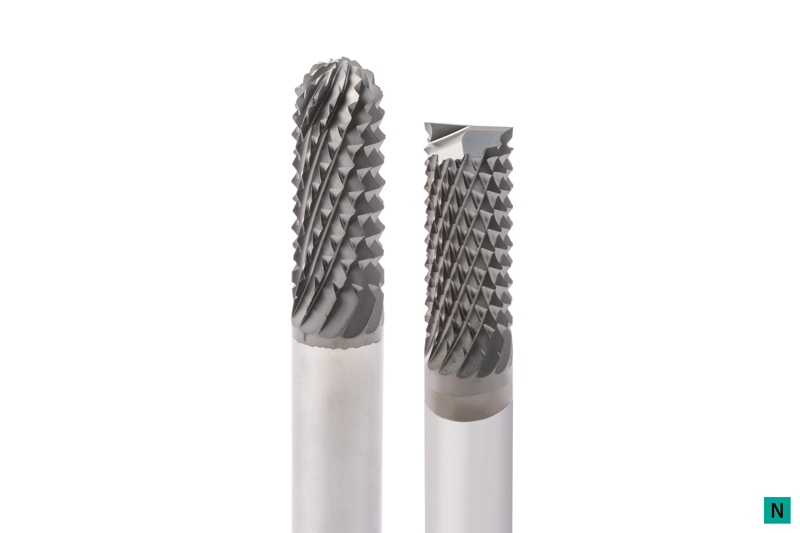
OptiMill-Graphite-MT
Fresa esférica e fresa de esquadrejamento Fresa multidente para desbaste eletrodos de grafite com altas taxas de remoção Gama ø: 3,00 - 16,00 mm
OptiMill-3D-Graphite
Fresa esférica e fresa com raio de canto Adequado para usinagem de eletrodos de grafite Projetos diferentes, dependendo da situação de usinagem Gama ø: 0,20 - 12,00 mm
OptiMill-3D-Copper
Fresa esférica e fresa com raio de canto Geometria especial para usinagem de elétrodos de cobre e ligas não ferrosas resistentes Gama ø: 0,10 - 20,00 mm
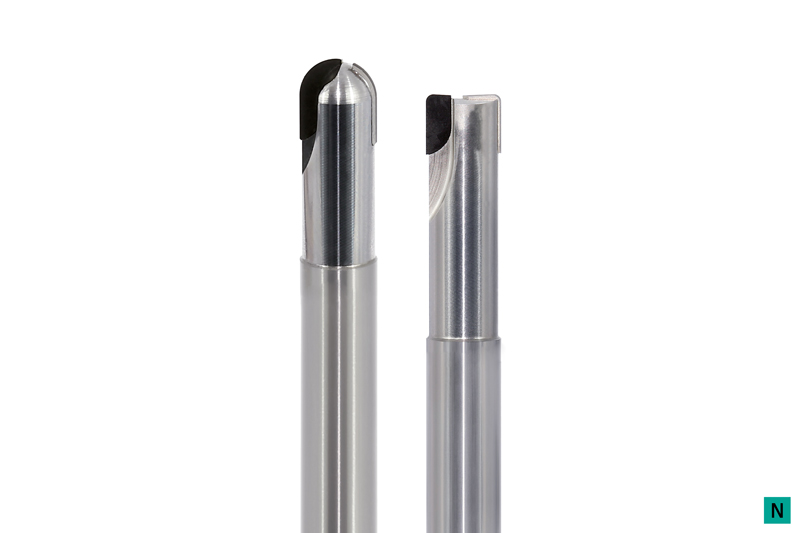
OptiMill-Diamond
Fresa esférica, fresa com raio de canto e fresa de esquadrejamento Lâminas de PCD para longa vida Gama ø: 3,00 - 12,00 mm
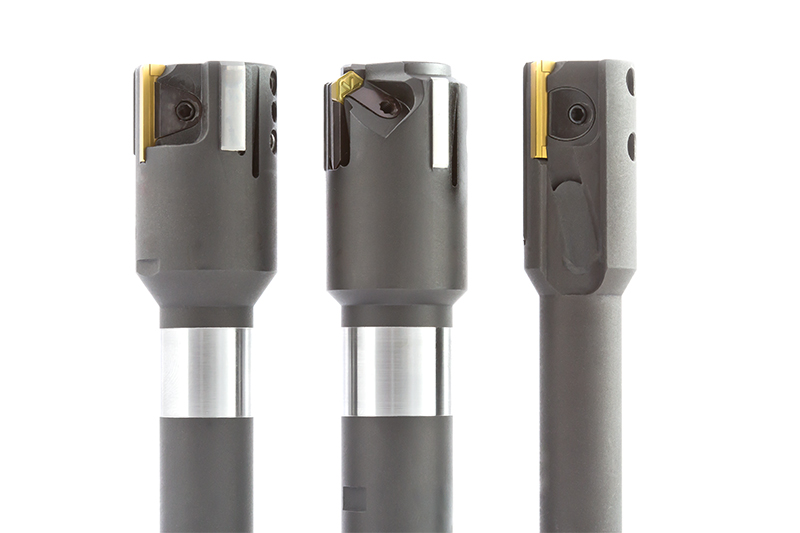
Fresas com insertos intercambiáveis
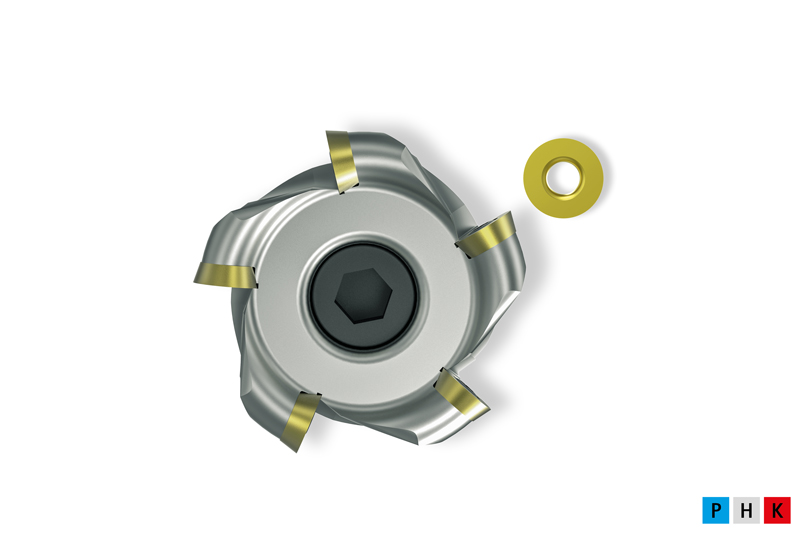
NeoMill-ISO-360
Milling cutter with round inserts Perfect for roughing and pre-finishing ø range: 10.00 - 160.00 mm
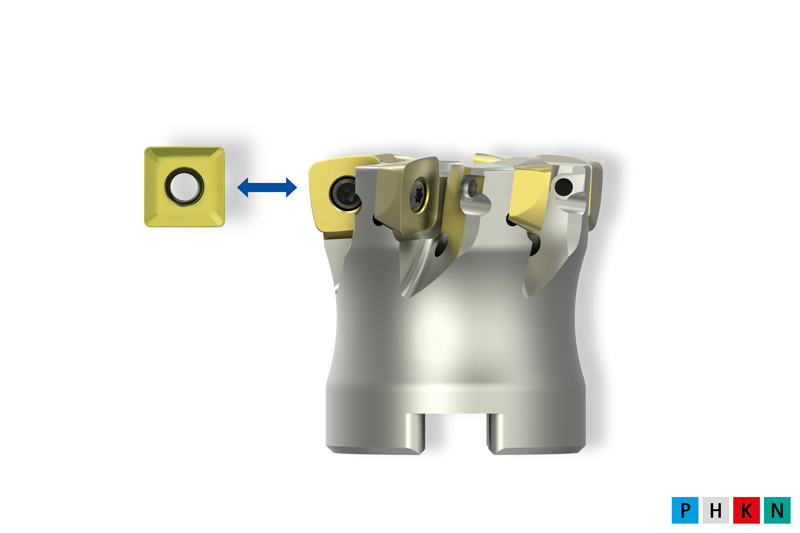
NeoMill-3D-Finish
Finishing milling cutter Perfect for finishing 90° surfaces, face surfaces and contours ø range: 16.00 - 42.00 mm
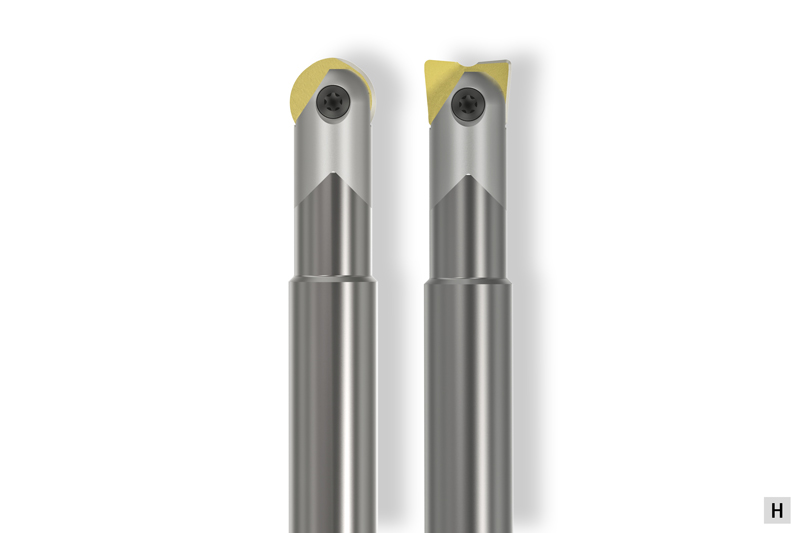
NeoMill-3D-Ballnose/-Torus
Ball nose and corner radius milling cutter One tool body with indexable insert for ball nose and corner radius milling for finishing and pre-finising ø range: 8.00 - 32.00 mm
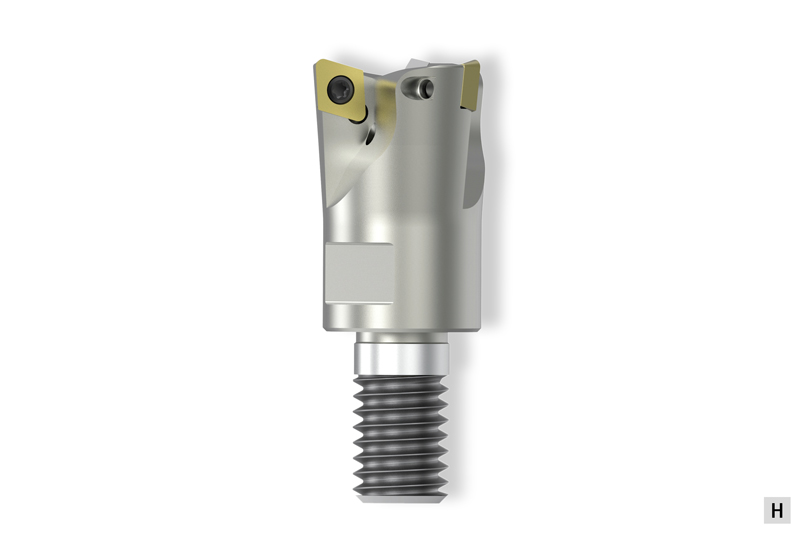
NeoMill-2/4-HiFeed90
High-feed/90° shoulder milling cutter Universal tool system to ensure maximum productivity ø range: 16.00 - 200.00 mm
Drilling | Countersinking
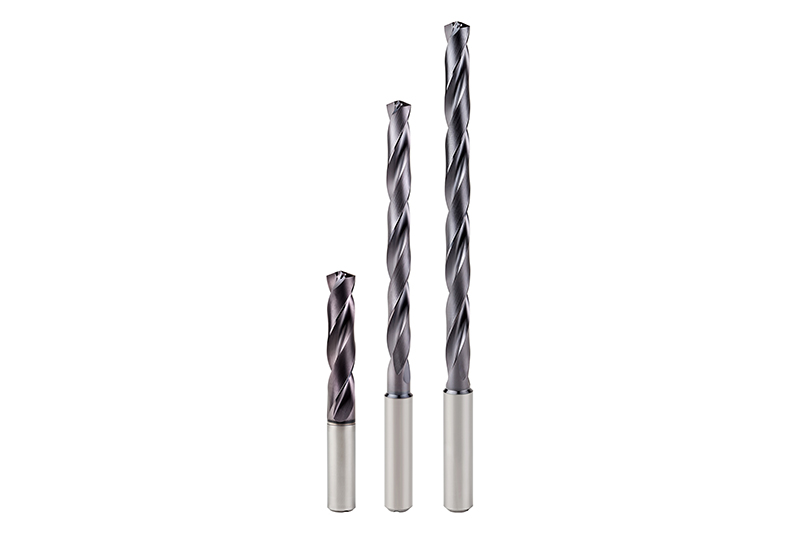
Wiertło ECU-Drill-Steel
Wiertła z węglika spiekanego
Wiertła dwuostrzowe o bardzo dobrym stosunku ceny do wydajności Szeroki zakres zastosowań Sprawdzone geometrie zapewniające wysoką precyzję i bezpieczeństwo procesu Zakres ø: 1,00–20,00 mm
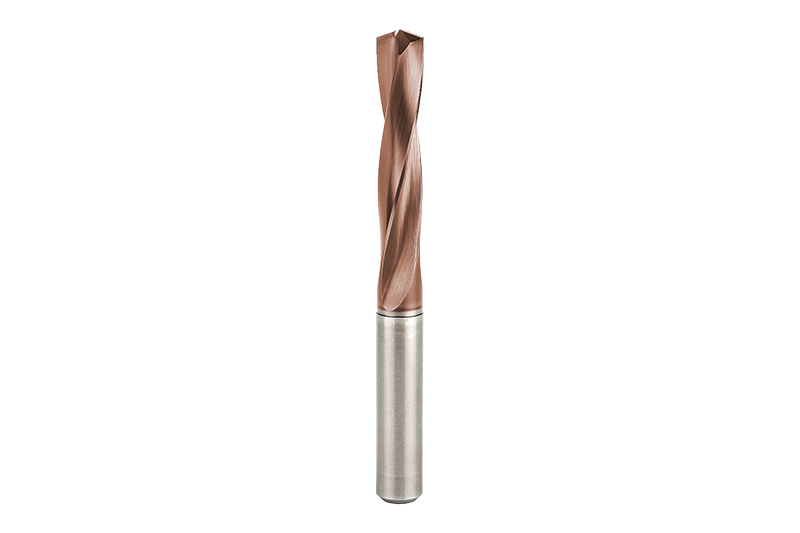
Wiertło MEGA hartowane
Wysokowydajne wiertła z węglika spiekanego
Wiertło dwuostrzowe z dopasowaną powłoką i geometrią do bezpiecznej obróbki materiałów hartowanych Nowa mikro- i makrogeometria zakres ø: 2,55–16,00 mm
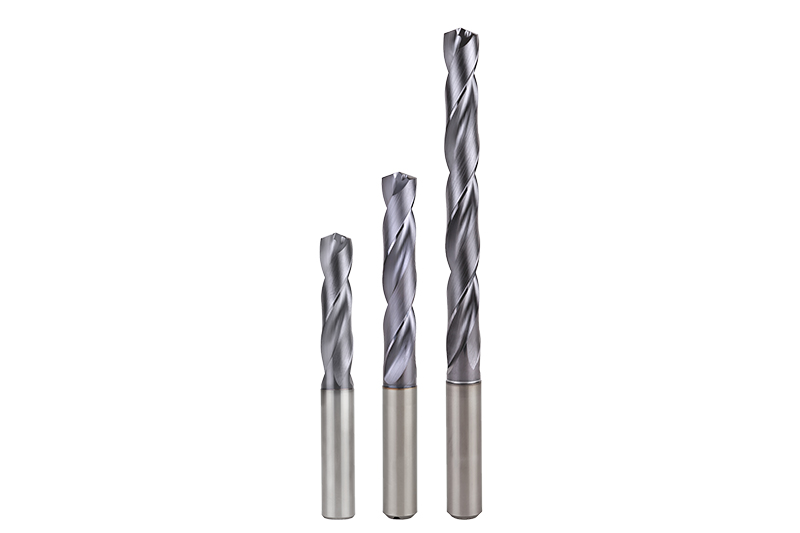
Wiertło MEGA-Drill-Steel-Plus
Wysokowydajne wiertła z węglika spiekanego
Wiertła dwuostrzowe z dostosowaną powłoką i geometrią do obróbki stali Zoptymalizowana geometria rowków i zmodyfikowane przygotowanie krawędzi skrawających Zakres ø: 3,00–25,00 mm
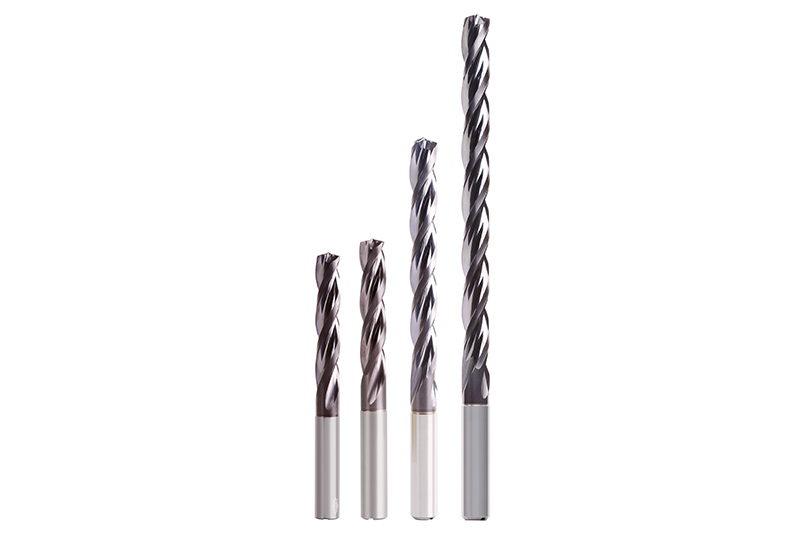
Wiertło Tritan-Drill-Steel
Wiertło z węglika spiekanego trójostrzowe
Wiertło z węglika spiekanego trójostrzowe do najwyższego posuwu Samocentrujące ostrze poprzeczne do trudnych sytuacji wiercenia Specjalnie dostosowane do obróbki stali Zakres ø: 4,00–20,00 mm
Wiertło Tritan-Spot-Drill-Steel
Wiertło z trzema ostrzami Wiertło z trzema ostrzami do wymagających sytuacji nawiercania Specjalnie dostosowane do wierteł z trzema ostrzami Zakres ø: 4,00 - 20,00 mm
Wiertło stopniowe Tritan
Wiertło stopniowe trójostrzowe Wiertło stopniowe trójostrzowe z samocentrującym ścinem Obróbka otworów z gwintem wewnętrznym bez ruchu oscylującego Zakres ø: 4,25 - 14,15 mm
Wiertło MEGA-Deep-Drill
Wiertła głębokie Niezawodna i wydajna obróbka głębokich otworów do 40xD Wiertło pilotowe MEGA-Pilot-Drill Zakres ø: 1,00 - 16,00 mm
MEGA-Drill-Reamer
Wiertło-rozwiertak do rozwiercania Dwie operacje – wiercenie i rozwiercanie – w jednym narzędziu Zoptymalizowane ostrze rozwiercające Skrócenie czasów głównej i dodatkowej obróbki Tolerancja otworu ≥ IT7 Zakres ø: 4,00–16,00 mm
Precyzyjne wiertło stożkowe
Precyzyjne wiertło stożkowe z nierównomiernym podziałem
Niezwykle nierównomierny podział ostrzy Wyższa dokładność i lepsze właściwości powierzchni Zmniejszone siły osiowe i promieniowe Znacznie mniej wibracji Zwiększone parametry skrawania dla najwyższej wydajności Zakres ø: 4,30–31,00 mm
Wiertło MEGA-Drill-Reamer-Pyramid
Wiertło-rozwiertak z końcówką piramidalną Nawiercanie, wiercenie i rozwiercanie jednym narzędziem Ulepszone właściwości centrowania dzięki końcówce piramidalnej Skrócenie czasu operacji głównych i dodatkowych Tolerancja otworu ≥ IT7 zakres ø: 4,00 – 16,00 mm
Wiertło z płytką skrawającą QTD
Wiercenie w pełnym materiale z systemem wymiennych głowic
Ekonomiczny system z wymiennymi płytkami skrawającymi System mocowania siłowego i kształtowego Łatwa obsługa Wysoka dokładność koncentryczności Zakres ø: 8,10–49,00 mm
Rozwiercanie
FixReam – FXR
Wysokowydajne wytrychowce z węglika spiekanego Proste rowki do otworów przelotowych i podstawowych Lewoskrętne rowki do otworów przelotowych zakres ø: 3,00–20,00 mm
CPReam – CPR
交换式铣头铰刀
锥面和平接触面带来最高的稳定性和刚性 5 µm 的高度径向跳动精度 简易的操作方式 ø-范围:8.00 - 40.00 mm
快速调节铰刀 – WN 50
手用铰刀
可调范围大的快调铰刀 特别适合维修工作 可提供备用刀刃组 ø-范围:6.40 - 95.00 mm
导杆刀具
带有导向板的刀具
采用MAPAL公司原理的最高准确度 通过导向板实现在孔中的直接导向 经精密磨削的可转位刀片 用于µm精确度孔加工的高精度校准
夹紧
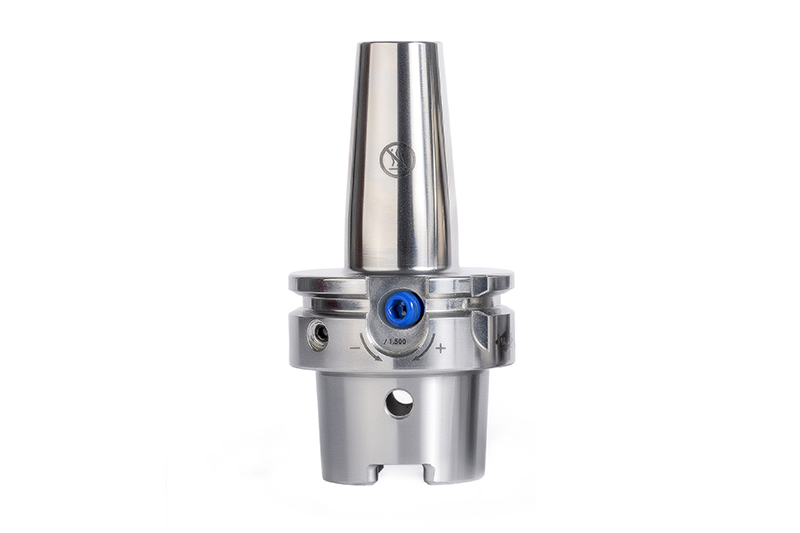
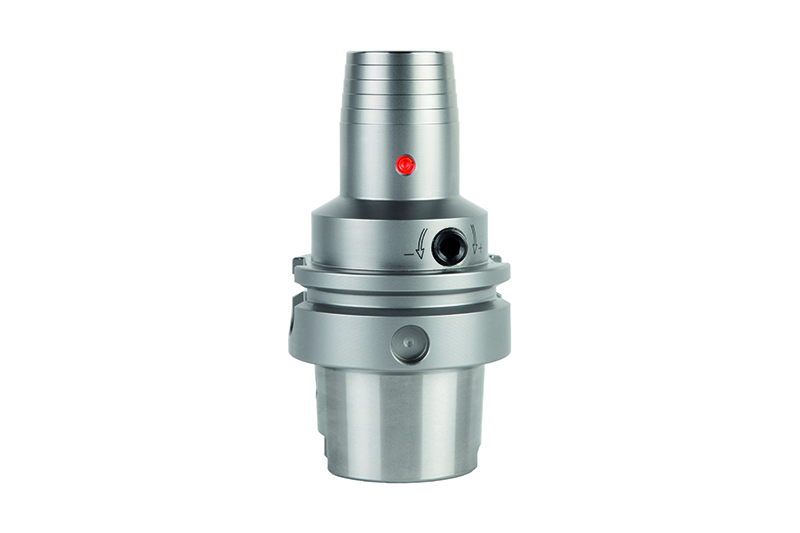
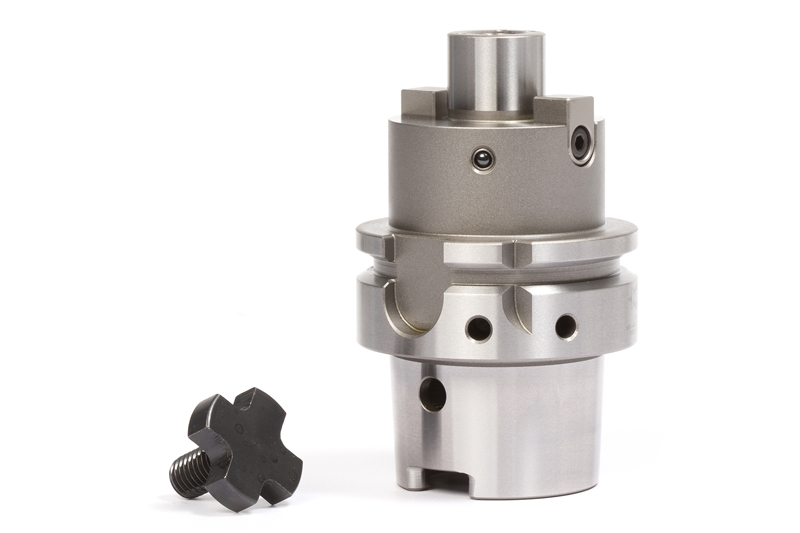
UNIQ DReaM Chuck, 4.5°
Hydraulic chucks with a new design
For reaming and drilling applications as well as for finishing during milling operations This is achieved through an optimal interplay of geometric and functional properties Outstanding surfaces as well as improved handling Increasing productivity during the machining of contour-critical parts To the shop
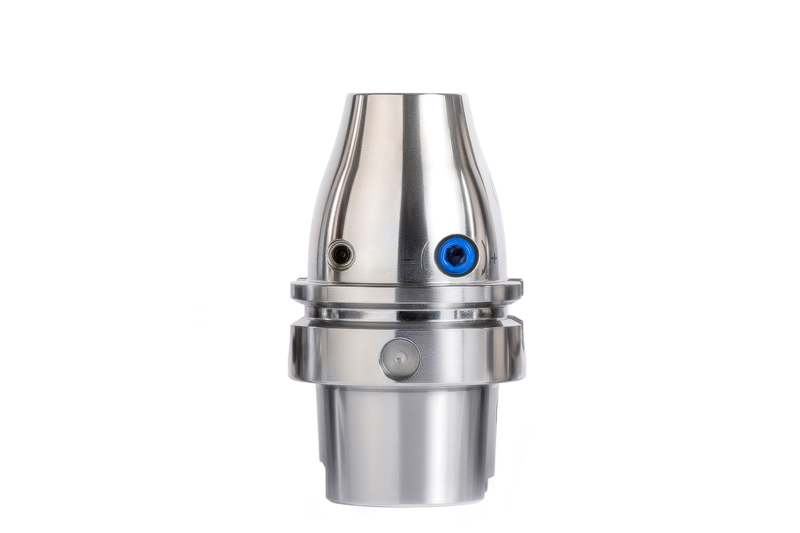
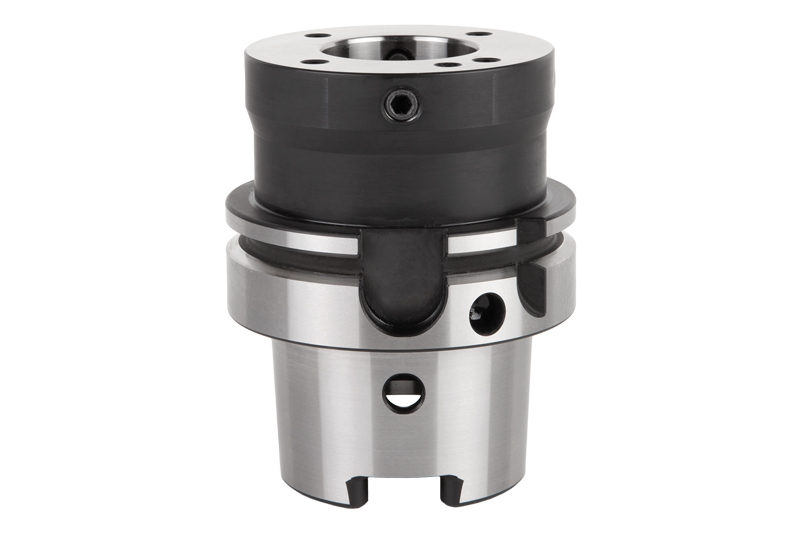
UNIQ Mill Chuck, HA
Hydraulic chucks with a new design
Hydraulic chuck for highly dynamic milling applications This is achieved through an optimal interplay of geometric and functional properties Excellent results when using tools with HA shanks Process reliability – even on high-quality parts To the shop
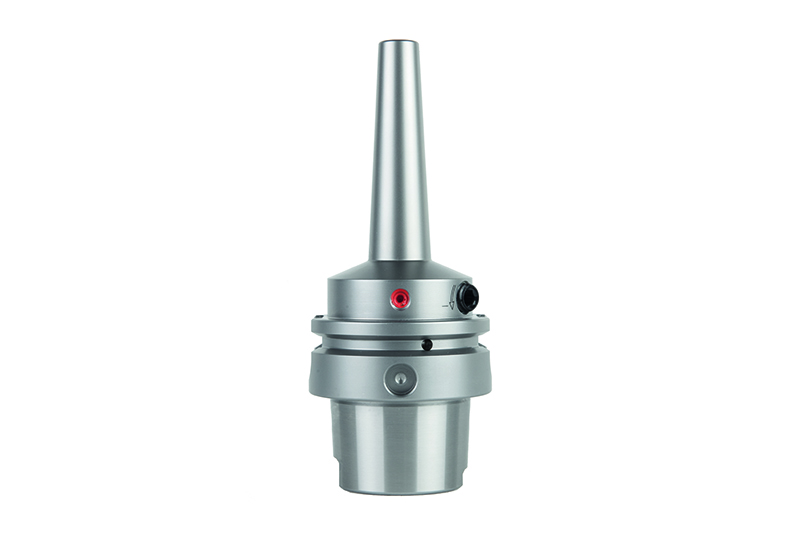
HighTorque Chuck HTC
Hydraulic chuck
High level of torque transmission Ideal damping properties Excellent rigidity of the entire system Radial run-out accuracy < 3 μm 3° slim design for use in contour-critical applications To the shop
HydroChuck MHC
Hydraulic chuck
Excellent vibration dampening High degree of radial run-out accuracy Ultra-short and compact design for high rigidity To the shop
ThermoChuck MTC
Shrink chuck
Long tool life through the use of high-temperature tool steel High torque transmission and radial rigidity Precision balanced as standard MQL-suitable With and without axial tool length adjustment To the shop
Mill Chuck, System HB
Side lock chuck
Easy to handle thanks to use of a differential screw Maximum cost-effectiveness and precision Axial tool positioning can be defined using spring system Decentralised coolant outlets for maximum process reliability To the shop
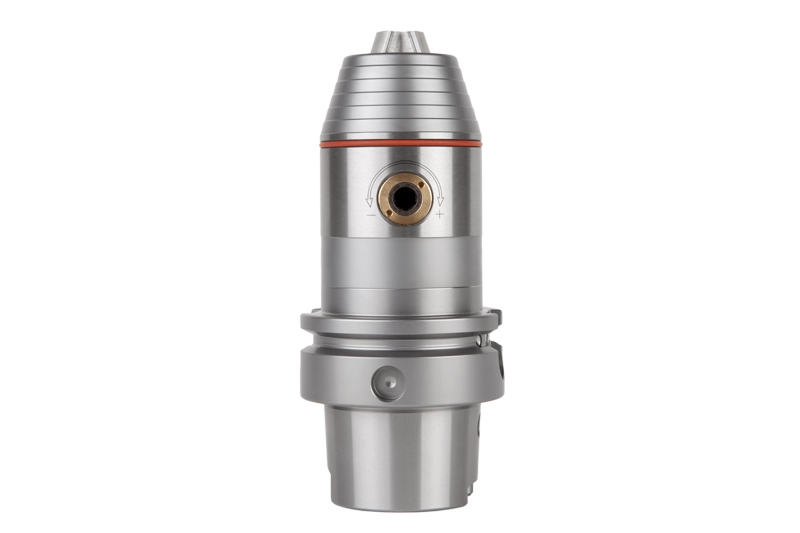
Precision-DrillChuck – MPC
Precision drill chuck
Simple construction, straightforward to handle Safe clamping independent of direction of rotation High degree of spindle speed strength Modular design allows drill chuck heads to be used with all tool connections
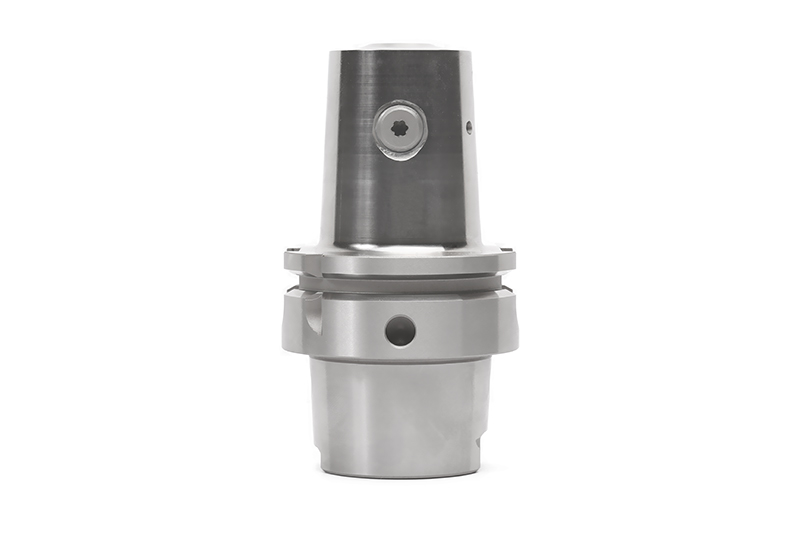
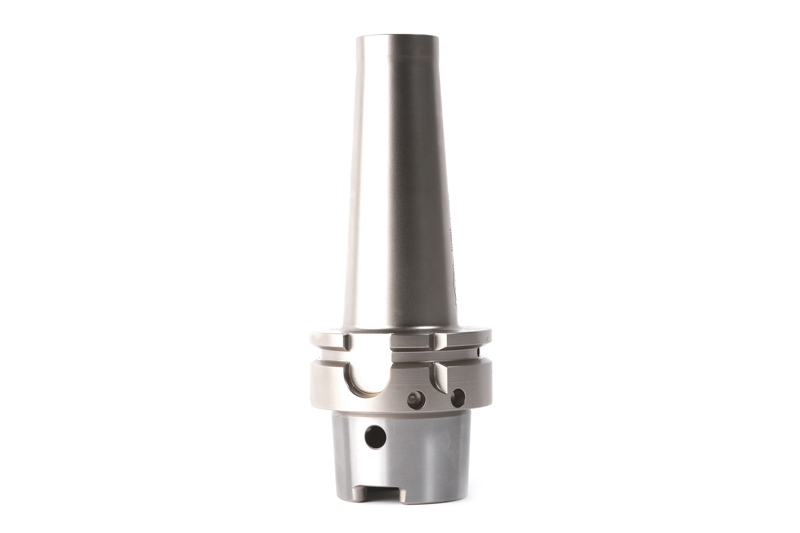
Milling cutter arbor – MDA / MCA
Milling cutter arbor
Vibration-cancelling design (MDA) with vibration dampening system Adapted to the rigidity of all common machine types Smooth, stable running despite long projections delivers better surface finish Milling cutter arbor (MCA) with large face connection for roughing and pre-finishing operations in large diameter ranges
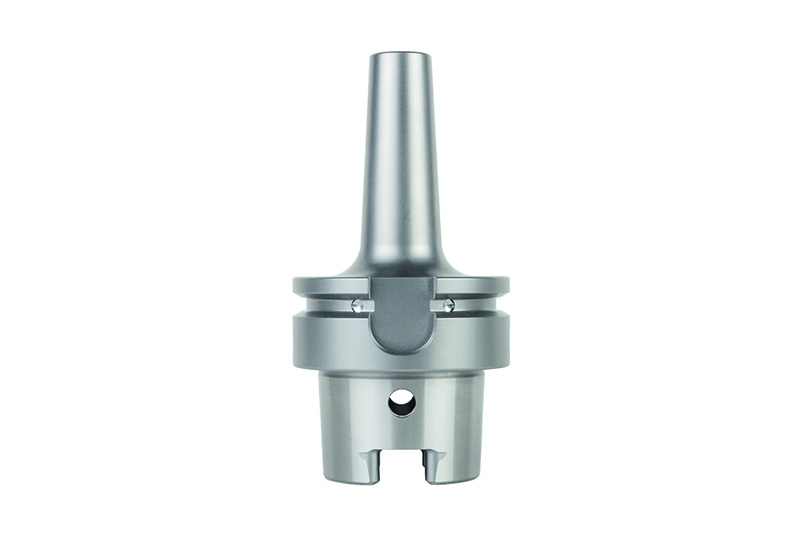
MFS milling head holder
Tool adapter for screw-in milling cutter
Simple and fast clamping of screw-in milling cutters Exact interaction of taper and face connection Greatest possible stability and rigidity Universally deployable for roughing and finishing operations
Adapter
Extensions, reducers and adapters
Wide range of options for modular tool systems Hydraulic extensions and tool extensions for thermal expanding chucks HSK reducers and extensions KS steep taper adapter To the shop
Components and workpiece material
Steel and hardened steel
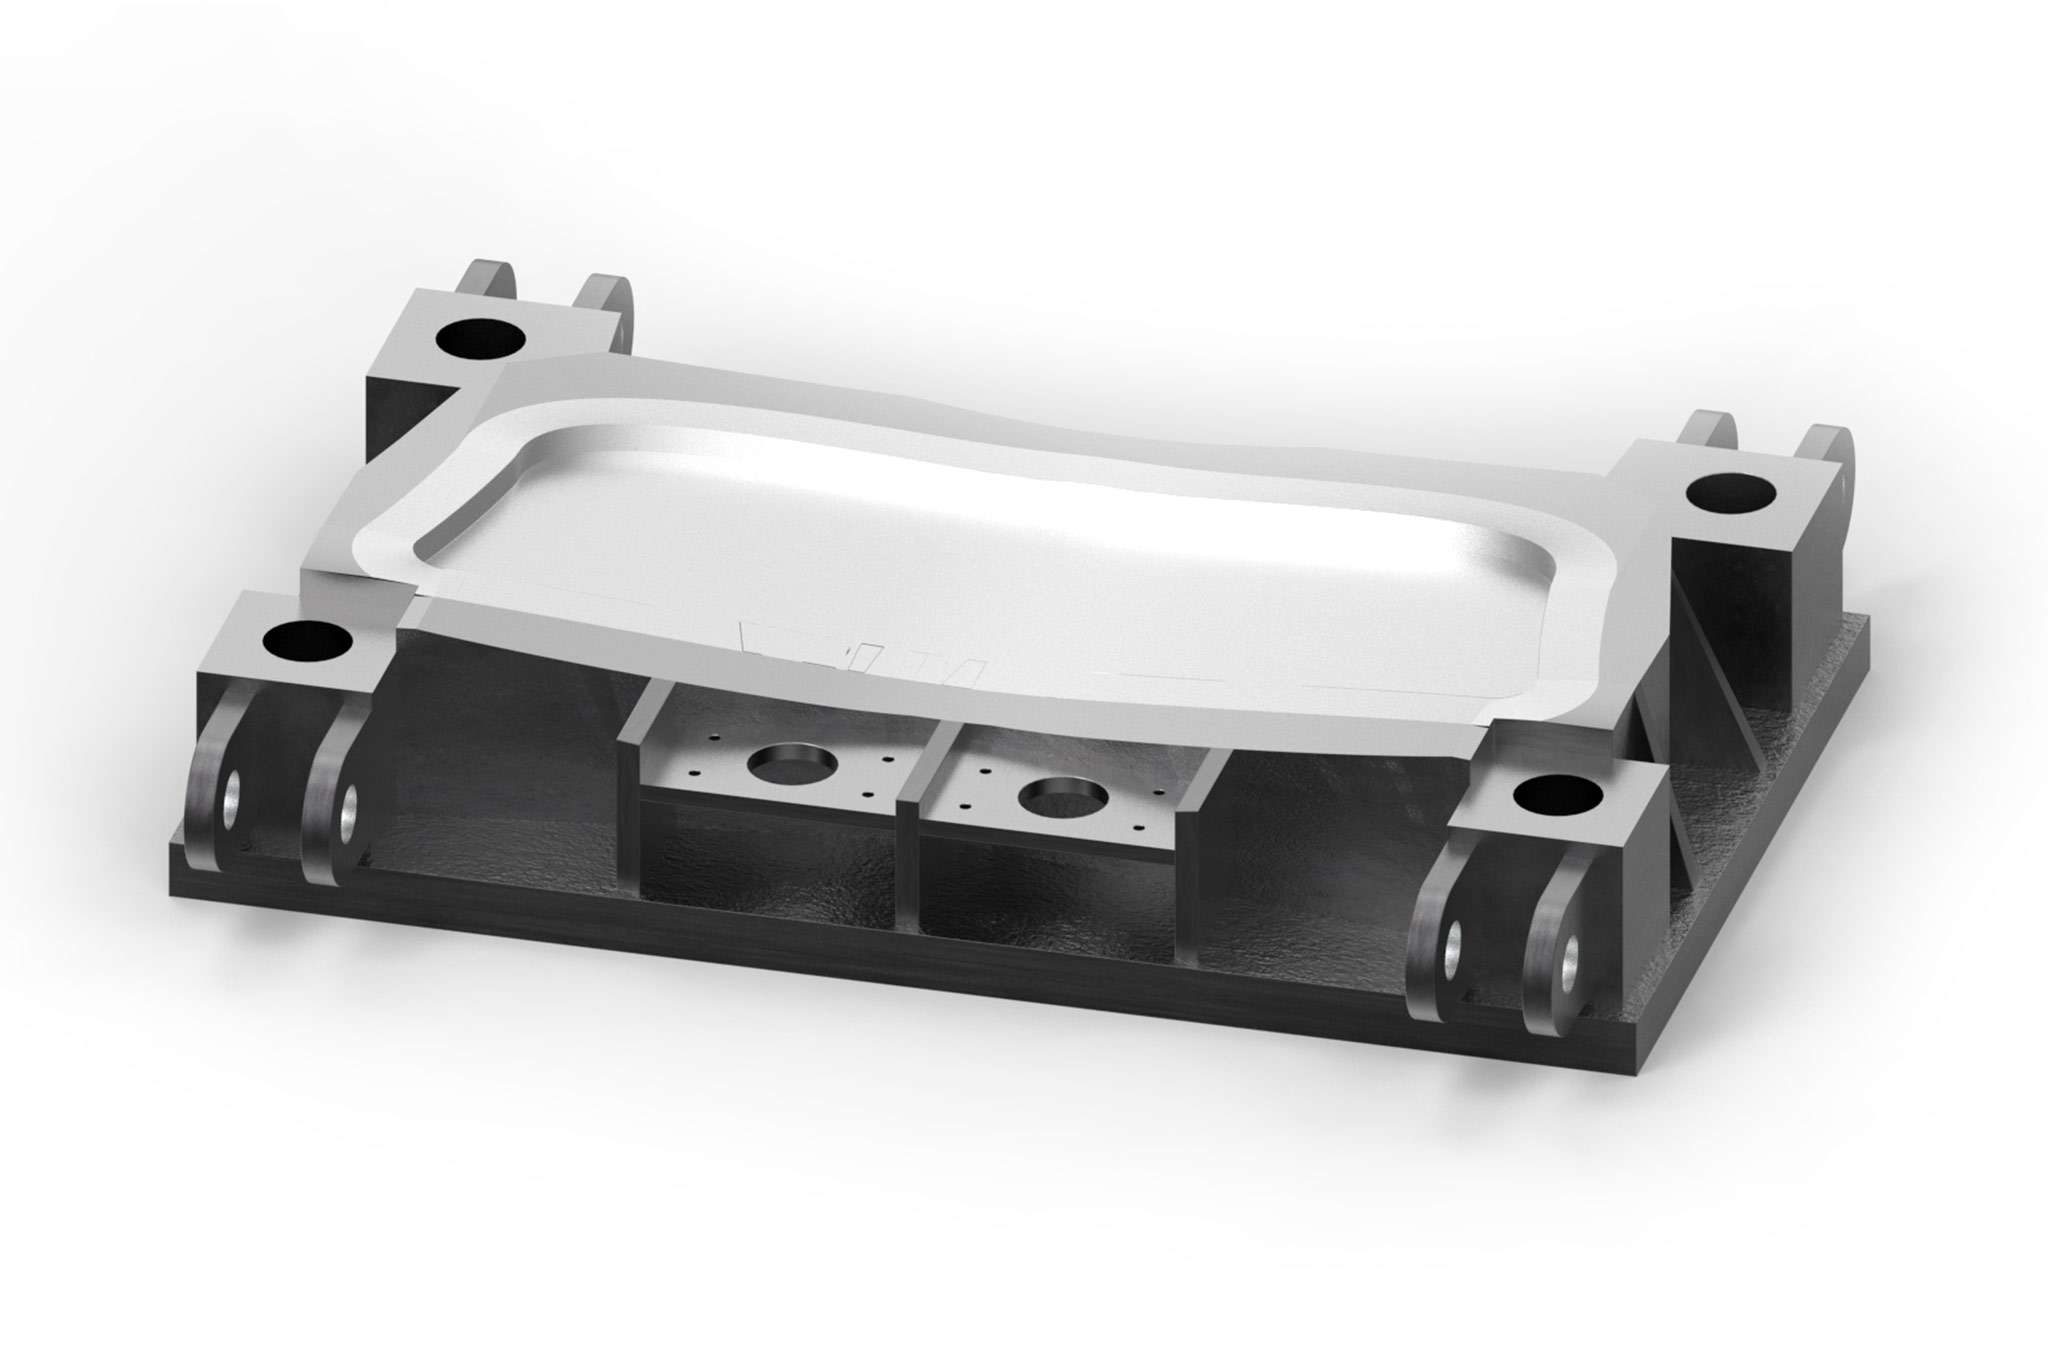
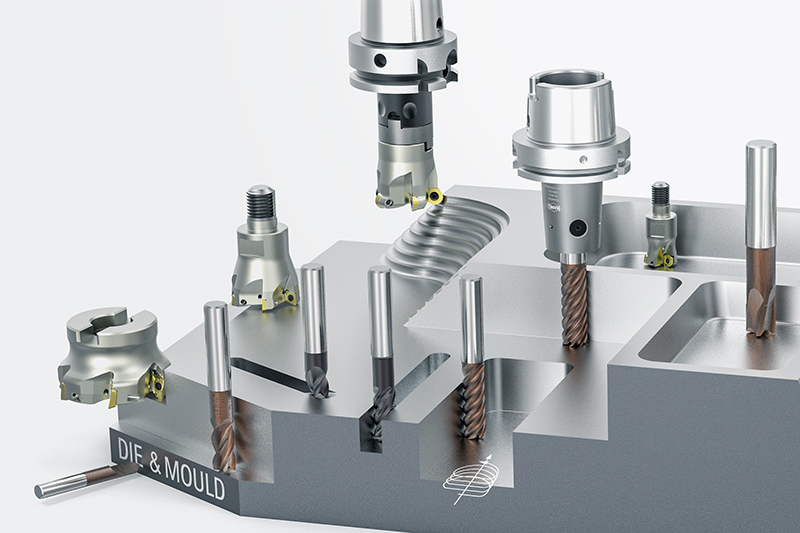
Parts that become more and more complex with increasingly deep cavities as well as moulded and reinforcement ribs in plastic injection moulds and pressure die casting moulds necessitate the use of extra long tools with diameters that can be very small. Complex part geometries and various material characteristics place the highest demands on machining and tool life.
Application examples: Plastic injection mould Pressure die casting mould
Cast iron
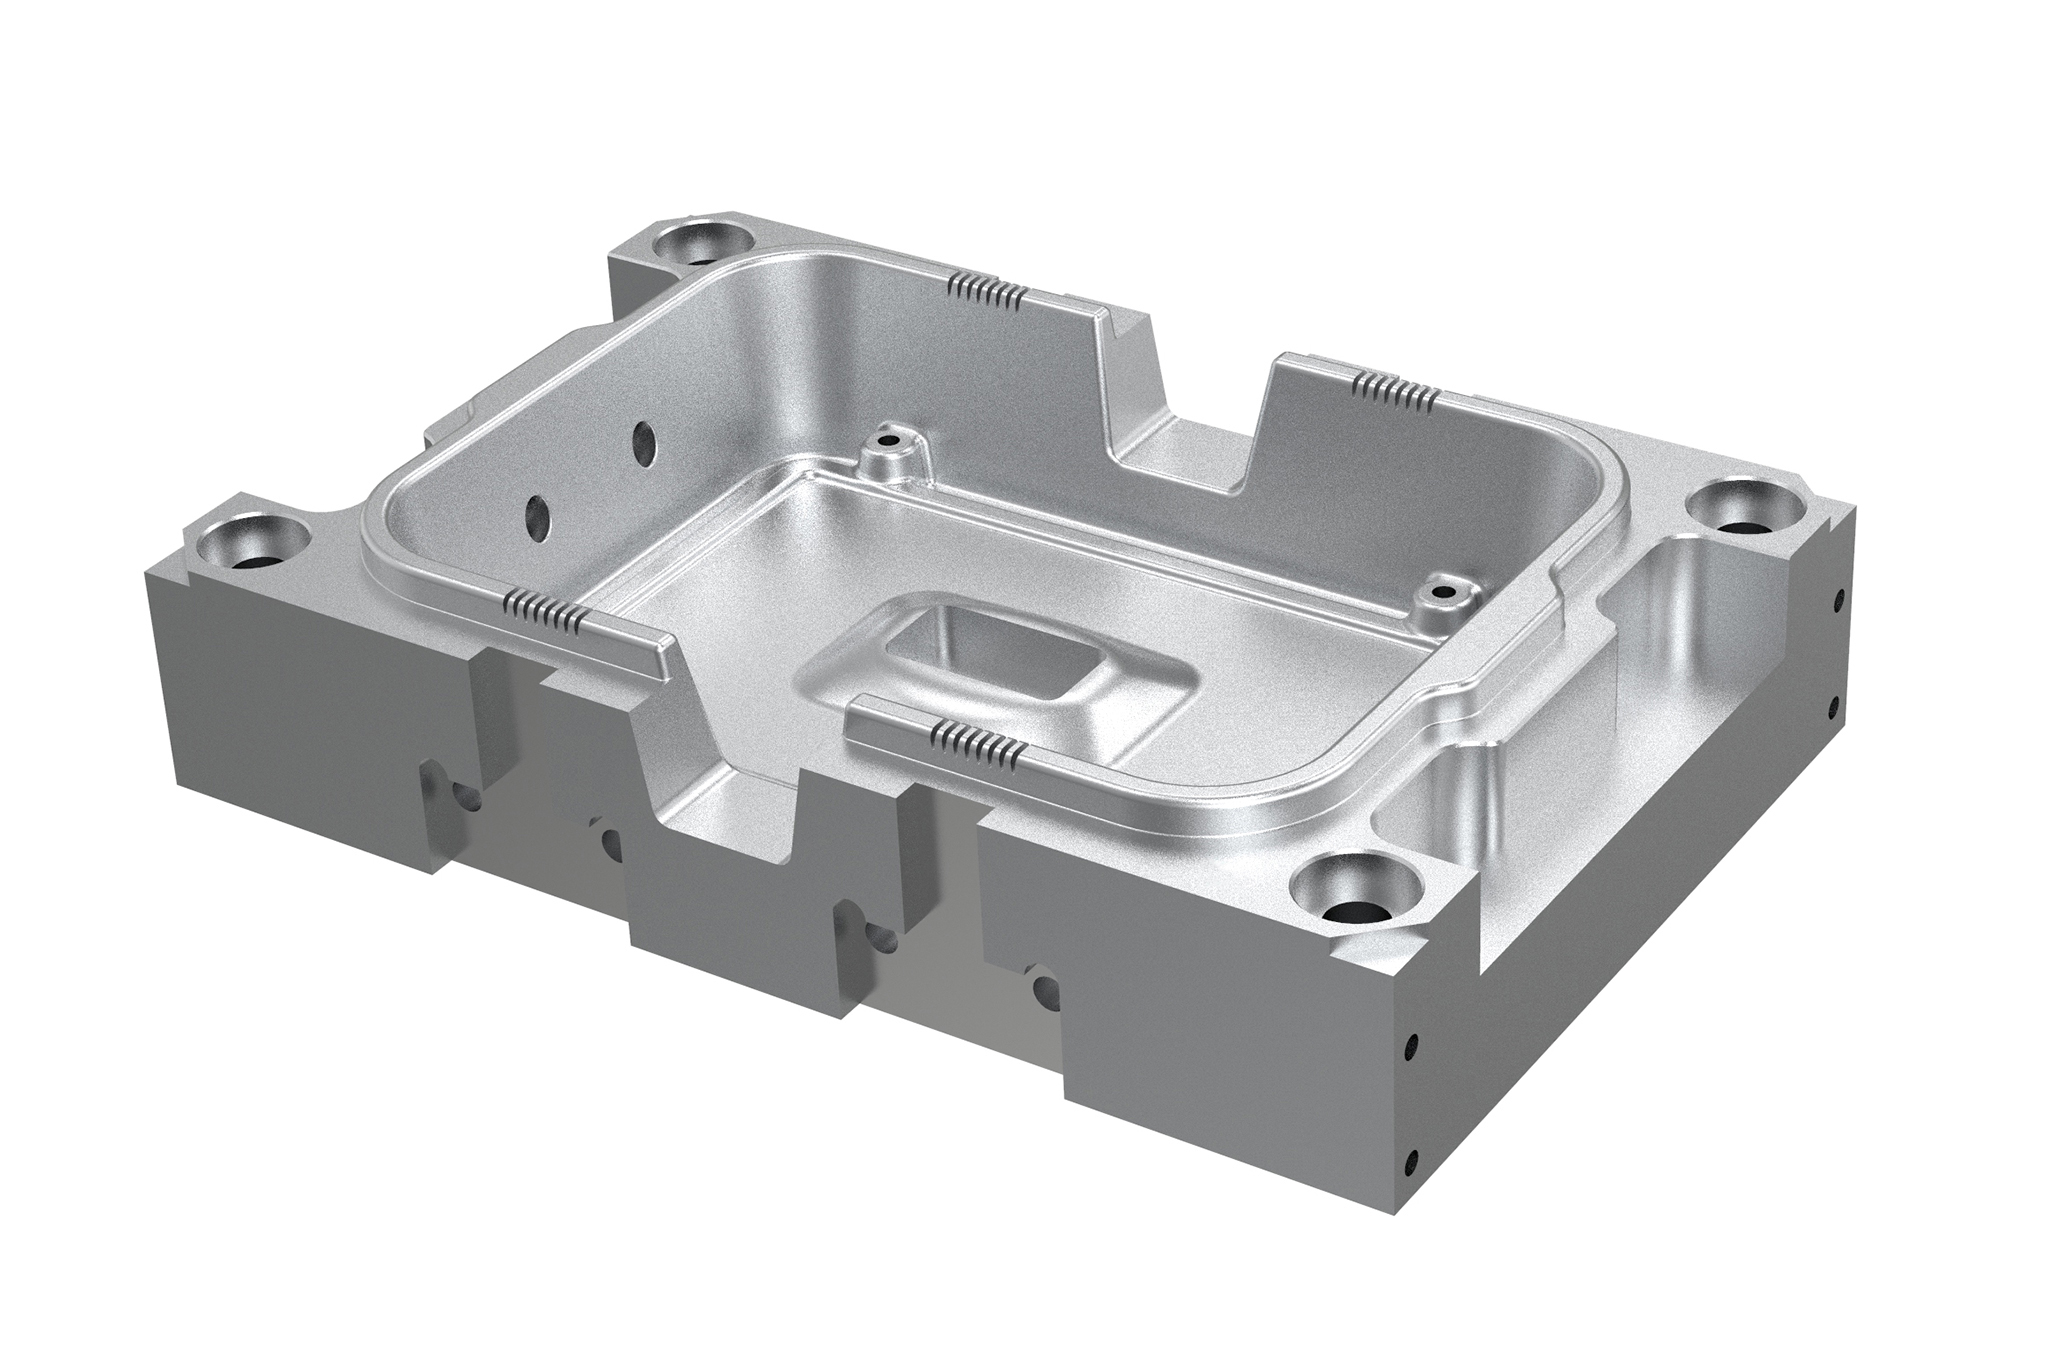
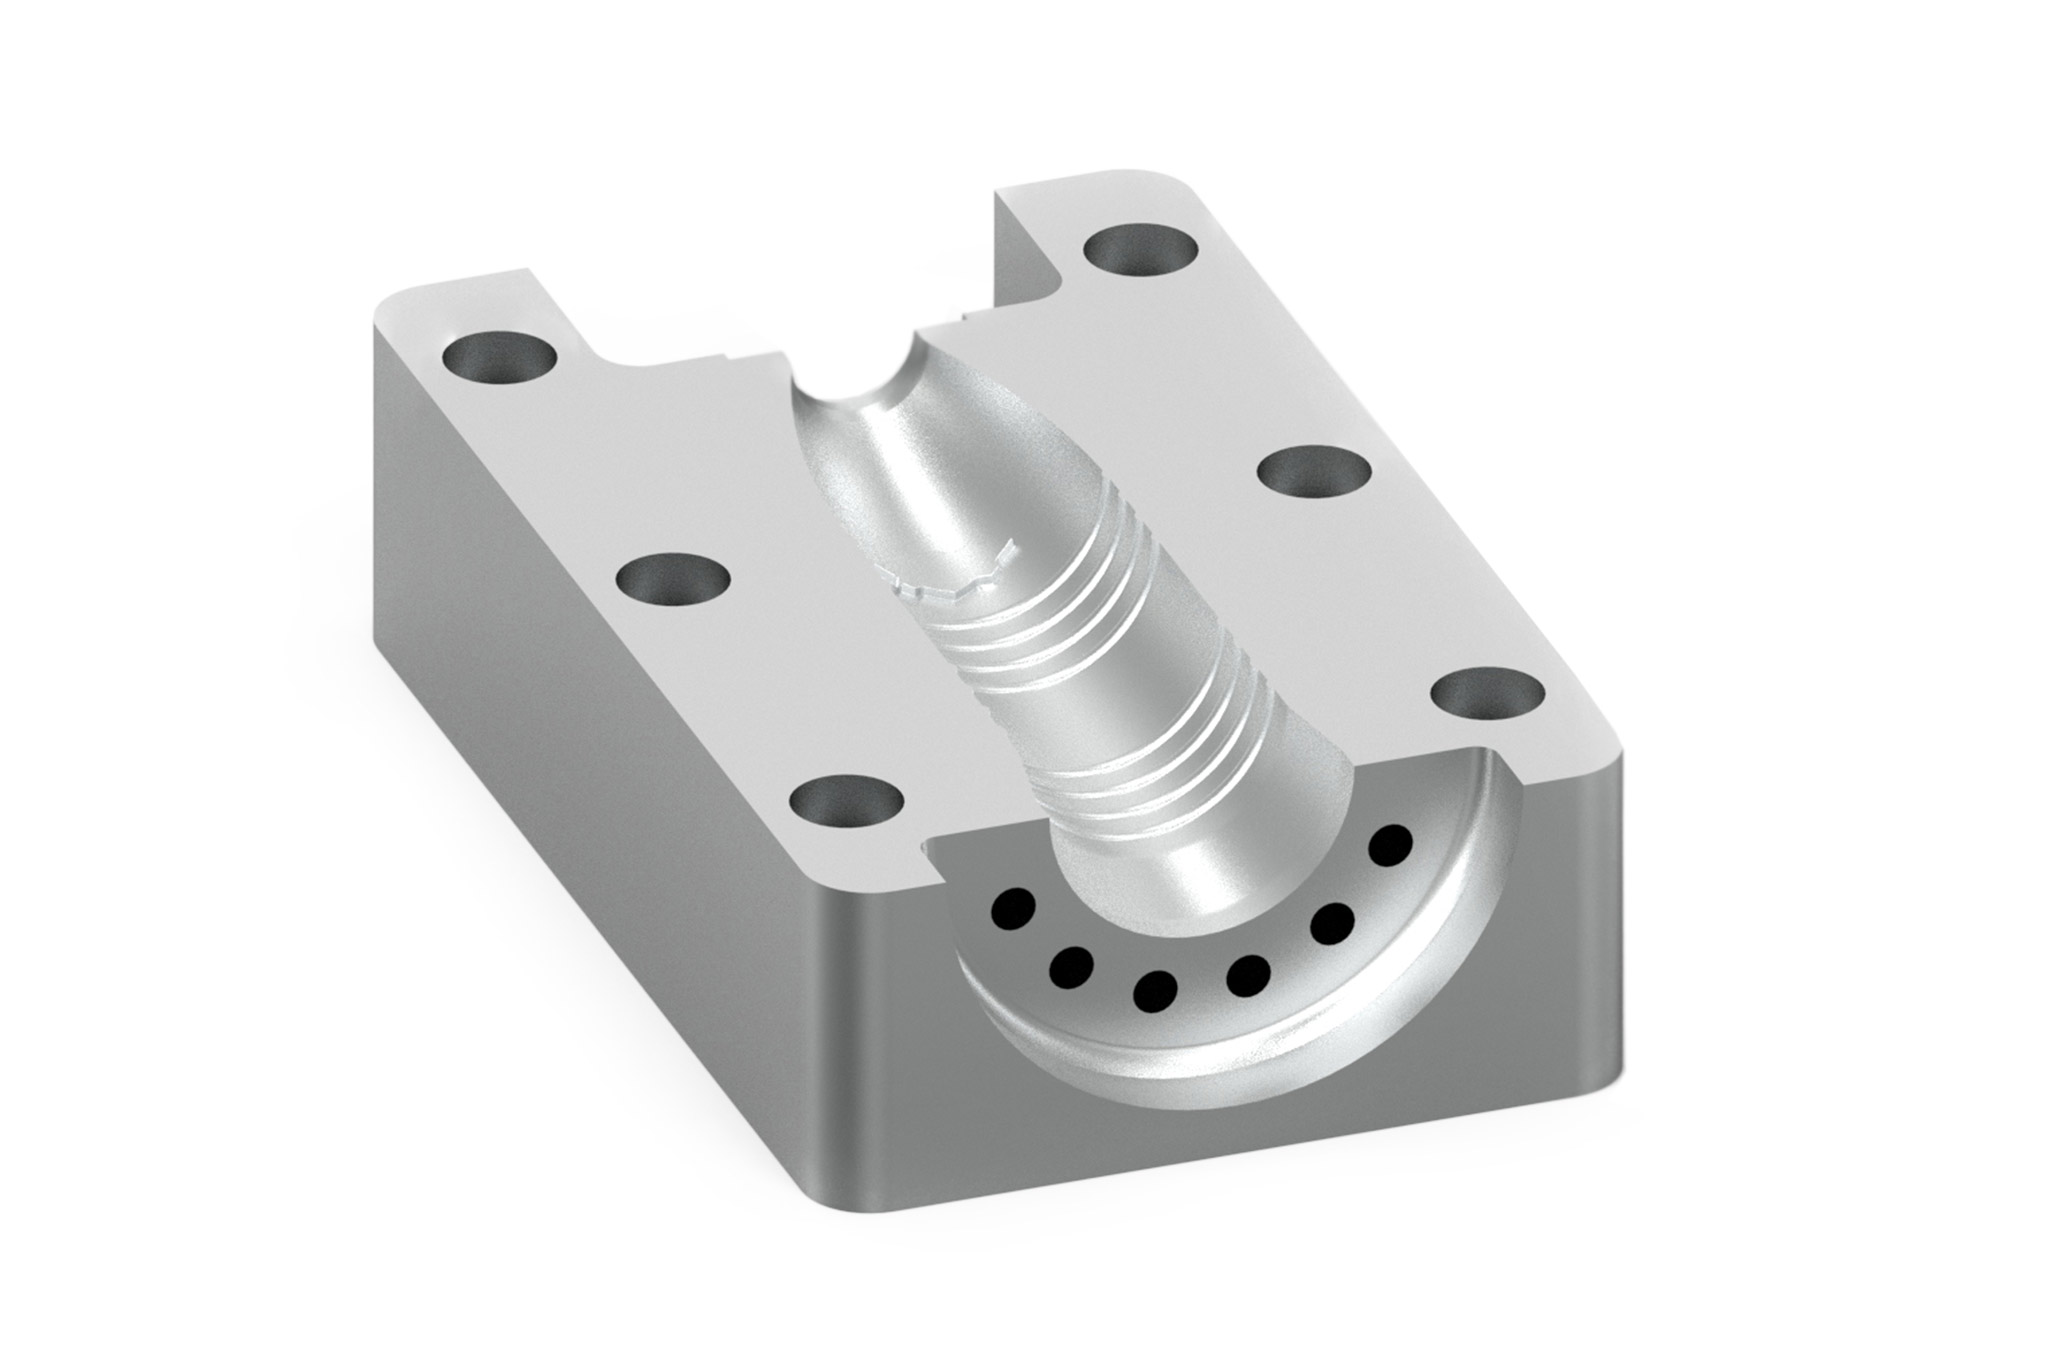
For designing, engineering and constructing medium- and large-sized cold forming tools, cast iron is often used due to material properties such as compressive strength and easy machinability. The main components here are mould plates and mould inserts. Here, MAPAL has a lot of experience with milling (2D and 3D) and drilling operations (drilling, reaming, thread cutting).
Application examples: Mould plates Mould inserts
Aluminium
When it comes to pre-series or prototype moulds, it is not unusual to use materials that are easy to machine. Aluminium alloys or uriol (plastics) are often used. In these cases, solid carbide tools with positive and partly polished cutting edges, or better still, PCD-tipped tools ensure high productivity and short machining times.
Application examples: Pre-series moulds Prototype moulds
Copper
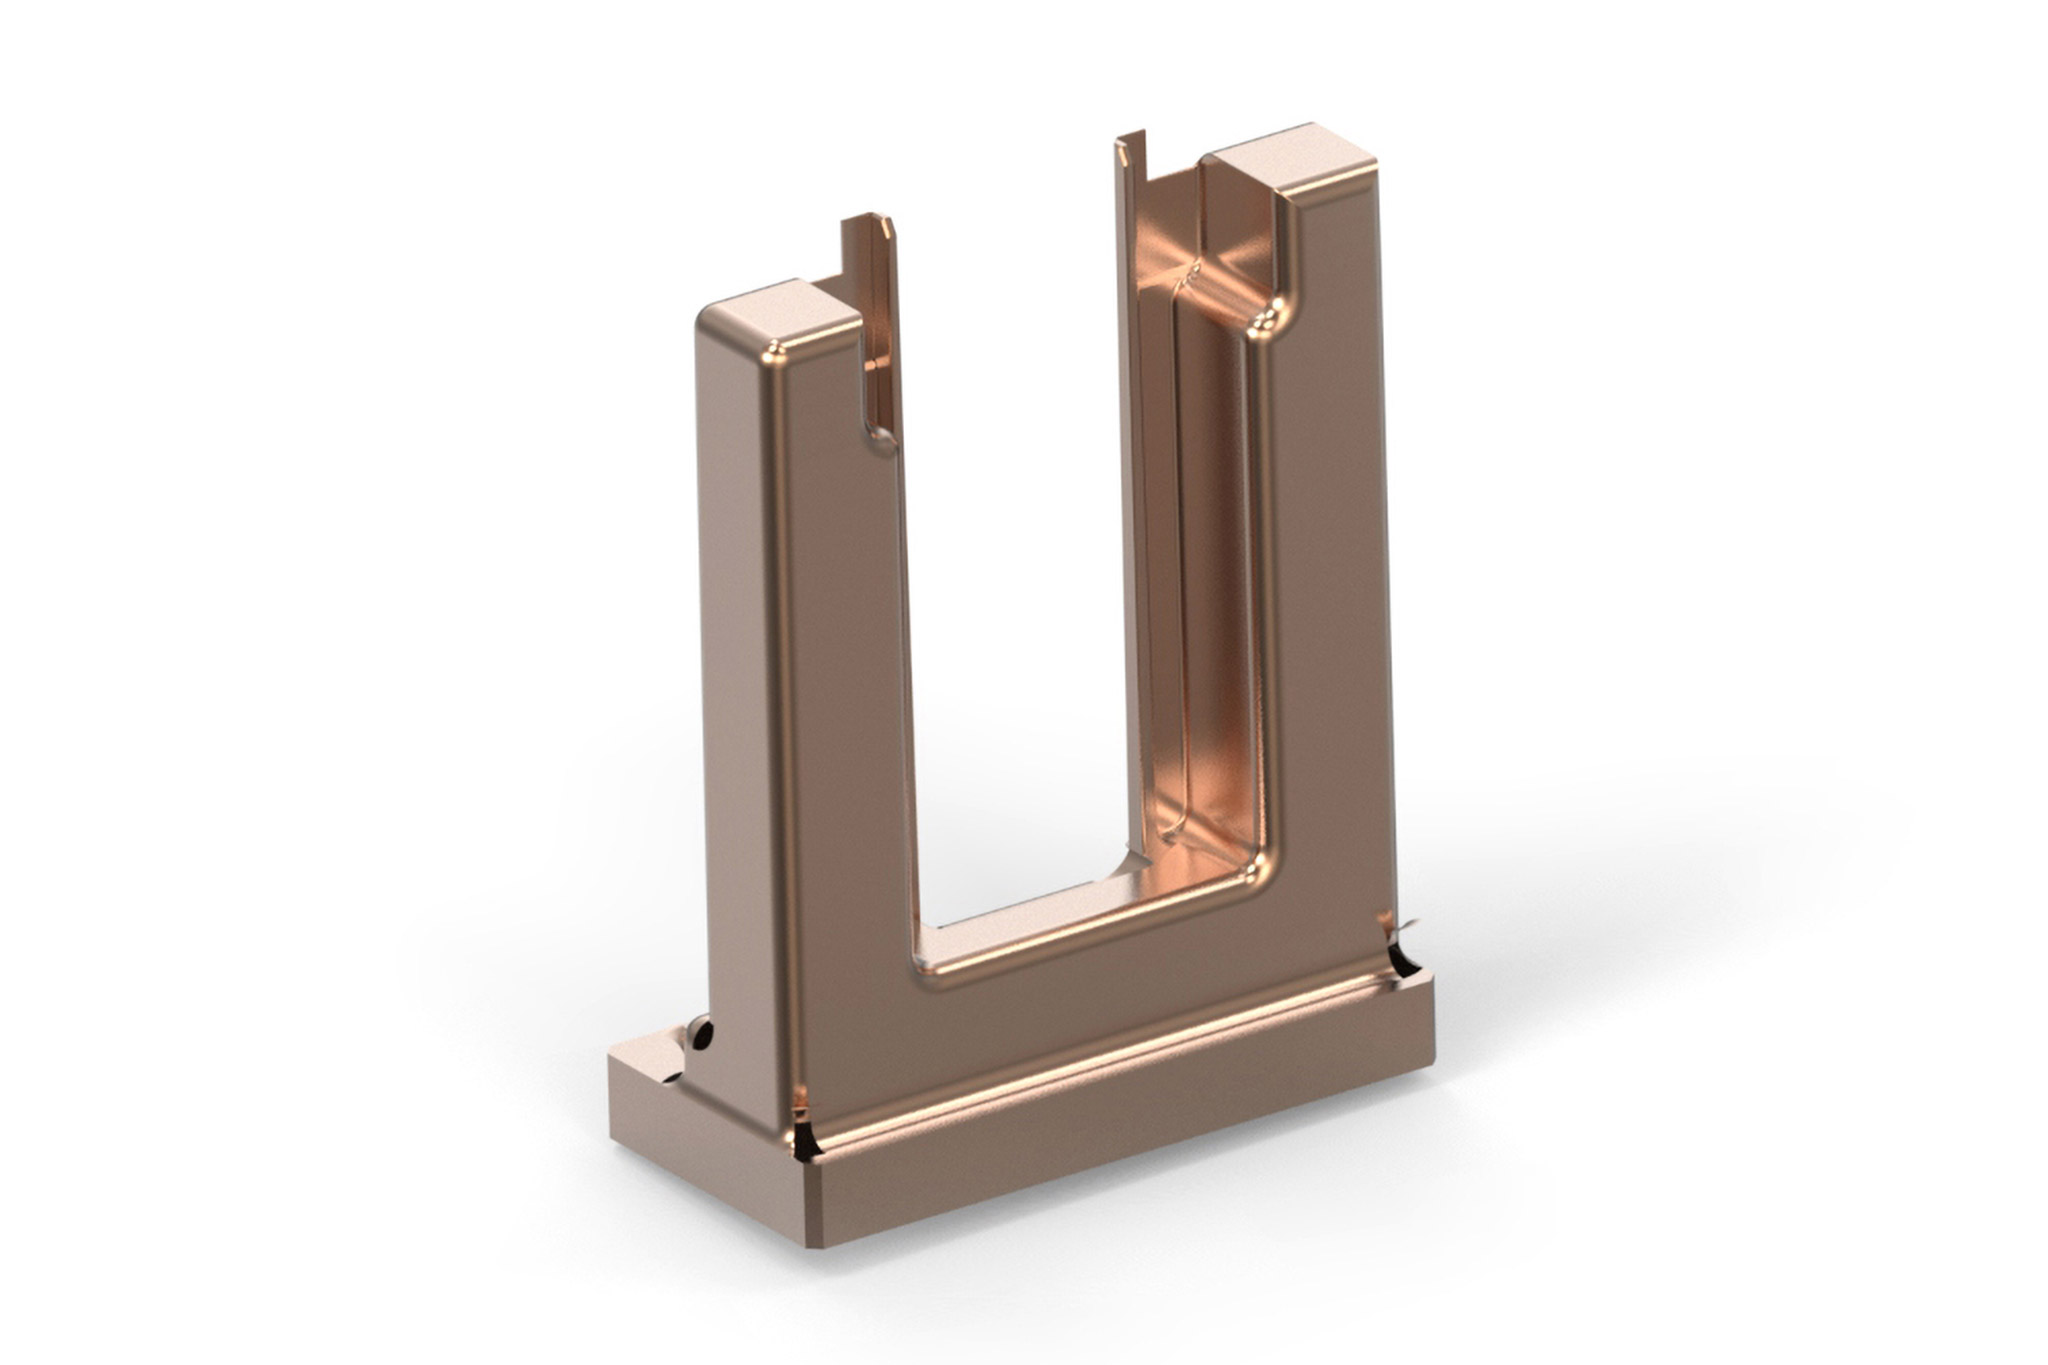
Manufacturing of electrodes for EDM processes requires machining of copper alloys and graphite materials. The selection of the electrode material depends on the requirements of the mould to be created. Copper alloys are comparatively expensive and are generally used for finishing the electrodes, when it comes to high surface quality and shape accuracy. Solid carbide end mills with special geometries by MAPAL guarantee high-precision machining results here.
Application example: Electrodes for spark eroding (EDM)
Graphite
Graphite has a highly abrasive effect on the tool and causes strong wear on the cutting edge. The profiles to be machined tend to burst with increasing wear. Therefore, a tool with suitable geometry and optimum cutting material is required. For machining graphite, MAPAL uses diamond-coated solid carbide tools or PCD-tipped tools.
Application example: Electrodes for spark eroding (EDM)
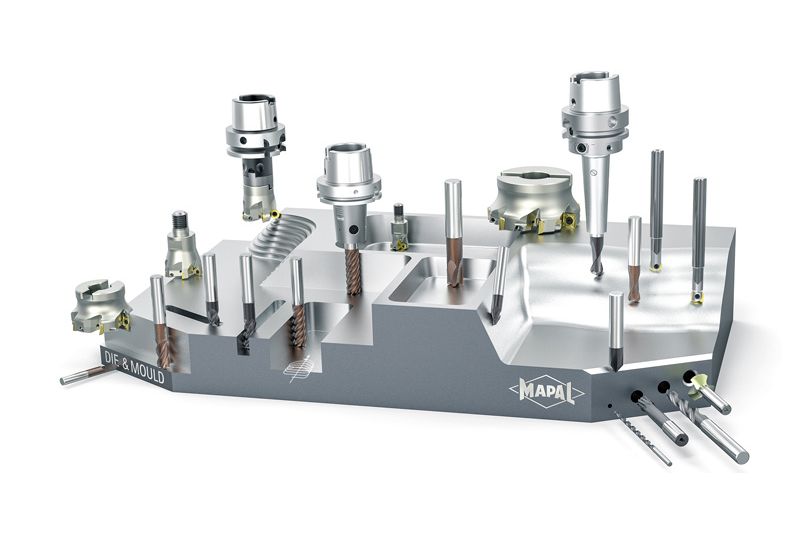
From the unmachined to the finished part
Find the right tool with just a few clicks: Depending on the machining, the specific operation and the tool requirement, you can quickly find the tool you want.
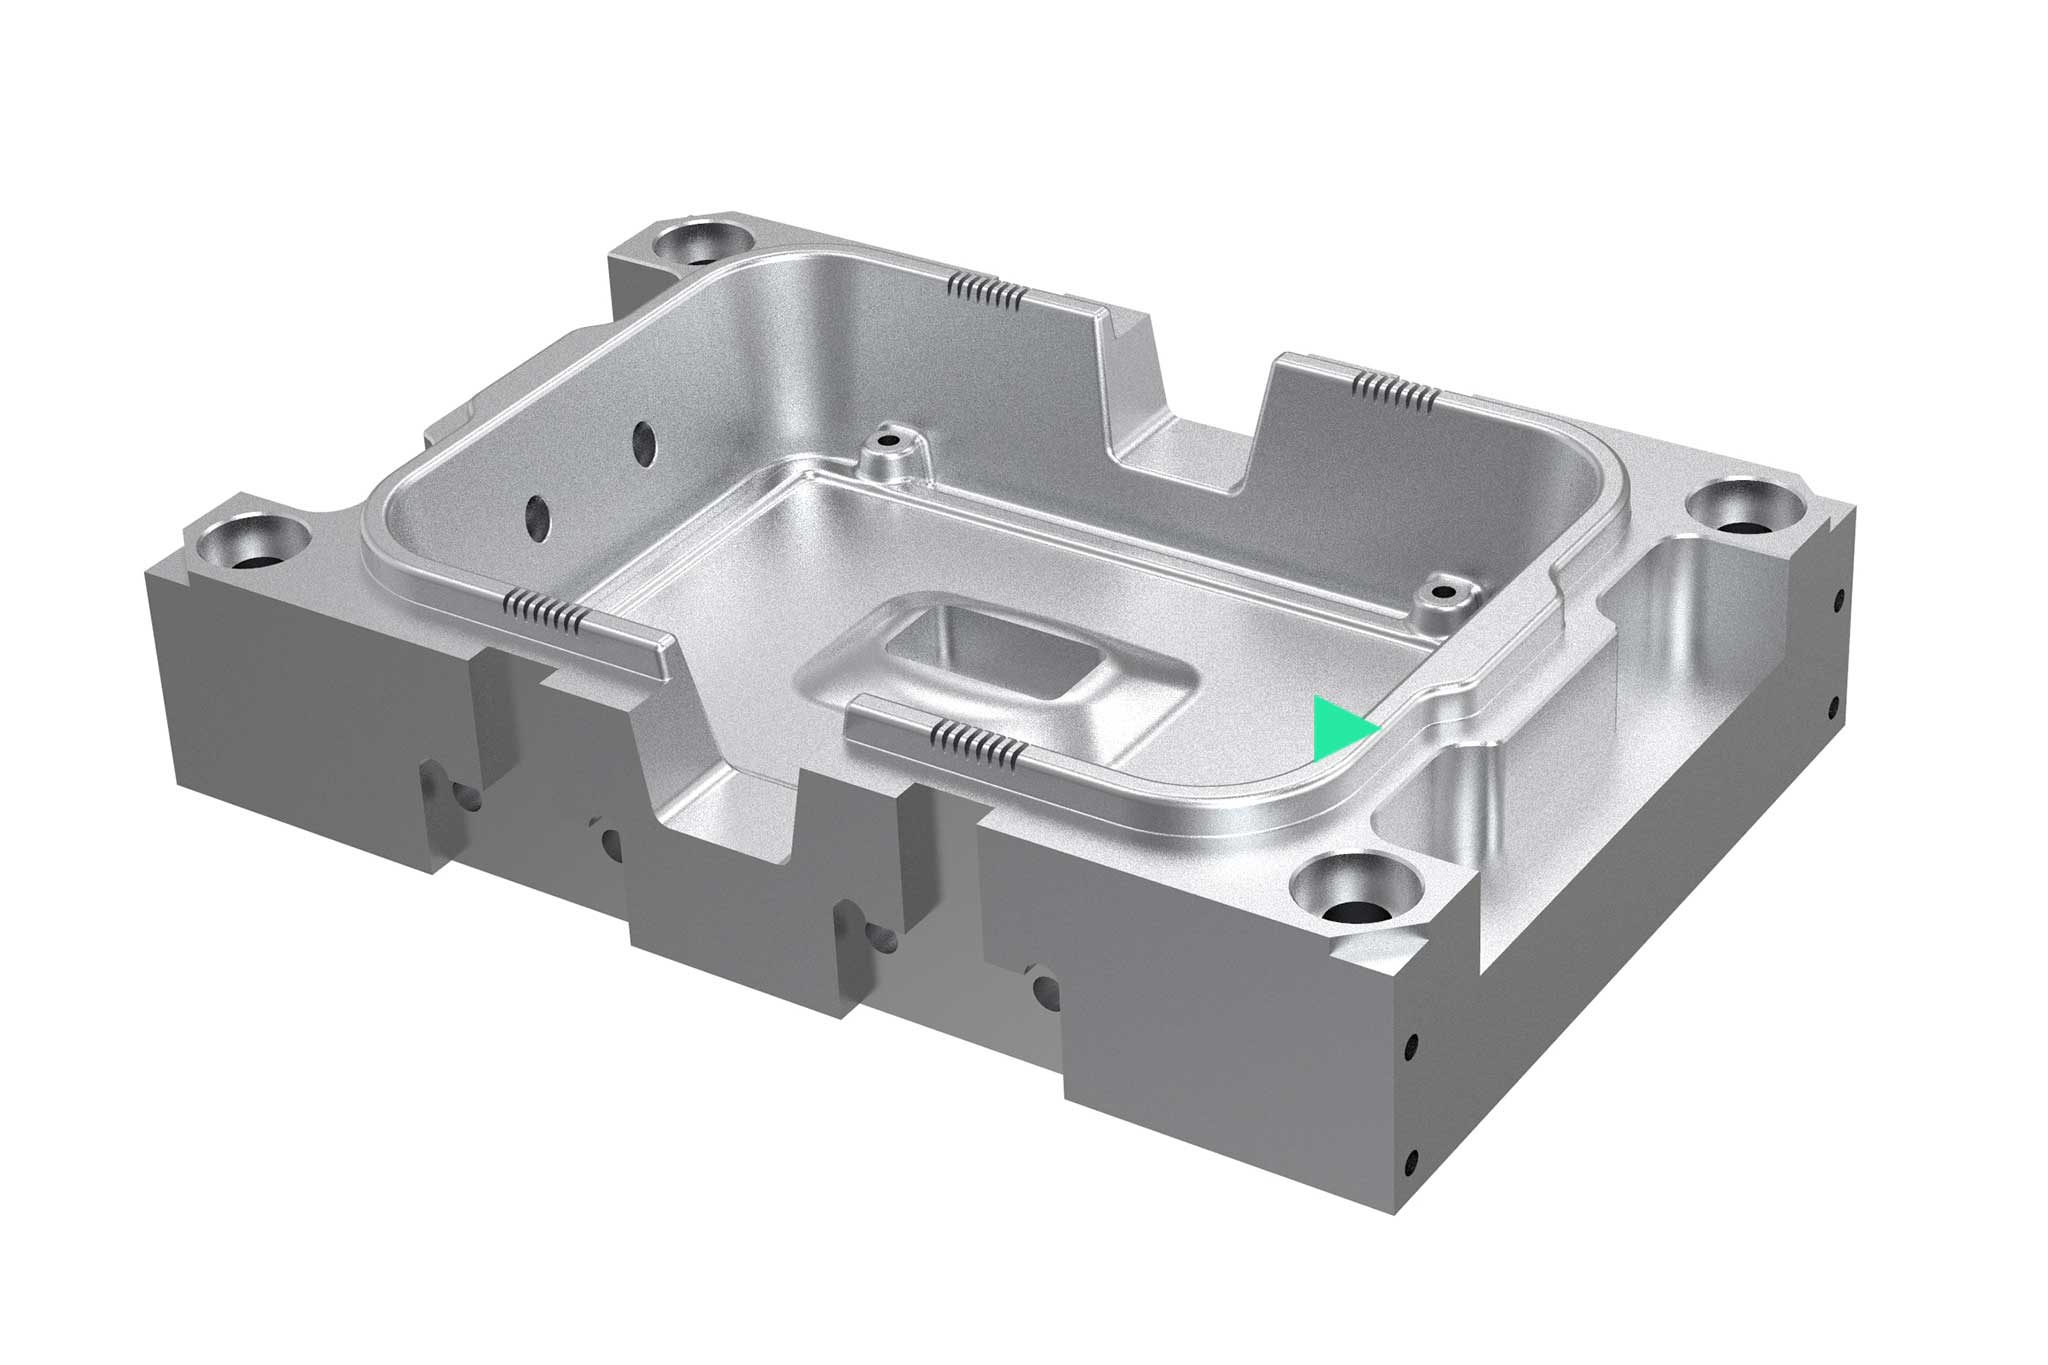
1__2D 表面
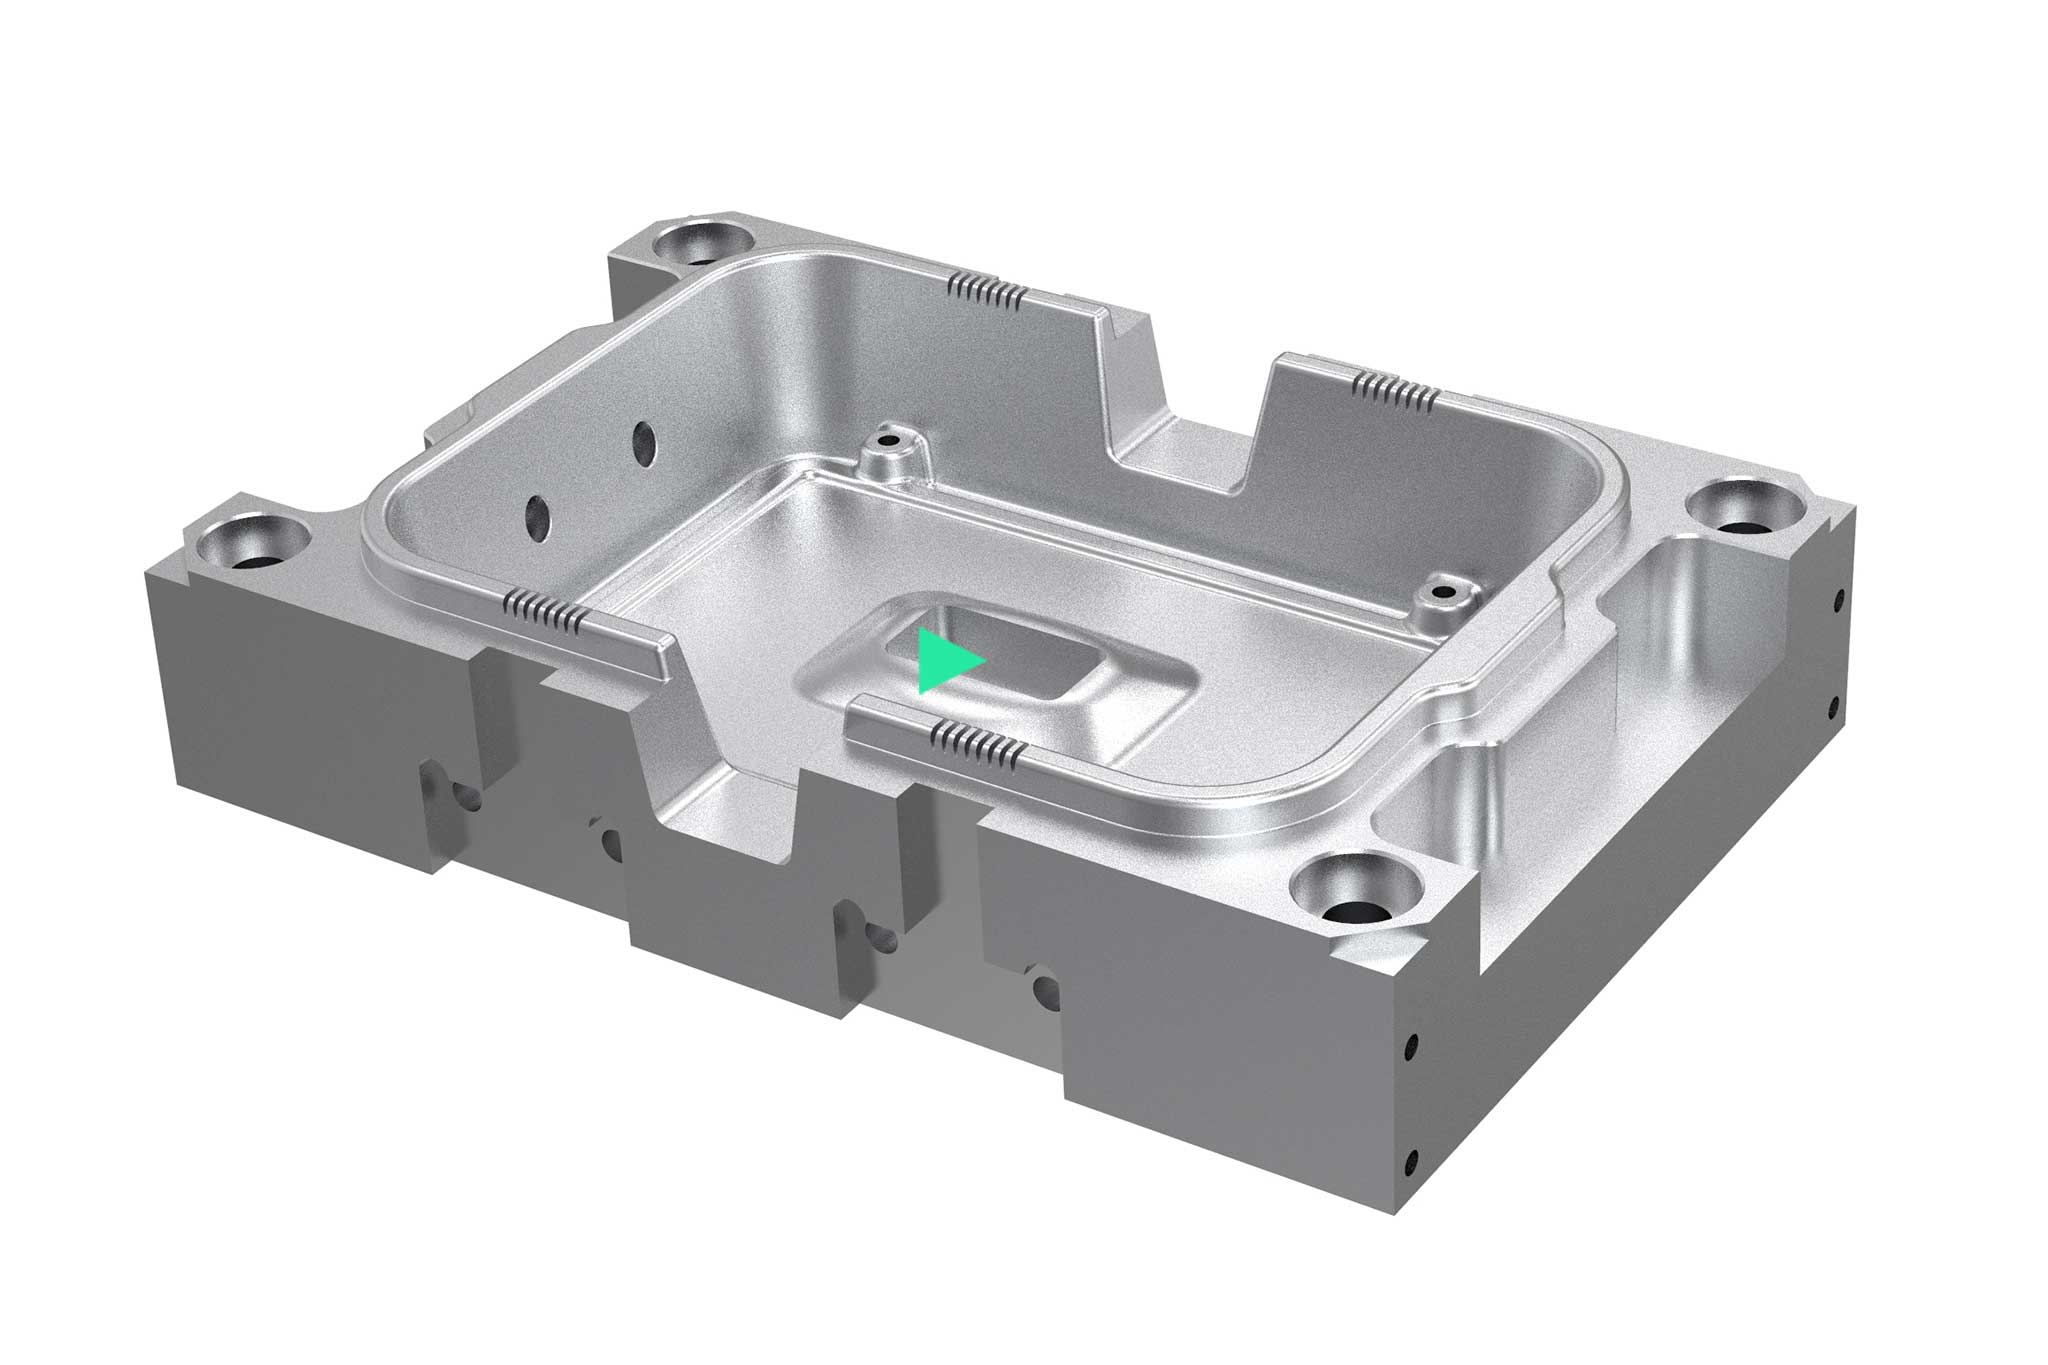
2__3D 表面
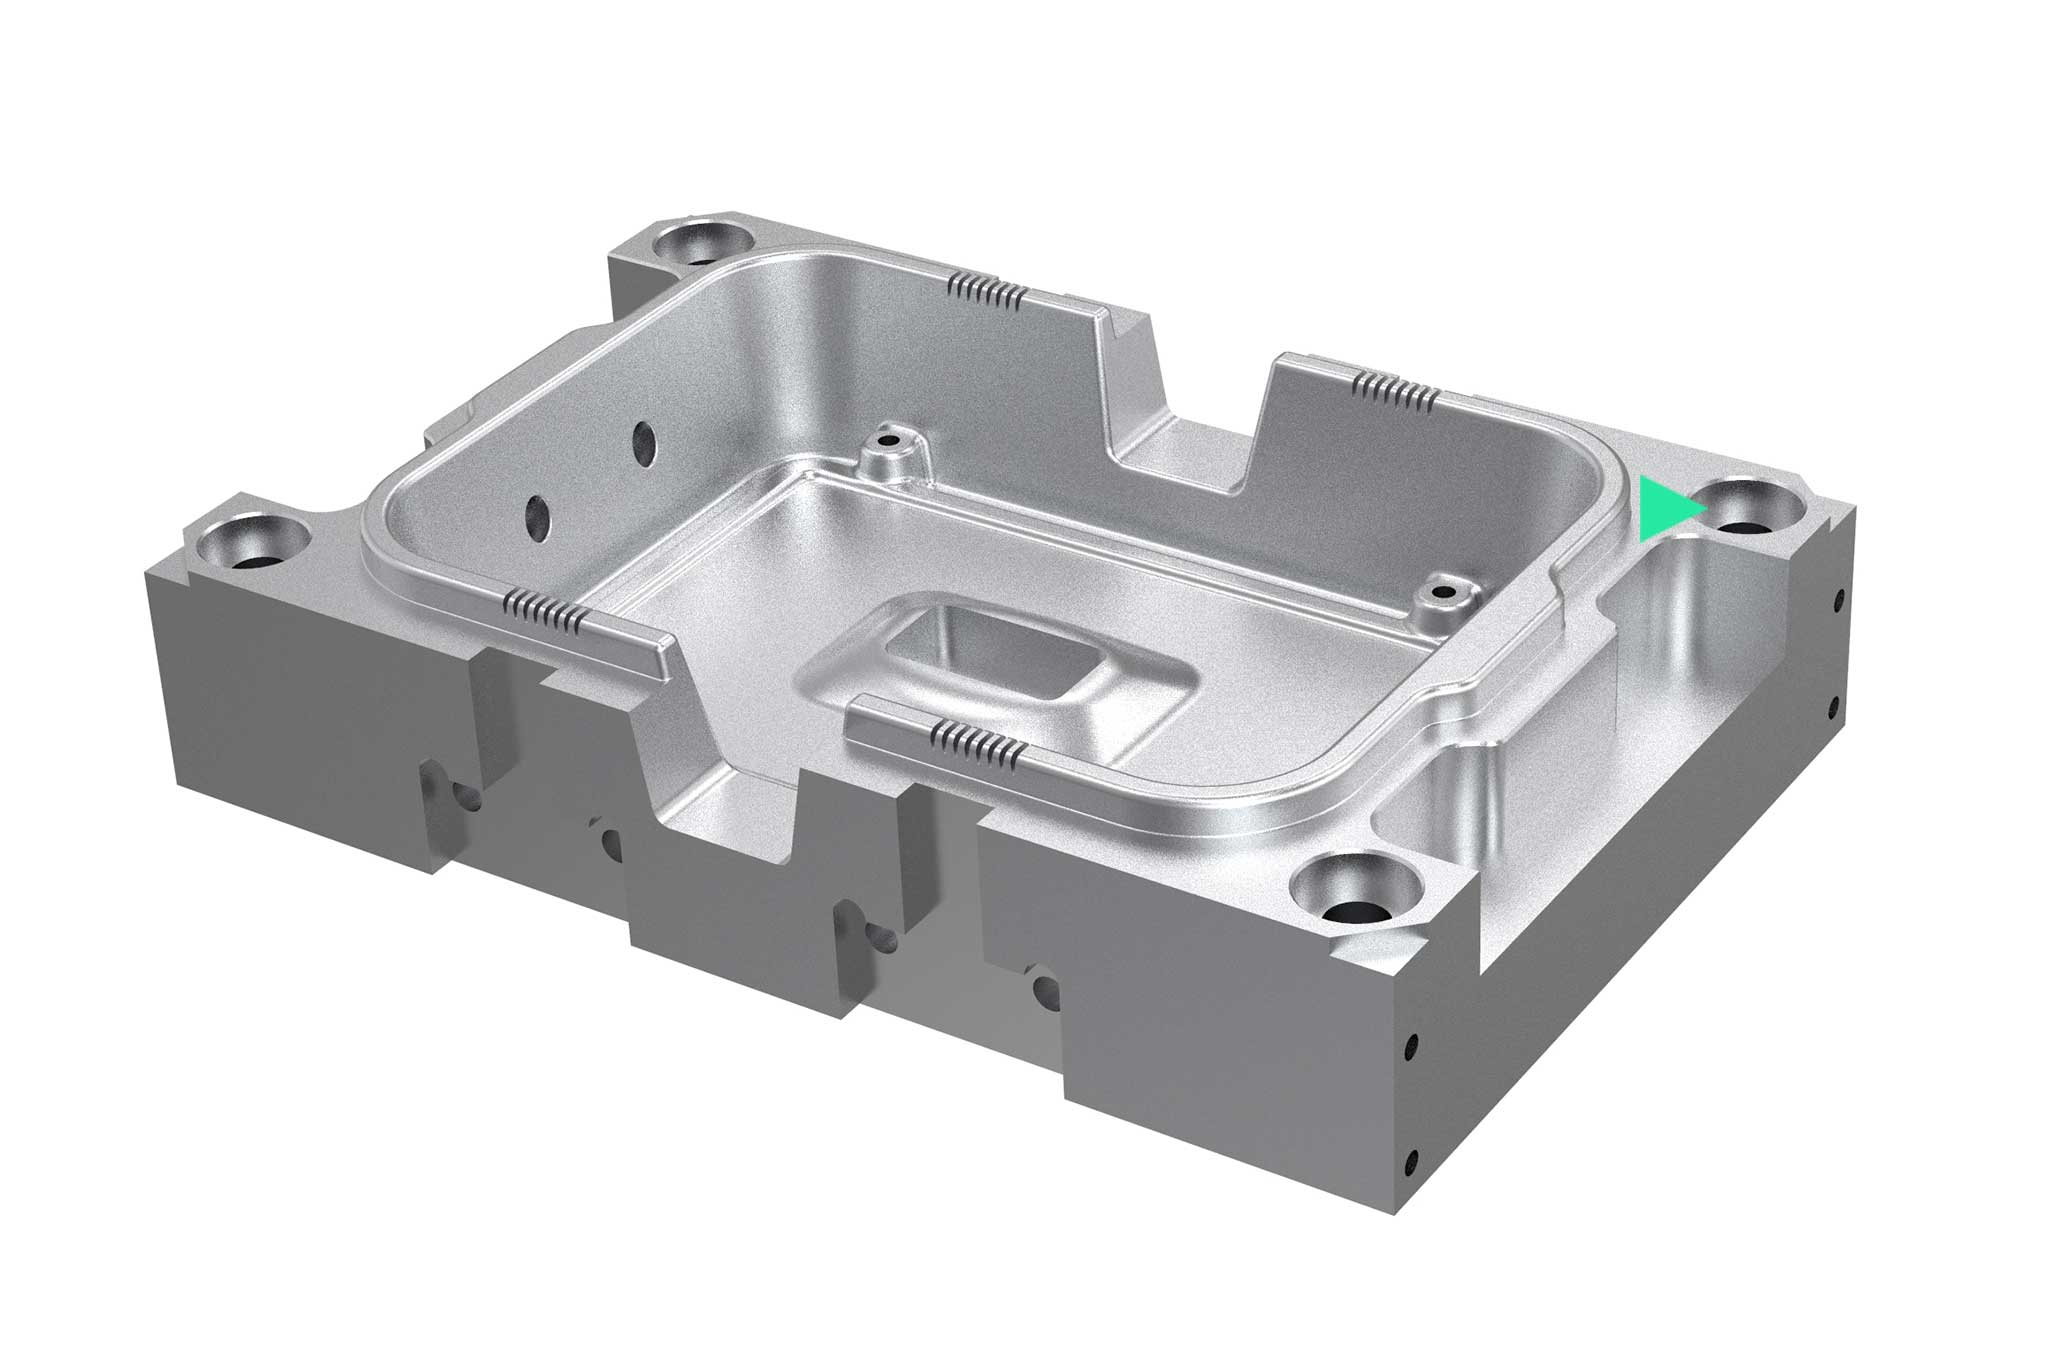
3__开放型腔
4__封闭型腔
5__螺旋铣削
6__平坦表面
7__薄壁和板翅
8__小孔和大孔
1 / 8
2D 表面
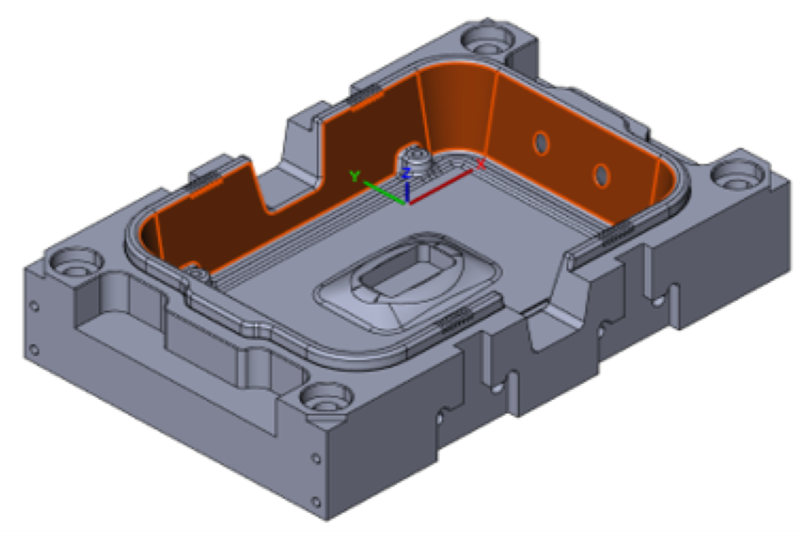
直接在机床上进行的加工过程,例如平面铣削、铣削型腔和直壁,都属于这一类。另一方面,使用 CAM 软件可以编程复杂几何形状。
前往加工 2D 表面的产品系列
2 / 8
3D 表面
在模具制造领域中,生产愈来愈复杂的形状是日常事务。。机床和 CAM 软件的不断发展将性能和生产力提高到一个更高的水平。因此,所使用的刀具也必须始终符合最先进的技术标准。为了在此处达到最佳状态,在设计之初就进行了工艺分析。
前往加工 3D 表面的产品系列
3 / 8
开放型腔
模具镶件还具有铸造或各种加装件所需的加工任务。用户越来越多地采用摆线铣削的方式来加工开放型腔(周长加工)。这种加工方式有助于优化加工时间并延长刀具寿命。
前往加工开放型腔的产品系列
4 / 8
封闭型腔
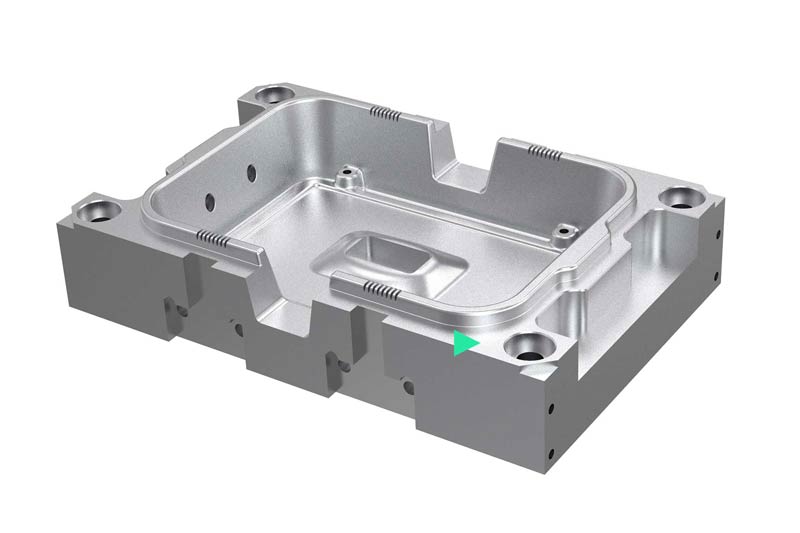
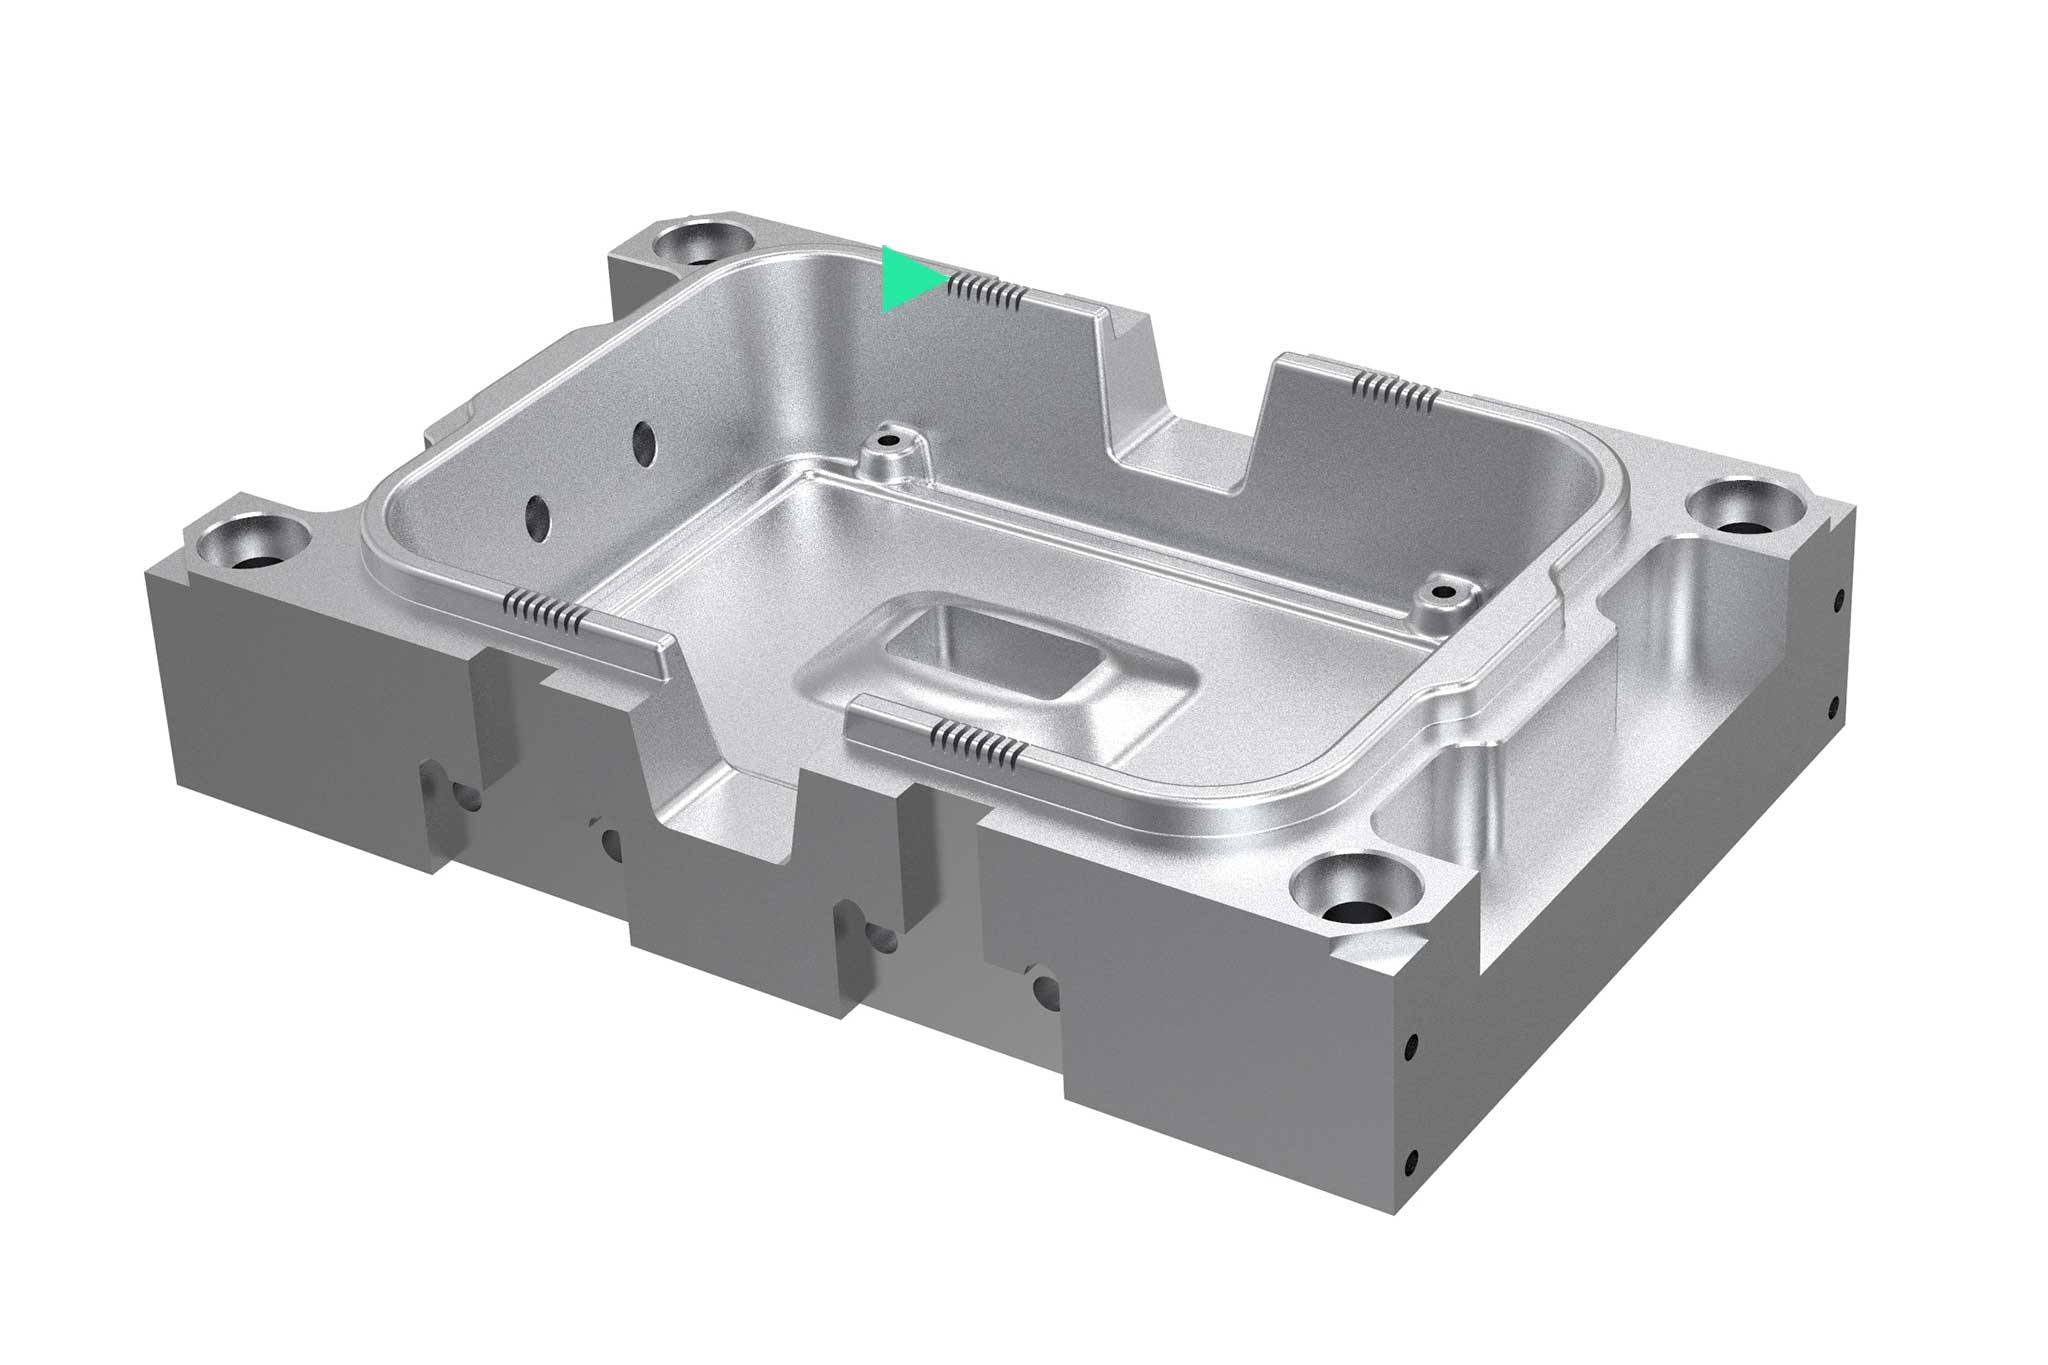
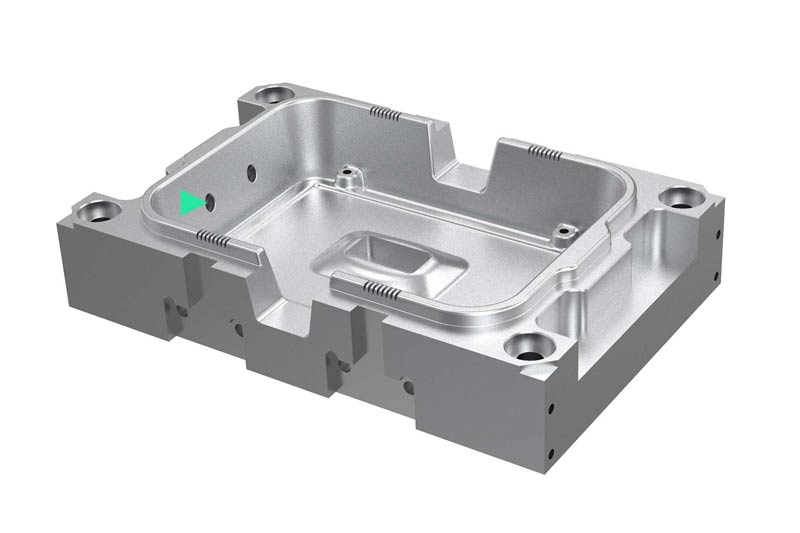
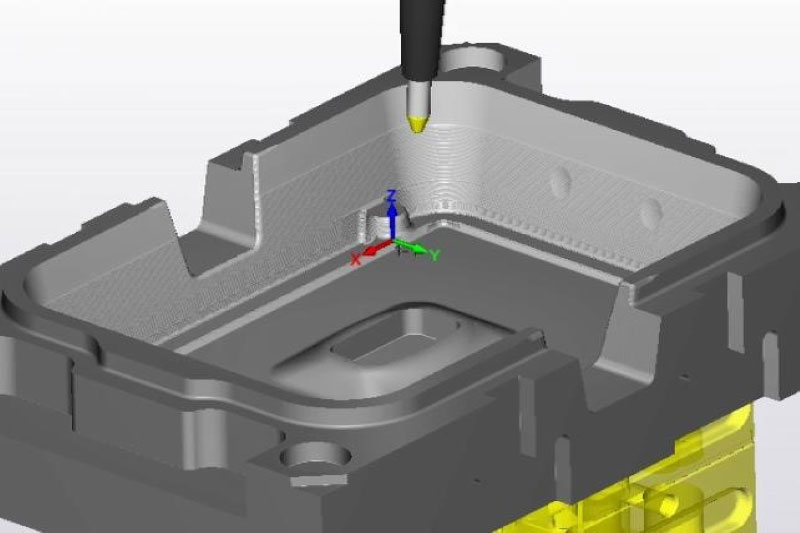
封闭型腔通常通过在Z平面上进行粗加工来产生。铣削时,通常选择通过斜坡开始加工。刀具的选择取决于墙壁的深度和要在组件上创建的起模斜度。具有模块化系统的MAPAL公司的广泛产品组合还包括大直径深型腔的加工。
前往加工封闭型腔的产品系列
5 / 8
螺旋铣削
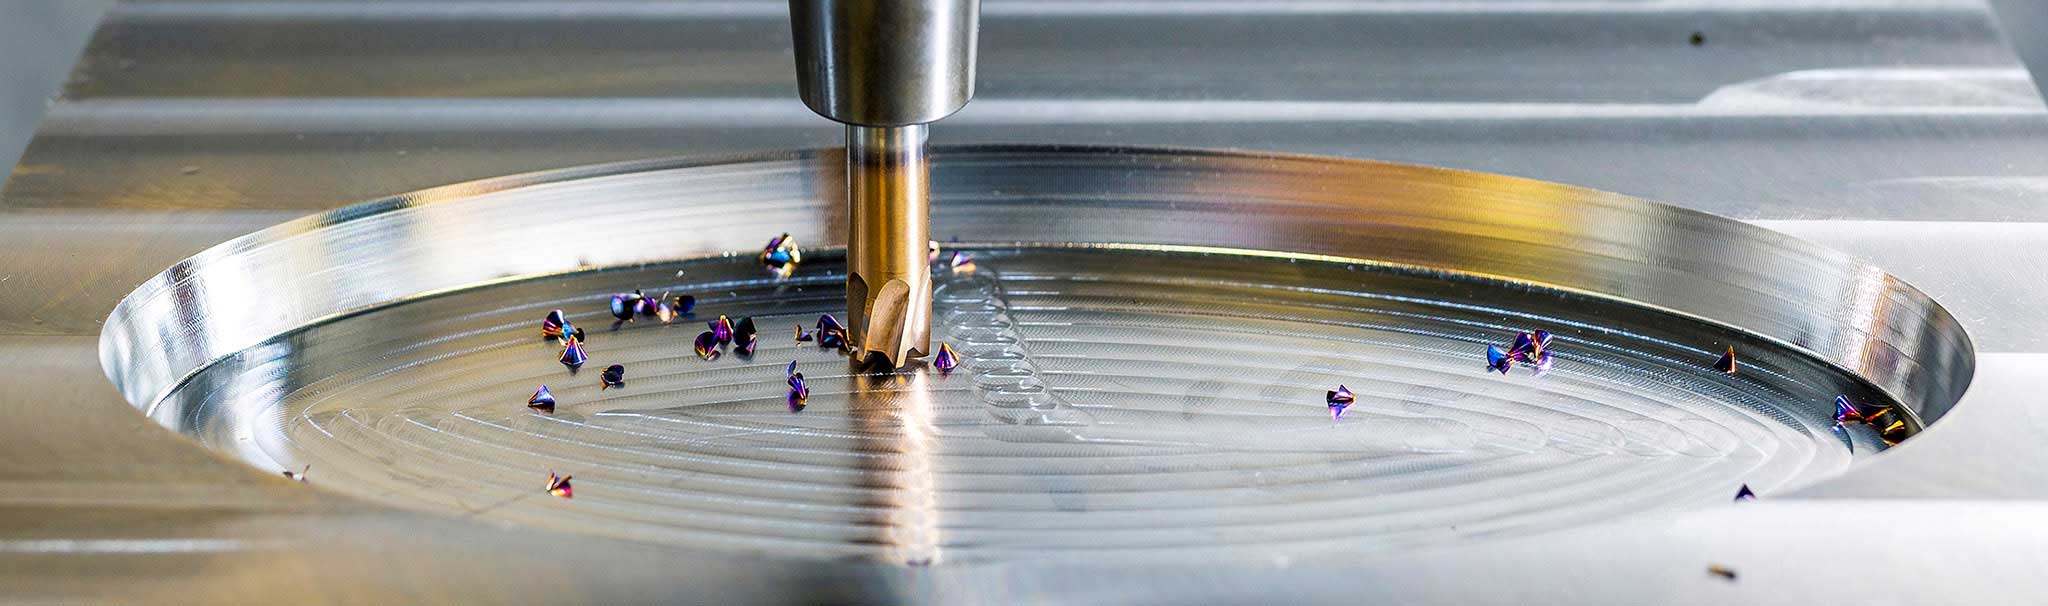
铣削加工时的主要重点是减少加工时间。对于加工封闭的圆形型腔的特定刀具几何形状,通常可以消除预钻孔过程。在进行螺旋式铣削时,编程具有螺旋形切口并适用于型腔尺寸的铣削轨迹 的。
螺旋式铣削产品系列
6 / 8
平坦表面
创建平坦表面的操作非常普遍,并且发生在模具制造的不同领域:无论是与组件相关,由于各自的铣削操作而与策略相关还是对模具闭合表面以及区段和冲压形状的要求。接着根据应用和要求选择正确的刀具。
前往加工平坦表面的产品系列
7 / 8
薄壁和板翅
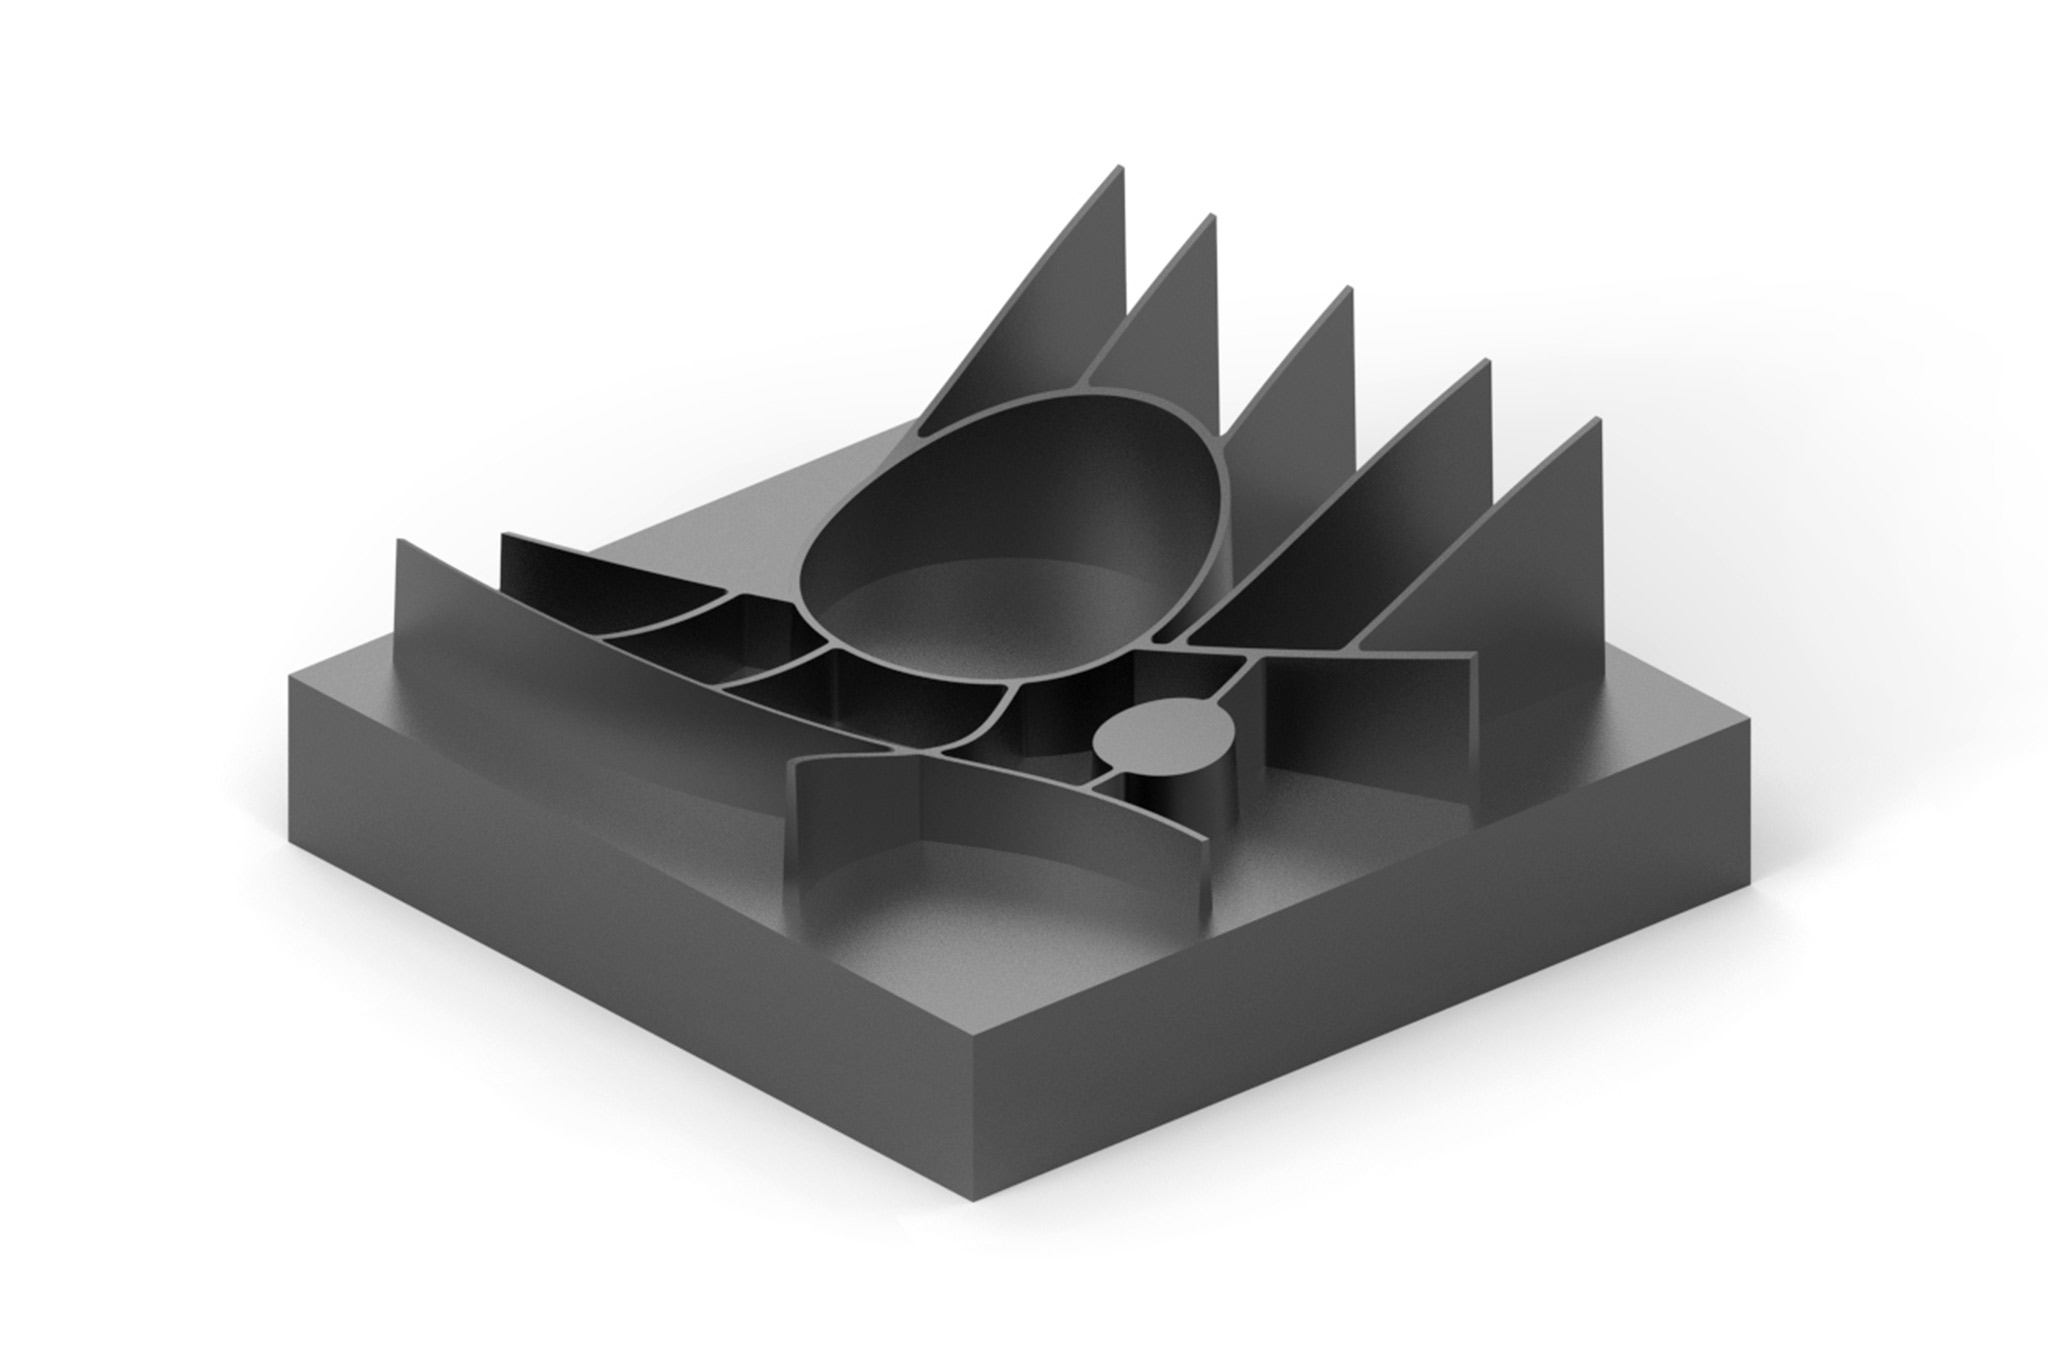
塑料注塑模具和压铸模具通常具有板翅和薄壁。例如,板翅越来越多地被铣削,因为这种加工方法与 EDM 加工方法(放电加工)相较便宜。通常使用小直径的长型或超长型硬质合金刀具。在此也可以提供适合相应板翅形状的定制解决方案(RibCutter)。
前往薄壁和板翅加工的产品系列
8 / 8
小孔和大孔
模具制造具有广泛的实心钻孔操作:从导柱的大孔到冷却系统的深孔,再到顶料销的高精度孔。MAPAL公司为各个制作工序提供全面的钻孔和铰孔刀具组合。
前往加工小孔和大孔的产品系列
1__2D 表面
1__2D 表面
2__3D 表面
2__3D 表面
3__开放型腔
3__开放型腔
4__封闭型腔
4__封闭型腔
5__螺旋铣削
5__螺旋铣削
6__平坦表面
6__平坦表面
7__薄壁和板翅
7__薄壁和板翅
8__小孔和大孔
8__小孔和大孔
全部来自同一供应商
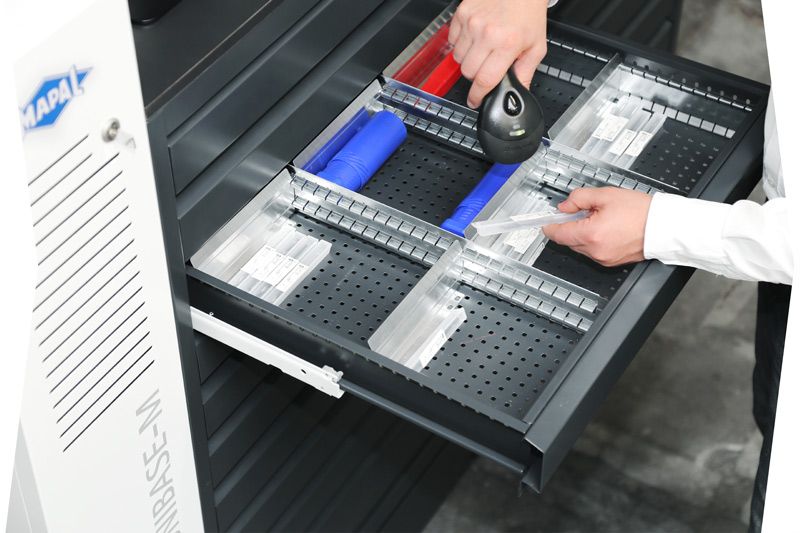
2. 刀具物流
即使在刀具管理中,也具有成本效益。智能分配系统大大减少了非生产时间。
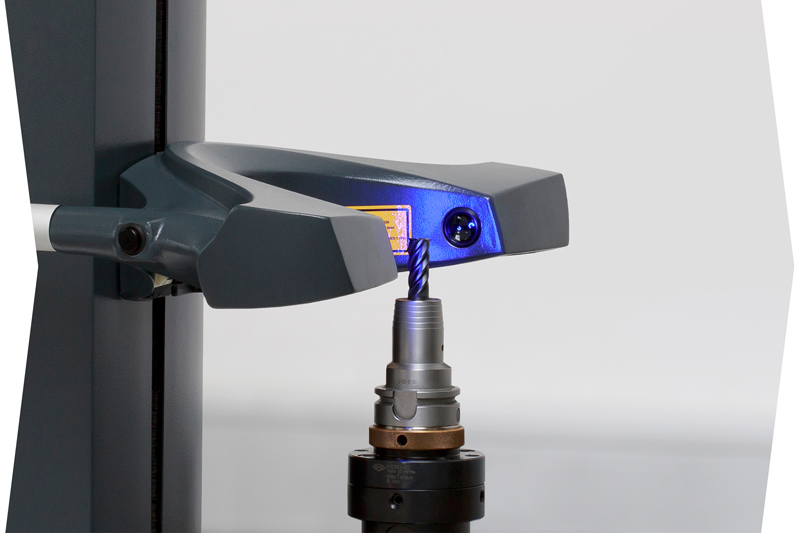
4. 测量和安装
可靠的安装和测量设备由于其准确性和安装刀具时的用户友好操作而令人信服。
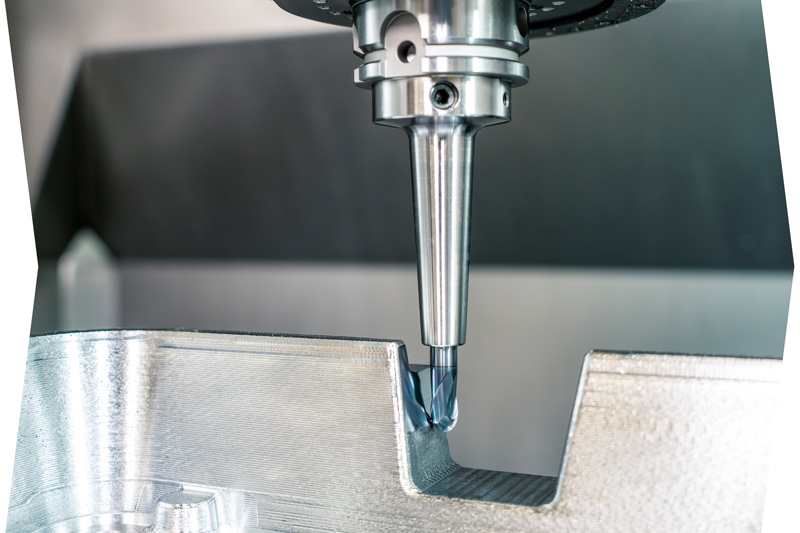
5. 刀具和夹持技术
从主轴到切削刃口 - MAPAL为模具行业提供广泛的刀具和夹持技术。
7. 数字化和自动化
快速和简单的数字化:C-Connect以数字方式将测量数据从设定的夹具传输到机床上。它还能监控机床的状态。
8. 修磨
客户可以在很短的时间内收到修磨后的刀具。也可根据要求提供上门收件和送货服务。
工程工作流程 - 从理论到实践
为客户需求寻找完美的解决方案即是MAPAL公司的主张。除了个性化的特殊解决方案和广泛的标准产品组合之外,还提供全面的服务来优化地设计从产品理念到切屑的整体过程。客户可以信赖切削加工技术领导者多年的经验。
1.客户咨询
如有个人咨询,请直接与MAPAL公司销售代表联系。在个人对话中,他们与客户一起探讨具体要求和范围(完整或部分加工),并直接在零件的3D模型上讨论细节。
MAPAL公司模具制造团队很期待收到电子邮件 咨询,并将尽快建立直接联系。
2.项目分析
受访者根据3D模型和机器数据,分析制造任务并制定有效的加工策略。
项目分析的组成部分包括:
3.工艺流程设计
无论重点是灵活性还是生产率:加工专家基于3D模型模拟所拟定的过程,从而指出可优化的潜力。他们在CAM编程中检查和改进加工参数,从而确保稳定和经济的生产。
工艺流程设计包括:
4.刀具解决方案
用于刀具和模具制造的范围广泛的MAPAL公司标准产品系列为各种应用提供了最佳的刀具解决方案。如有必要,还可提供个性化的特殊解决方案。
对用户的优势:
5.刀具测试和报价
在对切削加工任务进行交流后,MAPAL公司支持客户使用切削加工所需的刀具。这是针对相应应用情况量身定制的有充分根据的报价的基础。
6.伙伴合作
即使在共同成功之后,MAPAL公司的专家仍然会与客户保持密切联系。若随着时间的推移出现可优化的潜力或其它刀具被证明更好,MAPAL公司将很乐意支持您进一步提高生产力和经济性。
刀具出入库管理 重磨服务 广泛的设定装置和测量仪器产品组合
Further items about the die&mould area
Our retail partners
Responsibility according to postcode areas
1__Postcode 35
2__Postcode 44
3__Postcode 51
4__Postcode 56, 57
5__Postcode 58, 59
6__Postcode 60, 61
7__Kod pocztowy 63 - 69
8__Kod pocztowy 70 - 73
9__Kod pocztowy 74, 75
10__Kod pocztowy 76 - 79
11__Kod pocztowy 80 - 87
12__Kod pocztowy 88, 89
13__Kod pocztowy 90 - 97
14__Dania
15__Włochy
16__Portugalia
1 / 16
Kod pocztowy 35
FRITZ WEG GmbH & Co. KG
Tel.: +49 2774 701-0www.fritzweg.de
2 / 16
Kod pocztowy 44
Jansen Schneidwerkzeuge Vertriebs GmbH
Tel.: +49 2391 9177-0www.j-s-v.com
3 / 16
Kod pocztowy 51
Jansen Schneidwerkzeuge Vertriebs GmbH
Tel.: +49 2391 9177-0www.j-s-v.com
4 / 16
Kod pocztowy 56, 57
FRITZ WEG GmbH & Co. KG
Tel.: +49 2774 701-0www.fritzweg.de
5 / 16
Kod pocztowy 58, 59
Jansen Schneidwerkzeuge Vertriebs GmbH
Tel.: +49 2391 9177-0www.j-s-v.com
6 / 16
Kod pocztowy 60, 61
Heinrich Meier GmbH
Tel.: +49 7041 9530-0www.heinrich-meier.de
7 / 16
Postcode 63 - 69
Heinrich Meier GmbH
Phone: +49 7041 9530-0www.heinrich-meier.de
8 / 16
Postcode 70 - 73
Dieter Schätzle GmbH & Co. KG
Phone: +49 7462 9465-0www.schaetzle-werkzeuge.de
9 / 16
Heinrich Meier GmbH
Phone: +49 7041 9530-0www.heinrich-meier.de
10 / 16
Postcode 76 - 79
Dieter Schätzle GmbH & Co. KG
Phone: +49 7462 9465-0www.schaetzle-werkzeuge.de
11 / 16
Postcode 80 - 87
AB1-Tools e.K.
Phone: +49 9826 333-2241www.ab1-tools.com
12 / 16
Postcode 88, 89
Dieter Schätzle GmbH & Co. KG
Phone: +49 7462 9465-0www.schaetzle-werkzeuge.de
13 / 16
Postcode 90 - 97
AB1-Tools e.K.
Phone: +49 9826 333-2241www.ab1-tools.com
14 / 16
Danmark
EDECO TOOL APS
Phone: +45 7060 2029www.edeco.dk
16 / 16
Portugal
Álamo-Ferramentas Unipessoal Lda Rua da ETAR, Lote 9
Zona Industrial de Oiã
3770-059 Oiã
Phone: +351 234 728-193
Email:
geral@alamo-ferramentas.com
1__Postcode 35
1__Postcode 35
2__Postcode 44
2__Postcode 44
3__Postcode 51
3__Postcode 51
4__Postcode 56, 57
4__Postcode 56, 57
5__Postcode 58, 59
5__Postcode 58, 59
6__Postcode 60, 61
6__Postcode 60, 61
7__Postcode 63 - 69
7__Postcode 63 - 69
8__Postcode 70 - 73
8__Postcode 70 - 73
9__Postcode 74, 75
9__Postcode 74, 75
10__Postcode 76 - 79
10__Postcode 76 - 79
11__Postcode 80 - 87
11__Postcode 80 - 87
12__Postcode 88, 89
12__Postcode 88, 89
13__Postcode 90 - 97
13__Postcode 90 - 97
14__Danmark
14__Danmark
15__Italy
15__Italy
16__Portugal
16__Portugal