Sistemi di trazione elettrici

I produttori e i fornitori di automobili stanno affrontando nuove sfide nel campo dei componenti dei motori elettrici. Un esempio che dimostra l’entità di tali sfide è costituito dal corpo di un motore elettrico: rispetto alla scatola del cambio, questo deve essere prodotto con tolleranze molto più strette, dal momento che la precisione influisce in maniera determinante sul grado di efficienza del motore elettrico. 

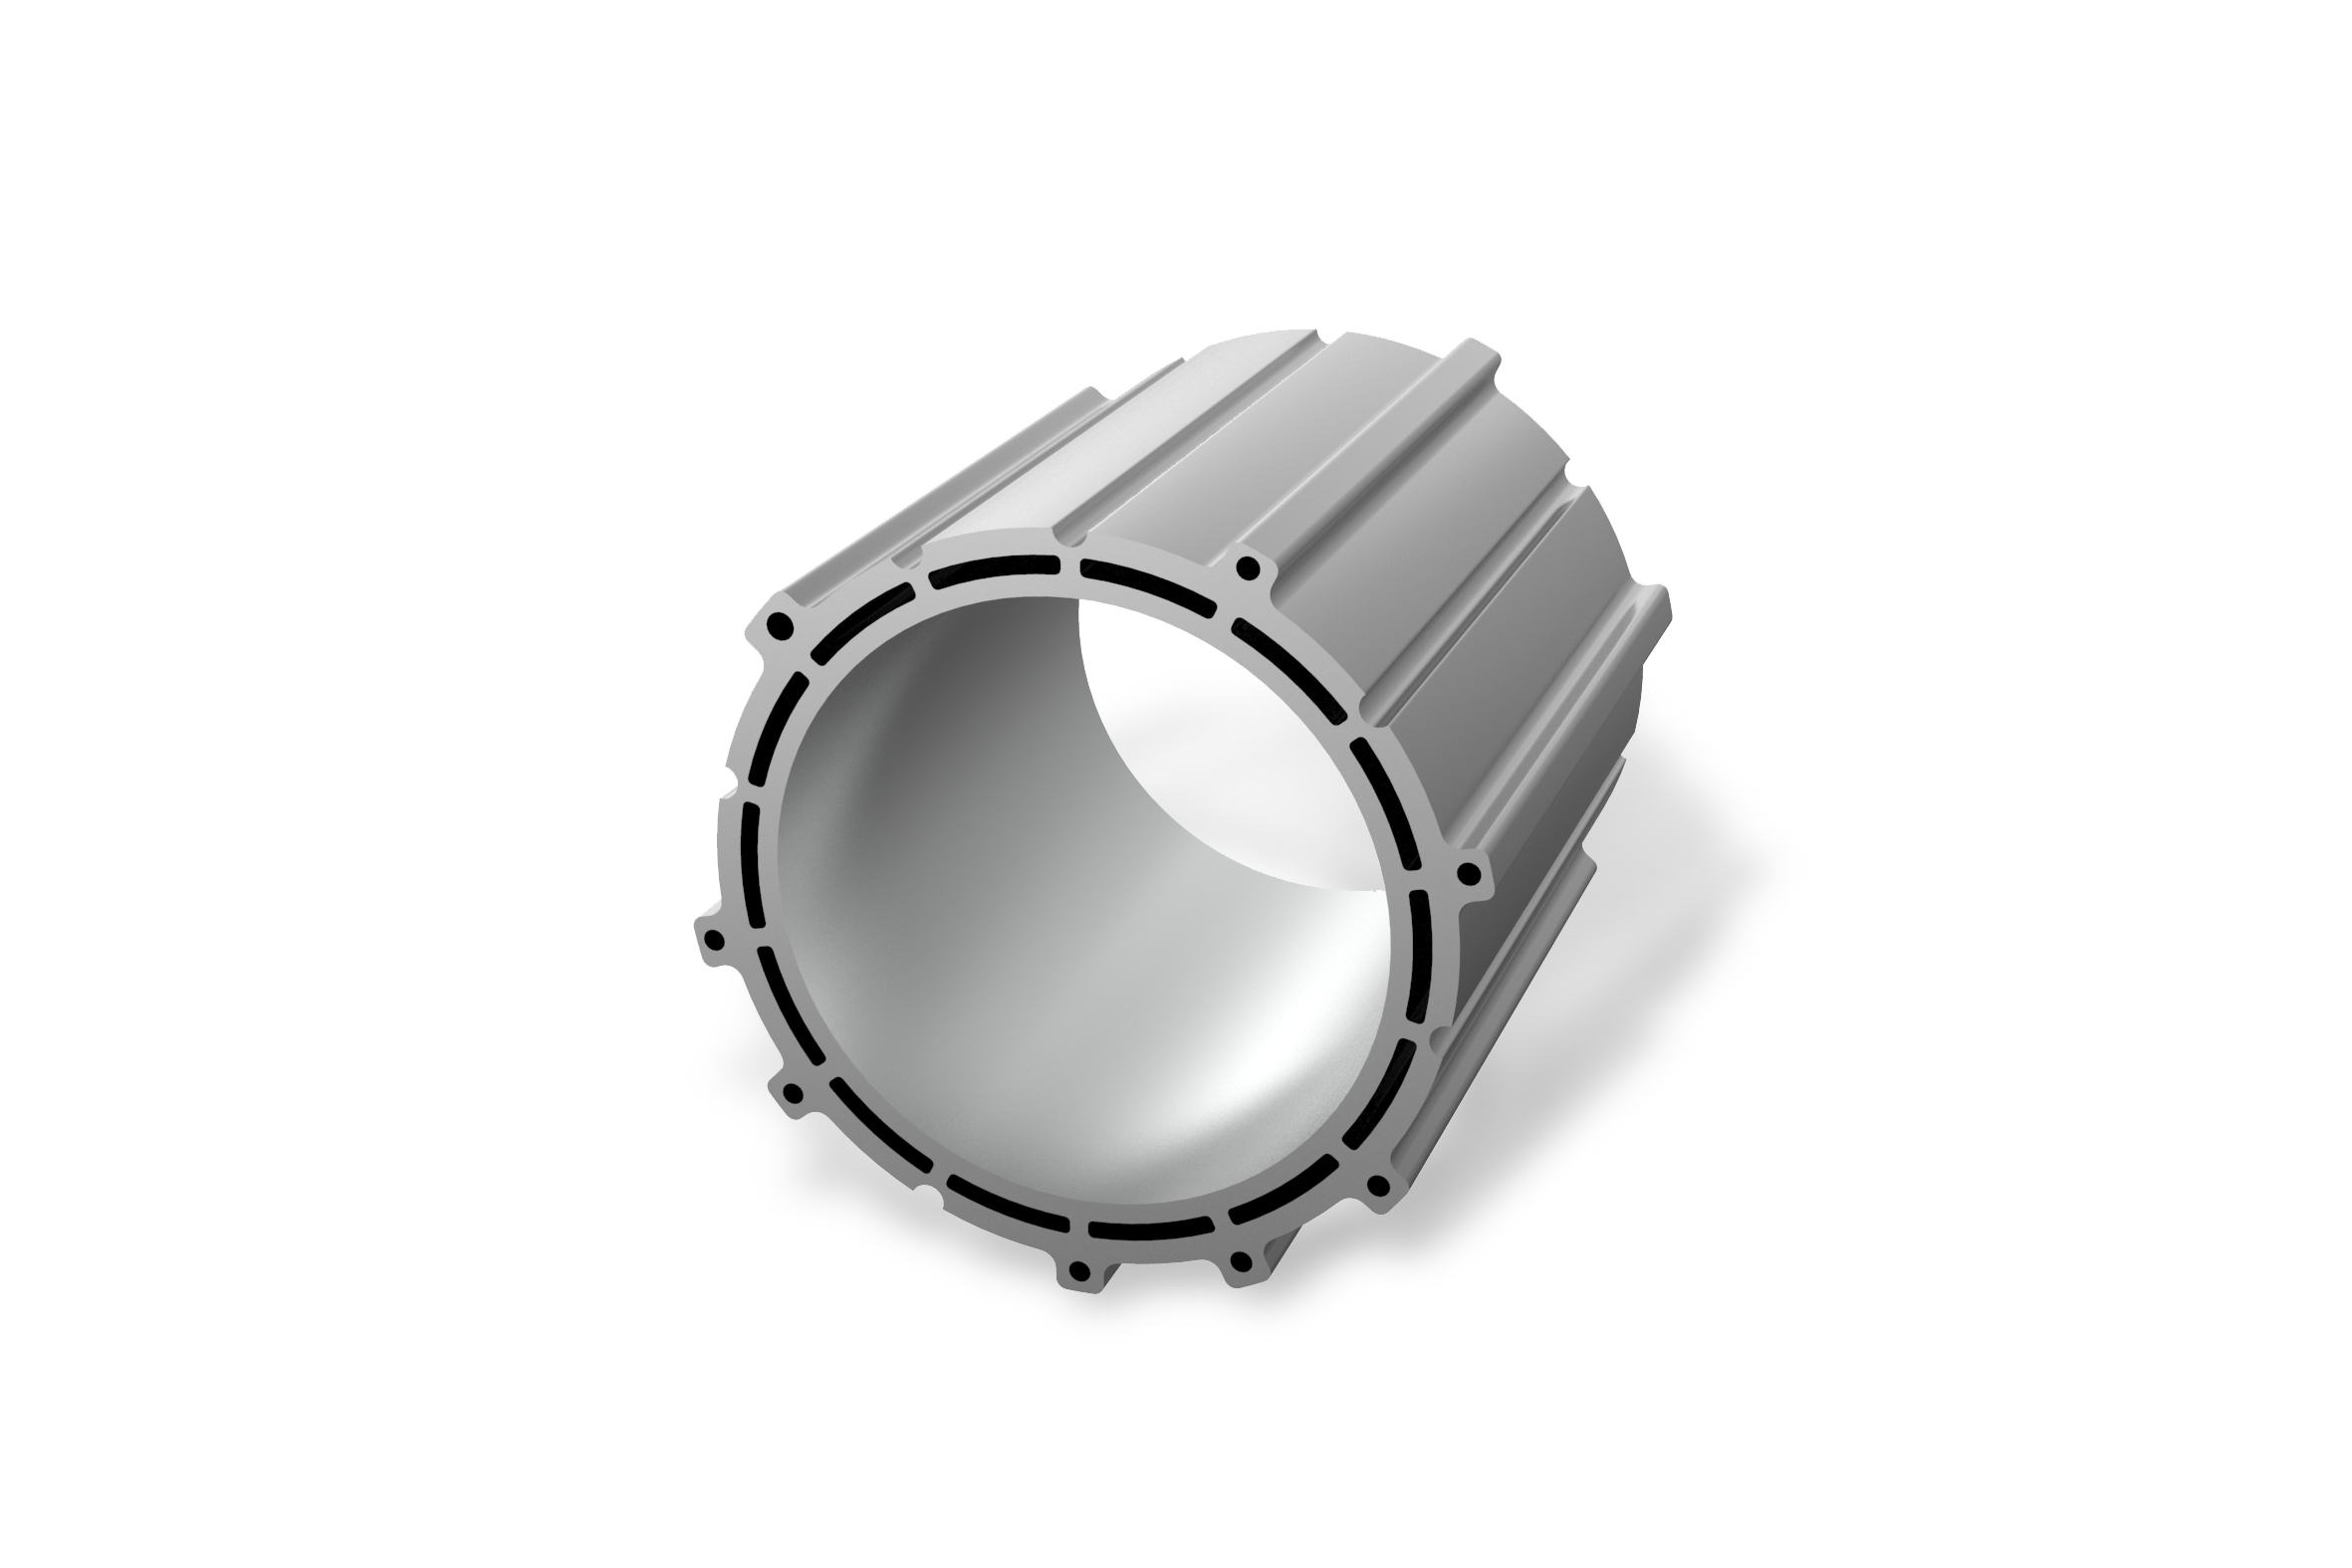
Inoltre, la sua speciale struttura, come ad esempio i canali di raffreddamento integrati, fa sì che il corpo del motore elettrico presenti pareti molto più sottili rispetto a quelle della scatola del cambio. In alcuni di questi corpi vengono anche pressate le bronzine in acciaio. Speciali schermi di protezione nell’utensile assicurano che i trucioli in acciaio non entrino in contatto con le superfici in alluminio durante la lavorazione e non le danneggino. 

さまざまなハウジングタイプの機械加工条件&特性
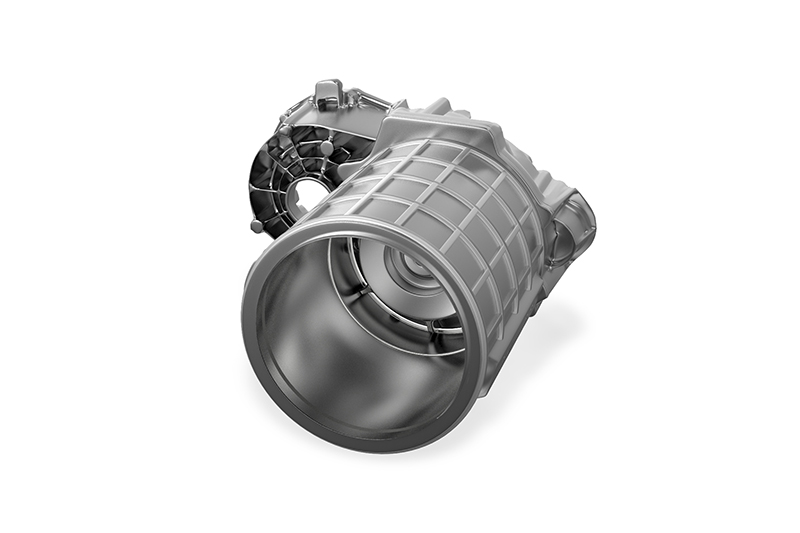

Basic procedure for machining of stator housings

The machining process as well as the tools are designed individually depending on the
measurement situation, machine park and clamping setup. In this way, the cutting forces
applied to the component are kept as low as possible. The machining of the stator bore is divided into 3 steps: Pre-machining, Semi-finish machining and Finish machining.
Stator housing external machining

External Machining stator housing
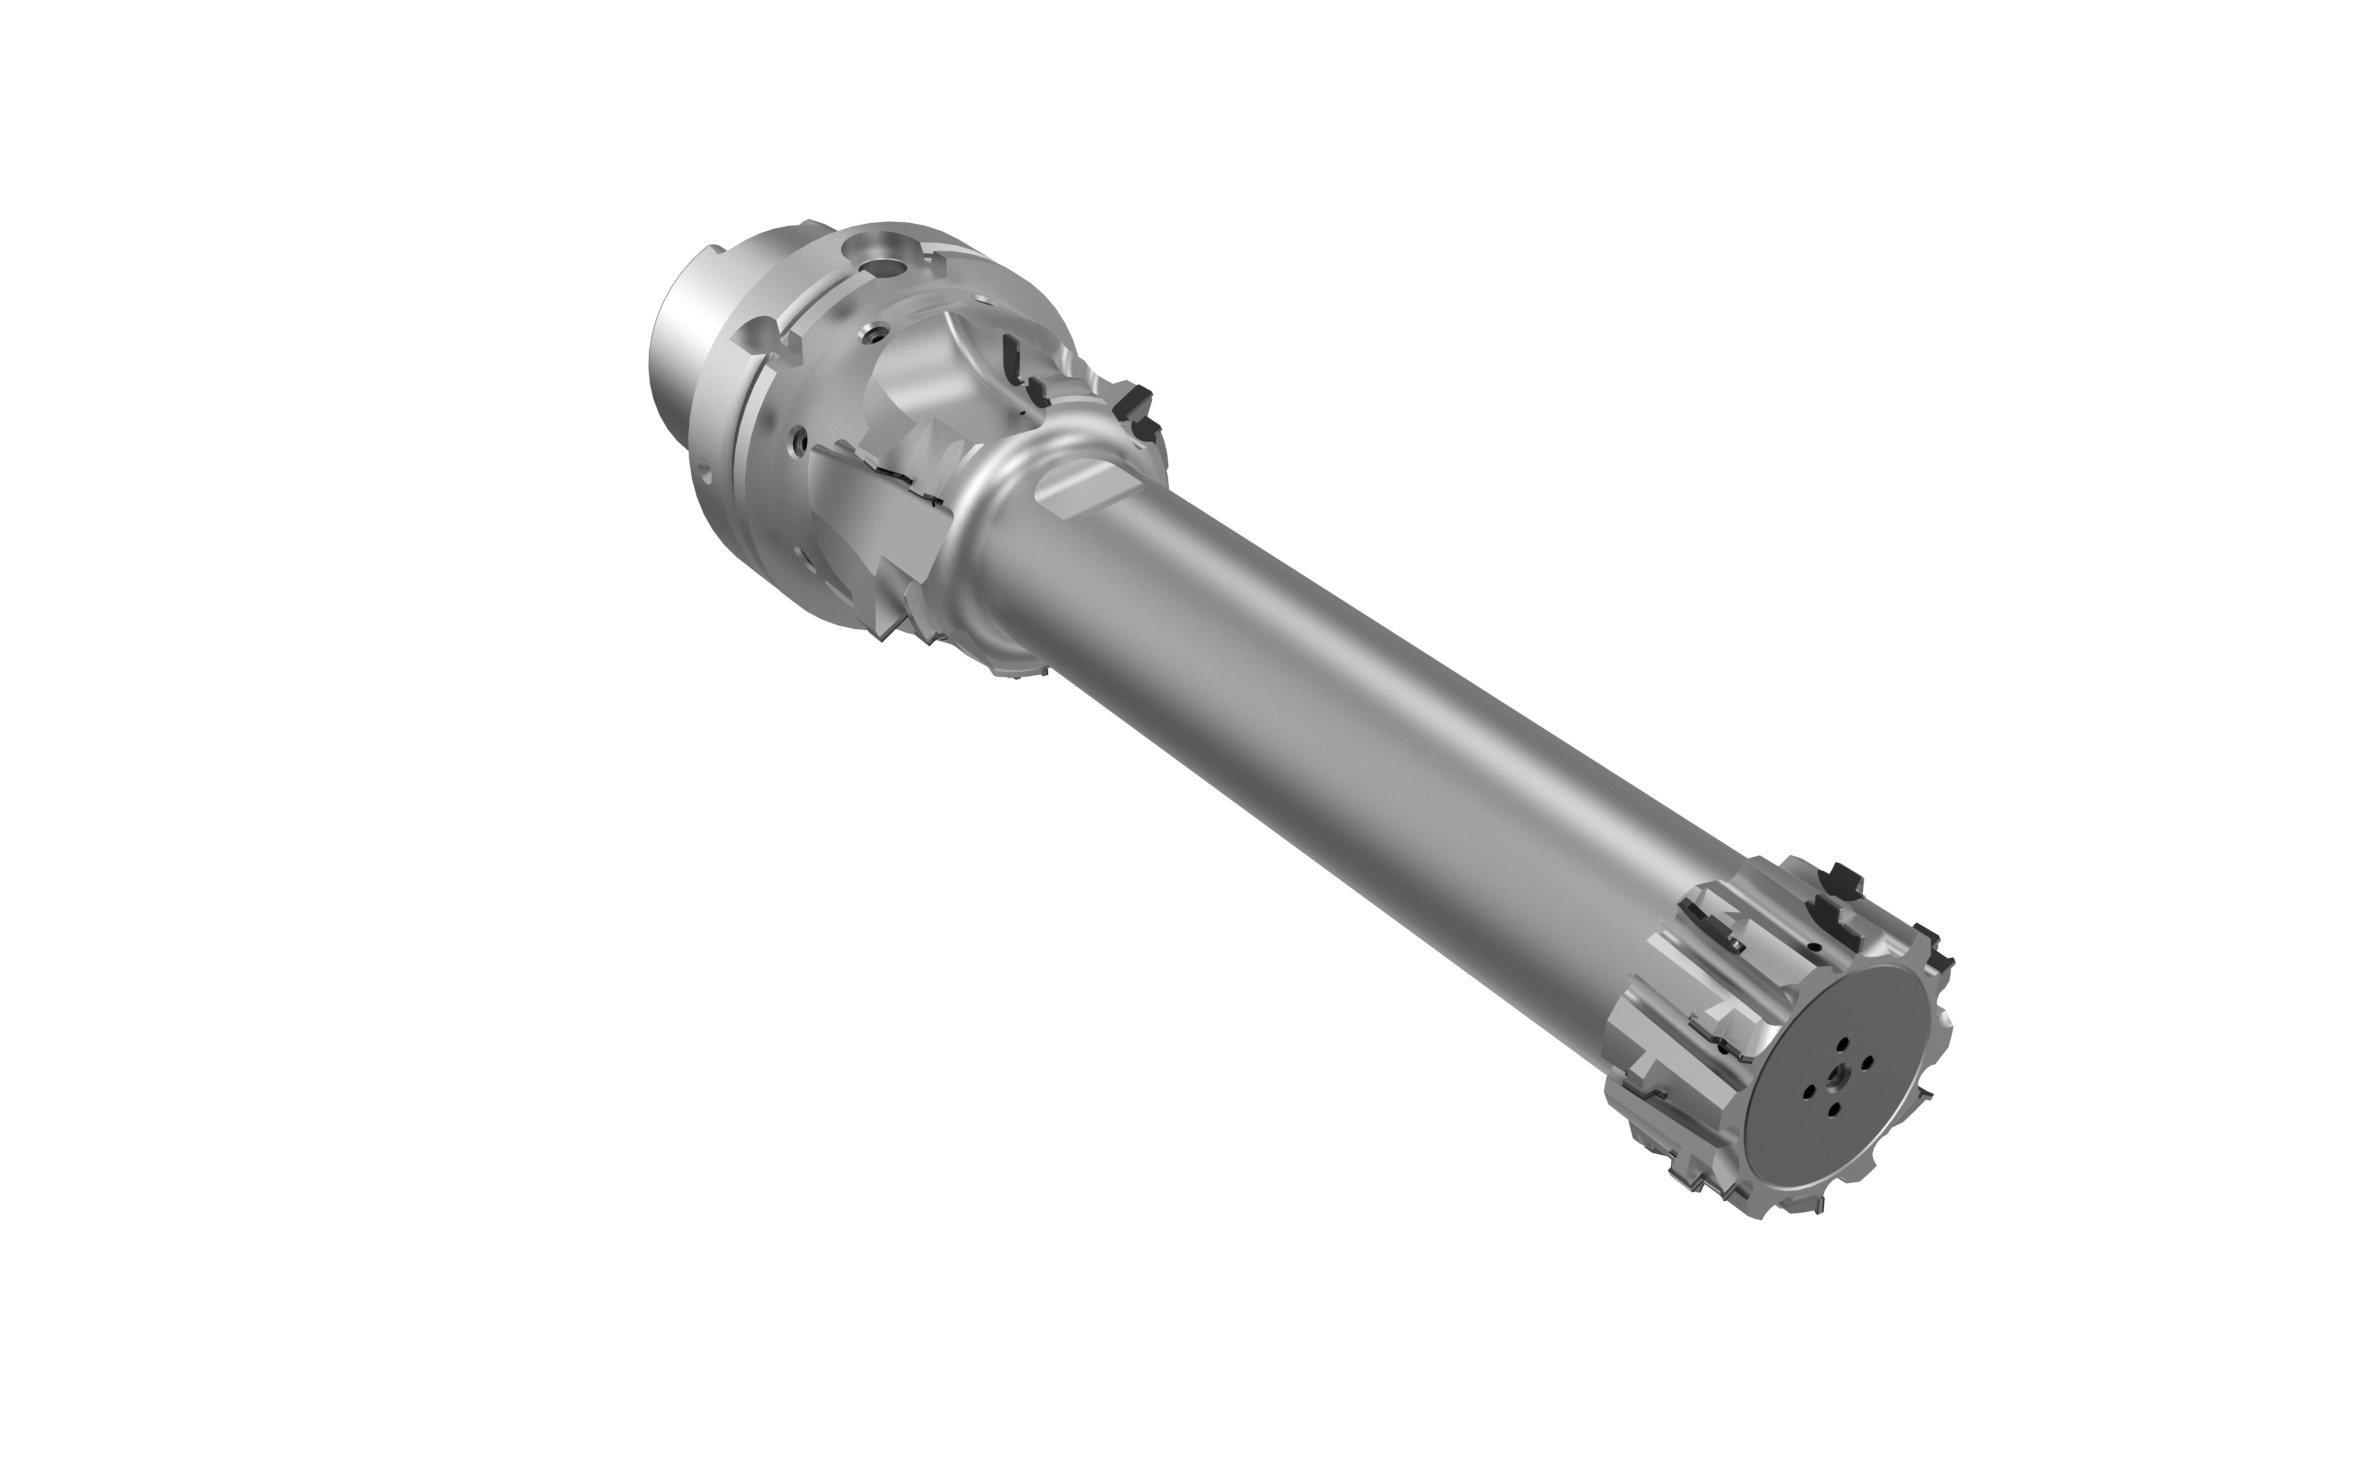
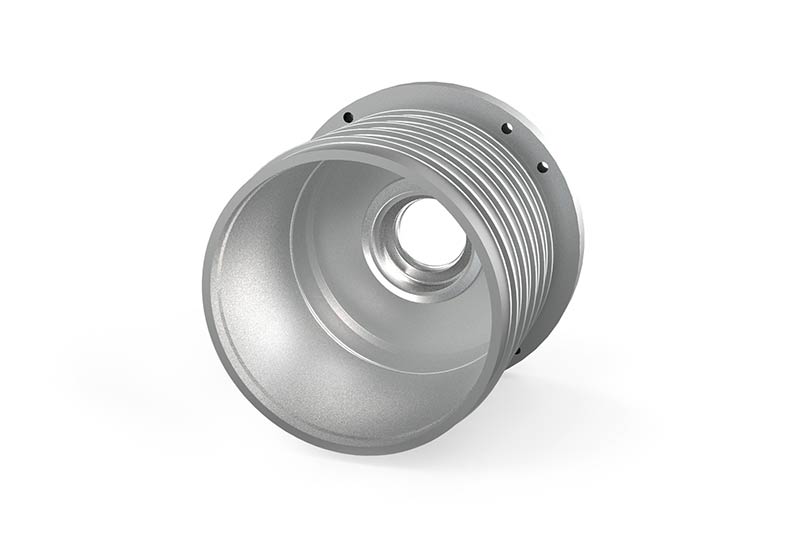
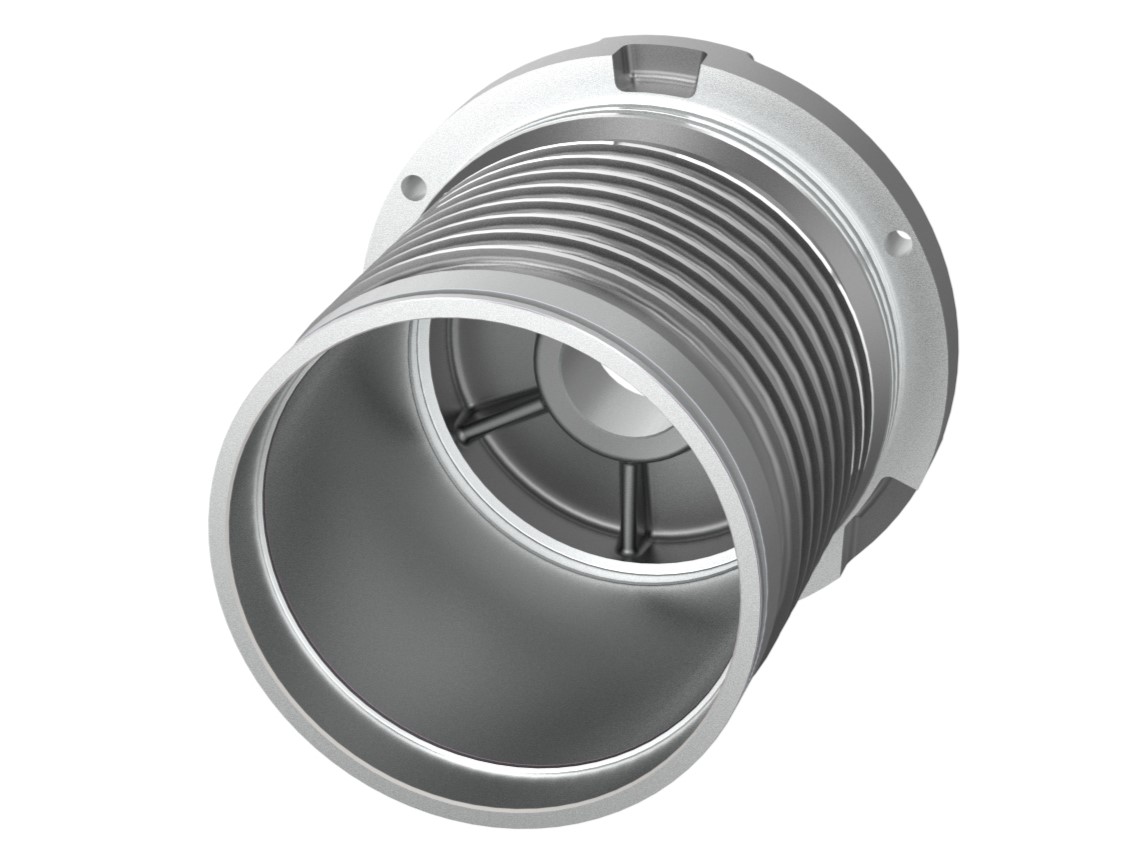
External machining of stator housings for electric motors is a demanding task. These housings, which often come in tubular or pot-shaped designs, are crucial for the efficiency of the electric motor. Several challenges have to be overcome during the process. The thin-walled aluminium housings with integrated ribs for the cooling circuit require the highest precision in terms of diameter accuracy, shape and position tolerances. The concentricity between different diameters is of huge importance.

Pre-machining
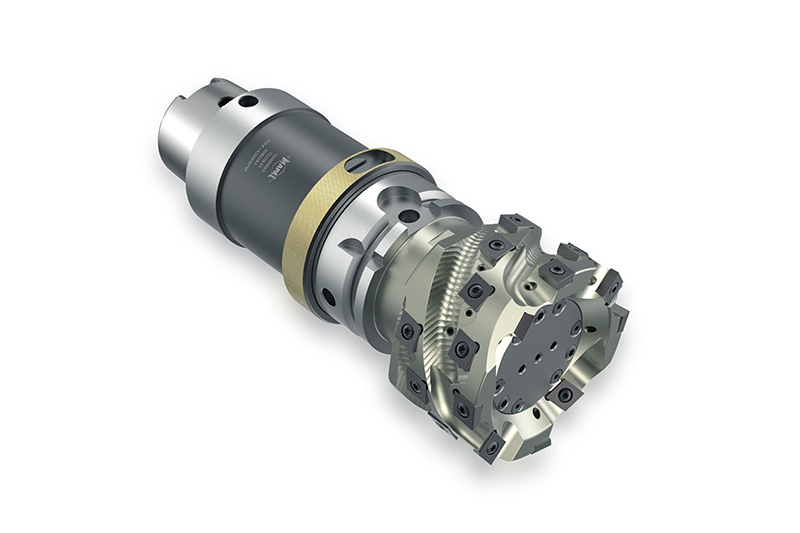
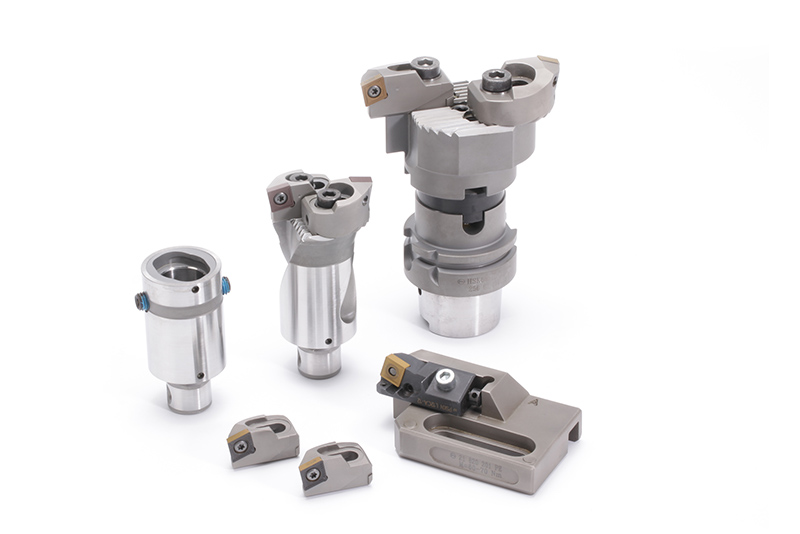
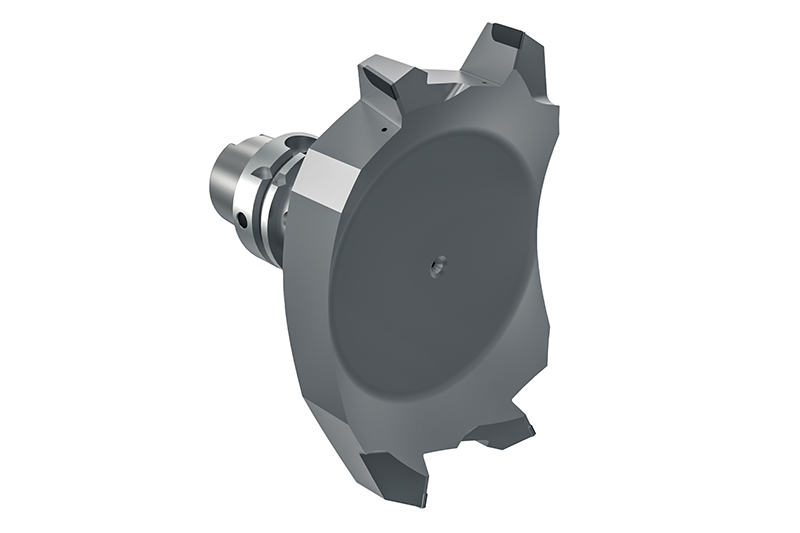
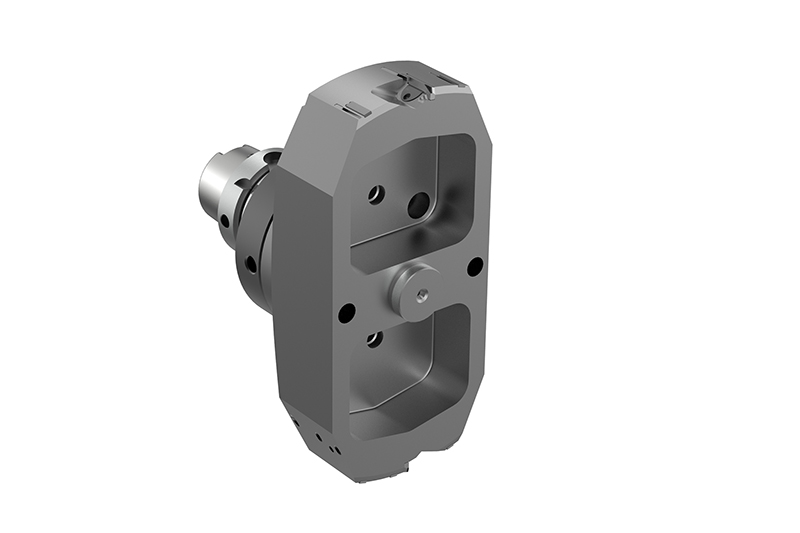
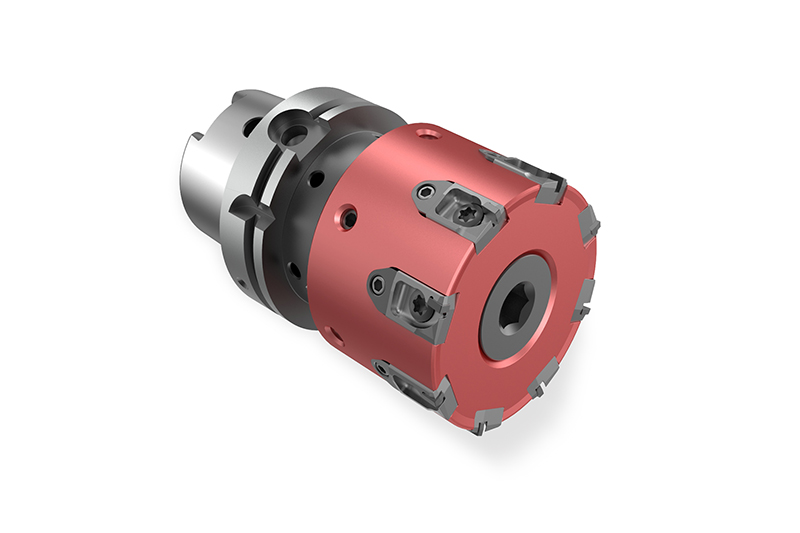
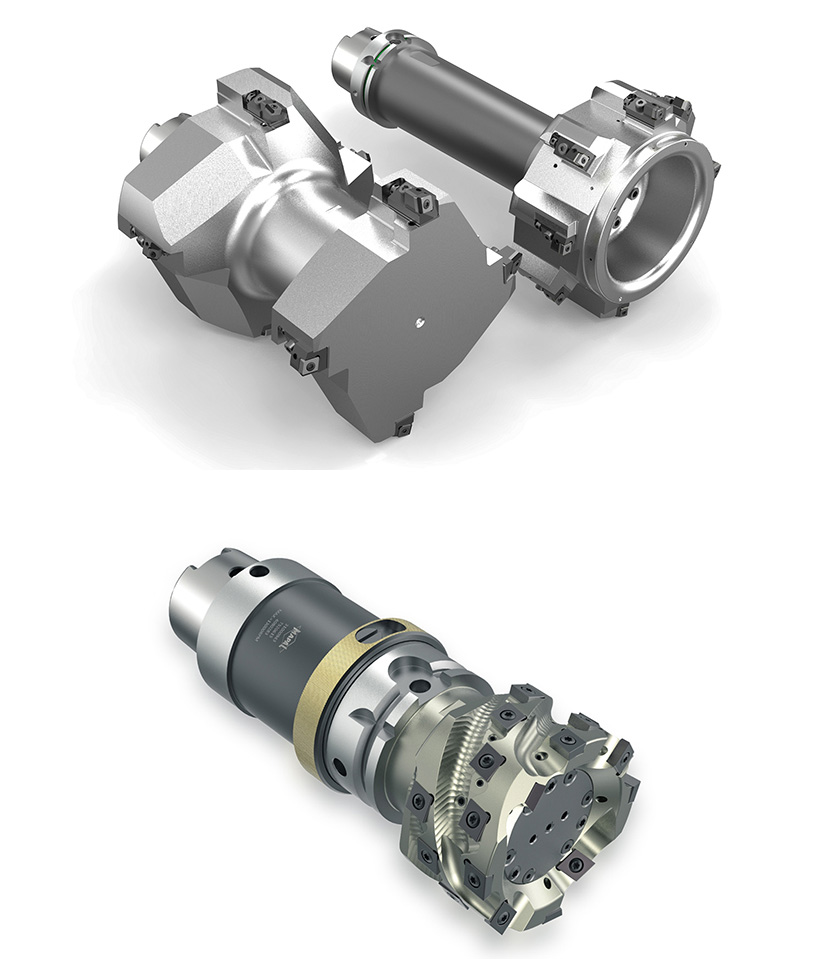
  • Helixfräser mit ISO-Wendeschneidplatten

    Helix milling cutter with ISO indexable inserts

    Roughing of outer diameter and surface

    • Coated ISO indexable inserts made of carbide or PCD-tipped indexable inserts
    • Reduced cutting forces
    • Standard product
    • HSK extension for different machining depths

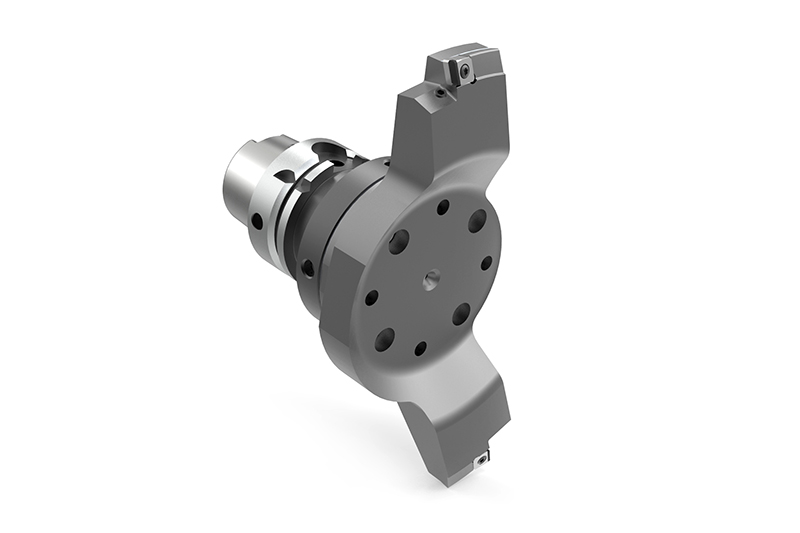
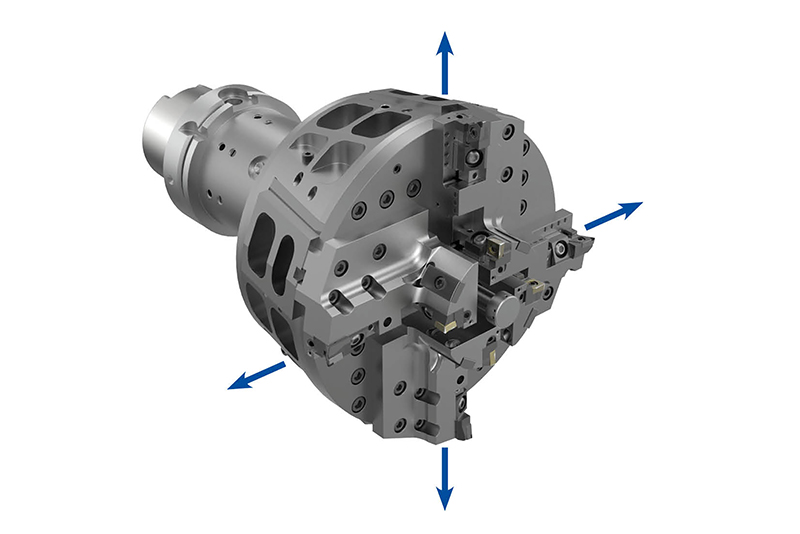
  • ISO BORING TOOL Roughing of outer diameter

    ISO boring tool

    Roughing of outer diameter

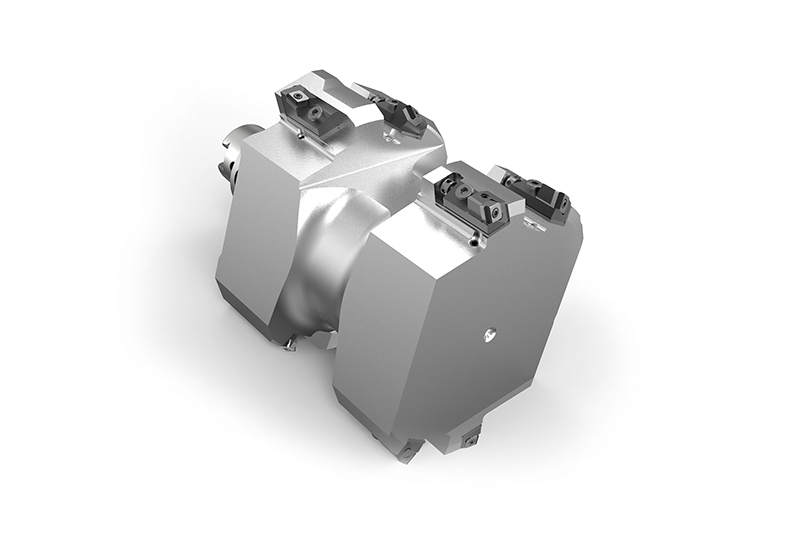
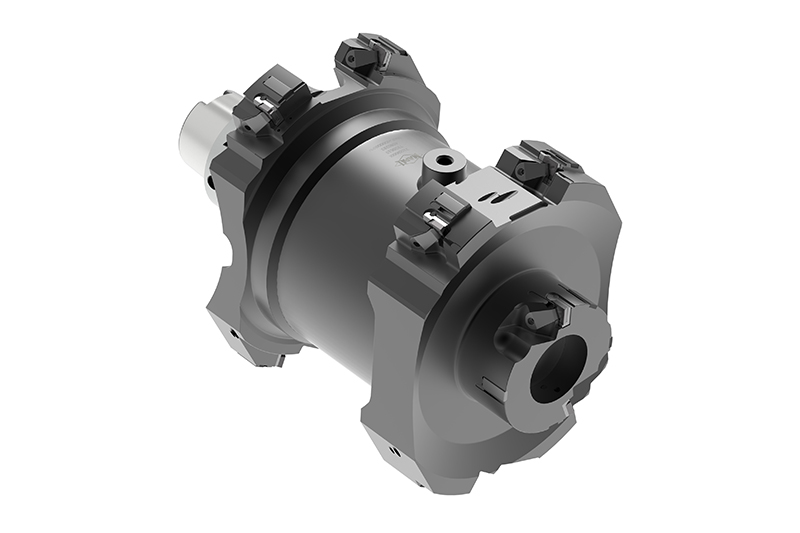
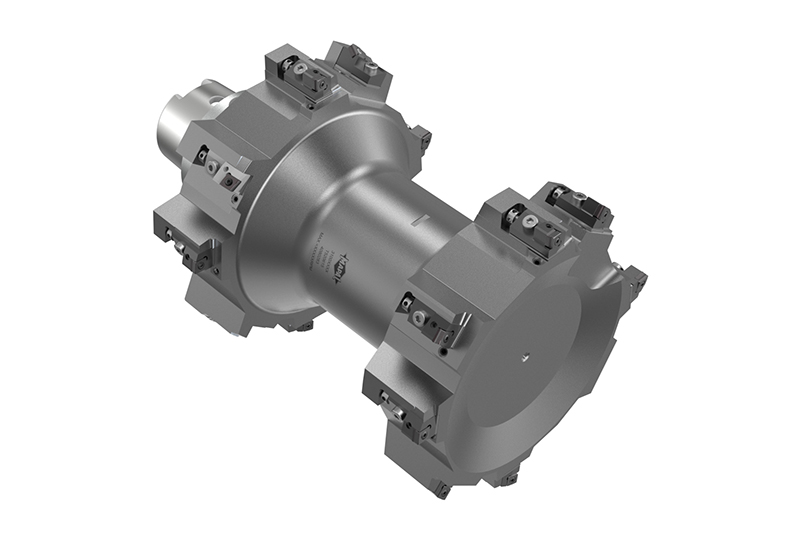
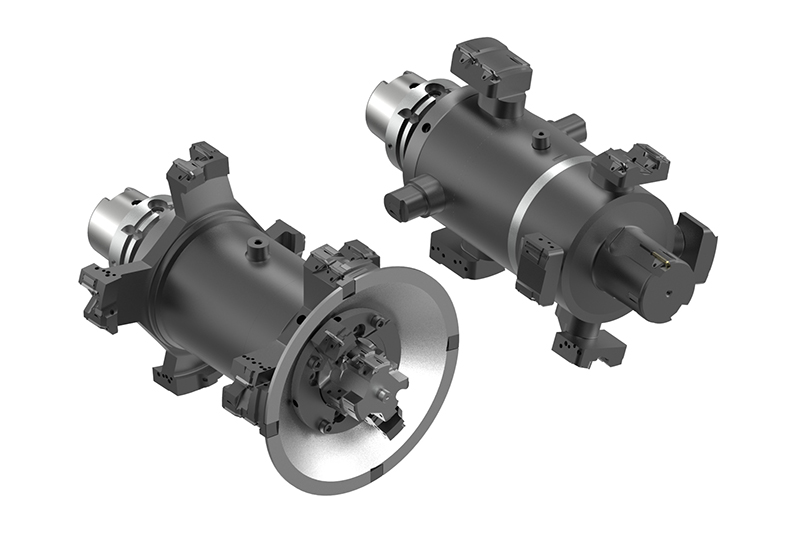
    • Multi-stage bell tool for external machining
    • ISO indexable inserts

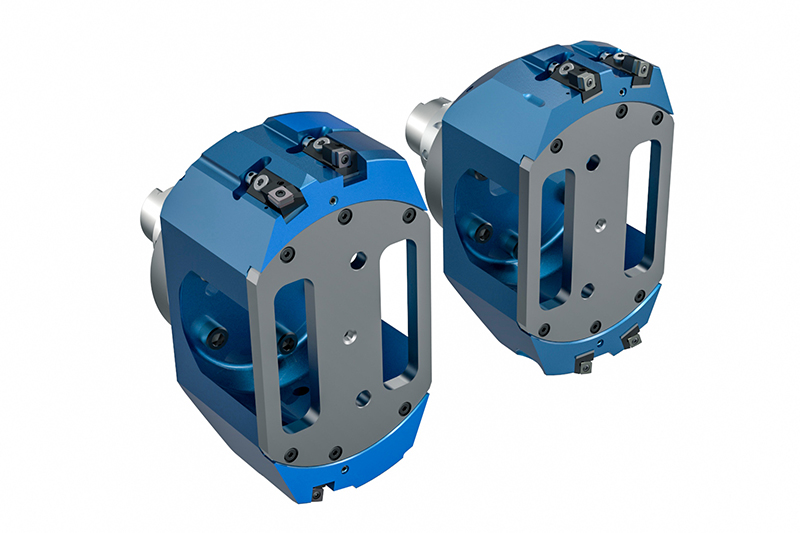
  • MILLING CUTTER WITH ISO INDEXABLE INSERTS

    Milling cutter with ISO indexable inserts

    Roughing the sealing groove

    • Coated ISO indexable inserts made of carbide
    • Optionally with vibration damper
    • Effective roughing of the sealing grooves

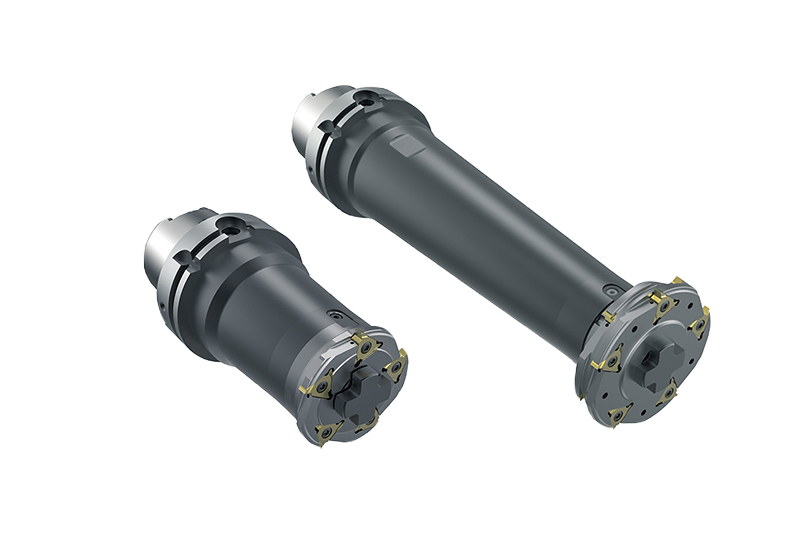
  • PCD MILLING CUTTER WITH SPECIAL CONTOUR

    Fresas PCD con contorno especial

    Acabado de las ranuras de sellado 

    • Corte de forma PCD 
    • Geometría perfecta de los contornos individuales de las ranuras 
    • Opcionalmente con amortiguador de vibraciones 
    • Mecanizado de acabado de todas las inserciones en un solo corte 

  • PCD MILLING CUTTER WITH SPECIAL CONTOUR Finishing the sealing groove

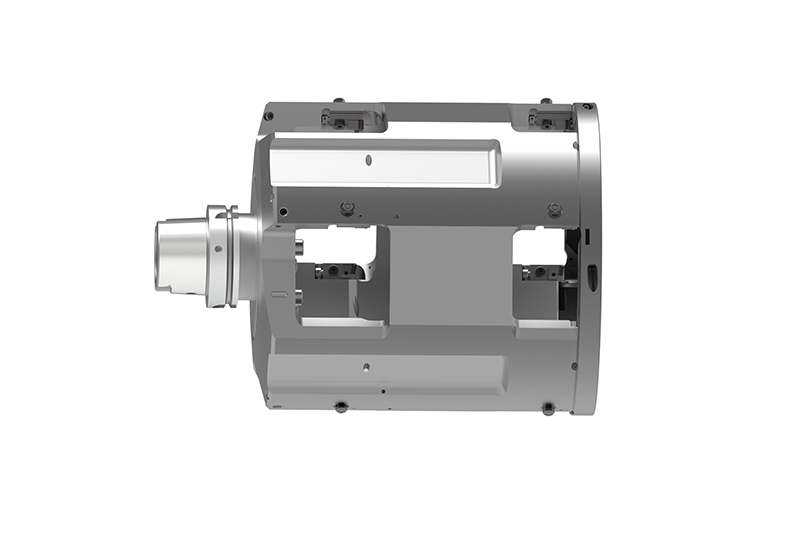
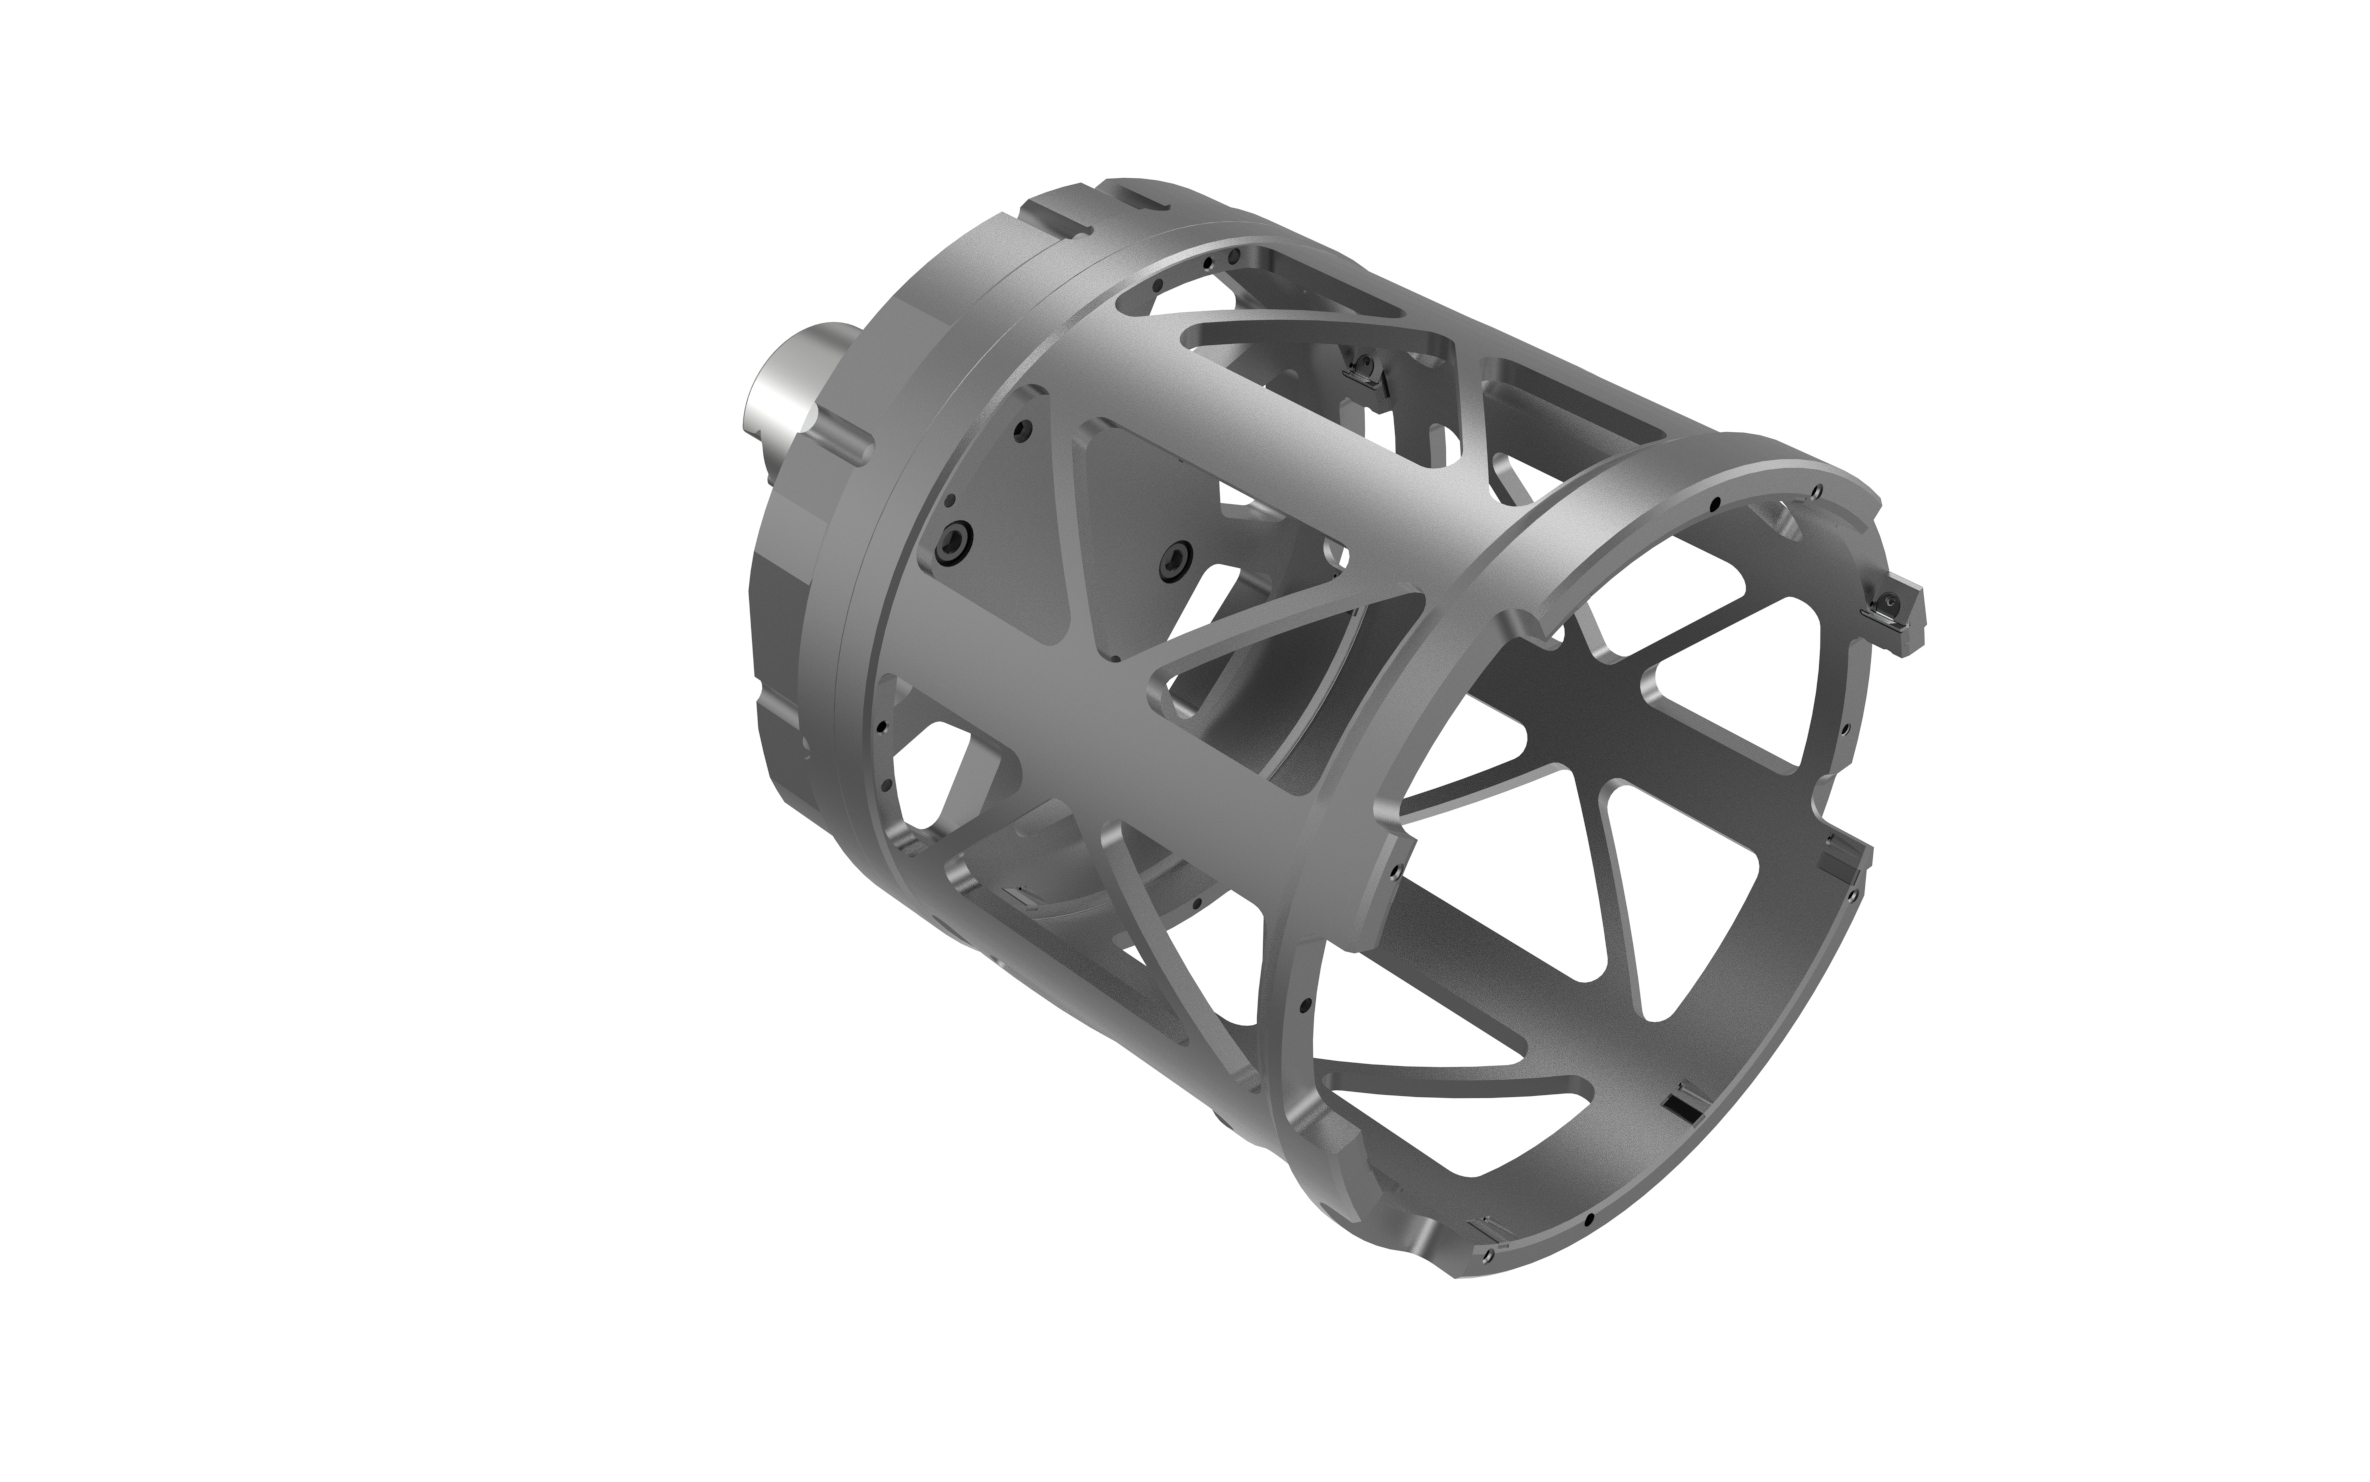
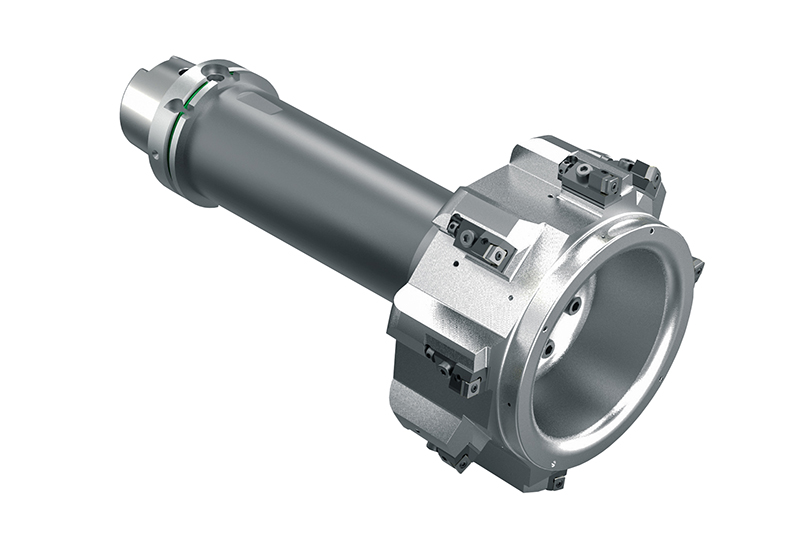
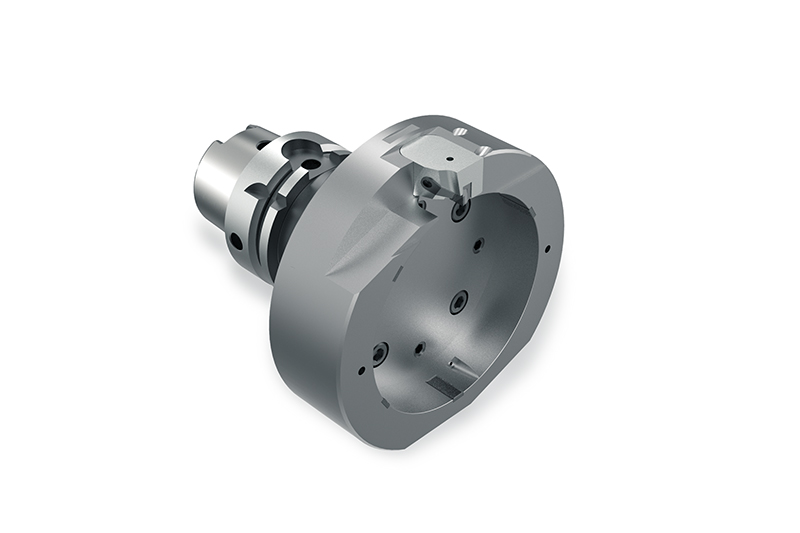
    Herramienta de taladrado de precisión en construcción ligera

    Acabado del diámetro exterior 

    • Insertos de PCD ajustables 
    • Cuerpo de la herramienta en construcción ligera 
    • Diámetro de mecanizado hasta Ø 260 mm 


Soluciones de mecanizado para…

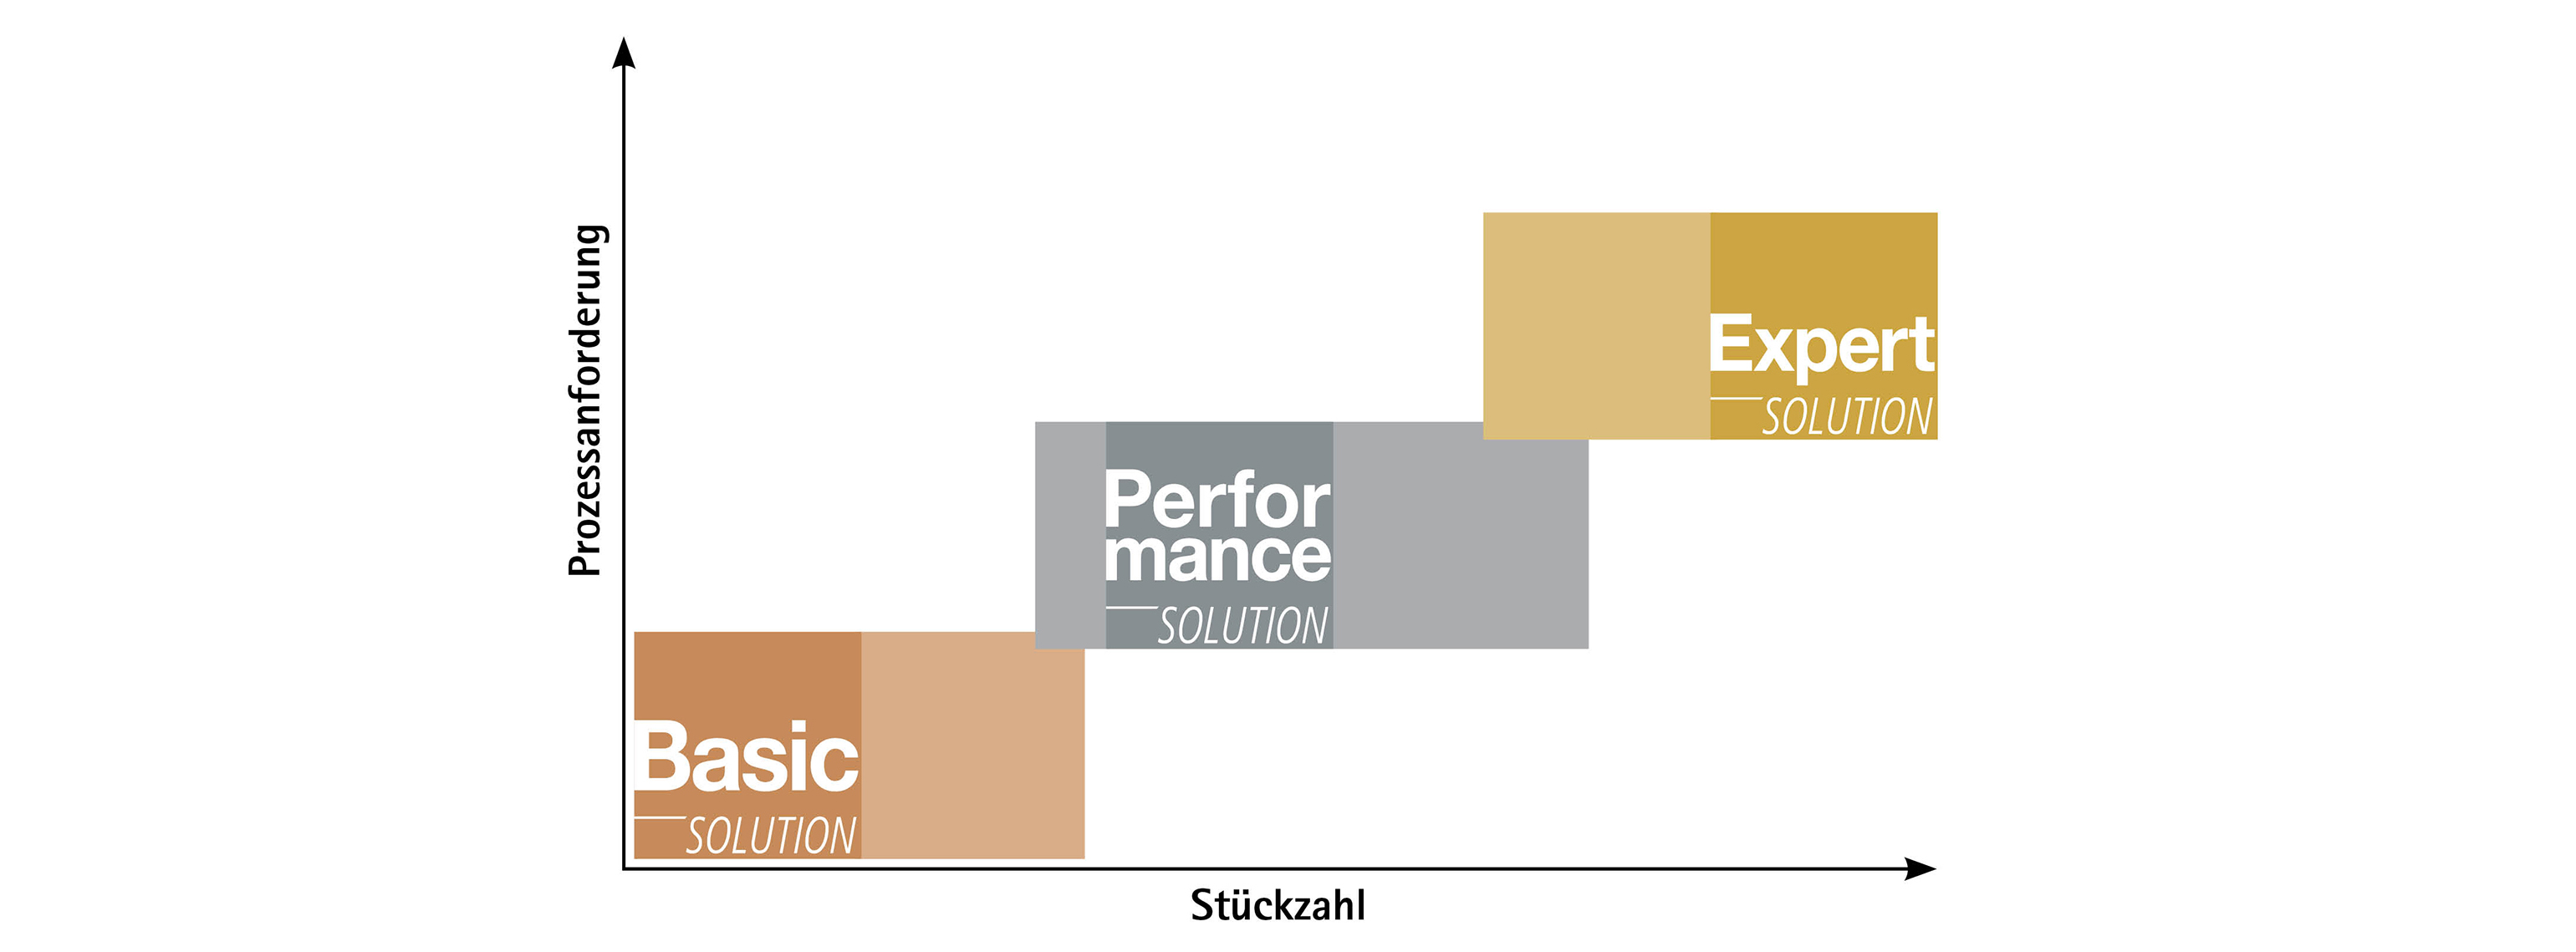
MAPAL Basic, Performance, Expert Line

Otras soluciones de mecanizado

  • Orificios de cojinete y posición

    Con la máxima concentricidad y circularidad

    Más información
  • Außenreibahle mit EA-System

    Escariador exterior con sistema EA

    • Mecanizado exterior del orificio de cojinete

  • Planfräser mit PKD-Fräseinsätzen

    Fresadora plana con fresas de PCD

    • Creación de perfiles de superficie definidos para superficies de junta y apoyo (por ejemplo estructuras con cortes cruzados)
    • Acabado de la superficie Rz < 1


Otros componentes electrificados