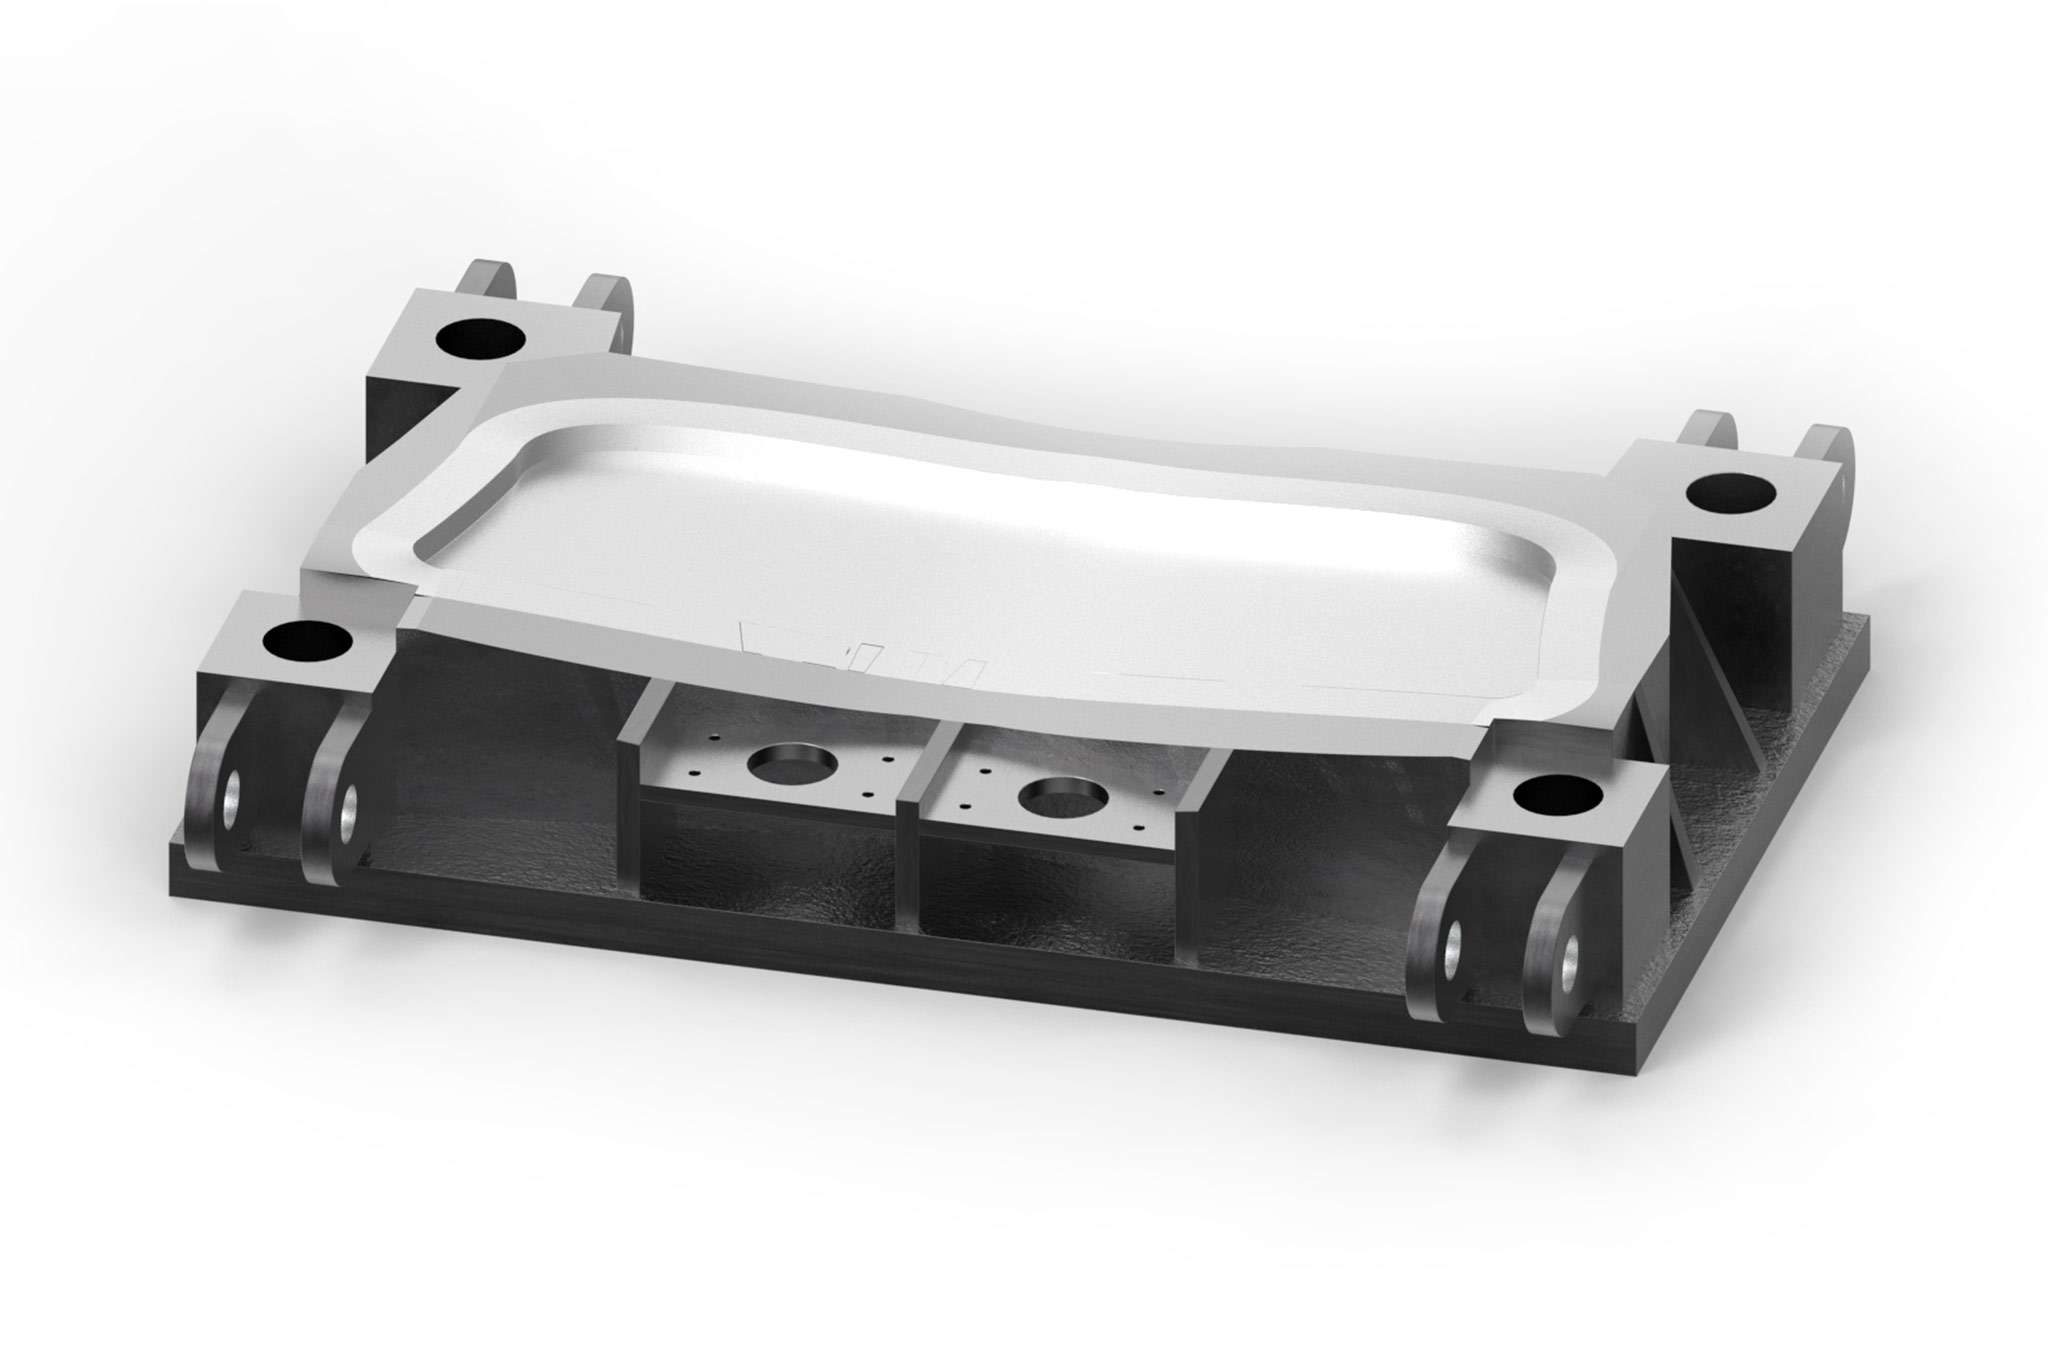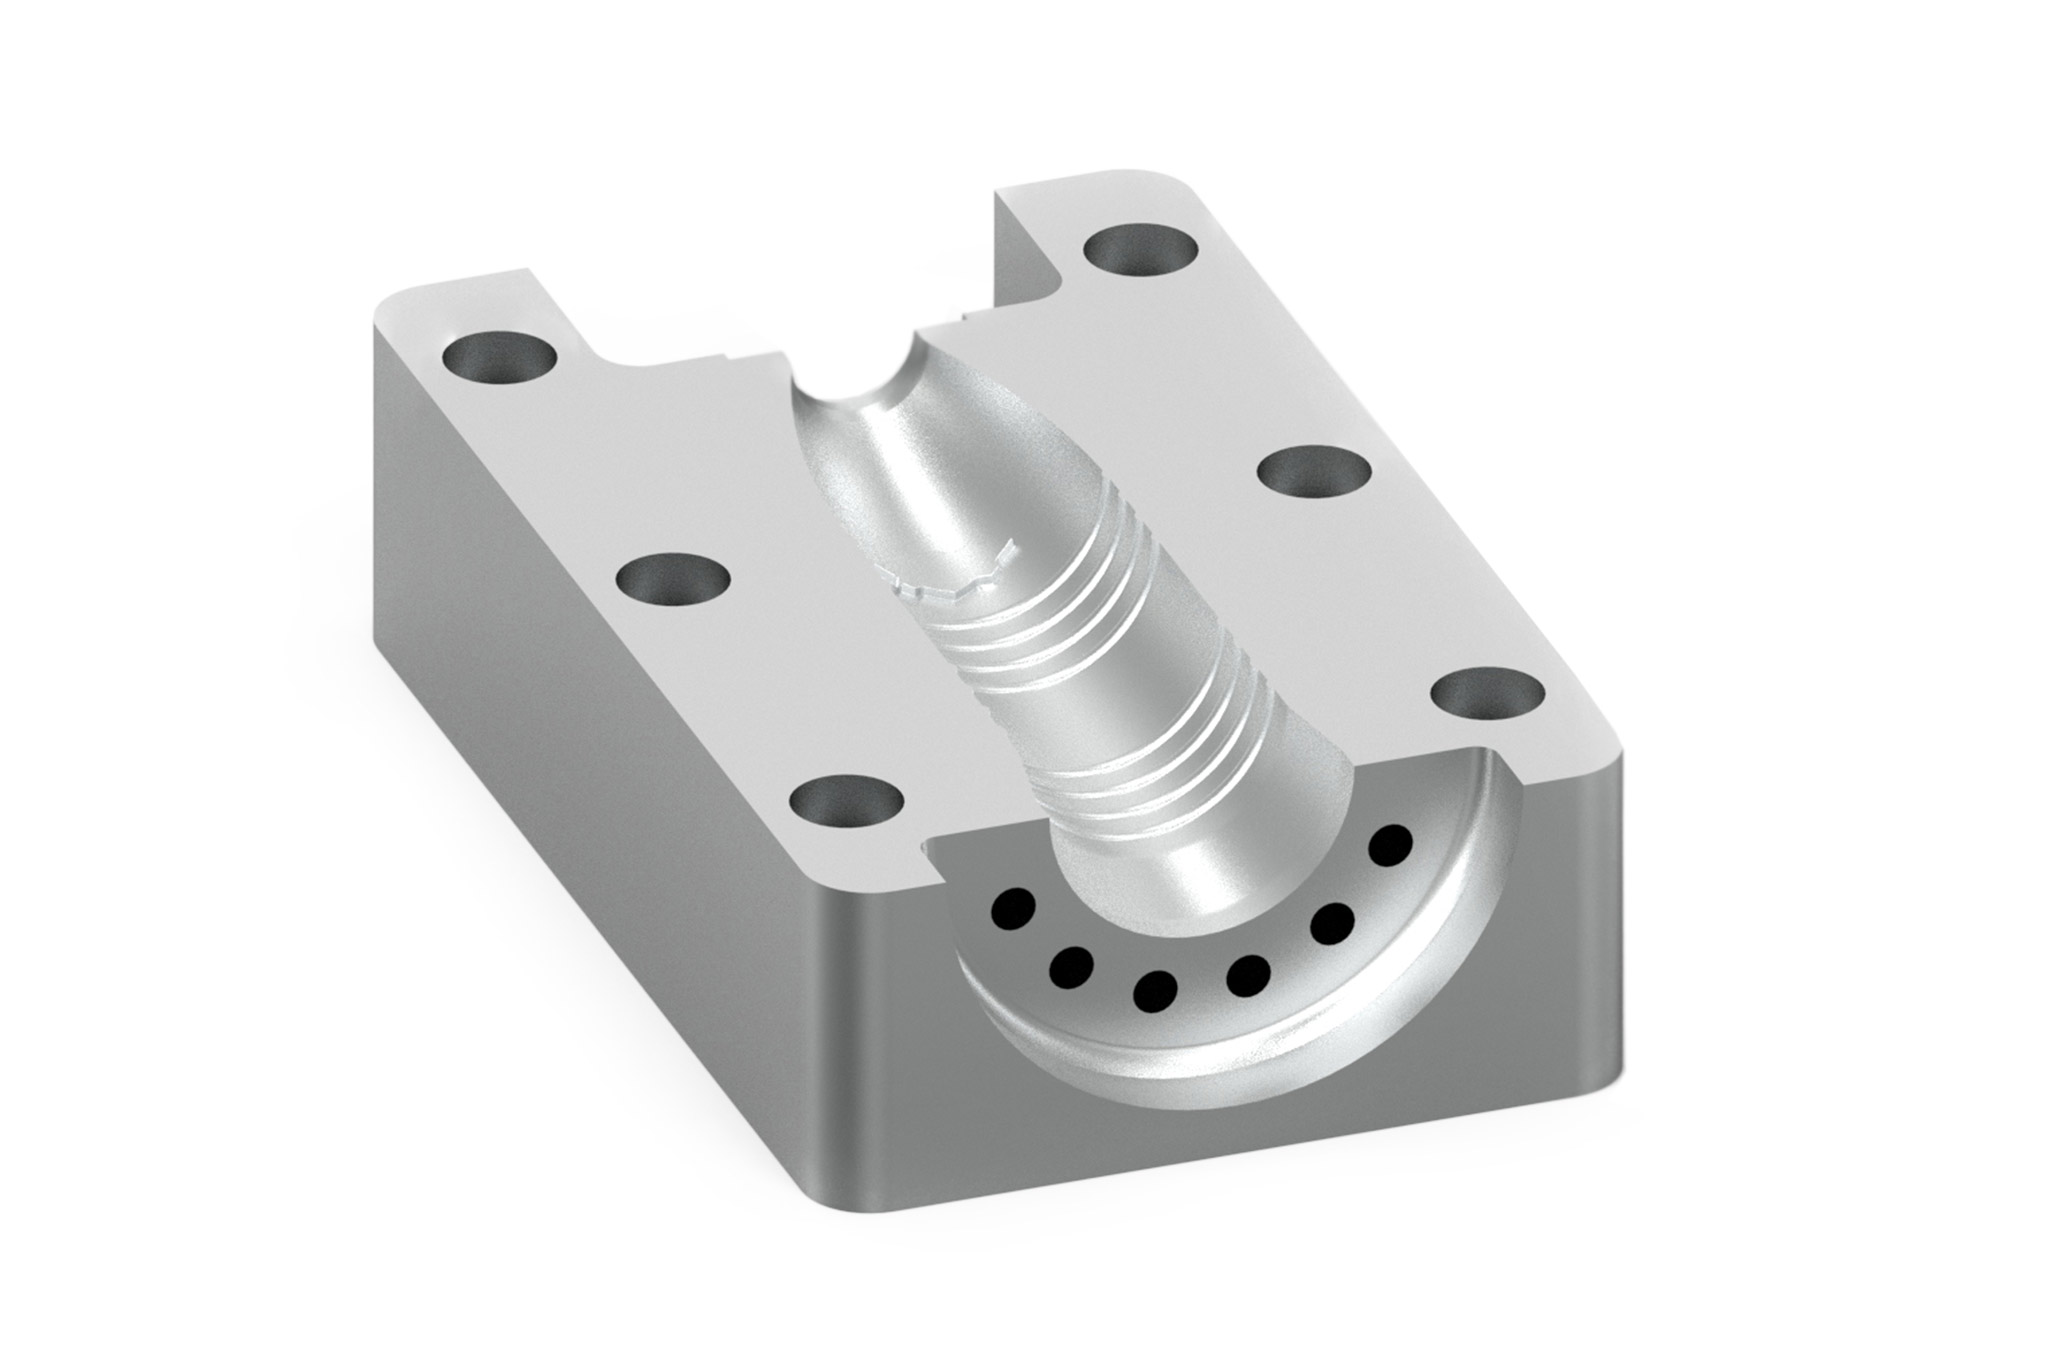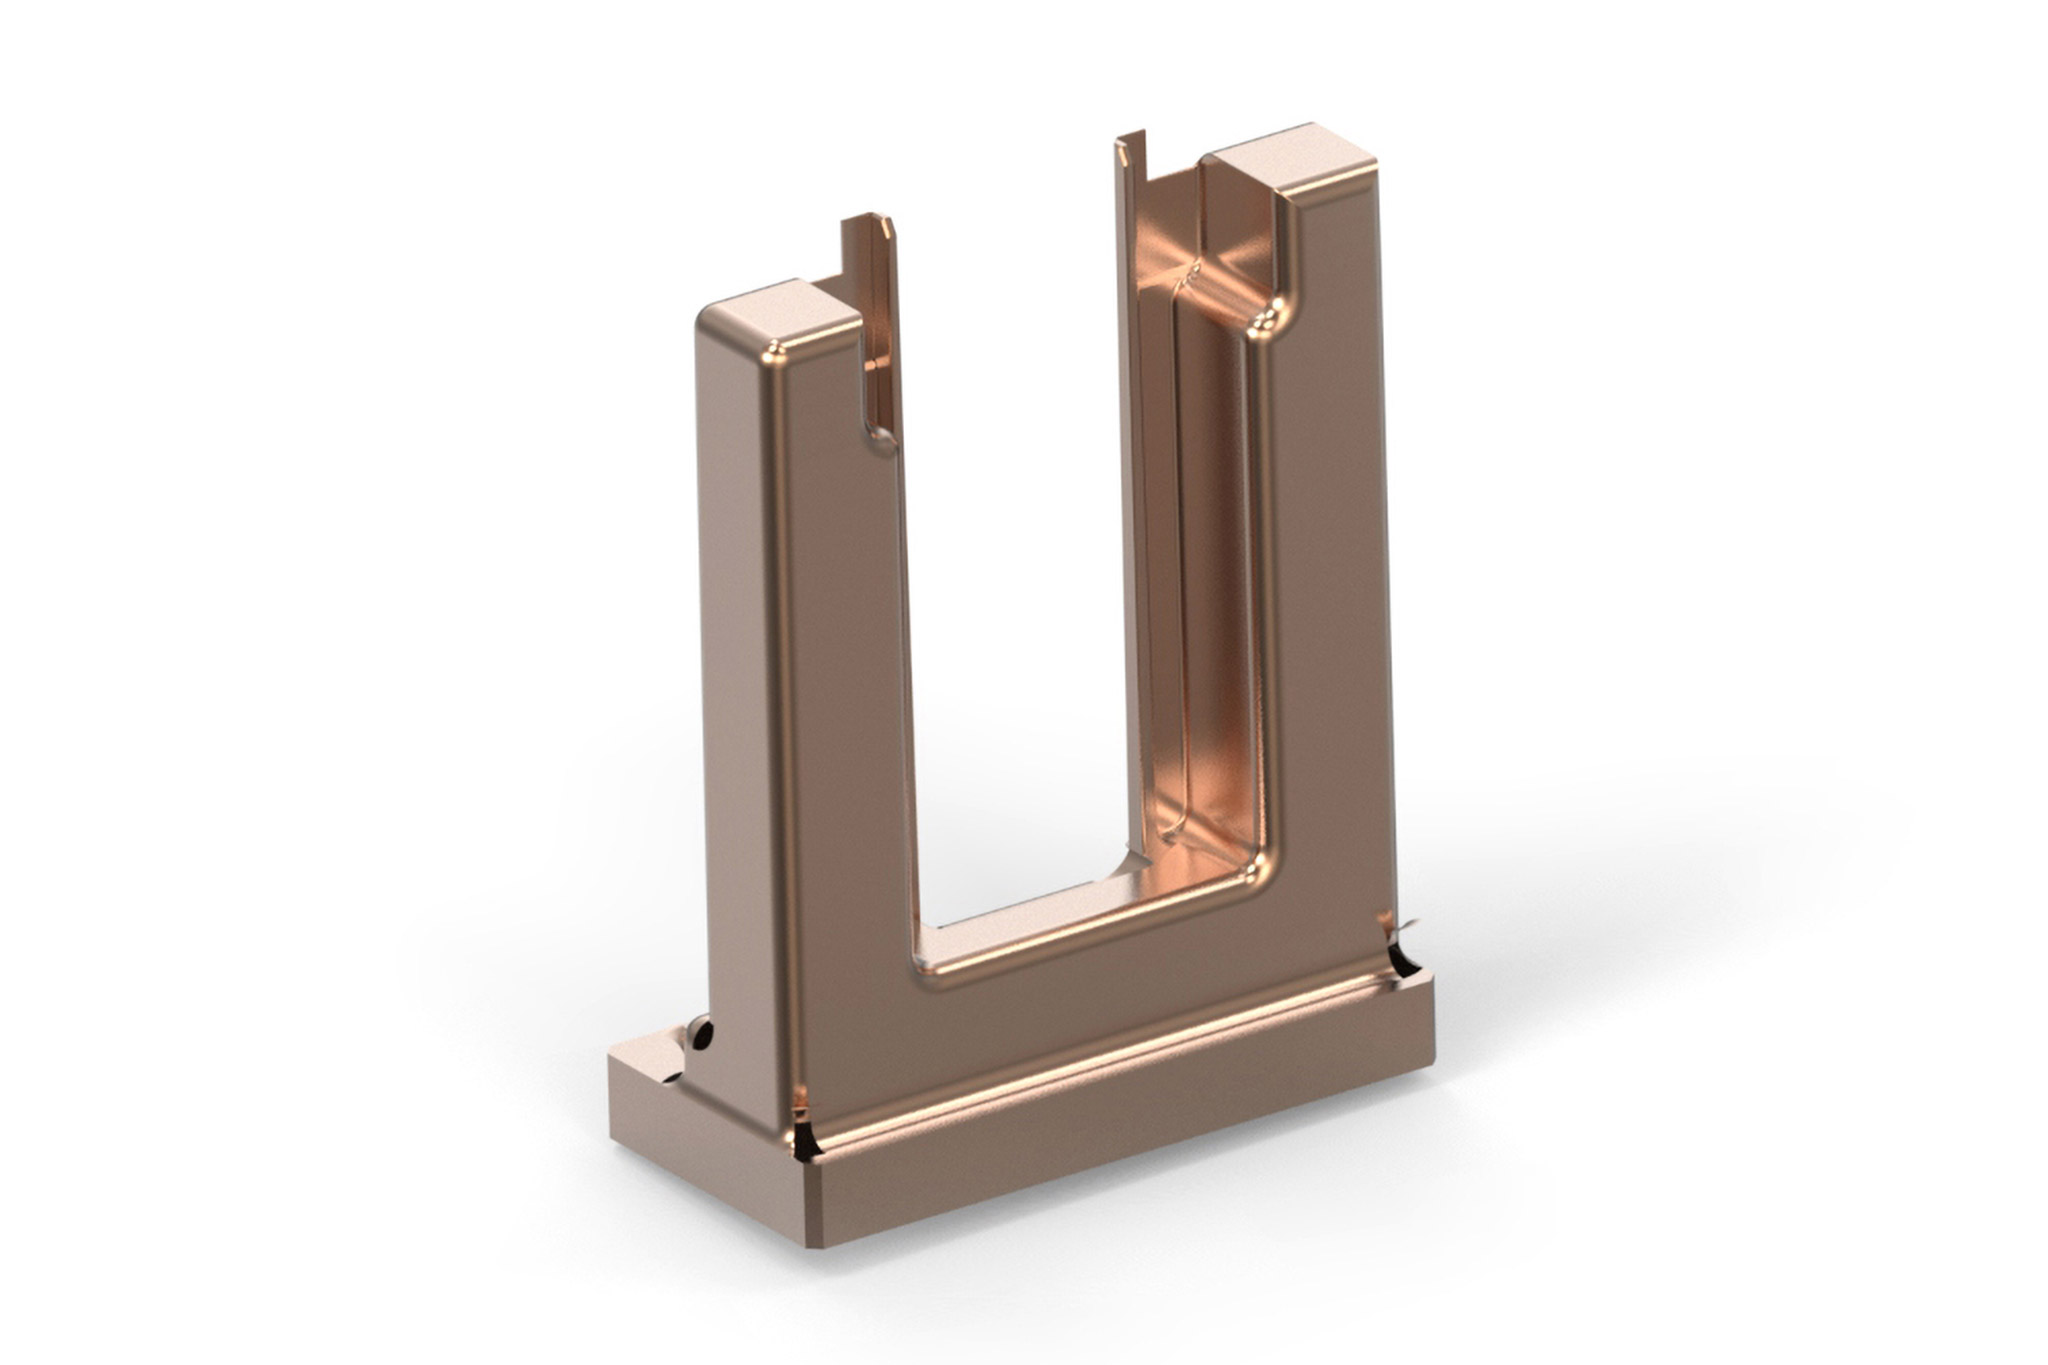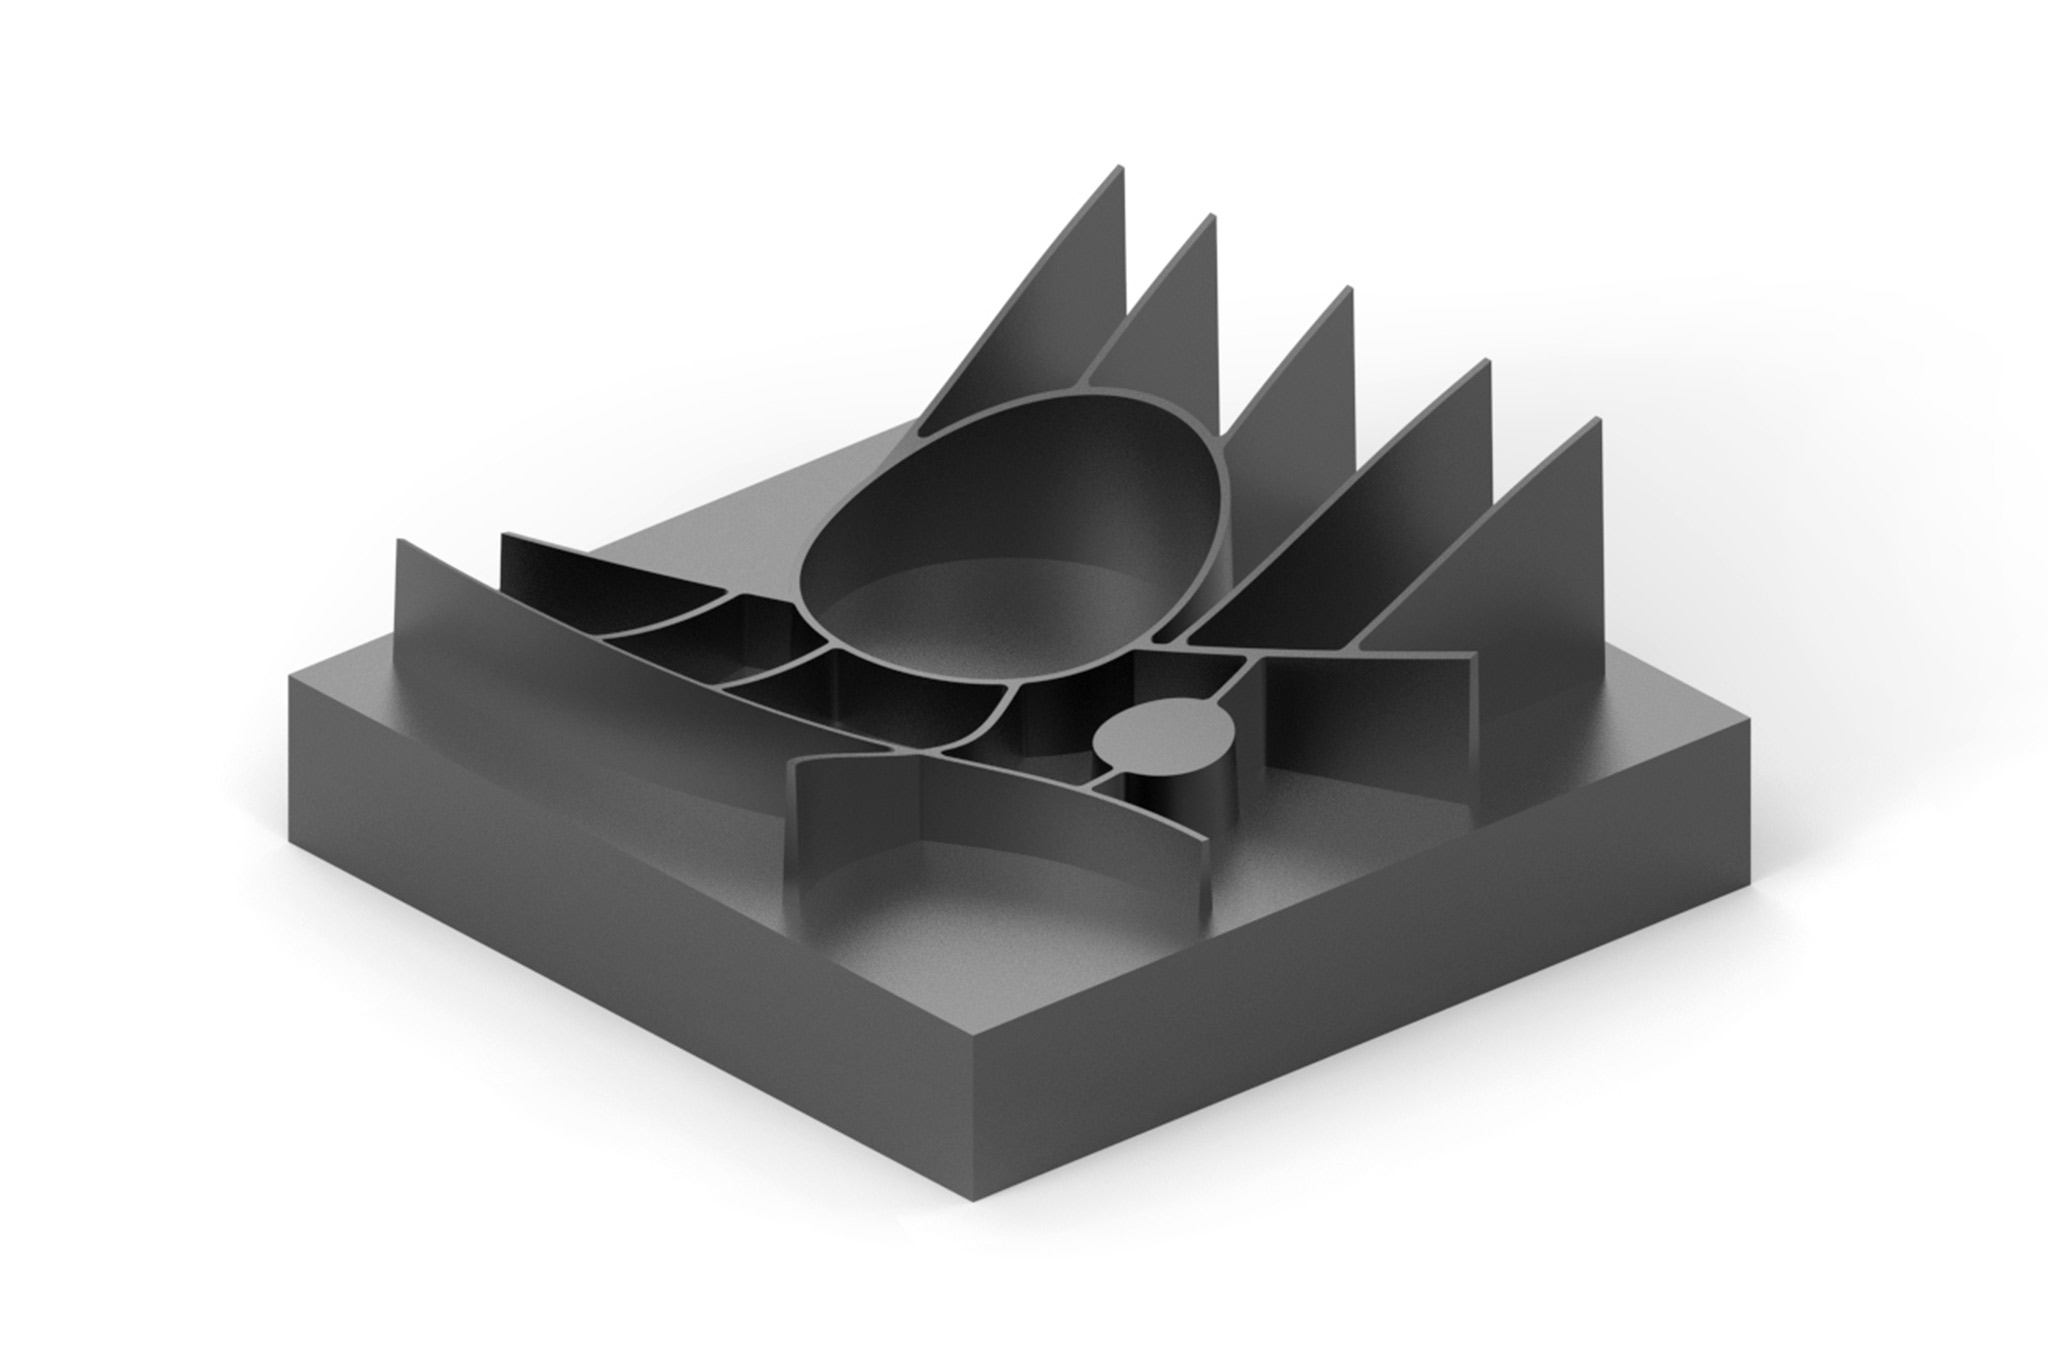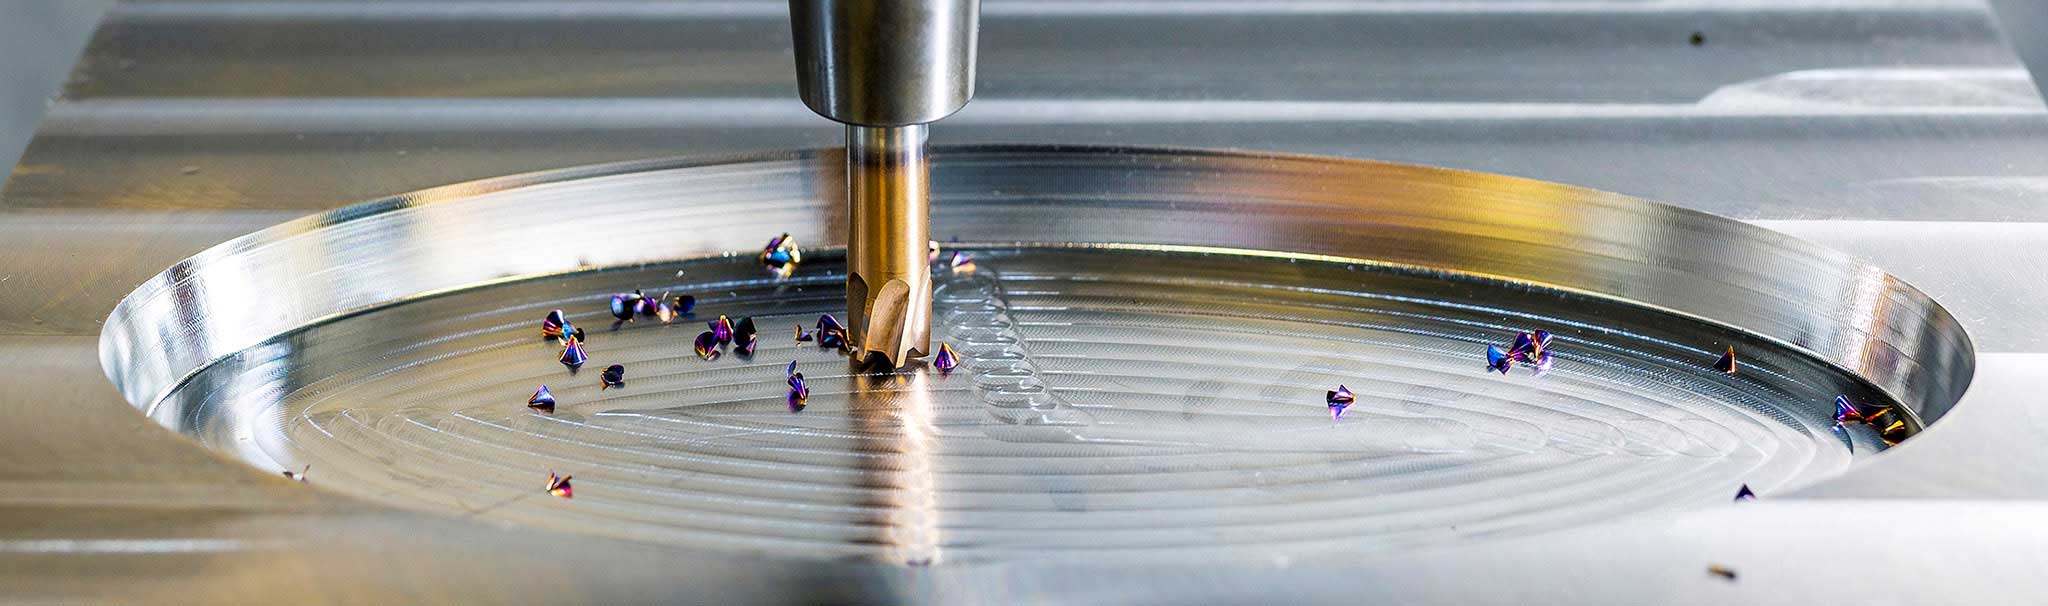
• MAPAL offers complete machining solutions for the die and mould industry.

Primi passi nel settore della costruzione di stampi e matrici

L’aspettativa dei costruttori di stampi e matrici è un alto livello di competenza di processo e di prodotto da parte del loro produttore di utensili da taglio. Questo perché la vita utile degli stampi da produrre e la precisione dei pezzi stampati sono enormemente importanti al fine della competitività nella produzione di massa. Gli utensili devono quindi garantire massima precisione, lunga durabilità e, soprattutto, sicurezza dei processi.
 

Questi sono gli aspetti che hanno determinato il successo di MAPAL in settori come l'industria automobilistica, l'ingegneria meccanica o l'industria aerospaziale. È quindi logico che il produttore di utensili di precisione offra anche soluzioni efficienti ed economiche per l'intero processo di lavorazione nella costruzione di stampi e matrici. Utensili ad alte prestazioni versatili e precisi, nonché portautensili specifici con contorni sottili e concentricità precisa minimizzano il lavoro di lucidatura e rilavorazione, assicurando una qualità di superficie costante durante il processo di fresatura. Essi consentono inoltre notevoli risparmi sui costi dell’intero processo.

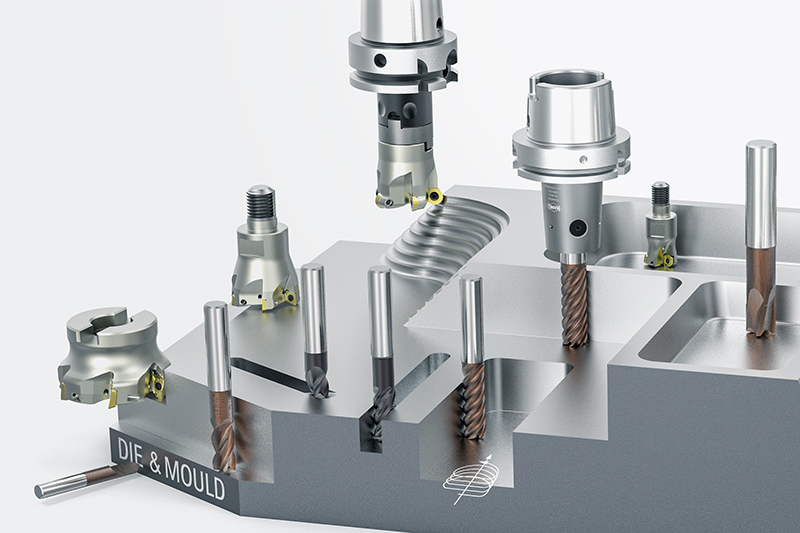
Assortimento di utensili per la costruzione di stampi
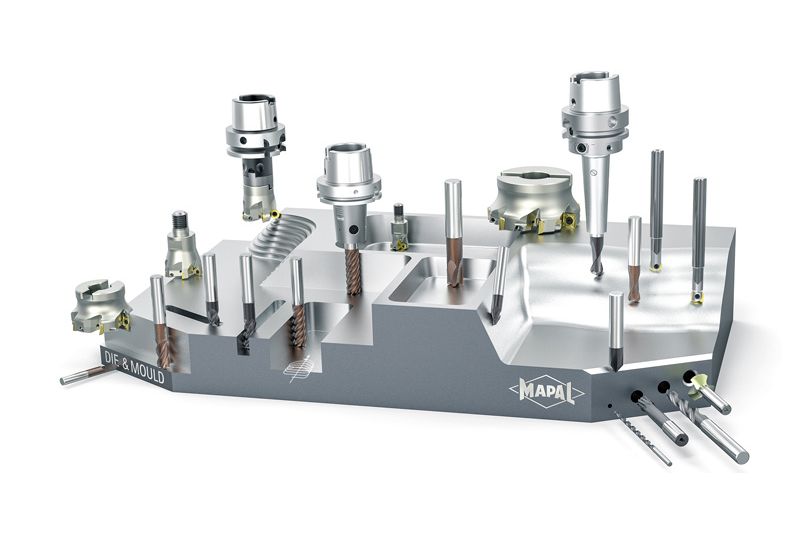
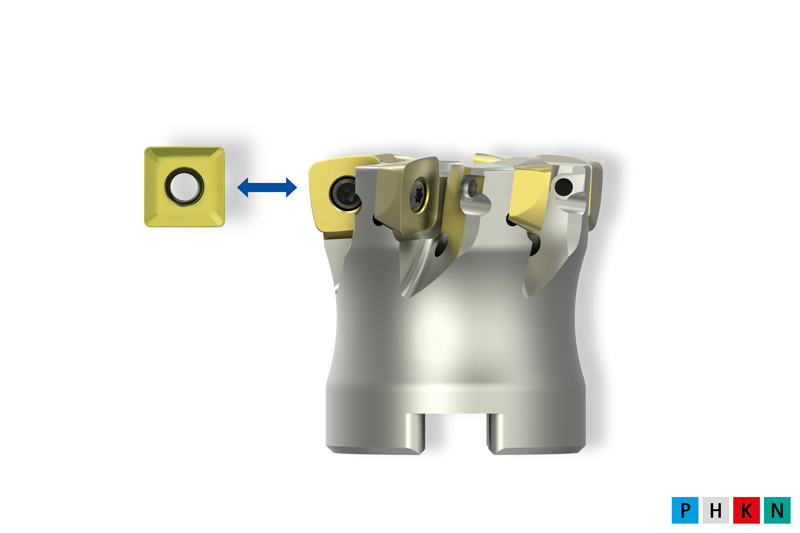
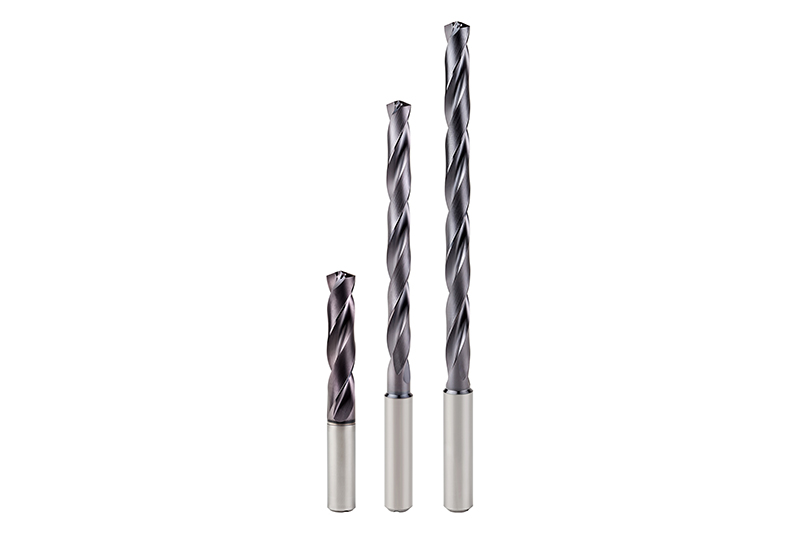
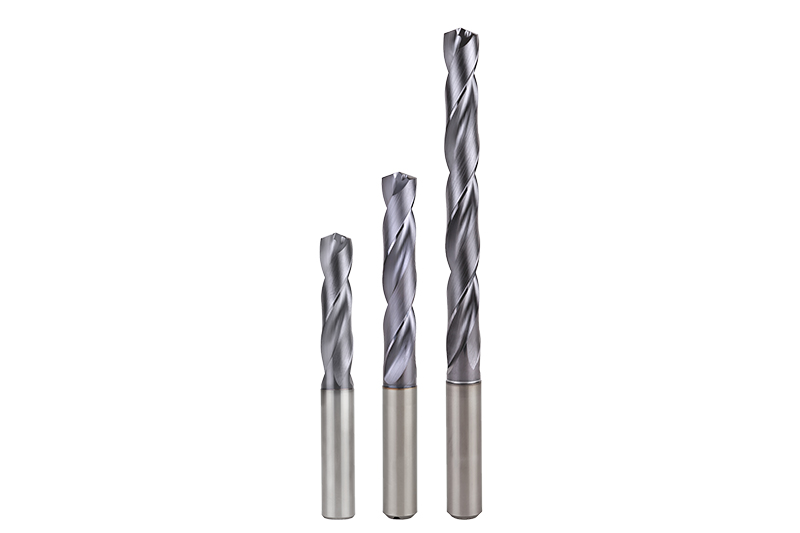
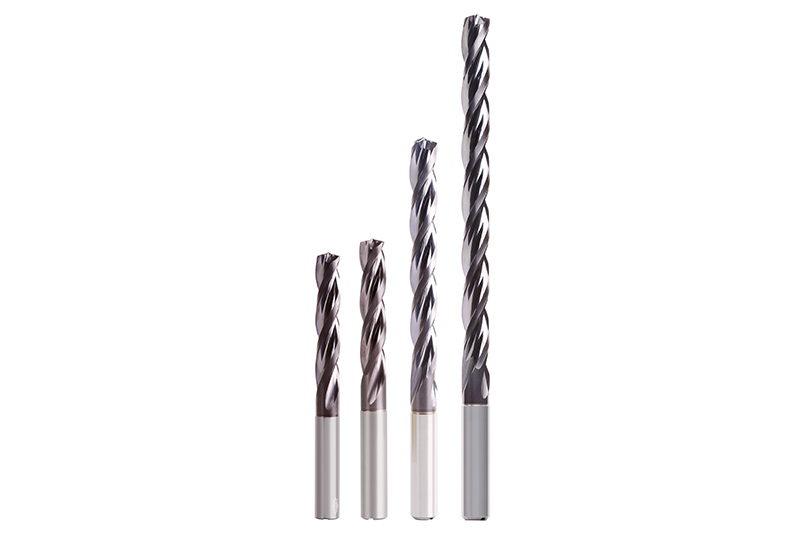
The picture shows the MAPAL tool range for mould making

Frese in metallo duro integrale
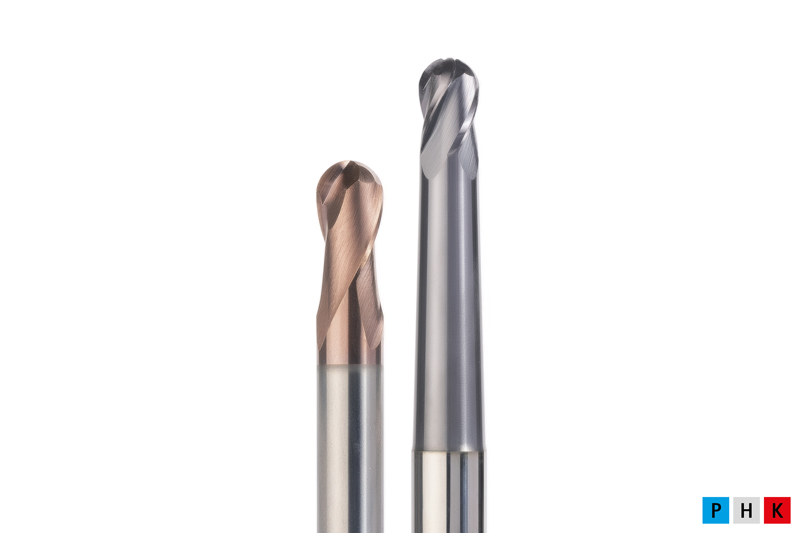
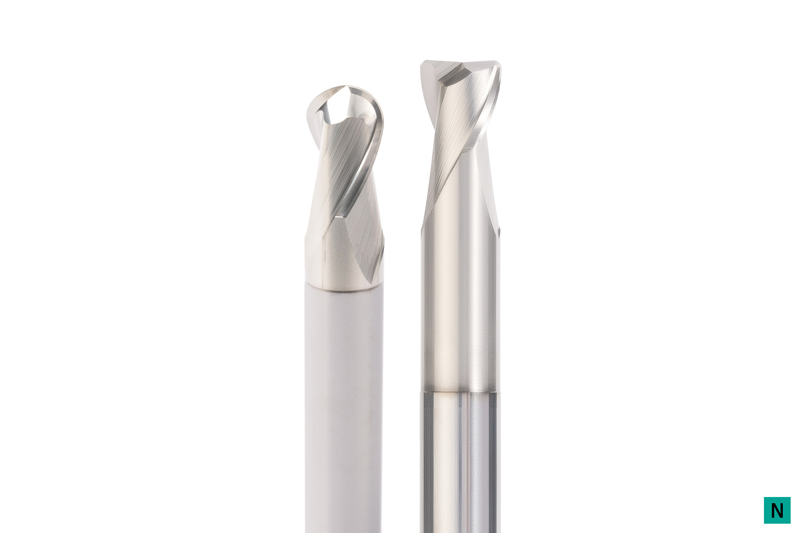
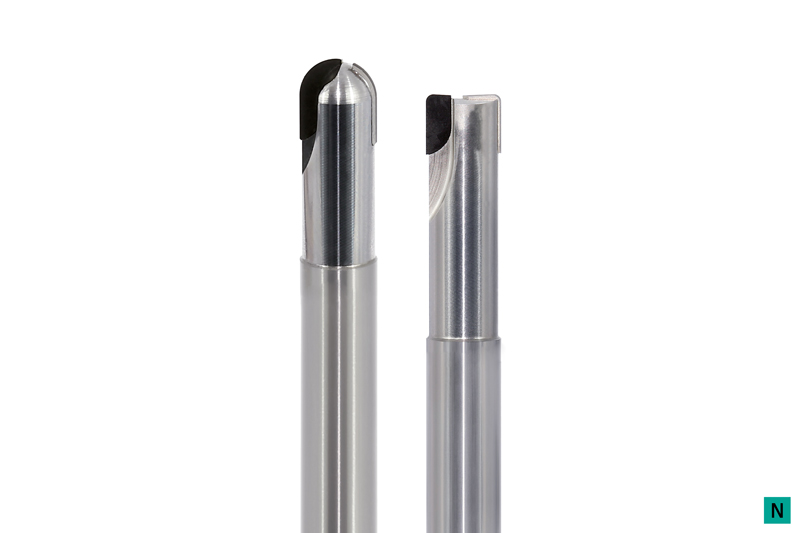
  • OptiMill-3D-BN

    Ball nose milling cutter
    • High-precision machining of 3D contours
    • ø range: 0.10 - 20.00 mm

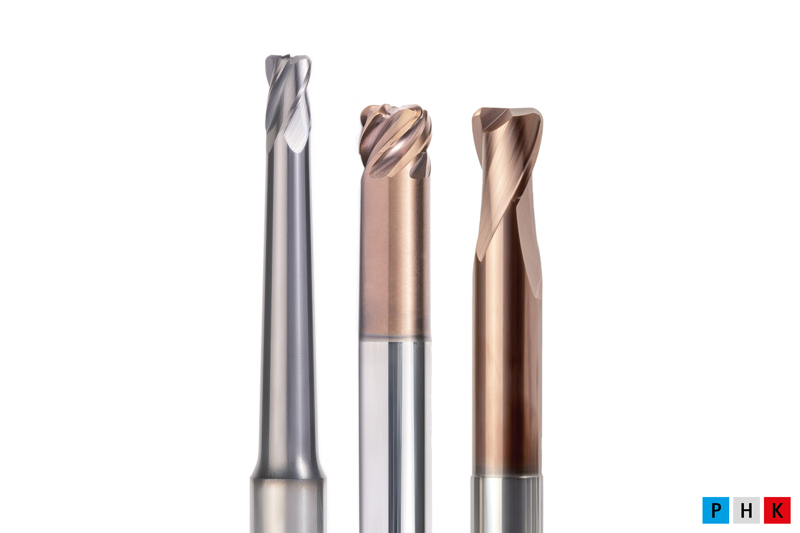
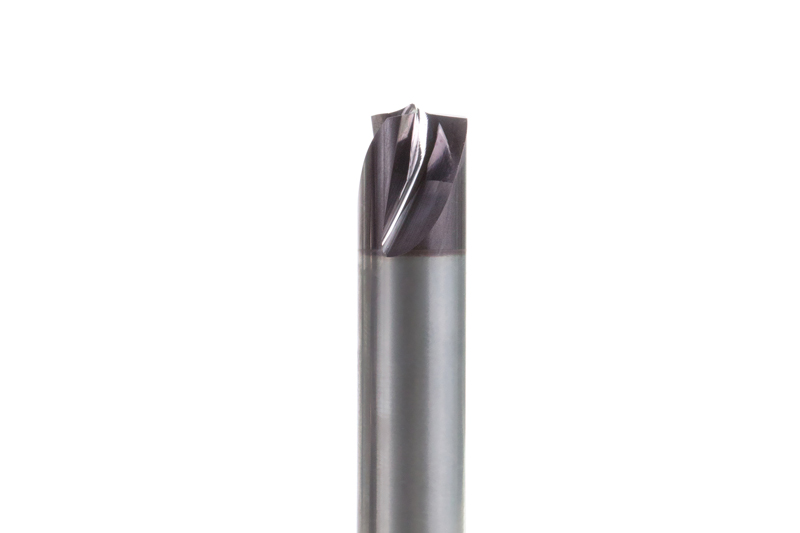
  • OptiMill-3D-CR

    Corner radius milling cutter
    • Milling with a very precise corner radius
    • ø range: 0.10 - 20.00 mm

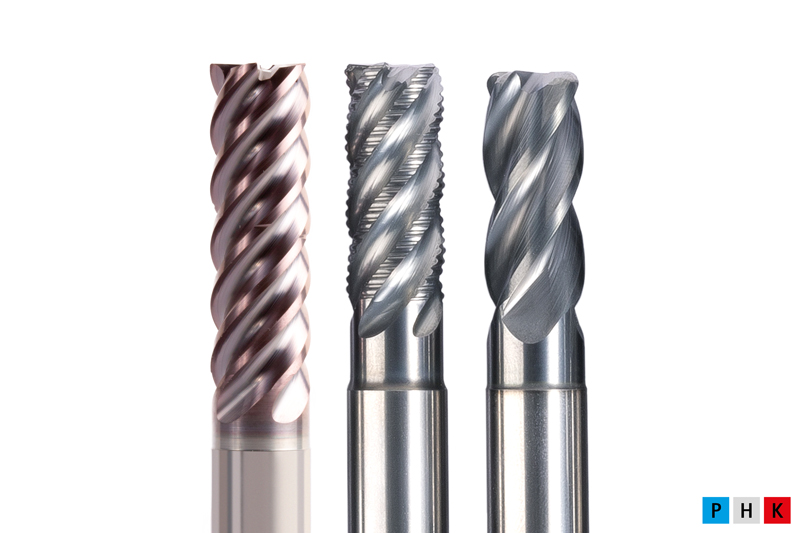
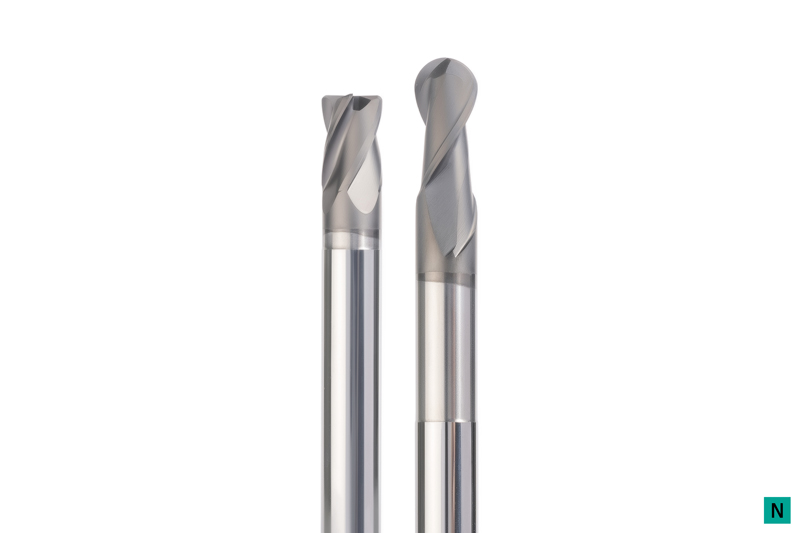
  • OptiMill Shoulder milling cutter

    Shoulder milling cutter
    • Ideal for roughing, finishing, trochoidal milling and milling pockets
    • ø range: 2.00 - 12.00 mm

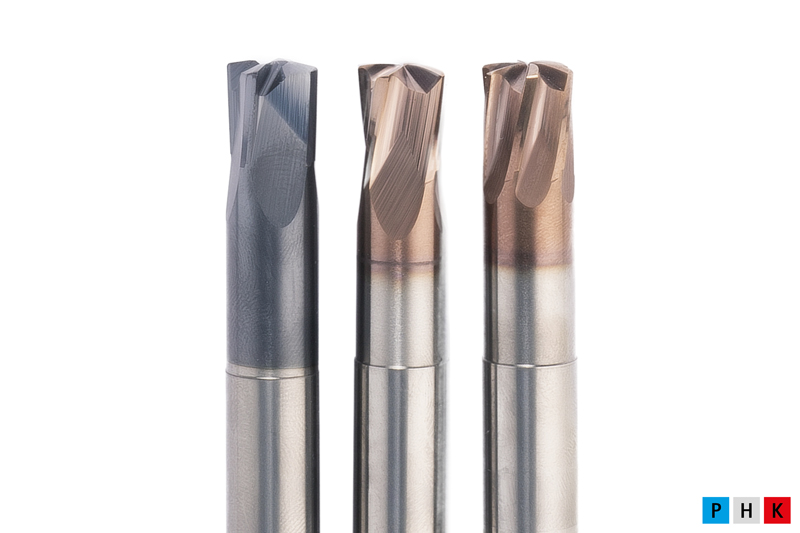
  • OptiMill-3D-HF

    Frez do wysokich posuwów
    • Idealny do obróbki z wysokimi posuwami, zapewniający dużą wydajność skrawania przy wysokim bezpieczeństwie procesu
    • Zakres ø: 2,00 - 16,00 mm

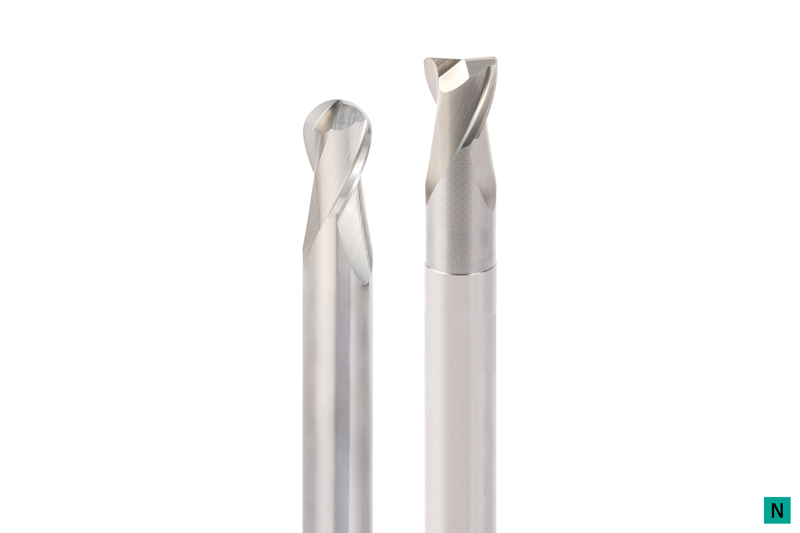
  • OptiMill-3D-Alu

    Frezy kuliste i narożne

    • Wysokoprecyzyjna obróbka konturów 3D
    • Zakres ø: 1,00 - 20,00 mm

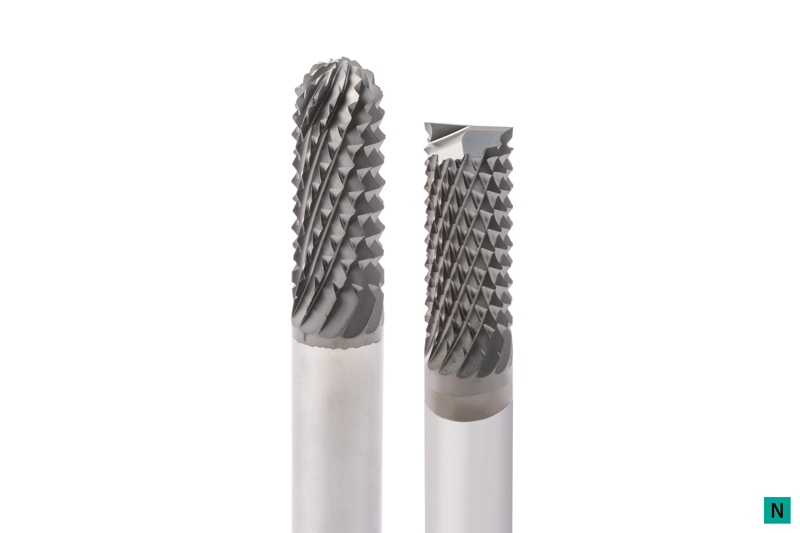
  • OptiMill-Graphite-MT

    Frez kulisty i frez walcowo-czołowy
    • Frezy wieloostrzowe do obróbki zgrubnej, zapewniające wysoką wydajność skrawania przy obróbce elektrod grafitowych
    • Zakres ø: 3,00–16,00 mm

  • OptiMill-3D-Graphite

    Frezy kuliste i narożne
    • Nadają się do obróbki elektrod grafitowych
    • Różne wersje wykonania w zależności od sytuacji obróbczej
    • Zakres ø: 0,20–12,00 mm

  • OptiMill-3D-Copper

    Frezy kuliste i narożne
    • Specjalna geometria do obróbki elektrod miedzianych i twardych stopów metali nieżelaznych
    • Zakres ø: 0,10–20,00 mm

  • OptiMill-Diamond

    Frezy kuliste, narożne i frez walcowo-czołowy
    • Ostrza PKD zapewniające długą żywotność
    • Zakres ø: 3,00 - 12,00 mm

Frezy z płytkami skrawającymi
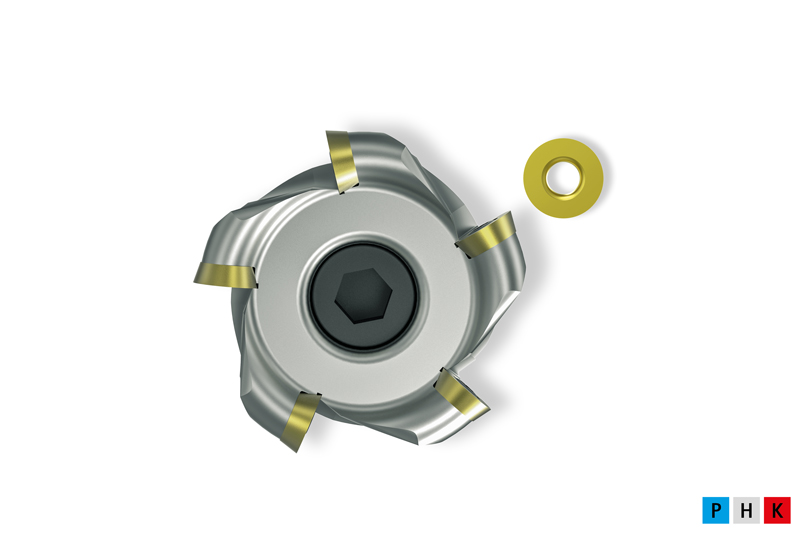
  • NeoMill-ISO-360

    Milling cutter with round inserts
    • Perfect for roughing and pre-finishing
    • ø range: 10.00 - 160.00 mm

  • NeoMill-3D-Finish

    Finishing milling cutter
    • Perfect for finishing 90° surfaces, face surfaces and contours
    • ø range: 16.00 - 42.00 mm

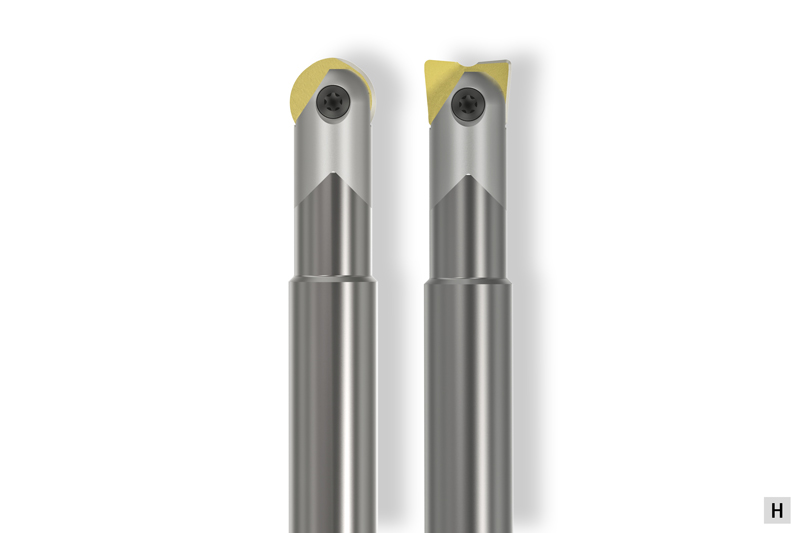
  • NeoMill-3D-Ballnose/-Torus

    Ball nose and corner radius milling cutter
    • One tool body with indexable insert for ball nose and corner radius milling for finishing and pre-finising
    • ø range: 8.00 - 32.00 mm

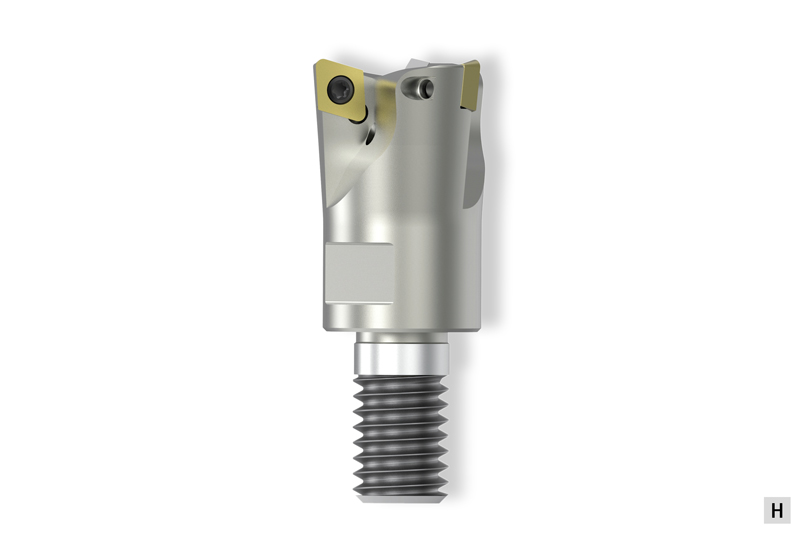
  • NeoMill-2/4-HiFeed90

    High-feed/90° shoulder milling cutter
    • Universal tool system to ensure maximum productivity
    • ø range: 16.00 - 200.00 mm

Wiercenie | Pogłębianie
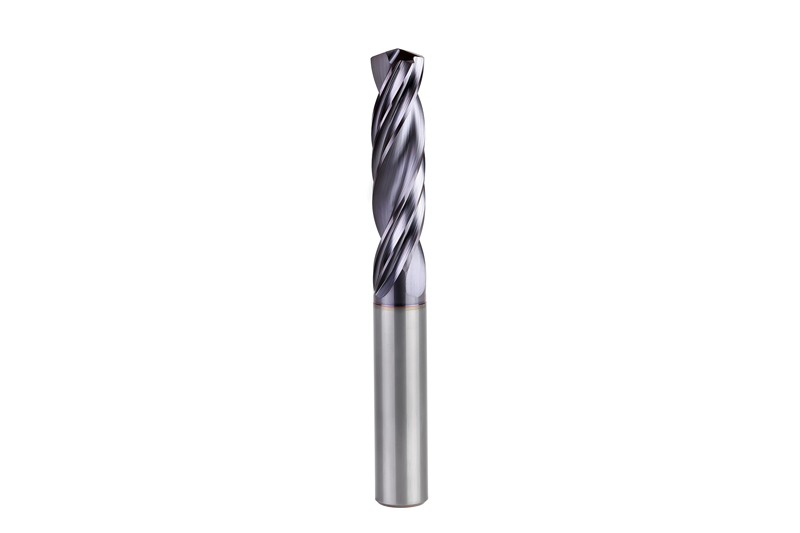
  • ECU-Drill-Steel

    Broca fabricada por completo en metal duro  

    • Taladro completo de doble filo con muy buena relación calidad-precio
    • Amplia gama de aplicaciones
    • Geometrías idóneas para lograr gran precisión y estabilidad en el proceso
    • Rango de Ø: 1,00 – 20,00 mm

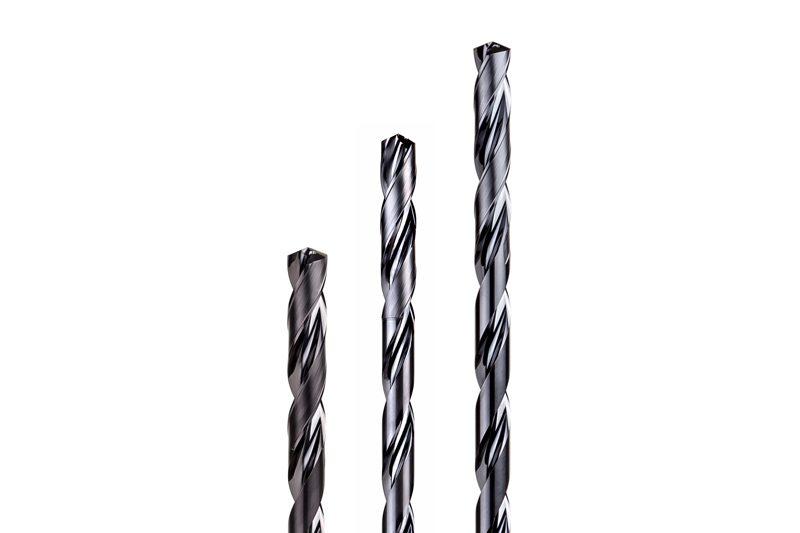
  • MEGA-Drill-Hardened

    Broca, de gran calidad, fabricada por completo en metal duro 

    • Taladro completo de doble filo con recubrimiento y geometría que se adaptan al mecanizado estable de materiales templados
    • Nueva micro y macrogeometría
    • Rango de Ø: 2,55 – 16,00 mm

  • MEGA-Drill-Steel-Plus

    Broca, de gran calidad, fabricada por completo en metal duro 

    • Taladro completo de doble filo con recubrimiento y geometría que se adaptan al mecanizado de acero
    • Geometría de ranura de virutas y preparación modificada de los filos de corte mejoradas
    • Rango de Ø: 3,00 – 25,00 mm

  • Tritan-Drill-Steel

    Broca, de tres filos, fabricada por completo en metal duro 

    • Taladro completo de tres filos para el máximo avance
    • Cuchilla transversal con autocentrado para situaciones de taladrado difíciles
    • Especialmente adaptada al mecanizado de acero
    • Rango de Ø: 4,00 – 20,00 mm 

  • Tritan-Spot-Drill-Steel

    Broca piloto
    • Broca piloto de tres filos para taladrado exigente
    • Se adapta especialmente al taladro de tres filos
    • Rango de Ø: 4,00 – 20,00 mm

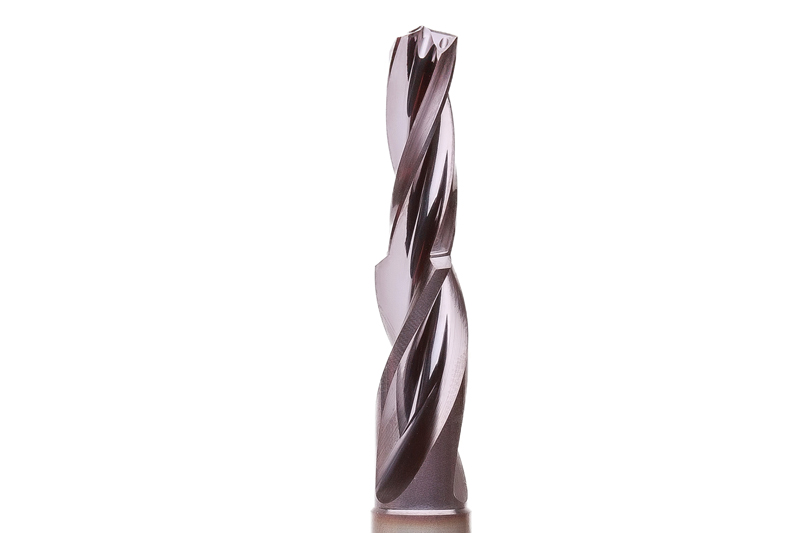
  • Tritan-Step-Drill

    Broca escalonada
    • Broca escalonada, de tres filos, con cuchilla transversal con autocentrado
    • Mecanizado de agujeros para roscar sin movimiento pendular
    • Rango de Ø: 4,25 – 14,15 mm

  • MEGA-Deep-Drill

    Taladro profundo
    • Taladrado estable y eficiente de agujeros profundos de hasta 40xD
    • Broca piloto MEGA-Pilot-Drill
    • Rango de Ø: 1,00 – 16,00 mm 

  • MEGA-Drill-Reamer

    Broca escariadora
    • Combina dos operaciones (taladrado y escariado) en una herramienta
    • Filos escariadores mejorados
    • Reducción de los periodos principales y los no productivos
    • Tolerancia del agujero ≥ IT7
    • Rango de Ø: 4,00 – 16,00 mm 

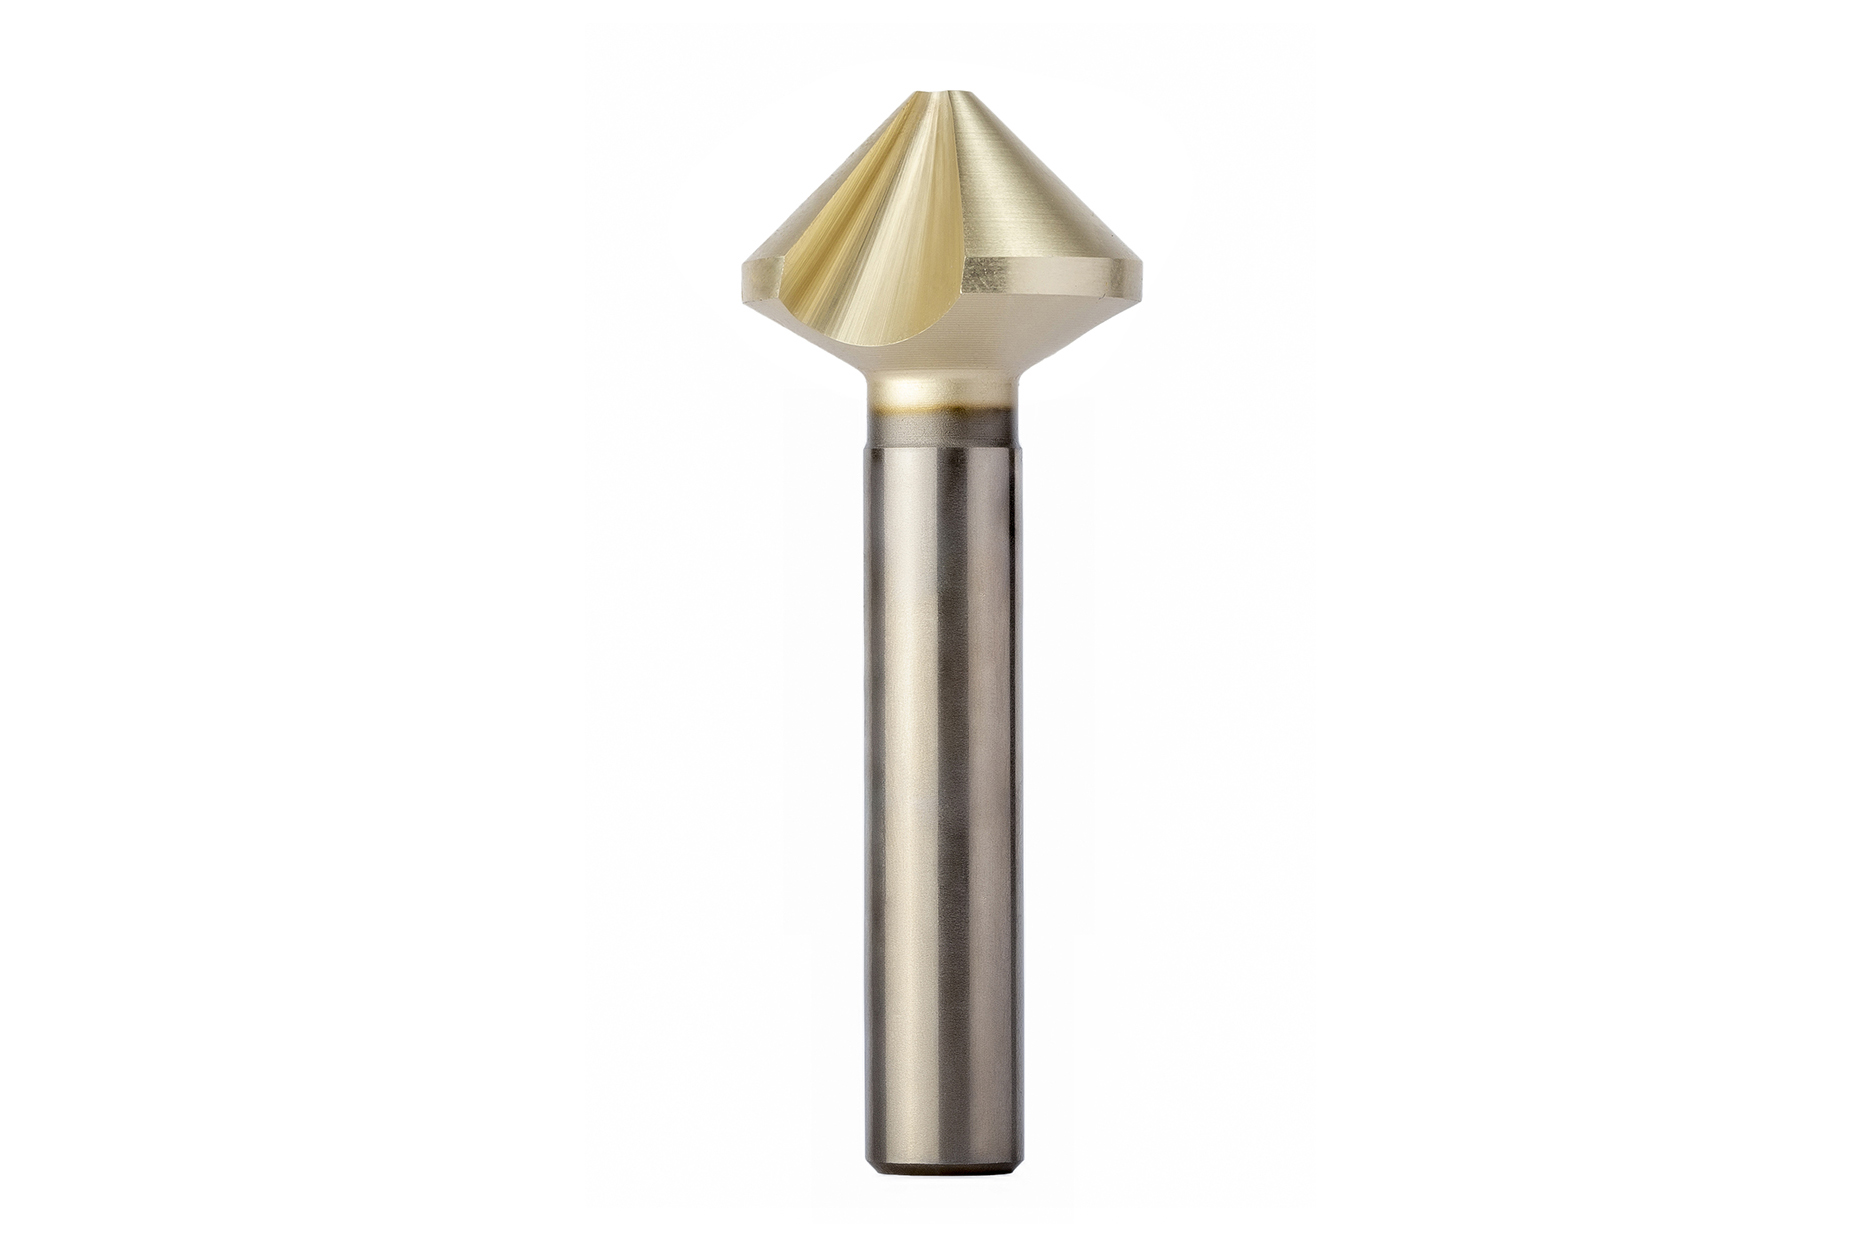
  • Avellanador cónico de precisión

    Avellanador con división irregular
    • Insertos divididos de forma muy irregular
    • Mayor precisión y mejores valores superficiales#
    • Fuerzas axiales y radiales reducidas
    • Vibraciones reducidas considerablemente
    • Aumento de los parámetros de corte para la máxima productividad
    • Rango de Ø: 4,30 – 31,00 mm

  • MEGA-Drill-Reamer-Pyramid

    Broca escariadora con punta piramidal 

    • Taladrado de inicio, taladrado y escariado con una herramienta
    • Centrado mejorado gracias a la punta piramidal
    • Reducción de los periodos principales y los no productivos
    • Tolerancia del agujero ≥ IT7
    • Rango de Ø: 4,00 – 16,00 mm 

  • Brocas de plaquitas de corte QTD

    Taladro completo con sistema de cabezal intercambiable 

    • Sistema rentable con placas de corte intercambiables
    • Sistema de sujeción con arrastre de fuerza y de forma
    • Manejo sencillo
    • Alta precisión de concentricidad
    • Rango de Ø: 8,10 – 49,00 mm 

Escariado
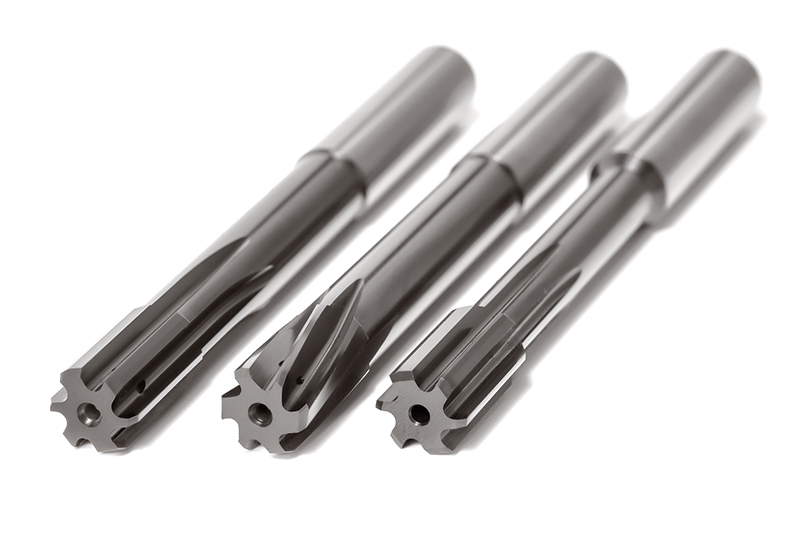
  • FixReam – FXR

    High-performance reamers with a cylindrical shank 

    • High-performance reamer made from solid carbide
    • Straight-fluted for through and blind bores
    • Left-hand fluted for through bores
    • Ø area: 3.00 – 20.00 mm 

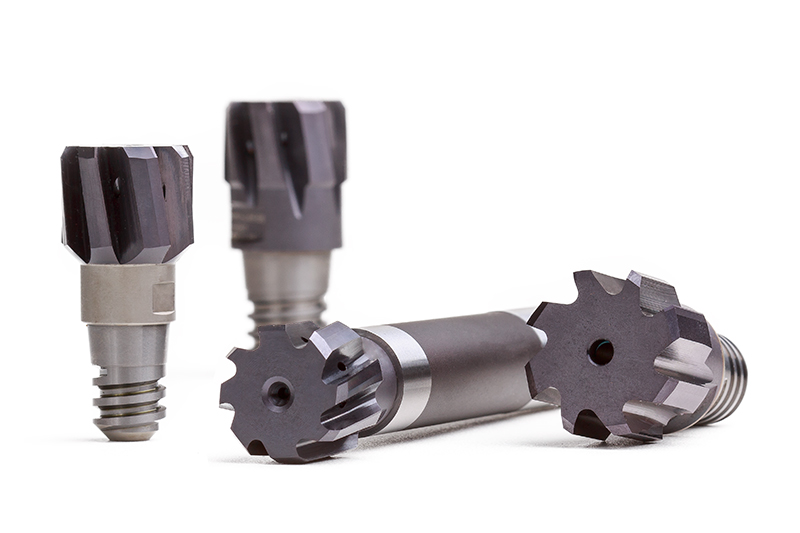
  • CPReam – CPR

    Replaceable head reamer 

    • Taper and face connection provide the greatest possible stability and rigidity
    • Highly precise radial run-out accuracy of 5 μm
    • Easy to handle
    • Ø area: 8.00 – 40.00 mm

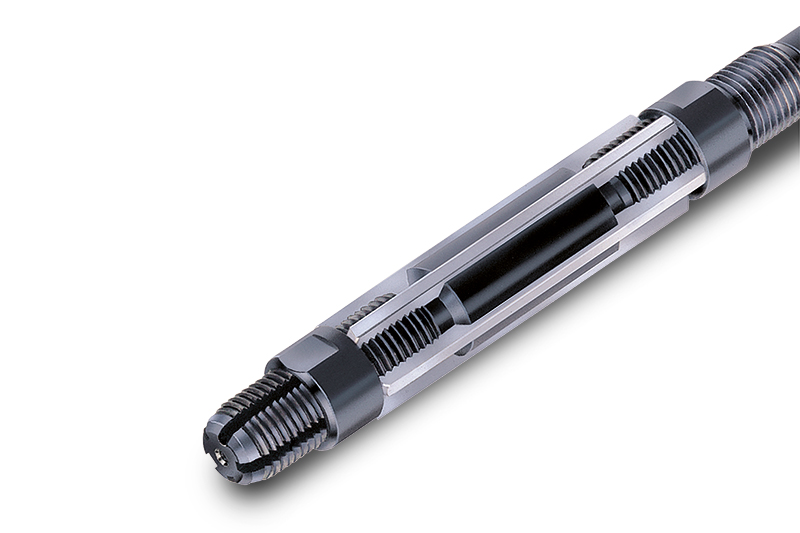
  • Quick adjustment reamer – WN 50

    Hand reamers 

    • Quick-adjust reamer with wide adjustment range
    • Especially suitable for repair work
    • Spare blade sets available
    • Ø area: 6.40 – 95.00 mm 

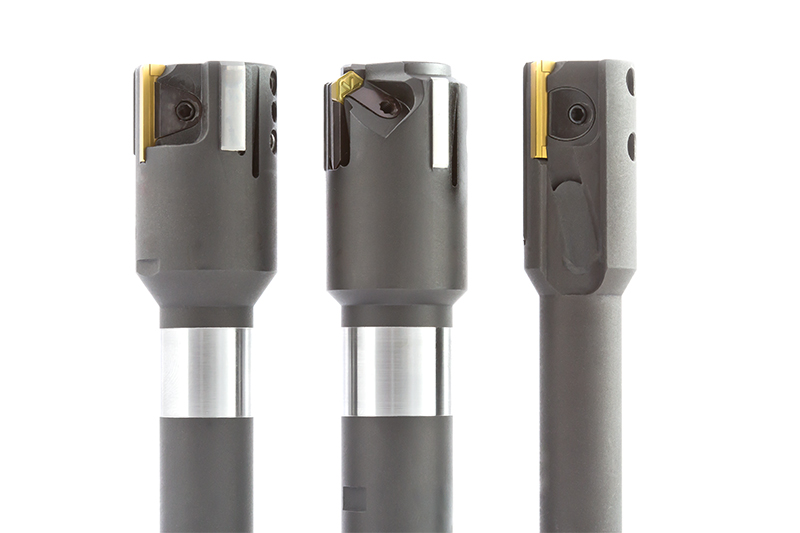
  • Guided tools

    Tools with guide pads 

    • Highest accuracy guaranteed with the MAPAL principle
    • Guide pads directly guide the tool into the bore
    • Precision-ground indexable inserts
    • High-precision adjustment for micrometre-precise bore machining

Clamping
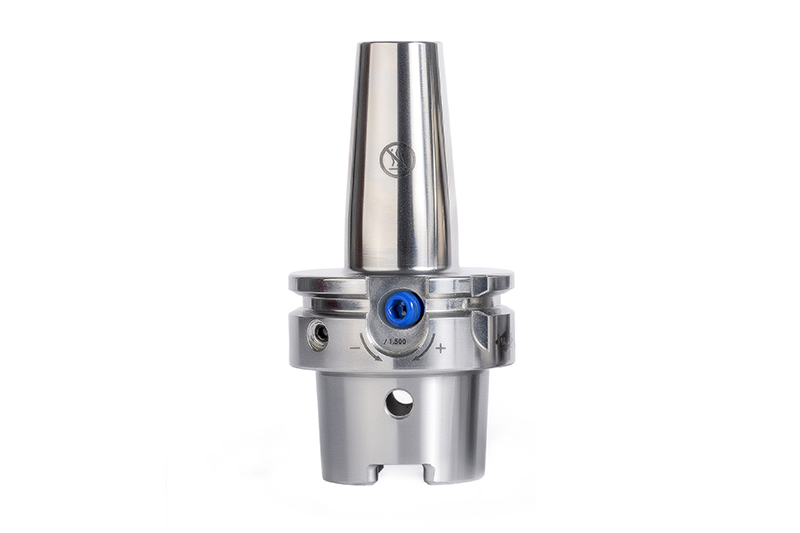
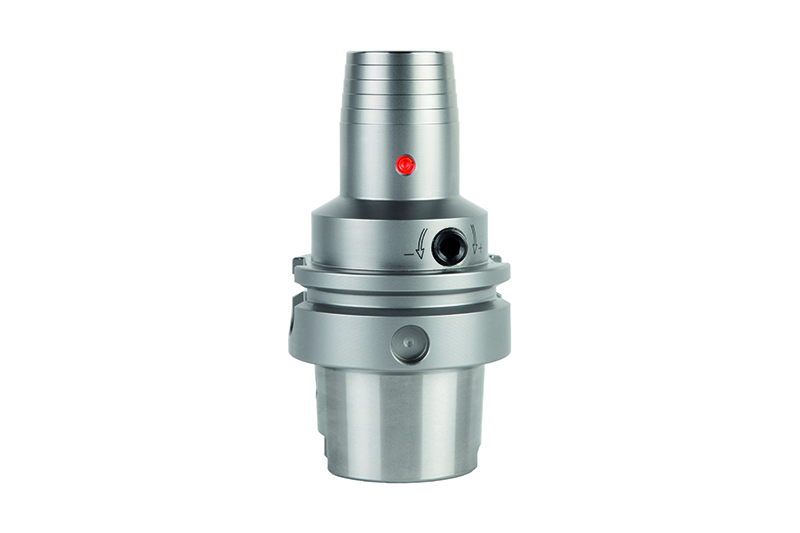
  • UNIQ DReaM Chuck, 4.5°

    Nuevo diseño del adaptador hidráulico

    • Para escariado y taladrado, así como acabado durante el fresado
    • Combinación óptima de propiedades geométricas y funcionales
    • Superficies extraordinarias con manejo mejorado simultáneo
    • Flexibilidad y productividad máximas durante el mecanizado de componentes de perfiles complicados

    Ir a la tienda

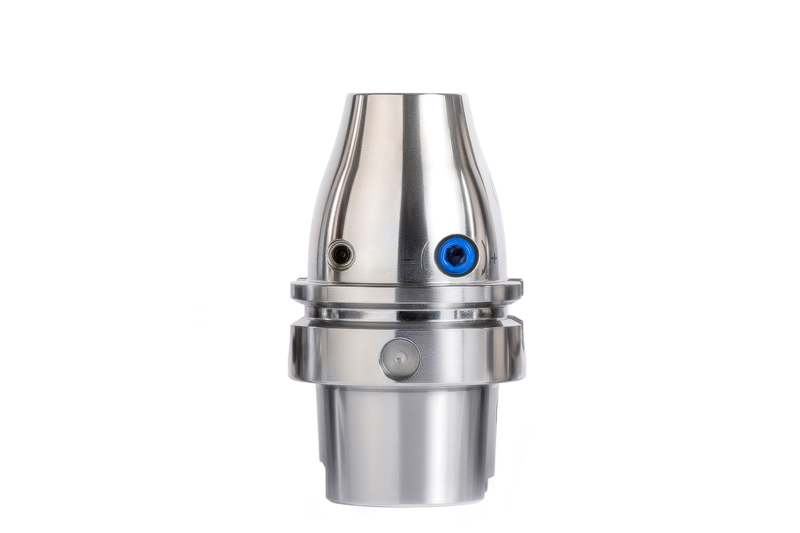
  • UNIQ Mill Chuck, HA

    Nuevo diseño del adaptador hidráulico

    • Adaptador hidráulico para fresados muy dinámicos
    • Combinación óptima de propiedades geométricas y funcionales
    • Resultados magníficos al usarse herramientas con mango HA
    • Máxima seguridad de proceso, incluso si los componentes son de alta calidad

    Ir a la tienda

  • HighTorque Chuck HTC

    Mandril de expansión hidráulica

    • Alta transmisión del par
    • Características de amortiguación idóneas
    • Resistencia extraordinaria del sistema completo
    • Precisión de concentricidad < 3 µm
    • Diseño estrecho de 3° para usarse en perfiles complicados


    Ir a la tienda

  • MAPAL HydroChuck MHC

    HydroChuck MHC

    Hydraulic chuck 

    • Excellent vibration dampening
    • High degree of radial run-out accuracy
    • Ultra-short and compact design for high rigidity


    To the shop

  • ThermoChuck MTC

    Shrink chuck 

    • Long tool life through the use of high-temperature tool steel 
    • High torque transmission and radial rigidity
    • Precision balanced as standard
    • MQL-suitable
    • With and without axial tool length adjustment 


    To the shop

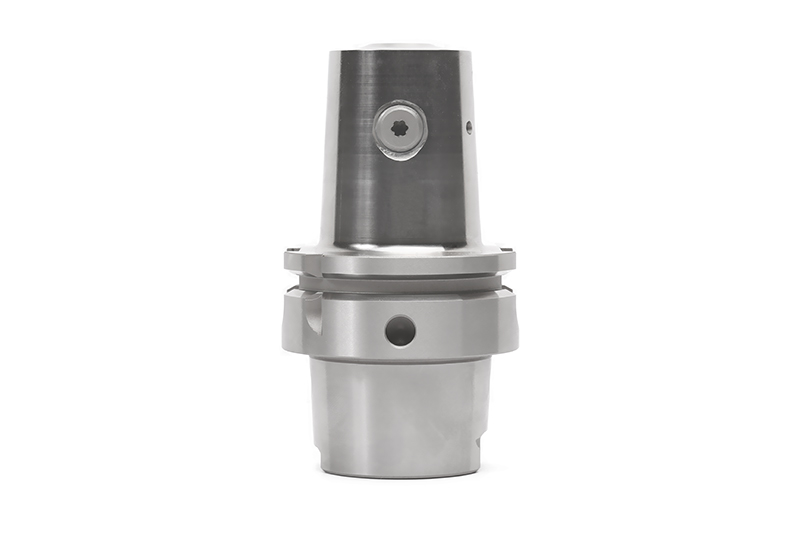
  • MAPAL MillChuck

    Mill Chuck, System HB

    Side lock chuck
    • Easy to handle thanks to use of a differential screw
    • Maximum cost-effectiveness and precision
    • Axial tool positioning can be defined using spring system
    • Decentralised coolant outlets for maximum process reliability


    To the shop

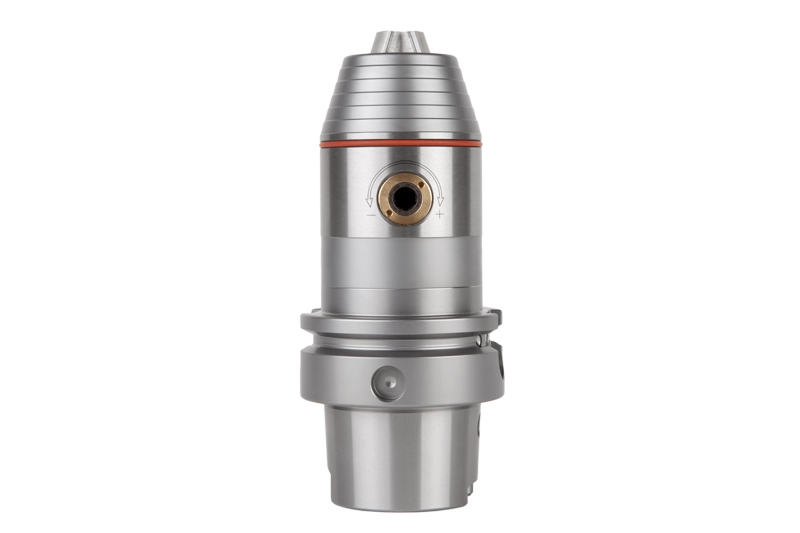
  • MAPAL Precision-DrillChuck MPC

    Precision-DrillChuck – MPC

    Precision drill chuck 

    • Simple construction, straightforward to handle
    • Safe clamping independent of direction of rotation
    • High degree of spindle speed strength
    • Modular design allows drill chuck heads to be used with all tool connections 

  • MAPAL slip-on reamer arbor

    Milling cutter arbor – MDA / MCA

    Milling cutter arbor 

    • Vibration-cancelling design (MDA) with vibration dampening system
    • Adapted to the rigidity of all common machine types
    • Smooth, stable running despite long projections delivers better surface finish
    • Milling cutter arbor (MCA) with large face connection for roughing and pre-finishing operations in large diameter ranges

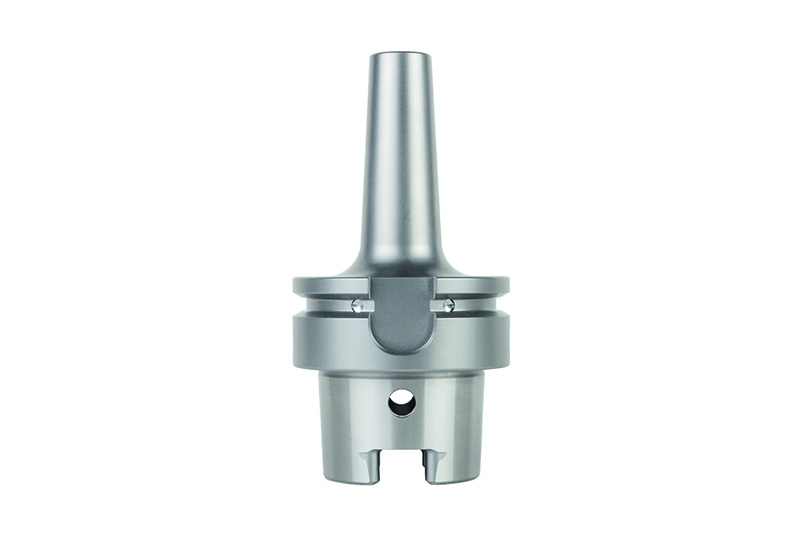
  • MAPAL MFS milling head holder

    MFS milling head holder

    Tool adapter for screw-in milling cutter 

    • Simple and fast clamping of screw-in milling cutters
    • Exact interaction of taper and face connection
    • Greatest possible stability and rigidity
    • Universally deployable for roughing and finishing operations

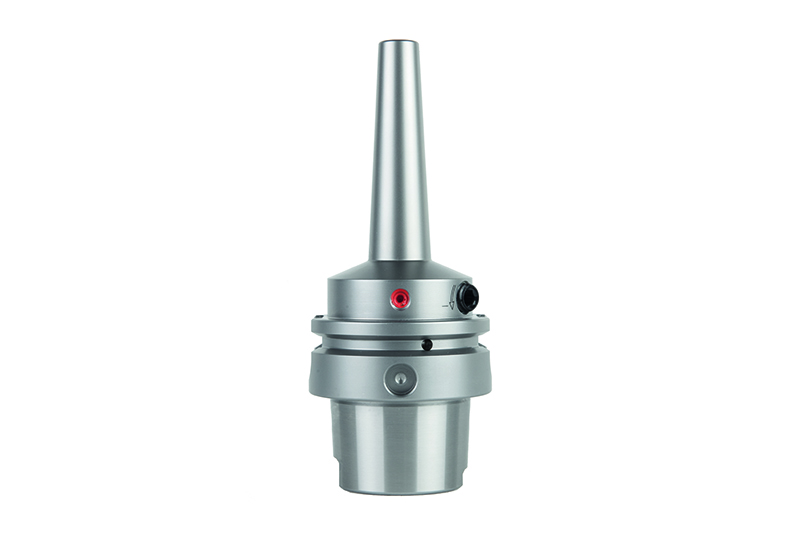
  • MAPAL HSK adapter

    Adapter

    Extensions, reducers and adapters 

    • Wide range of options for modular tool systems
    • Hydraulic extensions and tool extensions for thermal expanding chucks
    • HSK reducers and extensions
    • KS steep taper adapter


    To the shop


Components and workpiece material
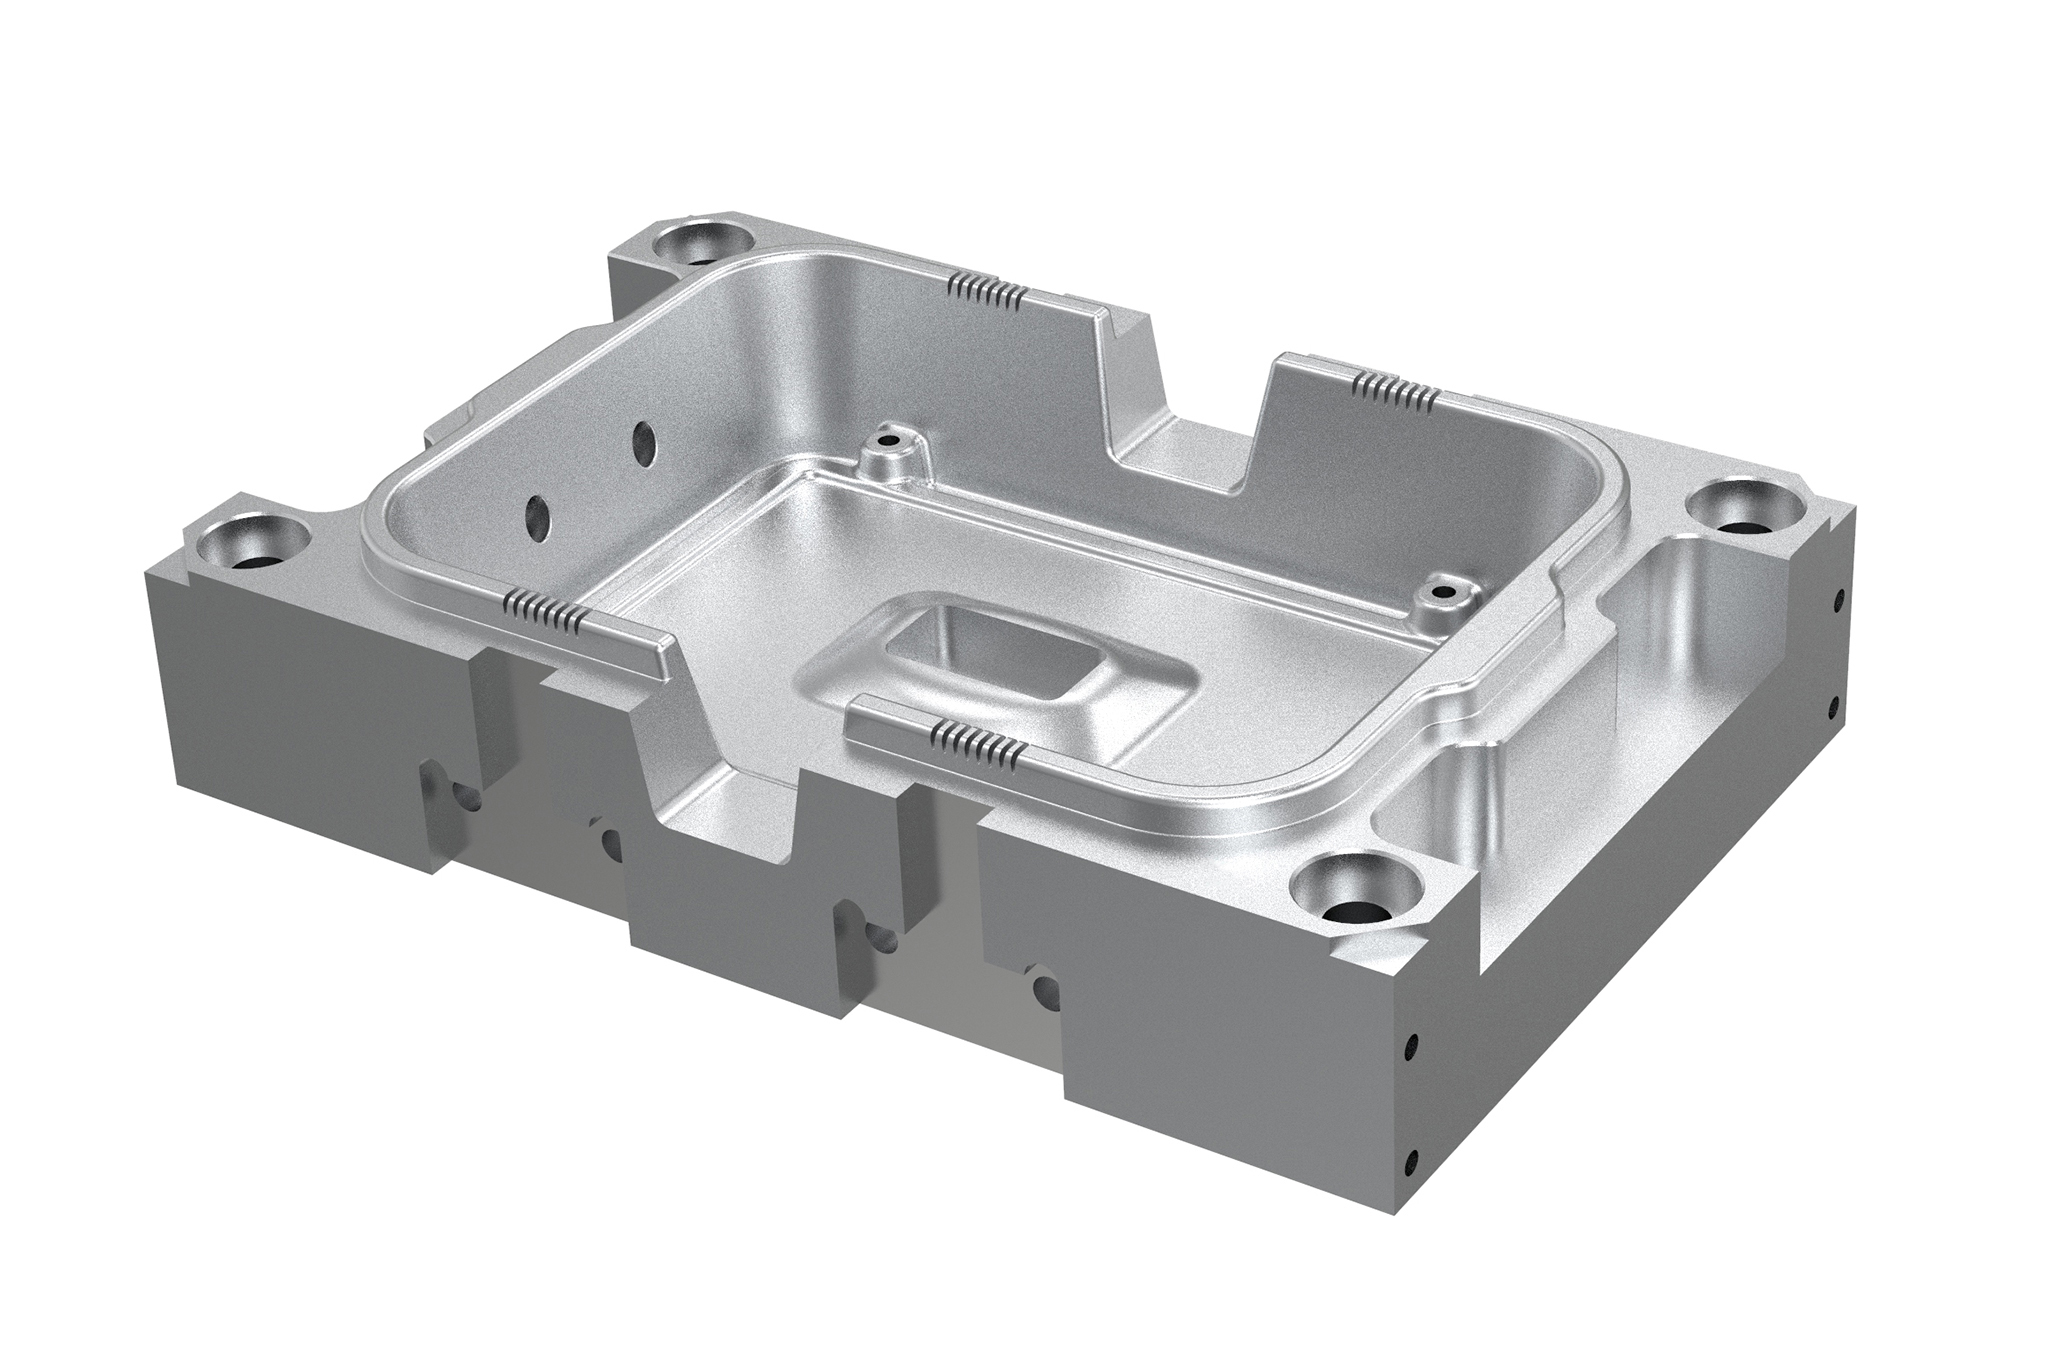

Vom Roh- zum Fertigteil

Mit wenigen Klicks zum passenden Werkzeug: In Abhängigkeit von der Bearbeitung, der konkreten Operation und der Werkzeuganforderung schnell zum gewünschten Werkzeug gelangen.
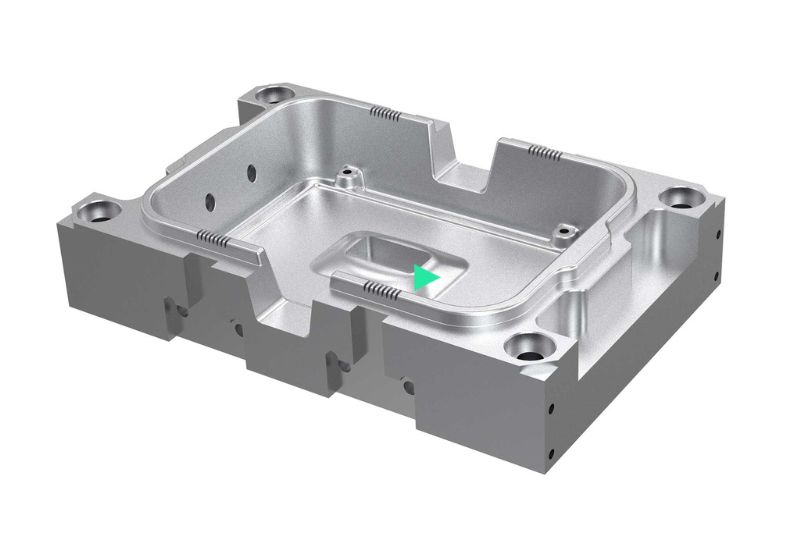
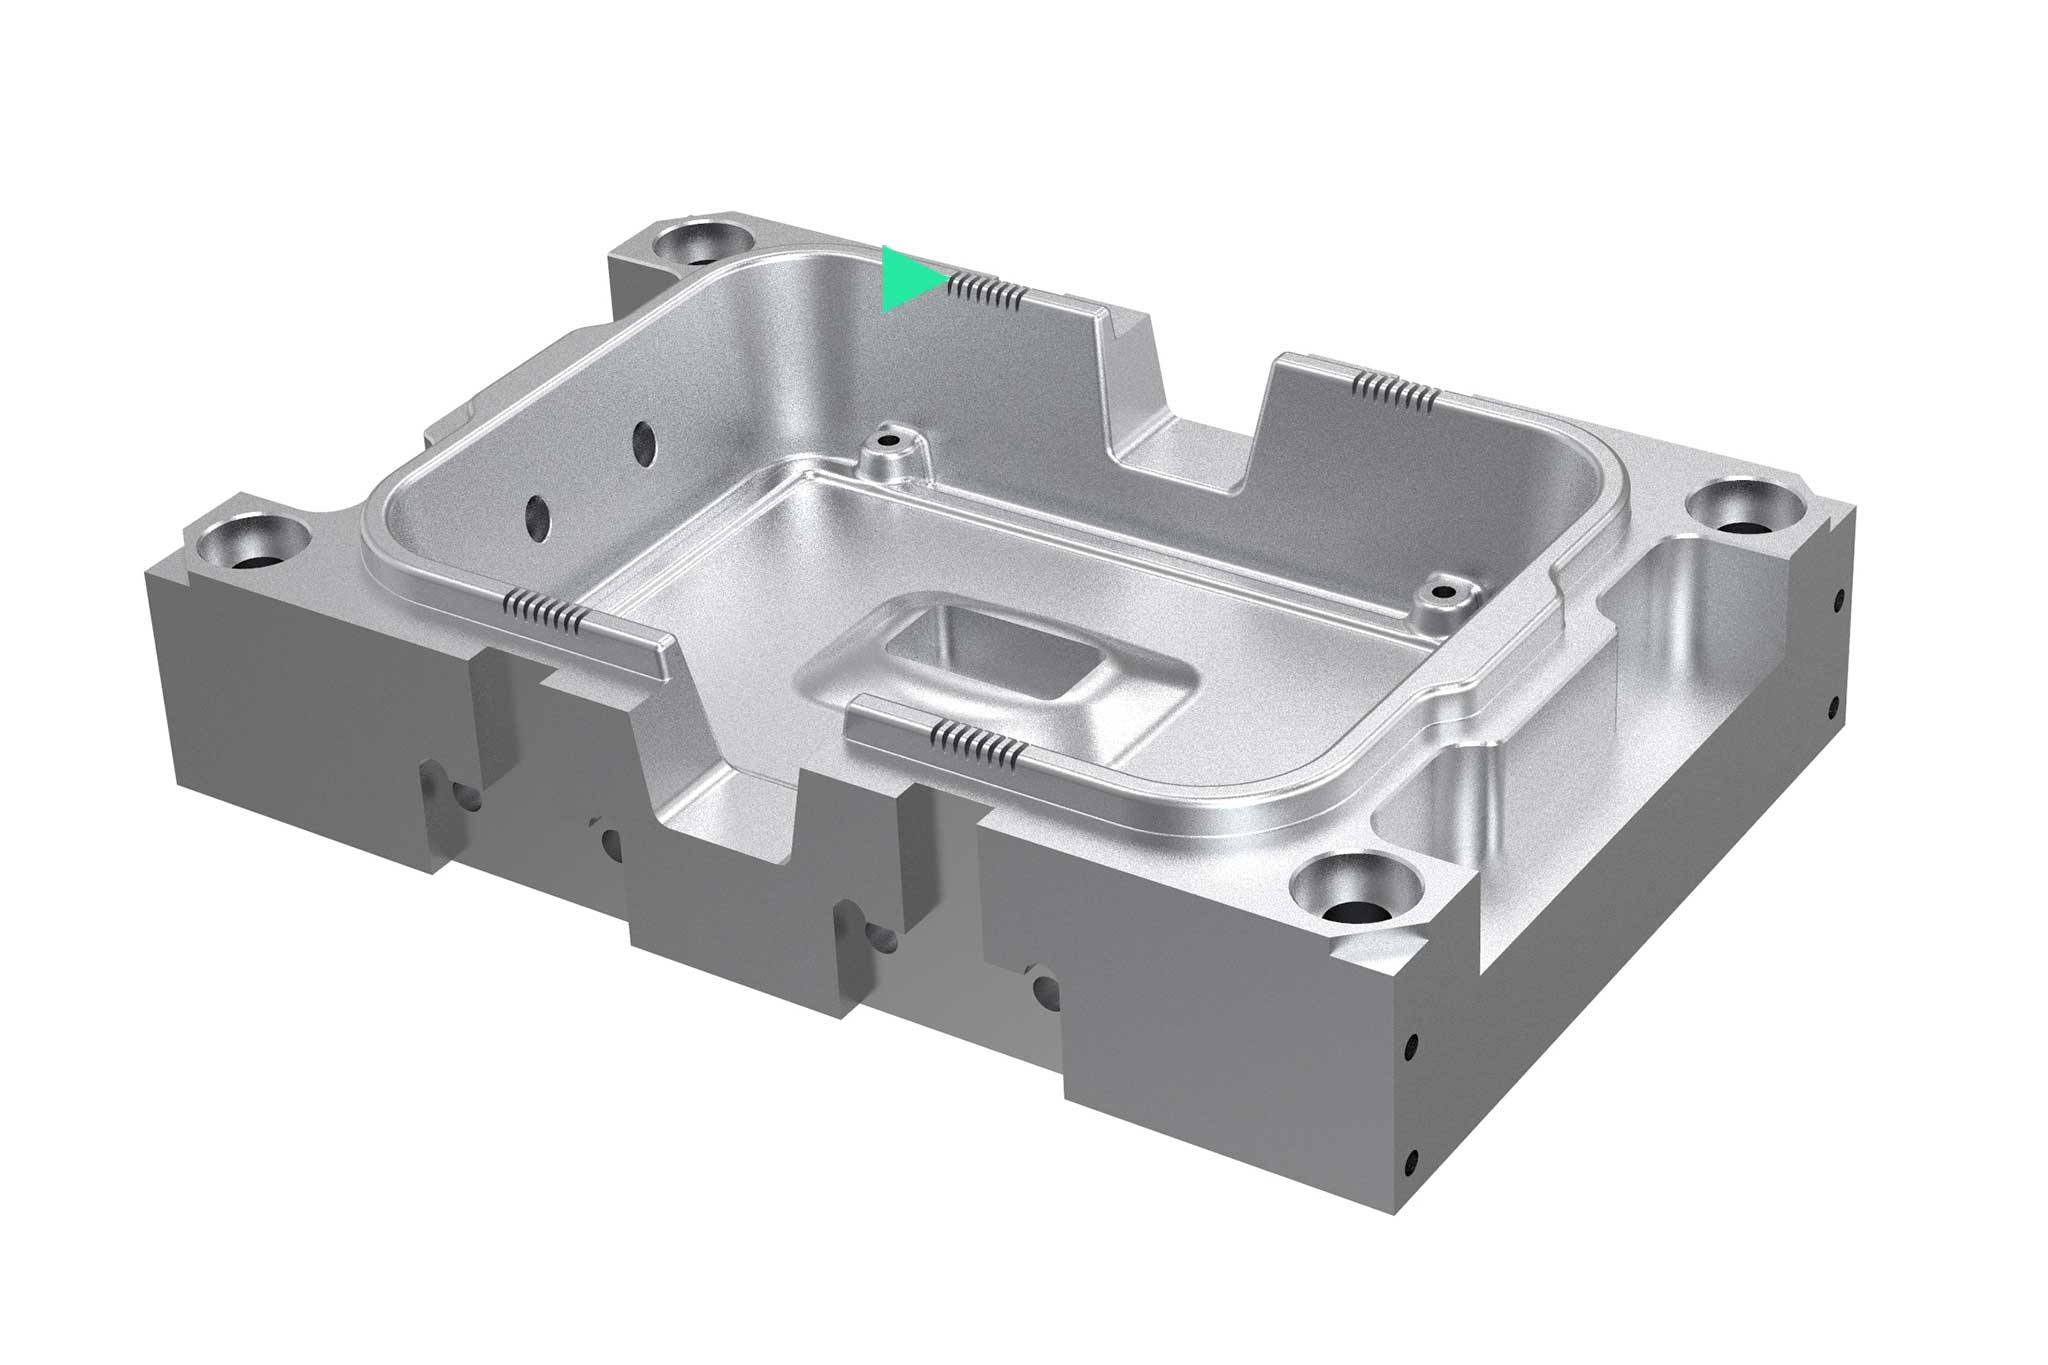
  • An einem gerenderten Beispielbauteil ist eine Bearbeitung hervorgehoben.
    1 / 8

    2D-Flächen

    In diese Kategorie fallen einerseits direkt an der Maschine ausgeführte Bearbeitungsprozesse wie Planfräsen, Fräsen von Taschen und geraden Wänden. Andererseits auch Operationen für komplexe Geometrien, die mithilfe einer CAM-Software programmiert werden.

    Zum Produktprogramm zur Bearbeitung von 2D-Flächen
  • An einem gerenderten Beispielbauteil ist eine Bearbeitung hervorgehoben.
    2 / 8

    3D-Flächen

    Im Werkzeug- und Formenbau ist die Herstellung komplexer werdender Formen Alltag. Kontinuierliche Weiterentwicklungen bei Werkzeugmaschinen und CAM-Software heben die Leistungsfähigkeit und Produktivität auf ein immer höheres Niveau. Somit müssen auch die eingesetzten Werkzeuge stets dem neuesten Stand der Technik entsprechen. Um hier ein Optimum zu erreichen, steht eine Prozessanalyse am Beginn der Auslegung.
    ​​​​​​​
    ​​​​​​​Zum Produktprogramm zur Bearbeitung von 3D-Flächen
  • An einem gerenderten Beispielbauteil ist eine Bearbeitung hervorgehoben.
    3 / 8

    Offene Taschen

    Formeinsätze weisen auch Bearbeitungsaufgaben auf, die für das Gießen oder diverse Anbauteile erforderlich sind. Offene Taschen (Umfangsbearbeitungen) bearbeiten Anwender zunehmend mittels Trochoidalfräsen. Diese Bearbeitungsmethode hilft, die Bearbeitungszeiten zu optimieren und die Werkzeugstandzeiten zu verlängern.
    ​​​​​​​
    ​​​​​​​Zum Produktprogramm zur Bearbeitung von offenen Taschen
  • An einem gerenderten Beispielbauteil ist eine Bearbeitung hervorgehoben.
    4 / 8

    Geschlossene Taschen

    Die Herstellung geschlossener Taschen erfolgt meist durch Schruppen in Z-Ebenen. Häufig wird hierbei beim Fräsen der Bearbeitungseintritt über eine Rampe gewählt. Die Wahl des Werkzeuges hängt von der Tiefe der Wände und der zu erzeugenden Ausformschräge am Bauteil ab. Das breite Portfolio von MAPAL mit modularen Systemen deckt auch die Bearbeitung tiefer Taschen mit großen Durchmessern ab.

    Zum Produktprogramm zur Bearbeitung von geschlossenen Taschen
  • An einem gerenderten Beispielbauteil ist eine Bearbeitung hervorgehoben.
    5 / 8

    Helixfräsen

    Ein wesentlicher Fokus bei Fräsbearbeitungen liegt auf der Reduzierung der Bearbeitungszeit. Mit spezifischen Werkzeuggeometrien für die Bearbeitung von geschlossenen, runden Taschen gelingt es häufig, den Vorbohrprozess zu eliminieren. Beim Helixfräsen werden Fräsbahnen mit helixförmigen Eintritten programmiert, die für Taschendimensionen geeignet sind.
    ​​​​​​
    ​​​​​​​Zum Produktprogramm Helixfräsen
  • An einem gerenderten Beispielbauteil ist eine Bearbeitung hervorgehoben.
    6 / 8

    Ebene Flächen

    Operationen zur Erzeugung von ebenen Flächen kommen sehr häufig und in unterschiedlichen Bereichen im Werkzeug- und Formenbau vor: Sei es bauteilbedingt, strategiebedingt durch die jeweilige Fräsbearbeitung oder durch Anforderungen bei Formschließflächen sowie Abschnitten und Stanzformen. Die Auswahl des passenden Werkzeuges erfolgt dann in Abhängigkeit von Anwendung und Anforderung. 

    ​​​​​​​Zum Produktprogramm zur Bearbeitung von ebenen Flächen 
    ​​​​
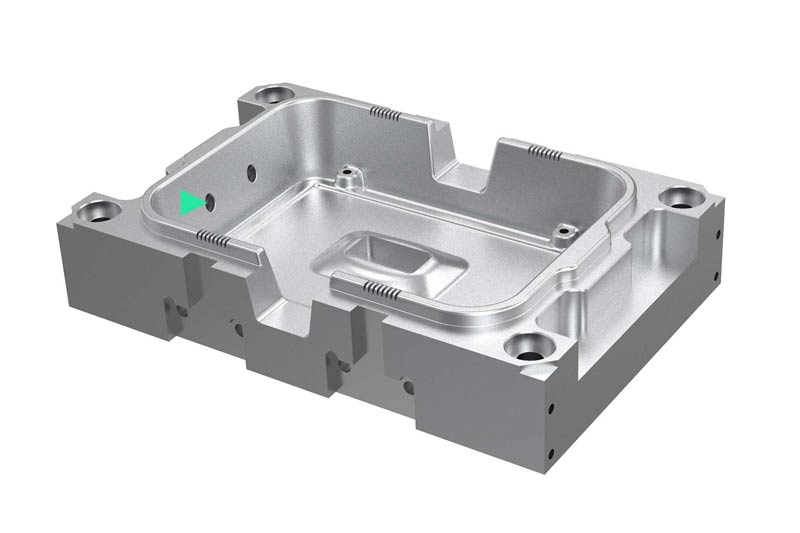
  • On a rendered example component, an operation is highlighted.
    7 / 8

    Thin walls and ribs

    Plastic injection moulds and die casting moulds often have ribs and thin walls. Ribs, for example, are increasingly being milled, as this process is more cost-effective than EDM (spark eroding). As a rule, long or extra-long carbide tools with small diameters are used. Customer-specific solutions (RibCutter) to match the respective rib shape are also possible here.

    Go to the product range for machining thin walls and ribs
  • On a rendered example component, an operation is highlighted.
    8 / 8

    Small and large bores

    There is a wide range of full bore operations in the die & mould sector: From large bores for guide pillars and deep bores for the cooling system to high-precision bores for ejector pins. MAPAL offers a comprehensive portfolio of drilling and reaming tools for the individual production steps.

    Go to the product range for machining small and large bores
All from a single source
  • 1. Planning and purchasing

    Optimised purchasing management is important for a clear organisation of the tool stock.

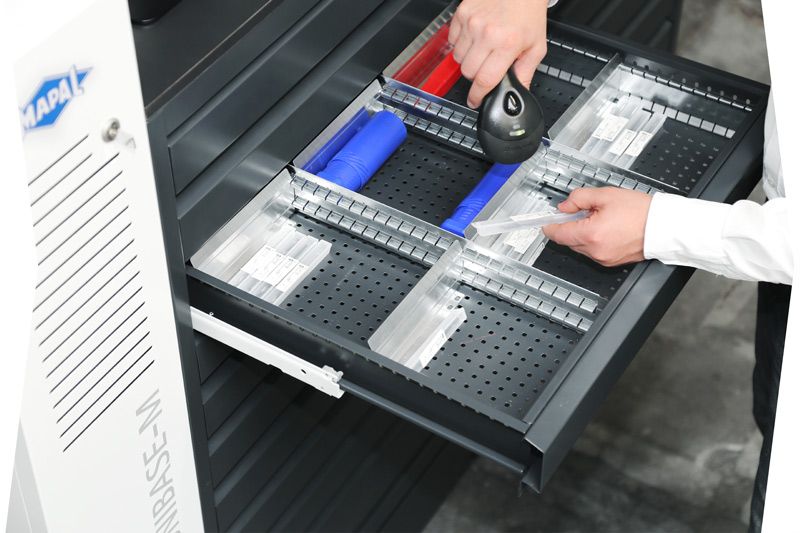
  • 2. Tool logistics

    Cost-effectiveness even in the periphery of machining: Intelligent dispensing systems significantly reduce non-productive times.

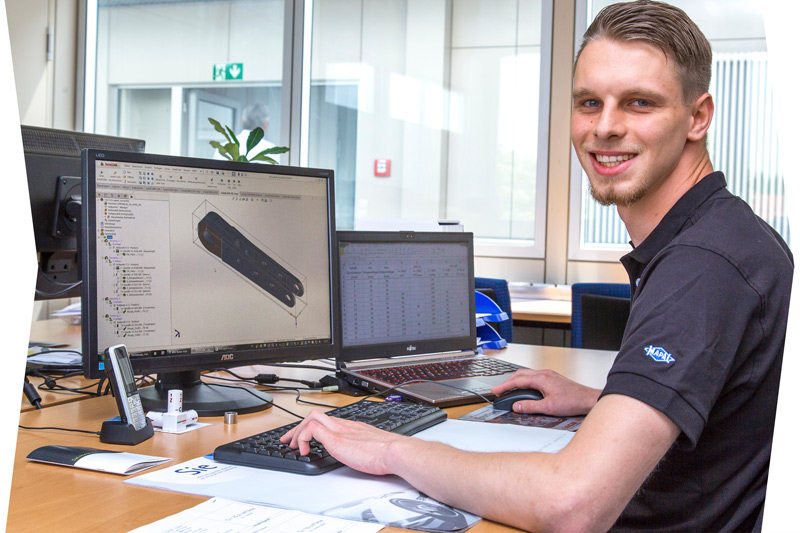
  • 3. Engineering

    The machining specialists provide support with process engineering, e.g. in the form of CAM simulations, general advice and the development of economic machining strategies.

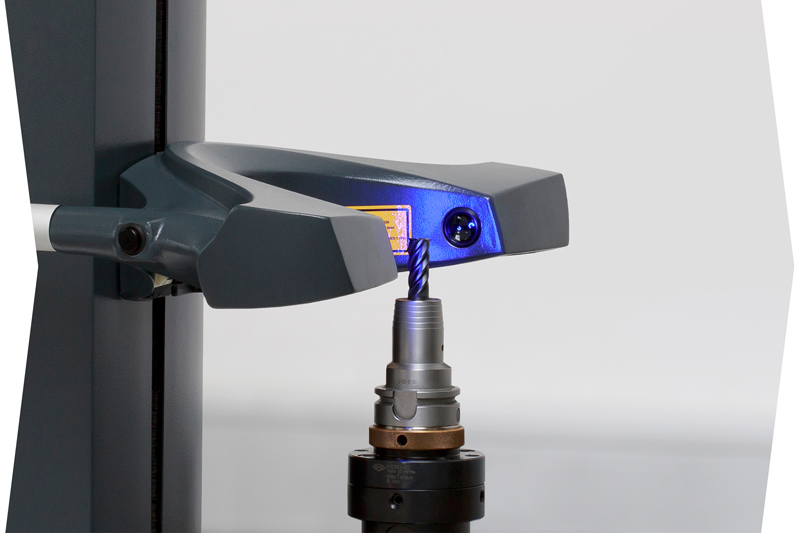
  • 4. Measuring and setting

    Reliable setting and measuring devices are convincing due to their accuracy and user-friendly operation when setting the tools.

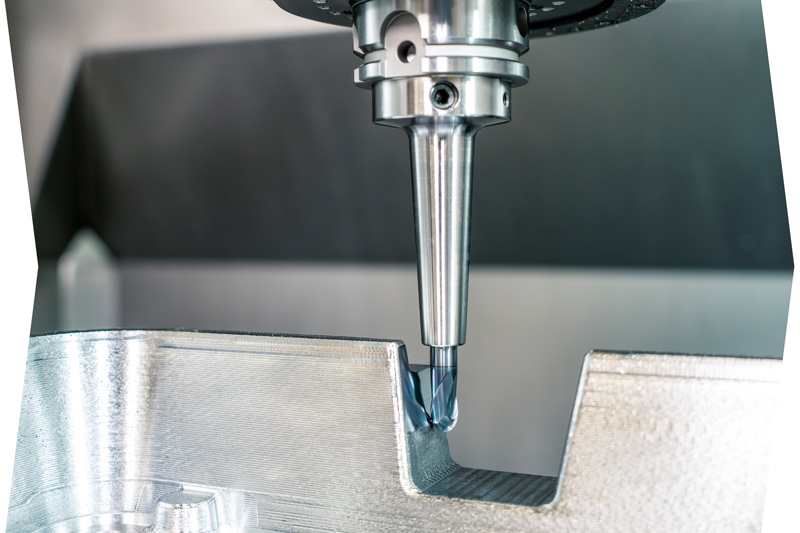
  • 5. Tools and clamping technology

    From the spindle to the cutting edge – MAPAL offers a wide range of tools and clamping technology for the die & mould sector.

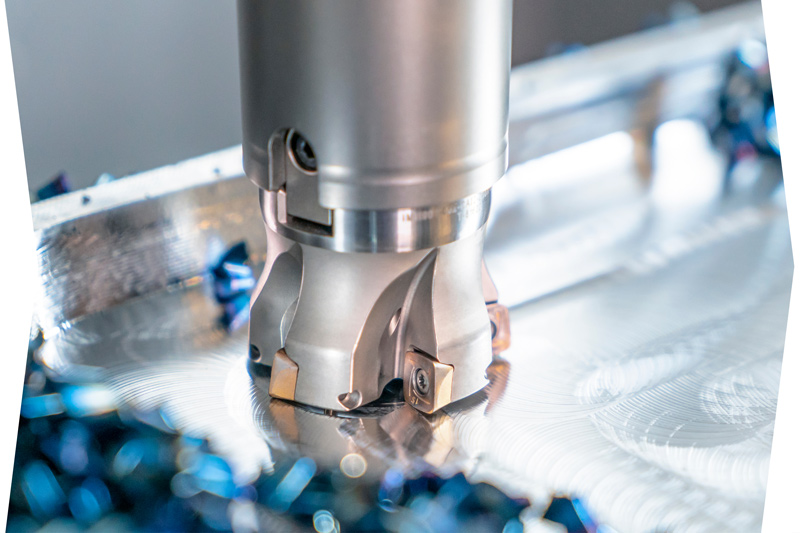
  • 6. Machining

    Efficient machining processes and customised machining strategies at the highest technological level.

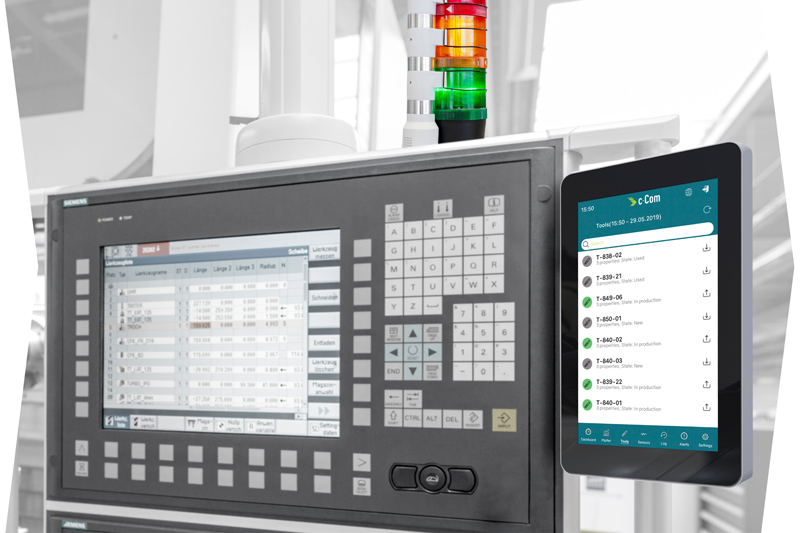
  • 7. Digitisation and automation

    Quick and easy digitisation: The c-Connect Box digitally transmits measurement data from the setting fixture to the machine tool. It also monitors the machine status among other things.

  • 8. Reconditioning

    Customers receive their reconditioned tools back in manufacturer quality within a very short time. Also available with pick-up and delivery service upon request.


Engineering Workflow - From theory to practice
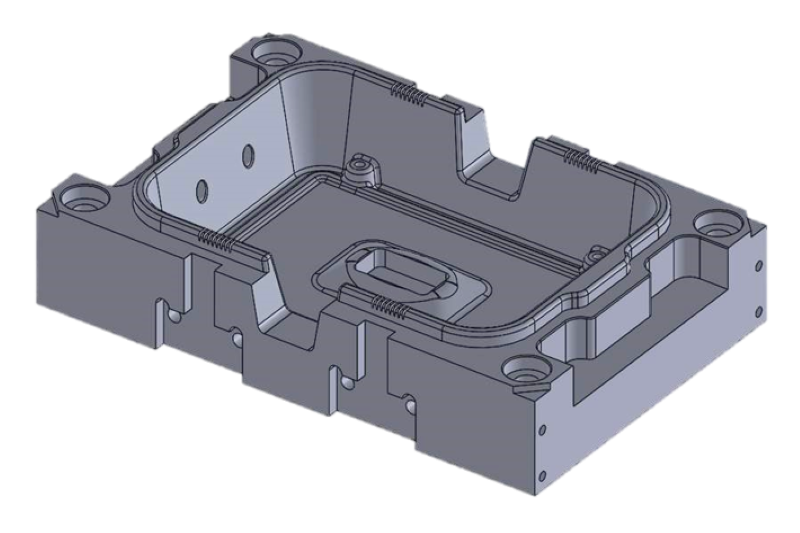
Finding the perfect solution for the customer is MAPAL’s main goal. In addition to individual custom solutions and a broad standard product portfolio, comprehensive services are available to optimally design the entire process from the product idea to the chip. Customers can rely on the technology leader’s many years of experience in machining.
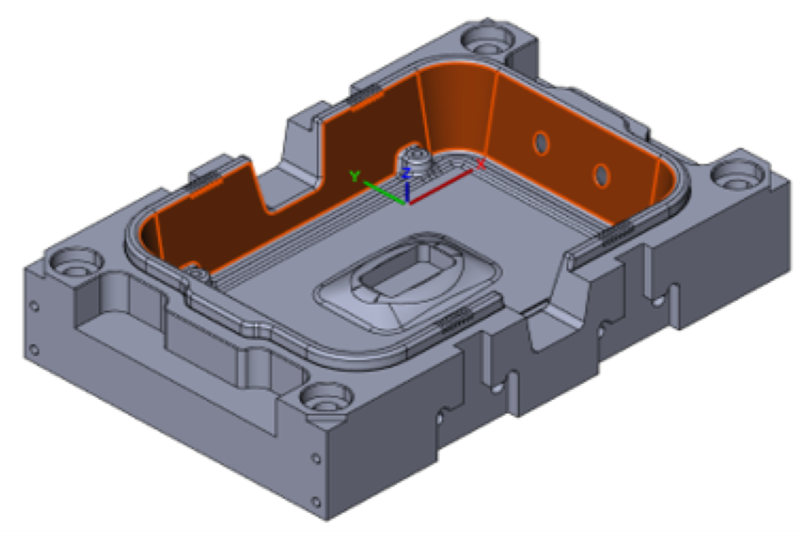
  • 3D model of a workpiece from the die and mould making.

    1. Customer enquiry

    MAPAL sales representatives are directly available for individual enquiries. In a personal conversation with the customer, they sound out the specific requirements and the scope (complete or partial machining) and discuss the details directly on the 3D model of the component.

    The MAPAL die & mould team looks forward to your enquiry by ​​​​​​​Email and will contact you directly as soon as possible.

  • 3D model of a workpiece from the die and mould making.

    2. Project analysis

    On the basis of 3D models and machine data, the conversation partners analyse the manufacturing tasks and develop effective machining strategies.

    The project analysis consists of the following:​​​​​​​
    • Machining suggestions for all machining steps
    • Tool list
    • Process optimisation

  • 3. Process design

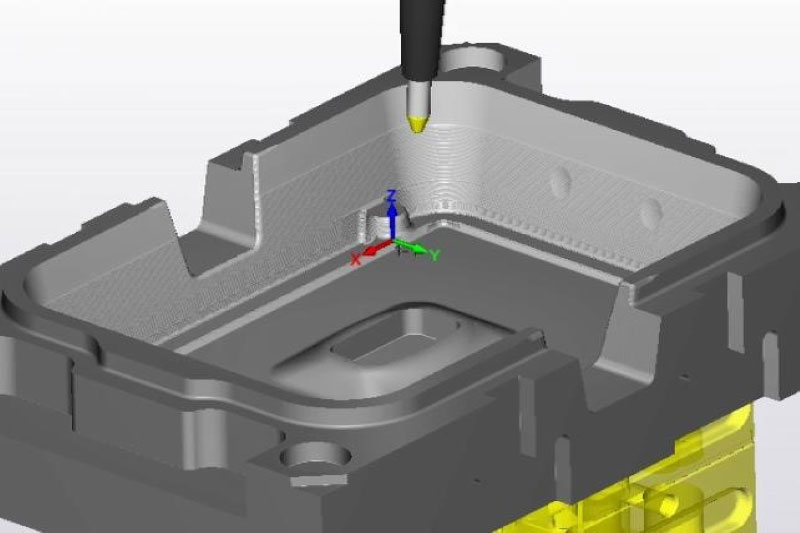
    Regardless of whether the focus is on flexibility or productivity: The machining specialists simulate the developed process on the basis of the 3D models and thus show potential for optimisation. They check and improve the machining parameters in CAM programming and thus ensure stable and economical production.

    The process design includes:​​​​​​​
    • Runtime analysis of the component
    • Technology data definition
    • CAM programming

  • Overview of all MAPAL tool solutions for die and mould making in one workpiece.

    4. Tool solution

    The wide-ranging MAPAL standard range for the die & mould sector offers the ideal tool solution for every application. Customised solutions are available upon request.

    Advantages for the user:​​​​​​​
    • Broad standard range
    • Availability of tool data

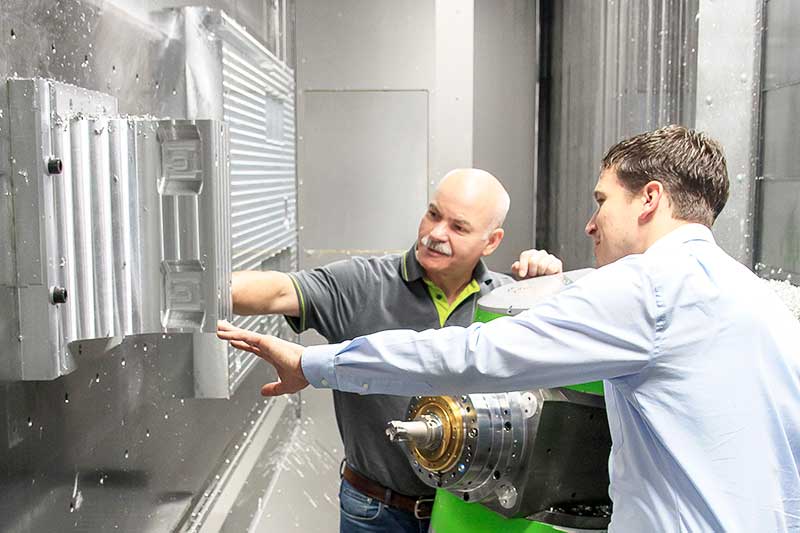
  •  The picture shows a technical advisor from MAPAL in conversation with a customer.

    5. Tool test and offer

    After discussing the machining task, MAPAL supports its customers in the selection of tools required in the process. This is the basis for a well-founded offer tailored to the respective application.

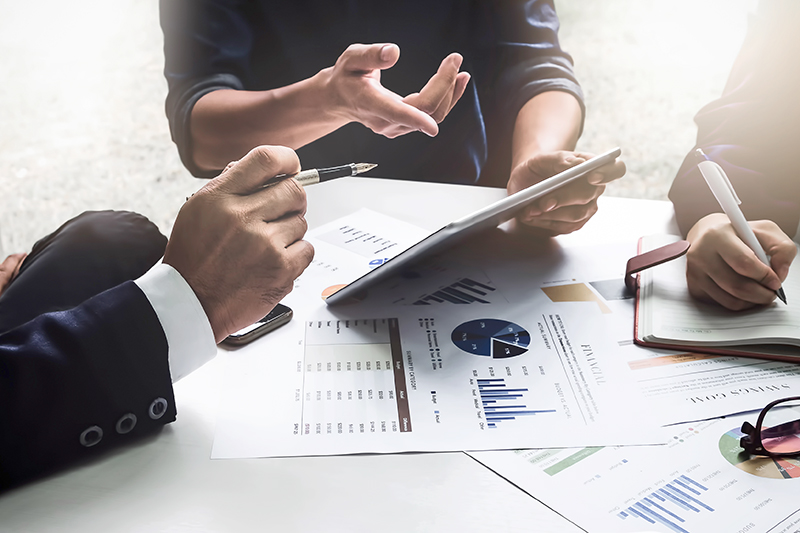
  • The picture shows documents for preparing offers on a table with three people.

    6. Cooperative partnership

    Even after mutual success, the specialists at MAPAL remain in close contact with the customer. Should optimisation potential arise over time or other tools turn out to be better, MAPAL will be happy to support you to further improve productivity and profitability.

    In order to ensure efficient production in the long term, MAPAL also offers comprehensive tool management options.
    ​​​​​​​
    Tool management options:

    • Dispensing systems
    • Regrinding service
    • Comprehensive product portfolio of adjustment and measuring devices


Further items about the die&mould area


Our retail partners

Responsibility according to postcode areas

  • 1 / 16

    Postcode 35

    FRITZ WEG GmbH & Co. KG
    Ahornweg 41
    35713 Eschenburg-Wissenbach

    Phone: +49 2774 701-0
    Fax: +49 2774 701-39
    Email: info@fritzweg.de
    Web: www.fritzweg.de

  • 2 / 16

    Postcode 44

    Jansen Schneidwerkzeuge Vertriebs GmbH
    Im Käsebrink 12
    58840 Plettenberg

    Phone: +49 2391 9177-0
    Fax: +49 2391 9177-20
    Email: info@j-s-v.com
    Web: www.j-s-v.com

  • 3 / 16

    Postcode 51

    Jansen Schneidwerkzeuge Vertriebs GmbH
    Im Käsebrink 12
    58840 Plettenberg

    Phone: +49 2391 9177-0
    Fax: +49 2391 9177-20
    Email: info@j-s-v.com
    Web: www.j-s-v.com

  • 4 / 16

    Postcode 56, 57

    FRITZ WEG GmbH & Co. KG
    Ahornweg 41
    35713 Eschenburg-Wissenbach

    Phone: +49 2774 701-0
    Fax: +49 2774 701-39
    Email: info@fritzweg.de
    Web: www.fritzweg.de

  • 5 / 16

    Postcode 58, 59

    Jansen Schneidwerkzeuge Vertriebs GmbH
    Im Käsebrink 12
    58840 Plettenberg

    Phone: +49 2391 9177-0
    Fax: +49 2391 9177-20
    Email: info@j-s-v.com
    Web: www.j-s-v.com

  • 6 / 16

    Postcode 60, 61

    Heinrich Meier GmbH
    Herrenwaag 31
    75417 Mühlacker

    Phone: +49 7041 9530-0
    Fax: +49 7041 9530-30
    Email: info@heinrich-meier.de
    Web: www.heinrich-meier.de

  • 7 / 16

    Postcode 63 - 69

    Heinrich Meier GmbH
    Herrenwaag 31
    75417 Mühlacker

    Phone: +49 7041 9530-0
    Fax: +49 7041 9530-30
    Email: info@heinrich-meier.de
    Web: www.heinrich-meier.de

  • 8 / 16

    Postcode 70 - 73

    Dieter Schätzle GmbH & Co. KG
    Präzisionswerkzeuge
    Unter Haßlen 12
    78532 Tuttlingen

    Phone: +49 7462 9465-0
    Fax: +49 7462 9465-50
    Email: info@schaetzle-werkzeuge.de
    Web:​​​​​​​ www.schaetzle-werkzeuge.de

  • 9 / 16

    Postcode 74, 75

    Heinrich Meier GmbH
    Herrenwaag 31
    75417 Mühlacker

    Phone: +49 7041 9530-0
    Fax: +49 7041 9530-30
    Email: info@heinrich-meier.de
    Web: www.heinrich-meier.de

  • 10 / 16

    Postcode 76 - 79

    Dieter Schätzle GmbH & Co. KG
    Präzisionswerkzeuge
    Unter Haßlen 12
    78532 Tuttlingen

    Phone: +49 7462 9465-0
    Fax: +49 7462 9465-50
    Email: info@schaetzle-werkzeuge.de
    Web:​​​​​​​ www.schaetzle-werkzeuge.de

  • 11 / 16

    Postcode 80 - 87

    AB1-Tools e.K.
    Goethering 45
    91732 Merkendorf

    Phone: +49 9826 333-2241
    Fax: +49 9826 333-3691
    Email: info@ab1-tools.com
    Web: www.ab1-tools.com

  • 12 / 16

    Postcode 88, 89

    Dieter Schätzle GmbH & Co. KG
    Präzisionswerkzeuge
    Unter Haßlen 12
    78532 Tuttlingen

    Phone: +49 7462 9465-0
    Fax: +49 7462 9465-50
    Email: info@schaetzle-werkzeuge.de
    Web:​​​​​​​ www.schaetzle-werkzeuge.de

  • 13 / 16

    Postcode 90 - 97

    AB1-Tools e.K.
    Goethering 45
    91732 Merkendorf

    Phone: +49 9826 333-2241
    Fax: +49 9826 333-3691
    Email: info@ab1-tools.com
    Web: www.ab1-tools.com

  • 14 / 16

    Danmark

    EDECO TOOL APS 
    Naverland 2
    2600 Glostrup
    Danmark

    Phone: +45 7060 2029
    Email: info@edeco.dk
    Web: www.edeco.dk

  • 15 / 16

    Italy

    TEKNOS S.r.l.
    Via A. Pigafetta, 2
    35011 Campodarsego (PD)
    Italia

    Phone: +39 049 8877061
    Email: info@teknositalia.it
    Web: www.teknositalia.it

  • 16 / 16

    Portugal

    Álamo-Ferramentas Unipessoal Lda
    Rua da ETAR, Lote 9
    Zona Industrial de Oiã
    3770-059 Oiã
    ​​​​​​​​​​​​​​
    Phone: +351 234 728-193
    Email: geral@alamo-ferramentas.com