Machining small and large bores

There is a wide range of full bore operations in the die & mould sector: From large bores for guide pillars and deep bores for the cooling system to high-precision bores for ejector pins. MAPAL offers a comprehensive portfolio of drilling and reaming tools for the individual production steps.
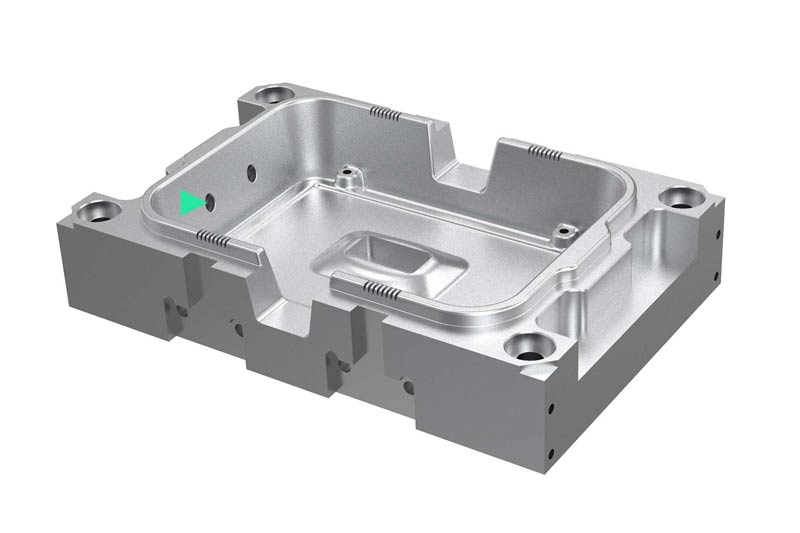
On a rendered example component, an operation is highlighted.
Tool overview for the following machining steps:
  1. Piloting
  2. Drilling from solid
  3. Deep hole drilling
  4. Reaming
  5. Countersinking

Pilotieren

Tiefe Bohrungen für Kühlsysteme sind hauptsächlich im Bereich der Kunststoffinjektion sehr verbreitet. Um eine gute Führung für extra lange Bohrwerkzeuge zu erhalten, empfiehlt sich eine Pilotierung der Bohrungen mit entsprechend kürzeren Werkzeugen. MAPAL liefert hier nicht nur die richtigen Produkte, sondern auch den entsprechend professionellen Support, um die Ziele in Sachen Rundheit und Präzision sicherzustellen.
Da die Bohrprozesse häufig auch an schrägen Oberflächen durchgeführt werden, vermeiden Anwender mit der Pilotierung der Bohrung ein Biegen und Brechen der Werkzeuge.
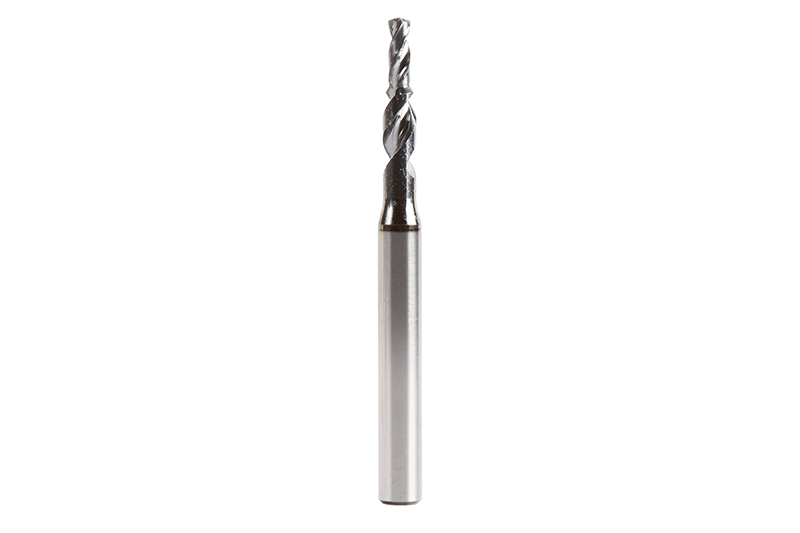
  • MEGA-Pilot-Drill

    VHM-Pilotbohrer
    • Pilotbohrer für tiefe Bohrungen bei kleinen Durchmessern in Stahl und Gusseisen
    • Optimal abgestimmt auf Tiefbohrer MEGA-Deep-Drill
    • Erhöht die Positionsgenauigkeit der Bohrung 
    • Erhältlich im Durchmesserbereich 1-3 mm

  • Tritan-Spot-Drill-Steel

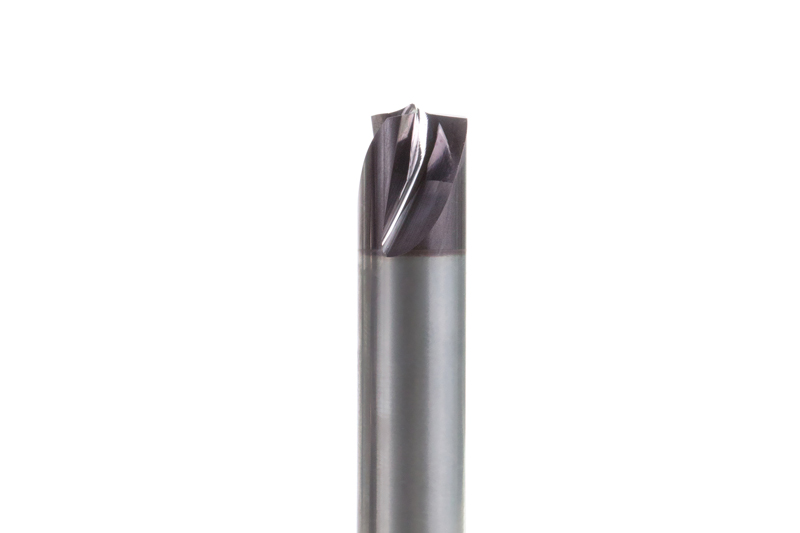
    NC pilot drill
    • Three-edged NC pilot drill for steel
    • Perfectly coordinated with the Tritan-Drill-Steel
    • Also suitable for difficult drilling situations
    • Offered in the diameter range 4-20 mm


Drilling from solid

Due to the multitude of bore sizes and features, the die & mould sector offers a wide range of solid drilling tools. Tap drills, guide bores for ejector pins and partial pin holes are just a few application examples.
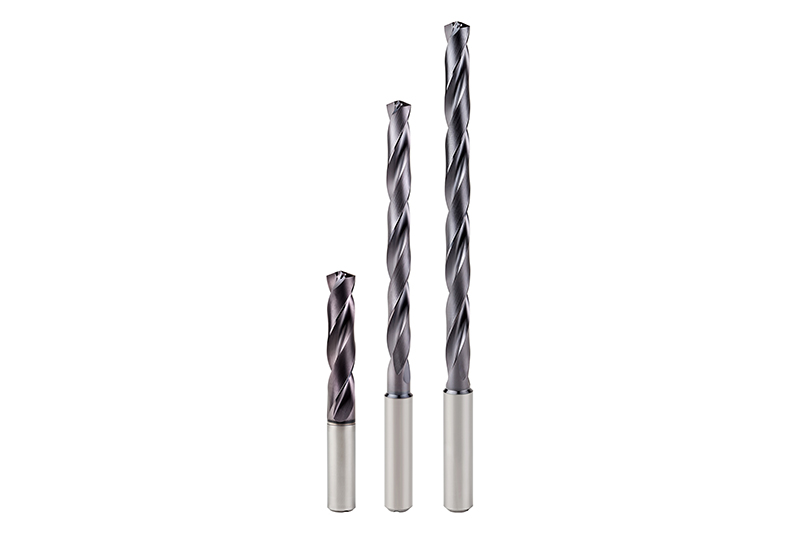
  • ECU-Drill-Steel

    Solid carbide twist drill
    • Double edge twist drill with a wide range of applications
    • Highly economical machining of steel
    • Universal application
    • Proven geometries for high precision and process reliability
    • Good chip formation and chip removal

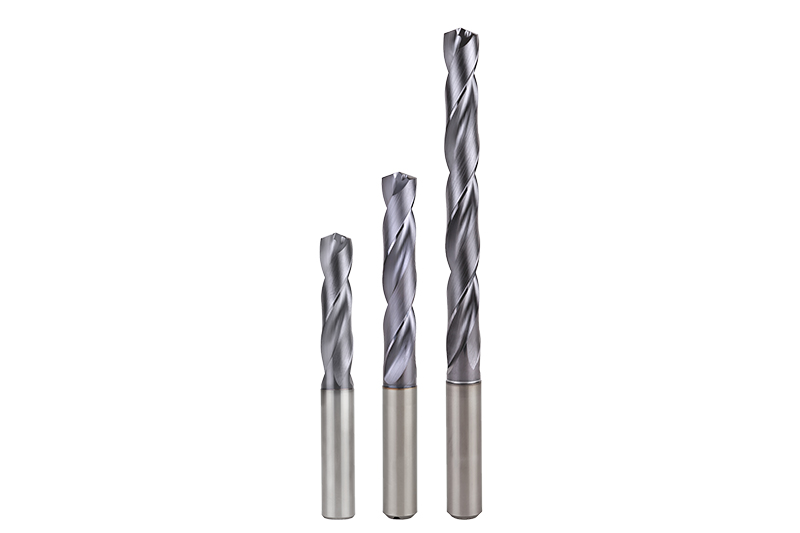
  • MEGA-Drill-Steel-Plus

    Solid carbide high-performance twist drill
    • Double edge high-performance twist drill for maximum productivity in steel machining
    • Optimised chip groove geometry
    • Modified cutting edge preparation
    • 30% more performance through cutting speed and feed rate compared to MEGA-Drill-Steel

  • MEGA-Drill-Hardened

    Solid carbide twist drill
    • Process-reliable machining of hardened workpiece materials up to 65 HRC
    • Coordinated micro and macro geometry for hard machining
    • New carbide substrate for maximum resistance to wear
    • Extremely temperature-resistant coating

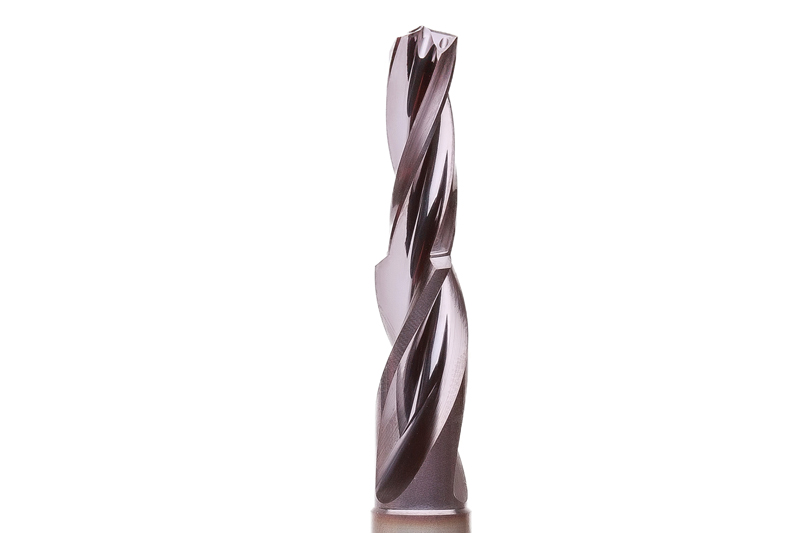
  • Tritan-Drill-Steel

    Solid carbide high-performance twist drill
    • Three-edged geometry enables significantly higher feed rates and a significantly longer tool life
    • High position accuracy even in difficult machining situations
    • Self-centring chisel edge
    • Tapping at an angle possible up to max. 12°
    • Safe chip removal due to the spherical shape of main cutting edge

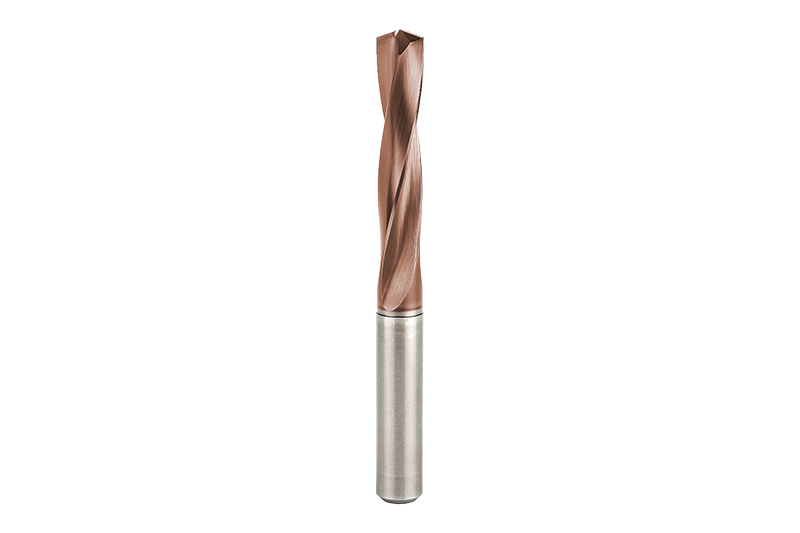
  • MEGA-Drill-Reamer

    Solid carbide drill reamer
    • Two working steps – drilling and reaming – combined in a single tool
    • Optimised reaming cutting edge
    • Reduction of productive and non-productive times
    • Bore tolerance ≥ IT7

  • Indexable insert drill - QTD Steel

    Indexable insert drill
    • Cost-effective system with indexable inserts that can be swapped out for steel machining
    • Hardened steel holder with coiled cooling channels
    • High degree of radial run-out accuracy
    • Very good chip formation and safe chip removal

  • Tritan-Step-Drill-Steel

    Solid carbide step drill
    • Three edge step drill for thread sizes from M5 to M16
    • With 90° countersink
    • Self-centring chisel edge
    • Maximum positional accuracy
    • Best chip breakage properties


Deep hole drilling

Deep drilling up to 40 and 50xD is very common in the die & mould sector. This type of drilling requires specialised tools. The most common are single-lip drills, with these tools being used on special drilling machines. Solid carbide drills are a real alternative for small and medium-sized components with bore diameters of up to 12 mm. The deep hole drills are equipped with two guiding chamfers and thus ensure good guidance in the bore.
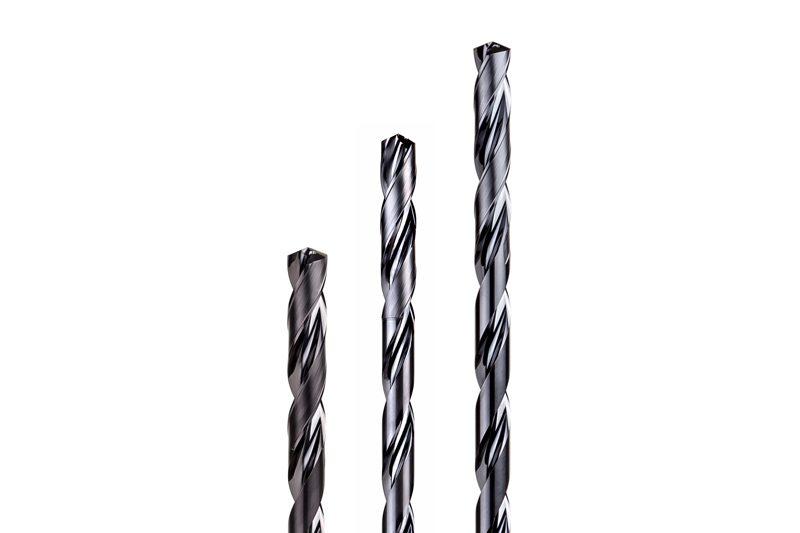
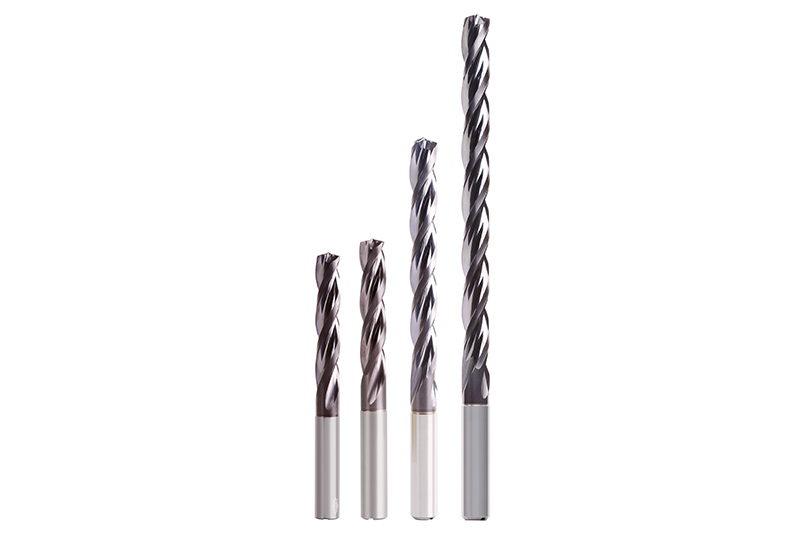
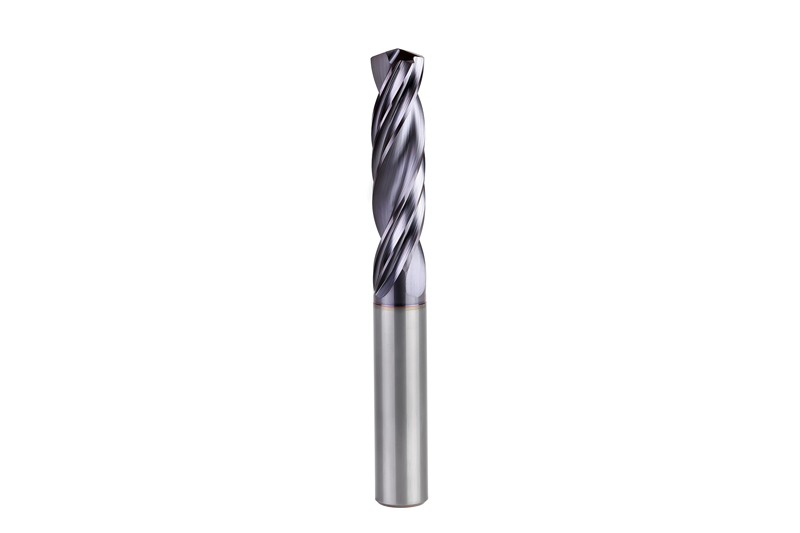
  • MEGA-Deep-Drill

    Solid carbide deep drill
    • Process-reliable and efficient production of deep bores up to 40xD
    • Up to 80 percent shorter machining times compared to single-lip drills
    • Self-centring chisel edge
    • Four guiding chamfers for high bore quality


Reaming

The bores for certain pins and positions require a high degree of accuracy in terms of roundness and diameter. A final reaming process is therefore mandatory. The pre-machining of these bores must also meet the requirements of the reaming tools in order to achieve the desired results.

Decades of expertise at MAPAL means a wide range of available products that are individually selected for specific requirements.
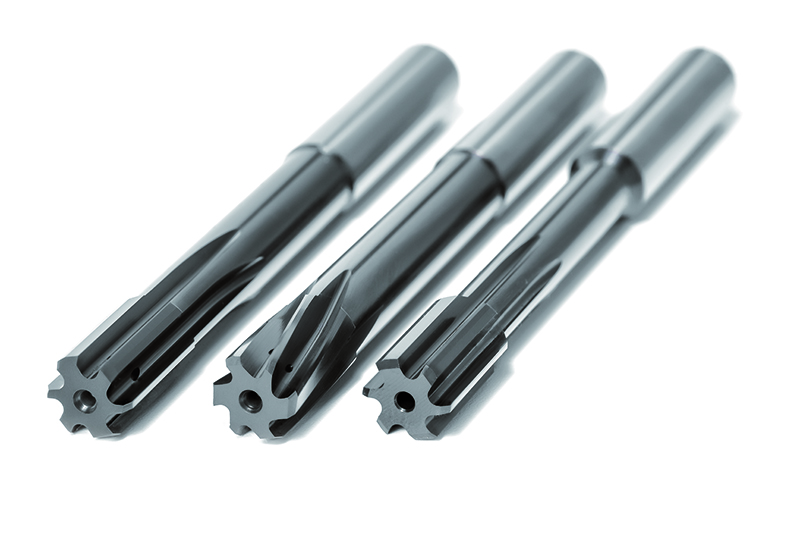
  • MEGA-Drill-Reamer

    Solid carbide drill reamer
    • Two working steps – drilling and reaming – combined in a single tool
    • Optimised reaming cutting edge
    • Reduction of productive and non-productive times
    • Bore tolerance ≥ IT7

  • FixReam FXR

    Solid carbide high-performance reamers
    • Fine machining of bores in H7 tolerance
    • Highly economical machining of steel and cast iron
    • For through holes and blind bores
    • High feed rate via 4 to 8 cutting edges

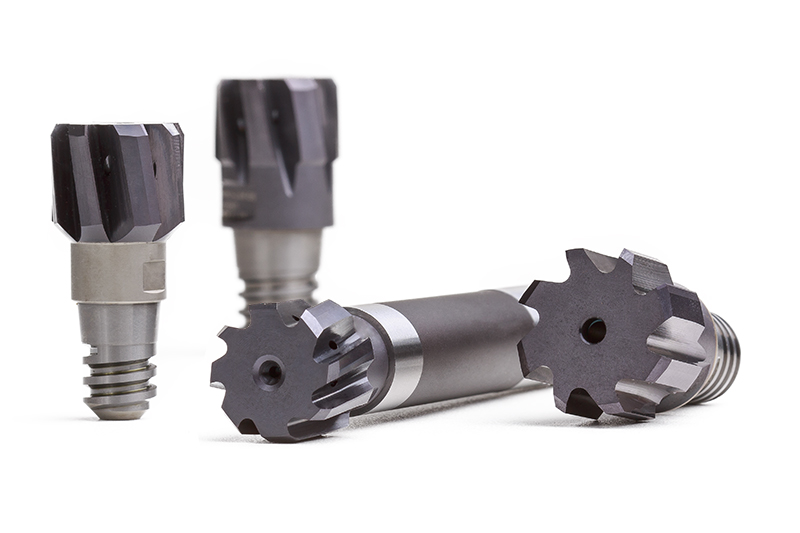
  • CPReam CPR

    Solid carbide replaceable head reamers
    • Economical replaceable head system with CFS connection
    • Fine machining of bores in H7 tolerance
    • For through holes and blind bores
    • Highly precise radial run-out accuracy of 5 μm

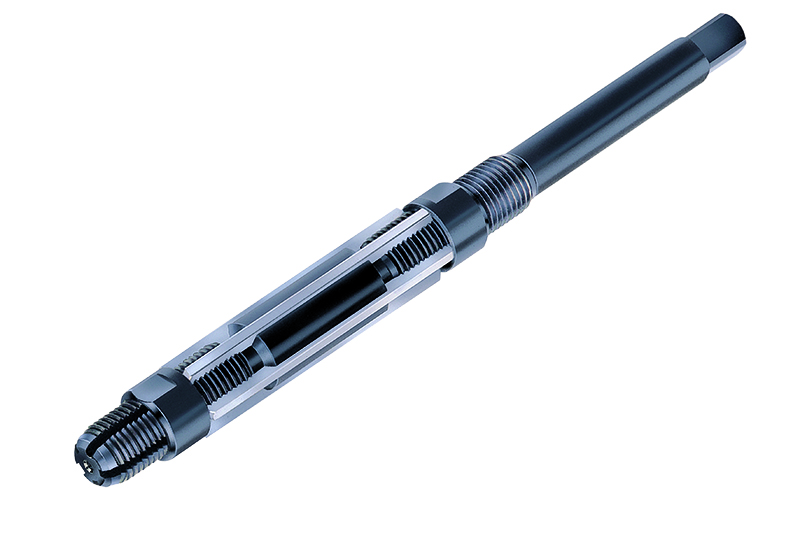
  • Quick-adjustable reamer WN50

    Hand reamers
    • Quick-adjustable hand reamer
    • Especially suitable for repair work
    • Easy to handle
    • Wide adjustment range


Senken

Jede Bohrung wird in der Regel mit einem Kegelsenker an der Kante vorbearbeitet. Senken ist eine einfache Anwendung, jedoch weisen manche Bohrungen spezielle Anforderungen an die Oberflächenqualität auf. Die gängigen Werkzeuge sind aus Vollhartmetall, aber auch aus HSS. Die innovativen Kegelsenker von MAPAL bieten auch für die Senkoperationen Vorteile durch eine bessere Leistung und höhere Oberflächenqualitäten.
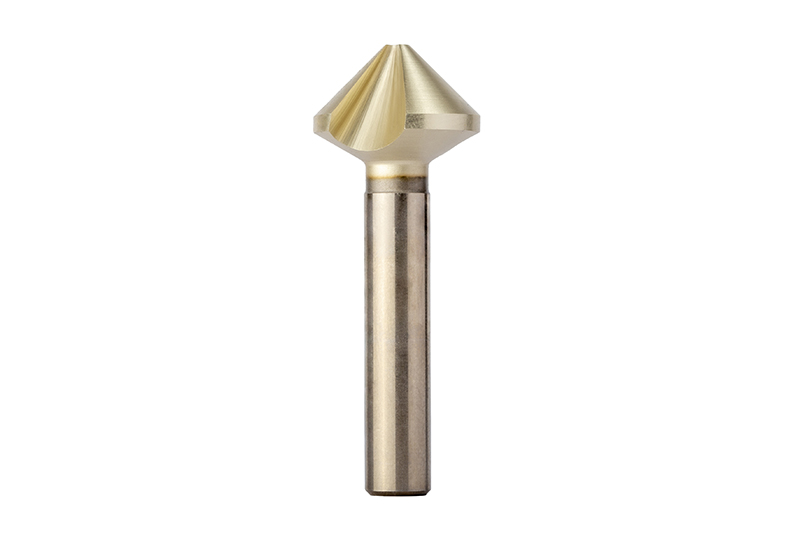
  • Kegelsenker 90°

    HSS-/VHM-Kegelsenker
    • Präzisionskegelsenker 90° mit Ungleichteilung
    • Höhere Genauigkeit und verbesserte Oberflächenwerte 
    • Reduzierte Axial- und Radialkräfte
    • Deutlich weniger Vibrationen
    • Erhöhte Schnittparameter für höchste Produktivität