27.06.2023
CFRP machining optimised
Optimum process reliability with the OptiMill-Composite-Speed-Plus
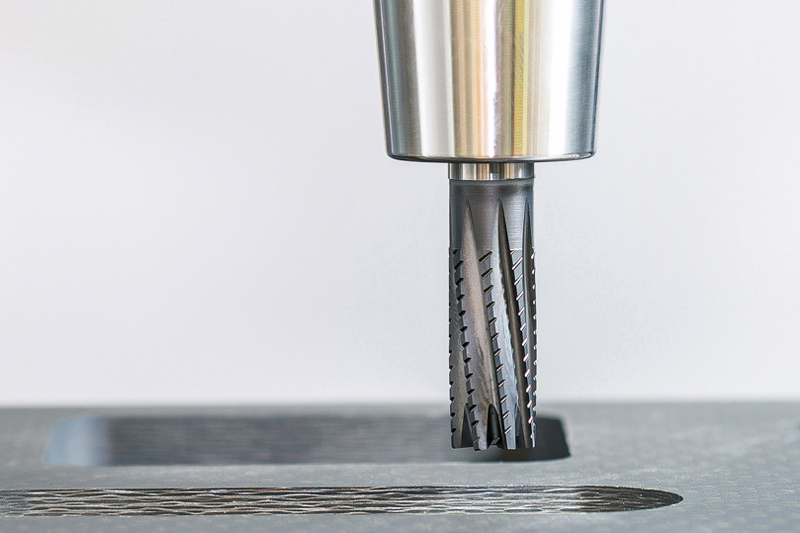
Improved workpiece clamping for large carbon-fibre parts enables the aerospace industry to machine more quickly. MAPAL supports this development with new tools. With its diamond coating and optimised geometry, the OptiMill-Composite-Speed-Plus guarantees process reliability.
The aerospace industry is reluctant to change functioning processes that have already been audited due to the large effort involved. However, growing cost pressures are also forcing this sector to make its production as efficient as possible. Aircraft manufacturers have so far identified the clamping technology as an obstacle on the path to higher performance. Large carbon-fibre parts are usually fixed using vacuum clamping technology. The limited holding forces of the suction cups require relatively low cutting speeds in order to prevent rising vibration. This can lead to a loss of quality and deviations in shape and position tolerances.
New clamping technologies now enable manufacturers to increase the cutting values. But with this came a new problem: under the changed process conditions, there was an increased risk of breakage due to the increased load on milling cutters that had previously worked perfectly. “Even very large manufacturers were affected by tool breakages after using the tools to their limits”, explains Tim Rohmer, Product Manager for solid carbide milling tools at MAPAL. The tool manufacturer saw a need to act and developed the OptiMill-Composite-Speed-Plus as a response to market demands.
Größerer Kern, weniger Spanraum
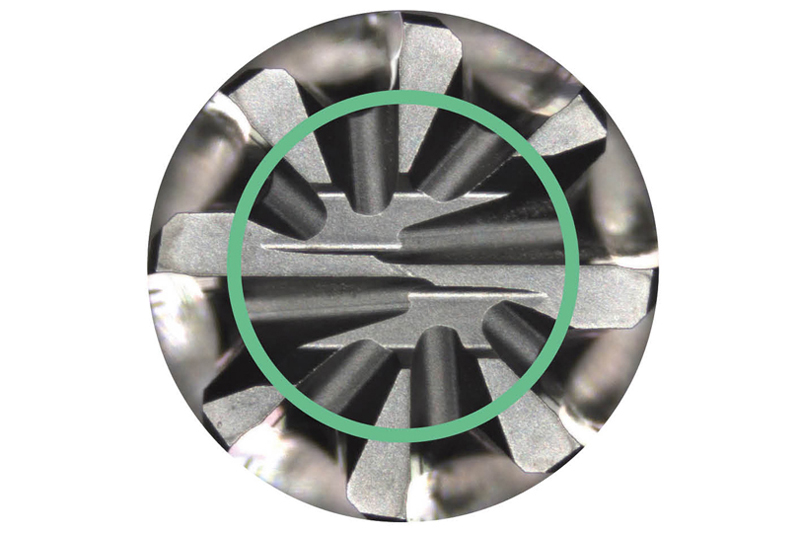
Bei den Anforderungen an das Nutprofil zeigen sich ebenfalls Unterschiede zur Bearbeitung von Metall, wo Vorschub, Zustelltiefe und Schnittbreite die Spandicke beeinflussen. Da der Spanwinkel bei CFK aufgrund eines niedrigen Zahnvorschubs nur gering im Eingriff ist, hat MAPAL den Schneidkeil auf maximale Stabilität ausgelegt.
Zur Verringerung von Hebelkräften und damit für eine erhöhte Bruchresistenz weist der neue OptiMill-Composite-Speed-Plus zudem eine optimierte Hüllkontur auf. In der Praxis kommt man damit gut zurecht, wie Rohmer erläutert: „Typische Bauteile für die Luftfahrt bestehen aus Stacks, also Verbundplatten, bei denen üblicherweise fünf bis 15 mm zerspant werden. Da reichen kürzere Werkzeuge vollkommen aus.“ Waren die Vorgängerwerkzeuge noch länger als in der DIN6527 festgelegt, so entspricht die neue Werkzeugreihe weitestgehend der Norm. MAPAL bietet die Werkzeuge in den Durchmessern von 4 bis 20 mm an.
Gleichmäßige Diamantschicht
Für hohe Standwege bei der Bearbeitung der abrasiven Kohlefasern sorgt der OptiMill-Composite-Speed-Plus zudem mit einer innovativen Diamantbeschichtung. Außergewöhnlich ist dabei die gleichmäßige Schichtdickenverteilung und die hohe Wiederholbarkeit, mit der MAPAL den Diamant im CVD-Verfahren aufbringt. Herkömmliche Beschichtungstechnologien erzeugen häufig unregelmäßige Schichten, die an der Spitze dicker sind als hinten an der Schneide. Dieser Verlauf sorgt für unterschiedliche Kantenverrundungen und damit schwankenden Schnittdruck und Verschleiß.
Die über die Schneidenlänge homogene Schichtdicke trägt zur Prozesssicherheit bei. Das ermöglicht eine gleichbleibende Performance unabhängig davon, welche Stelle der Schneide im Eingriff ist. Damit sind die Werkzeuge auch höhenunabhängig zur Umfangbearbeitung eines Stacks einsetzbar: Anwender nutzen den Fräser teilweise bis zum Verschleißende, setzt ihn dann nach und arbeitet mit einem frischen Teil der Schneide weiter. Der Eckfräser eignet sich für ein breites Anwendungsfeld. Neben der Umfangsbearbeitung werden mit ihm auch Nuten, Kanten und Taschen erzeugt.
Pull or push: improvements of up to 30 percent
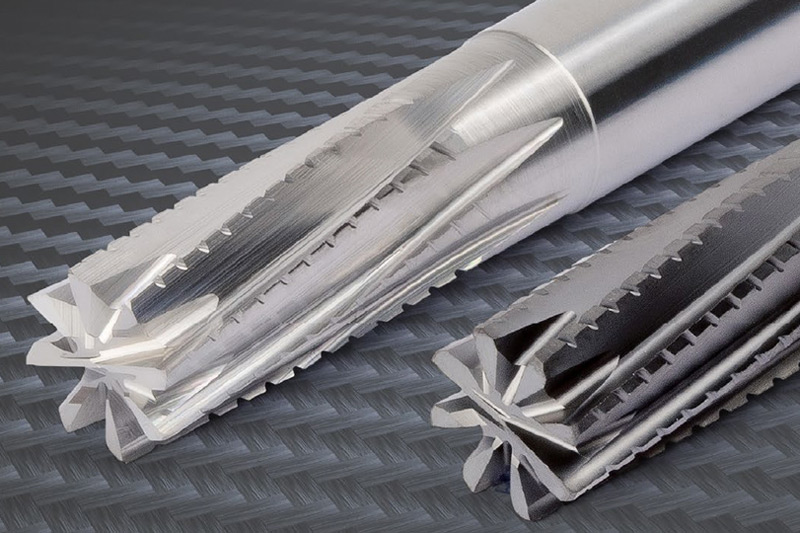
One aspect of CFRP machining is that the tools available today produce different machining qualities on the workpieces. The user must decide which quality requirements are placed on the part according to the existing material composite and therefore make the ideal tool selection. It is often connection points for which particularly neat edges are required. MAPAL provides two different variants of its milling cutters. The right-hand spiral model produces a pulling effect and thus axial tensile forces, while the left-hand spiral variant has a pushing effect and thus forms compressive forces in the axial direction. The fibre catchers counteract the force created by the respective spiralisation.
The previous model had a third, neutral variant. With further development, this variant is no longer required as the new tools reduce the axial forces by up to 40 percent. As such, the two versions of the new product also assume all tasks for which the neutral variant was previously used. In terms of tool life, quiet running, productivity and cutting quality, the new tools are up to 30 percent better than their predecessors.
Whilst the aviation industry is still recovering from the coronavirus slump, the use of CFRP is growing rapidly in other areas. In addition to automotive engineering and racing, the focus here is shifting to the consumer sector. Manufacturers of sports equipment such as bicycles, skis, snowboards or fishing rods increasingly use the modern material.
With its sharp cutting edges, the OptiMill-Composite-Speed-Plus can also be used to machine thermoplastics and thermosets. As these plastics are not abrasive, coating is not required here and sharp cutting edges are used. The uncoated milling tools replace the previous router tools as they are far superior, especially in terms of cutting quality. MAPAL also recommends the uncoated tools for machining fibreglass materials.
Contact
Kathrin Rehor Public Relations Kathrin.Rehor@mapal.com Phone: +49 7361 585 3342