01.05.2020
For Short Machining Times – Try Whirling Instead of Grinding
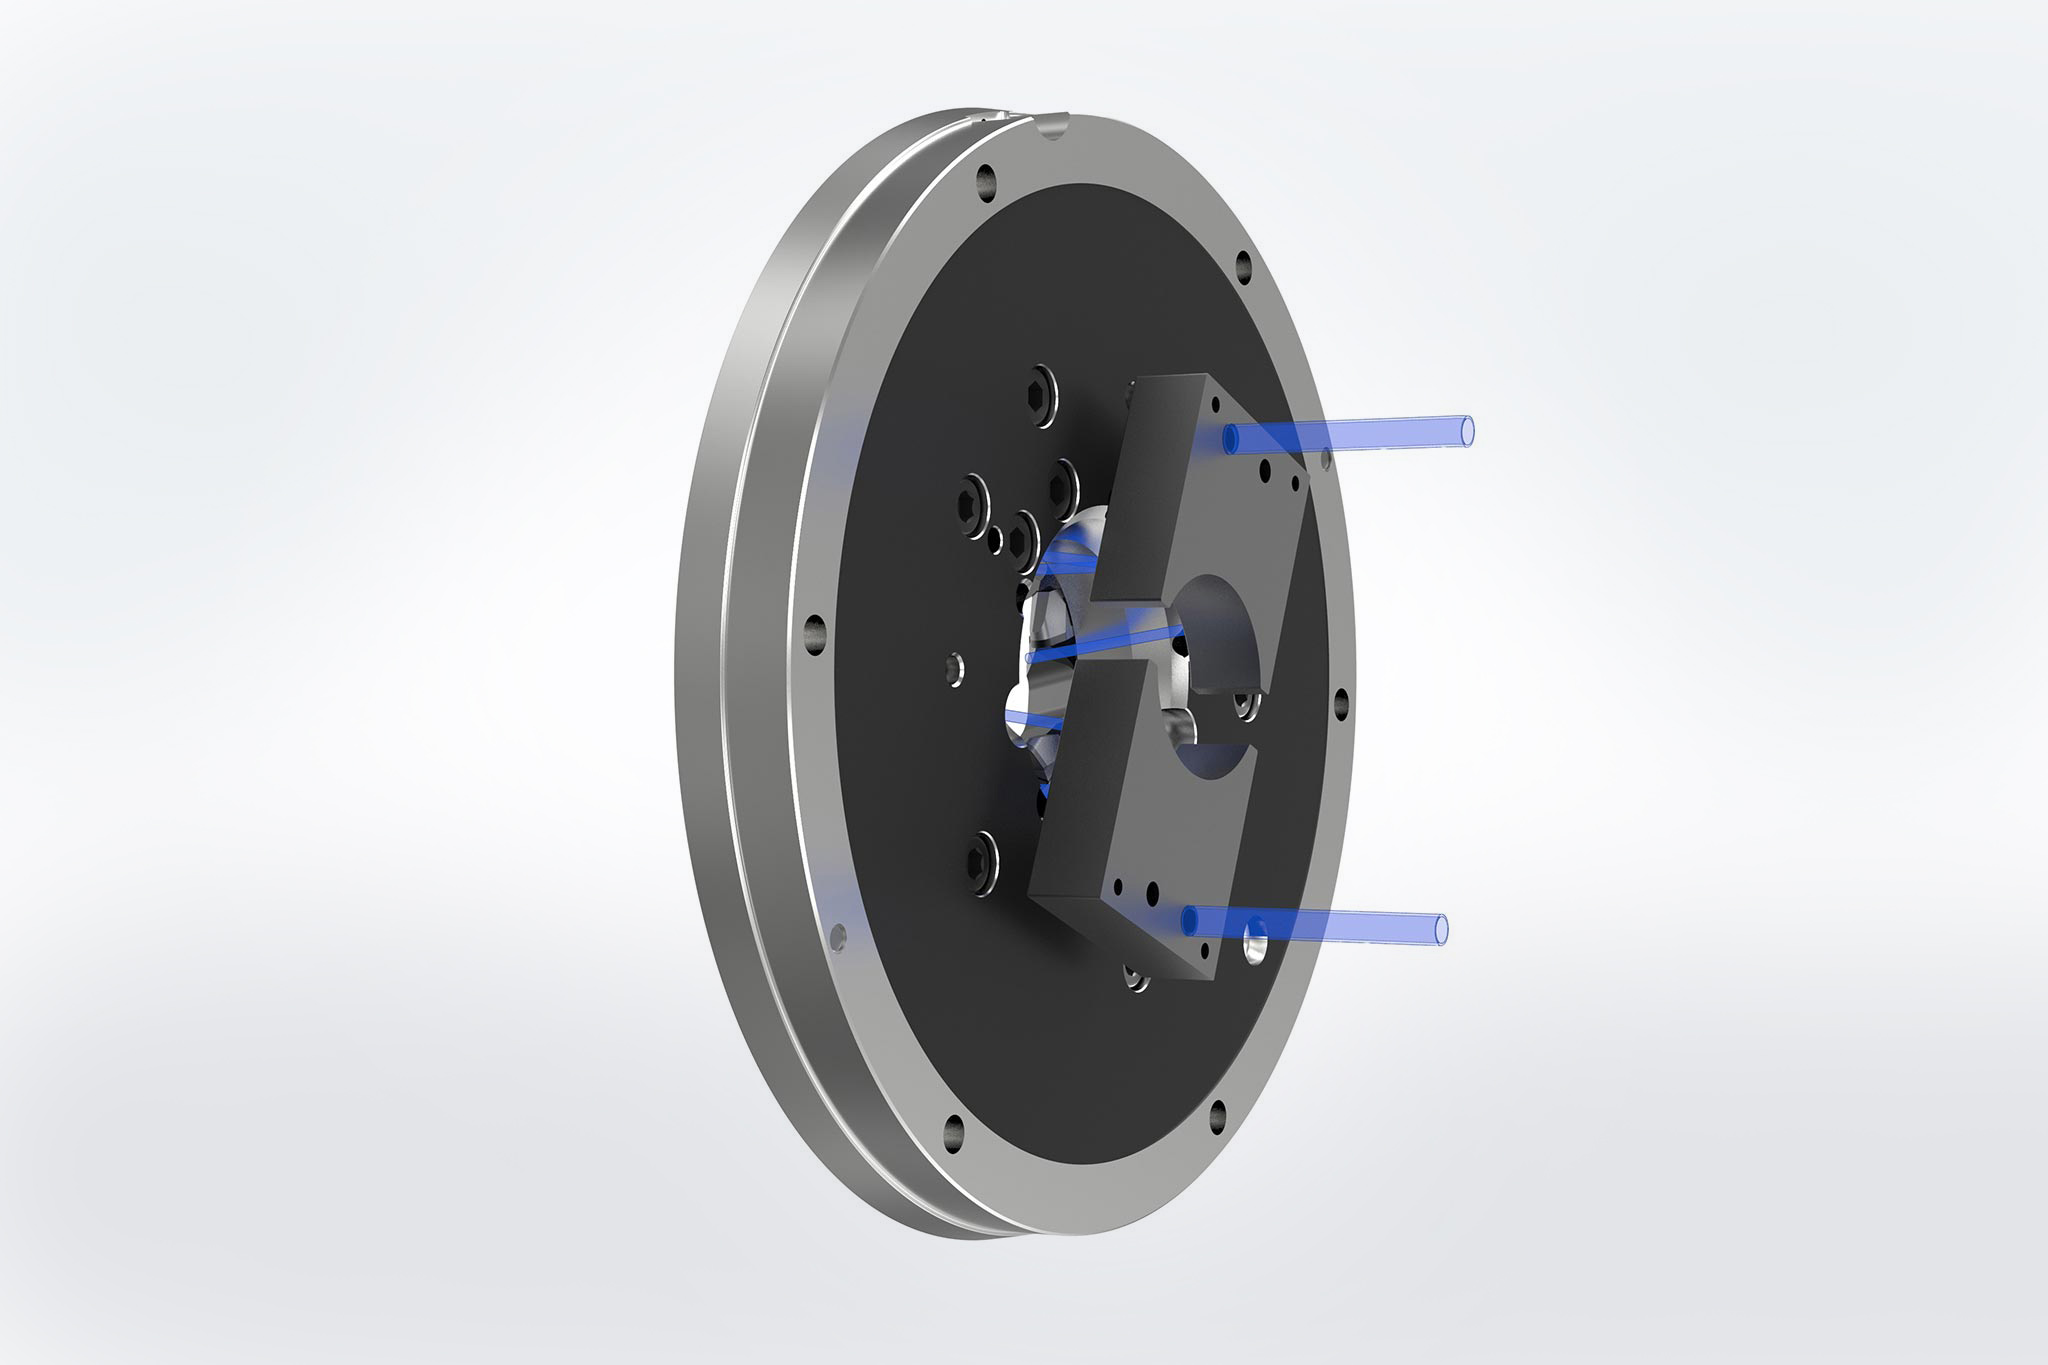
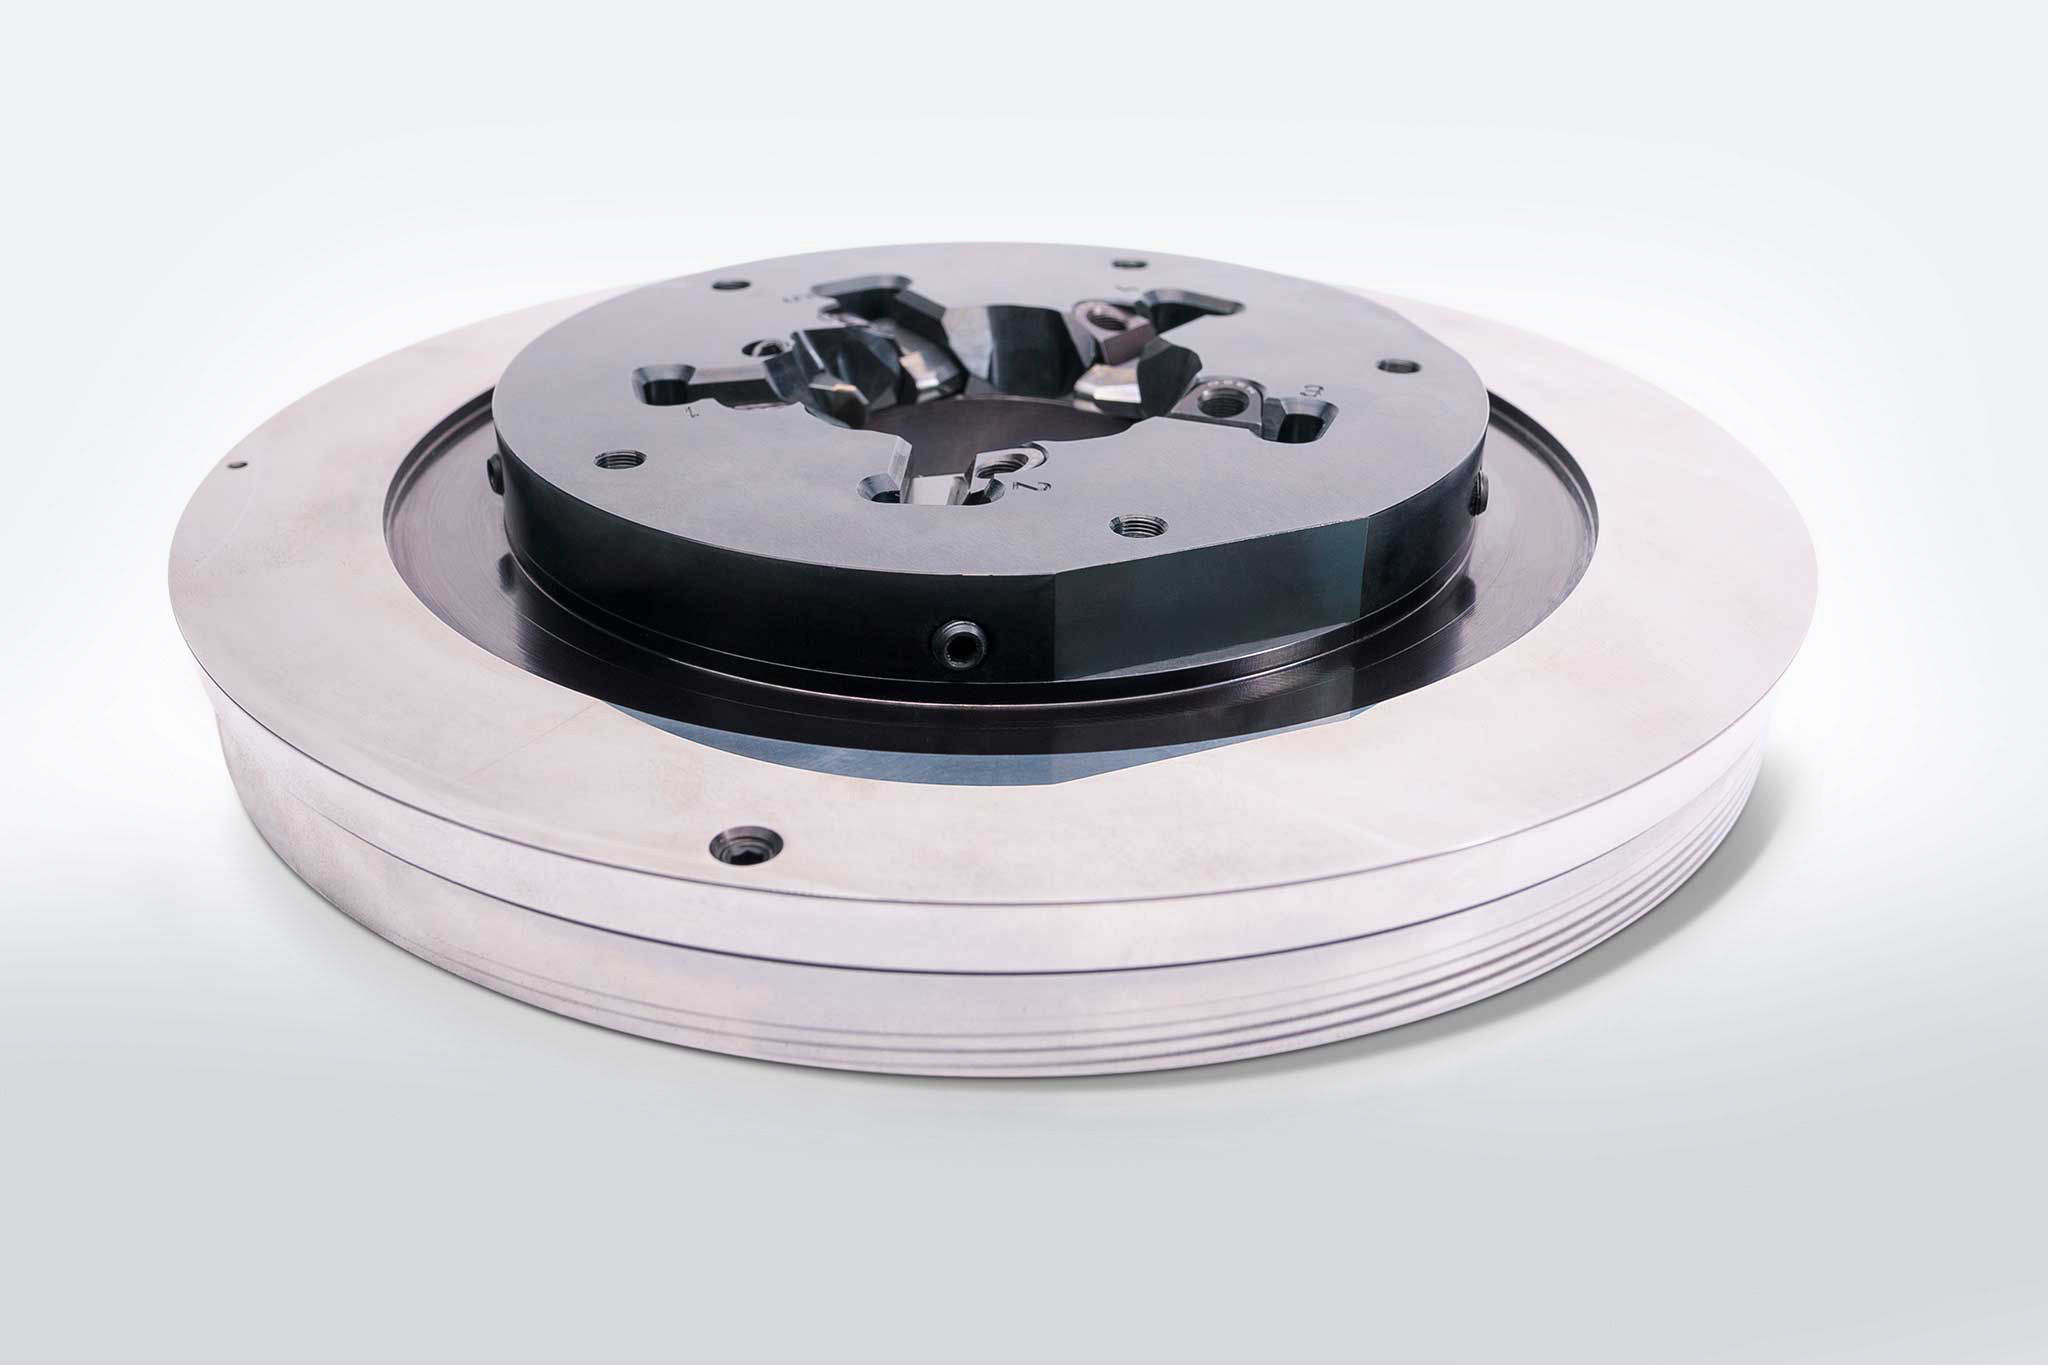
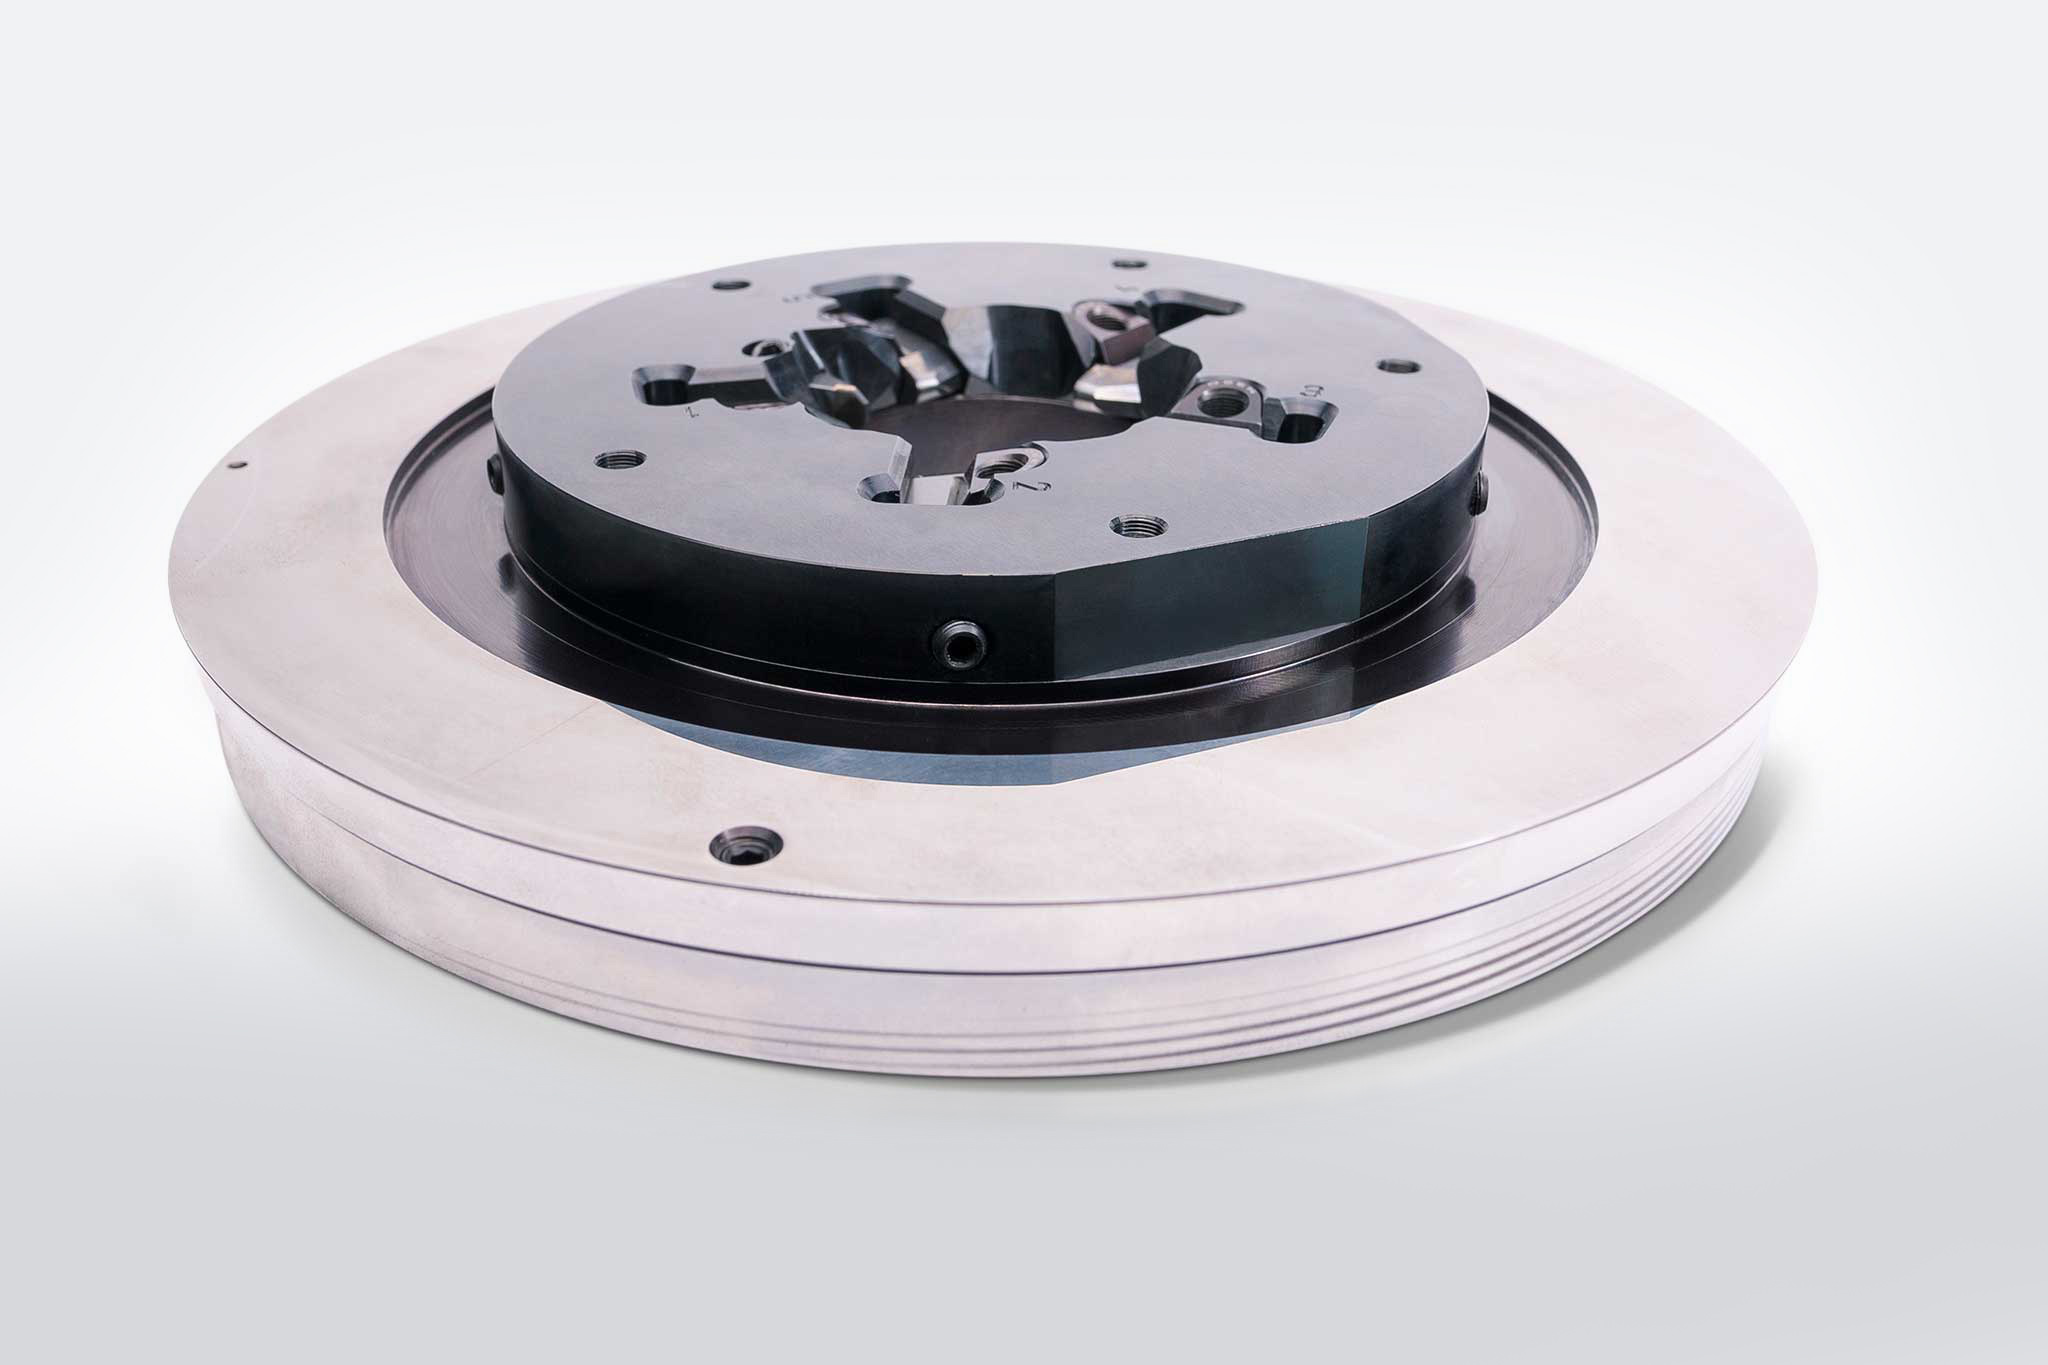
MAPAL presents a tool system in ring form with PcBN-inserts.
On ball castors, which are required for applications such as vehicle steering rods and machine drive systems, the thread profiles are often created by grinding. There is a much quicker way, and that is “whirling”. MAPAL has developed a tool system for hard machining intended for this very purpose, featuring suitable air nozzles to ensure optimised chip removal
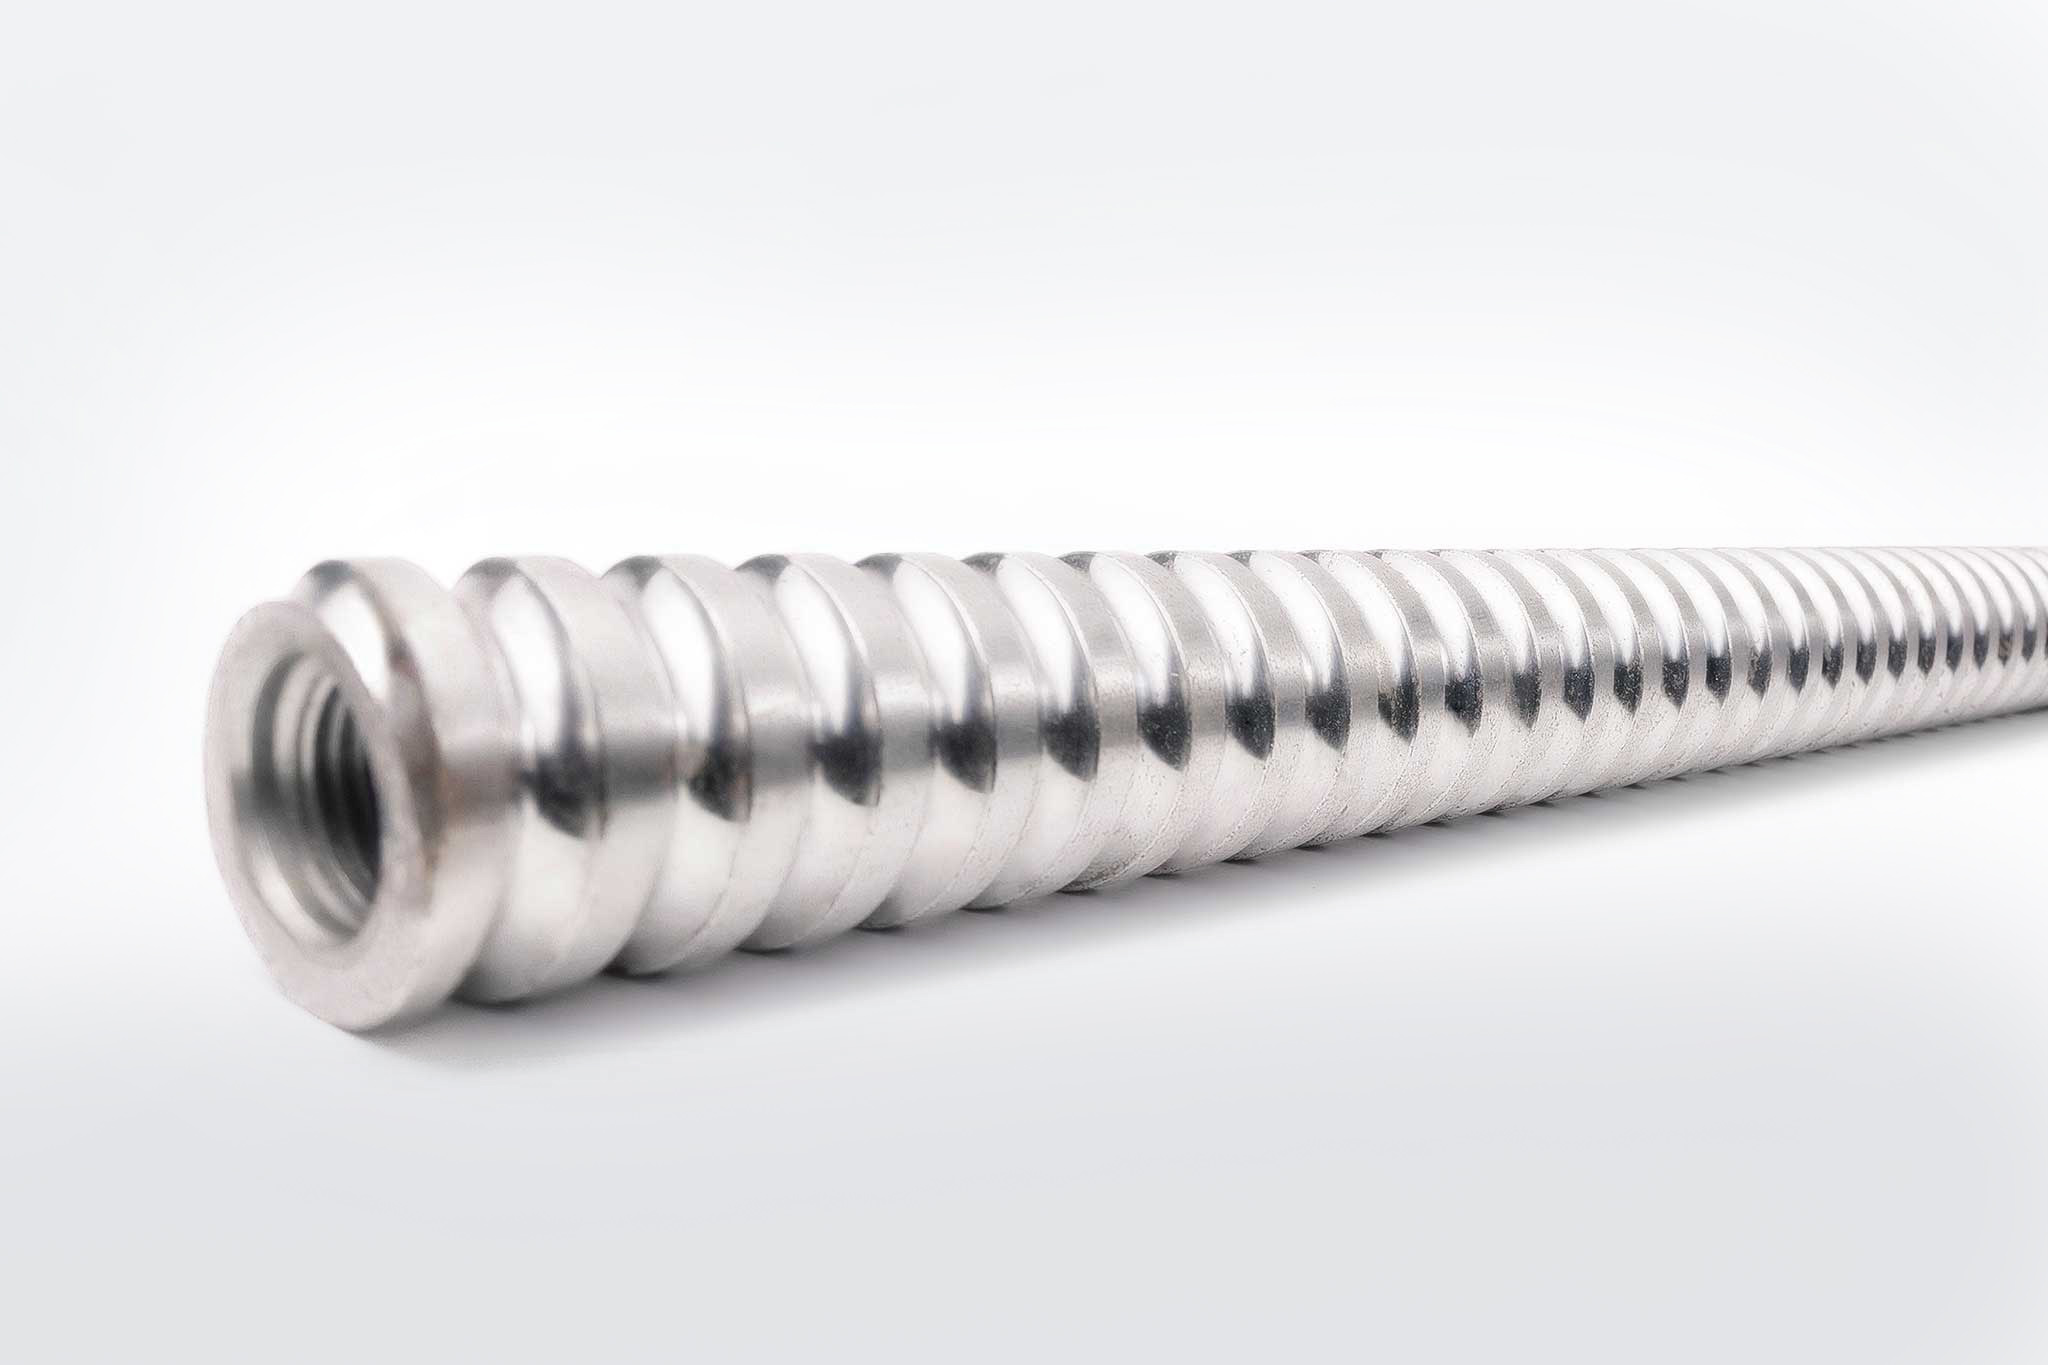

Das Fertigungsverfahren des Wirbelns ist ein besonderes. Kombiniert es doch eine Dreh- mit einer Fräsoperation. Das heißt, nicht nur das Werkzeug dreht sich, sondern zusätzlich rotiert das Werkstück. Aus diesem Grund sind spezielle Maschinen nötig, um zu „wirbeln“. Es stellt sich die Frage, warum Unternehmen auf ein solches Fertigungsverfahren setzen sollten, wenn damit doch die Investition in eine neue Maschine einhergeht. Die Antwort gibt Michael Gebhard, Produktmanagement Hartbearbeitung: „Zwar ist das Schleifen ein bewährtes Verfahren, das Wirbeln allerdings um ein Vielfaches schneller.“ In Zahlen ausgedrückt: „Um das Gewinde einer Zahnstange für eine Lenkung herzustellen, dauert der Schleifprozess über sieben Minuten. Mit Wirbeln wird es in 60 Sekunden fertigbearbeitet“, berichtet er von einem konkreten Anwendungsfall. Bei hohen Stückzahlen an Bauteilen mit Kugelrollgewinden hat sich die Anschaffung einer entsprechenden Maschine für das zerspanende Unternehmen folglich schnell amortisiert.
Als ein Kunde von MAPAL dieses Verfahren einführte, entwickelten die Werkzeugexperten für ihn das entsprechende Werkzeugsystem. Denn beim Außenwirbeln von Kugelrollgewinden im Bereich der Hartbearbeitung werden ähnliche Anforderungen an das Werkzeug gestellt, wie beim Kugelbahnfräsen von homokinetischen Gelenken. „Wir sind seit Jahren einer der führenden Anbieter im Bereich des Kugelbahnfräsens und haben unsere Erfahrung auf das Wirbeln übertragen“, sagt Michael Gebhard. So müssen Zerspaner bei Kugelrollgewinden wie bei Kugelbahnen die Kontur, der Kontaktwinkel und den Schmiegeradius beachten und die Toleranzen prozesssicher einhalten.
Schneidstoff PcBN bestmöglich nutzen
The ring-shaped tool system developed by MAPAL is fitted with PcBN profile indexable inserts and a PcBN indexable insert that creates the chamfers. Various numbers of profile inserts are used depending on the diameter. Although chamfer machining could be integrated into the profile inserts, this would make regrinding much more difficult owing to the significantly more complex shape. The inserts can be reground numerous times to get the most out of the PcBN cutting material.
The indexable inserts, which are directed inwards, are clamped via a specially developed system. “We have based the clamping on that used for our VersaCut system, which has proved its worth in hard grooving with PcBN,” explains Gebhard. The insert is pressed into the insert seat over bevelled edges and clamped effectively using a clamping jaw. Our inserts are clamped directly to the base plate of the tool and not in an additional cassette, which means one connection fewer and thus a positive impact on the axial run-out.
The indexable inserts can be adjusted axially to μm accuracy. “Our system gives us outstanding results in machining”, says Gebhard, “although we have identified some room for improvement with regard to cooling.”
Additiv gefertigte Luftdüsen für prozesssichere Spanabfuhr
Whirling is an air-cooled process. The whirling machines are fitted with two coolant tubes that have to be adjusted to suit each machining operation. “The problem with that is that the tube is easy to move. That means that it occasionally also happens by accident,” says Gebhard. If the air supply tubes move, the chips are not reliably removed during machining, which in a worstcase scenario can result in the cutting edges breaking, but certainly means a much shorter tool life.
MAPAL has developed special air nozzles to prevent this from happening. These can quickly and easily be attached to the machine directly behind the tool system. The nozzles are adjusted to the diameter to be machined. The compressed air is directed through the nozzles and split across several ducts. MAPAL has designed the ducts to ensure that the air is aimed at exactly the right places. This has been made possible by additive manufacturing. “With this, we can ensure an optimized air supply and thus chip removal,” says Gebhard, “which means that we can offer our customers a complete package to whirl ball castors quickly and reliably.”