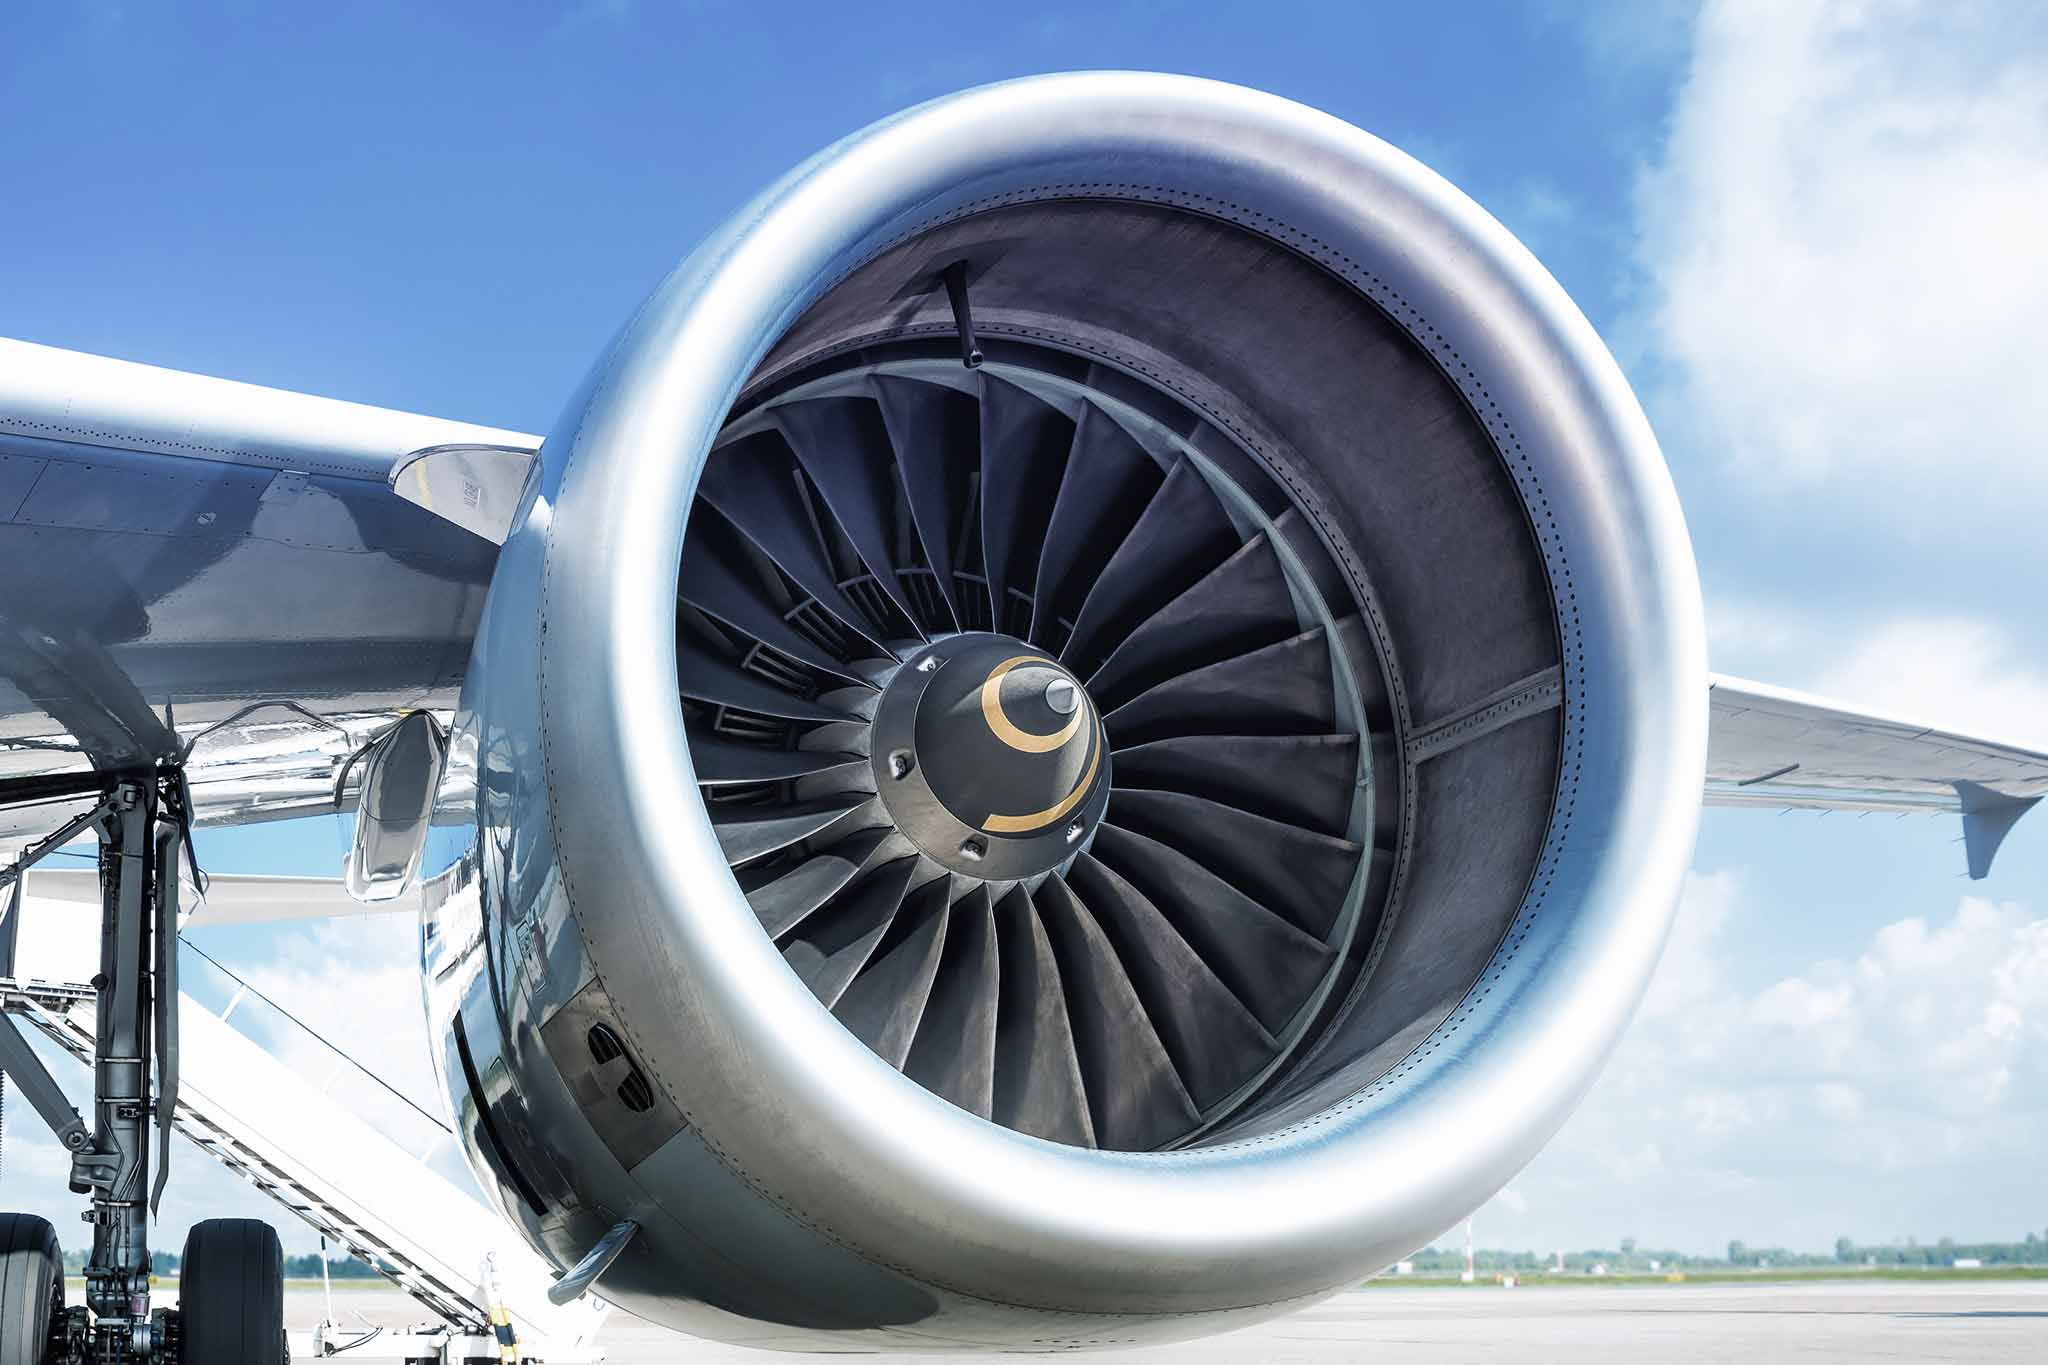
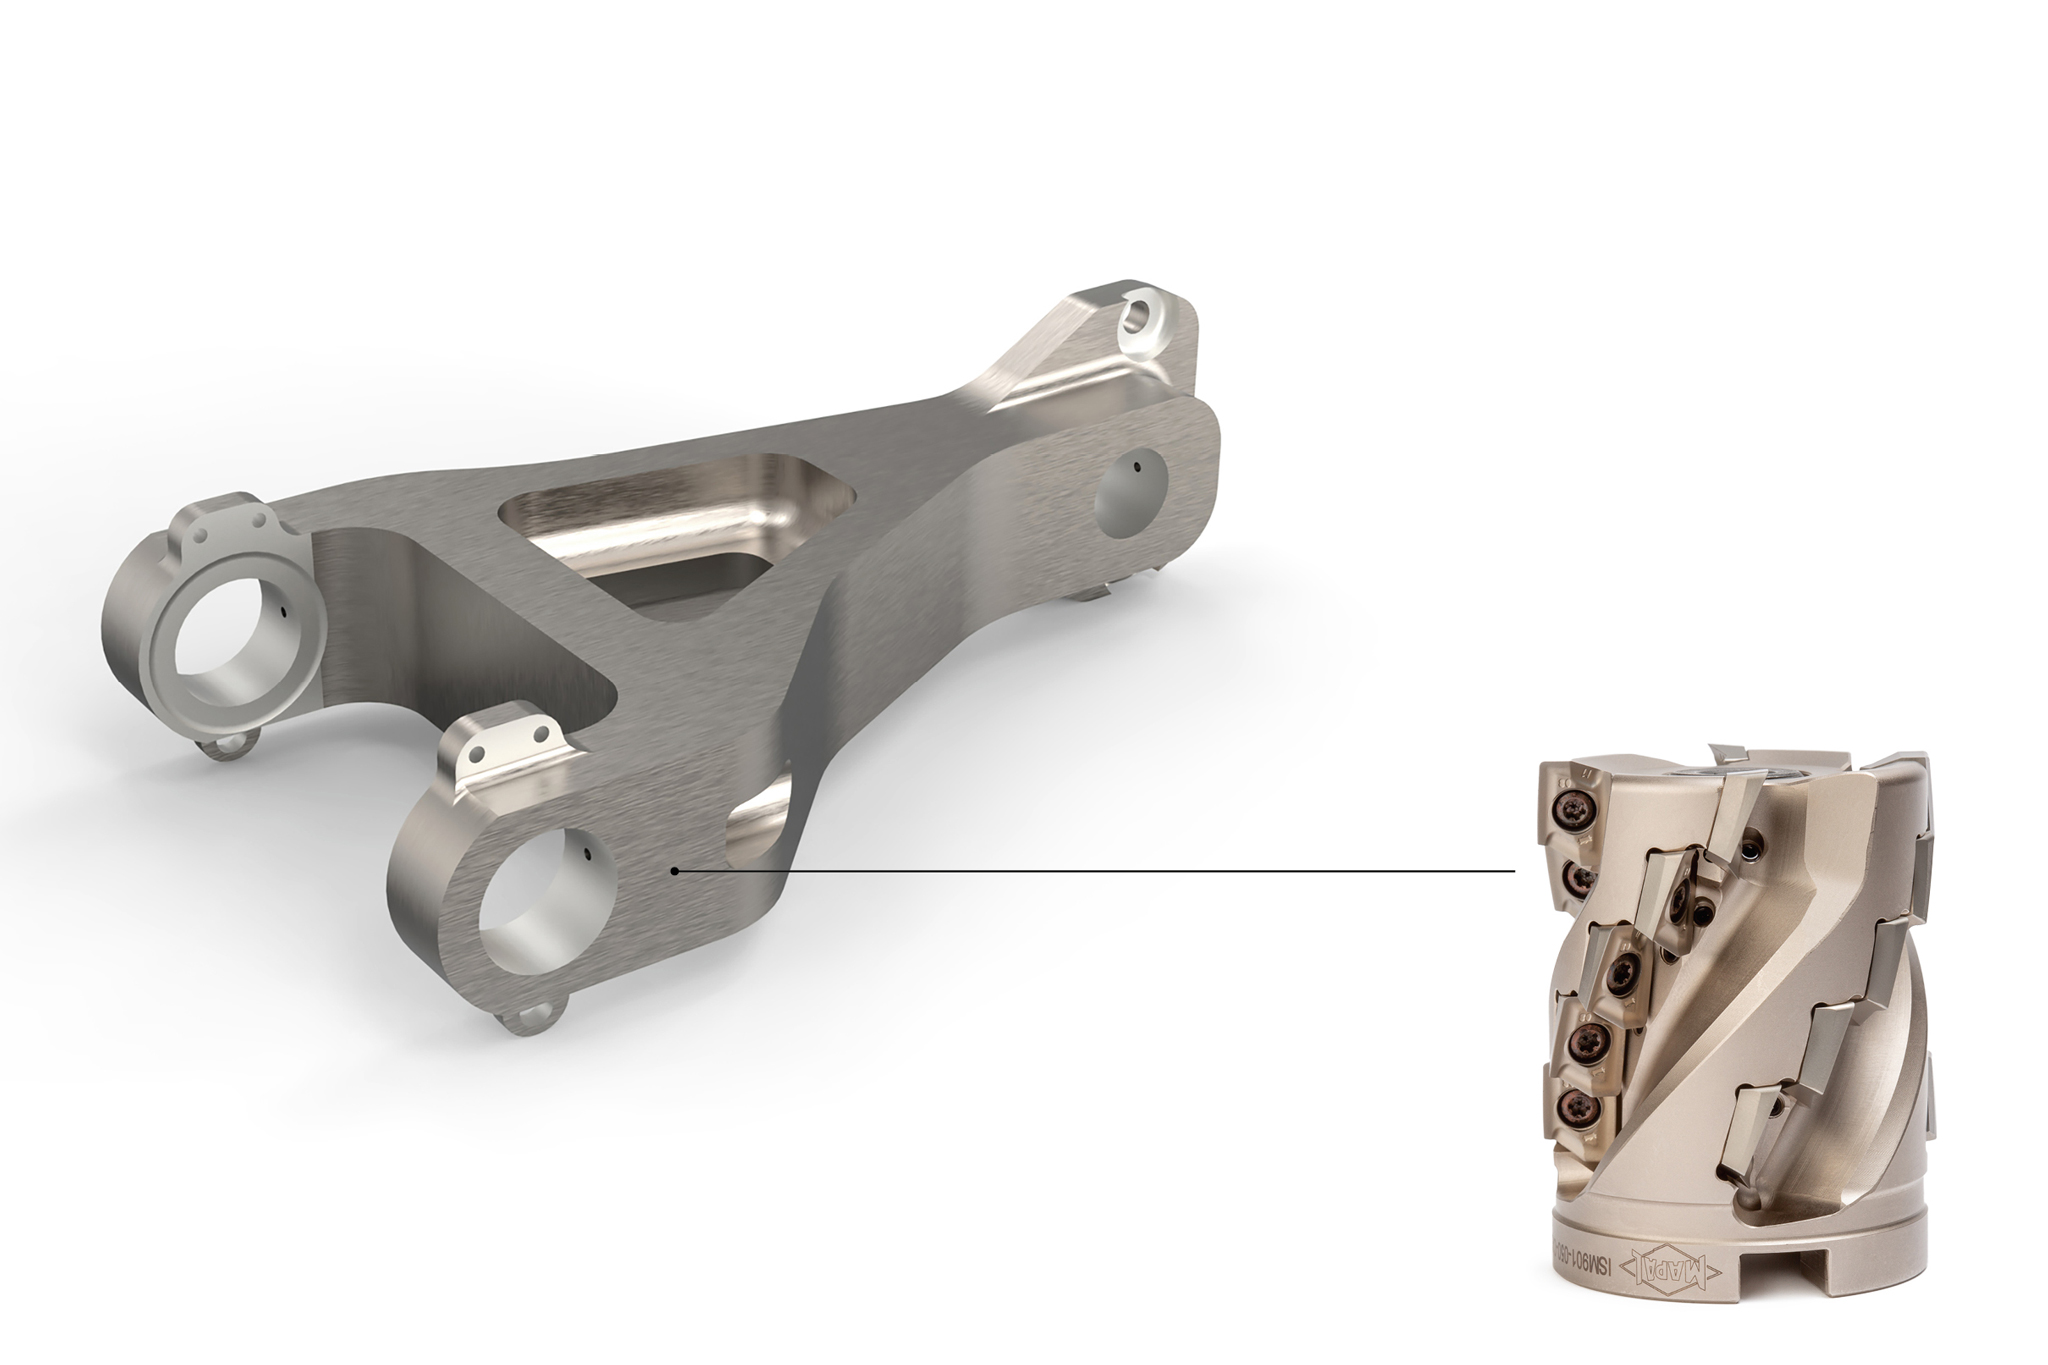
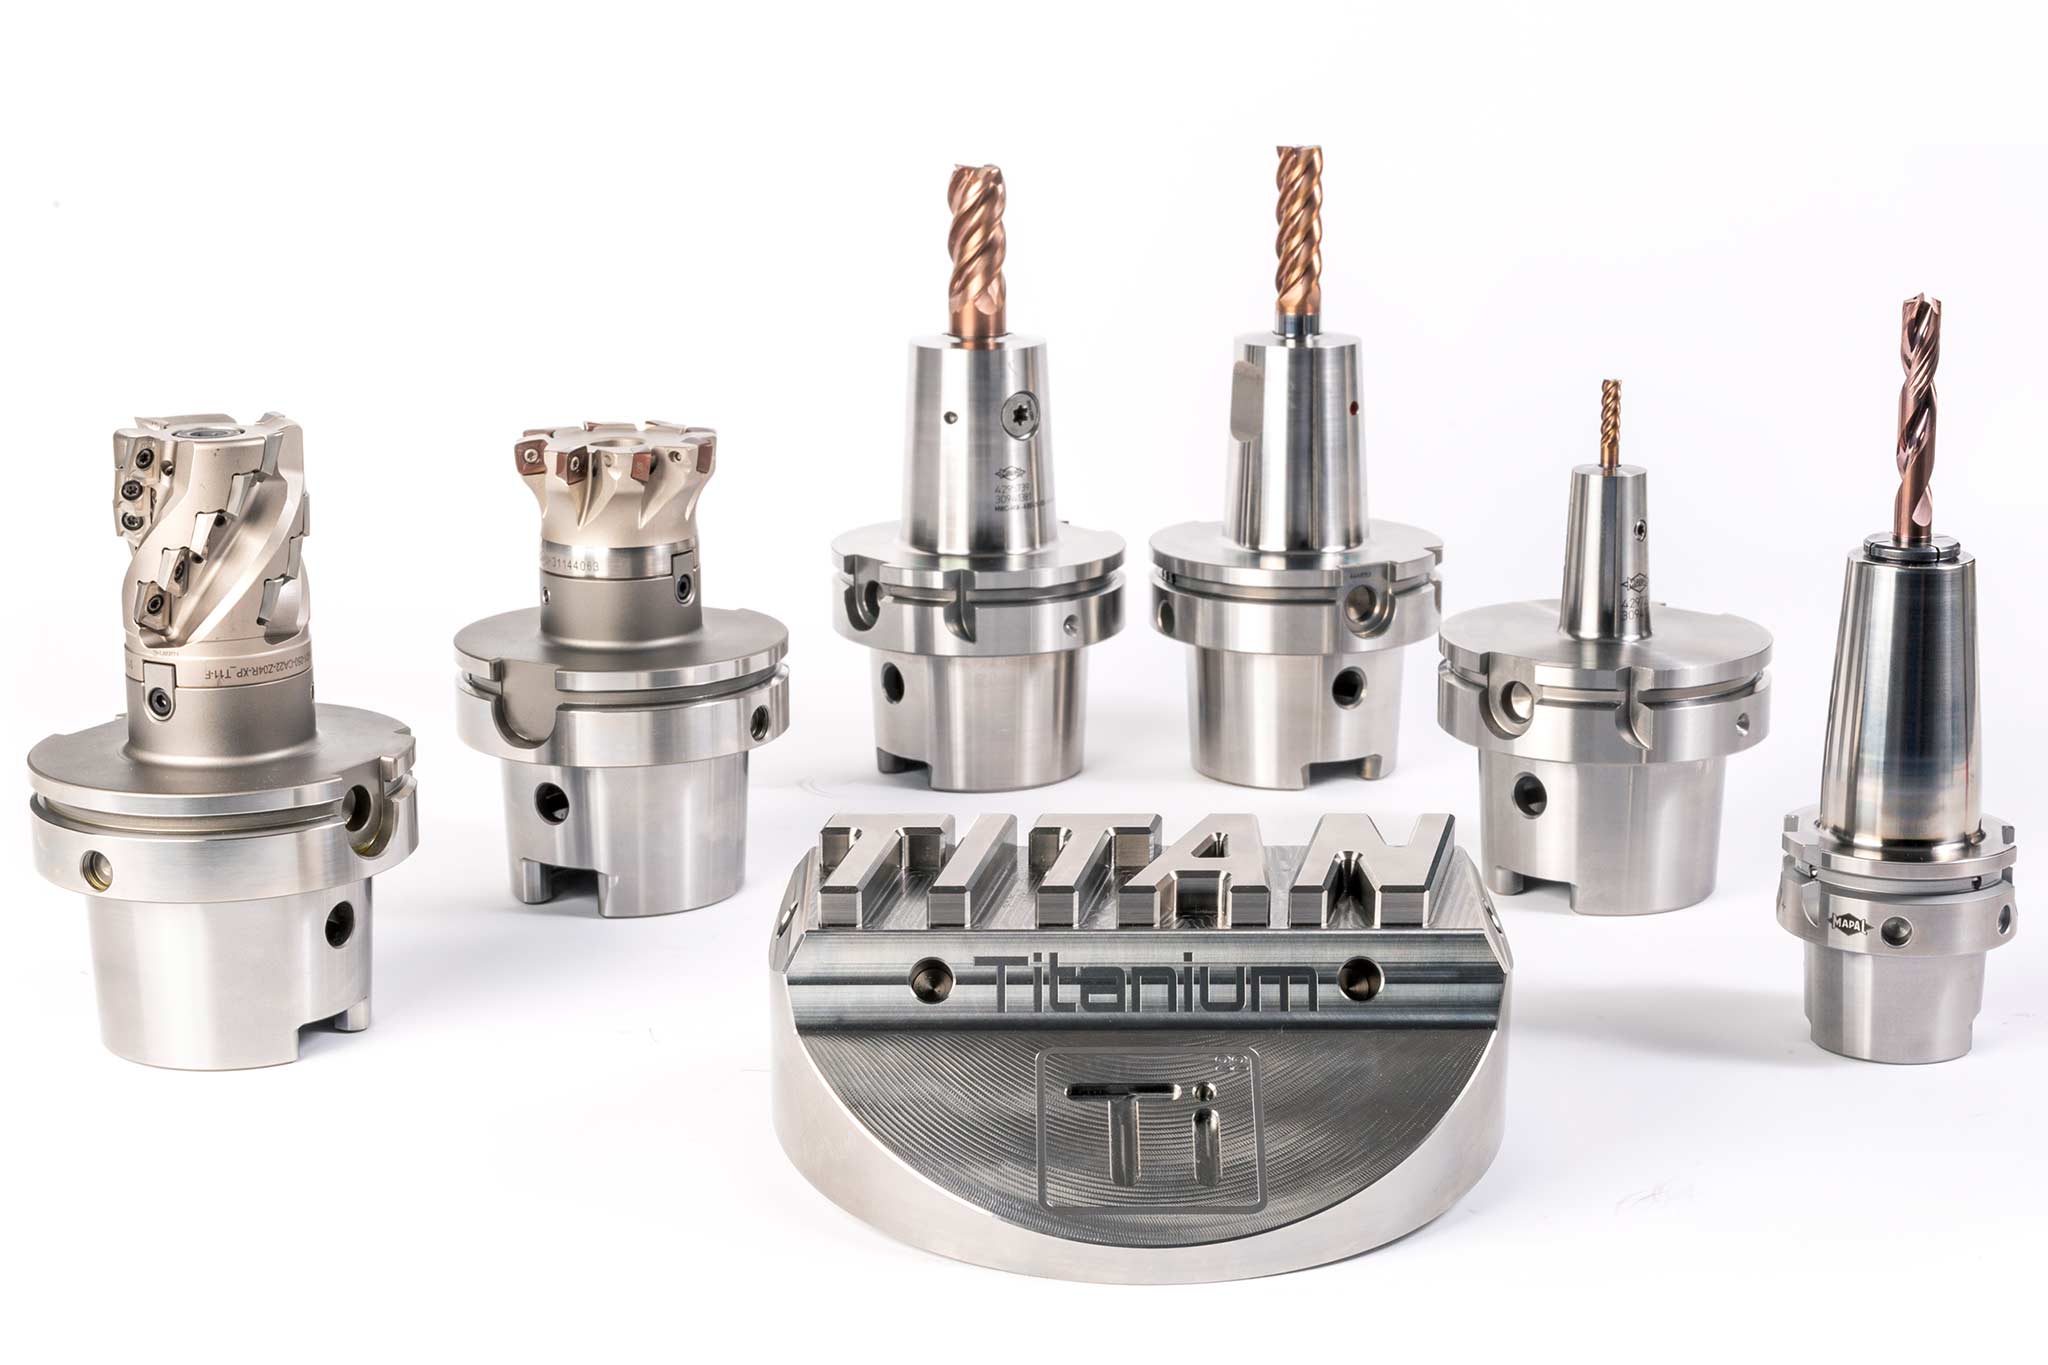
Materiały o wysokiej wytrzymałości, a jednocześnie lekkie mają kluczowe znaczenie w lotnictwie. Zastosowanie nowych kombinacji materiałów pozwala na dalszą redukcję masy, zwiększenie wytrzymałości i odporności na korozję, a także uproszczenie montażu dzięki zintegrowanej konstrukcji. Podczas gdy elementy konstrukcyjne z aluminium, tytanu czy stali o wysokiej wytrzymałości są obrabiane na centrach obróbczych lub obrabiarkach portalowych, obróbka na etapie montażu końcowego jest wykonywana za pomocą urządzeń ręcznych, wiertarek lub robotów.
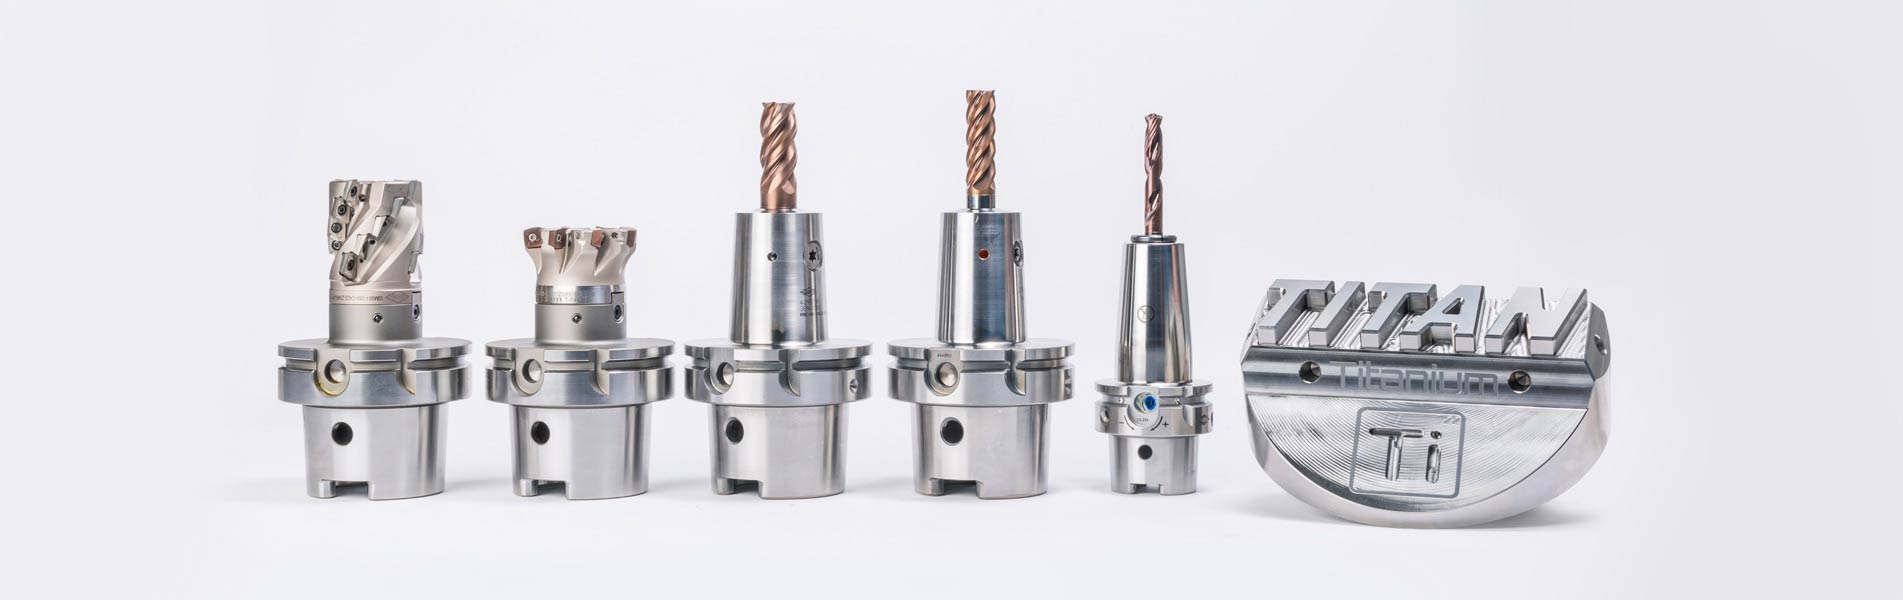
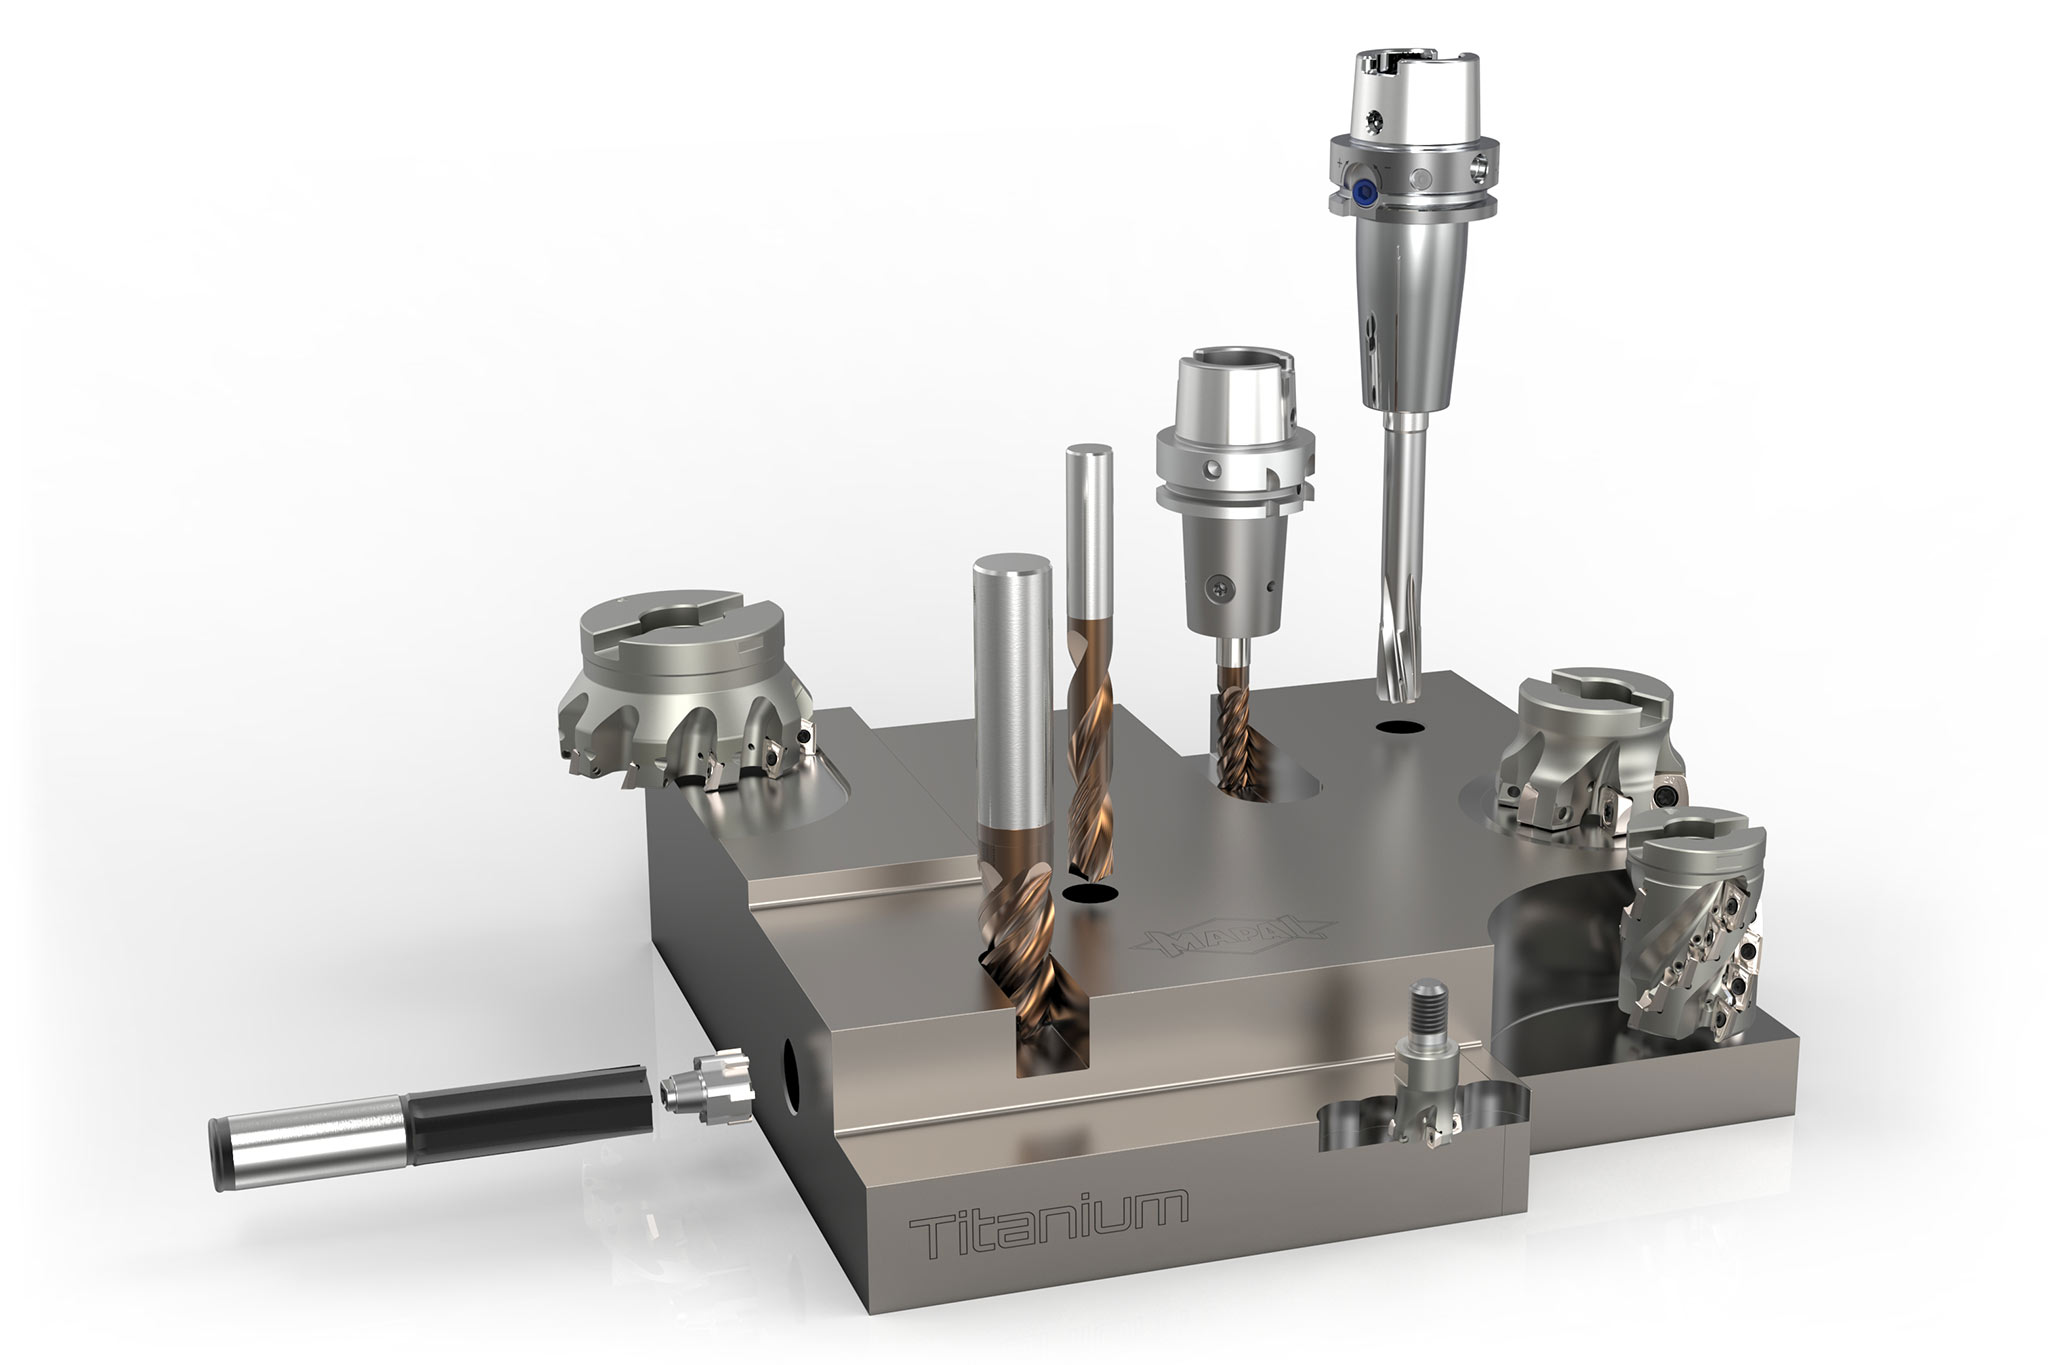
Program narzędzi do obróbki tytanu
Frezy z stałymi ostrzami
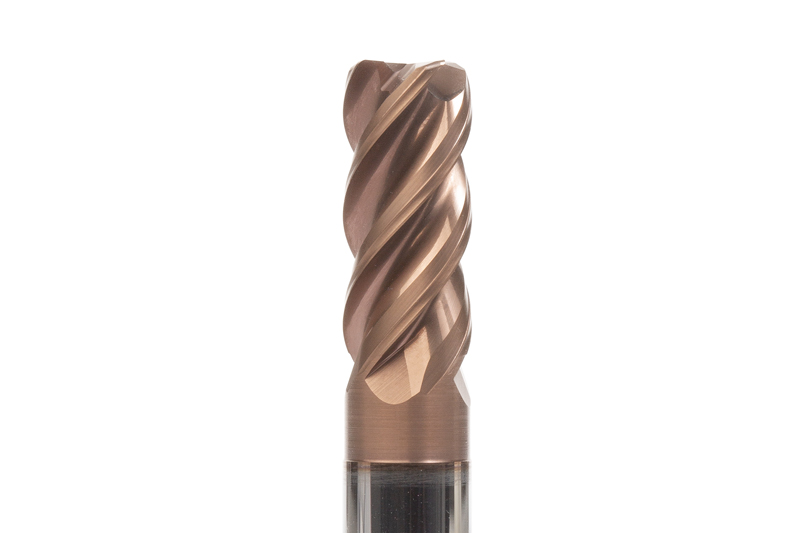
OptiMill-Titan-HPC
Frez walcowo-czołowy
Czteroostrzowy frez walcowo-czołowy do obróbki zgrubnej i wykończeniowej tytanu
Specjalne przygotowanie krawędzi skrawających zapewnia optymalną powierzchnię
Najwyższa stabilność narzędzia dzięki maksymalnej średnicy rdzenia i jego nachyleniu w stosunku do chwytu
Dostępne różne promienie narożników
Zakres ø: 6,00 - 25,00 mm
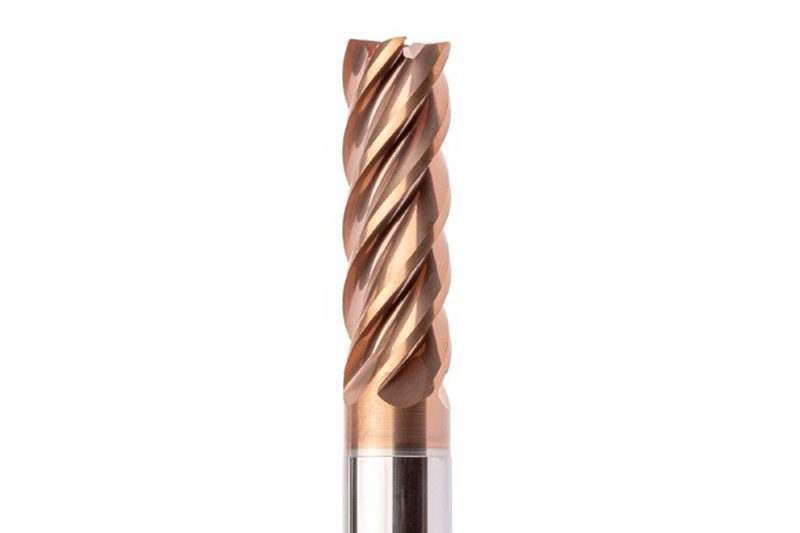
OptiMill-Tro-Titan
Frez trochoidalny
Pięciostronny frez trochoidalny
Maksymalna wydajność skrawania przy jednoczesnej wysokiej jakości powierzchni
Zoptymalizowany nierównomierny podział
Precyzyjnie wyważona część tnąca chroniąca wrzeciono maszyny i zapewniająca dłuższą żywotność
Głębokość skrawania do 3xD
Zakres ø: 6,00 - 25,00 mm
Frezy z wymiennymi ostrzami
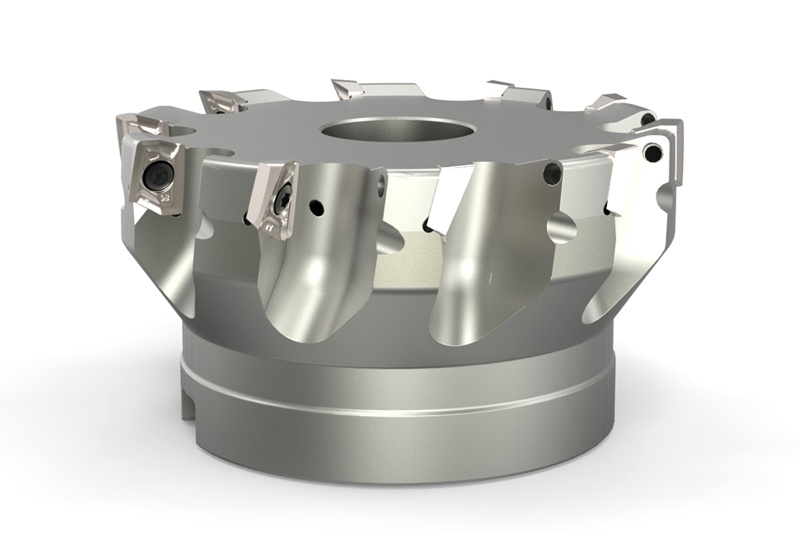
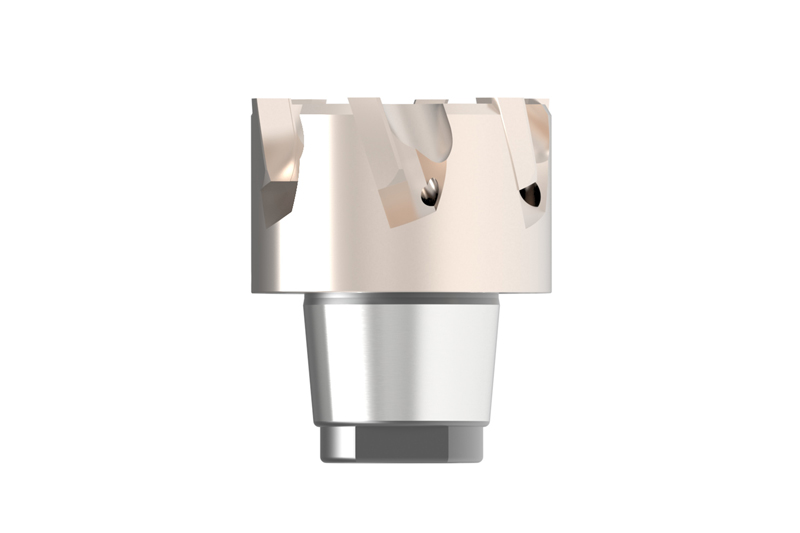
NeoMill-Titan-2-Corner
Frez walcowo-czołowy
Frez walcowo-czołowy z dwuostrzowymi płytkami skrawającymi promieniowymi
Pozytywna geometria podstawowa dla elementów podatnych na drgania
Głębokość skrawania do 10 mm
Zakres ø: 40,00–100,00 mm
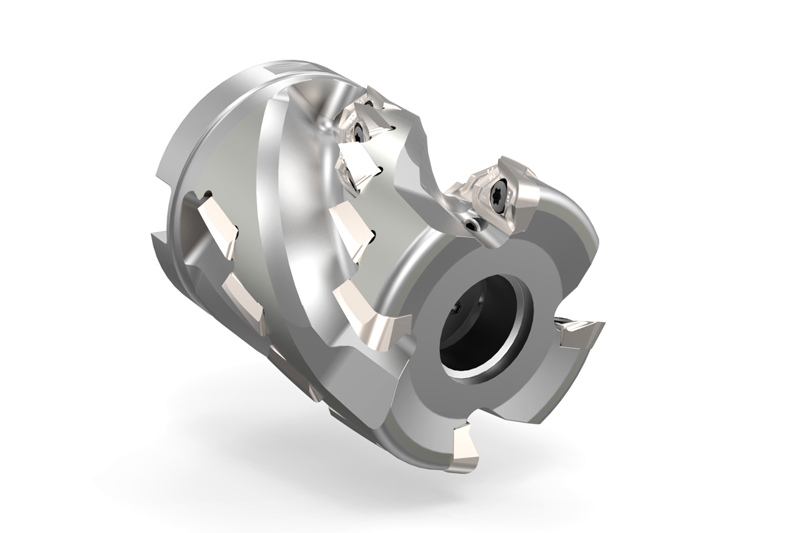
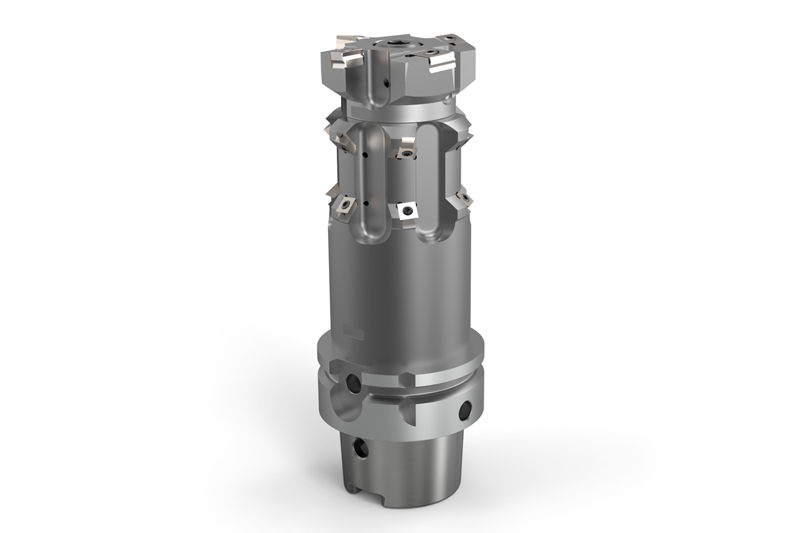
NeoMill-Titan-2-Shell
Frez walcowo-czołowy
Frez walcowo-czołowy z dwustronnymi, promieniowymi płytkami skrawającymi
Idealny do głębokiego frezowania narożnego i do przycinania z dużą głębokością skrawania do 57 mm
Zakres ø: 32,00–80,00 mm
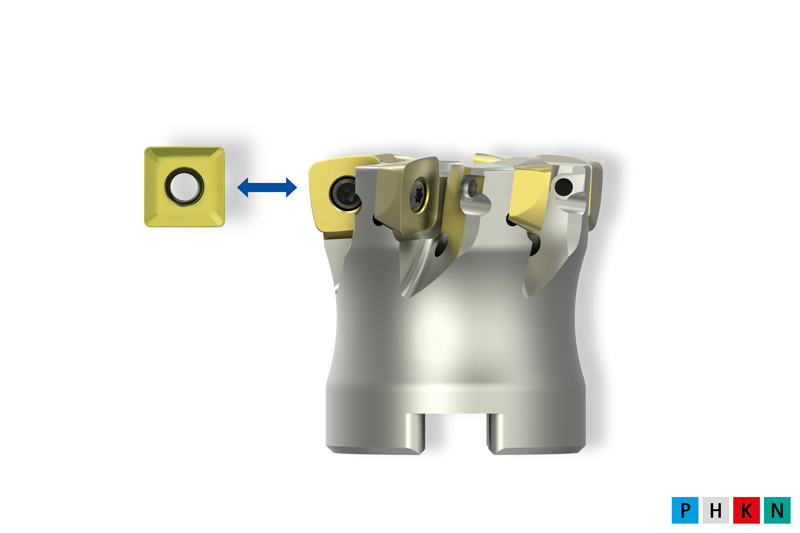
NeoMill-2/4-HiFeed90
Frez walcowo-czołowy o wysokim posuwie/90°
Uniwersalny system narzędziowy zapewniający najwyższą wydajność
Zakres ø: 16,00 - 200,00 mm
Wiercenie w pełnym materiałe
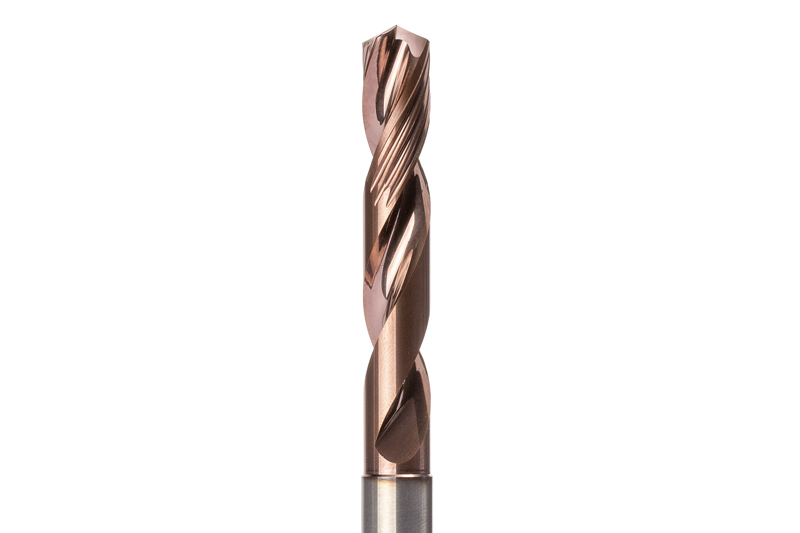
MEGA-Speed-Drill-Titan
整体硬质合金钻头
双刃高速钻头
四个导向倒角可保证实现高精密表面精度和高圆柱度(可实现公差等级IT9, IT8)
带倒角的凸形切削刃,稳定性高
新颖的螺旋轮廓以保护导向倒角
最大的耐热性和耐磨性
ø-范围:3.00 - 20.00 mm
铰削和精镗
FixReam-FXR
带有圆柱柄的高性能铰刀
整体硬质合金高性能铰刀
直槽,用于通孔和盲孔
斜向左侧开槽,用于通孔
实现短加工循环的理想选择
提供多种切削材质和涂层
ø-范围:2.80 – 20.20 mm
快换式铰刀 HPR
带有HFS结构的快换式铰刀
固定设计的高精度可更换刀头系统带钎焊切削刃
精确的径向跳动和转换精度 < 3 μm
模块化系统设计实现最高的经济效率
适用于微量润滑 (MQL)
ø-范围:7.00 - 65.00 mm
镗孔
Mandrilamento em titânio
Ferramentas para mandrilamento com tecnologia tangencial
Ferramentas especiais específicas ao componente para a máxima produtividade, processos rentáveis e conceitos de usinagem estáveis
Pastilhas intercambiáveis tangenciais CTHQ e FTHQ
Os melhores resultados de usinagem na proporção de comprimento/diâmetro > 3,5 D devido à geometria em arco
Titanium and titanium alloys are predestined for use in aerospace. High demands are placed on workpiece material strength and corrosion resistance in relation to their specific weight. This results in a wide range of applications extending from small mechanically processed structural parts to load-bearing parts in the fuselage or blades in the engine.
加工示例:扭力杆
1 / 5
精镗刀具
极精准的切削刃调节
完美的镗孔同心度
极佳的表面粗糙度
完美的镗孔几何形状
通过导向条实现极其稳定的加工
高度的重复定位精度和简单的对刀方式
2 / 5
NeoMill-Titan-2-Shell
最大的切削去除率
最佳排屑效果
运转非常平稳
可变量的冷却方案
可以使用具有各不相同圆角半径的切削刃
可提供多种不同的切削刃材料
3 / 5
MEGA-Speed-Drill-Titan
140°钻尖角
通过异常光洁的涂层,避免了粘附现象
4个导向倒角(最佳圆度值)
凸起的切削刃
内部冷却液供给
最新的排屑槽设计(获得最佳排屑效果)
高效的冷却液流动(避免了切削刃上产生摩擦并极大降低了加工中产生的热量)
4 / 5
OptiMill-Titan-HPC
特殊的切削刃处理(切削刃稳固)
不同螺距的螺旋构件(确保切削过程稳定、加工运行平稳)
核心提升(更稳定)
5 / 5
FixReam
结构来自整体硬质合金或者经过钎焊
孔径质量:H7
DLC-涂层(=DIAMOND-LIKE CARBON,类金刚石涂层),以获得最佳的性能
可配置直径(Speedline)
提供针对通孔或者盲孔的结构
适用于微量润滑(MQL)
加工示例:铰链轴线
1 / 6
Deburring tools made from solid carbide
With these custom tools in a special spherical shape, the bore entrance and exit of the main bore as well as the fixing bore are deburred through circilar milling.
2 / 6
NeoMill-Titan-2-Corner
High machining rates
Very quiet running
Cutting edges with various corner radii can be deployed
Variety of cutting materials available
3 / 6
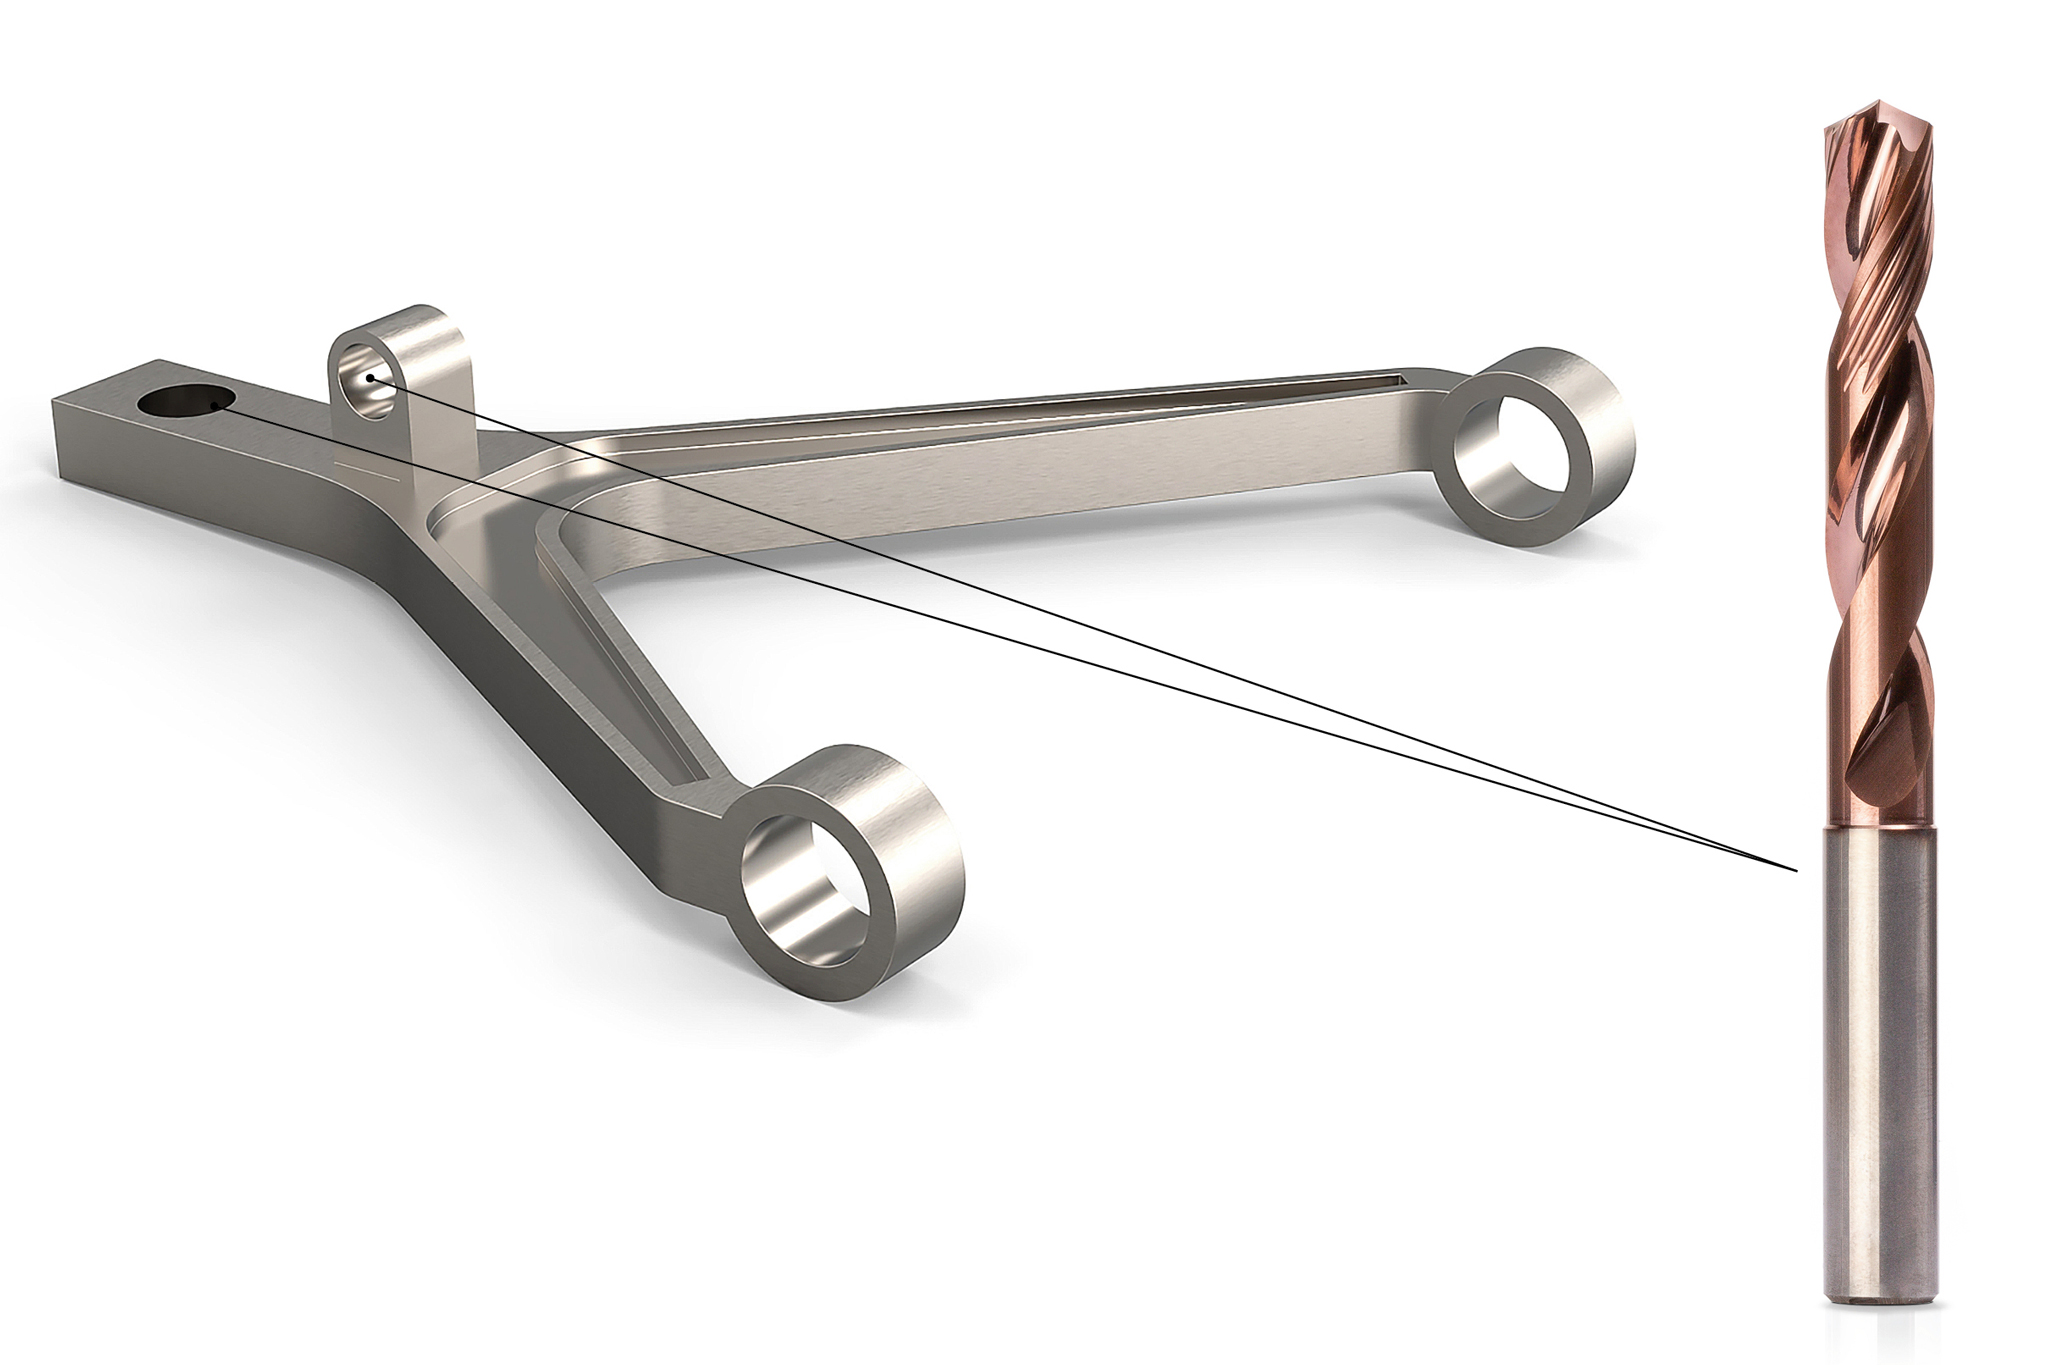
MEGA-Speed-Drill-Titan
Extends tool life by 30% compared to previous solutions
Drilling specialist for high cutting speeds and feed rates
Short cycle times
4 / 6
TTD replaceable head drill, custom drill, boring bar
TTD replaceable head drill for piloting the first lug
Custom drill with additional guide element at the neck for medium machining of lugs from both sides
Bearing-guided boring bar for precise finishing of the main bore from one side
5 / 6
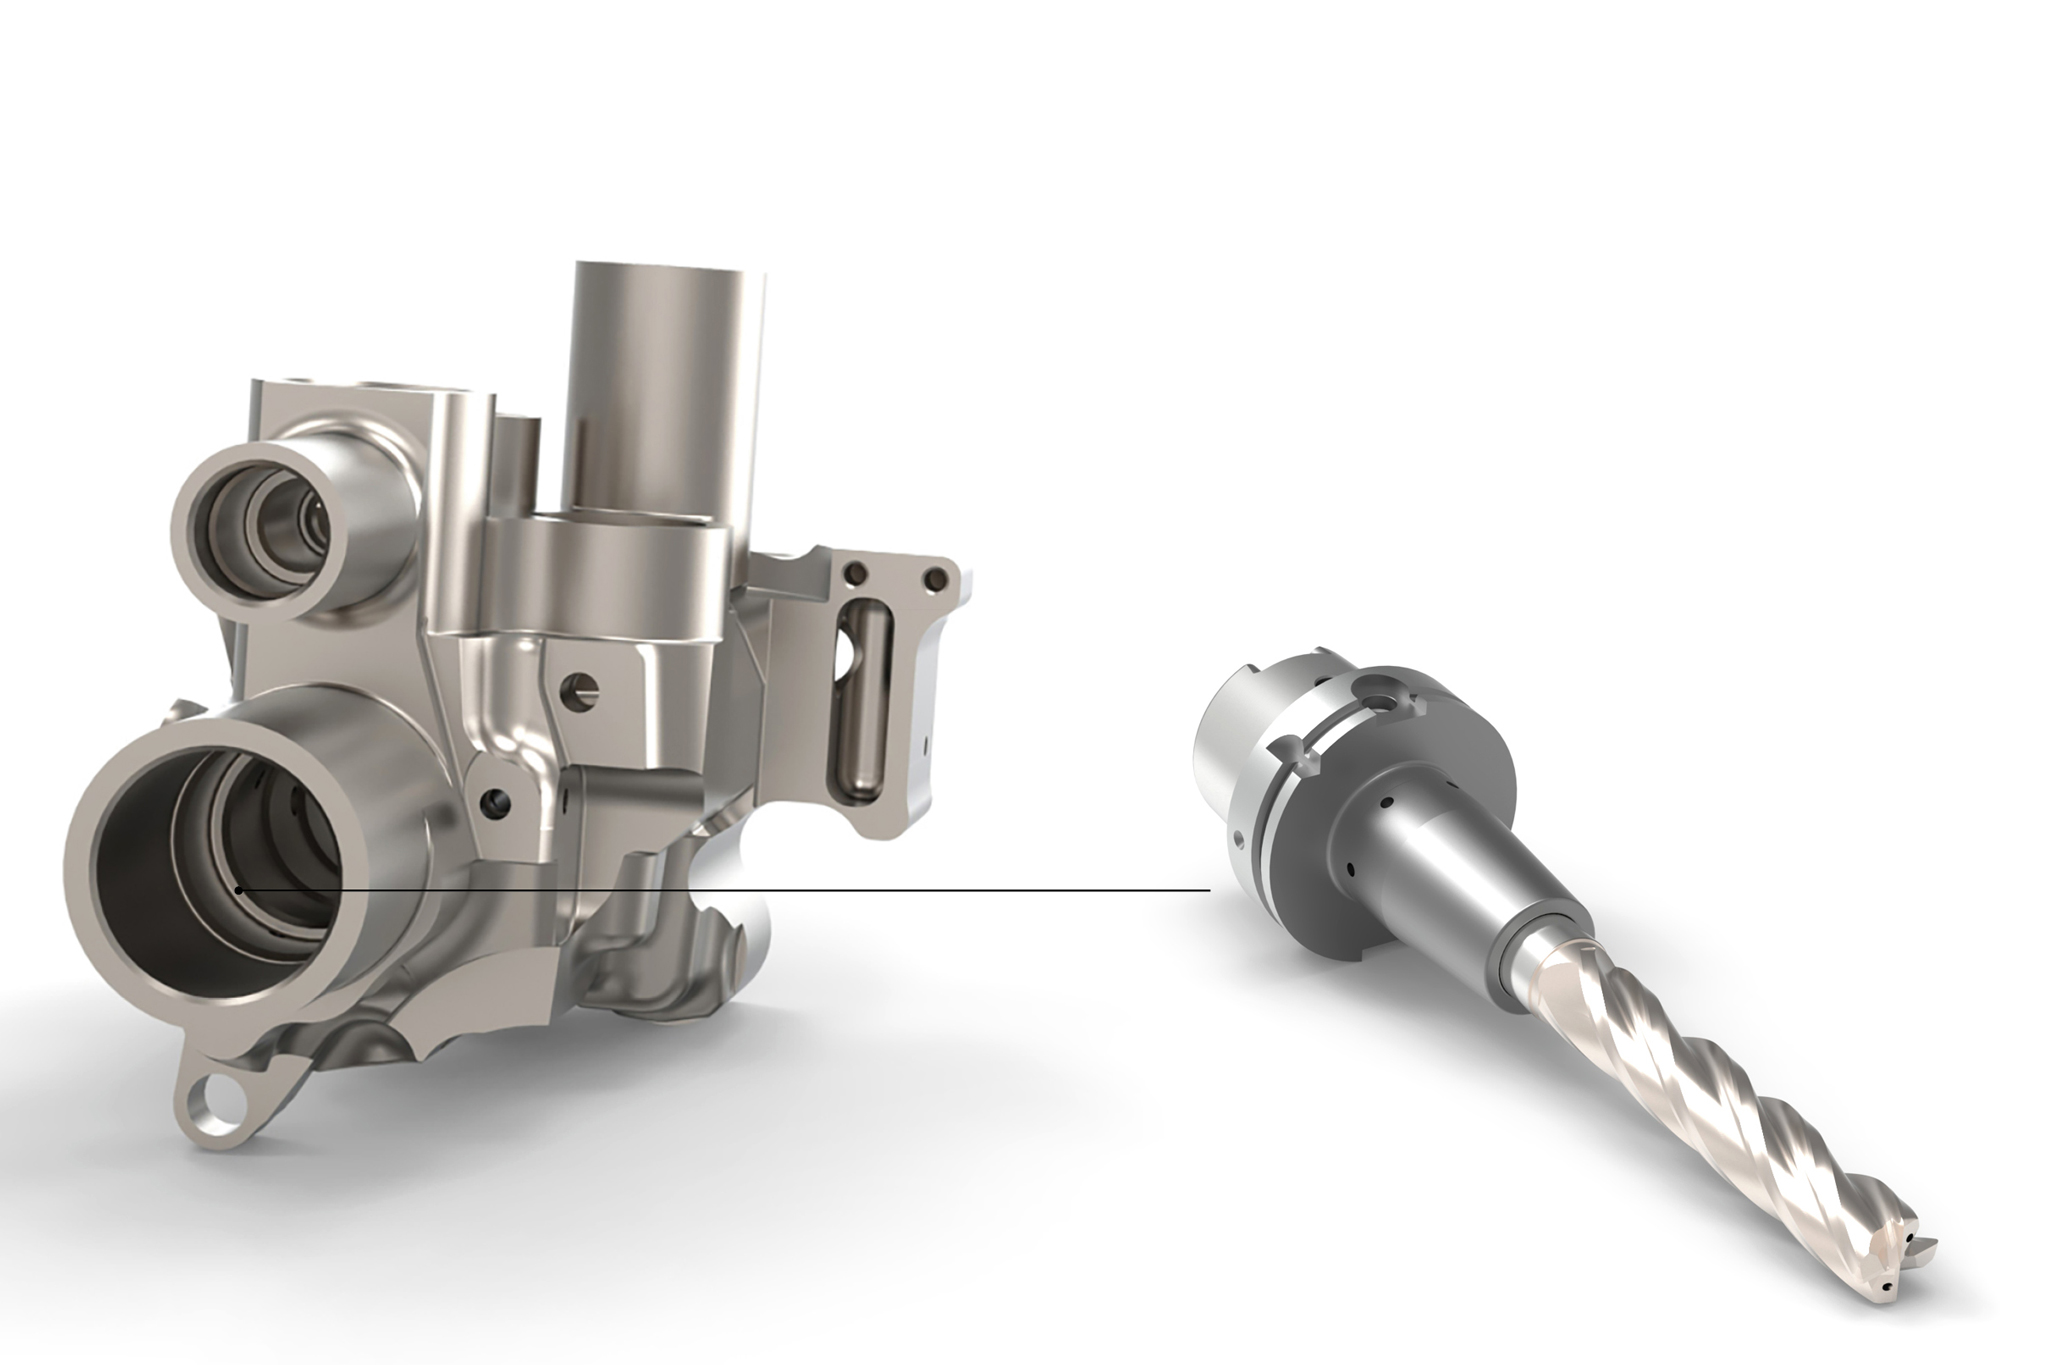
OptiMill-Titan-HPC
Increases tool life by 35%
Perfect solution for roughing, medium machining and finishing
Excellent price-performance ratio
Fits Mill Chuck, System HB
Optimal pitch (stable cut, smooth running)
Core rise for more stability
6 / 6
Extends tool life by 10% compared to previous solutions
High removal rates possible
Unequal spacing of the cutting edges
Special coating to avoid deposits
Specially designed chip flute for optimum chip removal
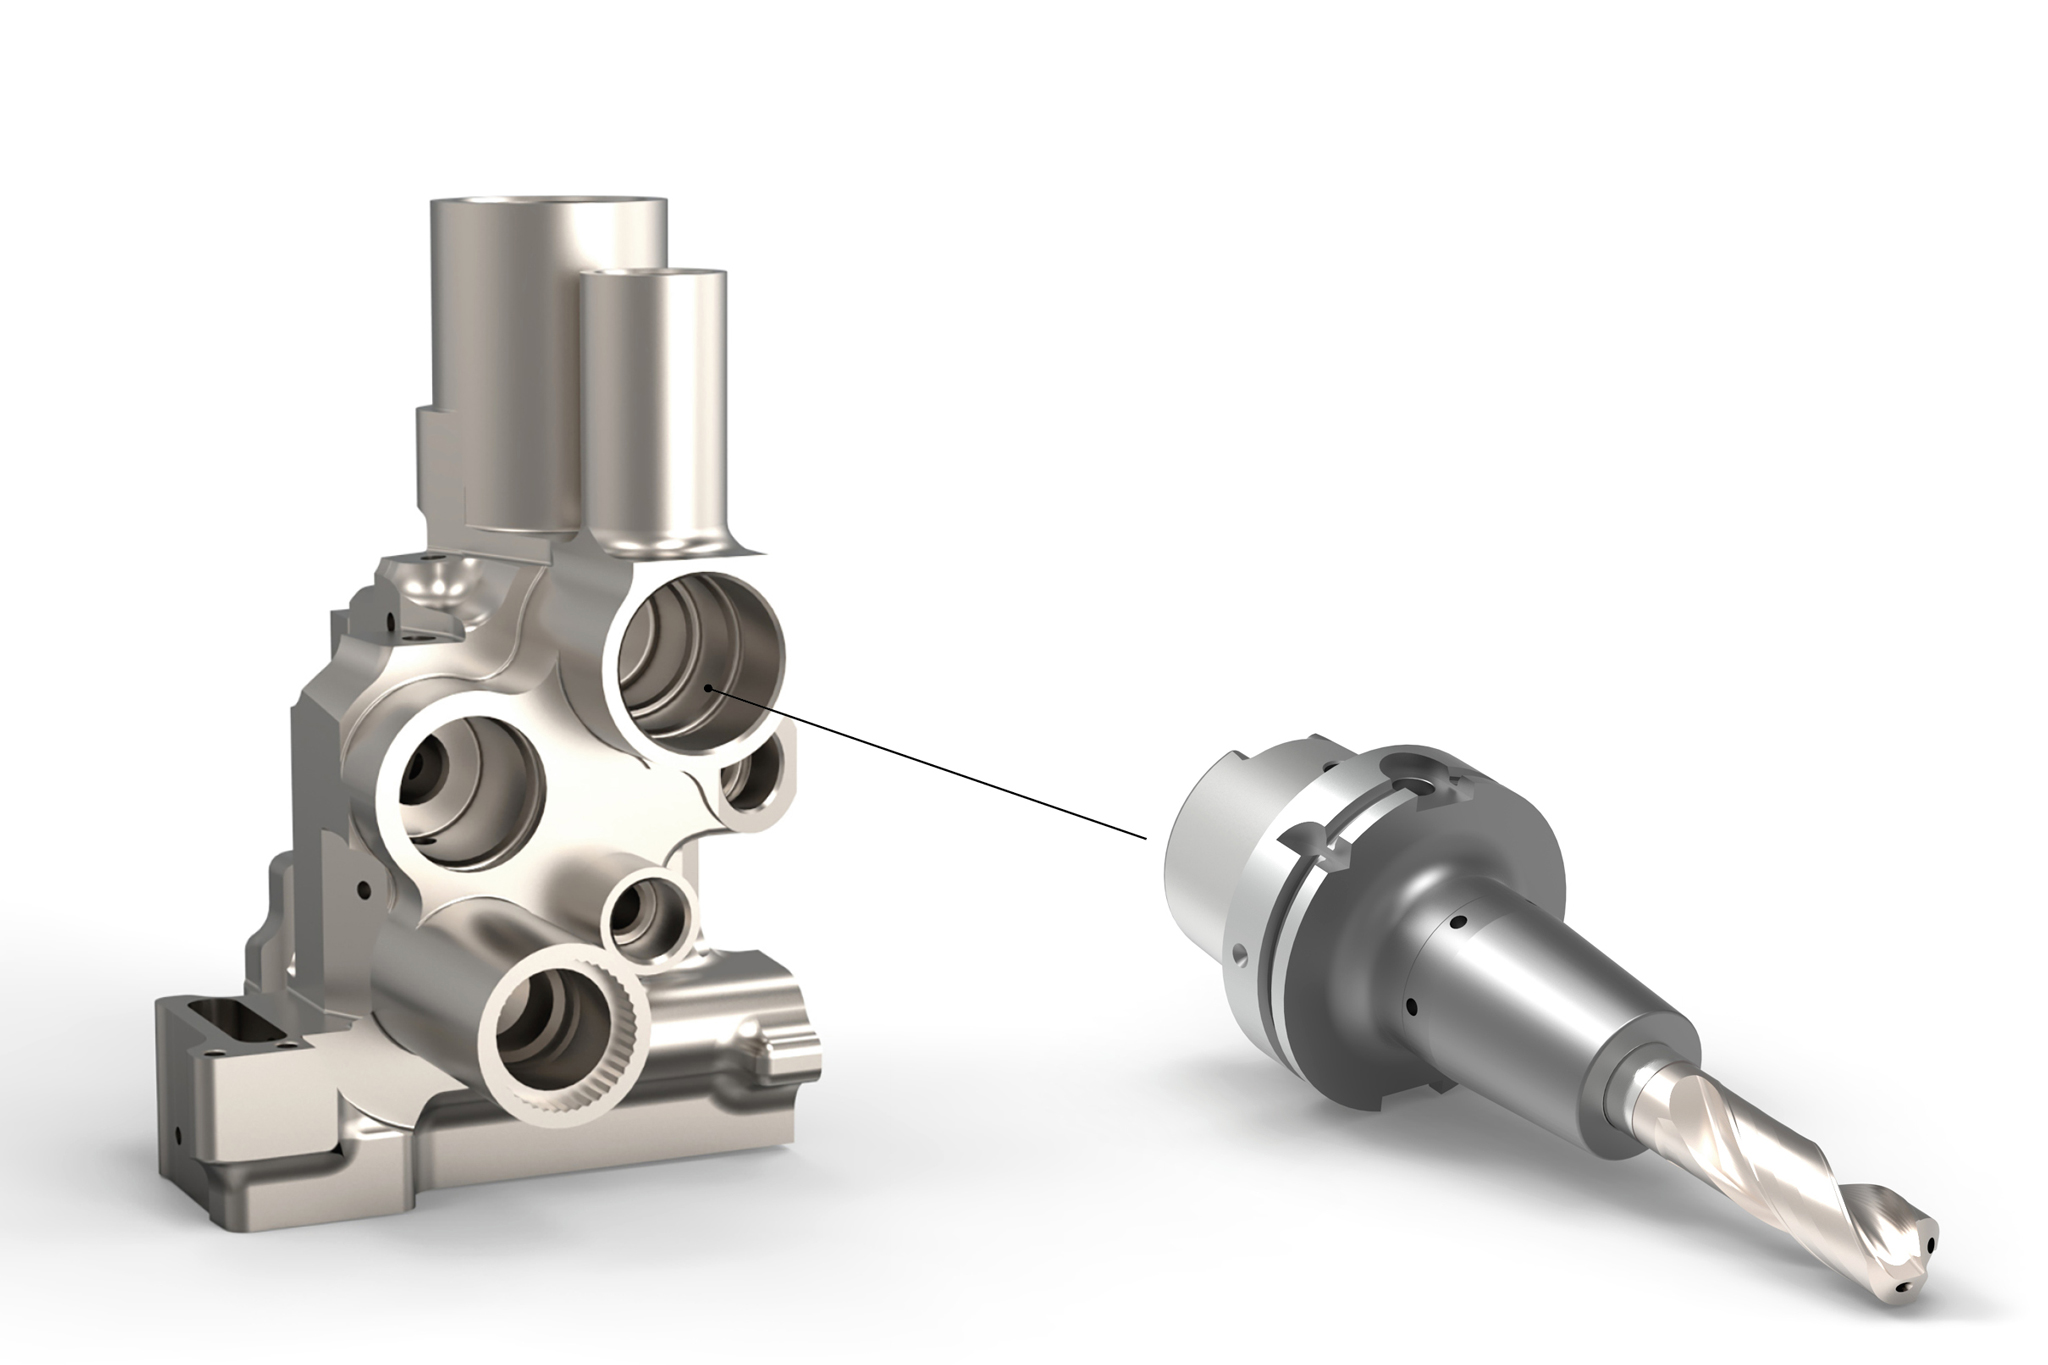
Machining example valve housing
1 / 7
Solid carbide drill
For difficult drilling applications
Innovative lead geometry for good chip removal and low cutting pressure
Significantly more performance, up to twice the feed rate compared to previous solutions
2 / 7
Boring tool with interchangeable blades
Three-stage boring tool for medium machining
No setting of cutting edges necessary
Economical tool concept for roughing bores
High machining rates possible
Indexable inserts with excellent thermal stability
3 / 7
Boring tool made of solid carbide with four edges
Long tool life thanks to special coating
Coating protects the cutting edges against high temperatures and excessive wear and tear
The internal coolant supply and chip channel geometries ensure efficient chip removal
4 / 7
HPR replaceable head reamer with six edges
Perfect concentricity of the bores
High feed rate possible and therefore less machining time
Adjustable adapter enables precise tool settings and eliminates spindle errors
Complete finishing in a single step
5 / 7
Solid carbide drill with three edges
Special triple-edge geometry
Perfect positioning of the drill
Highly suitable for inclined bore entrances or cross bores
6 / 7
Boring tool made of solid carbide with four edges
Special geometry
Stable machining
Optimal guide into the bore
Four cutting edges ensure the right geometry of the bore prior to finishing
7 / 7
HPR reamer with six edges
Can be repaired by desoldering/soldering the blades
Perfect roundness of the bore due to the matching multi-cutting edge geometry
Dans le secteur médical, le titane est le matériau presque parfait, car il peut être largement utilisé en raison de sa biocompatibilité, c'est-à-dire de sa résistance dans un environnement biologique (antiallergique), de sa faible conductivité thermique et de son comportement antimagnétique intrinsèque.
Exemple d'usinage d'une prothèse de hanche
1 / 1
OptiMill-Tro-Titan
Revêtement haute performance résistant à la chaleur
Conception spéciale de la goujure pour une évacuation optimale des copeaux
Réduction de la chaleur dans la zone de coupe
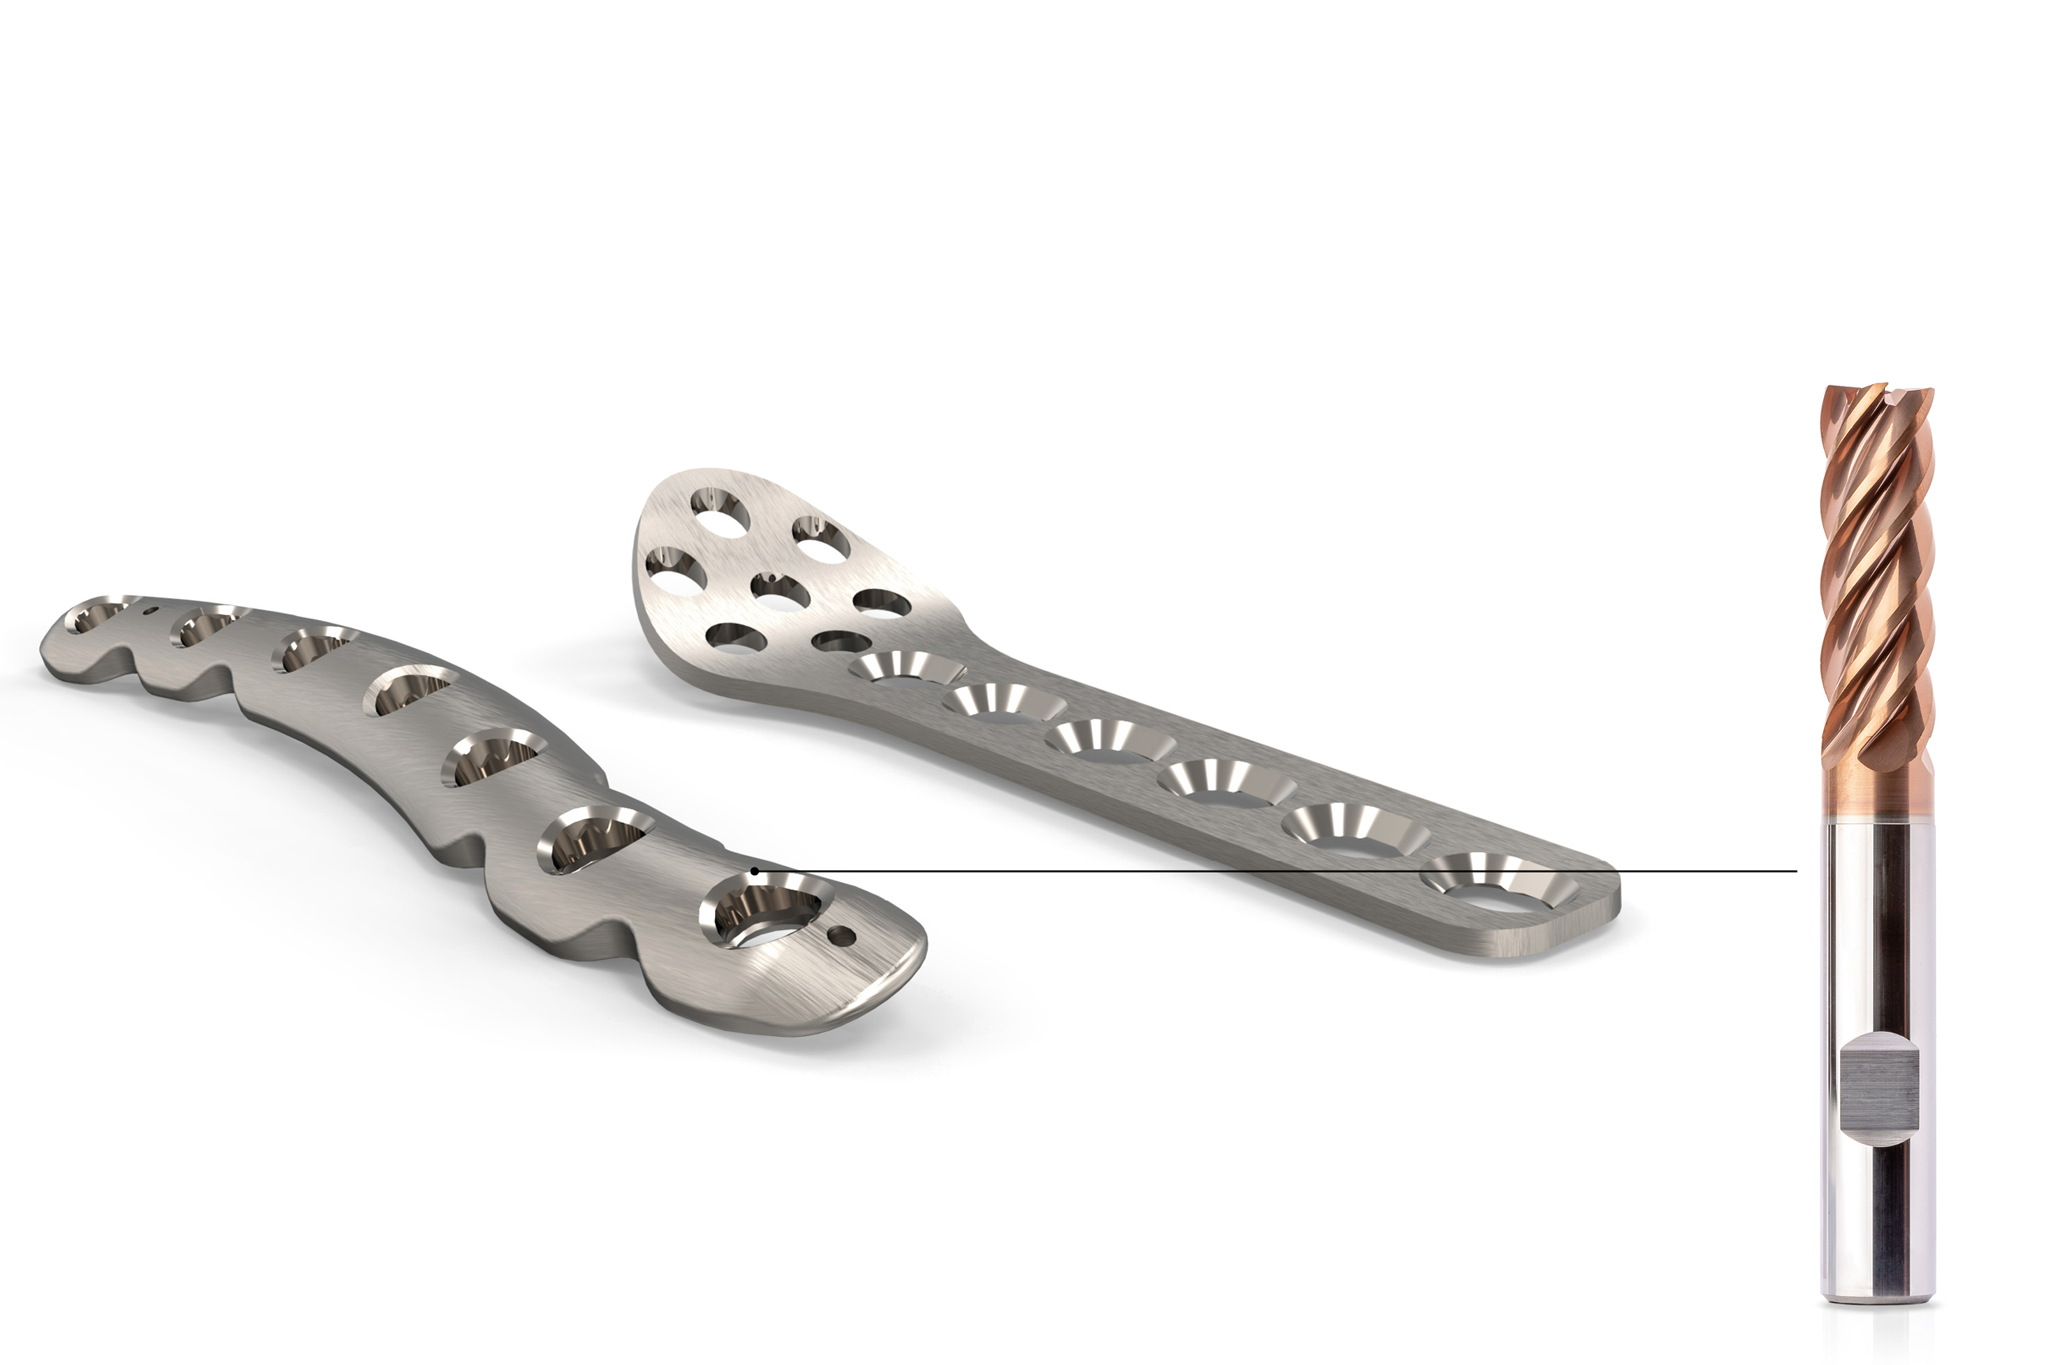
Exemple d'usinage d'une plaque d'ostéosynthèse
1 / 2
OptiMill-Tro-Titan
Hitzebeständige Hochleistungsbeschichtung
Speziell gestaltete Spannut für optimale Spanabfuhr
Wärmereduzierung in der Schnittzone
2 / 2
MEGA-Speed-Drill-Titan
Standzeiterhöhung um 30 % im Vergleich zur bisherigen Lösung
Bohrspezialist für hohe Schnittgeschwindigkeiten und Vorschübe