11.05.2023

-Strategy- バッテリーフレーム

部品の完全な機械加工は、加工工程を検討し調整を行う必要があります。これが、コスト効率・信頼性の高い製造を実現し、完璧な結果を得る方法です。このような高度な加工工程をお客様に提供するために、マパールは電気自動車に重点を置くコンポーネントを定義し、最適な加工工程を提供出来るように策定しました。バッテリー フレームはこれらのコンポーネントの 1 つです。
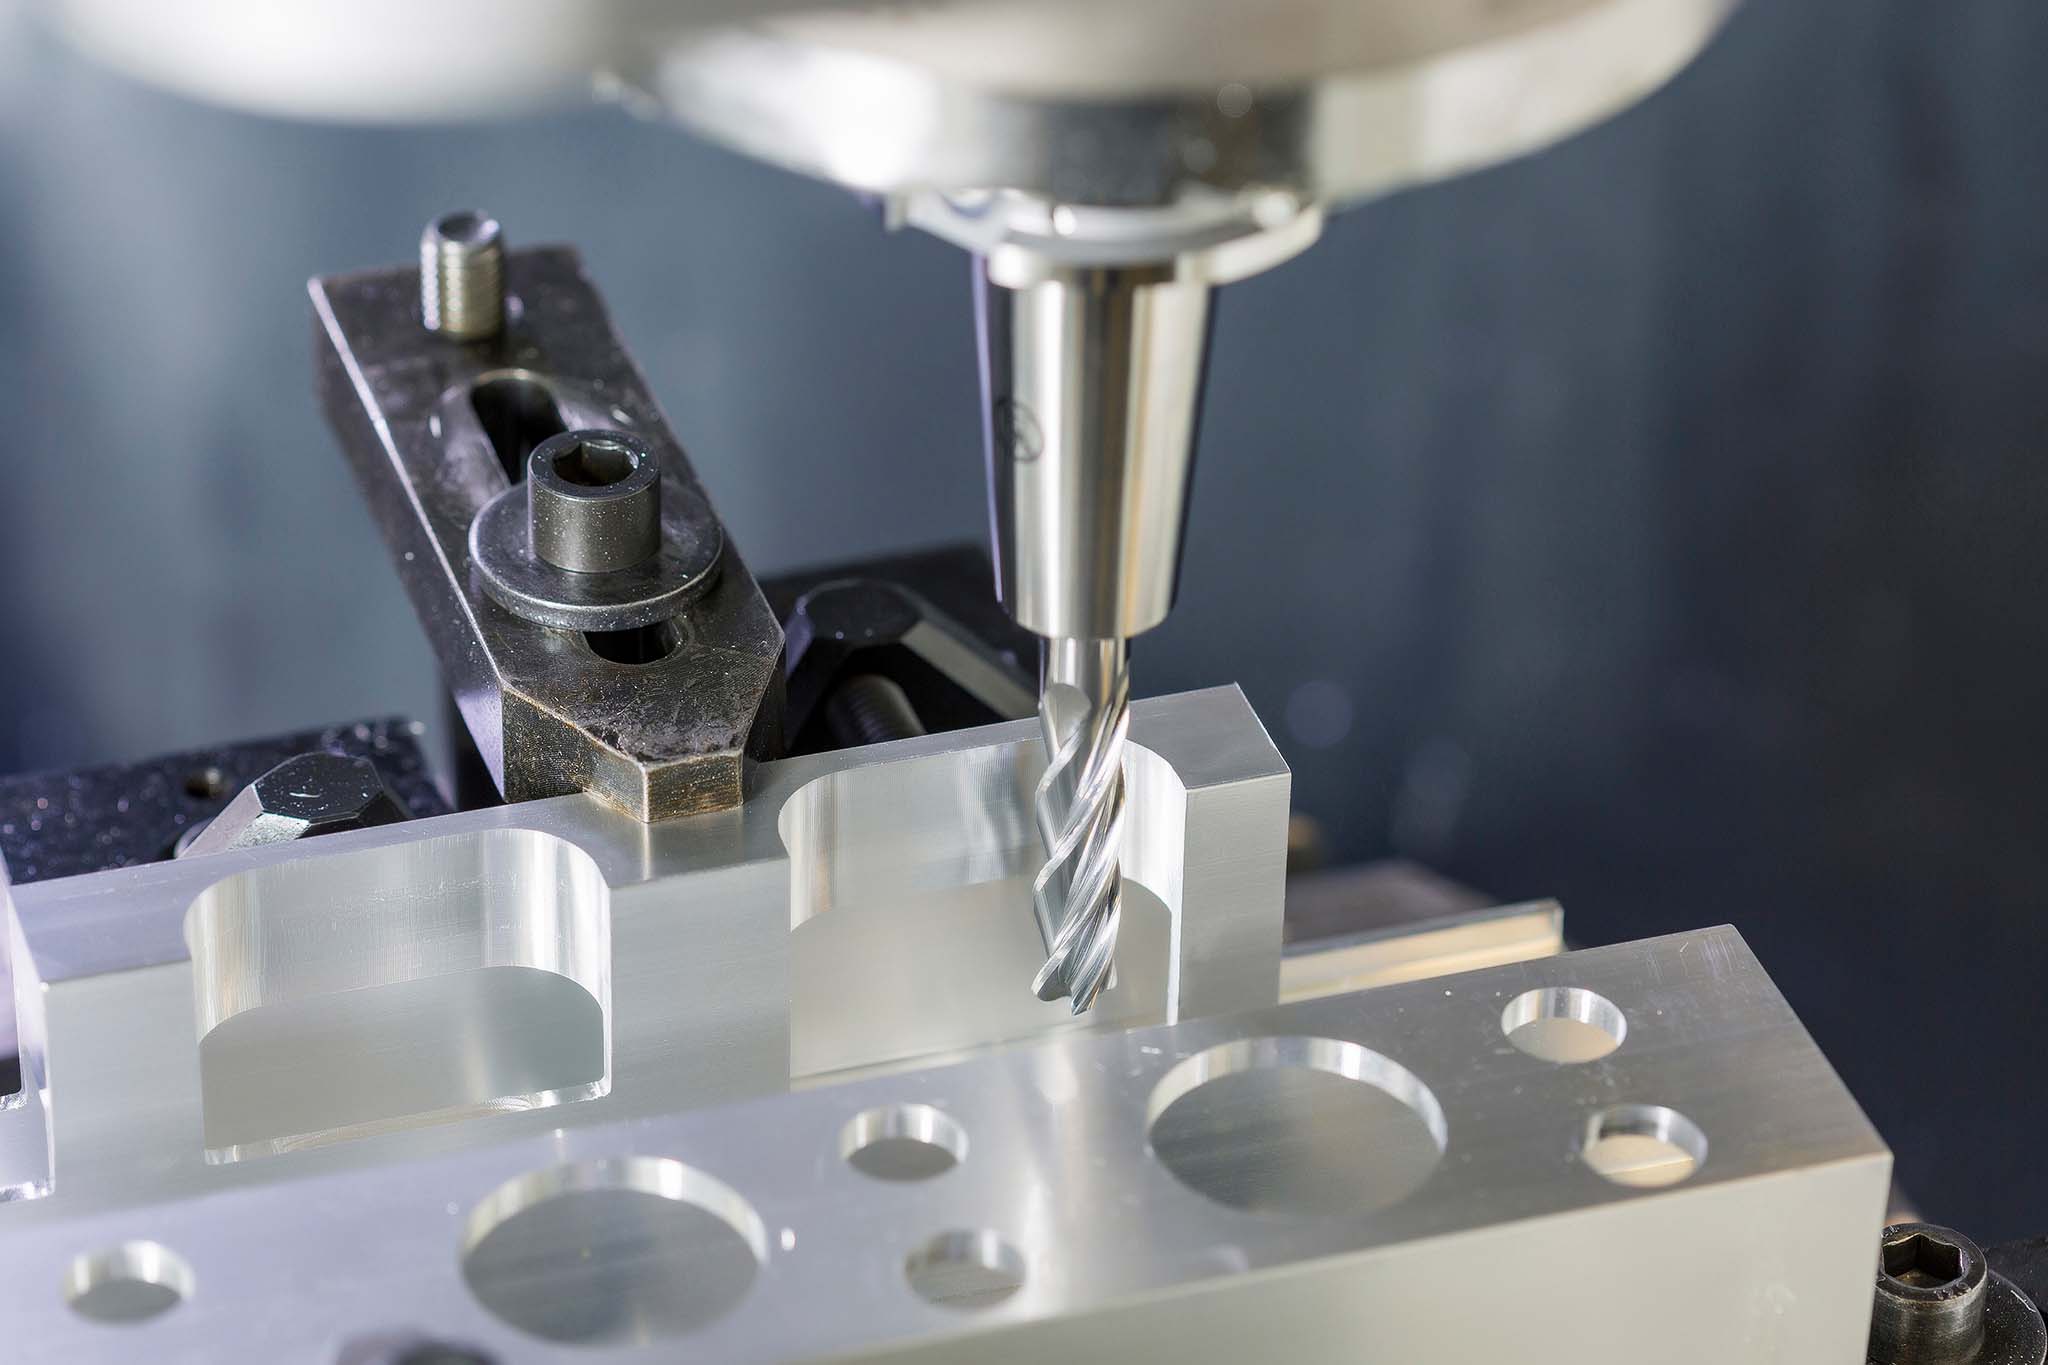
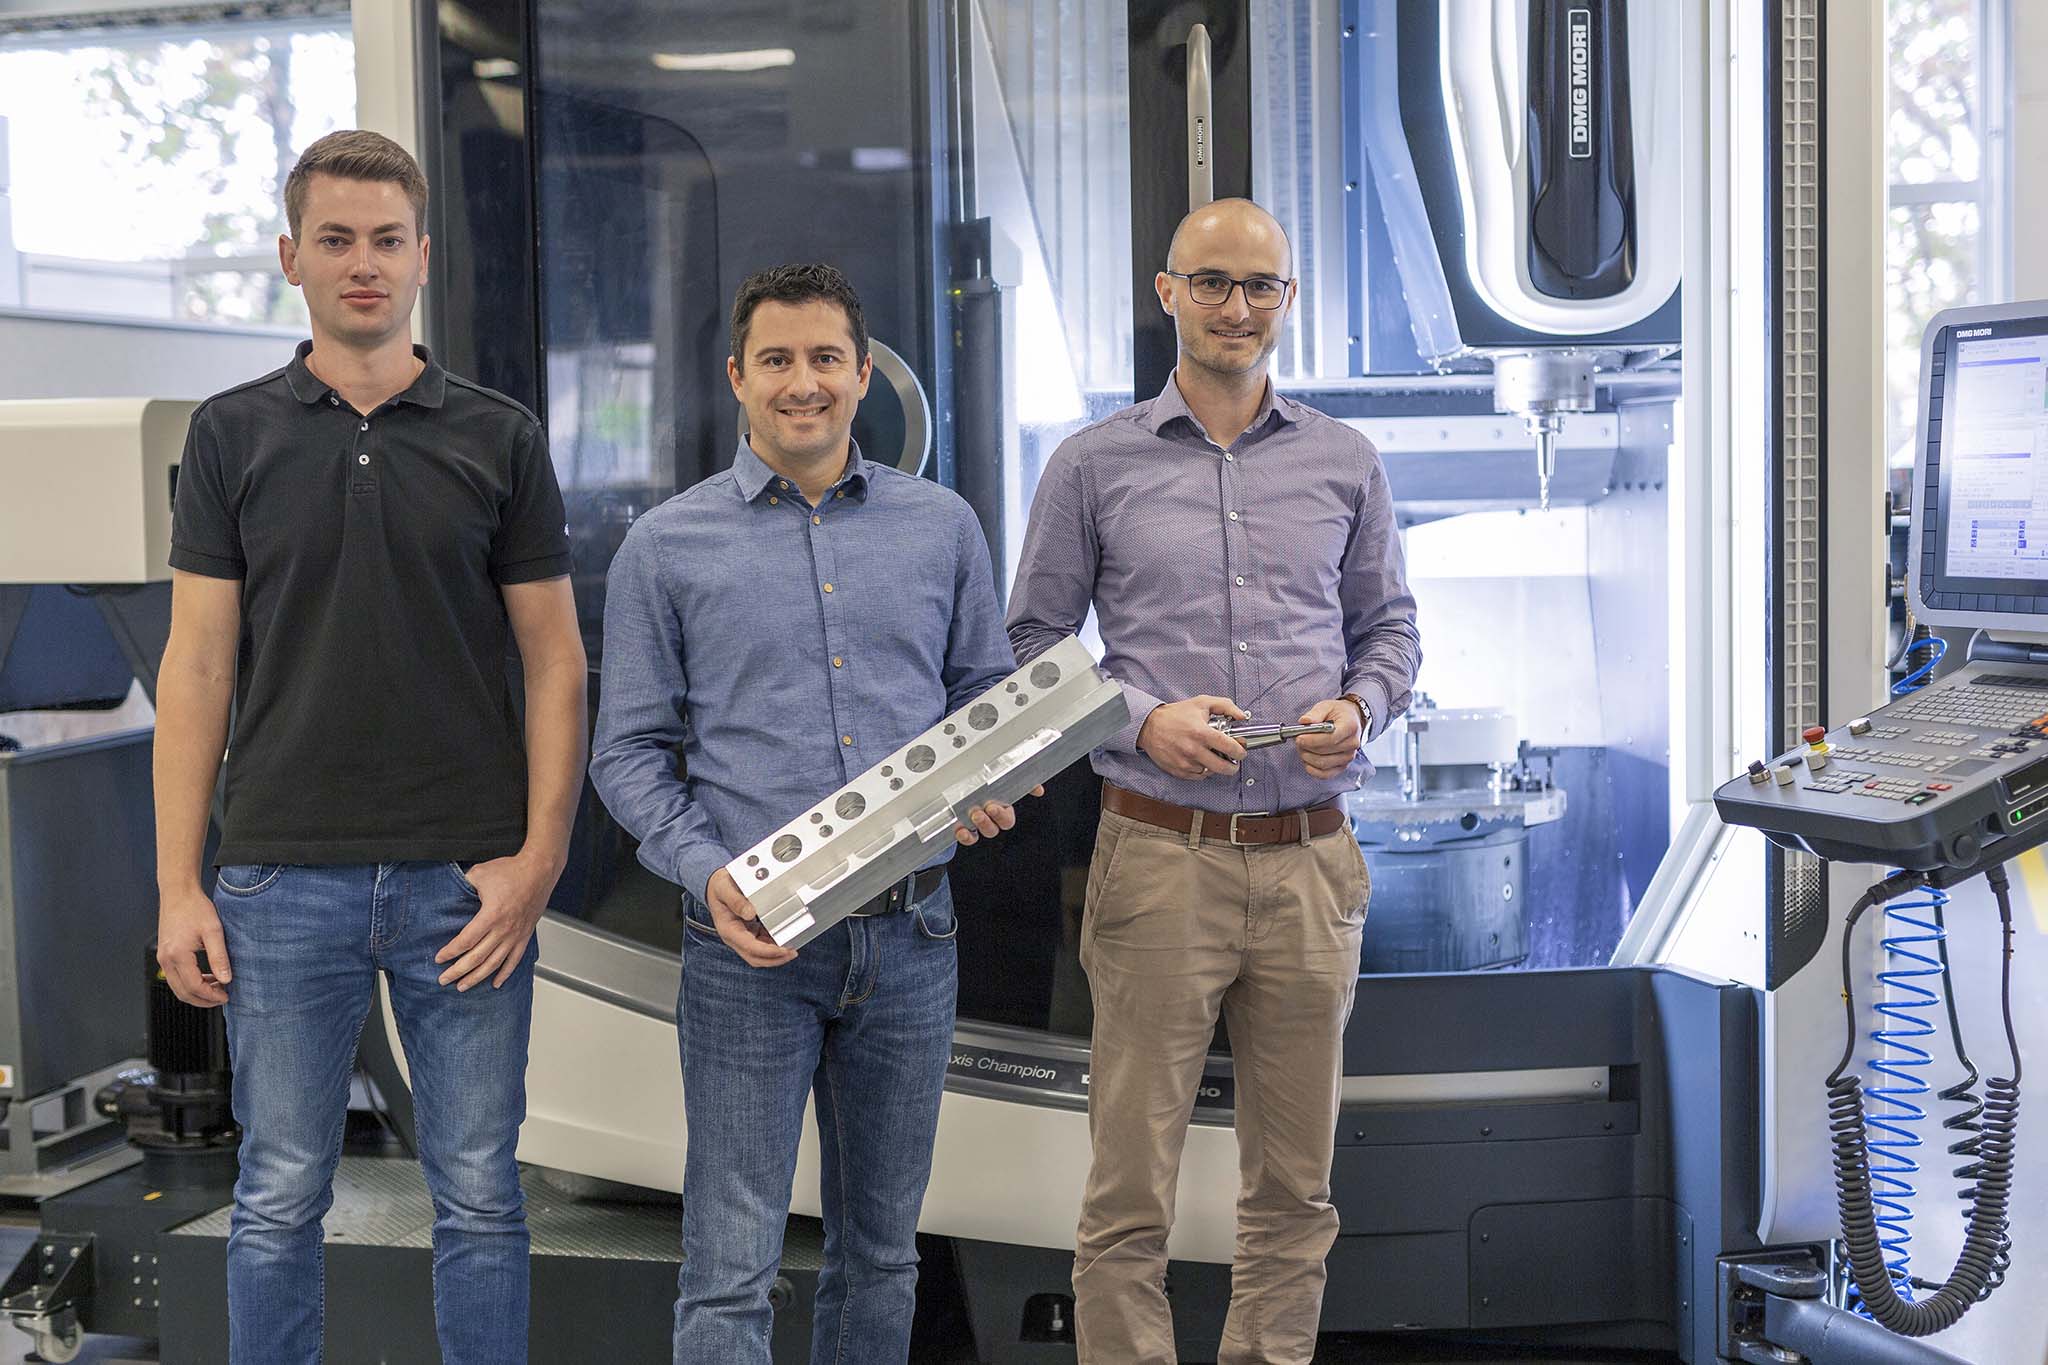
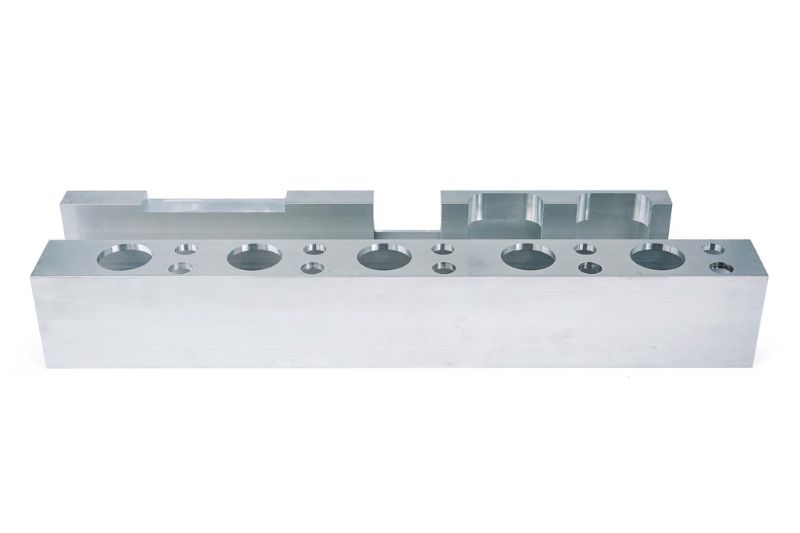
The generic component presents the challenges involved in machining a battery frame.   ©MAPAL
“We master these challenges above all with the optimally designed milling cutters”, says Kucher. Milling is even used for most bores on the frame part. Depending on diameter and machining depth, the experts decide in each case whether to drill or mill. “While the cycle time during the milling of bores is somewhat longer, milling offers decisive advantages in this case, which more than make up for the lost time.” In the past, long chips which occurred while drilling aluminium parts often proved very problematic to customers. “Removing long chips from inside the frame part presented a risk for the process”, says Kucher. The short milling chips are easy to remove. There is also a lot less burr formation during milling than drilling. And there is no need for tools changes. Multiple bores with different diameters can easily be machined with a single milling cutter.

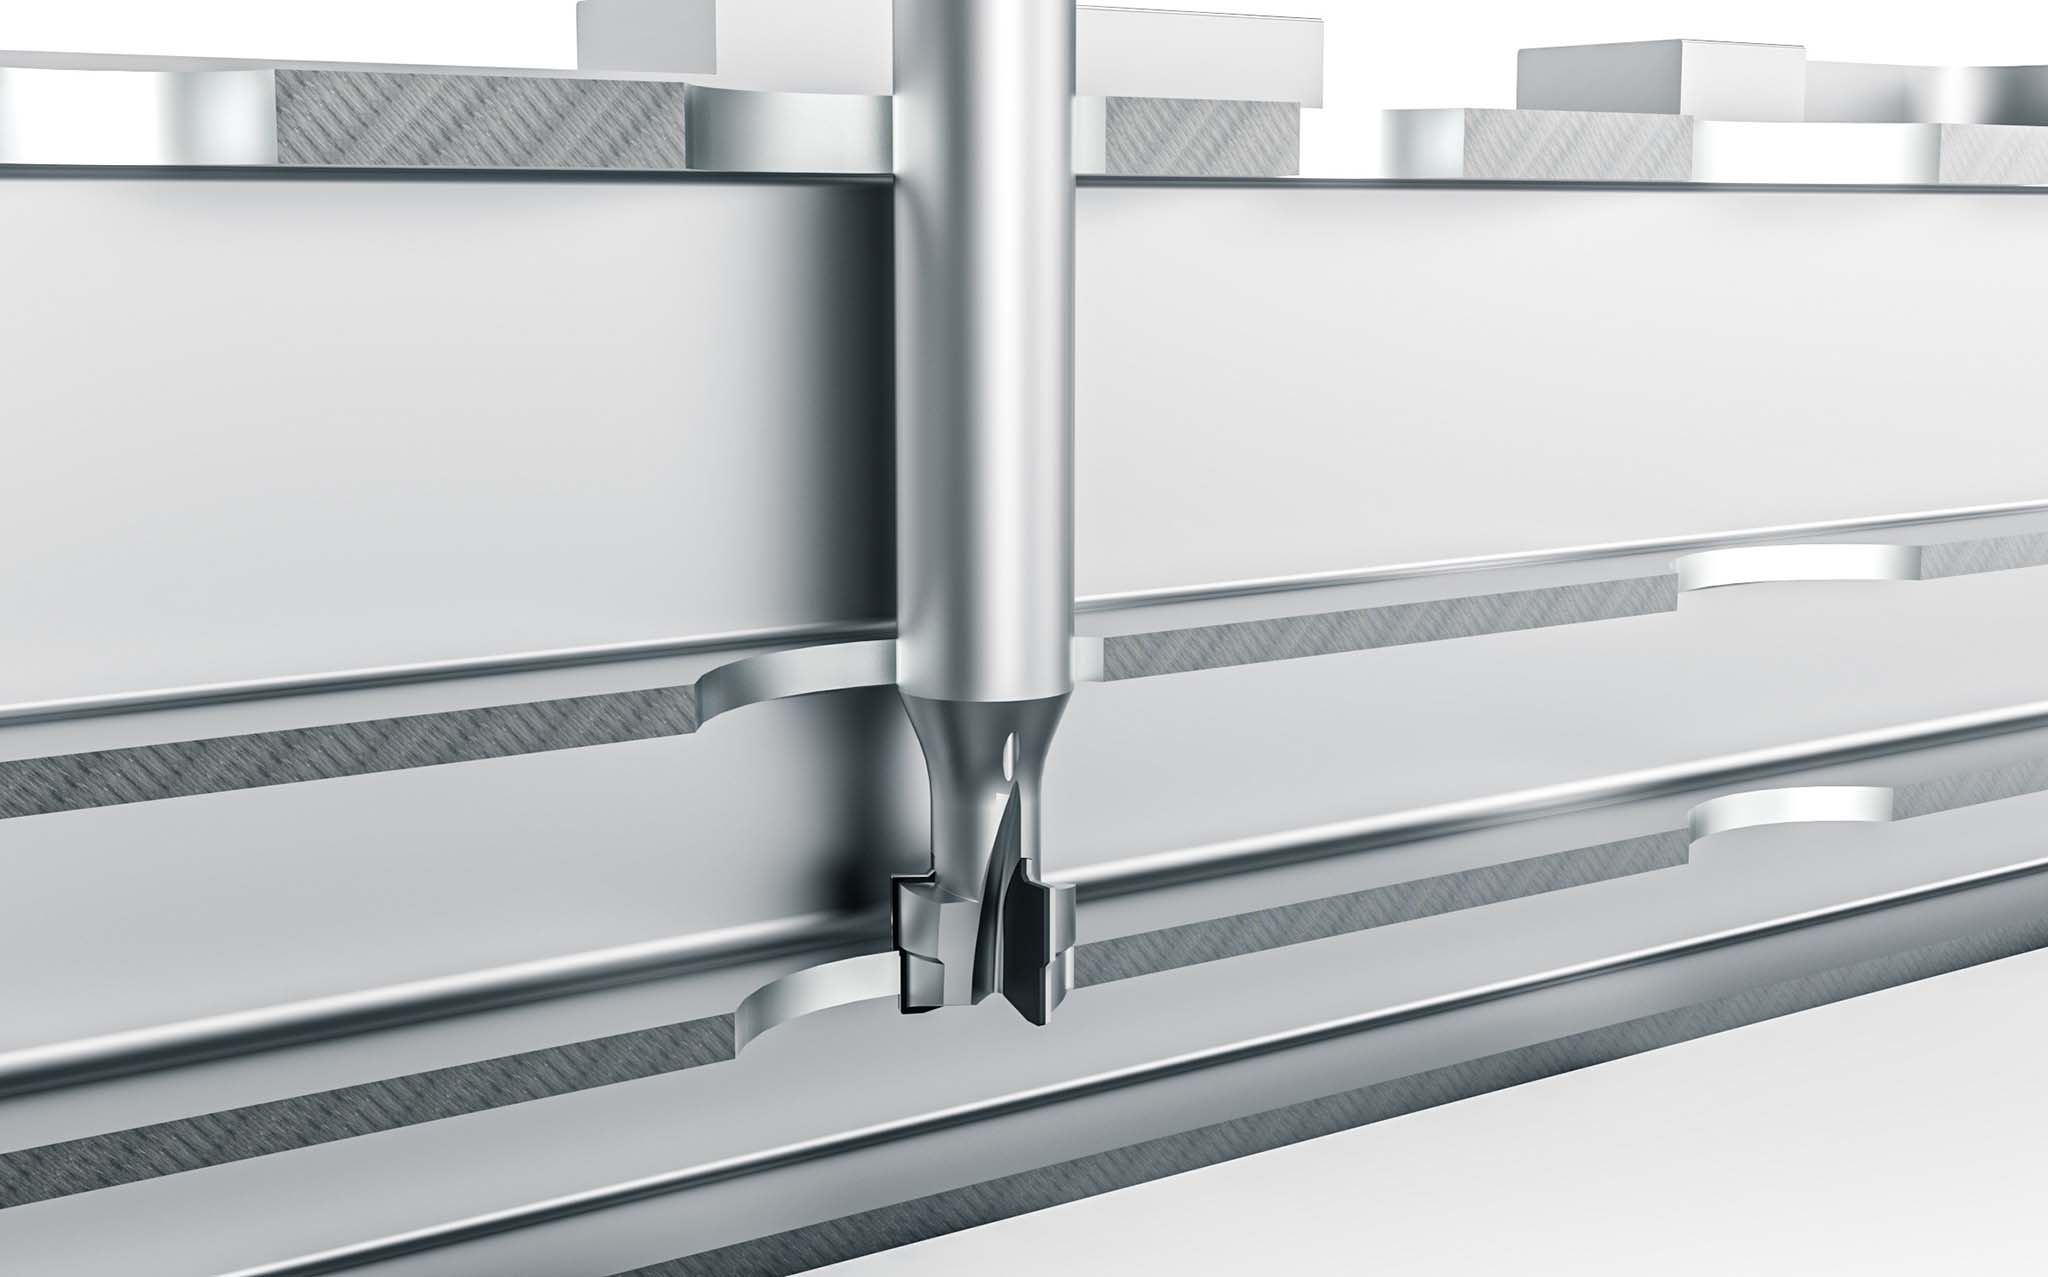
This advantage is brought to bear particularly when a bore has a larger diameter in one of the lower layers than the bore entrance at the top layer. “This can be done effectively with a reverse cutting edge on the milling cutter”, says Kucher. The alternative would be reclamping the workpiece in order to machine the bore from the bottom with a drill. A specially designed PCD milling cutter from MAPAL machines the bore at a spindle speed of 16,000 rpm, a cutting speed of 650 m/min and a feed of 0.063 mm.
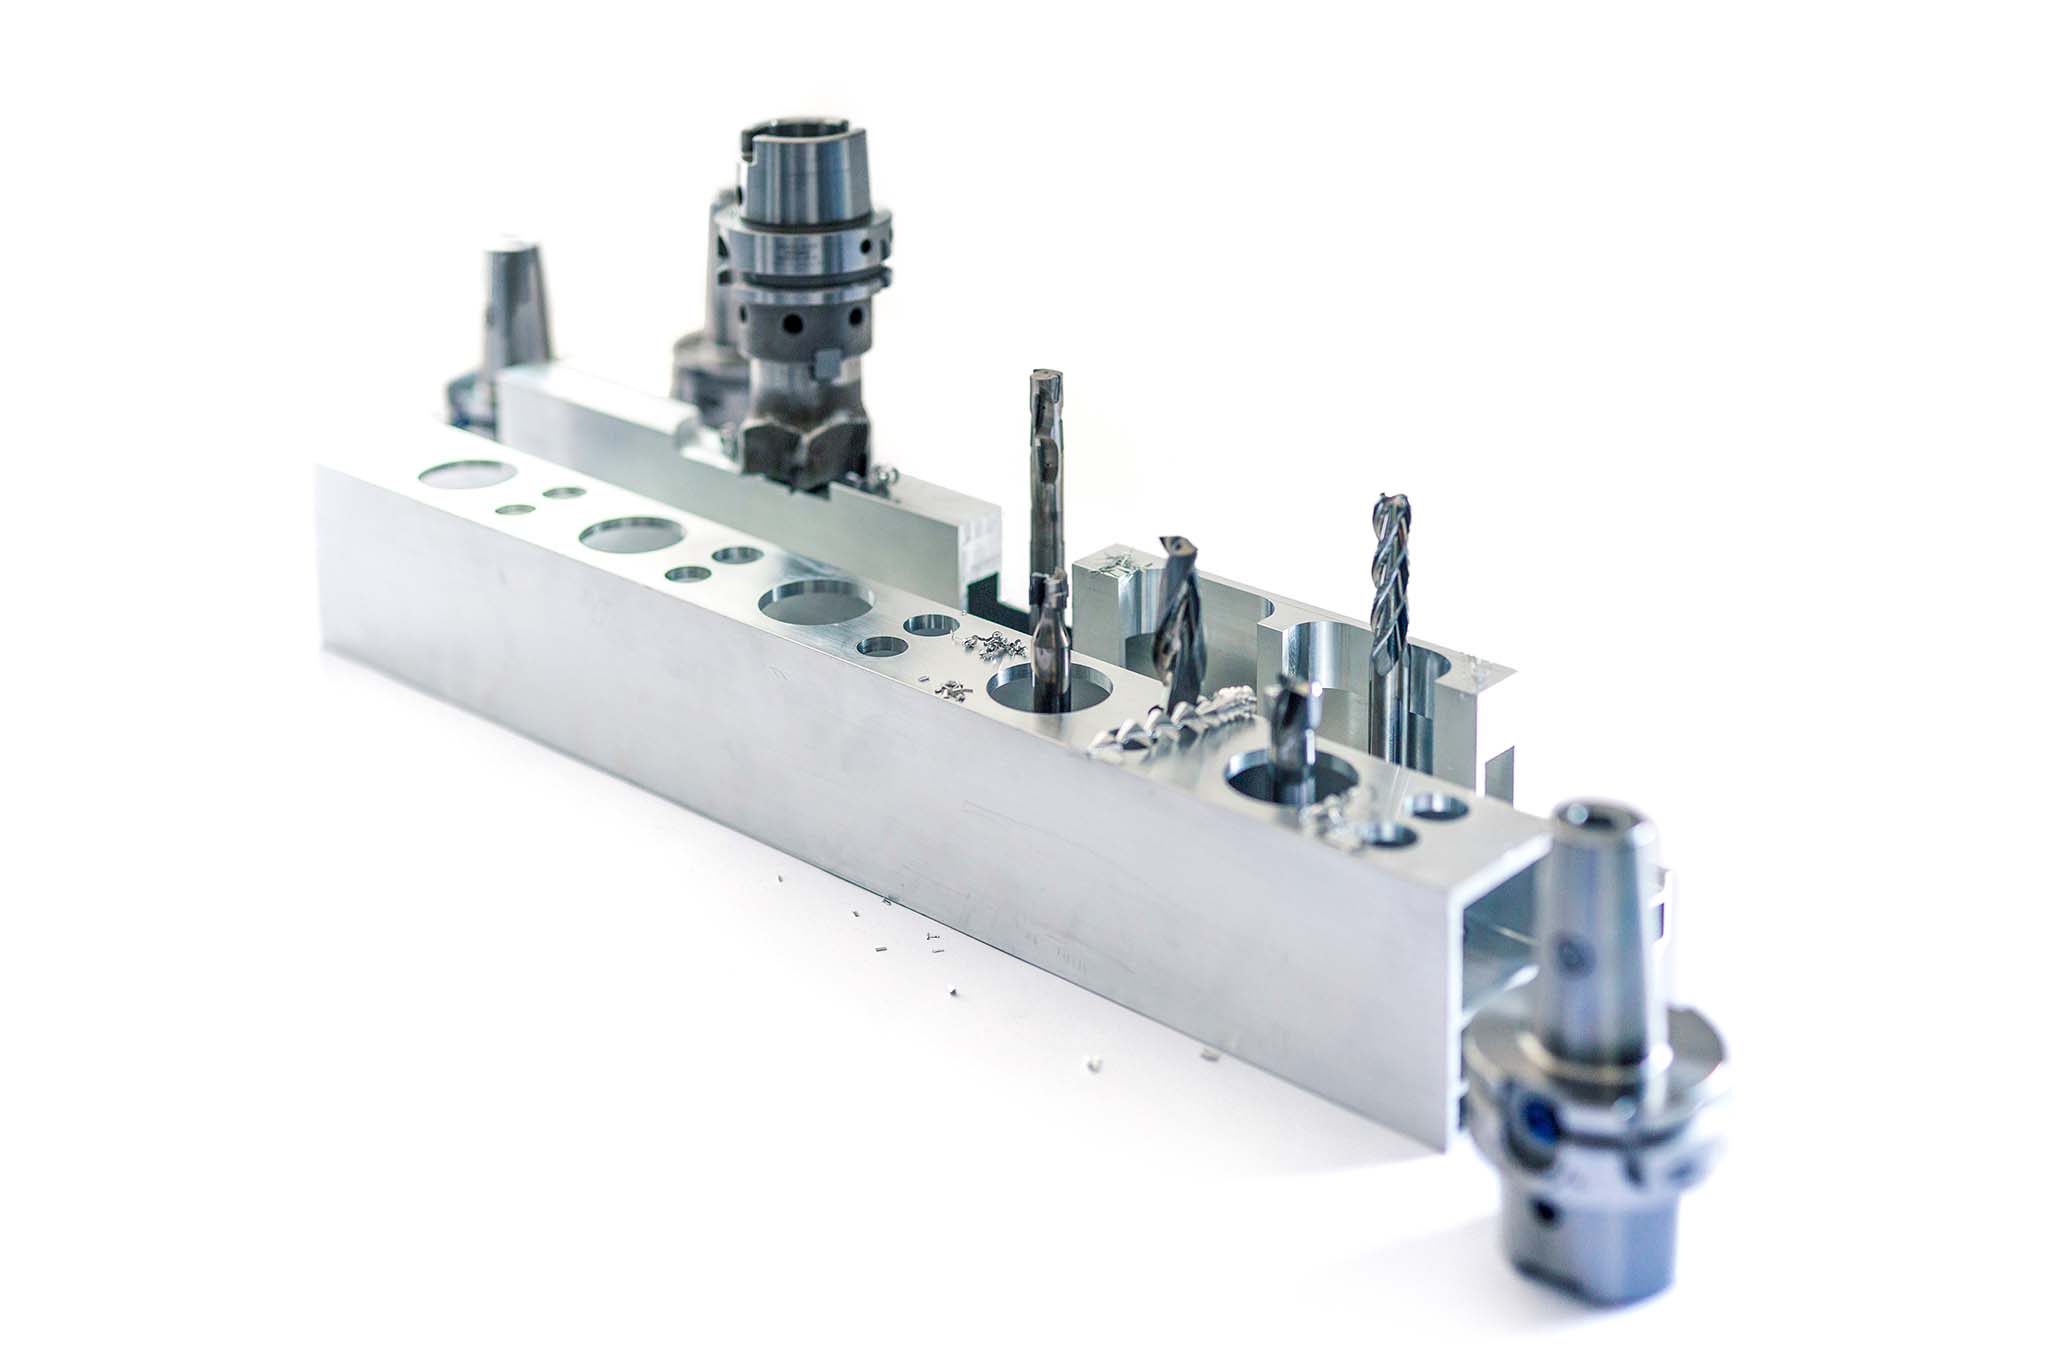
 
In total, seven tools are employed by the generic process to machine the battery frame  ©MAPAL

Optimal surfaces with the OptiMill-SPM-Finish
マパールでは、ポケットの仕上げ加工だけでなく、ショルダー、ポケット、スロットの荒加工にも OptiMill-SPM-Finish を推奨しています。 「最適な表面仕上げを実現し、大きなラッピングや高負荷がかかるコーナーでも安定して動作します」と Kucher 氏はこのツールについて語ります。 フルートを研磨しているため、切りくず排出機能も万全です。 このツールの特別な特徴は、 1 回の加工パスで大きな切込み深さできることです。 これにより加工時間が短縮され、生産コスト効率が良くなります。 バッテリーフレームの仕上げでは、最大 Rz = 1 µm の表面仕上げが達成可能です。 荒加工中は、主軸速度 10,981 rpm、切削速度 414 m/min、送り速度 0.12 ~ 0.22 mm で動作します。 送り 0.075 mm で仕上げ加工を行う場合、同じ主軸と切削速度が達成されます。
The specially designed PCD milling cutter machines both bores with different diameters.   ©MAPAL

In total, seven tools are used during the generic process, including six milling cutters: besides the OptiMill-SPM-Finish, amongst others the recently introduced FaceMill-Diamond-ES. In order to attain a perfectly harmonised system, all of the tools with cylindrical shanks are clamped in the new UNIQ chucks in the generic process.


“We can now offer our clients an all-round package to meet the challenges of machining battery frames, which includes PCD and solid carbide tools, chucks, and the corresponding process. For this we adapt the generic process for our customers based on their concrete situation”, Kucher explains.  

Kathrin Rehor, PR Project Manager at MAPAL

Contact

Kathrin Rehor Public Relations Kathrin.Rehor@mapal.com Phone: +49 7361 585 3342


Further articles from the e-mobility market