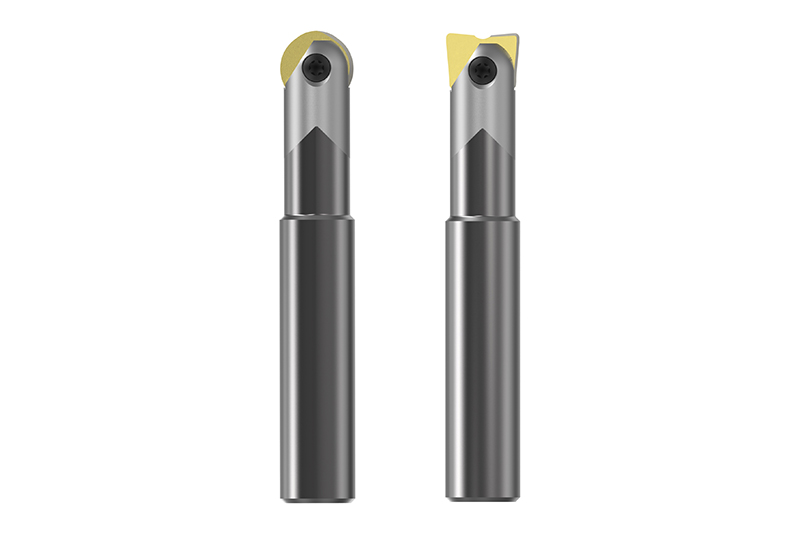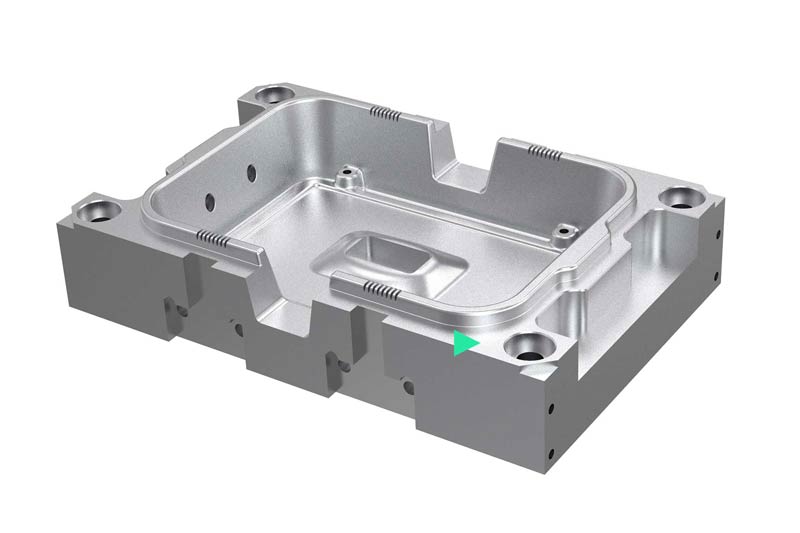
粗旋削
加工量の大半を占めるのが粗旋削加工です。高送り加工やトロコイドミリング加工などの特殊な加工方法により、加工時間を短縮し、経済性を高めることができます。交換可能な切削インサート付きツールや超硬ソリッドエンドミルに加え、特殊な粗削り形状を持つ高性能ミリングカッターも使用されます。
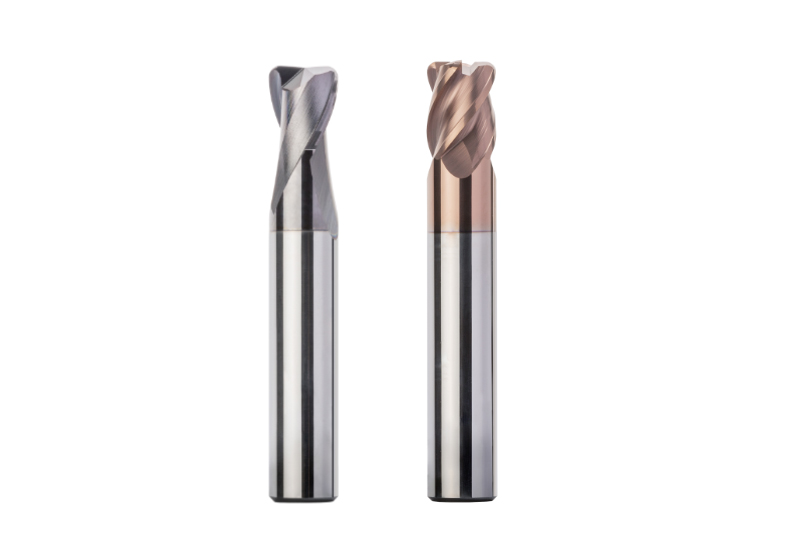
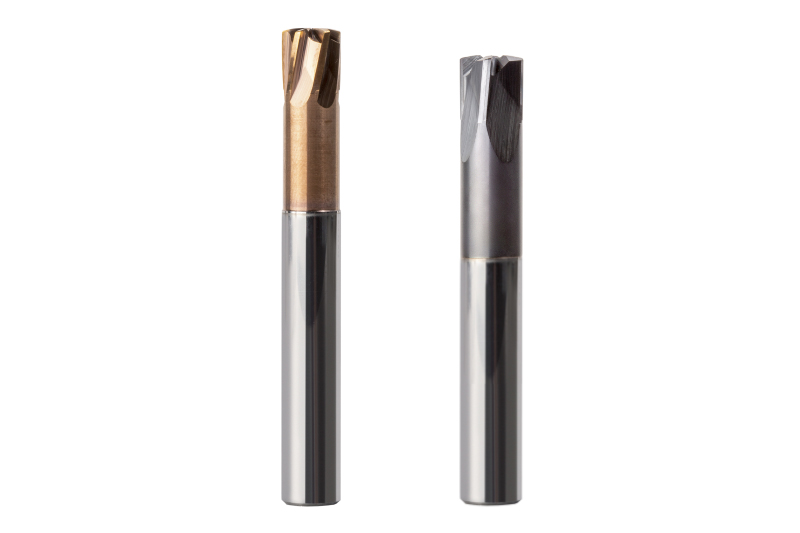
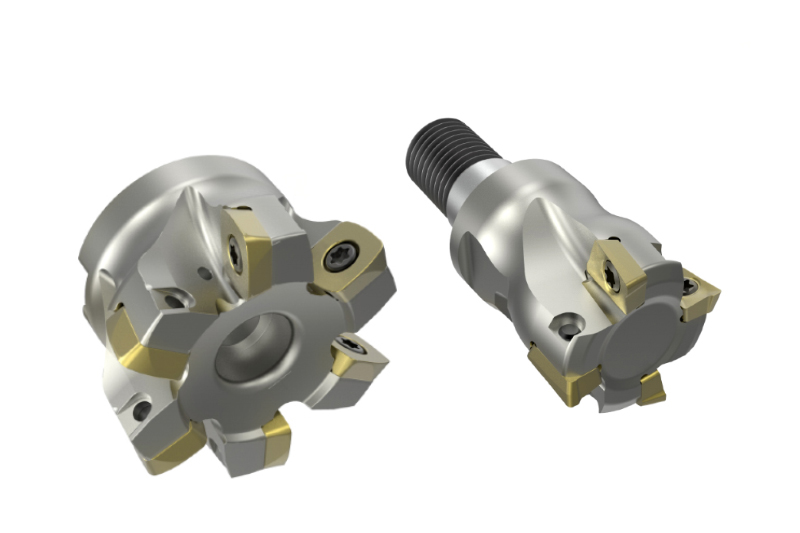
残材の粗旋削
粗旋削後、特にコーナー部やキャビティ部の残材を、二次加工でできるだけ一定の取り代になるように事前に機械加工します。通常、コーナーRのあるツールまたは高送りミリングカッターが使用されます。必要に応じて、球面シートカッターでコーナー部の残材を除去することも可能です。
Pre-finishing
If there are high demands on dimensional accuracy and surface finish, semi-finishing is recommended before finishing. With pre-finishing, machining approaches the final mould profile. The aim is to obtain a residual material that is as constant as possible in order to enable fast finishing with high demands on the surface quality. The stock removal after roughing is approx. 0.5-1 mm for hardened materials and 0.03-0.5 mm for soft materials. After pre-finishing, the constant stock removal is 0.05-0.1 mm for hardened materials or 0.1-0.3 mm for soft materials.
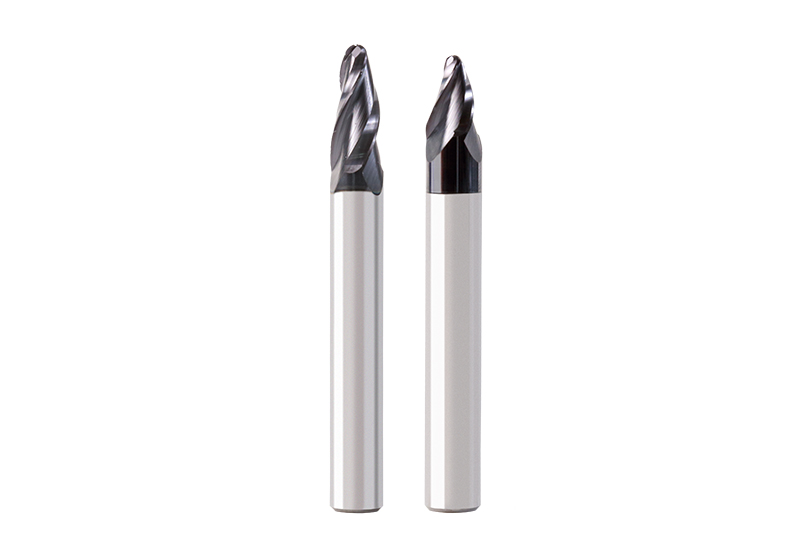
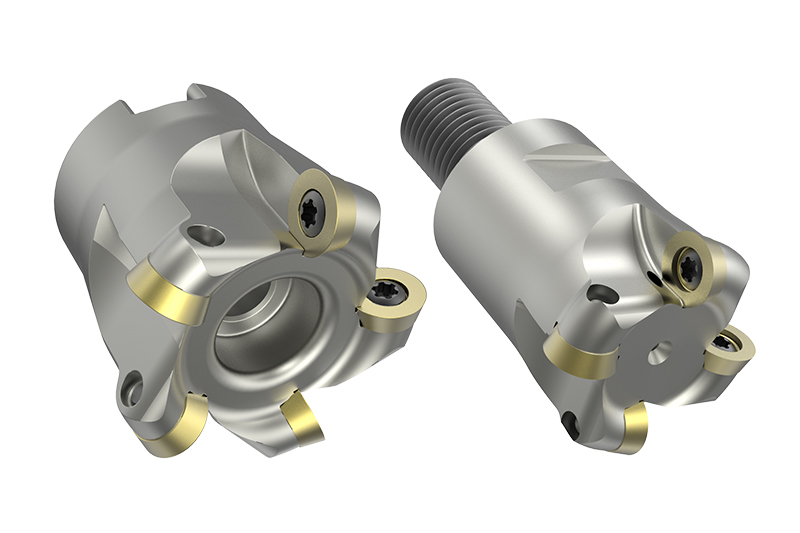
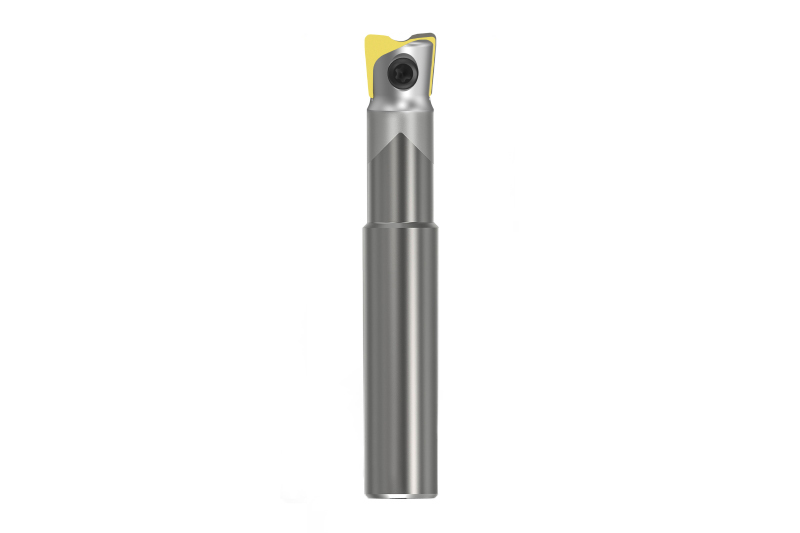
精加工
精加工去除剩余的加工余量以达到最终形状。在半精加工后,淬硬材料的加工余量为 0.05-0.1 mm,软质材料的加工余量为 0.1-0.3 mm。球形和/或圆角铣刀是首选刀具,具体取决于工件的最终轮廓。