Energy supply housing
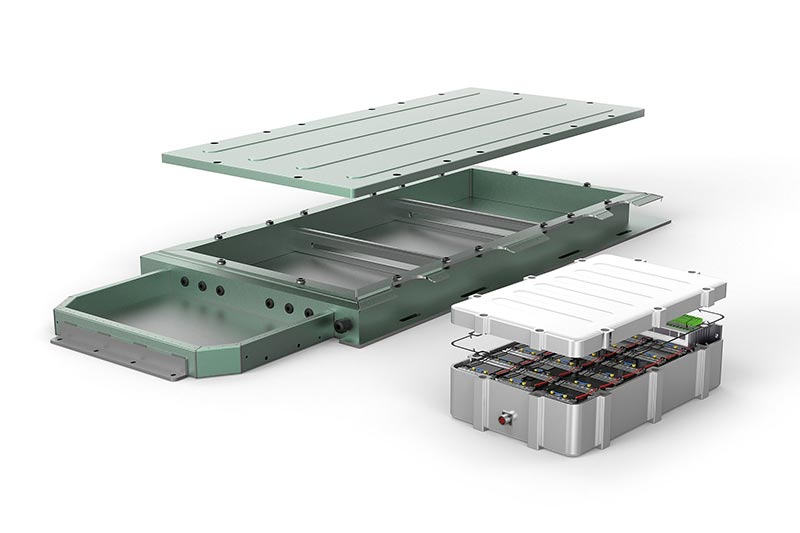
Different housings are used to protect electronic components, such as battery systems or power electronics, from external environmental influences and to attach the components to the interior in order to ensure that they function properly during vehicle operation. The requirements for the housing depend on the electronic system and drive concept. Different materials and manufacturing processes are currently used.
FEATURES
- Unstable, thin-walled components (susceptible to vibration)
- Construction as a cast tub or as a frame construction made of hollow profiles
- Partly low-silicon aluminium
- Large area (2 x 3 m)
- Mainly drilling and milling operations and threading
- Accuracy and surface requirements for cable bushing and cooling
connections


Panoramica degli utensili
-
 1 / 9
Standard programme for the machining of aluminium structural parts
- Highly positive cutting edge geometry
- Reduced cutting forces
- Low vibration cut
-
2 / 9
OptiMill-SPM-Rough
- Low vibration roughing with deep cutting depth
-
3 / 9
OptiMill-SPM
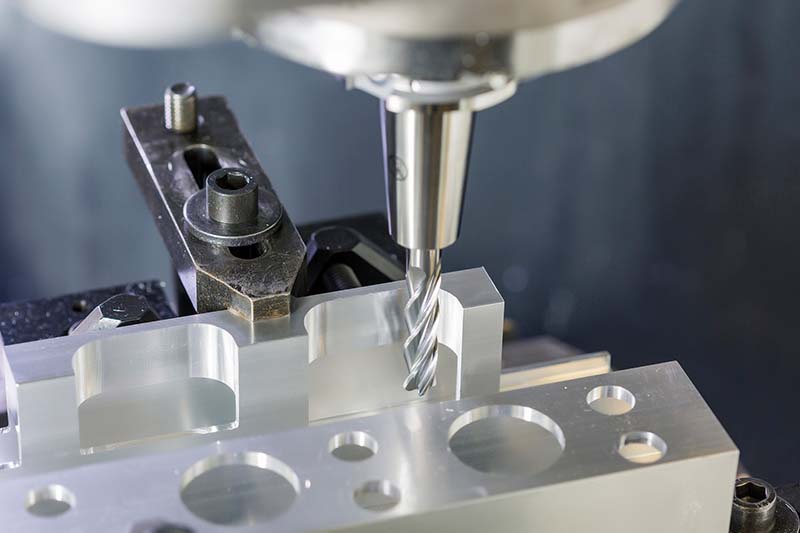
- Ideal for making openings or pockets
- Solid carbide design or with brazed PCD cutting edges
-
4 / 9
OptiMill-SPM-Finish
- Finishing of great depths in one go
- Strong performance with high wraps
-
5 / 9
Tritan-Drill-Alu
- Creation of core holes
- Three cutting edges for the highest feed rates
- Highest positioning accuracy through self-centring cross cutting edge
-
6 / 9
MEGA-Drill-Alu
- Solid carbide drill
- Drilling with lower cycle time
- Focus on chip formation
- Effective drilling processes with a larger number of equal diameters
-
7 / 9
FaceMill-Diamond-ES
- PCD face milling cutter
- Roughing and finishing of face surface
- Machining face surfaces with different stock removal using a single tool
- Roughing and finishing operations possible
-
8 / 9
OptiMill-Diamond-SPM
- PCD milling cutter
- Circular milling operations of various diameters and surfaces
- Less tool changes thanks to flexible tool deployment
-
9 / 9
OptiMill-Alu-HPC-Pocket
- Corner milling cutter
- Pocket milling of aluminium materials
- Optimum chip removal
- Optimum stability


-
1 / 5
PCD milling cutter overview
-
2 / 5
PCD milling cutter with alternately arranged cutting edges
- Low cutting forces over the entire machining depth
-
3 / 5
Spiralled PCD milling cutter
- Finishing of thin-walled structures
-
4 / 5
PCD Helix milling cutter
- Trimming with a large cutting depth
-
5 / 5
PCD face milling cutter
- Face milling for a cutting depth of up to 10 mm
- Creation of defined surface profiles for sealing and contact surfaces


Case studies from the energy supply sector
-
03.11.2022
Efficient deburring with robots
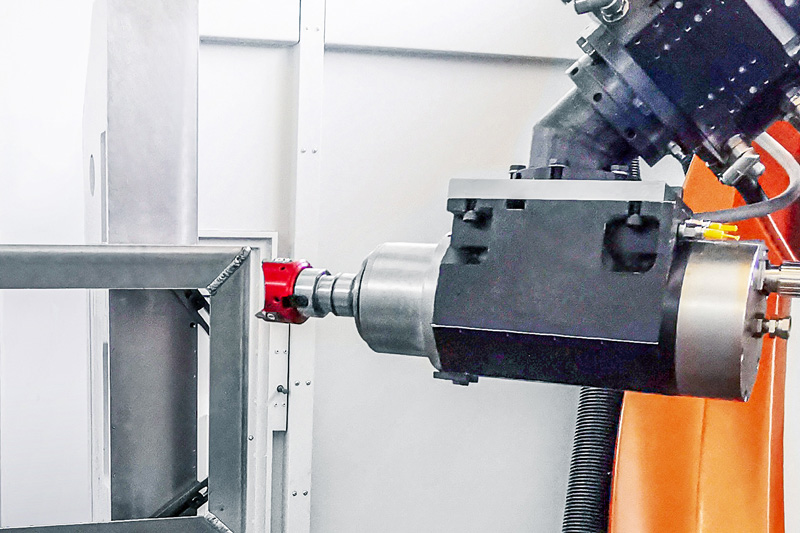
The FlyCutter from MAPAL is ideally suited for deburring battery trays. Robot manufacturer KADIA is enthusiastic about the PCD-tipped milling tool.
-
11.05.2023
A strategy for battery frames
MAPAL’s electric mobility experts have designed a generic component that encompasses the main machining operations of a battery frame.
-
12.07.2023
Milling instead of drilling
Why milling instead of drilling can be a sensible alternative? MAPAL shows how higher process reliability and shorter machining times can be achieved.