
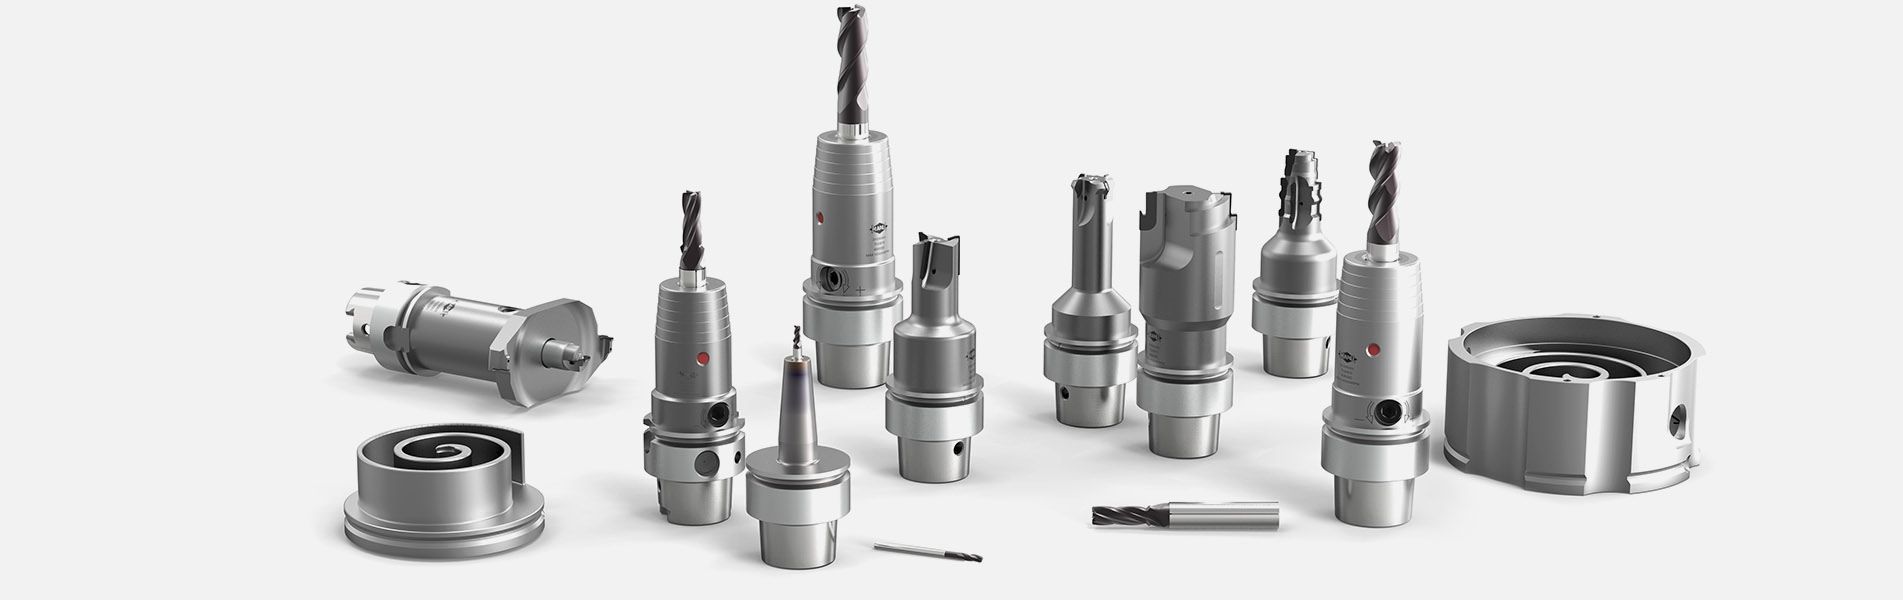
Series production of scroll compressors
Scroll compressors have been successfully used in air-conditioning applications and heat pumps for quite some time. They stand out thanks to their high cooling capacity and reliability as well as excellent energy efficiency and low noise emission. With electrification, they are also increasingly finding their way into the automotive sector, primarily as refrigeration compressors for air conditioning systems.
At the heart of each scroll compressor are two interlocking spirals (fixed scroll and moving orbiting scroll) whose opposing movements compress the medium. The level of efficiency depends, in particular, on how precisely these parts are manufactured. In this regard, the requirements on form and position tolerances lie within the range of a few μm.
MAPAL offers the complete process for machining scroll compressors from a single source. Three specific machining operations on an aluminium scroll compressor for use in an electrified vehicle are presented as examples.
At the heart of each scroll compressor are two interlocking spirals (fixed scroll and moving orbiting scroll) whose opposing movements compress the medium. The level of efficiency depends, in particular, on how precisely these parts are manufactured. In this regard, the requirements on form and position tolerances lie within the range of a few μm.
MAPAL offers the complete process for machining scroll compressors from a single source. Three specific machining operations on an aluminium scroll compressor for use in an electrified vehicle are presented as examples.
High-precision spiral shapes
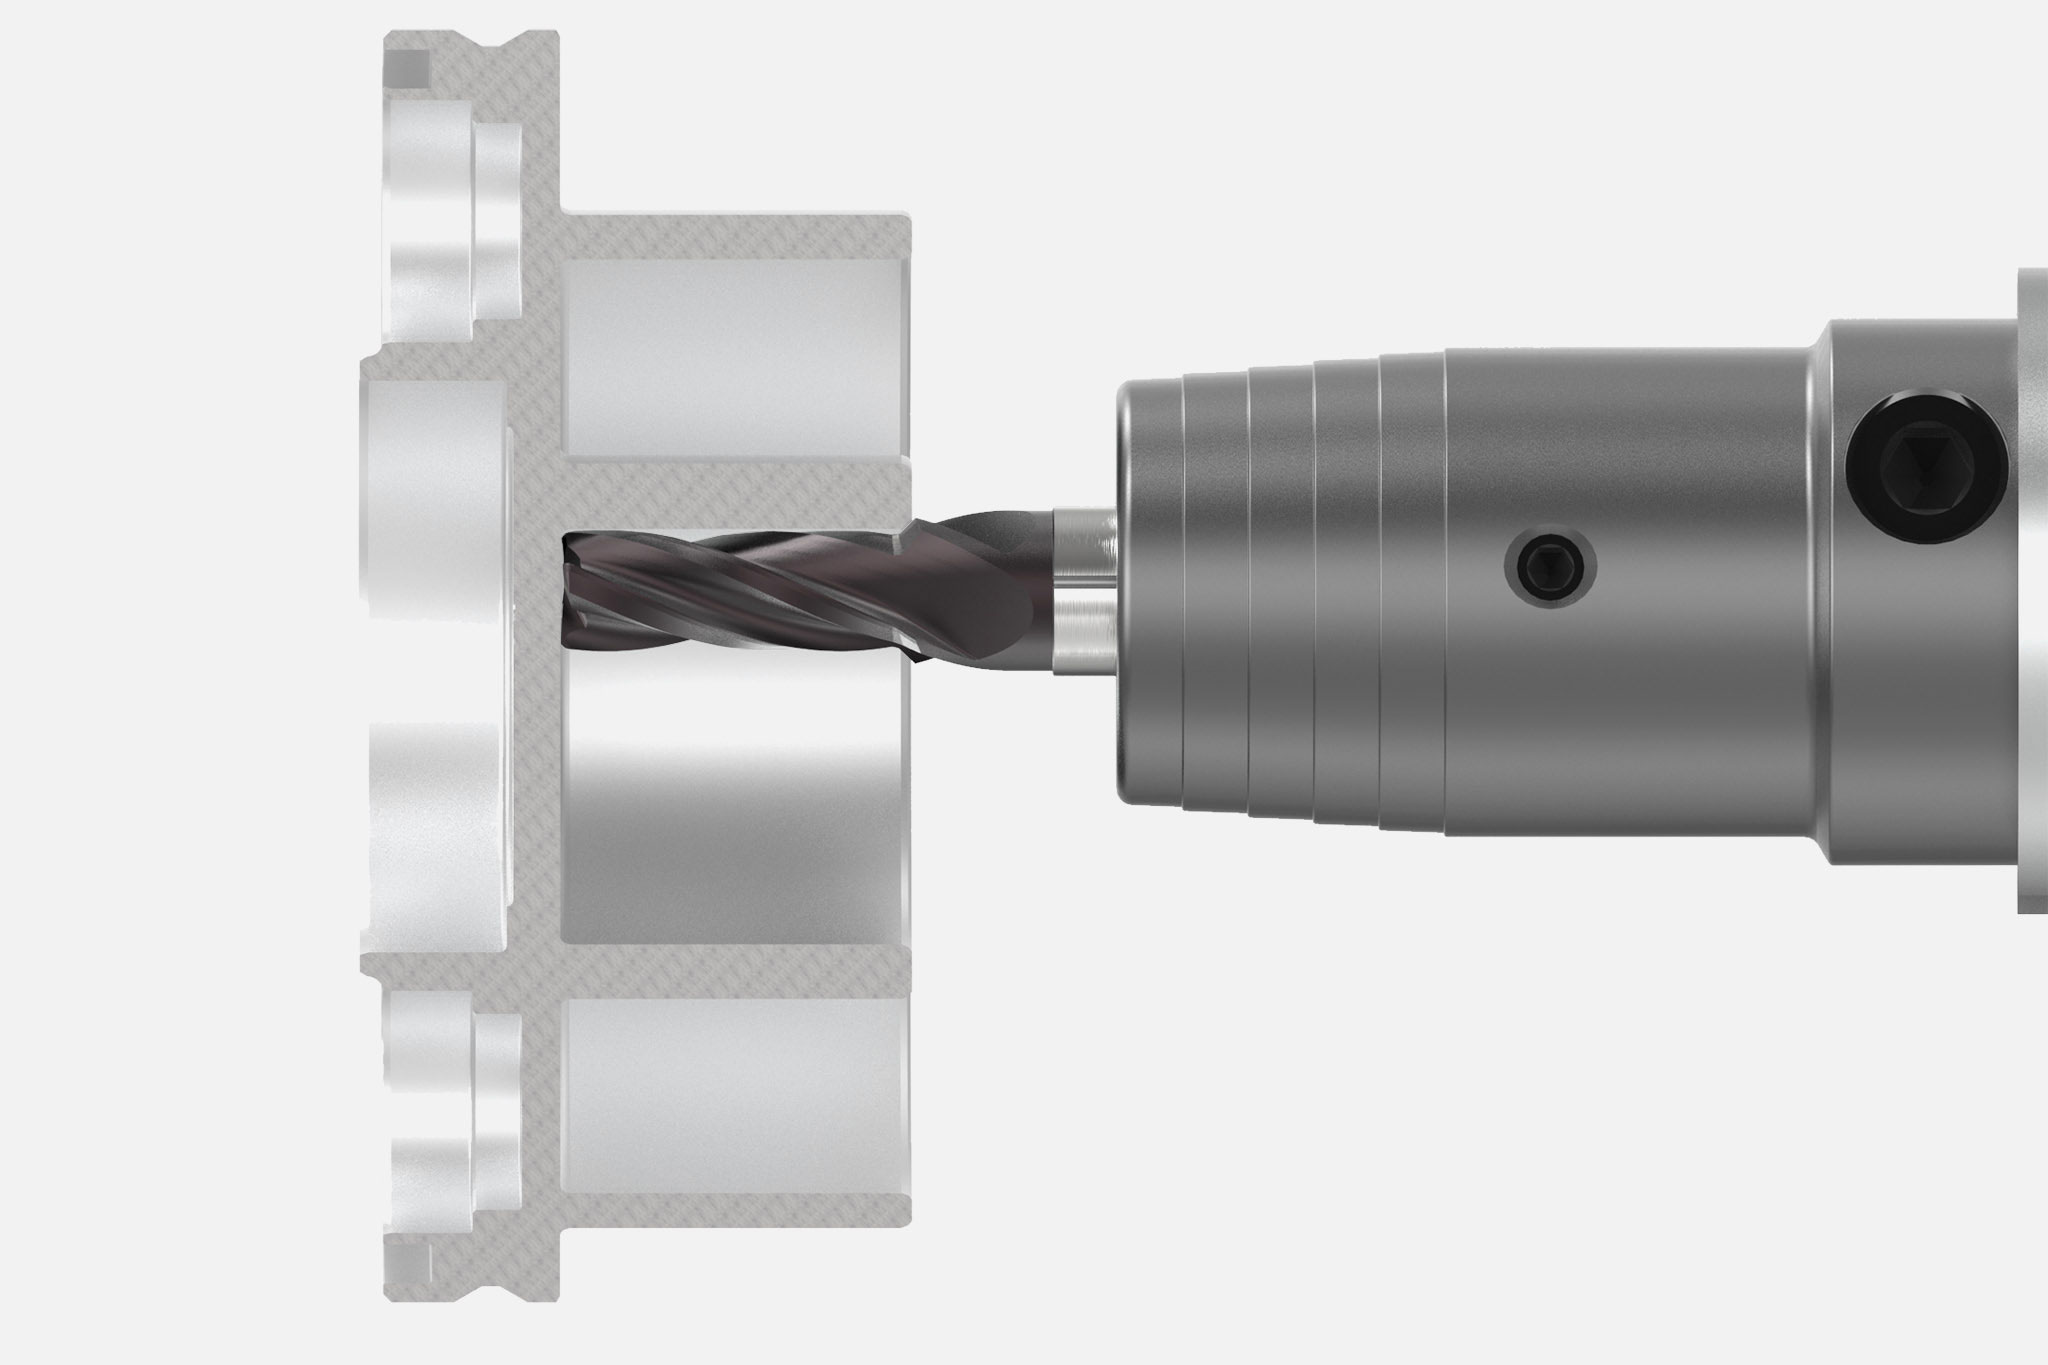
The machining of the spiral poses a particular challenge as it must have a defined squareness of less than 0.02 mm and an average roughness depth in the single-digit µm range. Despite these requirements in addition to the thin walls and the depth of the part, the finishing process should be carried out in one process.
The pre-machining and fine machining of the spirals is carried out with two three-edged milling cutters made of solid carbide. The decisive factor is the high accuracy of the tools, which ensures that the tolerances in radial and axial run-out are less than 10 µm. The extremely sharp cutting edges ensure high dimensional accuracy. The reinforced core diameter makes them particularly stable. Finely finished chip flutes ensure safe and fast chip removal.
The finishing milling cutter is fitted with an additional chamfer on the diameter. The machining of the base, wall and the chamfer on the front face of the part can be carried out in a single step, and the tool reliably satisfies the tight tolerances with regard to perpendicularity and surface.
The pre-machining and fine machining of the spirals is carried out with two three-edged milling cutters made of solid carbide. The decisive factor is the high accuracy of the tools, which ensures that the tolerances in radial and axial run-out are less than 10 µm. The extremely sharp cutting edges ensure high dimensional accuracy. The reinforced core diameter makes them particularly stable. Finely finished chip flutes ensure safe and fast chip removal.
The finishing milling cutter is fitted with an additional chamfer on the diameter. The machining of the base, wall and the chamfer on the front face of the part can be carried out in a single step, and the tool reliably satisfies the tight tolerances with regard to perpendicularity and surface.
准确的轴承孔
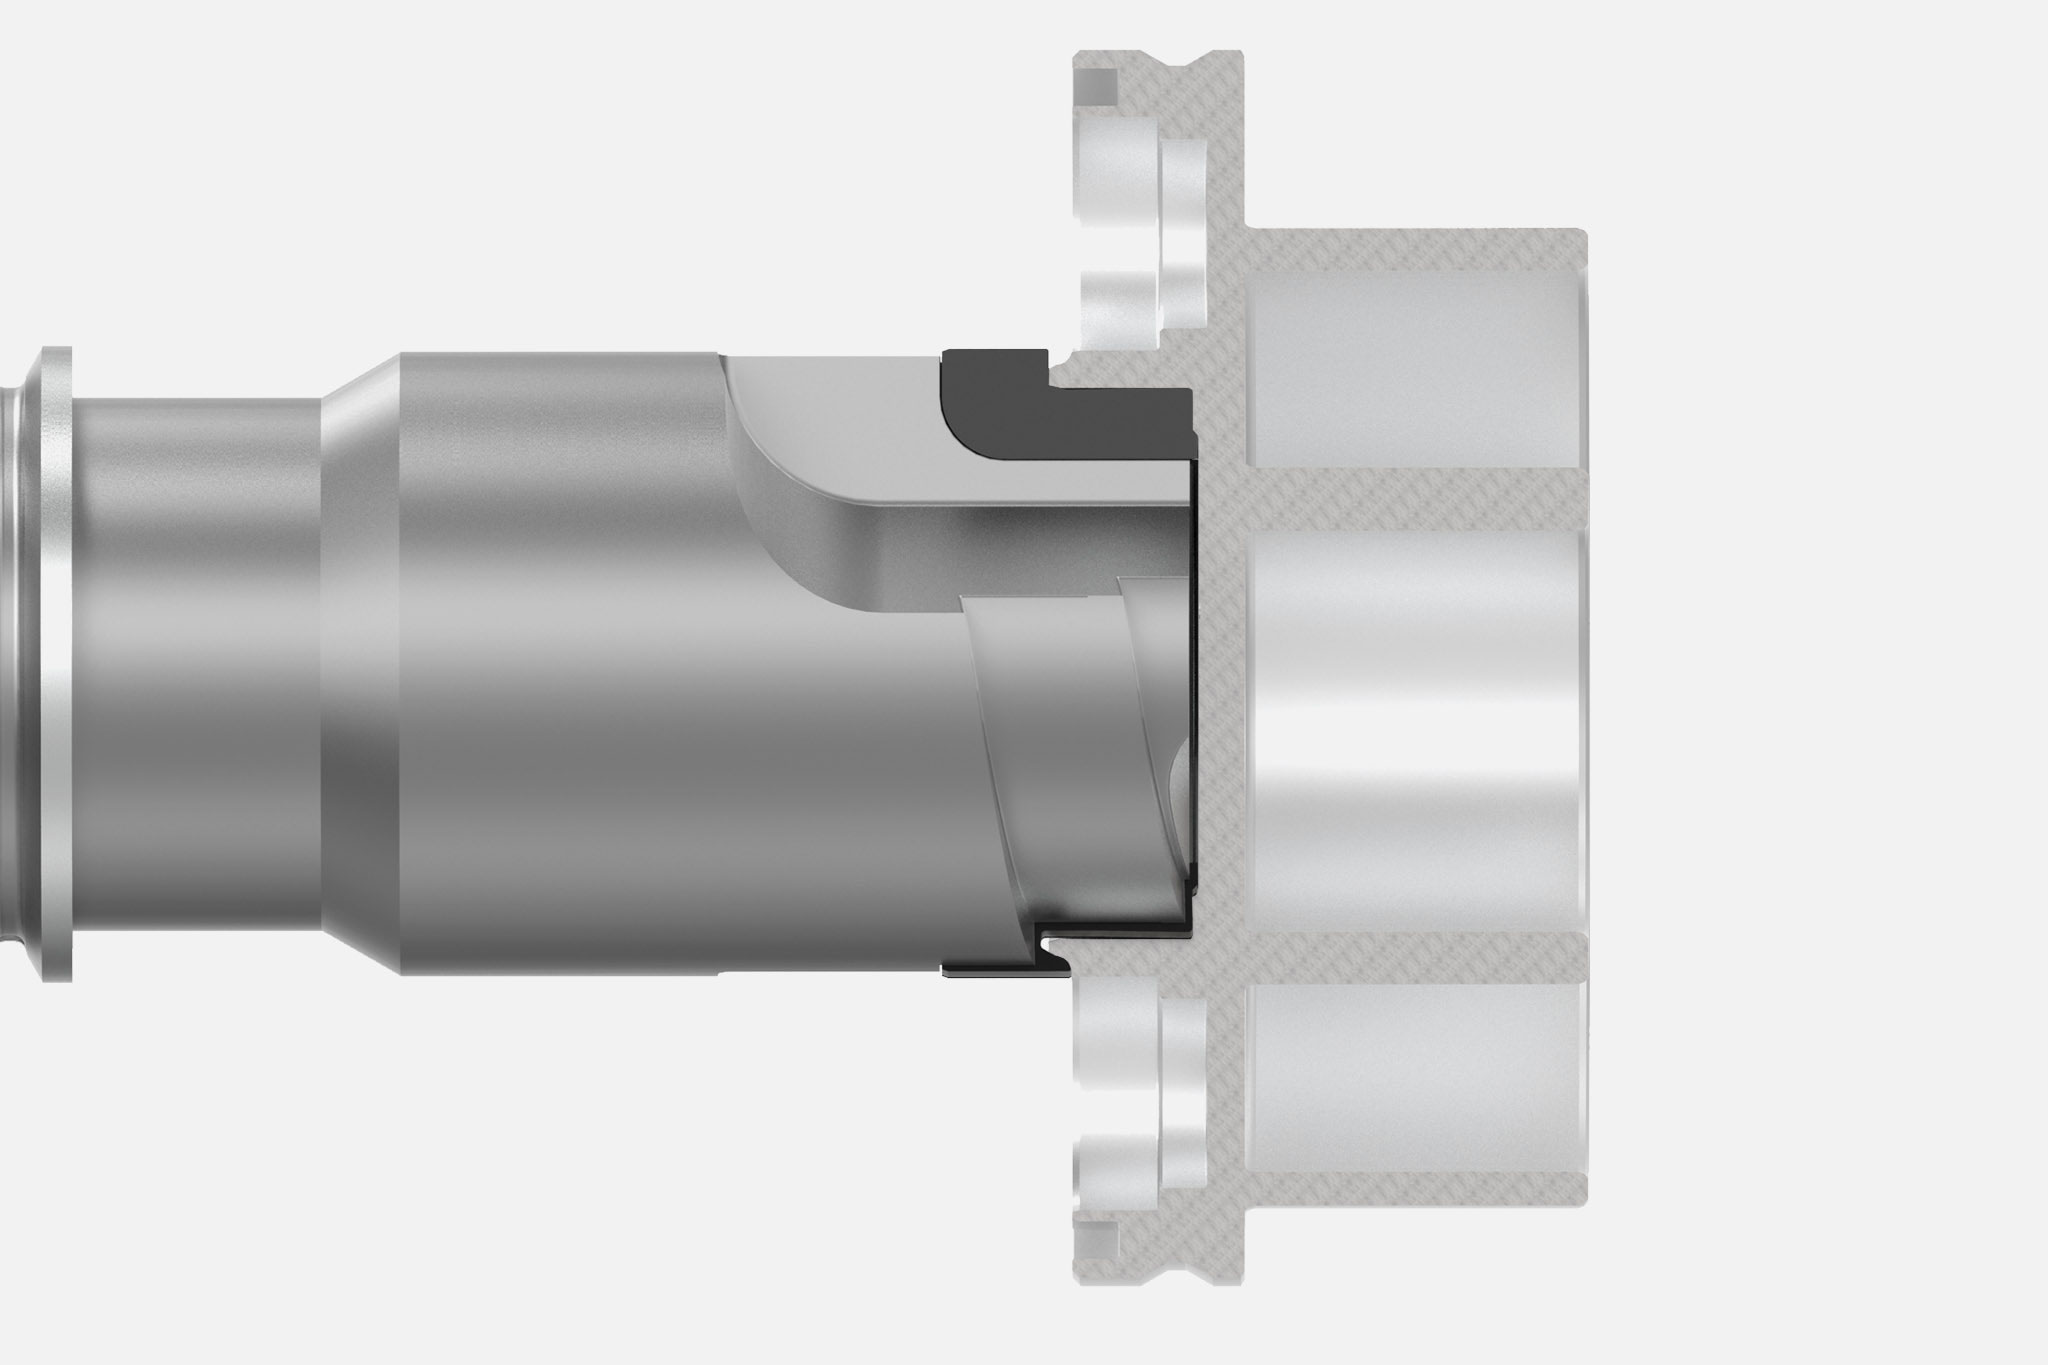
驱动轴将由一个滑动轴承或球轴承支承,沿着摆线移动驱动涡旋盘。此时的轴承孔精度对两个螺旋槽的相互定位起决定性作用。
用一把三刃PCD铣刀首先通过圆周铣削进行粗加工。紧接着对轴环进行铣削。对轴承孔通过一把两刃PCD两阶镗孔刀进行精加工。第一阶加工轴承孔的大直径,第二阶加工轴环。为了降低切削力,对切削量进行合理分配至关重要。
用于密封件的凹槽
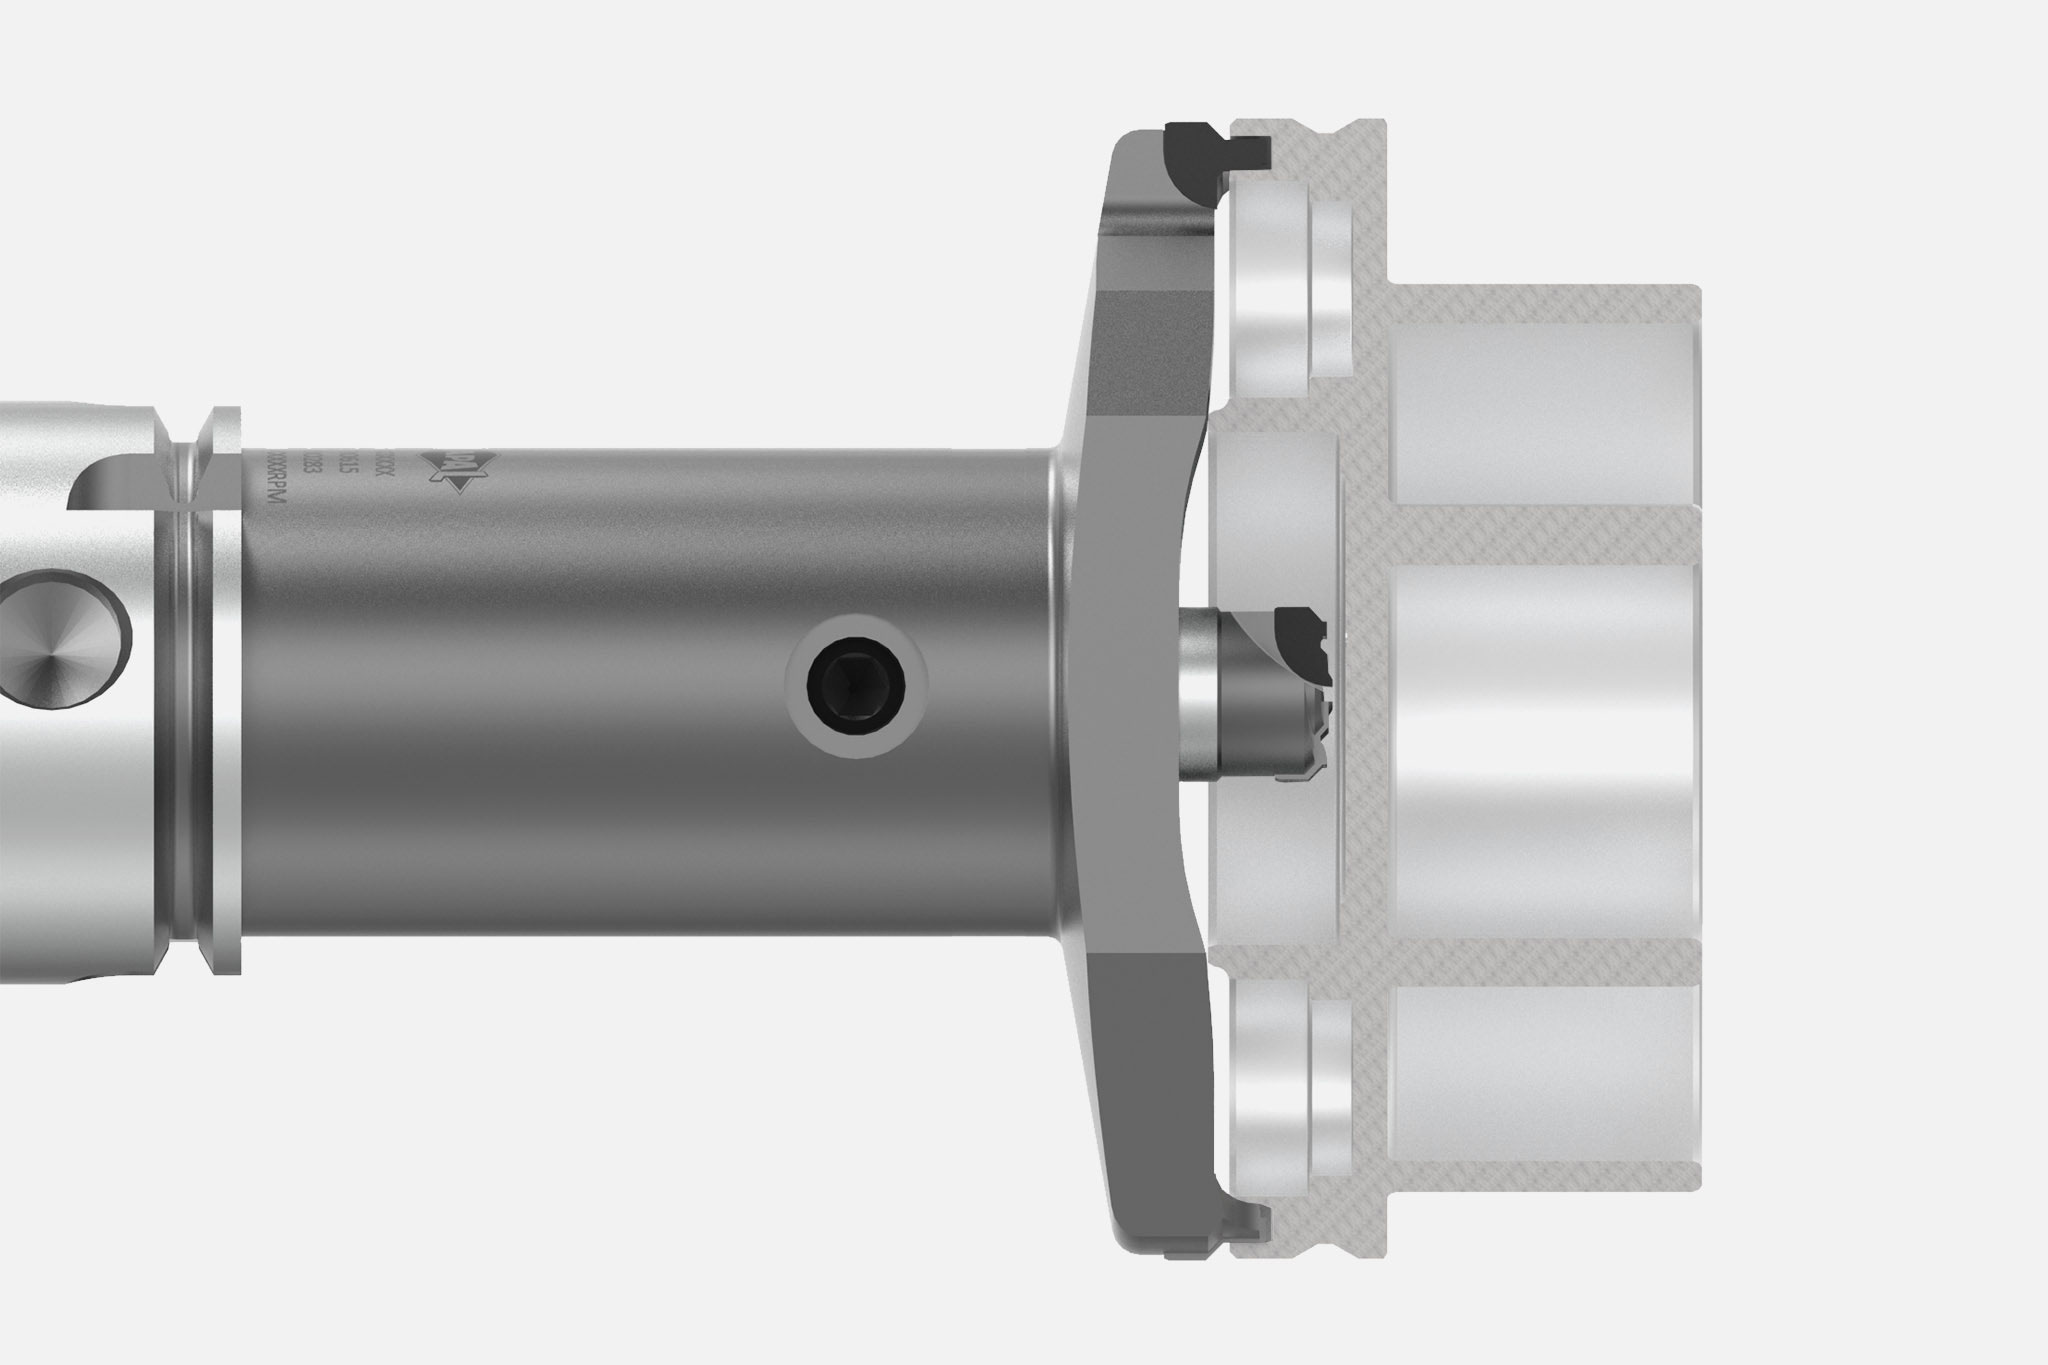
可以附加使用密封件以密封连接孔或整个系统,来最小化制冷剂从高压侧到低压侧之间的流量。为了容纳这些密封件需要加工出相应的凹槽。这类凹槽的粗加工和精加工都通过采用两刃 PCD-镗孔刀完成。此间必须合理分配切削量以降低切削力。
精加工刀具采用组合刀具,由此可以附加加工出固定涡旋盘背面上的连接孔中的凹槽。PCD-刀片上的断屑槽确保更好的控制切屑并提高过程的安全性。
您的直接联系方式
联系人
Matthias Winter 行业管理汽车行业 matthias.winter@mapal.com +49 7361 585 3360