
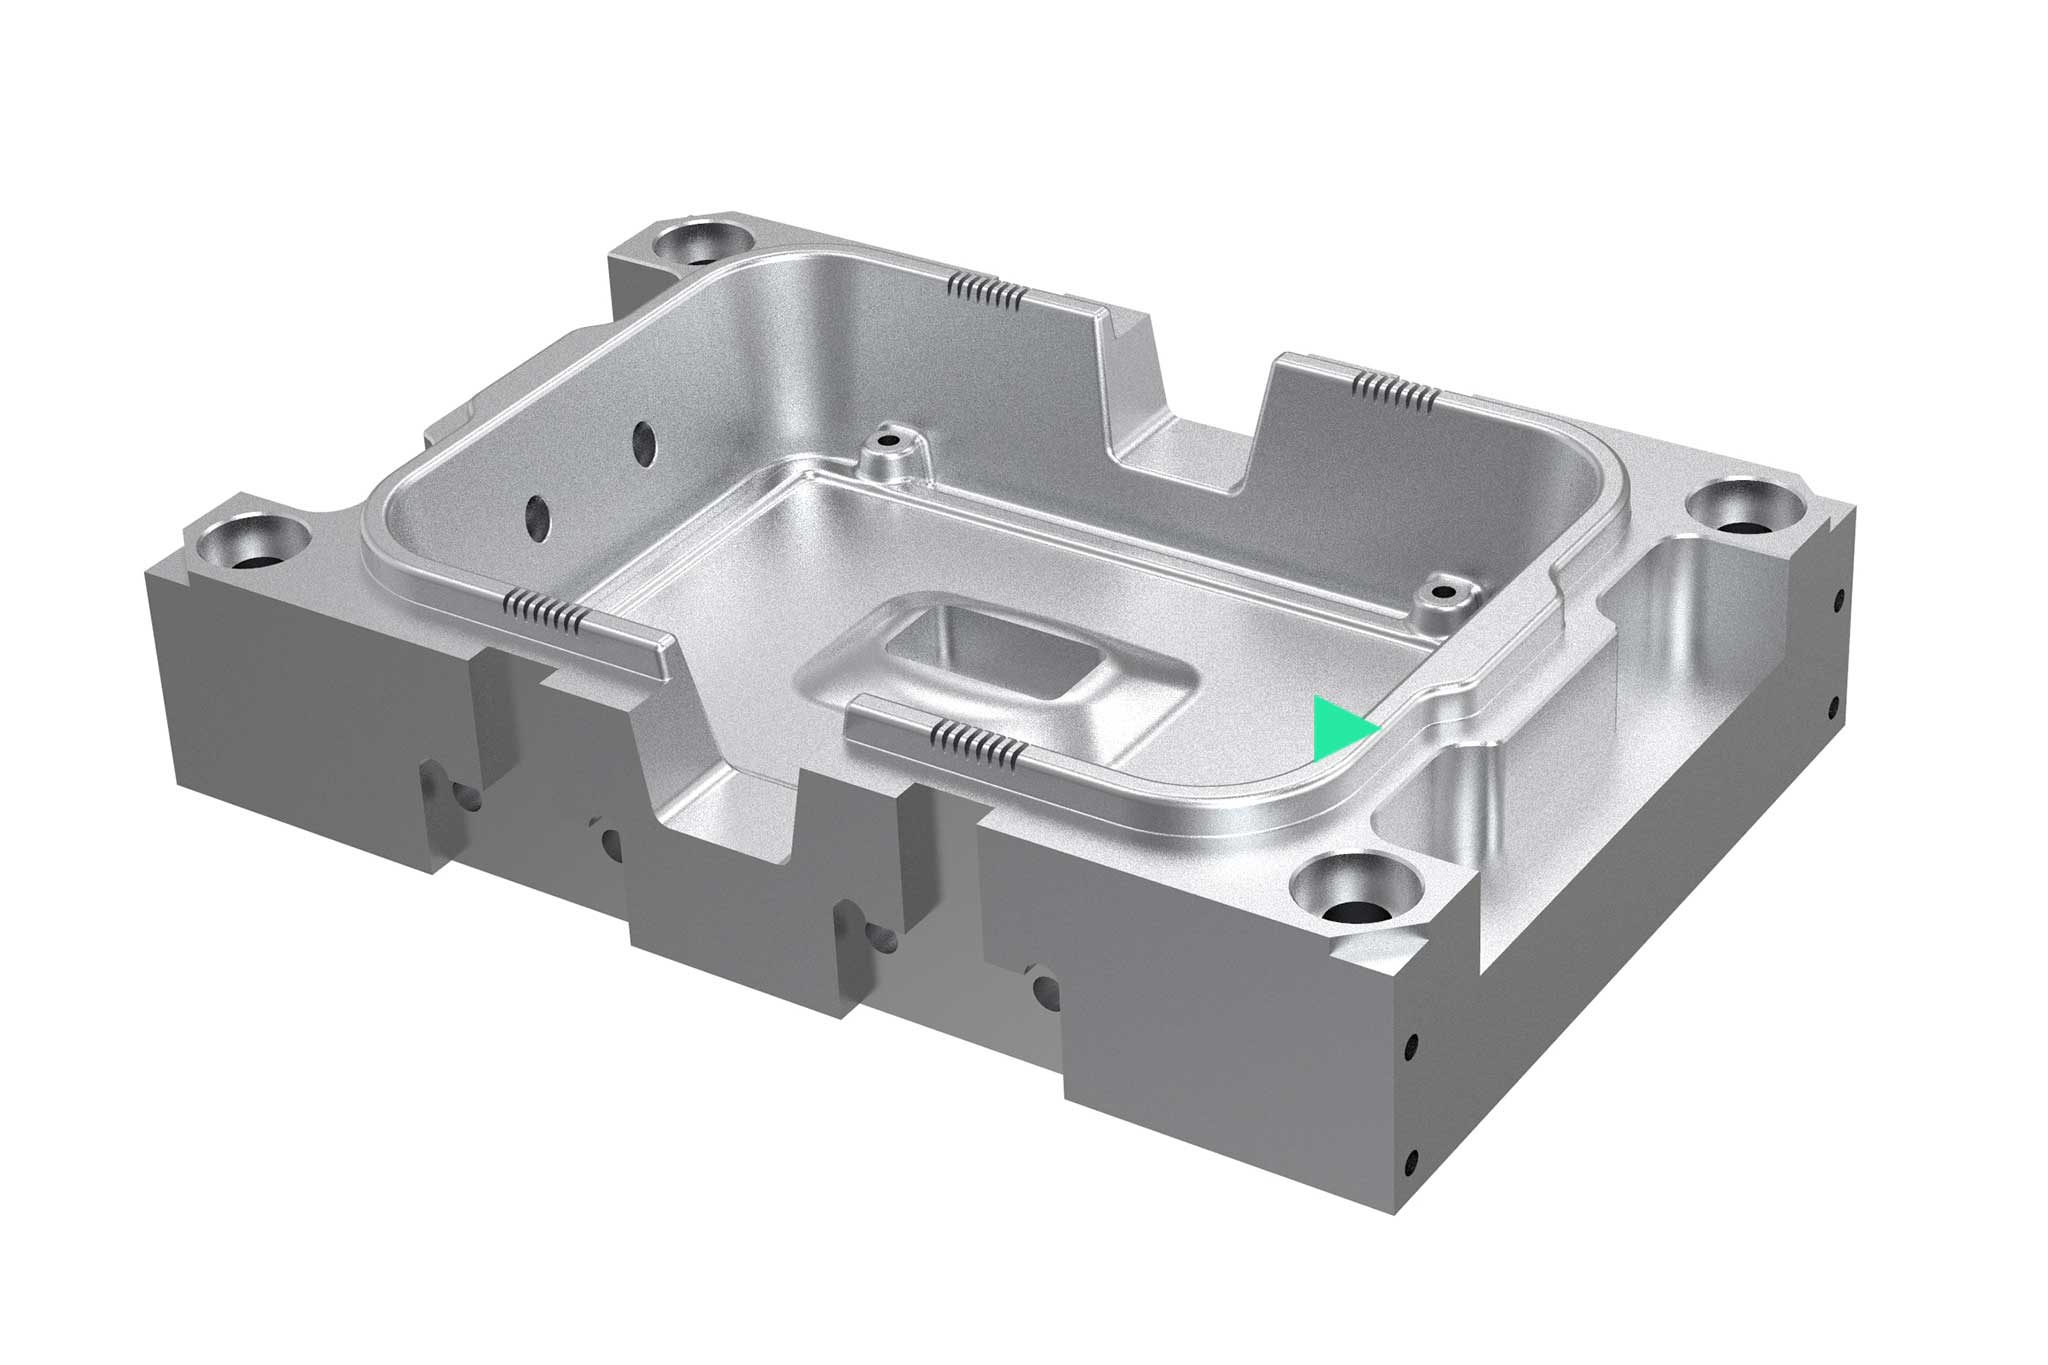
粗加工
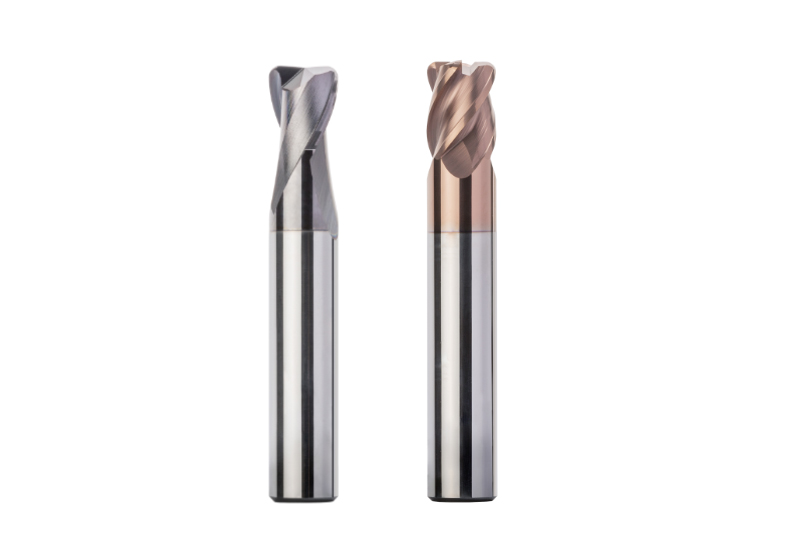
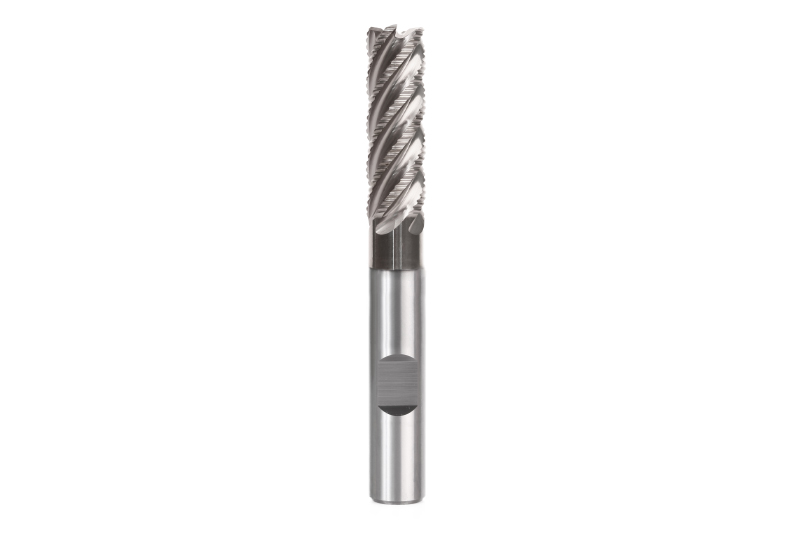
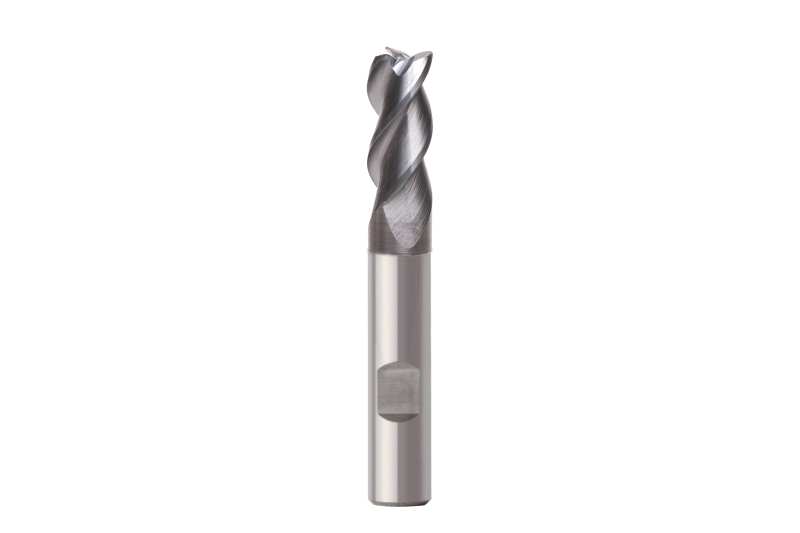
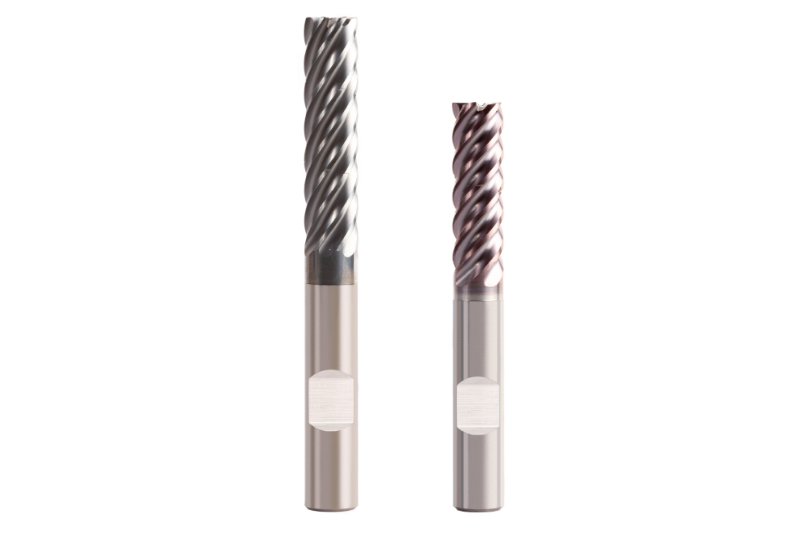
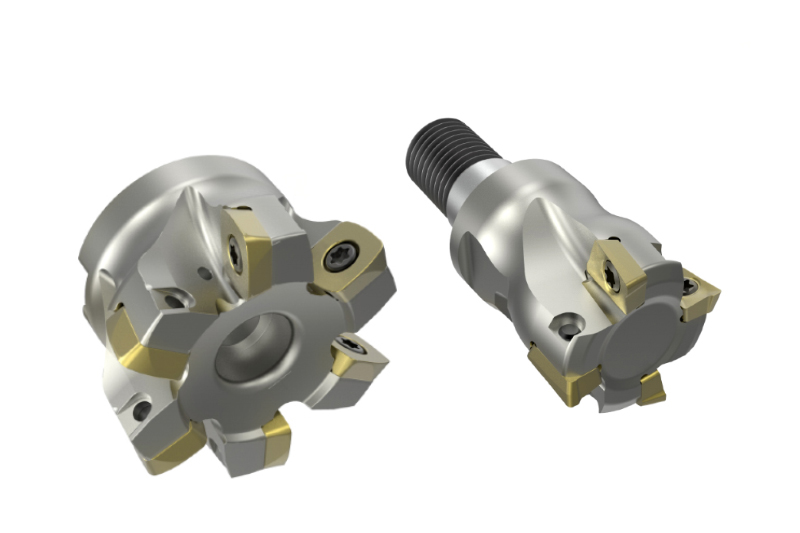
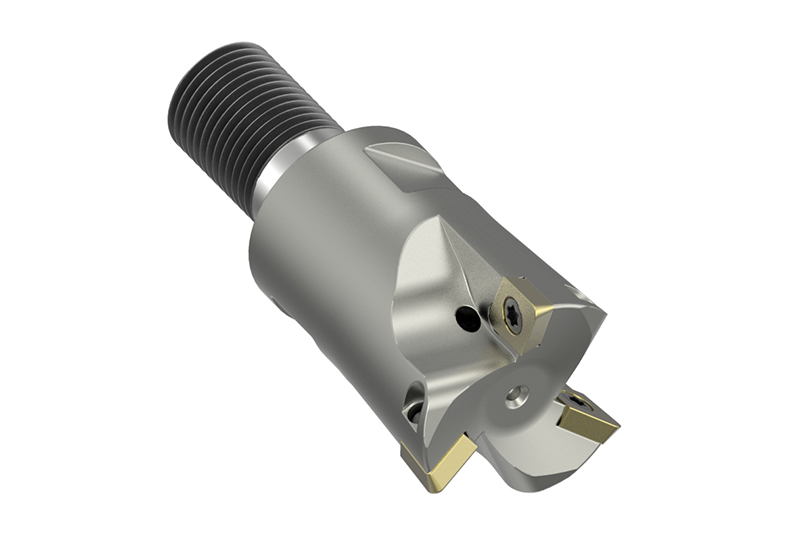
粗加工操作负责大部分的切削加工量。特殊铣削策略,例如高进给加工或摆线铣削,可以减少加工时间,从而提高经济效率。除了带有可转位刀片的刀具和整体硬质合金铣刀外,还使用了具有特殊粗加工几何形状的高性能铣刀。
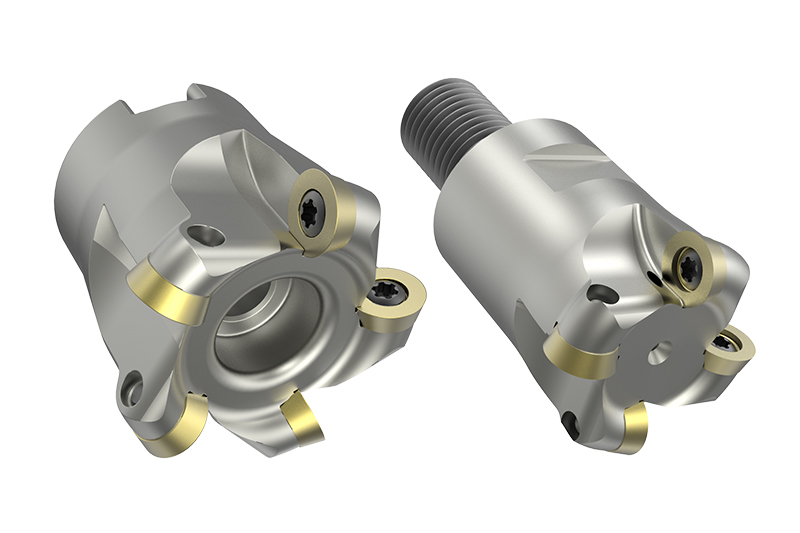
粗加工剩余材料
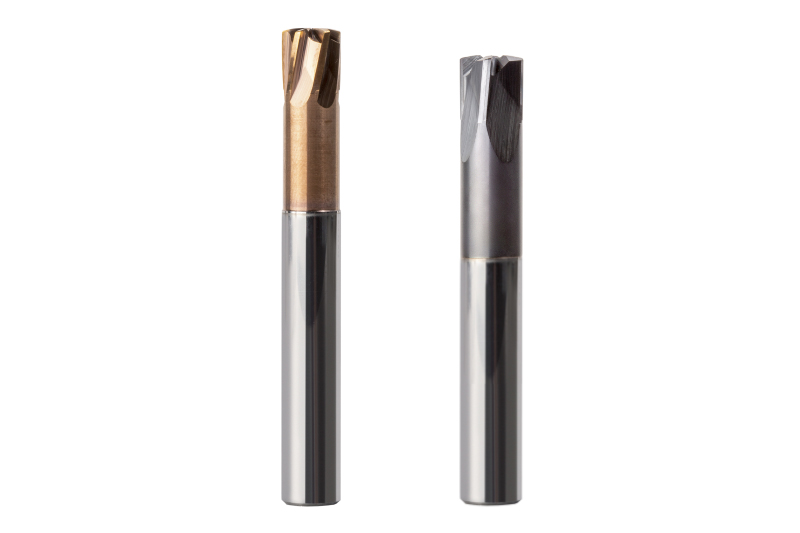
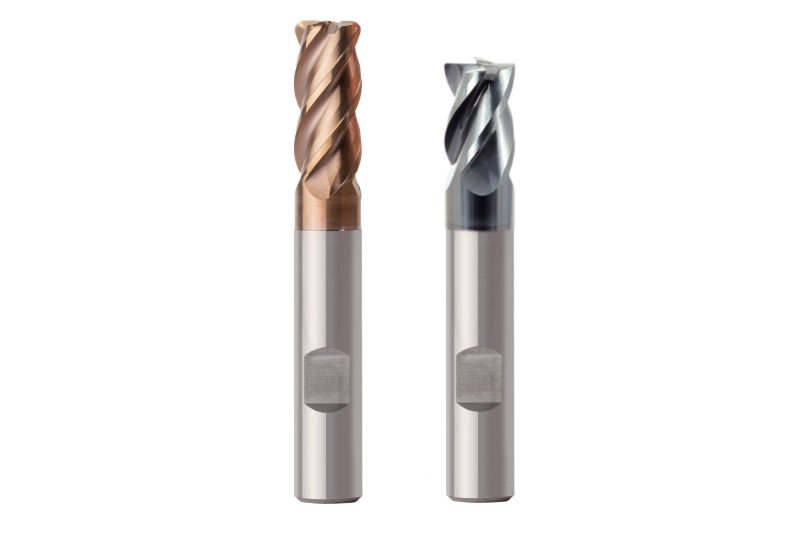
粗加工后,在第二个加工步骤中,用户对剩余材料进行加工,特别是在圆角和型腔中,使其加工余量尽可能恒定。通常使用具有圆角的刀具或高进给铣刀。如有必要,球形铣刀也可以去除角落中的残留材料。
半精加工
对尺寸精度和表面质量要求较高时,建议在精加工前进行半精加工。通过半精加工,加工接近最终的形状轮廓。目的是获得尽可能恒定的残余材料,以实现对表面质量要求高的快速精加工。粗加工后的加工余量对于淬硬材料约为 0.5-1 mm,对于软质材料约为 0.03-0.5 mm。在半精加工后,淬硬材料的恒定加工余量为 0.05-0.1 mm,软质材料为 0.1-0.3 mm。
Acabamento
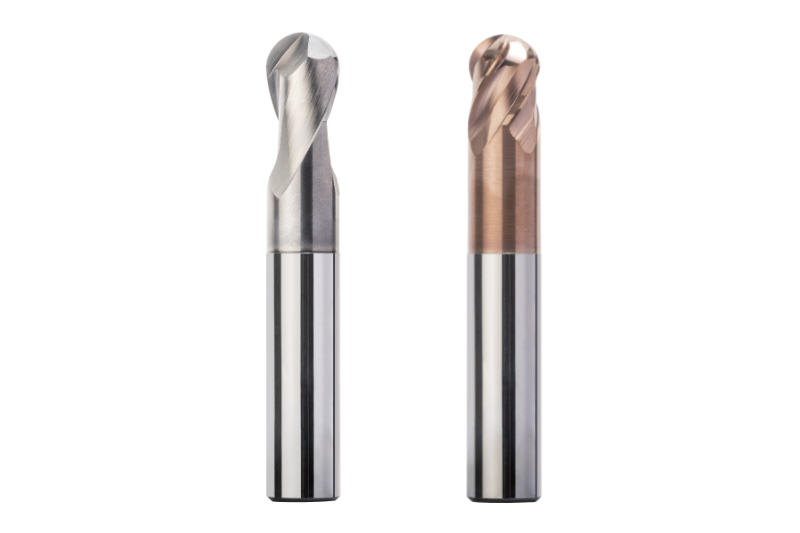
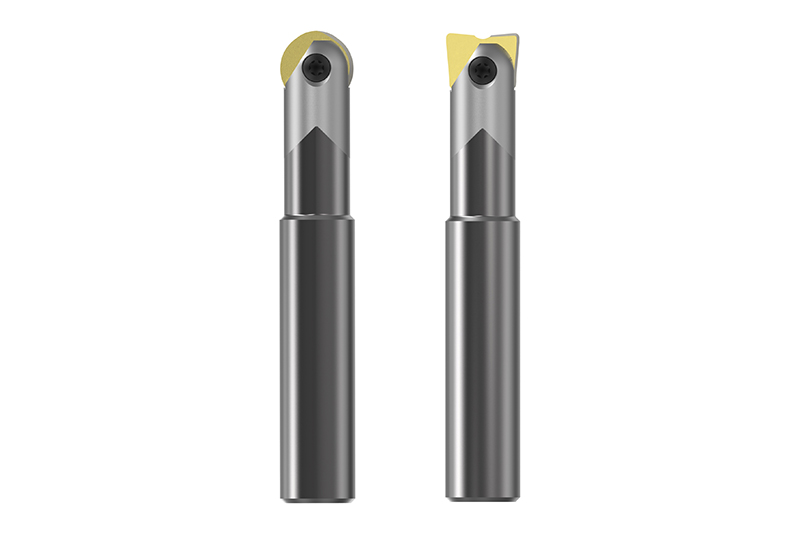
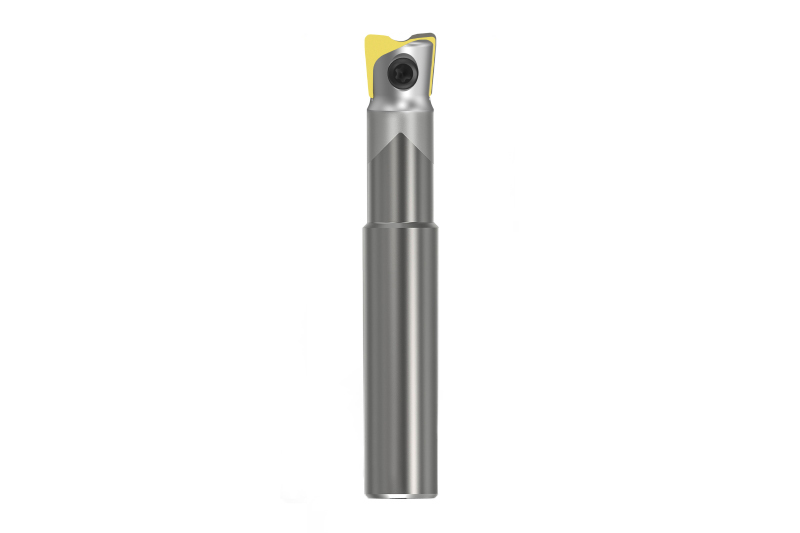
A operação de acabamento remove a permissão restante para alcançar a forma final. Após o semi-acabamento, isto é 0,05-0,1 mm para materiais endurecidos e 0,1-0,3 mm para materiais macios. As fresas esféricas e/ou com raio de canto são a ferramenta de escolha, dependendo dos contornos finais da peça a ser trabalhada.
Residual material finishing
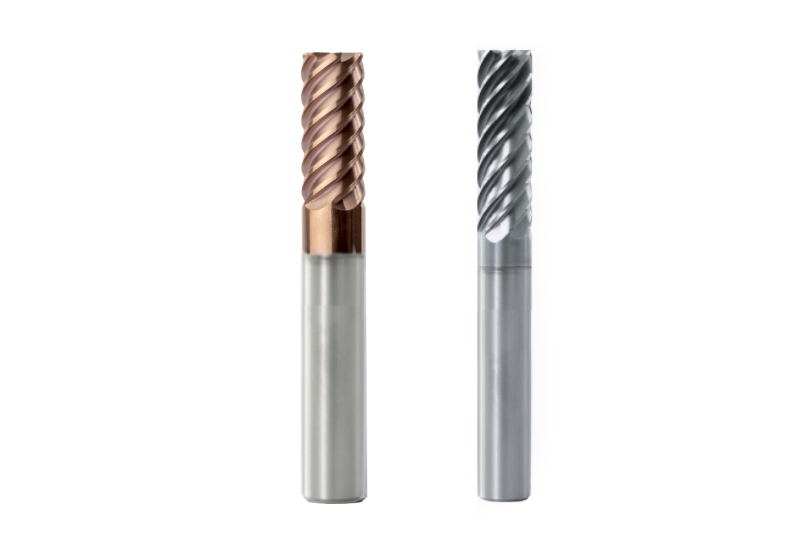
The increasingly complex properties of the shapes to be produced require milling of the residual material after finishing, mainly in the corners. Solid carbide ball cutters are usually used for this.