Internal Combustion Engine
Focus components from the internal combustion engine sector
- Cylinder head
-
Cylinder head
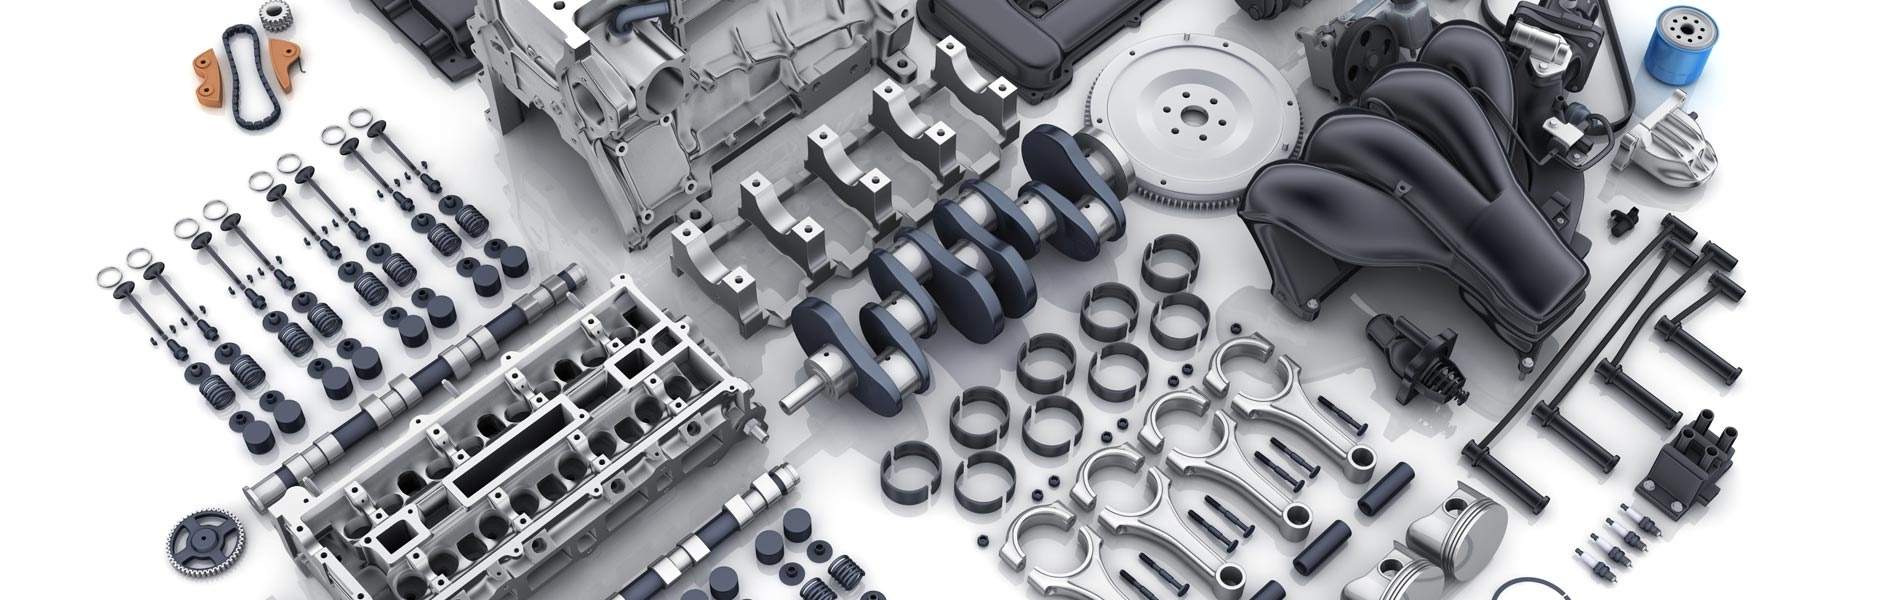
In the passenger car sector, the cylinder head is usually cast from aluminum alloys, whereby the structure and the features to be machined differ slightly depending on the engine fuel. It is mounted on the cylinder crankcase and is primarily responsible for the fuel and fresh air supply. Due to its extremely high quality and tolerance requirements, the cylinder head is the most demanding component to be machined in engine production. Precise valve control in the valve train and minimal friction losses in the camshaft bearings reduce fuel consumption and thus emissions even before the combustion process begins.
Machining highlights:
- Valve train
- Injector bore
- Camshaft bearing bore
- Face milling
- Spark plug bore
- Cylinder crankcase
-
Cylinder crankcase
The cylinder crankcase, also known as the engine block, is the central element of every combustion engine. Depending on the vehicle model and engine size, there are a variety of different designs and sizes, from 2-cylinder in-line engines to 12-cylinder V-arrangements. Due to the weight advantage, aluminum alloys are predominantly used in the automotive sector today. However, this forces car manufacturers to use cast liners or wear-resistant coatings, especially for cylinder bores, in order to guarantee a high mileage. During machining, tool manufacturers are increasingly encountering mixed machining (cast aluminum) or extremely abrasive coatings. The increased combustion pressures of modern engines also increase the mechanical and thermal load requirements, which, among other things, leads to increasing quality requirements for the features to be machined.
Highlight machining:
- Cylinder bore
- Crankshaft bearing bore
- Honing pass
- Connecting rod
-
Connecting rod
High-strength steel materials such as 70MnVS4 or C70 are generally used for the connecting rods, which are subject to alternating heavy loads, in order to convert the linear movement of the pistons into a rotational movement of the crankshaft. In order to reduce the moving mass during engine operation, the components are reduced to a minimum weight. Over the years, this has resulted in an enormous number of variants with, for example, parallel, trapezoidal or stepped shapes, which entail a wide variety of tapping situations, especially when machining the small connecting rod eye. Due to the enormous production quantities, manufacturers are particularly focused on cost-effectiveness in series production.
Highlight machining:
- Large eye
- Small eye
- Screw hole drilling
- Turbocharger
-
Turbocharger
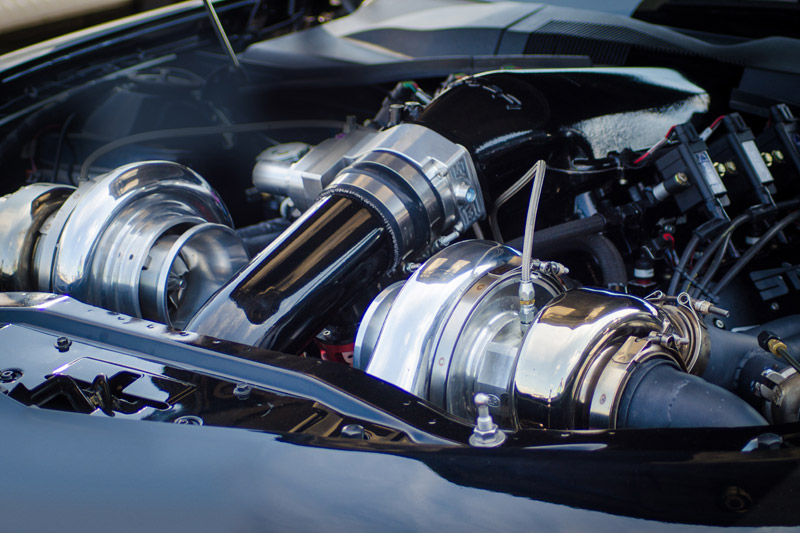
To increase the efficiency and performance of modern combustion engines, exhaust gas turbochargers are increasingly being used today. The compressed air supply via the turbocharger increases the efficiency of engines and at the same time reduces emissions. At speeds of up to 300,0001 rpm, it is imperative that quality requirements are met, especially with regard to coaxiality and roundness. Extremely abrasive high-alloy materials, especially on the exhaust gas side (turbine side), demand maximum wear resistance from the cutting tools. If the tool life quantities for the various machining operations are increased by even just a few components, this has an enormous cost benefit for the manufacturer.
Highlight machining:
- Turbocharger housing connection surface
- Turbine housing
- Control pin bore
- Turbine inner contour & V-band
- Connection machining
- Rocker/toggle lever
-
Bilanciere/braccio mobile
Importante per le prestazioni e l’efficienza dei motori a combustione è il controllo ad alta precisione delle valvole di aspirazione e di scarico. Nel settore automobilistico, di solito vengono controllate quattro valvole per cilindro: due per l’aspirazione dell’aria fresca o della miscela aria-carburante e le altre due per lo scarico dei gas di combustione. A seconda del modello di motore, per i sistemi di azionamento delle valvole OHV e SOHC vengono utilizzati diversi bilancieri o bracci mobili (su rullo) per ridurre al minimo l’attrito e la relativa usura delle parti in movimento. Inoltre, tramite le rondelle di regolazione integrate, è possibile impostare e ripristinare il gioco delle valvole per garantire un processo di combustione ottimale e prevenire possibili danni al motore.
Lavorazioni principali:
- Foro cuscinetto
- Foro di accoppiamento
- Rail
-
Rail
Conosciuto come common rail nei motori diesel, ora il carburante viene iniettato nella camera di combustione anche di un’auto a benzina su due, attraverso efficienti sistemi di iniezione diretta. La miscela aria-carburante si forma dapprima nella camera di combustione. Ciò garantisce motori a benzina più potenti con consumi ridotti e minori emissioni di scarico. I crescenti requisiti di pressione fino a 2.500 bar sono decisivi per l’utilizzo di materiali che presentano difficoltà di lavorazione moderata e complessa come l’acciaio fuso o l’acciaio inossidabile.
Lavorazioni principali:
- Foro centrale del rail
- Foro dell’iniettore / trasferimento iniettore
- Collegamento ad alta pressione
- Lavorazione delle estremità
- Albero a gomiti
-
Albero a gomiti
La forma base dell’albero a gomiti è determinata principalmente dal numero di cilindri e dalla variante del motore. Tuttavia, gli alberi, per lo più in acciaio forgiato, devono diventare sempre più leggeri per ridurre le emissioni. Ciò significa che sono necessarie ulteriori lavorazioni nella produzione di componenti già complessi. Inoltre, a causa delle crescenti pressioni di combustione dei motori moderni, l’albero a gomiti è costantemente esposto a maggiori sollecitazioni di flessione e torsione, con conseguenti requisiti di qualità superiori.
Lavorazioni principali:
- Foro centrale di alleggerimento
- Foro del canale dell’olio
- Lavorazione delle estremità
- Face and sealing surfaces
-
Face and sealing surfaces
Machining flat sealing surfaces in the combustion engine requires the utmost in dimensional accuracy, flatness and surface quality – often in dry conditions. MAPAL supplies high-performance face milling tools with maximum number of teeth, sturdy tool design and optimal chip removal. Whether roughing or finishing: The solutions are designed for cost-effectiveness, process reliability and component quality.
Case studies from the internal combustion engine sector
-
26.08.2025
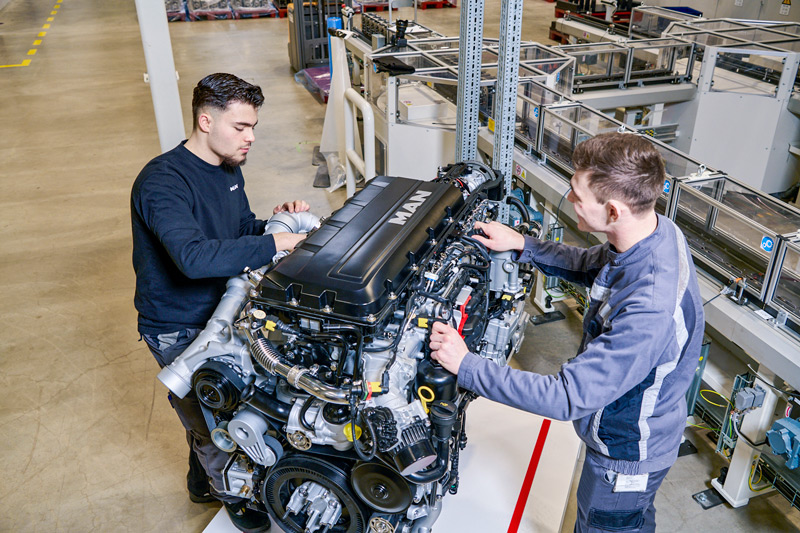
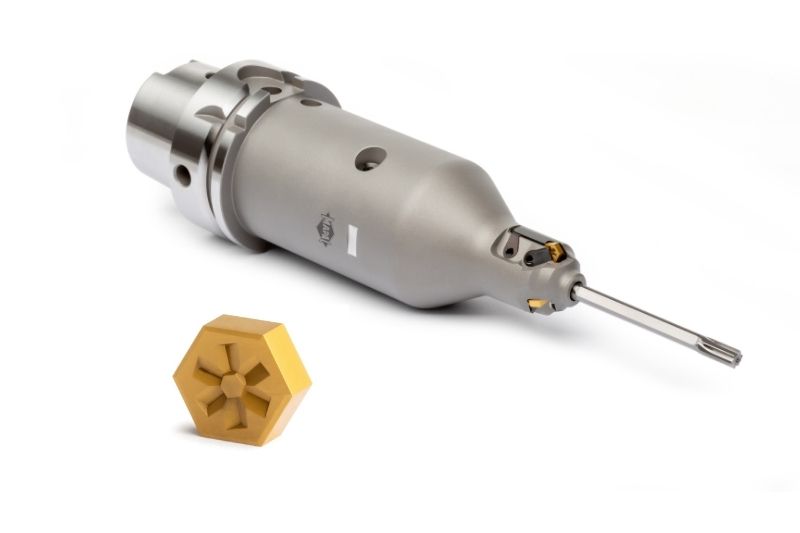
MAN uses MAPAL fine boring tools for machining cylinder heads
At MAN engines, fine boring tools from MAPAL are used to machine the valve guide and valve seat counterbores of cylinder heads."
#Alesatura #Technology #Industries #Automotive #Reaming&FineBoring
-
22.07.2025
Crankshaft and valve seat machining: MAPAL sets standards
Optimised machining of crankshafts and valve seats: MAPAL offers innovative tool solutions for modern combustion and hybrid engines.
-
16.01.2025
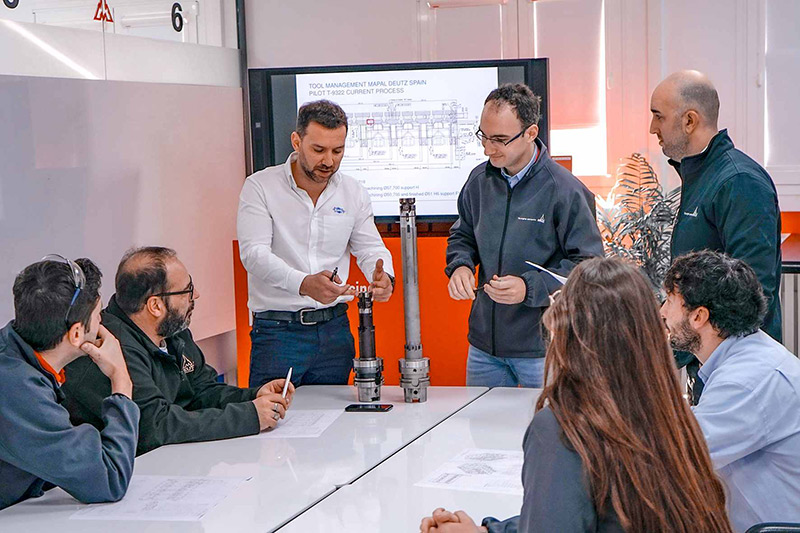
Tool management from MAPAL completed for DEUTZ in record time
MAPAL completed the entire engineering including tool design, cycle time study and cost calculation for the engine manufacturer Deutz in the Spanish plant in Zafra within a very short time.
#Prodotti #Industries #CaseStudies #Technology #Services #Automotive #Reaming&FineBoring
-
23.03.2023
The production must go on
Digital tool management with more than 750 tools from MAPAL ensures smooth large-scale production at Schabmüller Automobiltechnik.
-
30.06.2022
Even more cost-effective turbochargers
How the complete machining of turbochargers becomes even more productive with indexable insert milling cutters from the NeoMill range.
-
09.12.2019
Highly precise machining of truck engine cylinder bores
High-precision MAPAL actuating tools and a special setting fixture ensure precise and economical production at Mercedes-Benz in Mannheim.