Energy supply housing
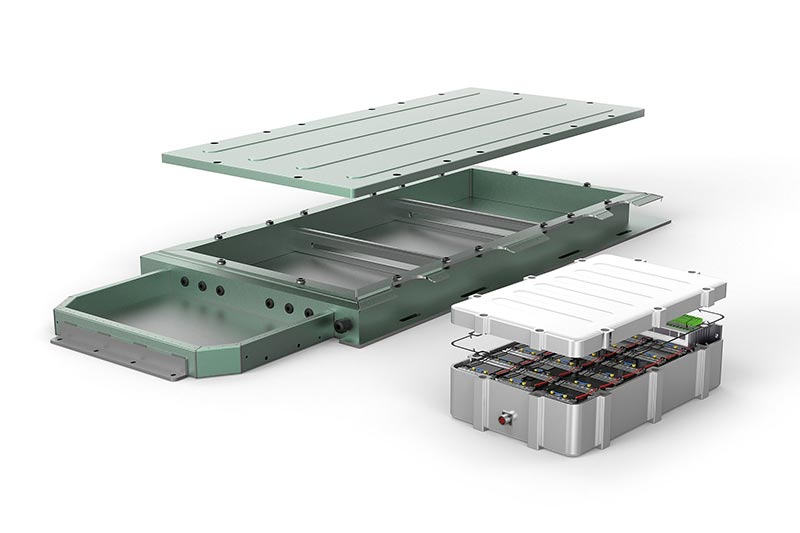
Se utilizan distintas carcasas para proteger los componentes electrónicos, como por ejemplo el sistema de batería o la electrónica de potencia, frente a influencias ambientales externas y para la fijación de componentes en el interior, a fin de garantizar su funcionamiento óptimo durante el accionamiento del vehículo. Los requisitos de la carcasa dependen del sistema electrónico y del concepto de propulsión. Actualmente, se utilizan diferentes materiales y procesos de fabricación.
CARACTERÍSTICAS
- Componentes inestables de paredes finas (propensos a vibraciones)
- Estructura de cubeta fundida o de bastidor con perfil hueco
- Parcialmente en aluminio con bajo contenido de silicio
- Grandes dimensiones (2 x 3 m)
- Principalmente operaciones de taladrado y fresado, y roscas
- Requisitos de precisión y superficie para pasacables y conexiones de refrigeración


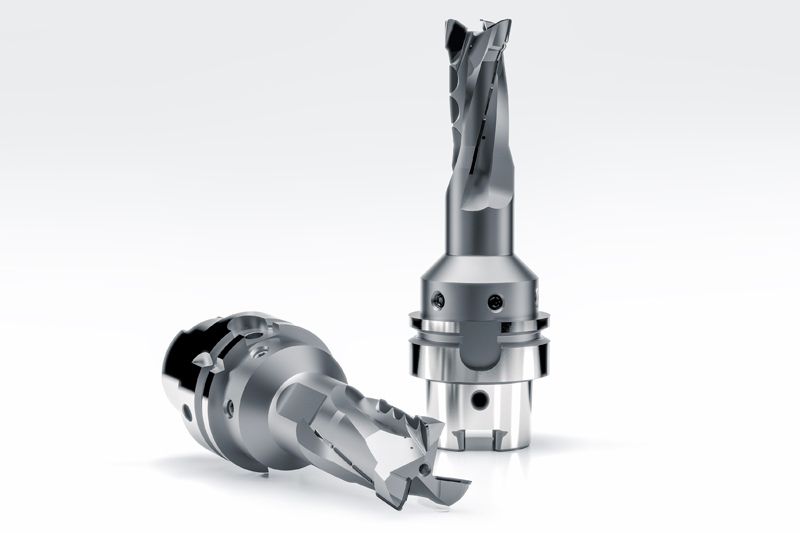
Tool overview
-
 1 / 9
Standard programme for the machining of aluminium structural parts
- Highly positive cutting edge geometry
- Reduced cutting forces
- Low vibration cut
-
2 / 9
OptiMill-SPM-Rough
- Low vibration roughing with deep cutting depth
-
3 / 9
OptiMill-SPM
- Ideal for making openings or pockets
- Solid carbide design or with brazed PCD cutting edges
-
4 / 9
OptiMill-SPM-Finish
- Finishing of great depths in one go
- Strong performance with high wraps
-
5 / 9
Tritan-Drill-Alu
- Creation of core holes
- Three cutting edges for the highest feed rates
- Highest positioning accuracy through self-centring cross cutting edge
-
6 / 9
MEGA-Drill-Alu
- Solid carbide drill
- Drilling with lower cycle time
- Focus on chip formation
- Effective drilling processes with a larger number of equal diameters
-
7 / 9
FaceMill-Diamond-ES
- PCD face milling cutter
- Roughing and finishing of face surface
- Machining face surfaces with different stock removal using a single tool
- Roughing and finishing operations possible
-
8 / 9
OptiMill-Diamond-SPM
- PCD milling cutter
- Circular milling operations of various diameters and surfaces
- Less tool changes thanks to flexible tool deployment
-
9 / 9
OptiMill-Alu-HPC-Pocket
- Corner milling cutter
- Pocket milling of aluminium materials
- Optimum chip removal
- Optimum stability


-
1 / 5
Fresa PCD para requisitos de mecanizado especiales
-
2 / 5
Fresa PCD con cuchillas dispuestas de forma alterna
- Bajas fuerzas de corte en toda la profundidad de mecanizado
-
3 / 5
Fresa PCD con forma espiral
- Acabado de estructuras de paredes finas
-
4 / 5
Fresas helicoidales de PCD
- Recorte con gran profundidad de corte
-
5 / 5
Fresa plana de PCD
- Fresado plano con profundidades de corte de hasta 10 mm
- Creación de perfiles superficiales definidos para superficies de contacto y apoyo


Case studies from the energy supply sector
-
03.11.2022
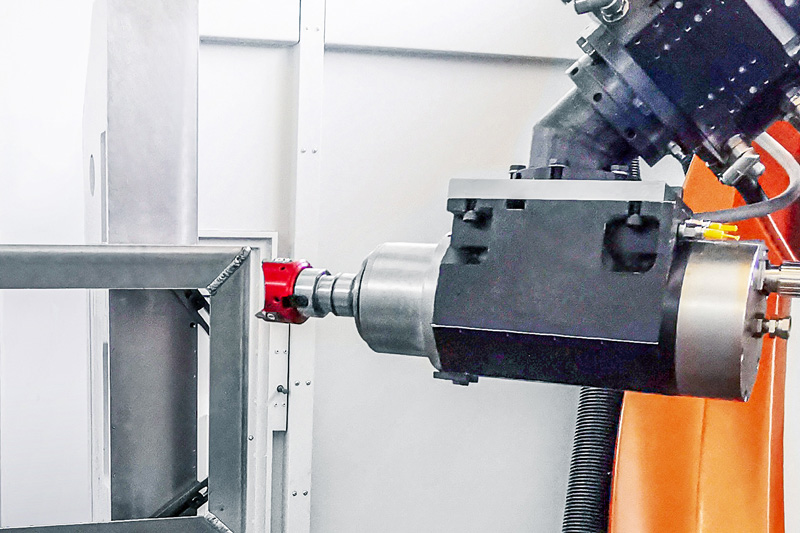
Efficient deburring with robots
The FlyCutter from MAPAL is ideally suited for deburring battery trays. Robot manufacturer KADIA is enthusiastic about the PCD-tipped milling tool.
-
12.07.2023
Milling instead of drilling
Why milling instead of drilling can be a sensible alternative? MAPAL shows how higher process reliability and shorter machining times can be achieved.