钛合金加工的新产品
钛合金的低导热性及其高抗拉强度导致刀具承受高热应力和机械应力。新的MAPAL钛合金系列加工刀具,具有复杂的散热和耐热涂层。因此,可以实现相对较高的切削参数,同时具有较高的工艺可靠性。与市场上的传统解决方案相比,可延长25%至35%的刀具寿命。
Indexable insert milling cutters with a bite
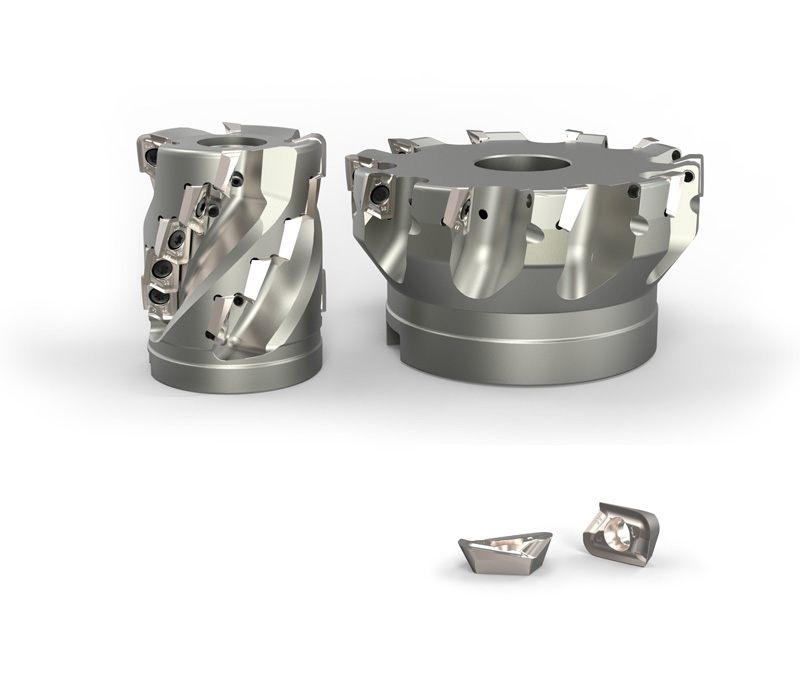
NeoMill-Titan is the name for a whole family of milling cutters with indexable inserts for titanium machining: Shell end face milling cutters in slip-on and shank versions, as well as shoulder milling cutters are part of the standard portfolio. The topography of the indexable insert has been redesigned from scratch for optimum chip formation and removal. The indexable inserts each have two cutting edges and are available with corner radii from 0.8 mm to 4 mm.
An equally new cutting material concept minimises wear and the formation of built-up on the cutting edges. There are two different substrates to choose from. In addition to a wear-resistant universal grade, a temperature-resistant high-performance grade has been developed with which cutting speeds of up to 70 m/min can be achieved.
The tool body has also been newly developed for the high-tech inserts. With ideally adapted shapes, the chip flutes transport the chips out of the shear zone. The unequal spacing of the inserts provides additional stability and smooth running.
Variably designed coolant outlets make the regulation of the flow rate of each individual insert possible.
粗精加工多功能铣刀
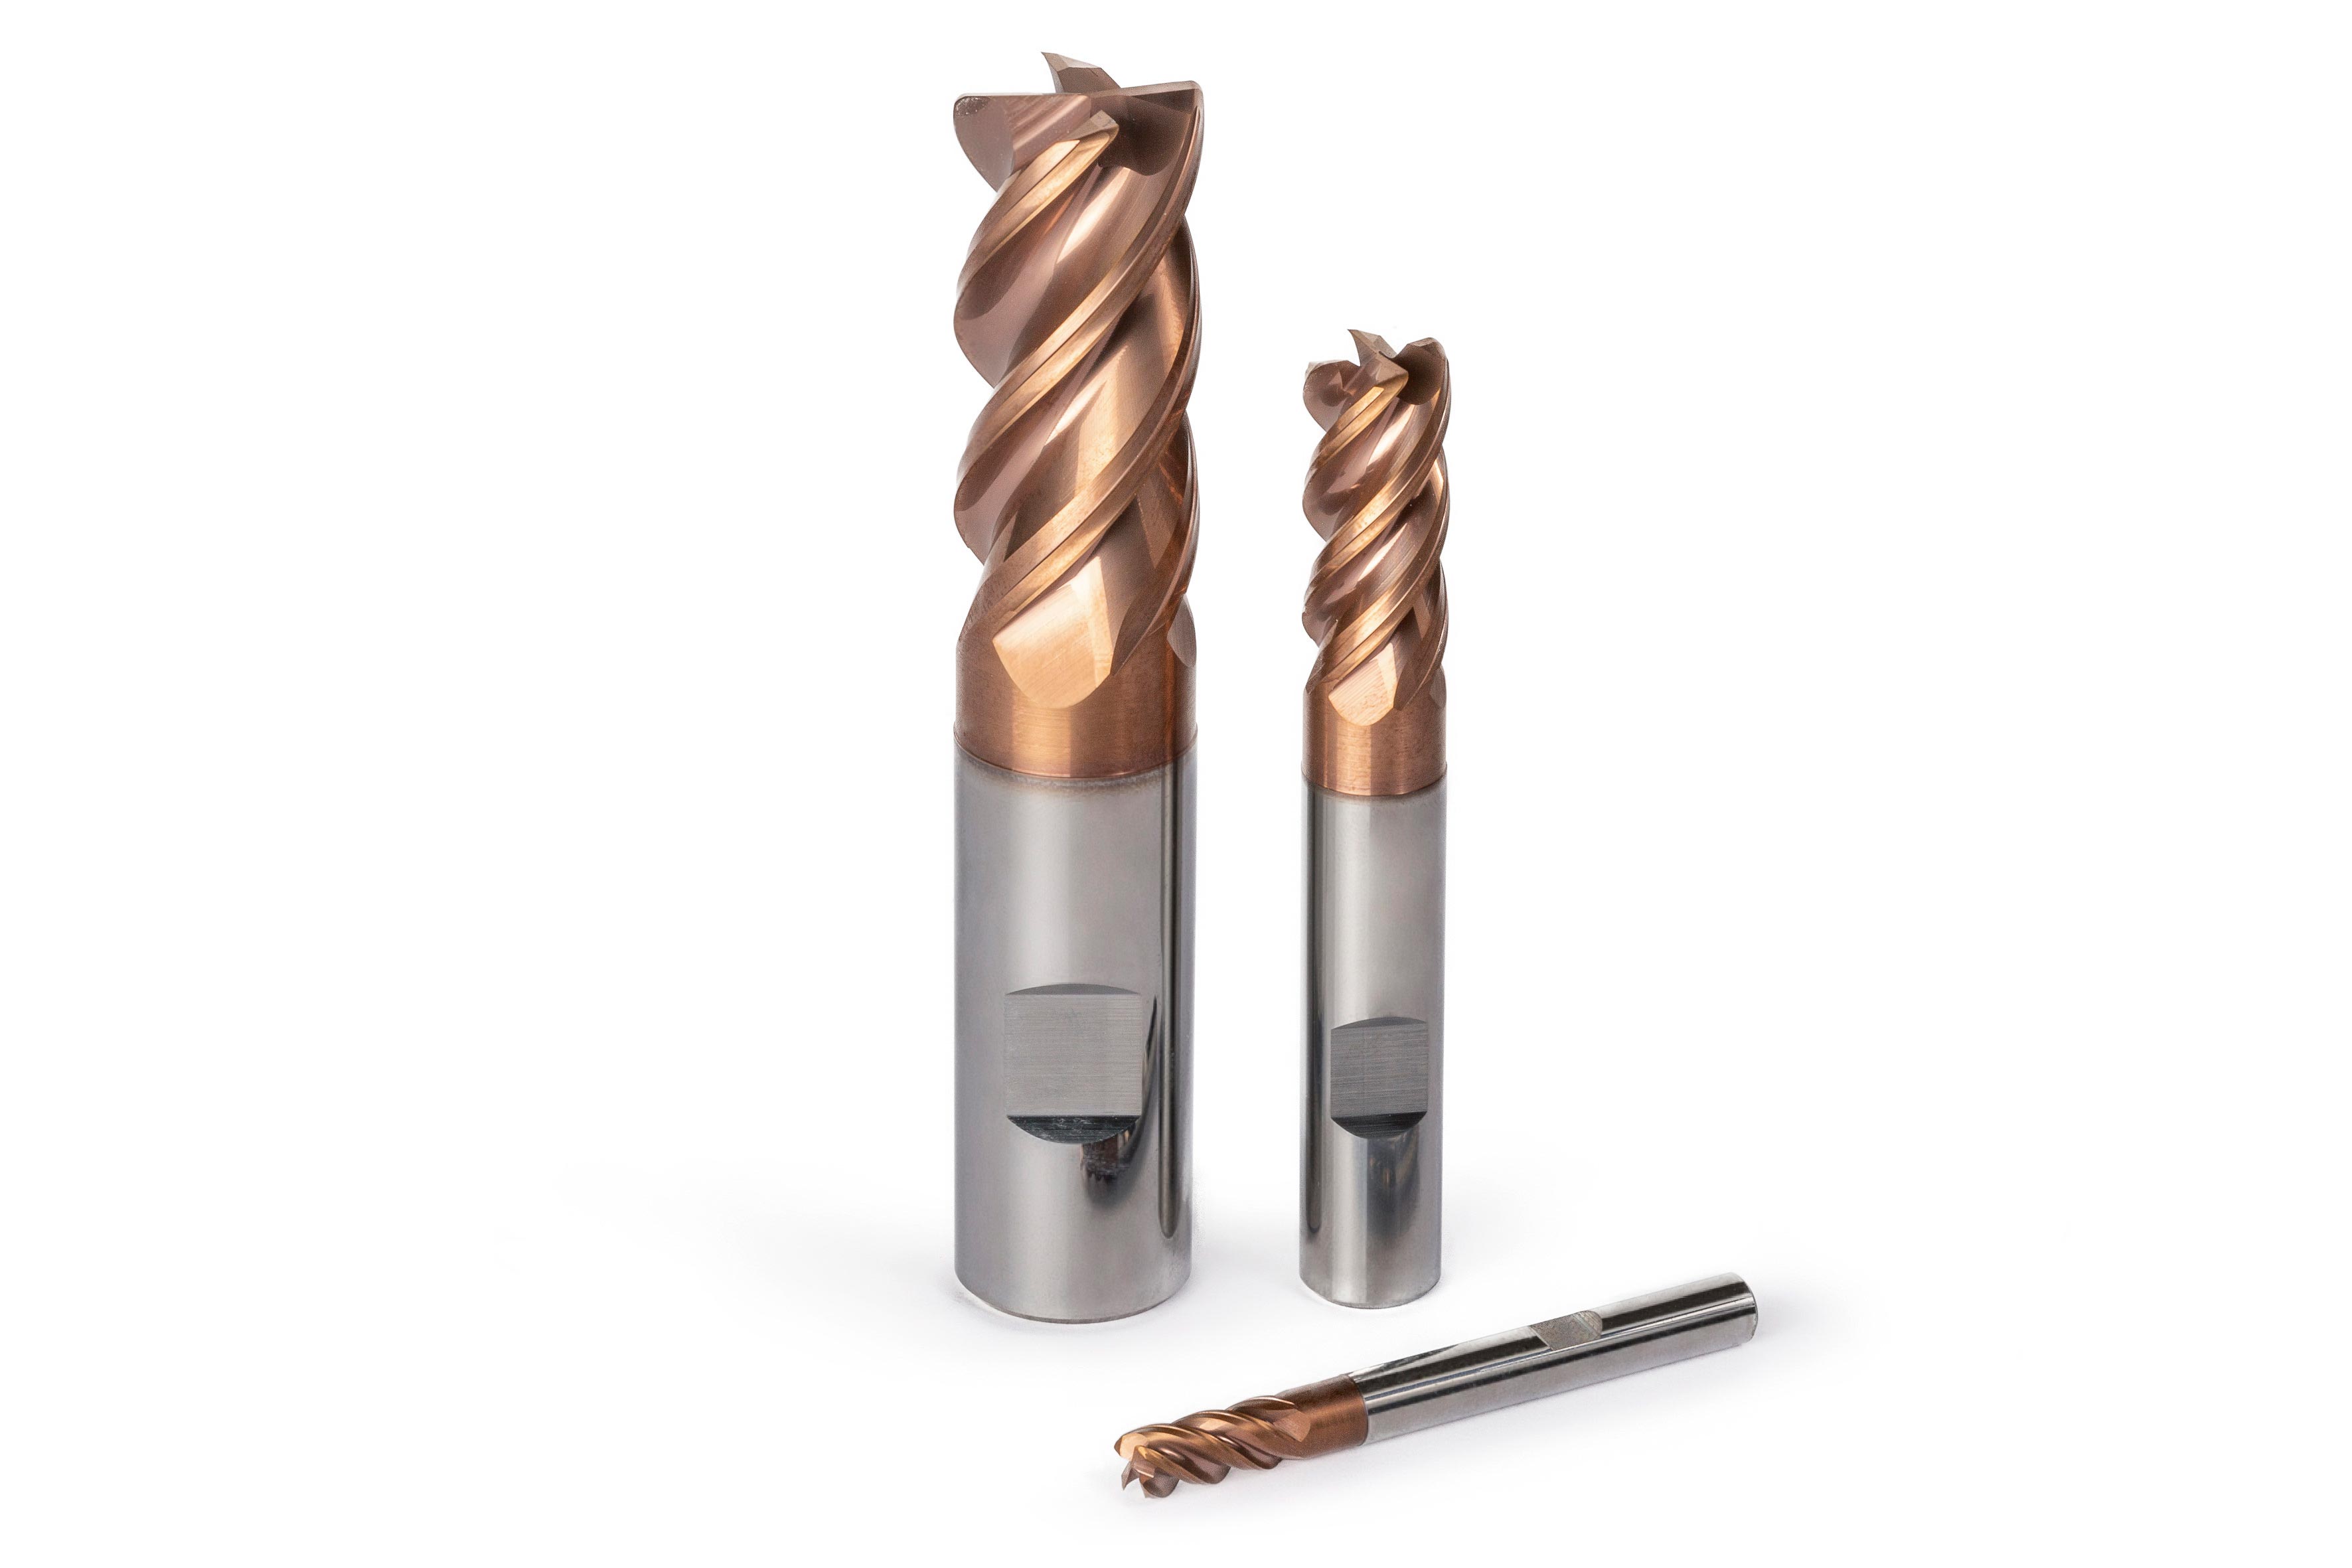
四齿的 OptiMill-Titan-HPC 是一款多功能方肩铣刀。整体硬质合金立铣刀既可以进行粗加工,也可以用于精加工。
通过特殊的刃口处理可获得最佳的表面质量,并允许精加工至 1,5xD 的工作深度。这种铣刀的芯厚从切削刃到刀柄增加,使其具有更高的稳定性。切削刃口不等分及渐变螺旋槽,以实现平稳运行。含硅涂层非常耐热,可抵抗粘附趋势,并与抛光的排屑槽一起确保最佳的切屑排出。OptiMill-Titan-HPC 的直径范围为 6 至 25 mm。可提供特殊尺寸。
Kosteneffizient und produktiv
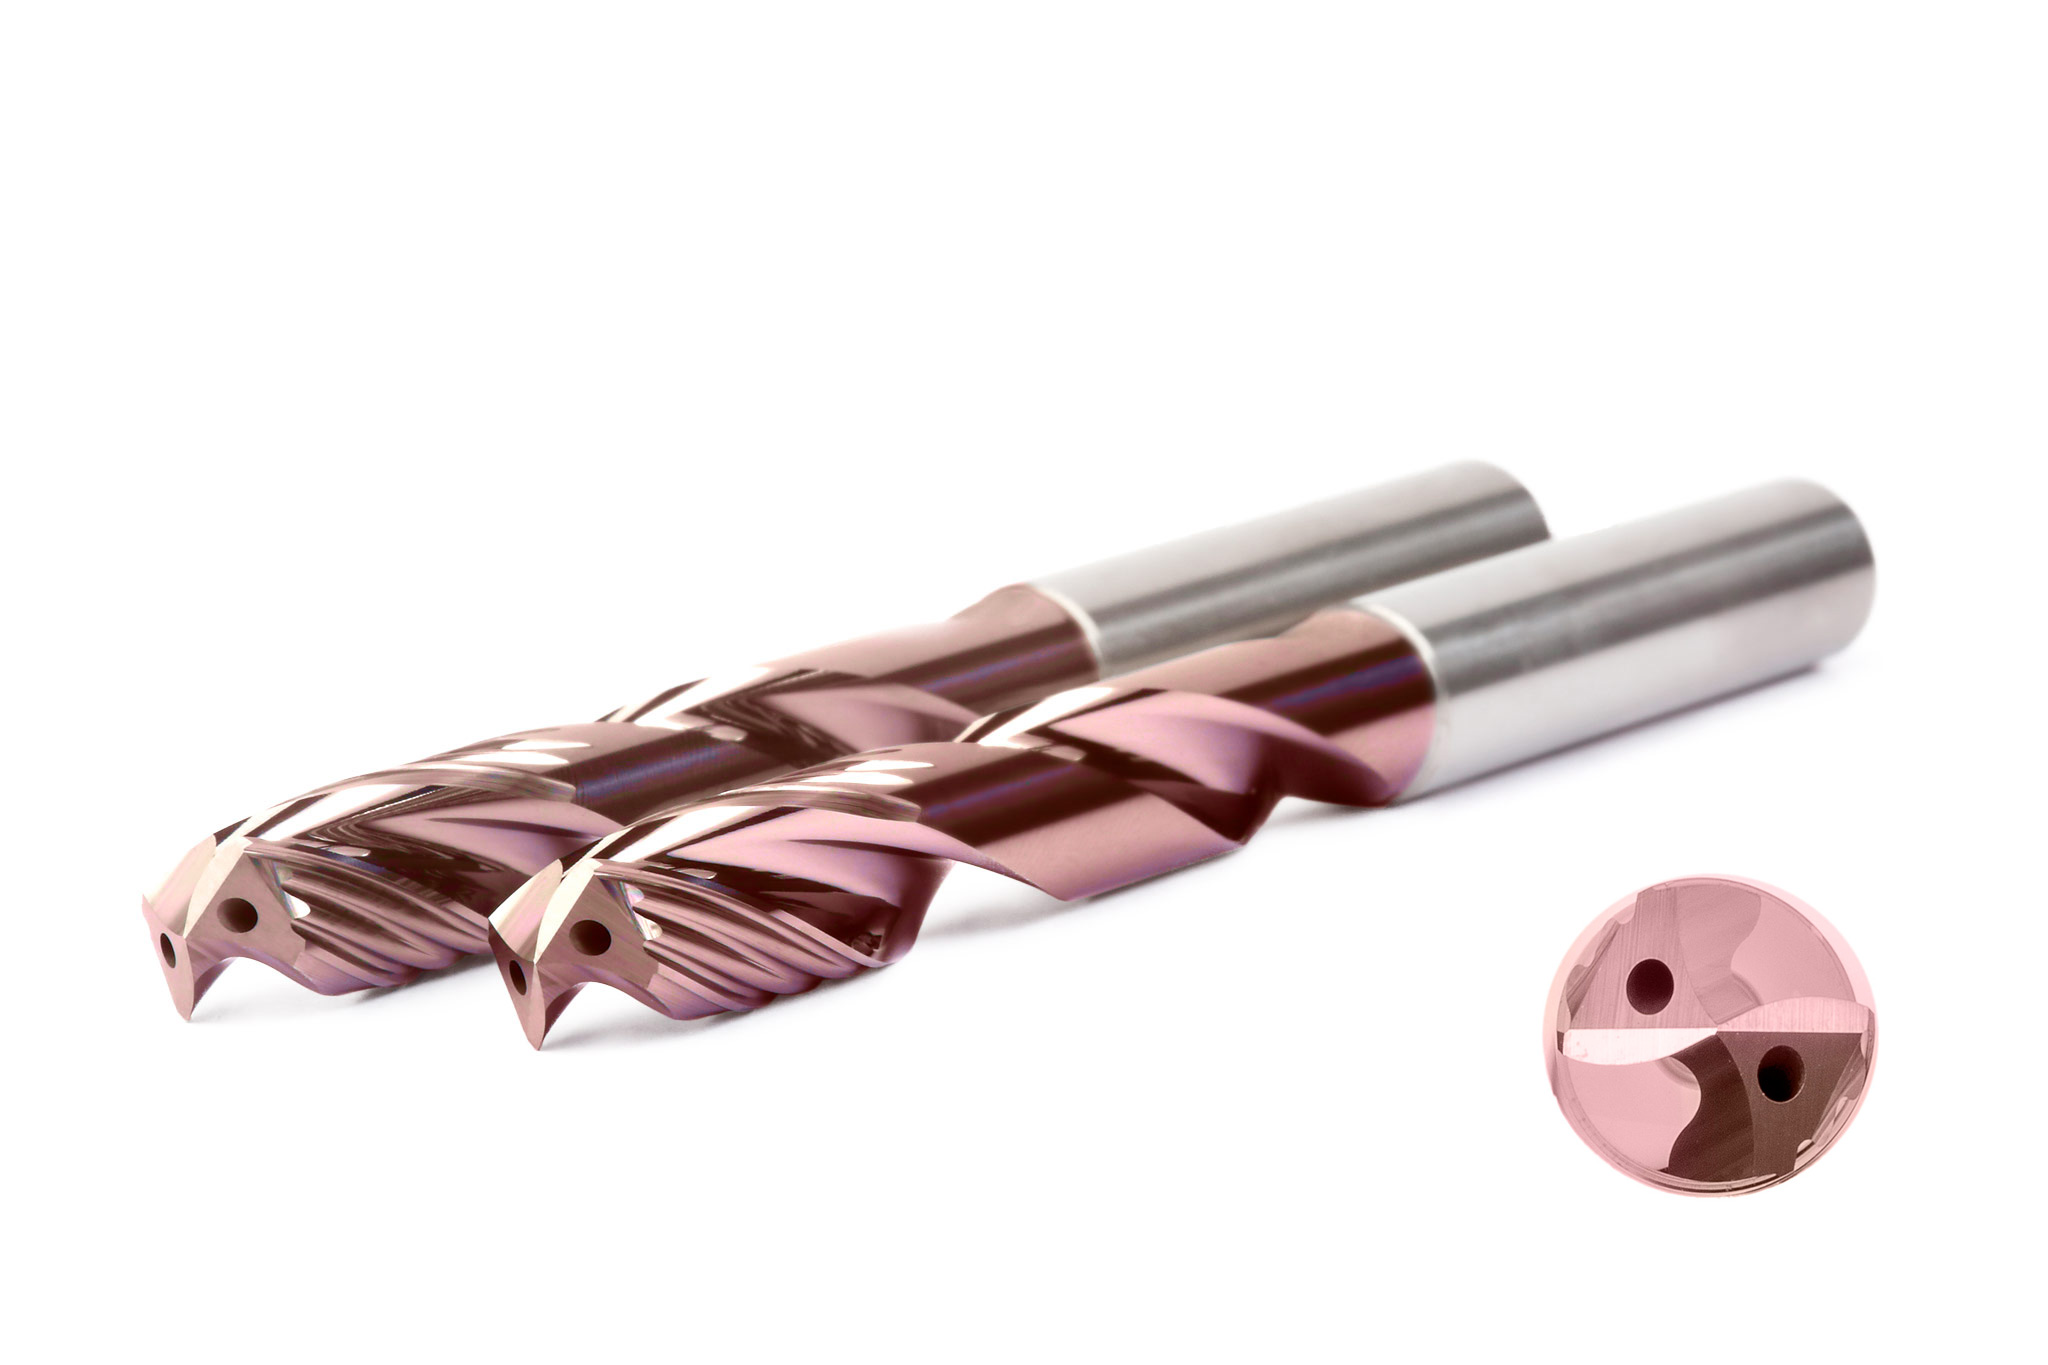
Der Hochgeschwindigkeitsbohrer MEGA-Speed-Drill-Titan zeichnet sich durch Kosteneffizienz bei höchster Produktivität aus. Der zweischneidige VHM-Bohrer ist mit vier Führungsfasen für optimale Rundheit ausgestattet. Um den maximalen Kühlmittelfluss an die Hauptschneide zu bringen, wird das Kühlmittel an der Mantelfläche entlang nach hinten geleitet. Damit erfahren die Führungsfasen die maximale Kühlung und führen die entstehende Hitze gut ab. Ein neues Design der Spannut erzeugt zudem kleine Späne. Die konvexe Hauptschneide sorgt für hohe Stabilität und Standzeit. Der Bohrer ist ab Durchmesser 3 bis 20 mm in der Länge 5xD verfügbar.
Typische Bauteile für den Bohrer, der eine Schnittgeschwindigkeit von bis zu 40 m/min ermöglicht, sind Strukturbauteile in der Luftfahrtindustrie, zum Beispiel Winkel für die Wing Box oder das Landing Gear mit seinen vielen Bohrungen.