10.03.2022

Titanium Machining Takes Off

There are numerous applications waiting for new titanium machining tools from MAPAL. In medical technology, this workpiece material is used for implants because of its strength and compatibility with human tissue. Automotive manufacturers use it to create powerful sports cars. The blades of large gas turbines, made of titanium, absorb enormous forces. The aircraft industry is producing more and more highly stressed parts made of titanium. MAPAL is making drilling and milling of the ductile, high-strength workpiece material more productive, thereby reducing costs.
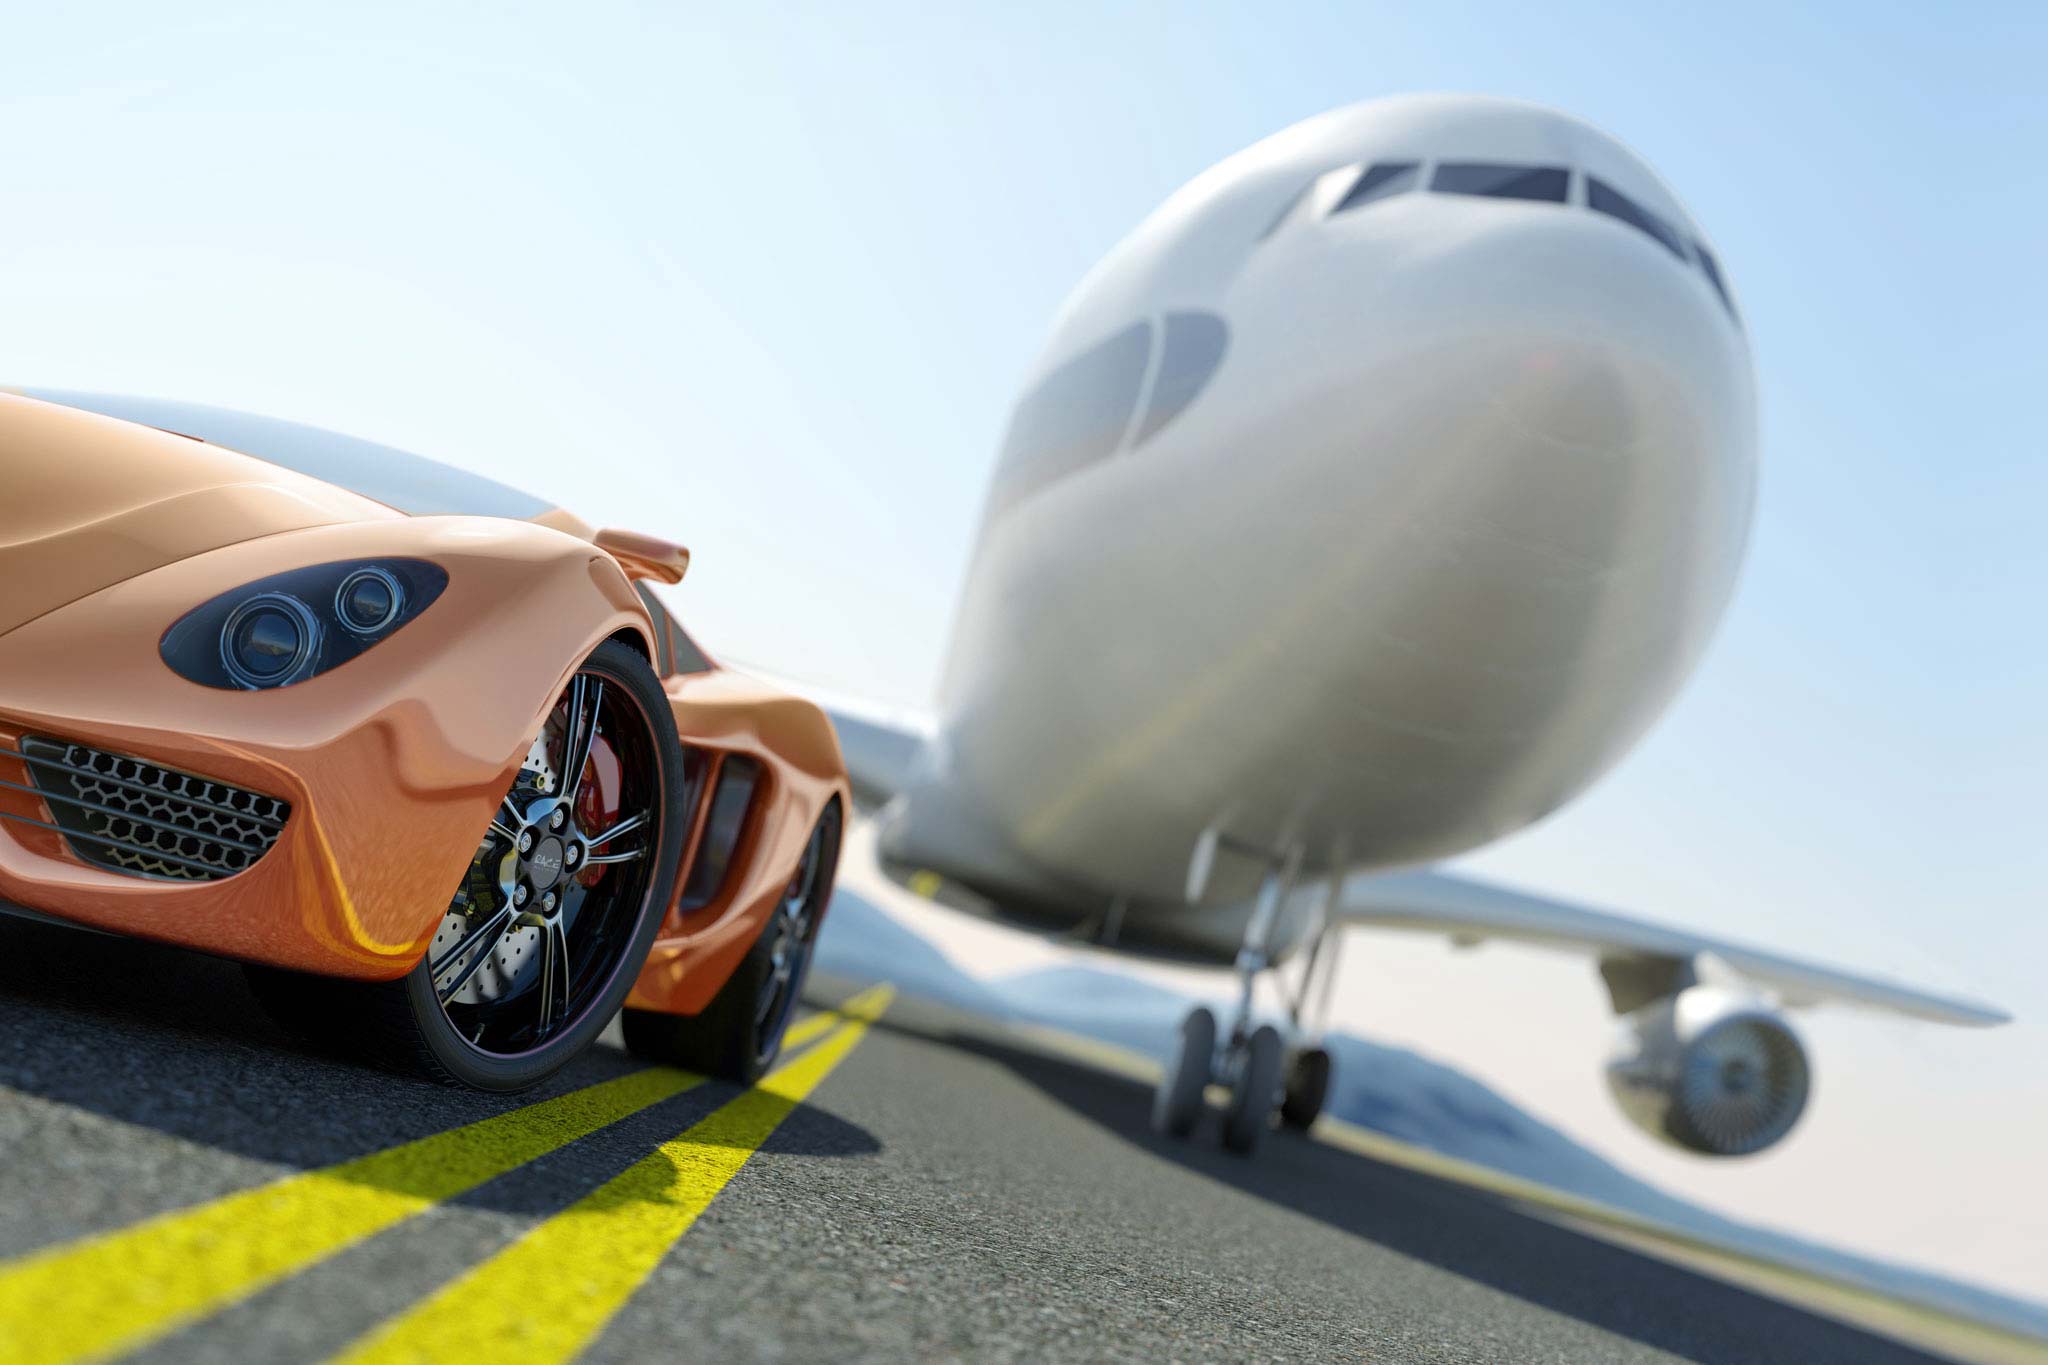
The picture shows an aeroplane and a sports car as representatives of important titanium application sectors.
  • The picture shows an aeroplane and a sports car as representatives of important titanium application sectors.
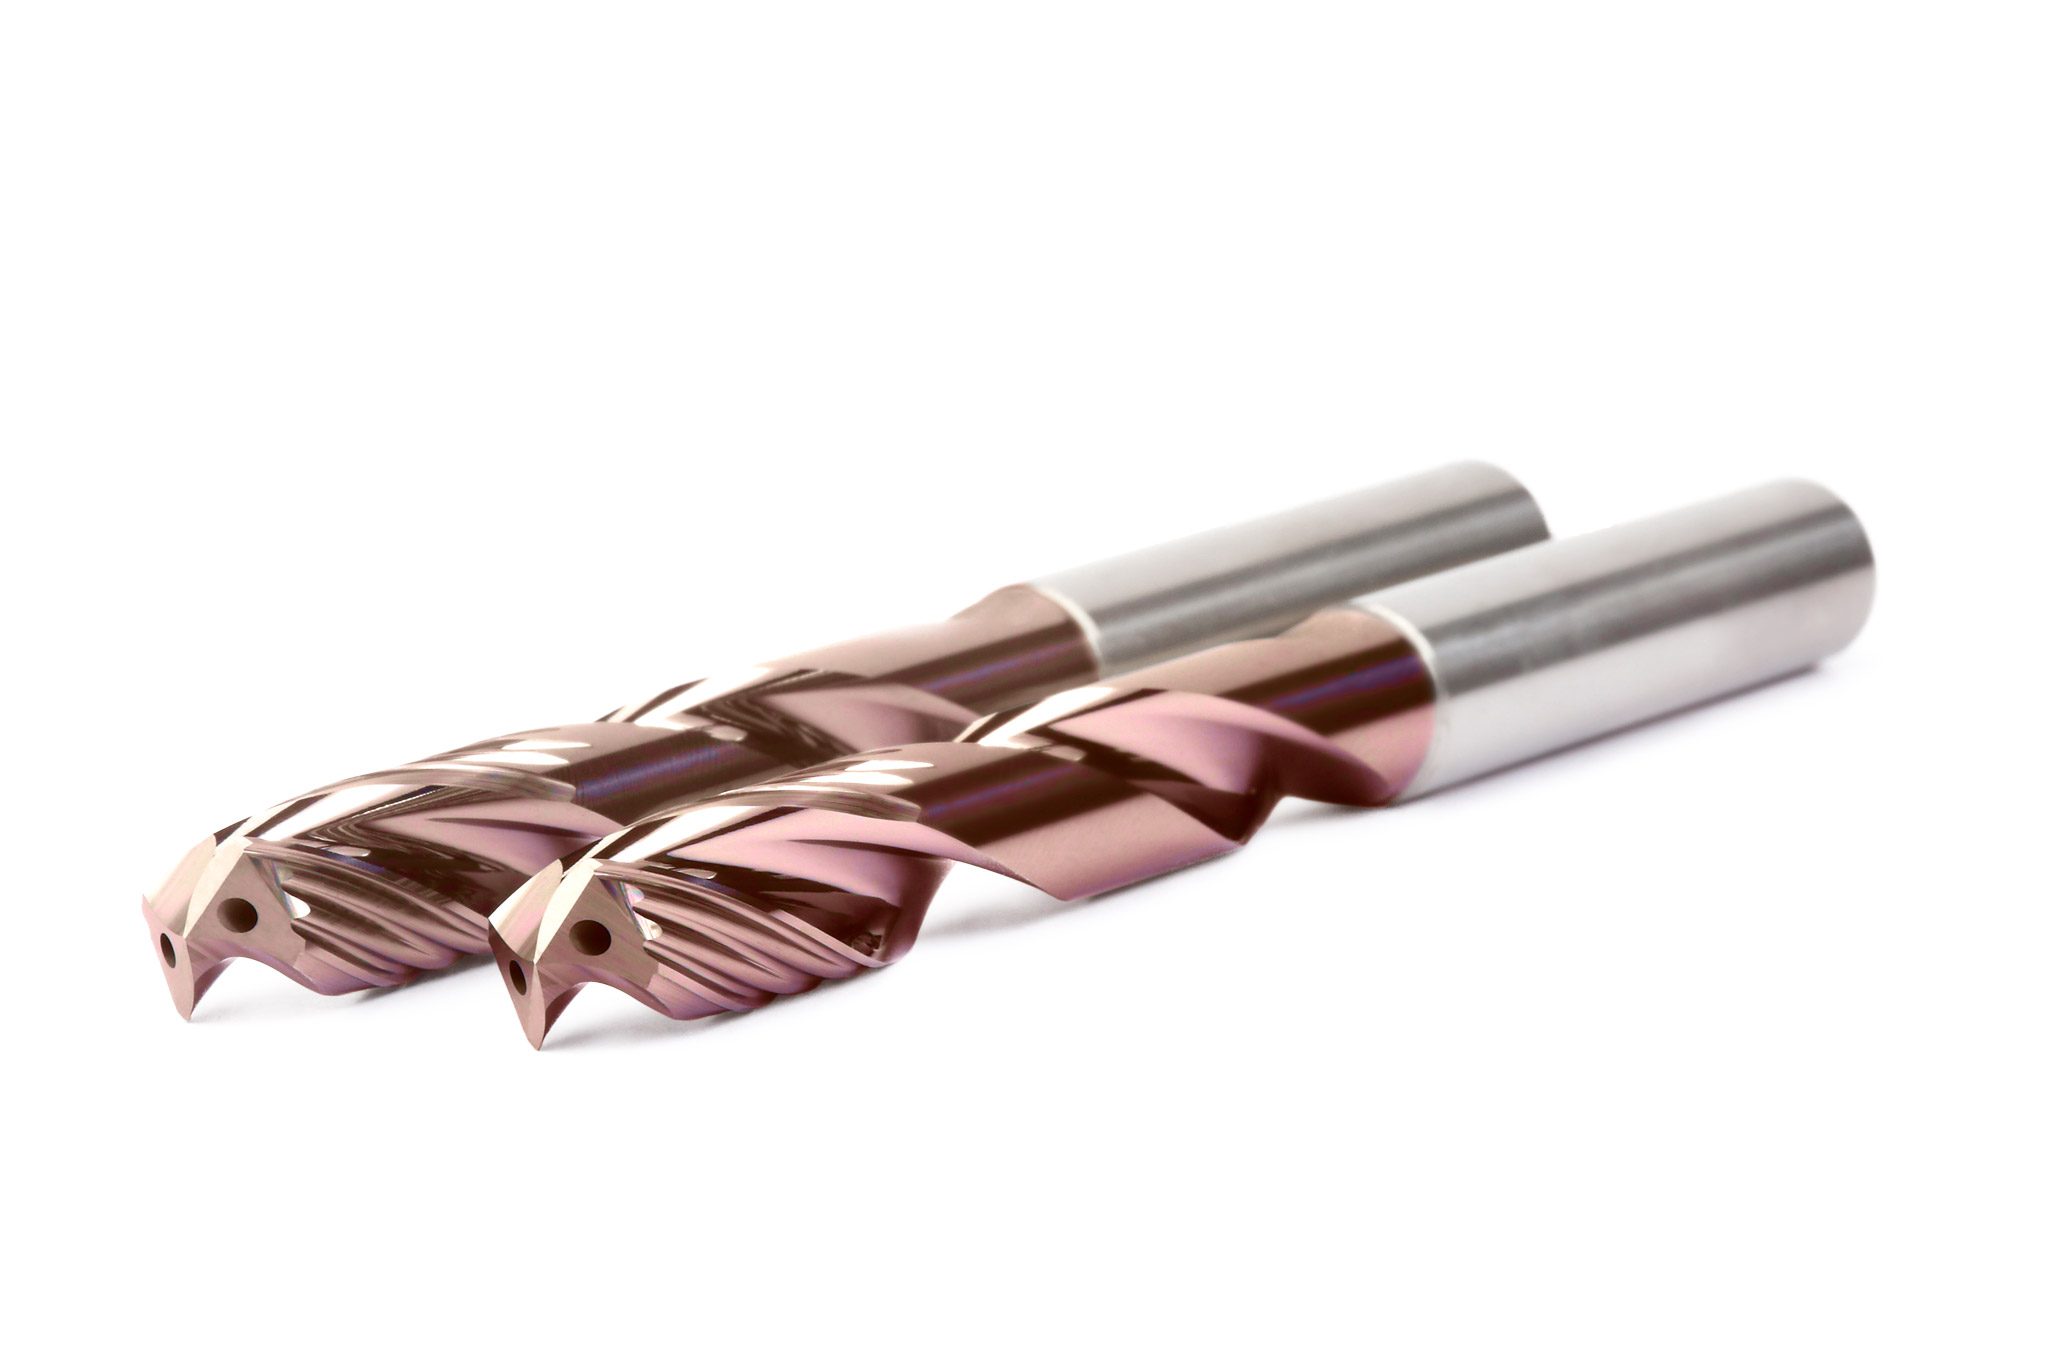
  • Two MEGA-Speed-Drill Titanium solid carbide drills from MAPAL for machining titanium
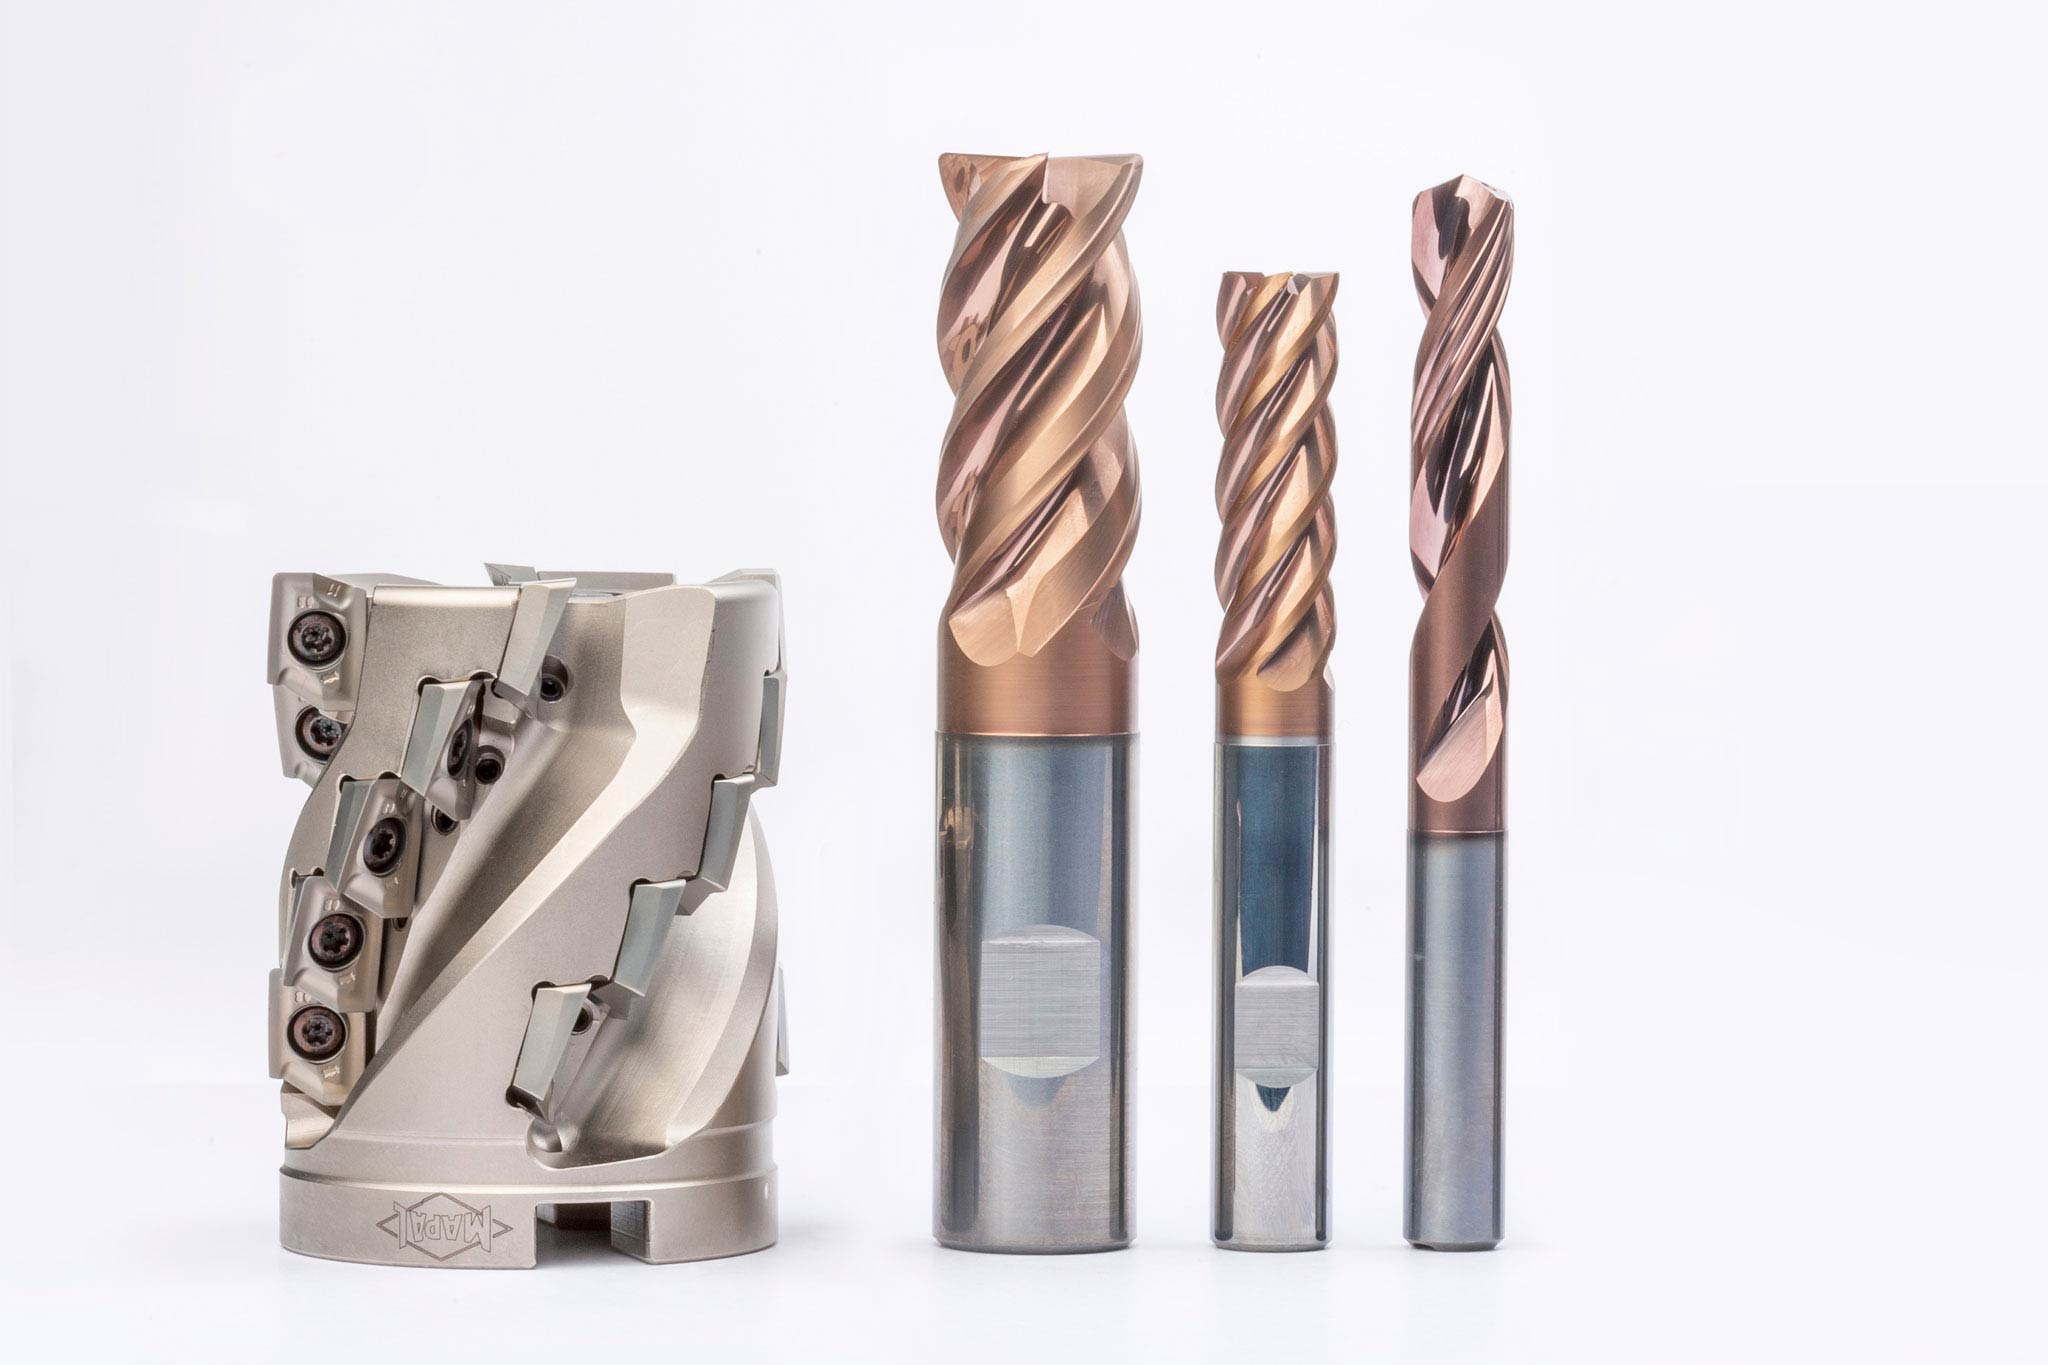
  • The solid carbide milling cutters OptiMill-Titan-HPC from MAPAL can be used both for roughing and for finish cuts in titanium.
  • A radial indexable insert milling cutter NeoMill-Titan from MAPAL.

MAPAL's three new titanium tools

MEGA-Speed-Drill-Titan: cost-efficient and productive
The focus in the development of the MEGA-Speed-Drill-Titan was on cost efficiency with maximum possible productivity. "Our goal was to develop a solid carbide drill that can run at a very high feed rate in titanium materials, resulting in very low cycle costs," explains Jens Ilg. In contrast to the assembly areas in aircraft construction, where no cooling lubricant or only a small amount of MQL can be used given the already finished assemblies, cooling lubricant can be used in parts production on machining centres to machine titanium efficiently.
Two MEGA-Speed-Drill Titanium solid carbide drills from MAPAL for machining titanium
Cost efficiency with the highest possible productivity – the new MEGA-Speed-Drill-Titan from MAPAL  ©MAPAL
MAPAL has equipped the drill with four guiding chamfers for optimum roundness. Convex cutting edges and an efficient coating allow for increases in tool life of up to 30 percent. To get the maximum coolant flow to the main cutter, the coolant channel is not open in the direction of the chip flute, but the coolant is guided along the outside surface to the rear. In this way, the guiding chamfers experience maximum cooling, dissipating the heat generated effectively. MAPAL uses a new design for the chip flute to produce the smallest possible chips and to discharge them through the flute. Typical parts that can be created with the drill, which achieves a cutting speed of up to 40 m/min, are structural parts in the aerospace industry, for example brackets for the wing box or the landing gear with its numerous bores.

OptiMill-Titan-HPC: versatile roughing and finishing
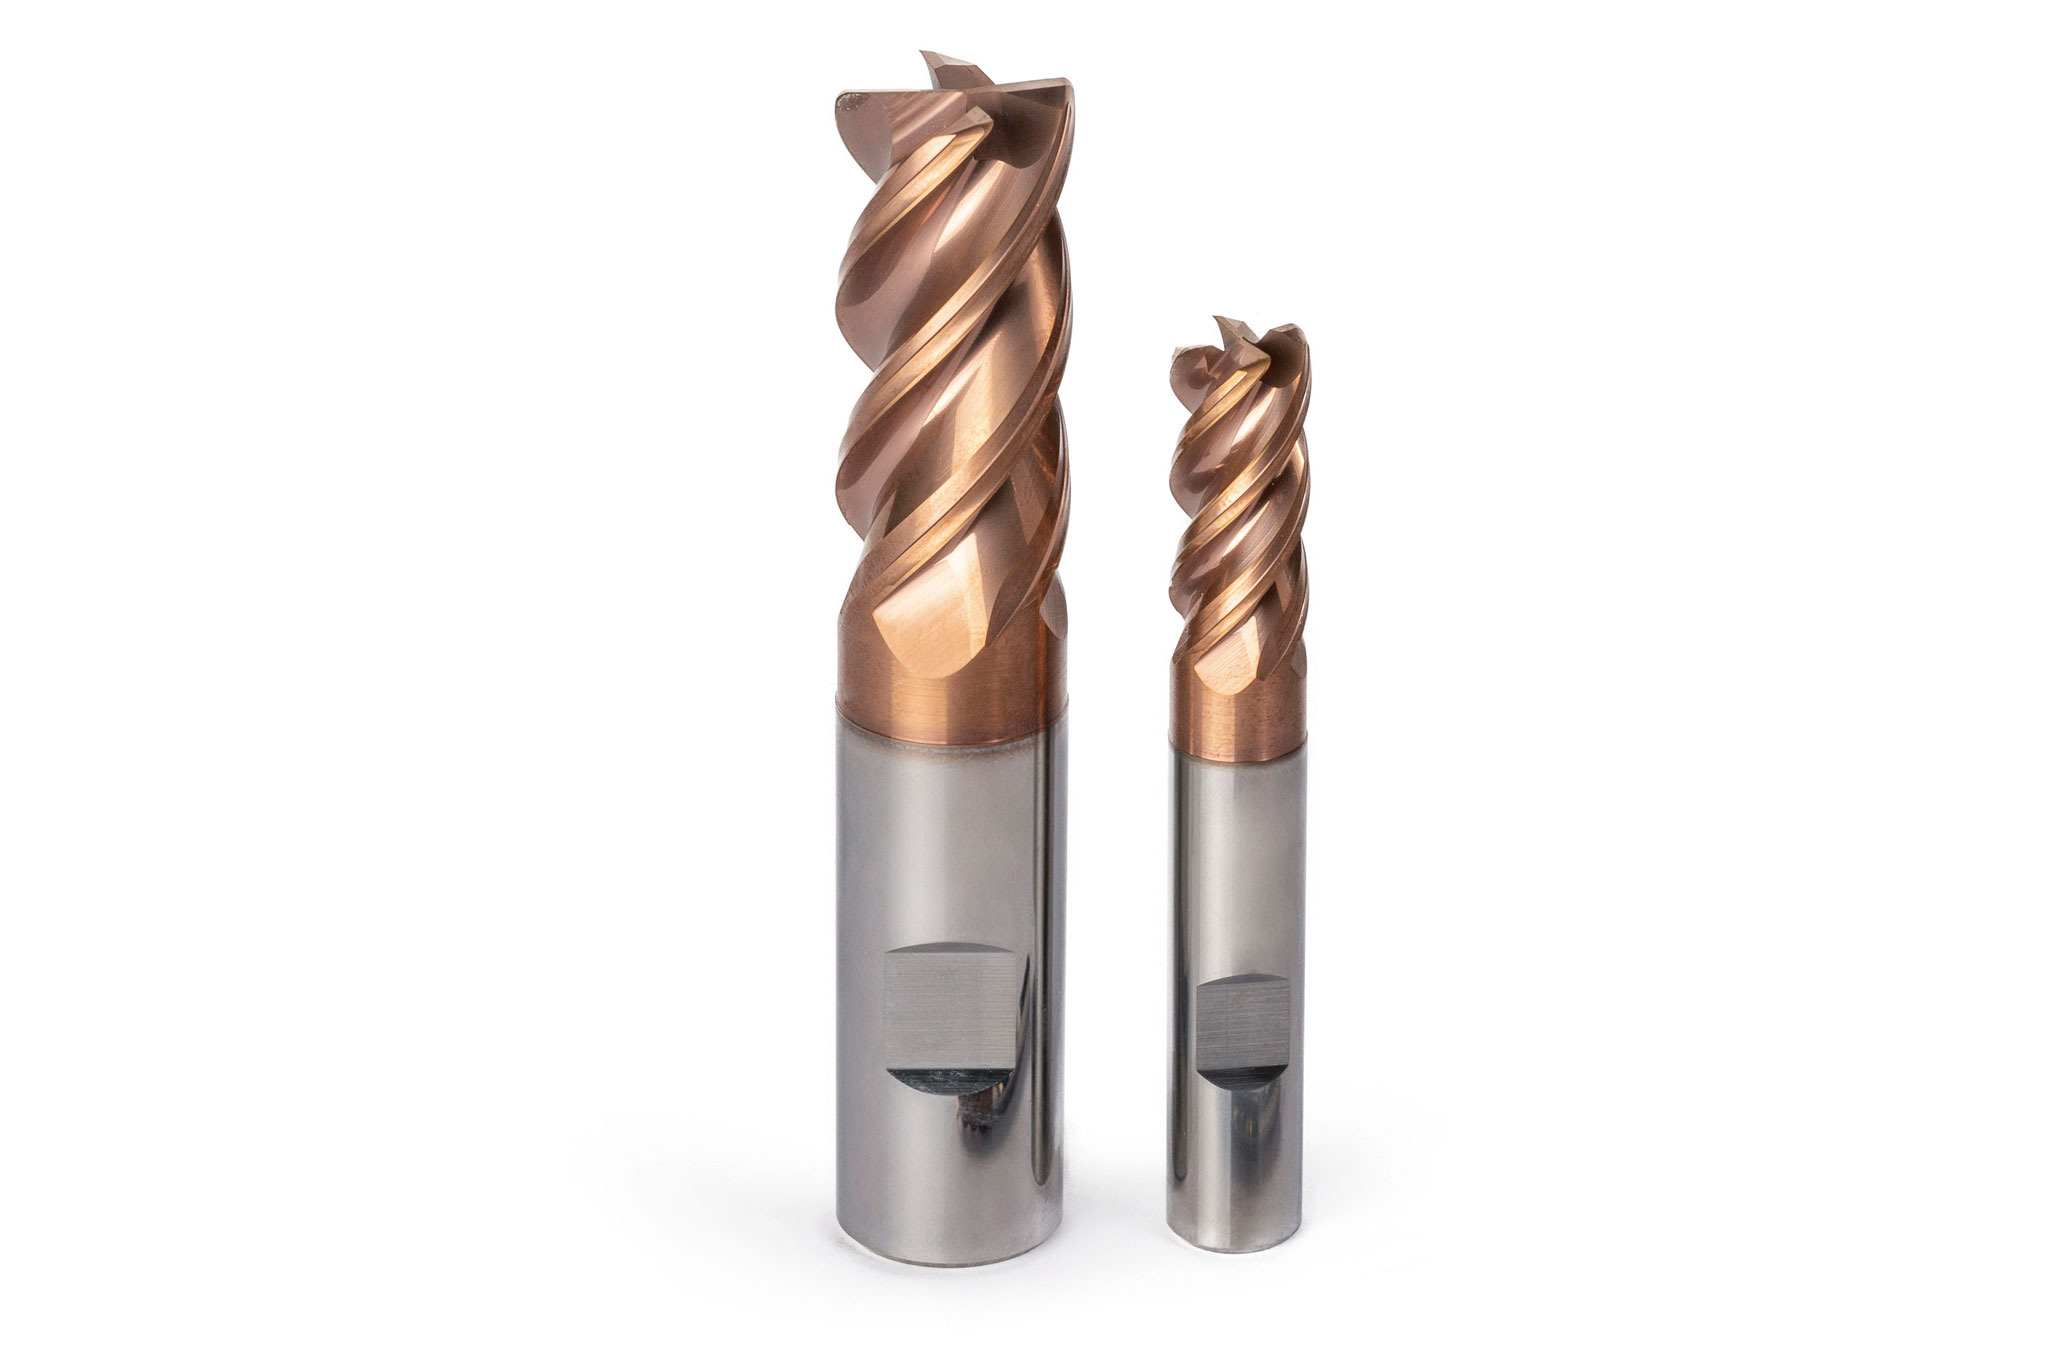
The solid carbide milling cutters OptiMill-Titan-HPC from MAPAL can be used both for roughing and for finish cuts in titanium.
The new OptiMill-Titan-HPC solid carbide milling cutter performs both roughing and final cuts in titanium very reliably  ©MAPAL

NeoMill-Titan: indexable insert milling cutters with a bite
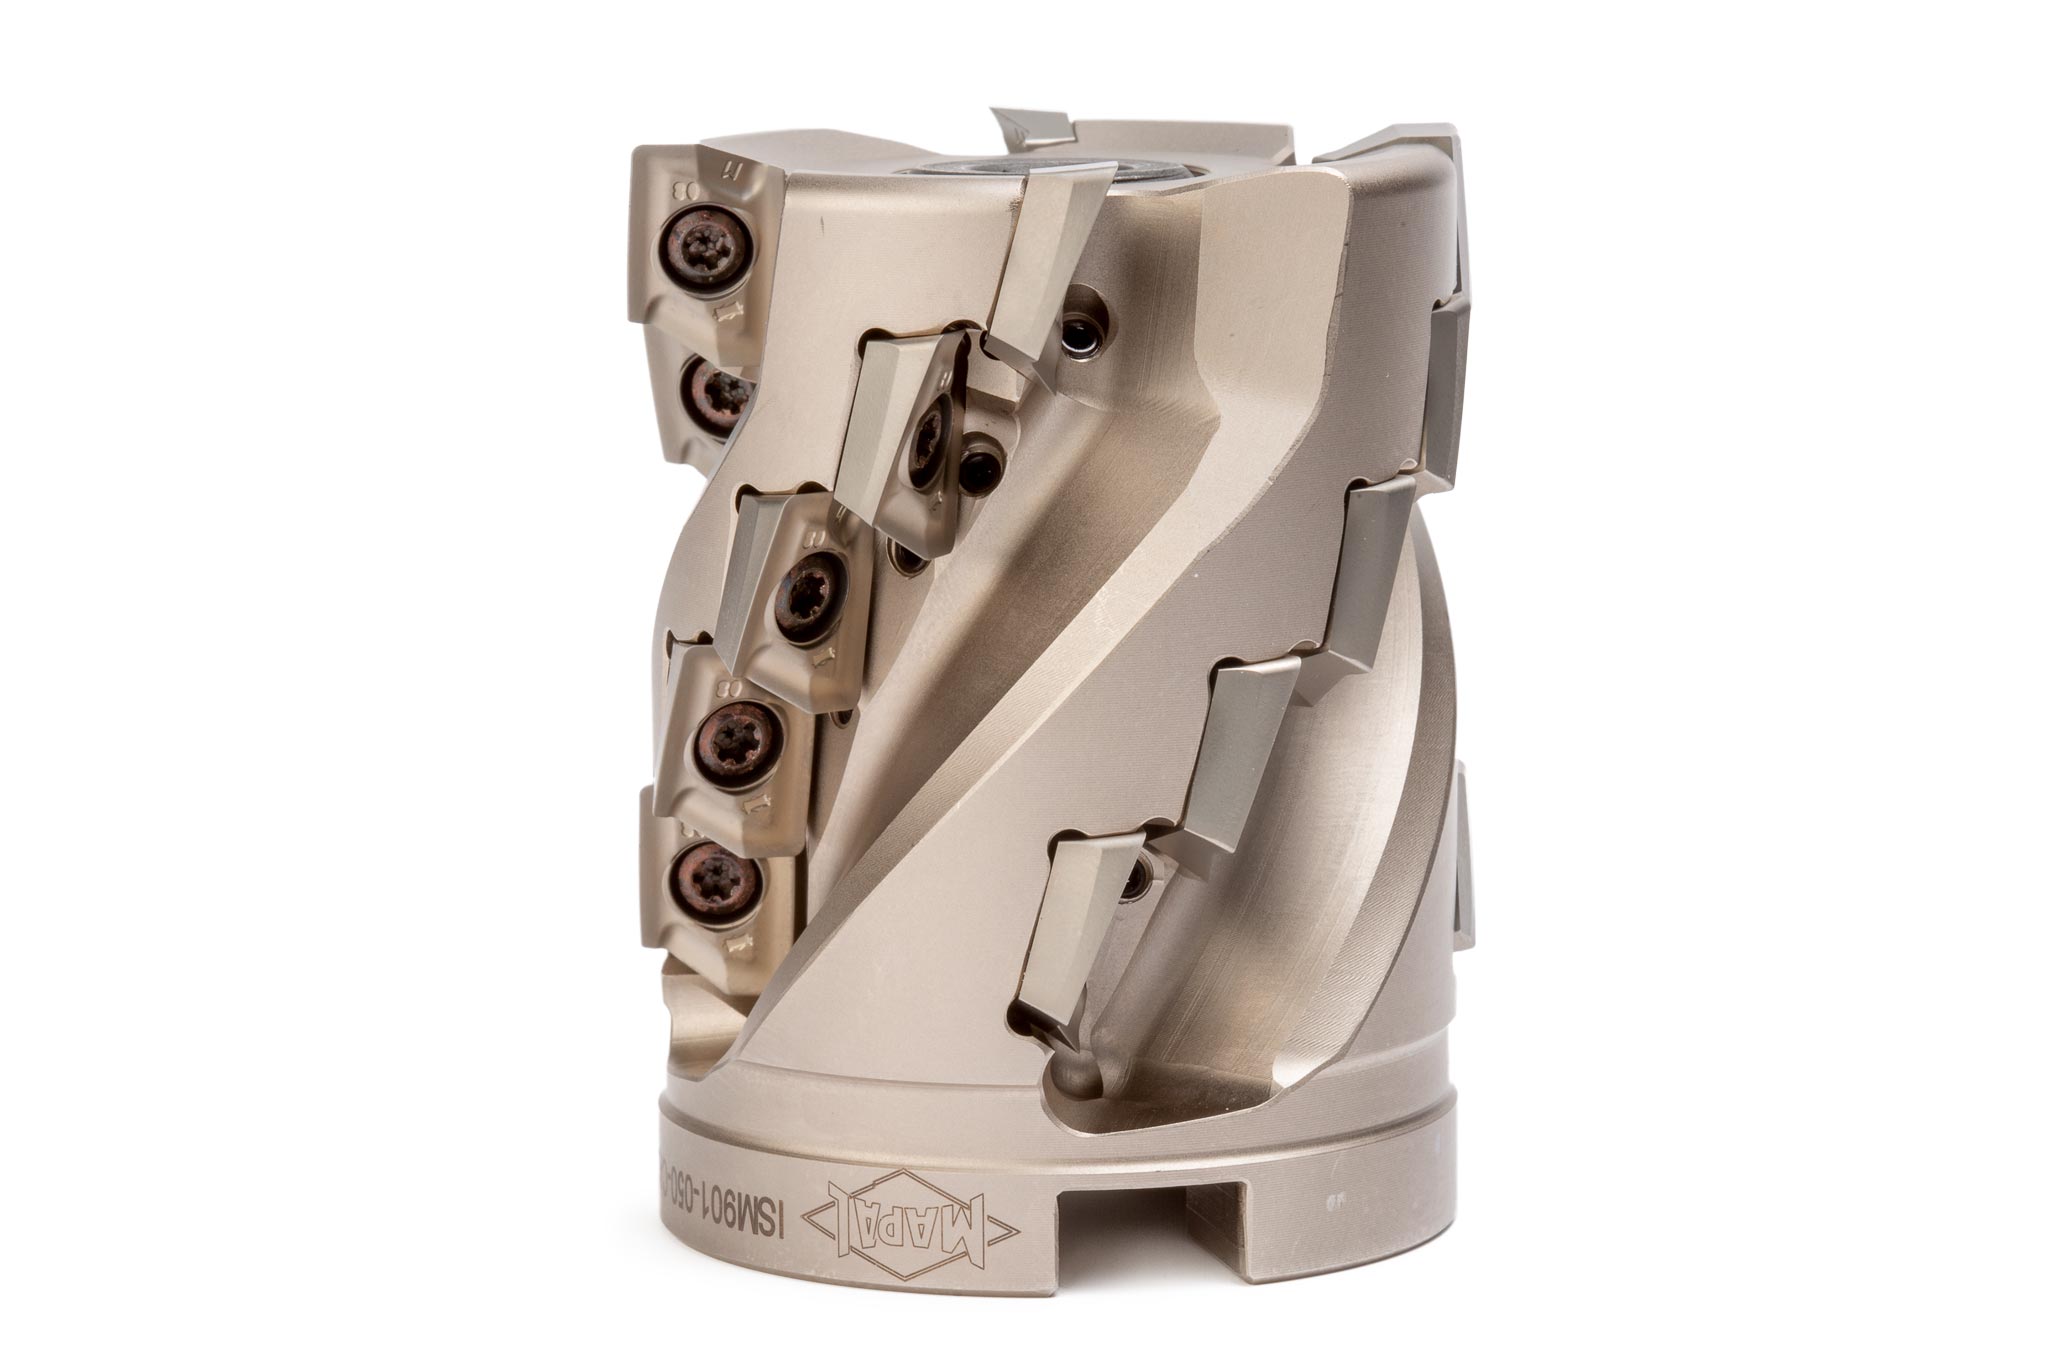
The NeoMill-Titan family of tools with indexable inserts for titanium machining consists of shell end face milling cutters in slip-on and shank versions as well as shoulder milling cutters in the standard portfolio. MAPAL has developed the topography of the indexable insert from scratch for optimum chip formation and evacuation. An equally new cutting material concept minimises wear and prevents the titanium from sticking. The available corner radii of 0.8 mm to 4 mm are tailored to structural parts in the aerospace industry. To save weight, several pockets are milled here, and their final contour should already be achieved as well as possible by pre-roughing. In the manufacturing of tail fin structures, about 90 percent of the material is removed.
A radial indexable insert milling cutter NeoMill-Titan from MAPAL.
The NeoMill-Titan milling cutter range for titanium machining with completely newly developed indexable inserts  ©MAPAL

MAPAL offers the indexable inserts with two different substrates. One grade is designed for universal applications and is aimed at customers whose focus is more on product price and less on cost per part. The second grade is more temperature-resistant, enabling higher cutting speeds and the machining of more highly annealed titanium material. Cutting speeds of up to 70 m/min can be achieved. "With this approach, we specifically address the requirements of the market," says Tyczyński. "We take into account the individual needs of our customers and offer an optimally fitting solution."

The tool body has also been newly developed for the high-tech inserts. With flowing shapes, the chip flutes transport the chips out of the shear zone. The coolant is fed axially directly through the milling arbour. The unequal spacing of the inserts provides additional stability and smooth running. The coolant is supplied axially directly via the milling arbor. The whole milling cutter is basically a hollow body with a large chamber in the centre, from where the coolant is conveyed to each insert. The coolant outlets are designed variably. By changing a threaded pin, the operator can regulate the flow rate for each individual cutting edge.

MAPAL supplies the shoulder milling cutters for titanium from stock in diameters from 40 mm to 125 mm. The shell end face milling cutters are stocked from a diameter of 32 mm to 80 mm. Special dimensions are also available upon request.


Kathrin Rehor, PR Project Manager at MAPAL

Contact

Kathrin Rehor Public Relations Kathrin.Rehor@mapal.com Phone: +49 7361 585 3342


Further articles on the milling product range