Orbitrol

Orbitrol housing GG25

Initial situation at the customer
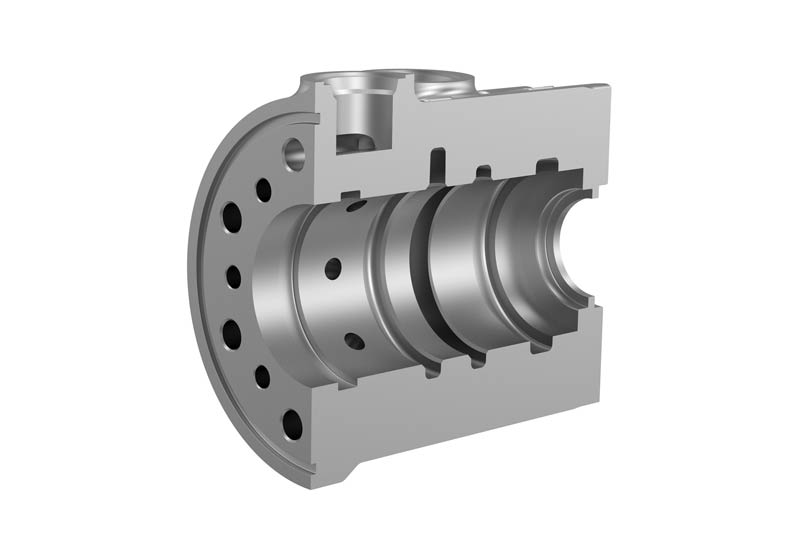
steering orbitrol housing

  • Small to medium quantities
  • High tool costs
  • High costs for subsequent mandrel honing

Special features of this solution

  • Multi-stage combination tools → Reduces tool change and associated processing costs as well as machining time
  • Quick renewal of cutting edges as inserts can be easily exchanged
  • Various workpiece material can be machined with a single tool body → Insert solutions enable maximum flexibility for small lot sizes

Spool bore
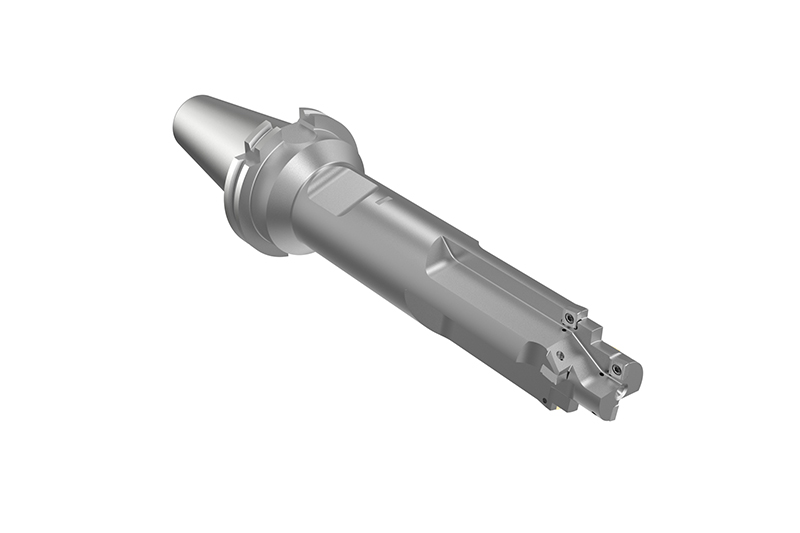
  • Machining steering orbitrol housing

    Boring

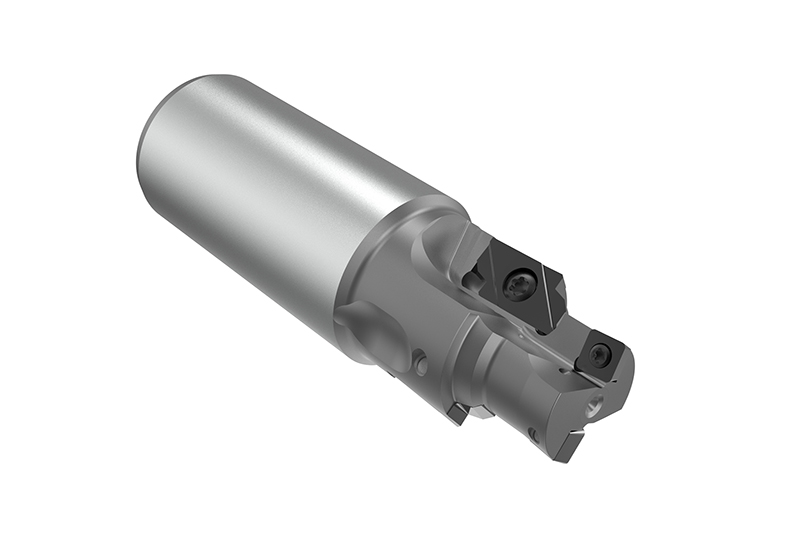
    Insert drills
    • Economical machining of connection bores and contour machining
    • Specially developed chip guiding stages ensure optimal chip flow and removal

  • Machining steering orbitrol housing

    Fine boring

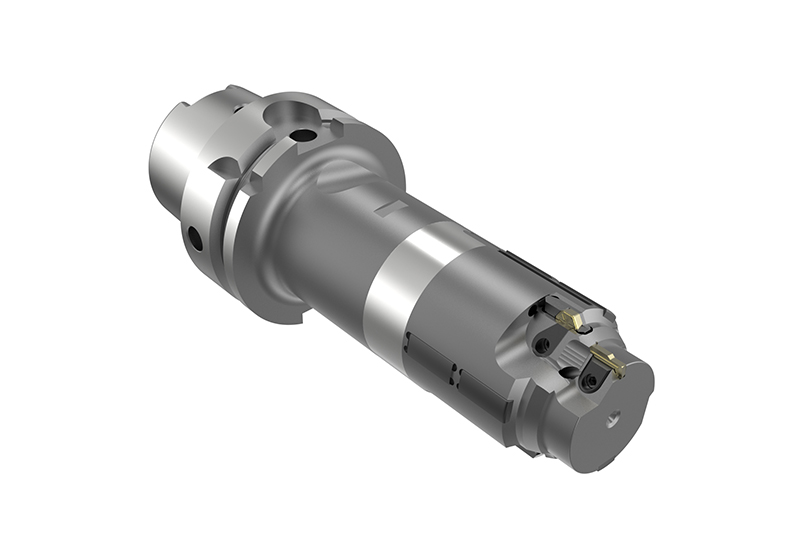
    Multi-stepped fine boring tool
    • Ideal cutting edge usage for finishing spool bores prior to honing
    • Ideal bore quality and tolerances to one another prior to honing

Anschlussbohrung

  • Bearbeitung Lenkorbitrolgehäuse

    Konturbearbeitung

    Wendeplatten-Aufbohrer
    • Wirtschaftliche Bearbeitung von Anschlussbohrungen und Konturbearbeitungen
    • Speziell entwickelte Spanleitstufen garantieren optimalen Spanfluss und Abtransport

O-Ring-Einstich

  • Bearbeitung Lenkorbitrolgehäuse

    Axialeinstich

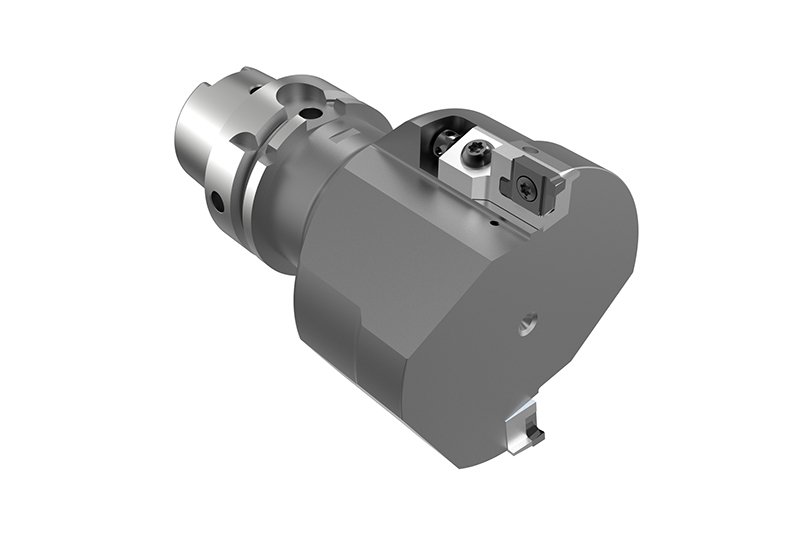
    Wendeplatten-Bohrwerkzeug
    • Einfaches Handling bei der Herstellung von axialen O-Ring Einstichen
    • Signifikante Taktzeiteinsparungen gegenüber Fräsoperationen

JÄHRLICHE WERKZEUGKOSTEN SCHIEBERBOHRUNG [€]*

Vorteile

  • Teurer Honprozess in der Schieberbohrung durch ideale Vorbearbeitung verkürzt 
  • Werkzeugkosten in großen Bauteildimensionen signifikant reduziert
  • Werkzeuglösungen bei hoher Bauteilvarianz ebenso problemlos in weiteren Lenkeinheit-Komponenten einsetzbar

HERSTELLKOSTEN PRO SCHIEBERBOHRUNG [€]*