Complex aircraft component for maximum performance
Co-engineering by bavius and MAPAL
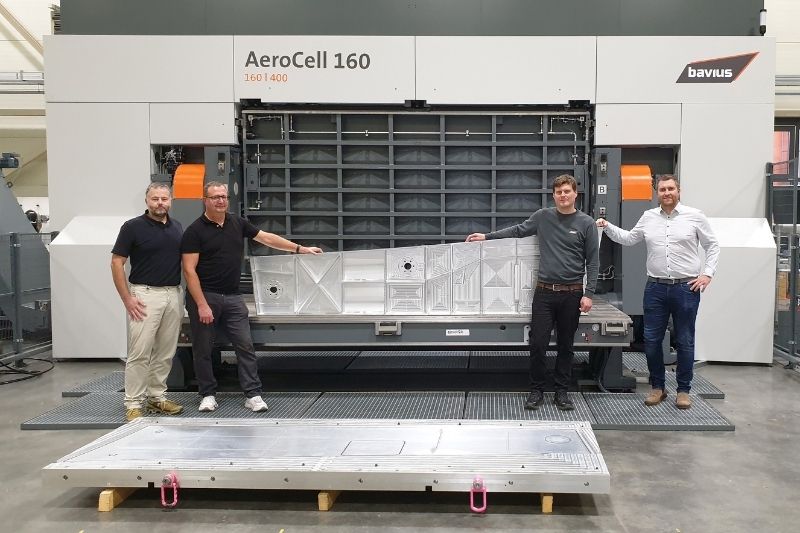
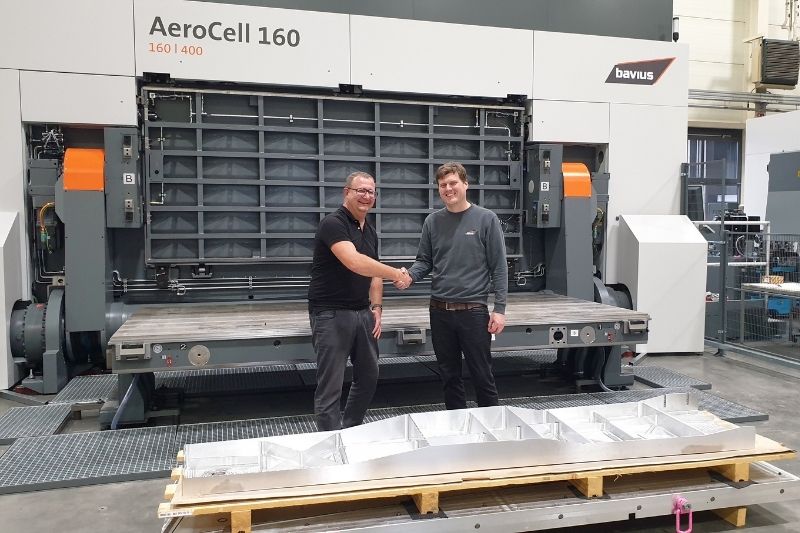
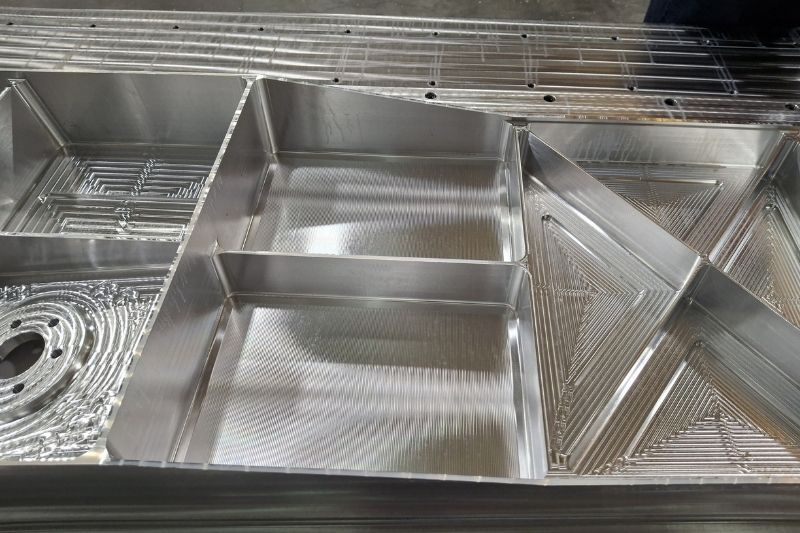
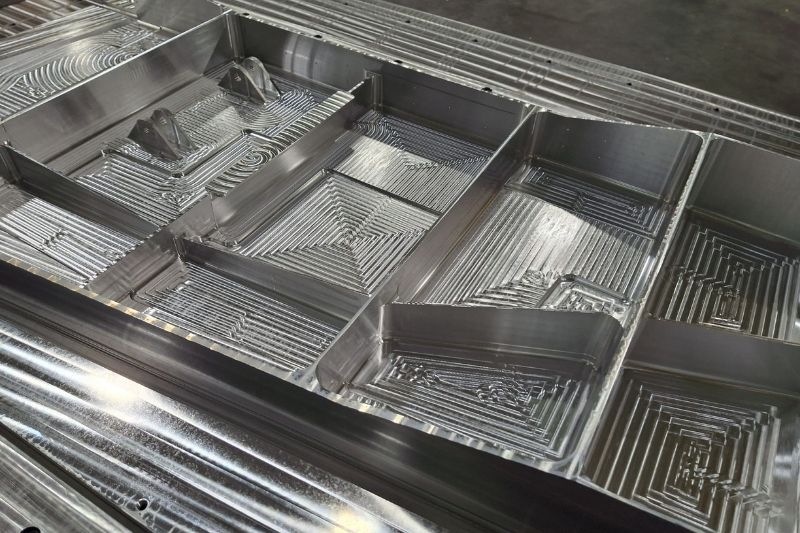
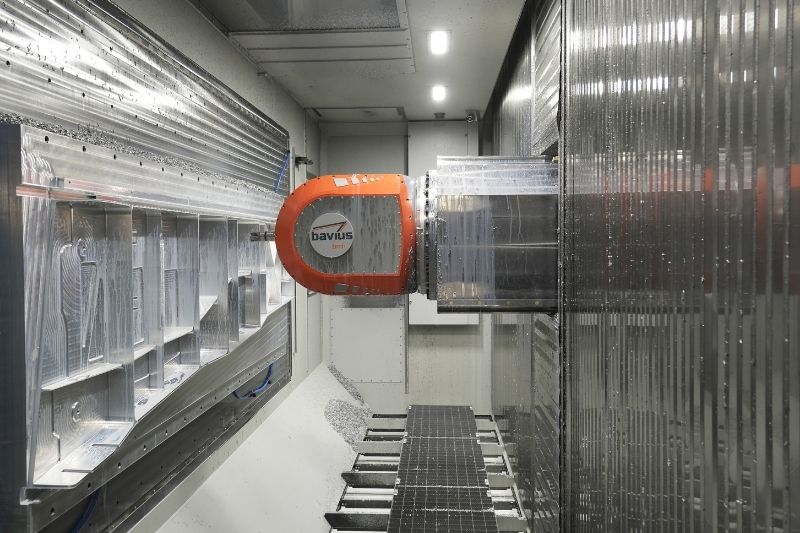
As part of a joint project, MAPAL and machine manufacturer bavius designed and manufactured a demonstration part for the aerospace industry. The aluminium component, measuring approximately three by one metres, is based on a real rear spar from aircraft manufacturing enhanced with a variety of complex features. Besides its complexity, the component is also impressive due to the relatively short machining time of ten hours thanks to the productivity of the bavius AeroCell and the special MAPAL tools used for aluminium machining.
bavius technologie, based in Baienfurt in Southern Germany, is specialised in the high-speed volume machining of structural components made of aluminium, which are typically required in the aerospace industry for wings and fuselages. Previously known as Handtmann A-Punkt Automation, bavius has been active as an independent family business since 2017, concentrating on two product lines: HBZ and AeroCell horizontal machining centres and the PBZ profile machining centres. With around 120 employees, bavius generates more than 80 per cent of its turnover in the aerospace industry. As an OEM or supplier, their customers produce components for commercial and military applications. Components for satellites or rockets like the Ariane 6 are also produced on their machines.
Most bavius machines are located in Europe, but they are also strong in North American and Asian markets. While the company has offices in the United States, production for all markets worldwide exclusively takes place in Baienfurt in two air-conditioned halls with a production area of approximately 10,000 square metres.
A particular strength of bavius’s five-axis machining centres is that they are extraordinarily dynamic, which ensures high productivity during high-speed machining. To get every last drop of productivity out of their machines, bavius manufactures its own milling heads. The flagship of their product range is the bavius AeroCell 160 | 400 with a spindle power of 140 kW and top speeds of 30,000 rpm. The 140 kW are already reached at 18,000 rpm, i.e. the maximum power is available over a wide range of speeds. “When we do something, we make sure it’s done excellently – we are global technology leaders with our AeroCell 160 | 400”, says Dominik Merz, Director Global Sales.
The rear spar is selected as a demonstration part because it fits perfectly on the machine with a table height of 1.6 metres and width of 4 metres. The rear spar is a common structural component in wings. Ribs run between the rear spar and front spar, which are arranged perpendicularly to the spars. These structural components define the geometry of the wings. The outer skin is riveted onto them. The completed component is made of 7075 aircraft aluminium and measures 2977 × 748 mm. Its flat form measuring 138 mm high is typical of aircraft components. From one ton of starting weight, only 70.61 kg remain after machining – a proportion that is quite common in the aerospace industry.
Among other factors, legal reasons prevented bavius and MAPAL from using a real aeroplane component for the machining. This however gave those responsible the freedom to use the design for a variety of applications. As a result, this demonstration piece is much more complex than any normal rear spar. It includes features that are not necessarily associated with a spar but could be useful for other components. “A customer who knows structural components and sees our part will recognise it and notice characteristics that are also found in their own components”, Merz says, explaining this approach.
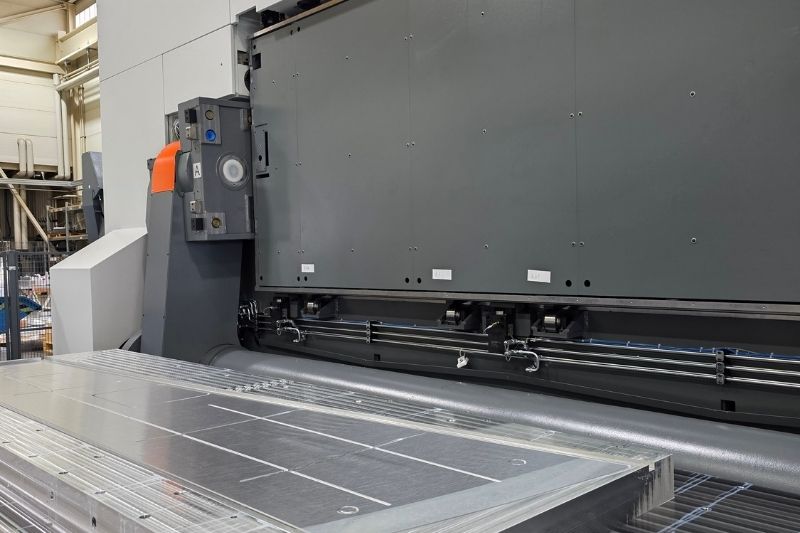
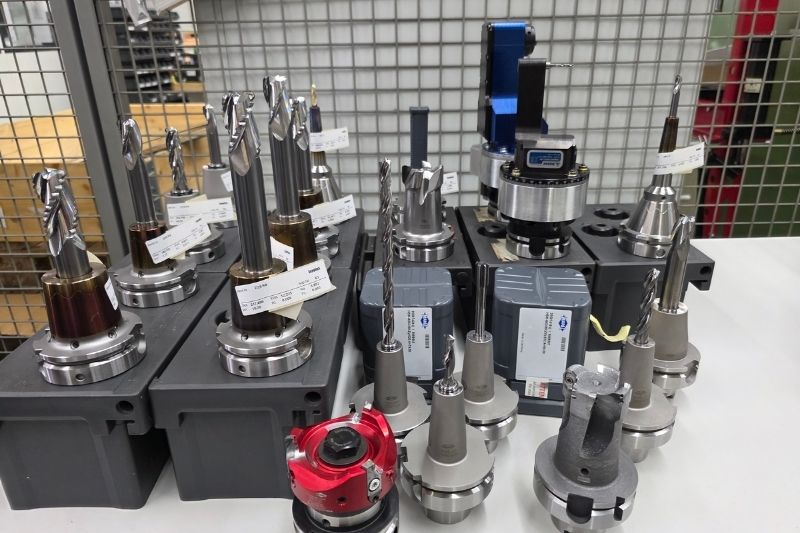
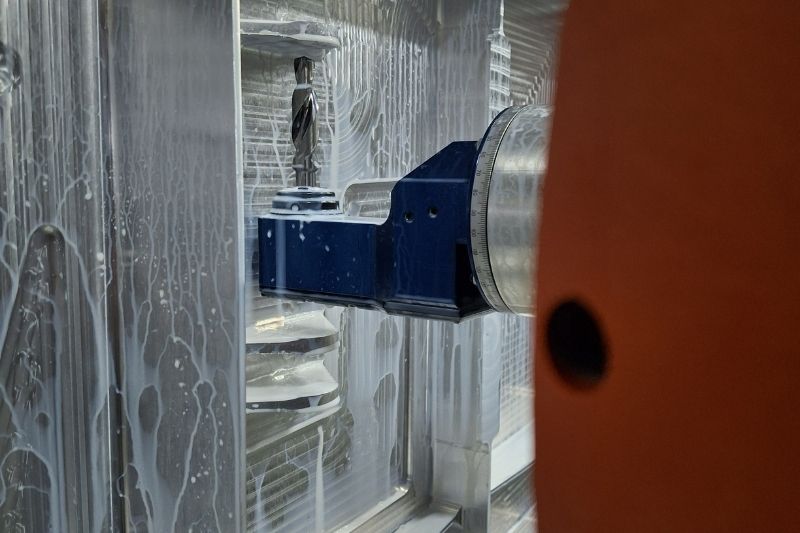
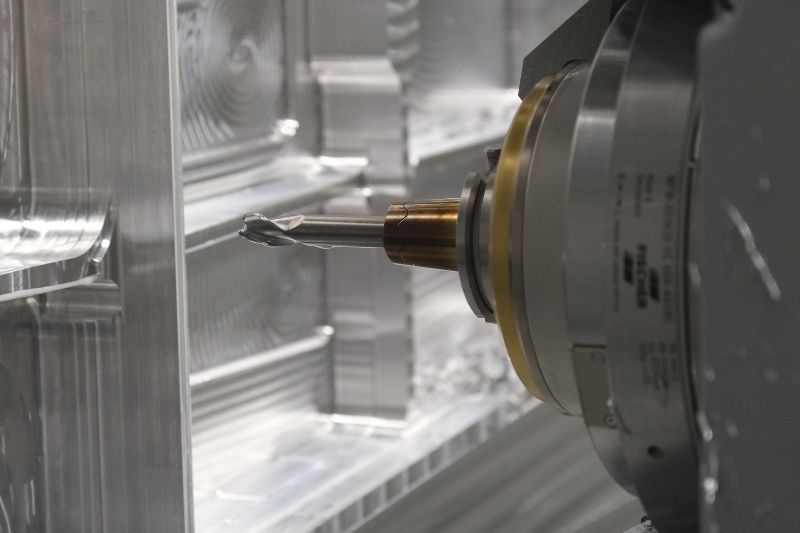
Die Bearbeitung fand in Baienfurt in zwei Aufspannungen statt. Setup 1 erfolgte in Niederzugspannung, im Setup 2 sorgte Vakuumtechnik für sicheren Halt. Die Vorderseite sieht auf den ersten Blick einfacher aus als sie tatsächlich ist. Die Fläche ist nicht eben, sondern biegt sich leicht konvex über einen Radius von 9,5 m. Damit kann man das Bauteil nicht einfach planfräsen, sondern muss Fünf-Achs-Bearbeitung nutzen. Zum Schruppen und Schlichten setzte MAPAL auf den NeoMill-Alu-QBig mit 50 mm Durchmesser und den OptiMill-Alu-Wave mit 25 mm Durchmesser. Das Oberflächenfinish führte ein PKD-Sonderfräser durch.
Taschen in allen Formen
Besonders anspruchsvoll gestaltete sich die Bearbeitung der Rückseite, die in neun verschiedene Sektionen mit jeweils besonderen Applikationen untergliedert ist. Wie jedes Rear Spar weist das Musterbauteil viele Taschen auf, hier allerdings in allen erdenklichen Formen ausgestaltet: rechteckig, dreieckig, rund, offen, geschlossen, teilweise mit schrägem oder gewölbtem Boden. Die Stege sind sehr dünn, Wandungen überwiegend schräg. Die Taschen haben eine Tiefe von bis zu 137 mm.
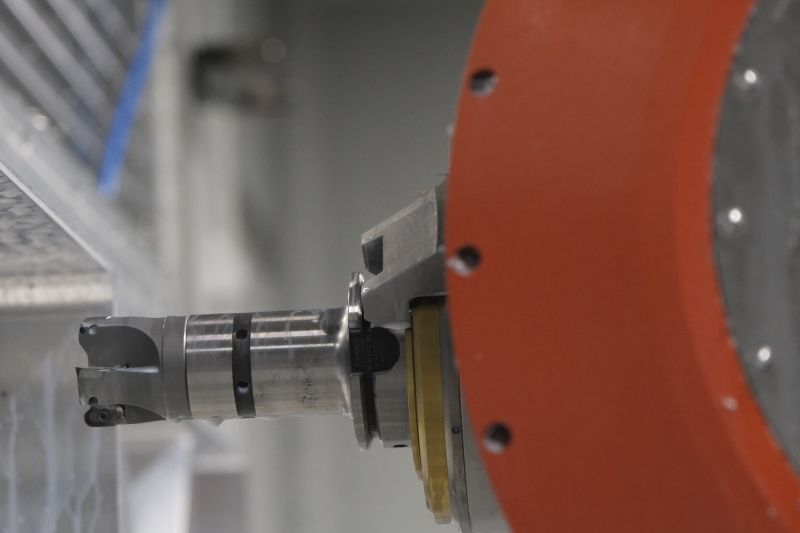
Nach der Vorbearbeitung durch den NeoMill-Alu-QBig kam zum Ausräumen der Taschen ein OptiMill-Alu-Wave in verschiedenen Längen zum Einsatz. Das Semi-Schlichten übernahm ein speziell für Luftfahrtanwendungen modifizierter Eckfräser. Dank seiner besonderen Geometrie eignet sich das Werkzeug insbesondere zur Restmaterialbearbeitung der Ecken sowie zum anschließenden Schlichtfräsen der Böden und Wände. Der spezielle Kernanstieg sichert dabei optimale Stabilität im Zerspanungsprozess. Um alle Bereiche effizient zu bearbeiten, setzten die MAPAL Spezialisten den modifizierten Eckfräser in verschiedenen Durchmessern und Längen ein.
Wie auch in der Programmierung bei MAPAL auf Effizienz geachtet wurde, beschreibt Komponentenmanager Alexander Follenweider: „Wir arbeiten mit einer Zickzack-Strategie im Gleichlauf und Gegenlauf, um Wege zu sparen. Während der Bearbeitung wird also die Strategie ständig gewechselt.“ Trotz hoher Bearbeitungsgeschwindigkeiten dürfe das Aluminium nicht beschädigt werden, da es bei Überhitzung seine Eigenschaften verändert.
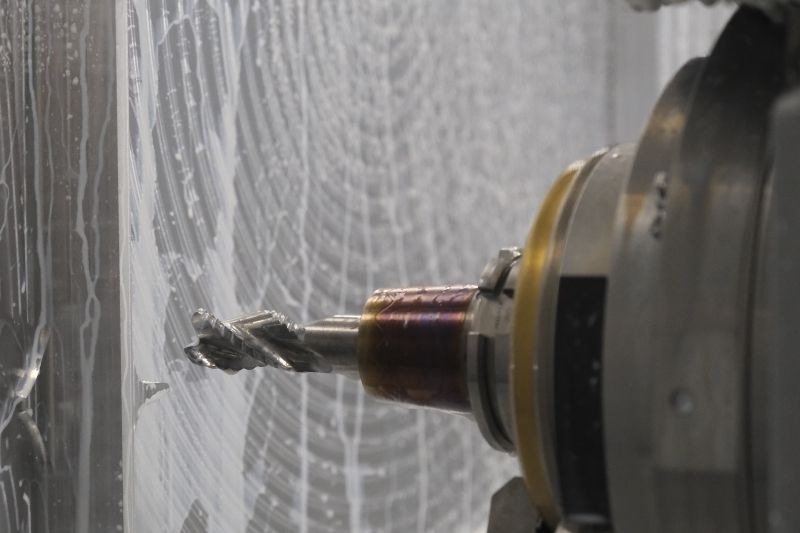
At top speeds, the OptiMill-Alu-Wave achieves a feed of 12 m/min at a cutting depth of 48 mm at 29,000 rpm. The bigger NeoMill-Alu-QBig achieves a feed of 25 m/min at 10 mm cutting depth. Alone in the first 55 minutes of machining of the second clamping, 425 kg of aluminium are thus machined. At its peak, this results in a chip volume of more than 14 l/min. “The results we were able to achieve here are excellent – and we were also able to create very good surfaces in the process”, says Stefan Diem, application engineer at bavius.
Nothing is standard
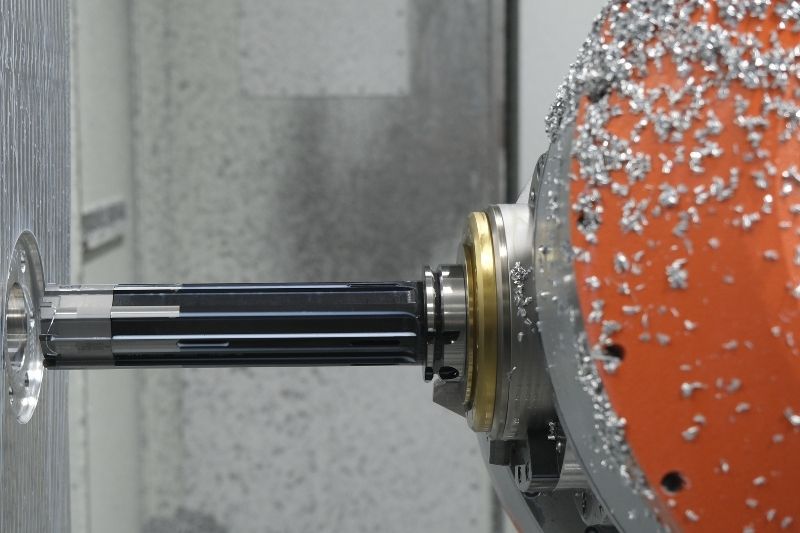
The various pockets are not the only challenges on the component: The bores on the four lugs can only be reached via an angled head. Undercuts are required elsewhere. A T-stiffener, which is common for structural components and provides rigidity, is also found on the demonstration part and is machined with a special PCD tool. Bore and reaming operations are also called for in certain areas. “Nothing is normal on our component”, Merz says, referring to the fact that you will be hard pressed to find a right angle anywhere on the part. Such oblique constructions are however the norm in the aerospace industry.
For the involved partners’ customer presentations and as an eyecatcher for trade fairs, five of these rear spars are produced in Baienfurt. Much to the satisfaction of all those involved, the machining of a part takes a total of almost precisely 10 hours. “A component like this can take between 20 and 30 hours on other machines”, Merz estimates. Structural parts are usually machined vertically on gantry machines with big tools. Cutter heads with diameters of 125 mm are normal. Feeds and speeds remain low. One disadvantage of this way of doing things is that chips are left behind which can cause scratches. Heat is also transferred to the component. Horizontal machining precludes this. Together with powerful tools that enable high cutting data, the dynamic AeroCell 160 | 400 opens entirely new possibilities thanks to its extreme acceleration.
Close collaboration
MAPAL and bavius have been profiting from their close cooperation for many years. While MAPAL was developing the NeoMill-Alu-QBig and OptiMill-Alu-Wave, they were able to test and further optimise prototypes of the new tools in Baienfurt. As a tool manufacturer, MAPAL doesn’t have equally powerful machines in Aalen. On the other hand, bavius depends on innovative tools, as Diem explains: “For our premium machines, we need top tools by suppliers like MAPAL offering high-volume milling cutters that take our machines to their limits. That doesn’t work with universal tools – we don’t gain any insights with them.” The partners demonstrated what the AeroCell 160 can do two years ago. During test operations with overloading, the solid-carbide milling cutter OptiMill-Alu-Wave achieved chip volumes of up to 20 l/min while full slot milling normal aluminium. The top results achieved here are every bit as impressive: 12 l/min for a component made of the AL 7075 with its higher tensile strength.
“I really appreciate the collaboration with MAPAL because we speak openly and treat each other fairly, and because they always provide a solution”, Diem highlights. For Jens Ilg, Business Development Aerospace & Composites at MAPAL, the shared success also has a personal dimension: “I also get an optimal feel of our own products when I see them being used in real and demanding conditions. And then I can offer them to customers with corresponding recommendations.”