• Excavator

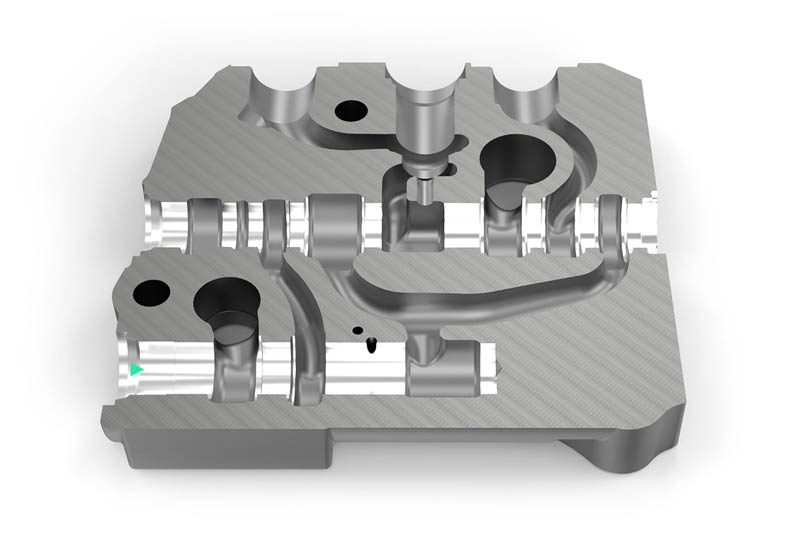
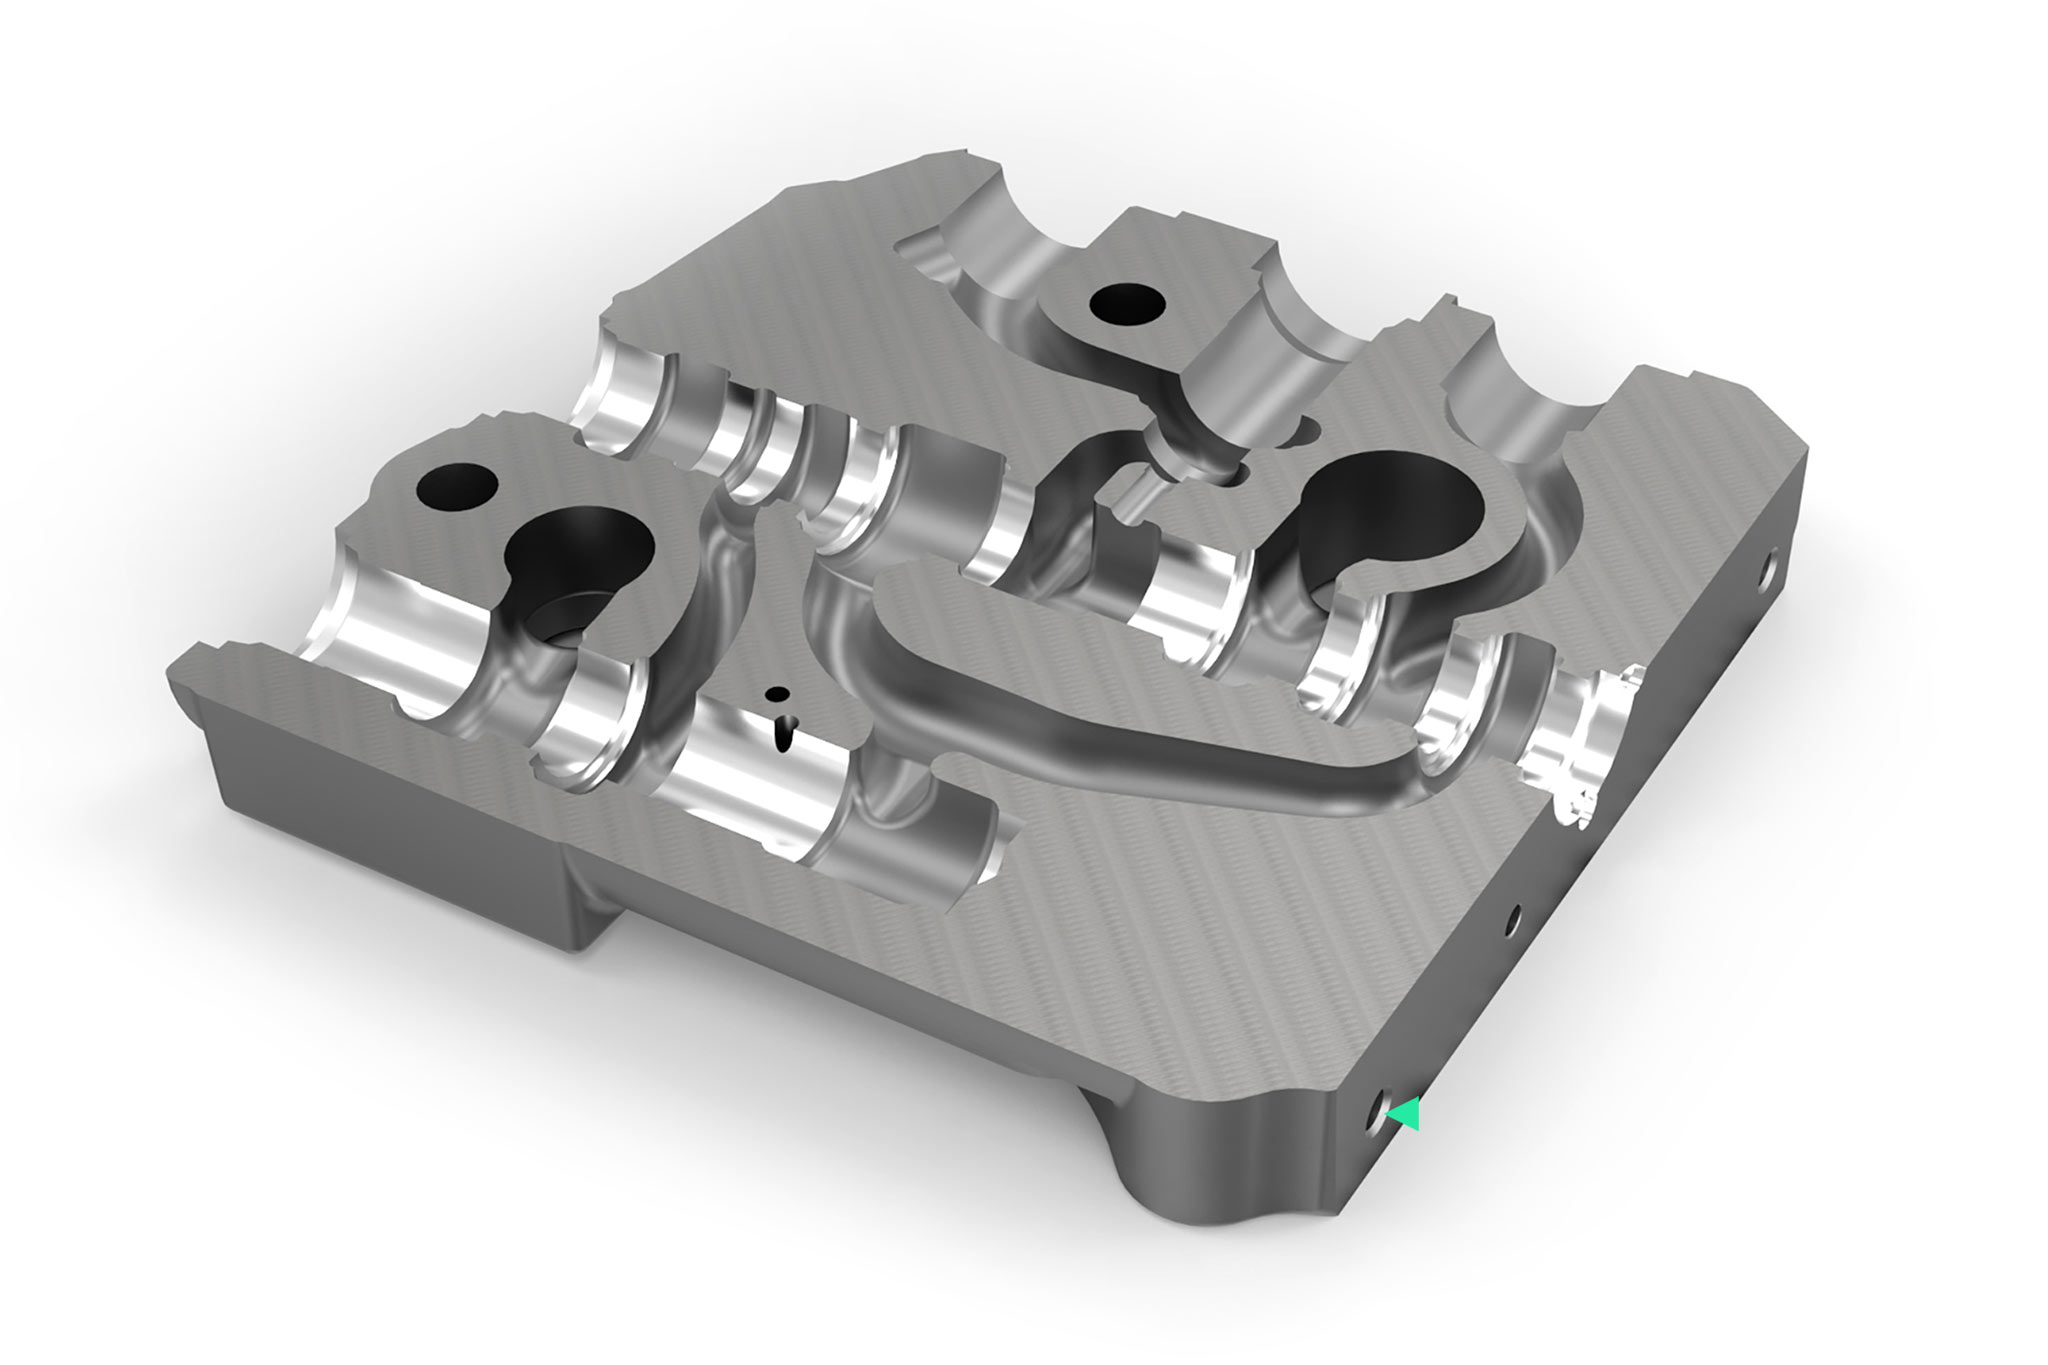
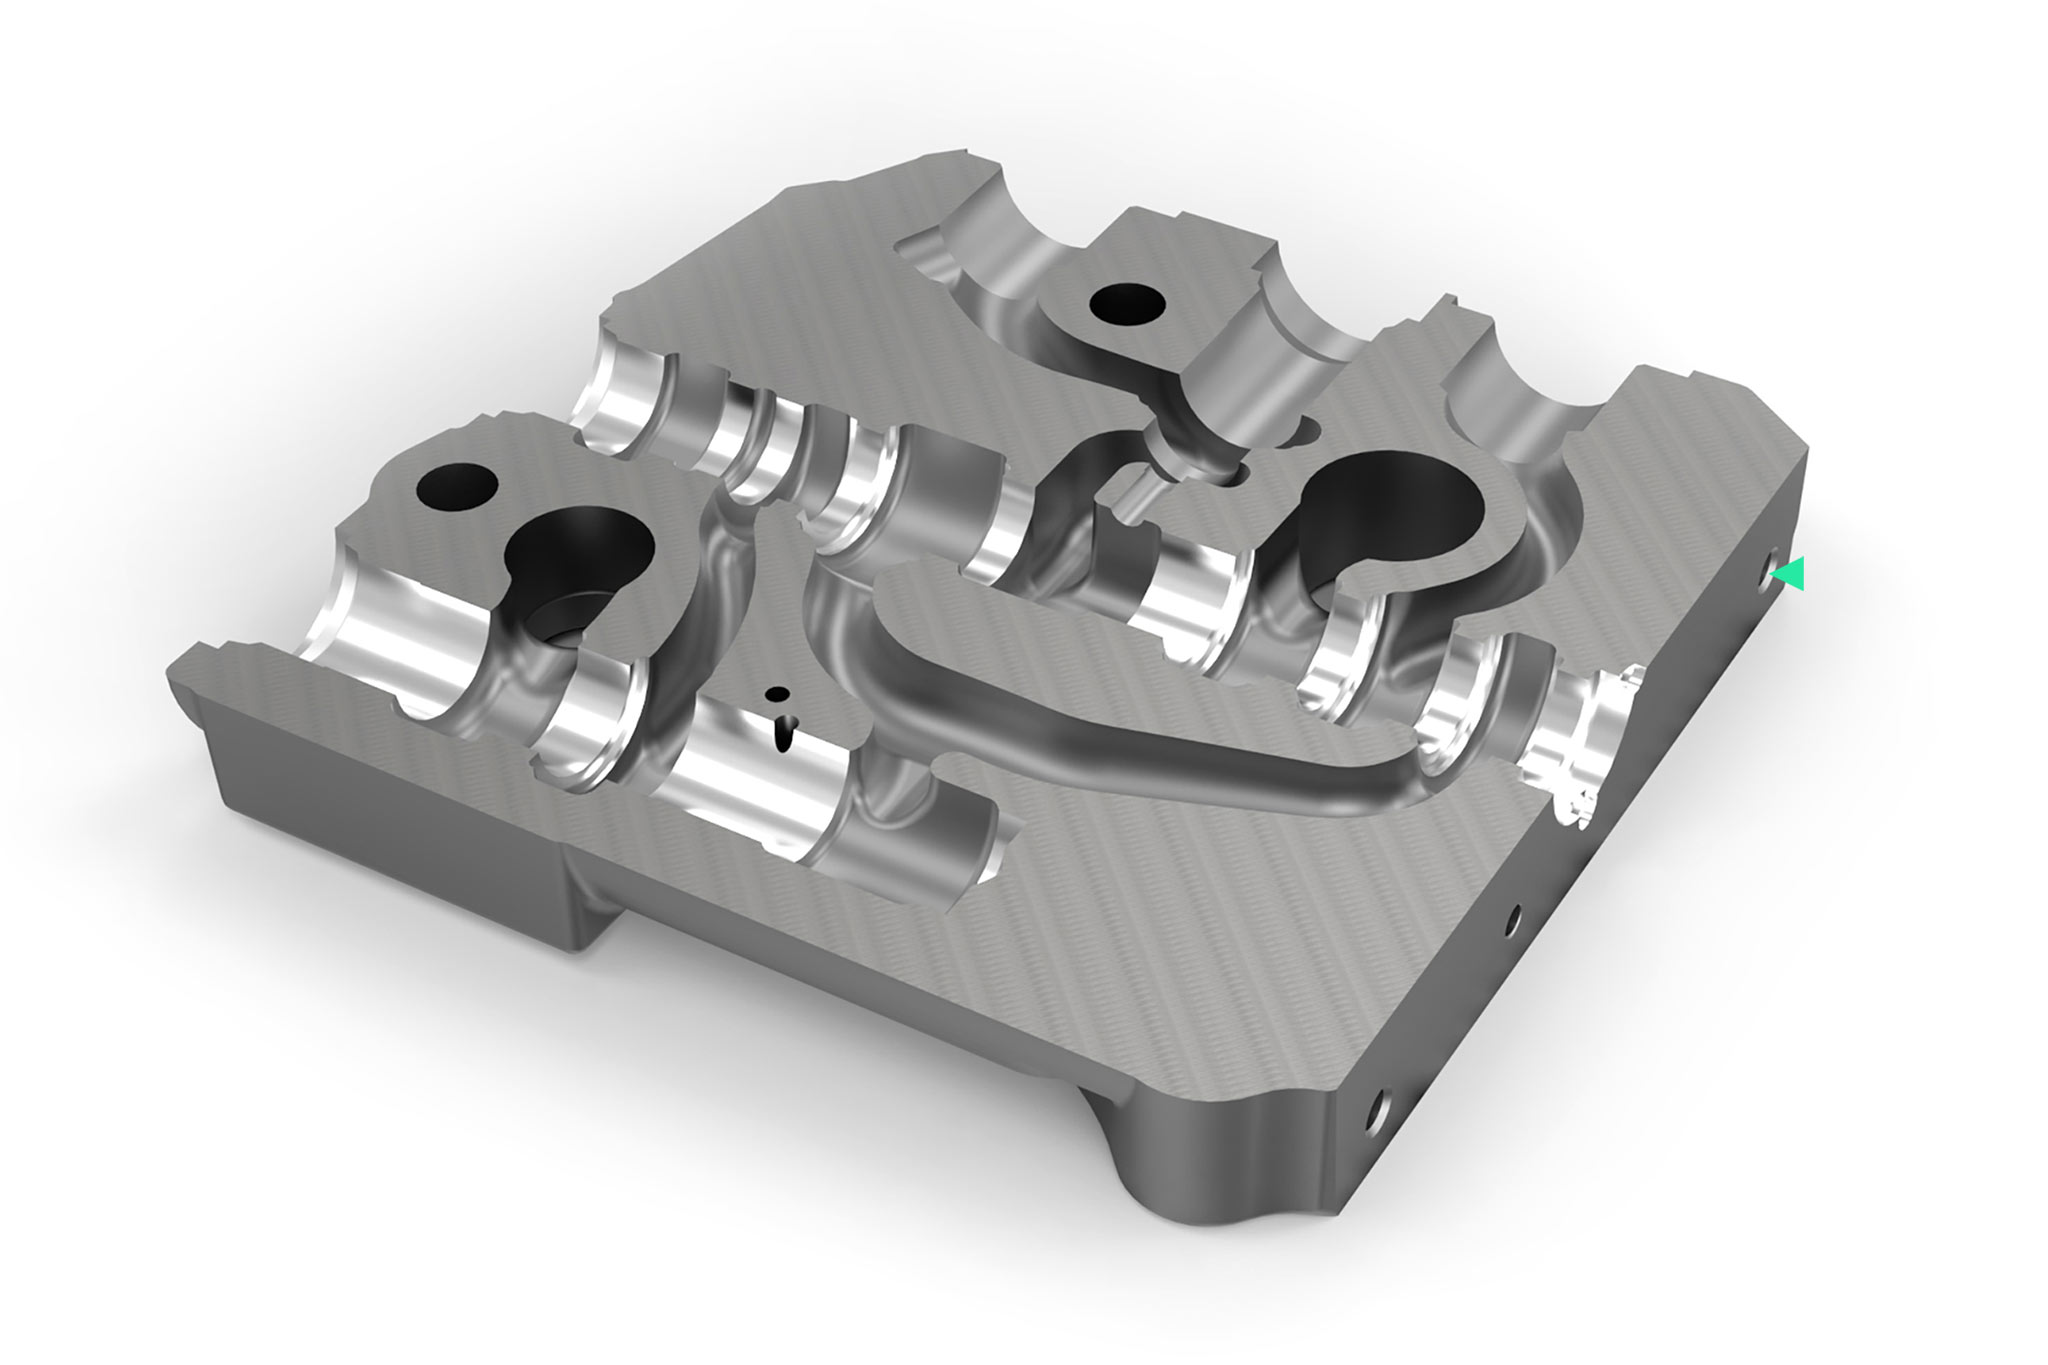
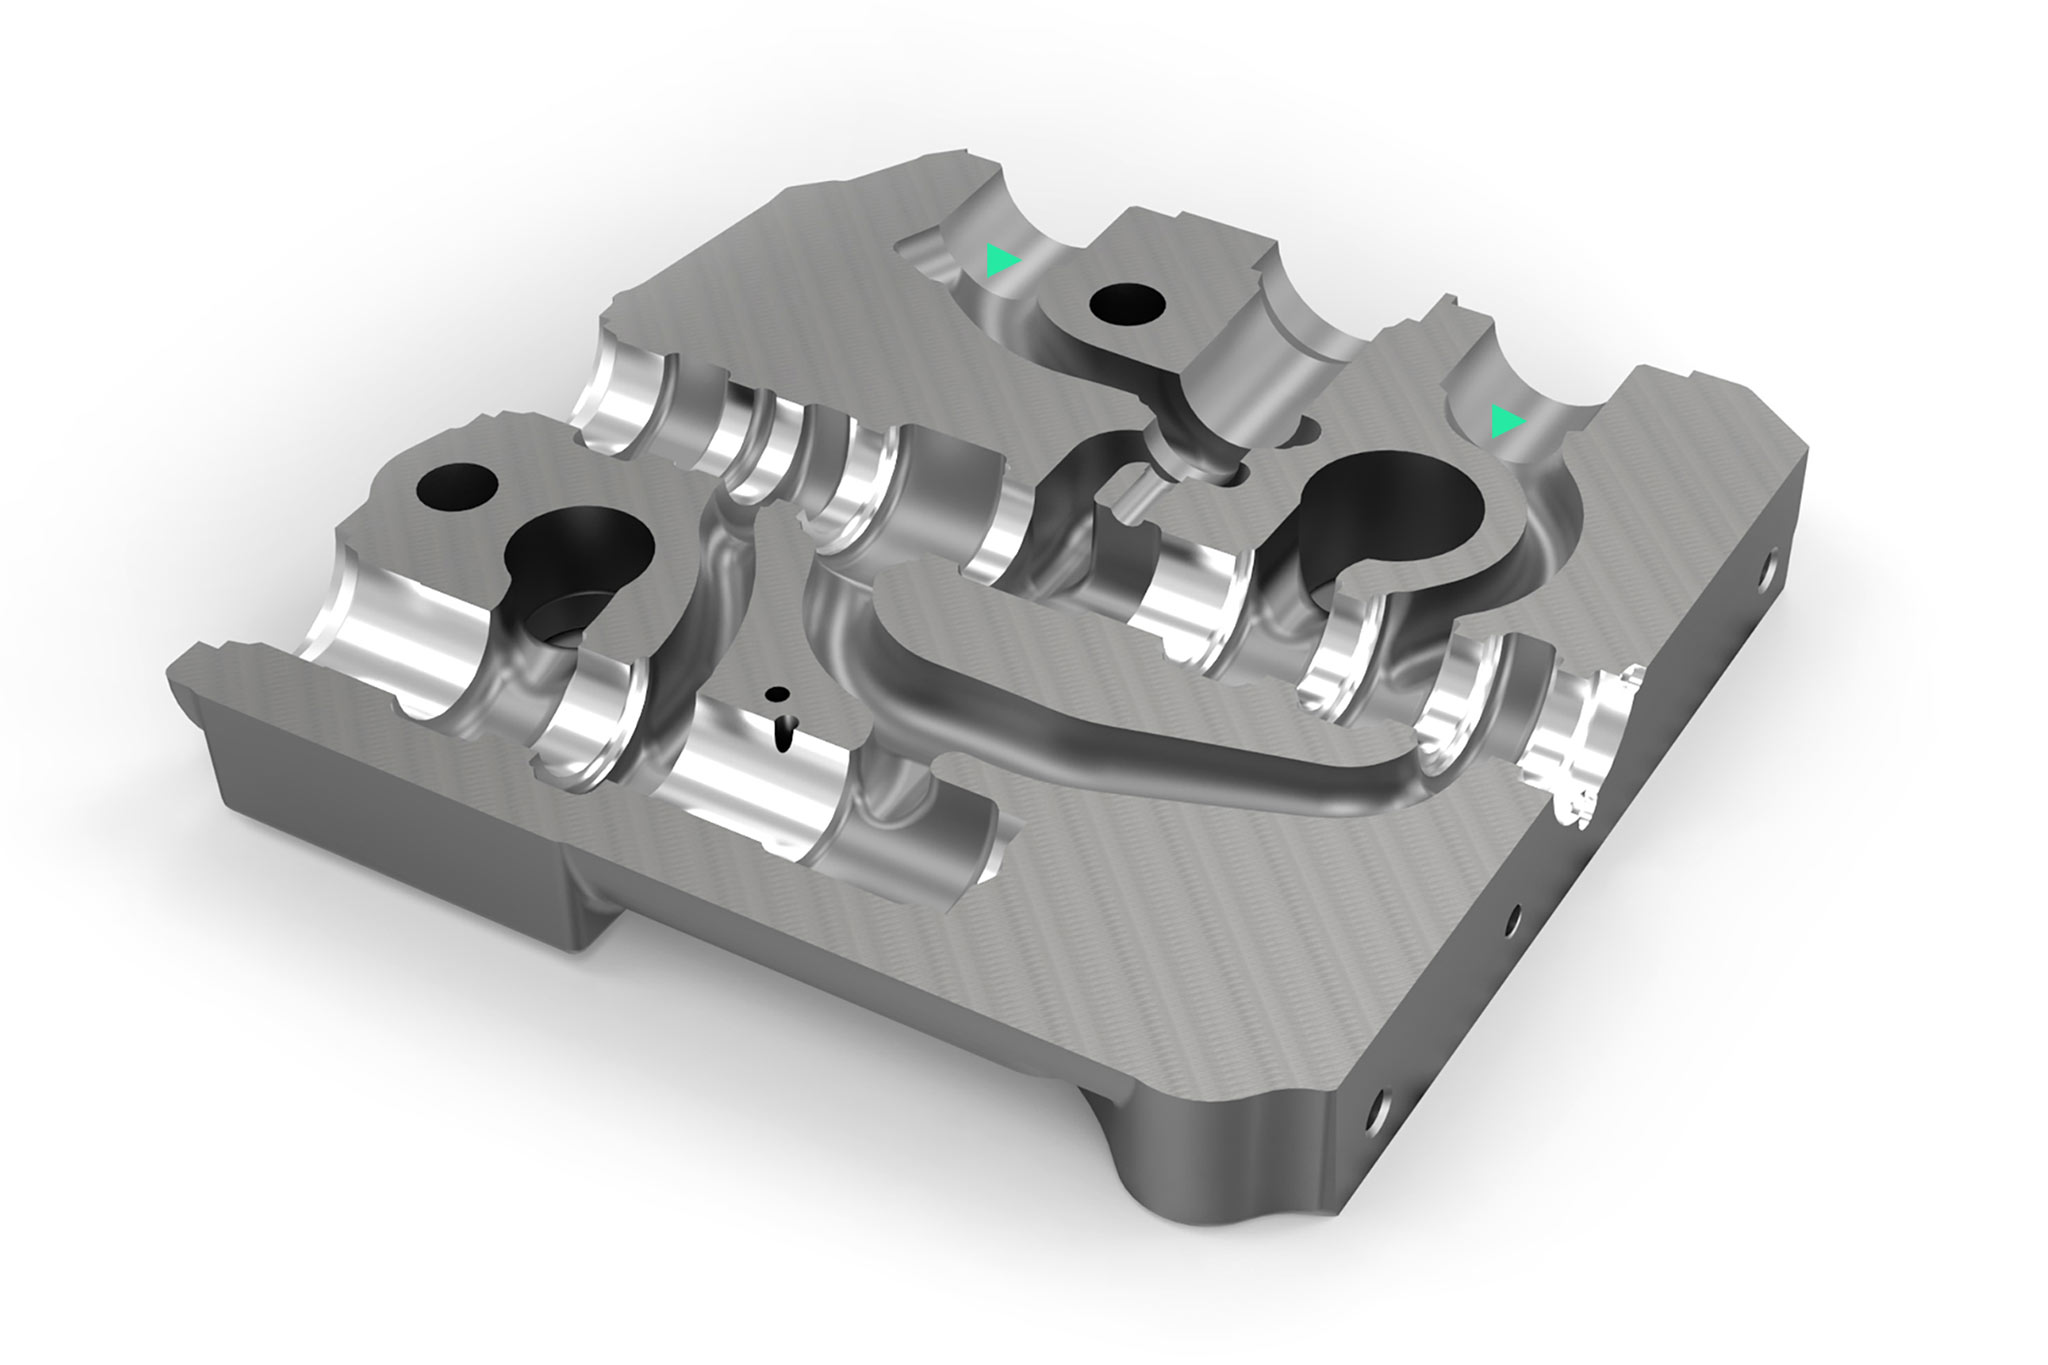
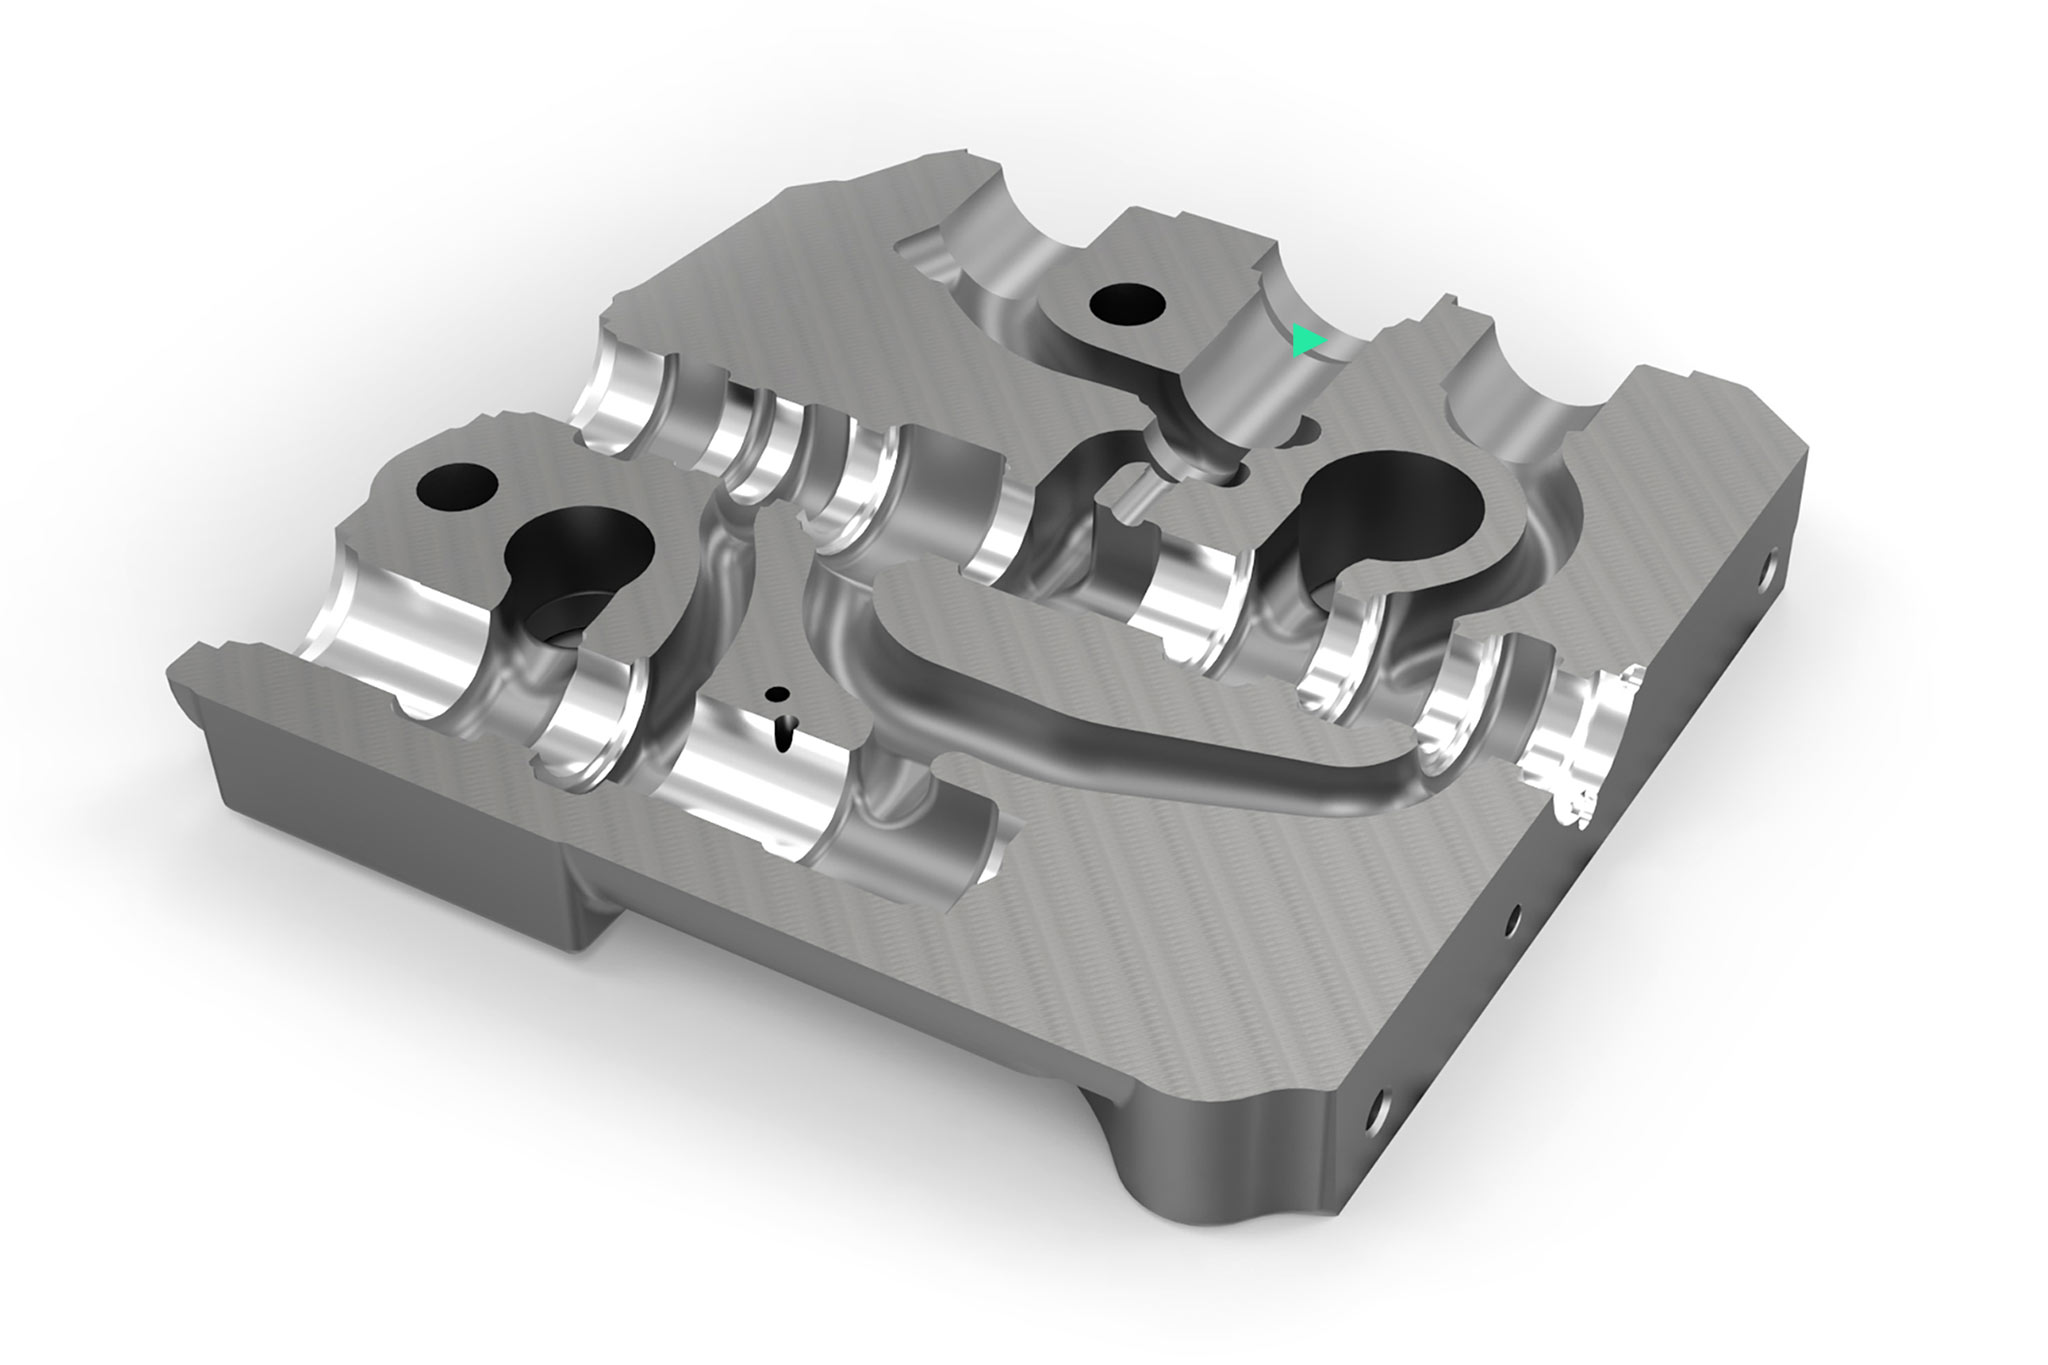
Corpo valvola idraulica
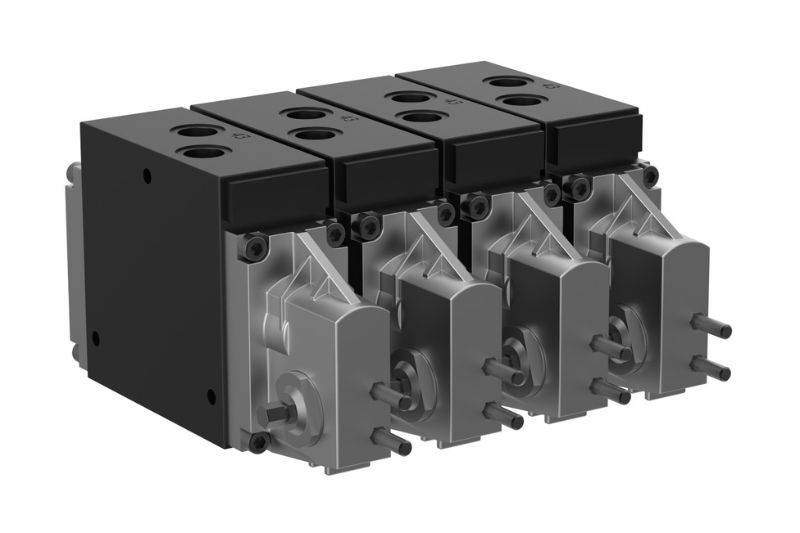
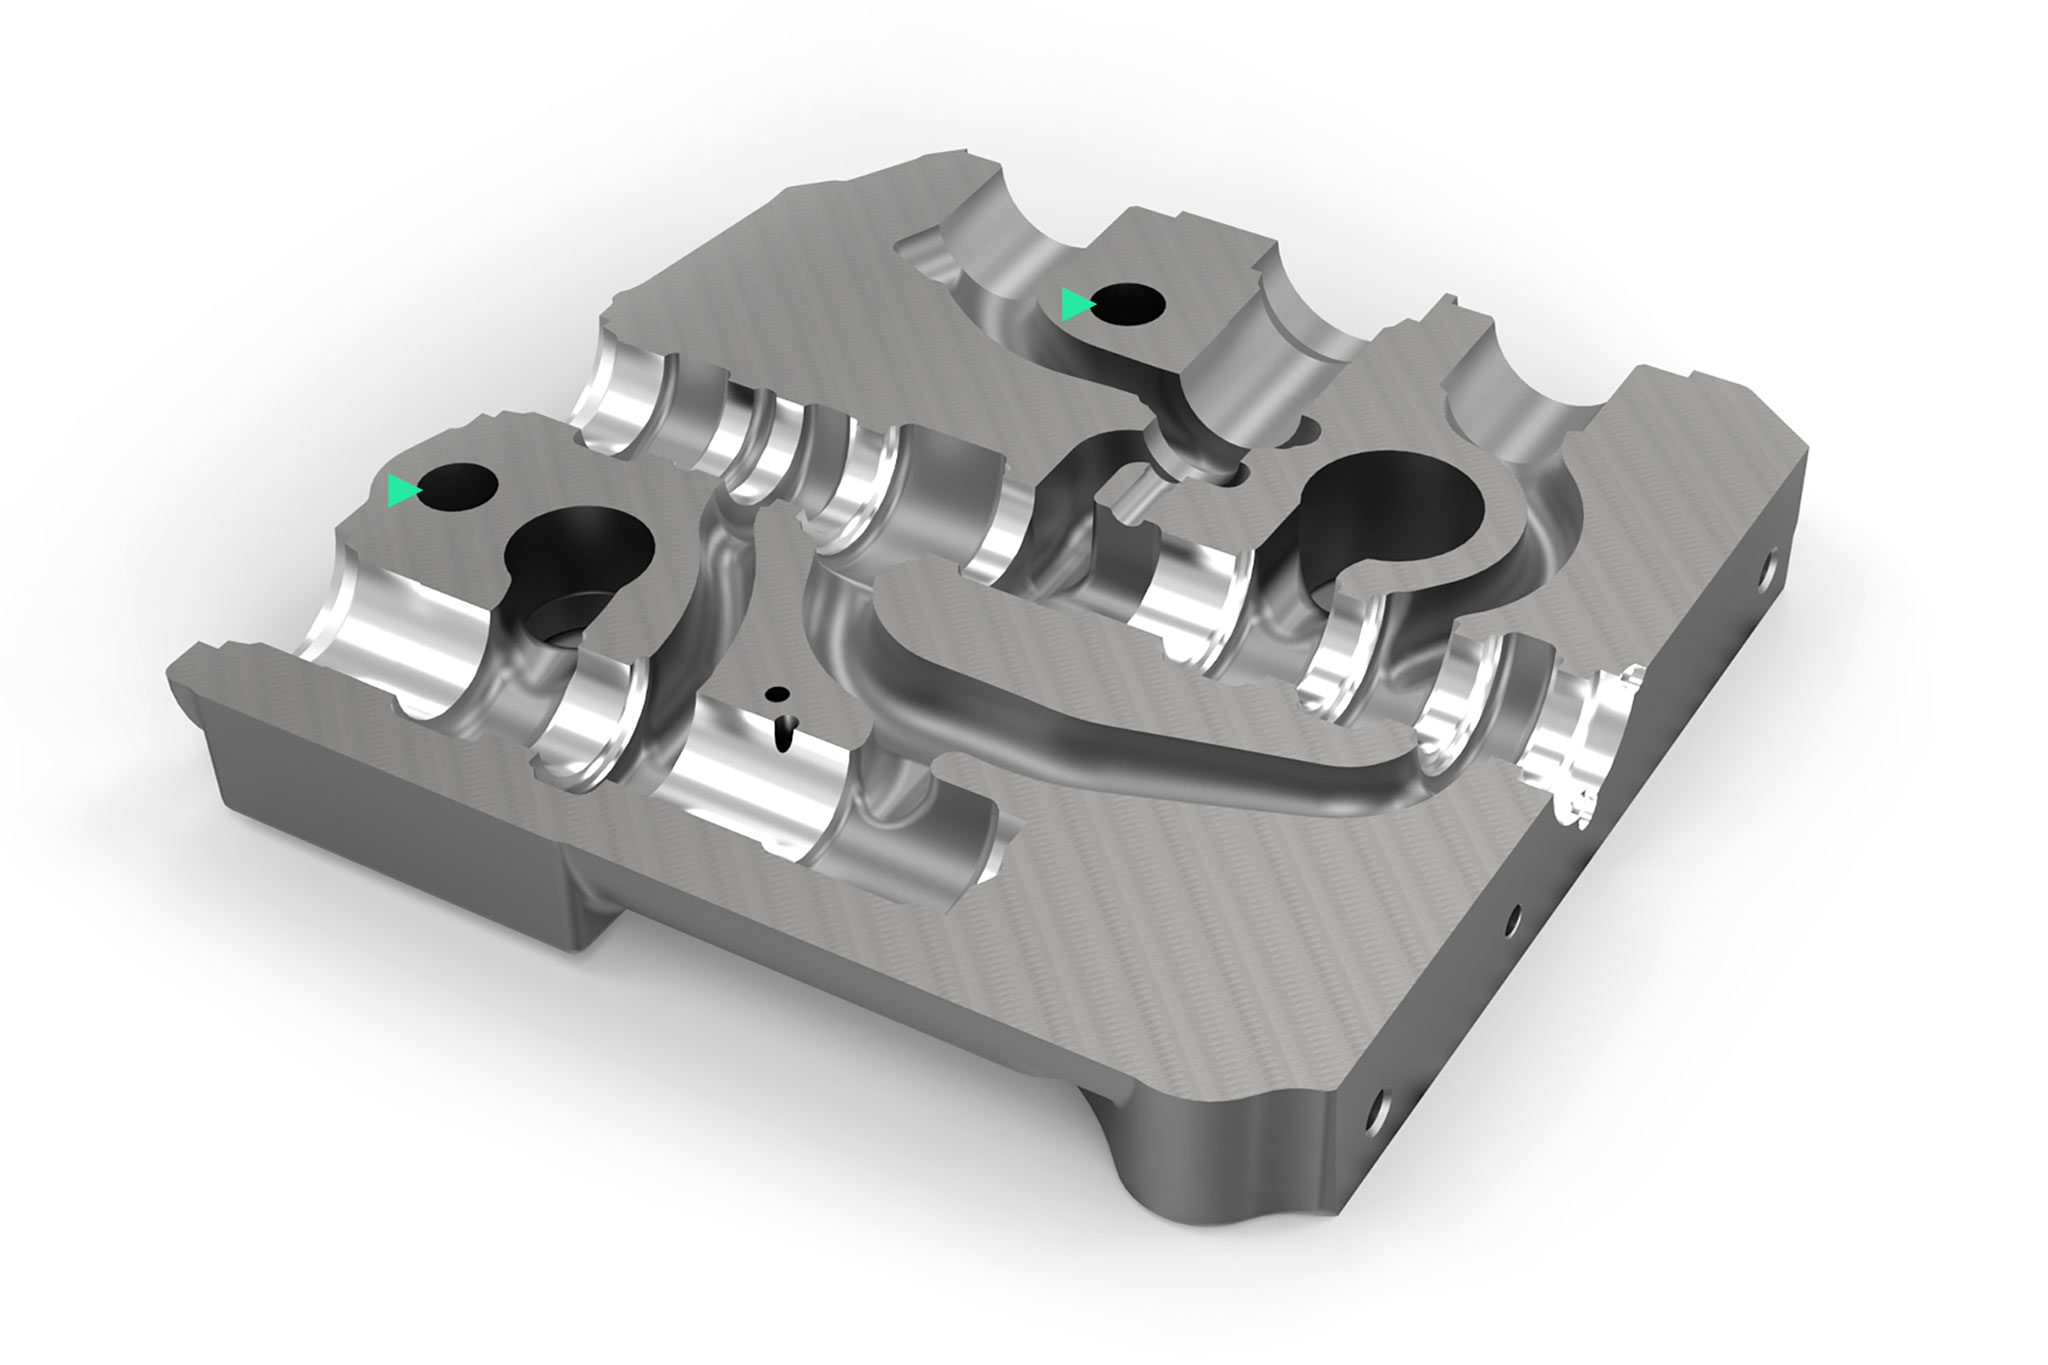
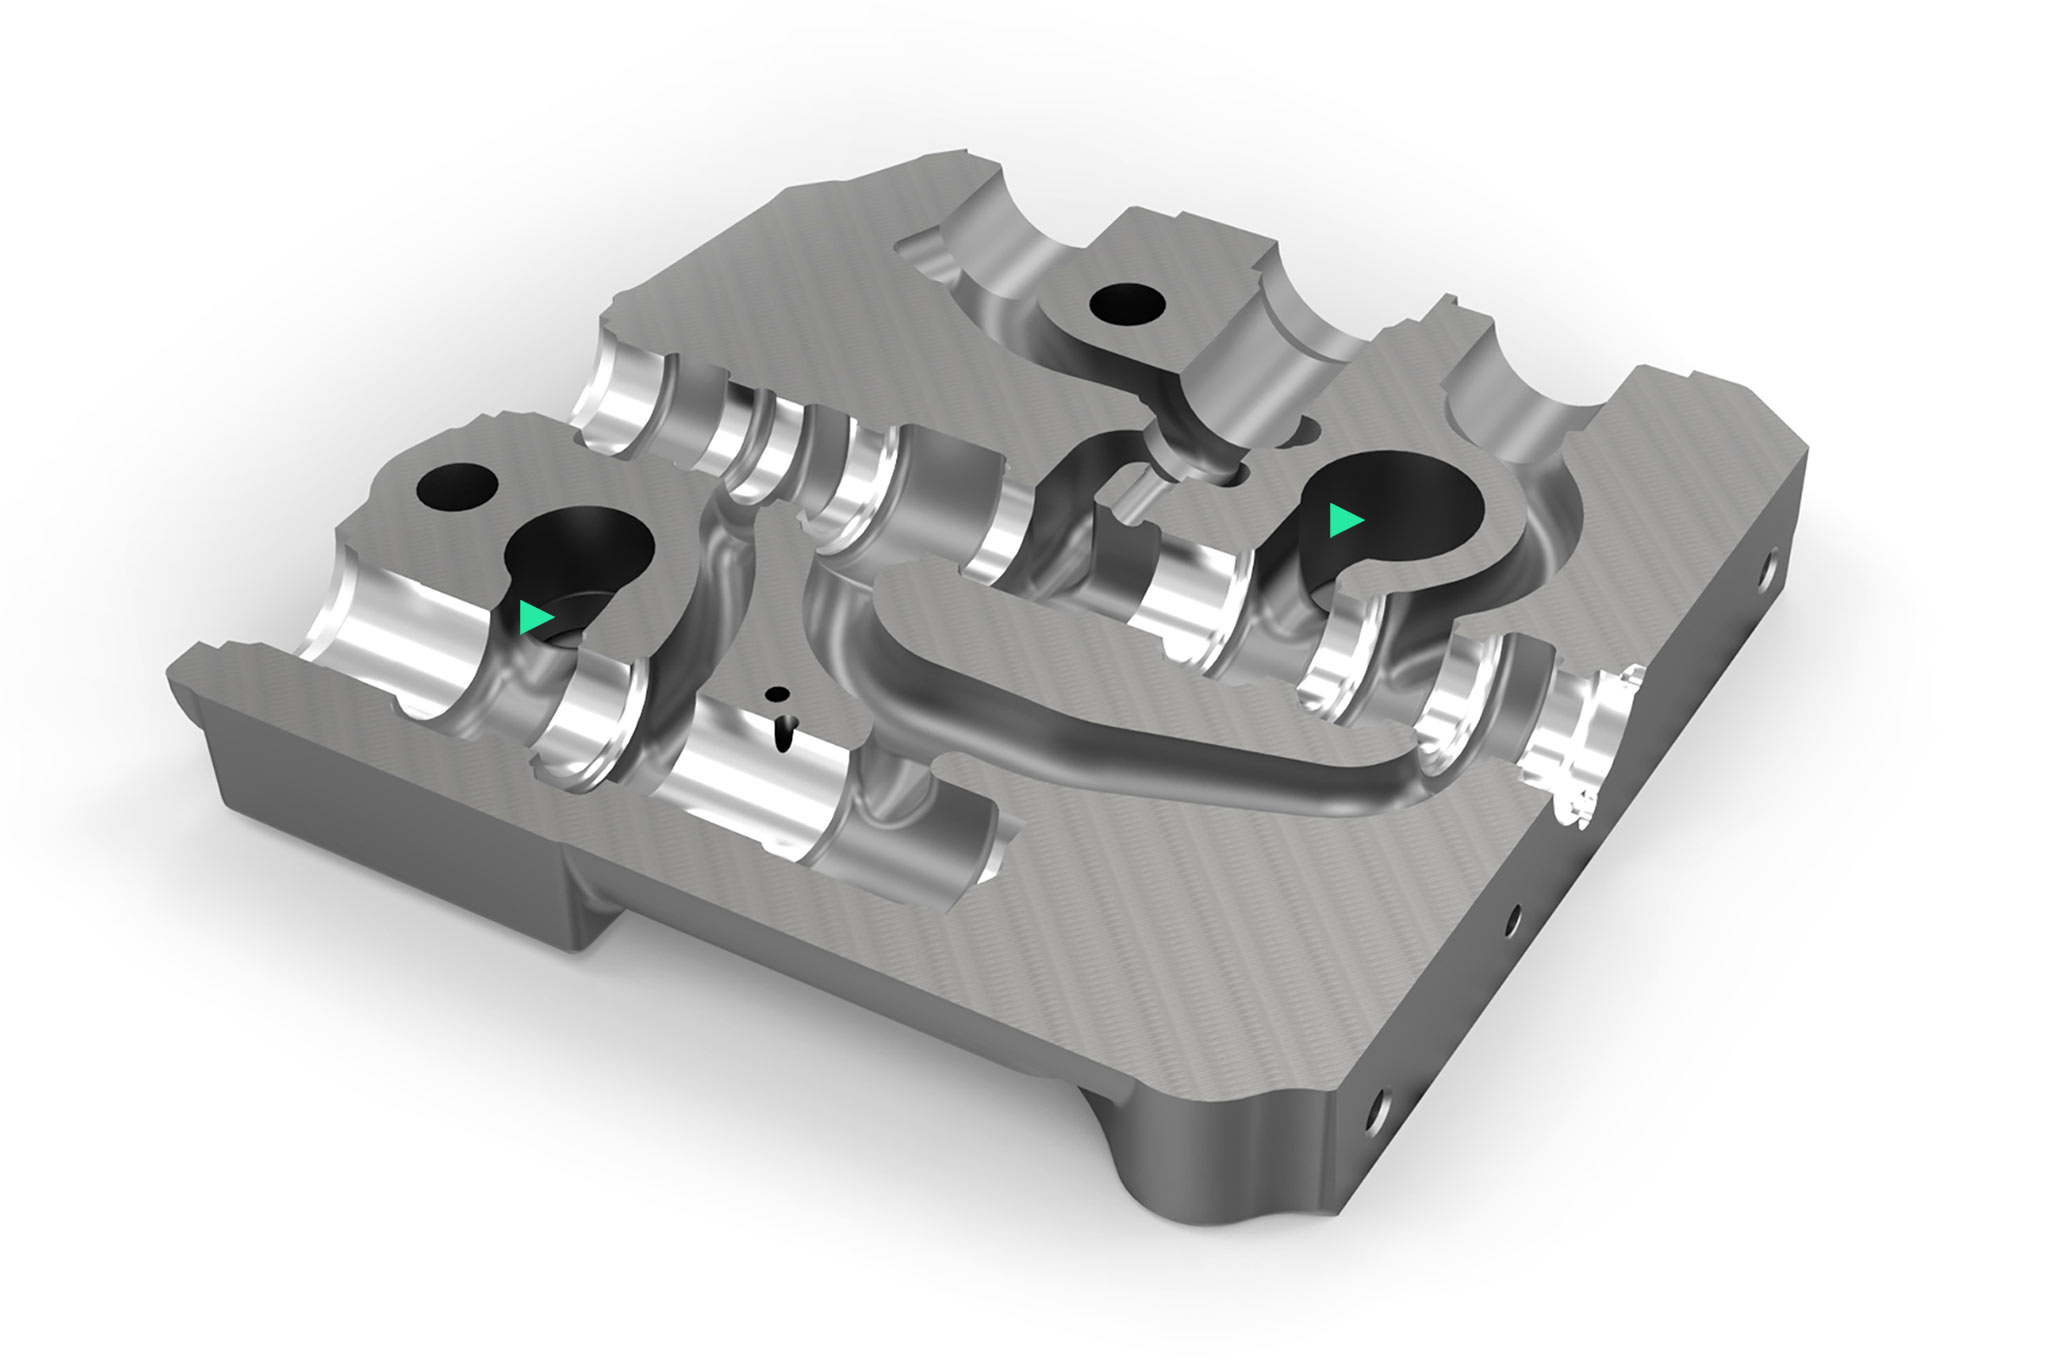
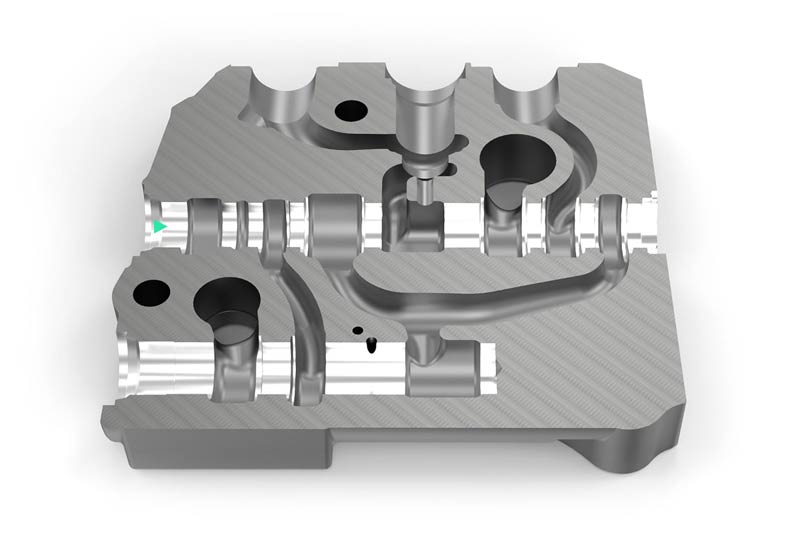
Everything depends on the main bore. Manufacturing valve housings is the supreme discipline in the world of fluid power. For years, MAPAL’s expertise has been in demand for the spool bore. The gap dimension with the spool depends on the accuracy of this bore, so that the hydraulic oil can only flow in the required direction without leaking. This is very narrowly defined in modern hydraulic valves. The roundness, cylindrical form, straightness and surface finish of this bore are therefore crucial.
Valve block

Machining requirements

  • Fluctuating cast allowance situation
  • Heavily interrupted cuts
  • Avoid ring formation during boring and ensure safe chip removal from the housing
  • Avoid macroscopic flaws on the control edges in the boring process
  • Very high demands on form and position tolerance
  • Constant stock removal before honing
  • Take part variance and limited tool storage places in the machining concept into account

Control valves

Control valves are mechanically or electronically actuated valves with several switch positions. Depending on the specified position of the spool along the control edges, a volume flow is set for operating the connected working equipment. The individual pressure compensator adjusts a constant load pressure drop via the supply control edge of the spool, so that a load pressure-independent volume flow control is achieved across the whole adjusting range, also in parallel operation (load compensation). The system must be leakage-free, to prevent accidental dropping of the load, even with parallel operation.

Bore machining
Application solutions

1 – Small and medium series with fixed tools

Initial situation at the customer

MAPAL Application solution 1

Valve housing EN-GJS-400-15 – spool bore

  • Individual orders, smaller and medium quantities
  • No option for tool setting
  • Short cycle times required
  • High machine hourly rates
  • Stable oscillating honing available
  • Tool concept adapted to several part versions
2 – Large series with solid and adjustable tools

お客様の初期の加工状況

MAPAL Application solution 2

バルブケース EN-GJS-400-15 - スプール穴と流量制御穴

  • 量産
  • ツール設定が必要
  • 高い機械稼働率
  • 次工程のワンパスホーニングによる高い費用の発生

3 – 少量生産 – コンビネーションツールによる工具交換の削減

お客様の初期の加工状況

MAPAL Application solution 3

バルブケース FCD-300 - スプール穴

  • 少量生産
  • ツール調整機能あり
  • 過度なツール交換
  • 高い機械稼働率
  • 次工程のワンパスホーニングによる高い費用の発生

4 – マシニングセンターでの柔軟なホーニング

Ausgangssituation beim Kunden

MAPAL Anwendungslösung 4

Ventilgehäuse EN-GJS-400-15 – Druckwaagenbohrung / Honbearbeitung

  • Anforderung zur Reduzierung der Nebenkosten
  • Bestehendes BAZ auf TOOLTRONIC umgerüstet
  • Honbearbeitung bei Prototypen-Bau, sowie Klein- und Mittelserie
  • Anforderung zur Einsparung des Honprozesses auf separater Maschine

5 – Toolmanagement

Ausgangssituation beim Kunden

MAPAL Toolmanagement

Ventilgehäuse EN-GJS-400-15 – Komplettbearbeitung

  • Hohe Lagerbestände
  • Prozessabläufe im Einstellraum nicht optimal und unvollständige Datenqualität
  • Kostentransparenz nicht ausreichend
  • Hohe Fluktuation aufgrund von allgemeinem Fachkräftemangel
  • Probleme mit Werkzeugbrüchen
  • Hohe Werkzeugkosten

ツールソリューション

パイロット加工とボーリング
  • Pilotieren

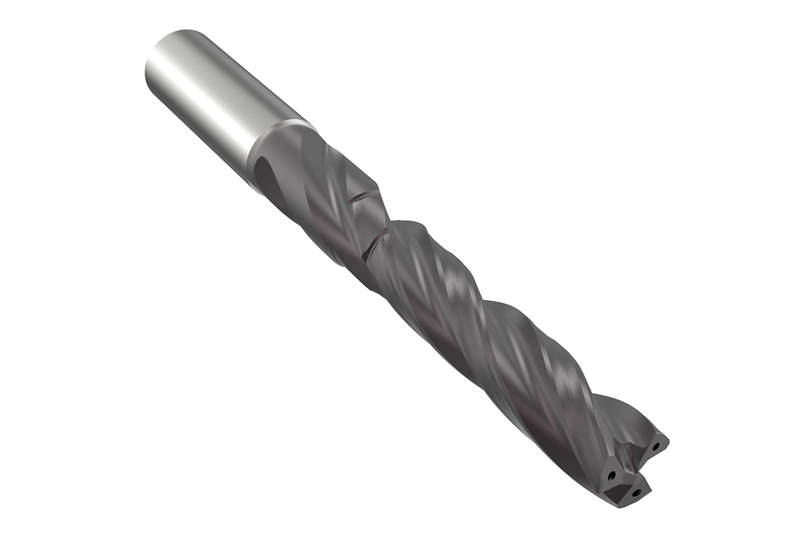
    超硬ソリッドボーリング工具

    • 優れた真円度と真直度を実現するための6つのガイドマージン
    • 多刃ツールの技術と適切なクーラント供給により最適な切り屑の流れを実現 

  • Boring

    超硬ソリッドボーリング工具

    • 3枚刃の切れ刃、6つのガイドマージン、特殊なリード形状
    • ストレート穴、加工穴全長にわたって理想的な切り屑の流れとガイドを実現。 

  • Boring

    超硬ソリッドボーリング工具

    • 6つのガイドマージン、特殊なリード形状
    • ストレート穴、加工穴全長にわたって理想的な切り屑の流れとガイドを実現。 
    • 1つの工具で2つの加工を行うことによる生産外時間の短縮

  • Piloting and boring

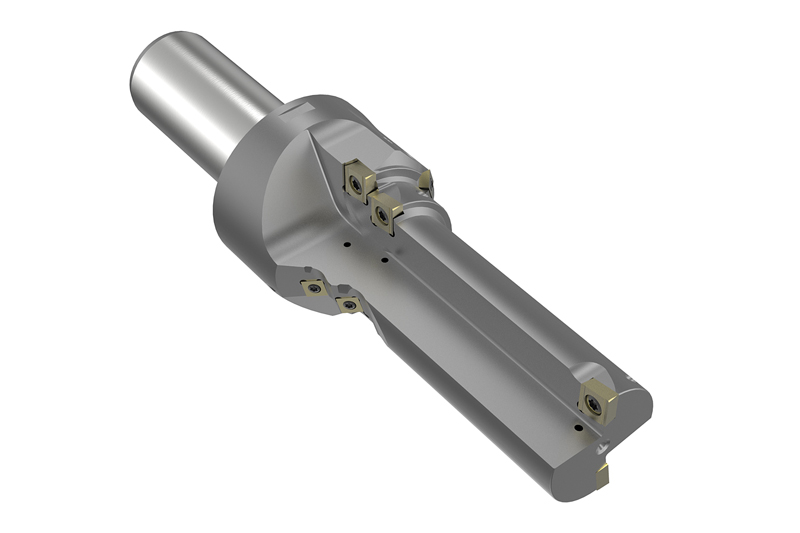
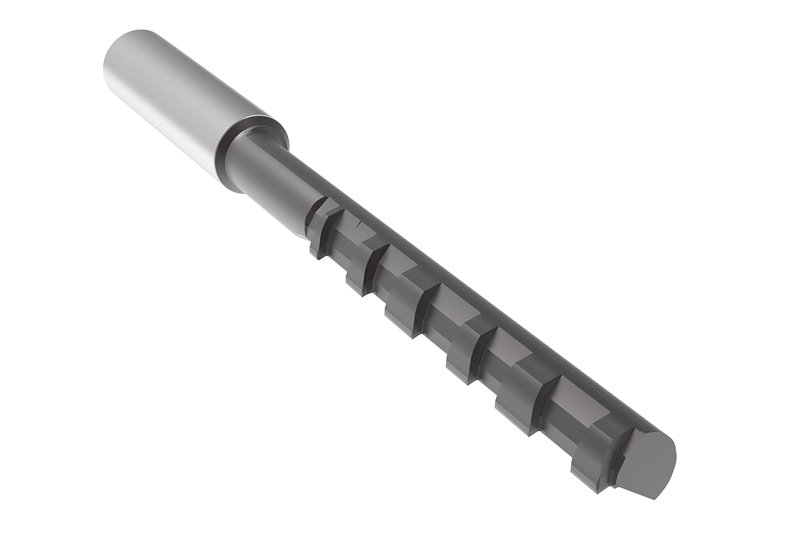
    多段式ガンボーリング工具

    • ラジアルおよびタンジェンシャルインサート
    • スプール穴の前加工と形状の仕上げを一度に行うことが可能

  • MAPAL Boring

    2枚刃ガンボーリング工具

    • 精密成型
    • 信頼性の高い形状加工
    • 容易な取り扱いで、工具材料費を低減

コントロールエッジ加工
  • Steuerkantenbearbeitung

    VHM-Zirkularfäser

    • Erhebliche Taktzeiteinsparung
    • Definierte Steuerkanten ohne Ausbrüche

  • Steuerkantenbearbeitung

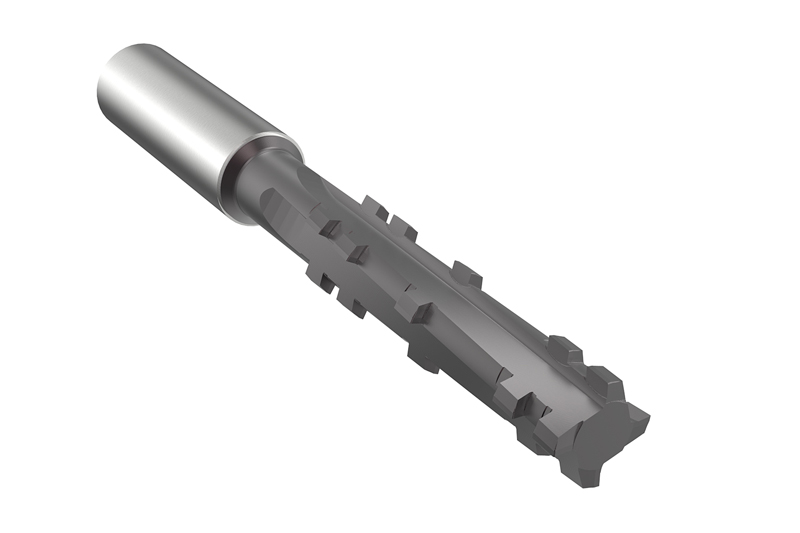
    VHM-Profilwerkzeug

    • Höchste Genauigkeit und Oberflächengüte der Steuerkanten
    • Definierte Steuerkanten ohne Ausbrüche

Reiben und Feinbohren
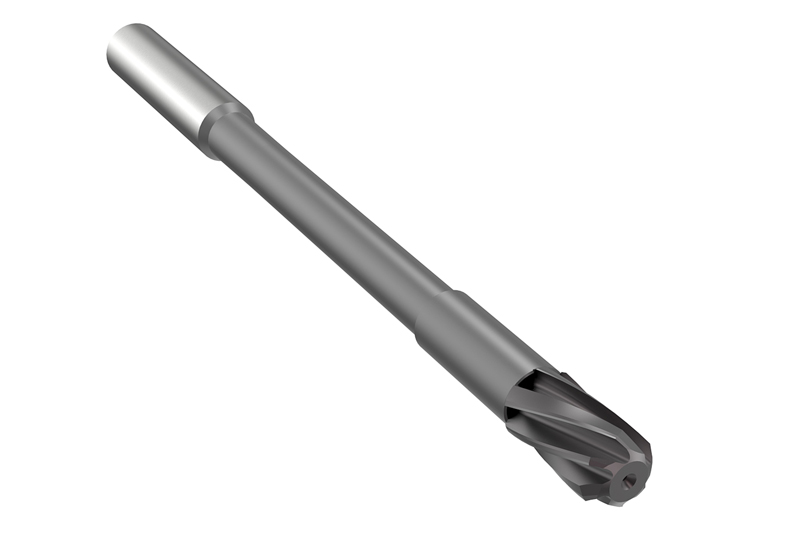
  • Reaming

    Multi-bladed reamer

    • High cutting data
    • Perfect chip control due to left-hand twist and optimum coolant supply

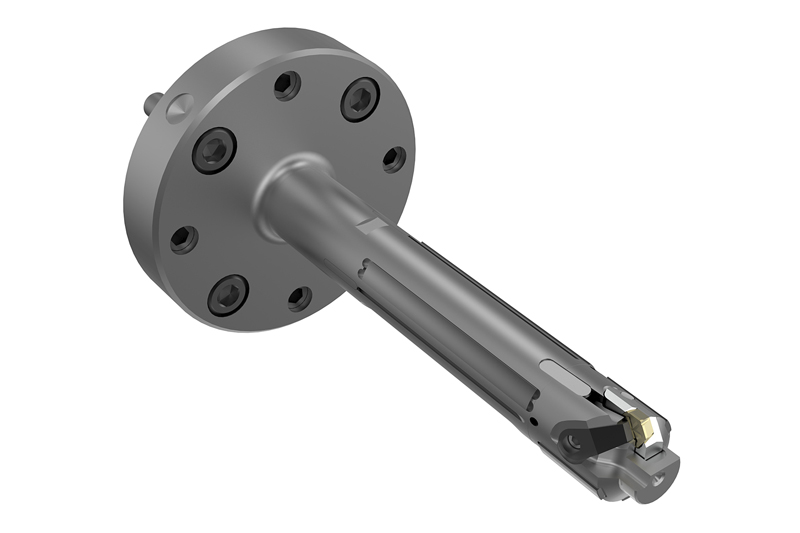
  • Fine boring

    Fine boring tool

    • EasyAdjust system and guide pads
    • Reliable precision machining with easy handling without subsequent honing
    • Best cylindrical forms due to optimum guidance

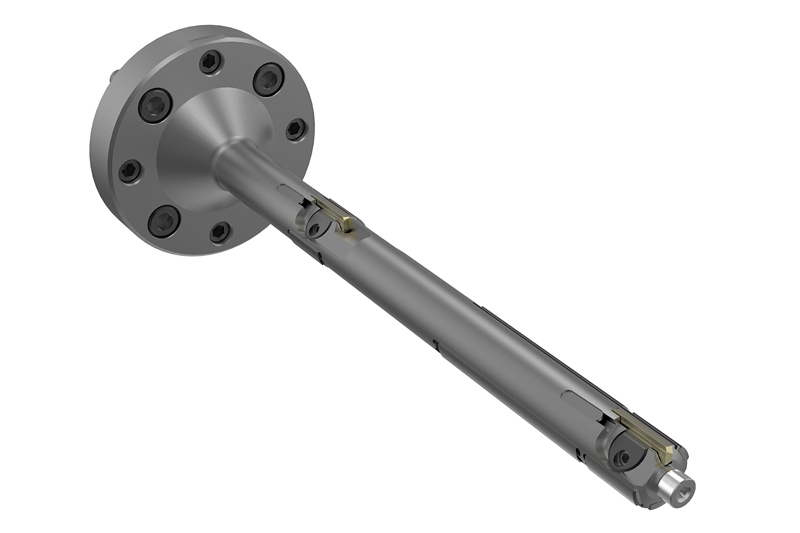
  • Fine boring

    Fine boring tool

    • Indexable inserts and guide pads
    • Ideal for bar machining of highly accurate and long bores

ホーニングによる仕上げ
  • MAPAL TOOLTRONIC

    • 生産時間、リードタイムの大幅な短縮を実現
    • 高い形状精度

ミーリング加工
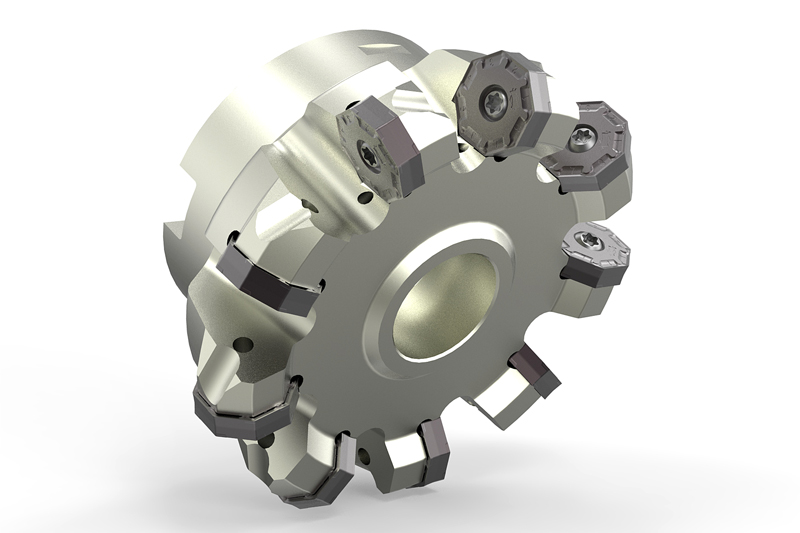
  • NeoMill-16-Face

    NeoMill®-16-Face

    • 16枚刃刃先交換式インサート/45°
    • 鋳鉄、耐熱鋳鋼での第1選択
    • ø-範囲 63~200mm/ap最大4mm
    • ネガ形状でも低い加工負荷
    • フェースミリングでの最高のコスト削減効果

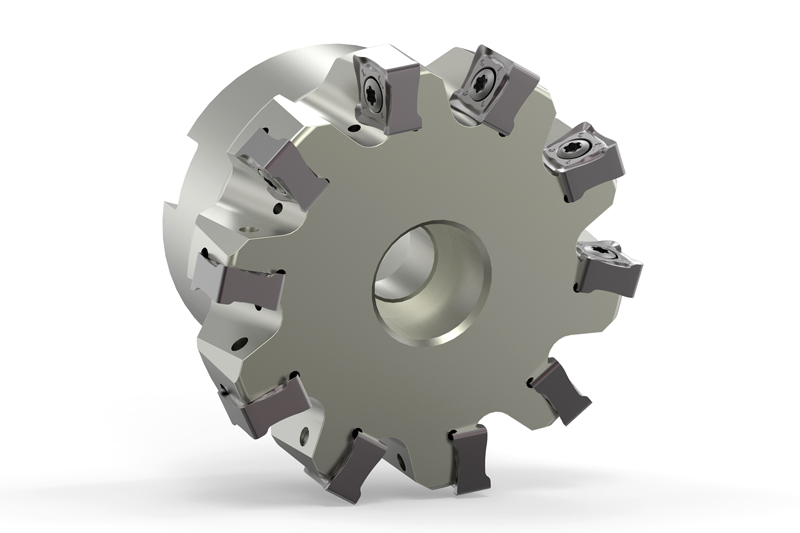
  • NEOMILL-8-CORNER

    NeoMill®-8-Corner

    • 8枚刃刃先交換式インサート/90°
    • 鋳鉄での第1選択
    • ø-範囲 50~200mm/ap最大8mm
    • コーナーミルの最高のコスト削減効果

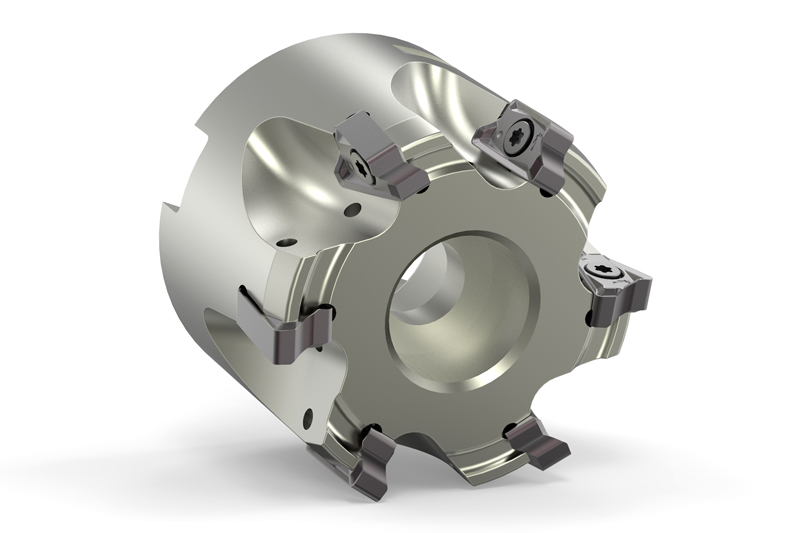
  • NEOMILL-4-CORNER

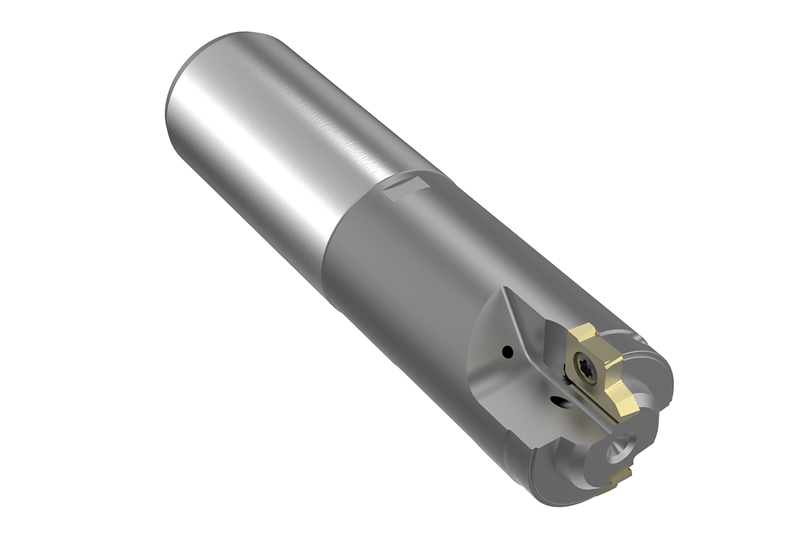
    NeoMill®-4-Corner

    • 4枚刃刃先交換式インサート/90°
    • 鉄鋼、ステンレス、鋳鉄、耐熱鋳鋼に最適
    • ø-範囲 25~200mm/ap最大10mm
    • 大きな高さ寸法の肩削りが可能
    • ネガ形状でも非常に低い加工負荷

クランプ
  • UNIQ Mill Chuck

    UNIQ Mill Chuck

    • 非常に長いミーリングサイクル(240分以上)でも80℃の高い耐熱性
    • 最大33,000rpmの高性能ミーリング加工
    • 最高の工程信頼性

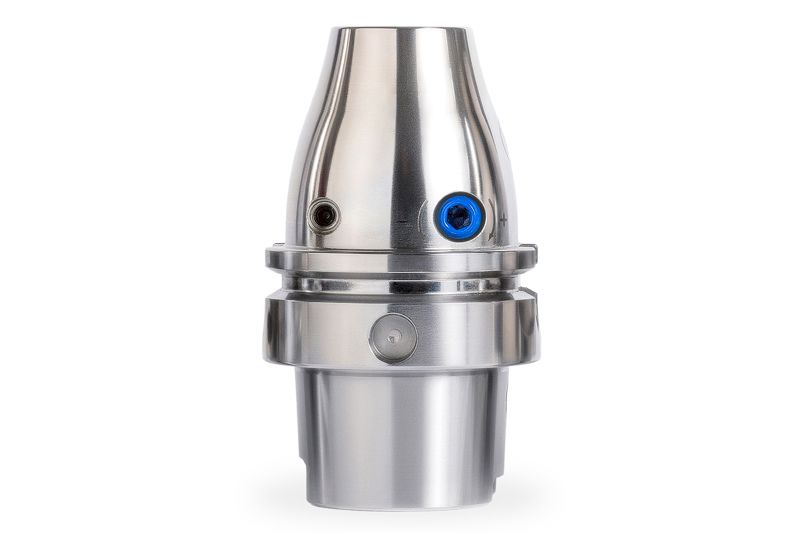
  • UNIQ DReaM CHUCK 4.5°

    UNIQ DReaM Chuck, 4.5°

    • シュリンキングチャック (4.5°のDIN輪郭)の原寸のハイドロチャック
    • アプリケーション指向のシステム設計
    • 最大限の工程信頼性と工具寿命
    • 高速・高精度なツール交換

  • HB MILL CHUCK SIDE LOCK CHUCK

    HBサーフェスチャック MILL CHUCK

    • デファレンシャルスクリューによる簡単な操作
    • 最高のコスト削減効果と精度
    • スプリングシステムにより設定された軸方向ツール位置決め
    • コントロールエッジ加工におけるプロファイルツールの最適な位置決め