Innowacyjna obróbka wstępna elementów hydraulicznych
Dzięki wydajnym wiertłom pilotującym i pogłębiaczom
MAPAL rozszerza swoje portfolio o wydajne rozwiązania narzędziowe do wiercenia otworów w suwakach.
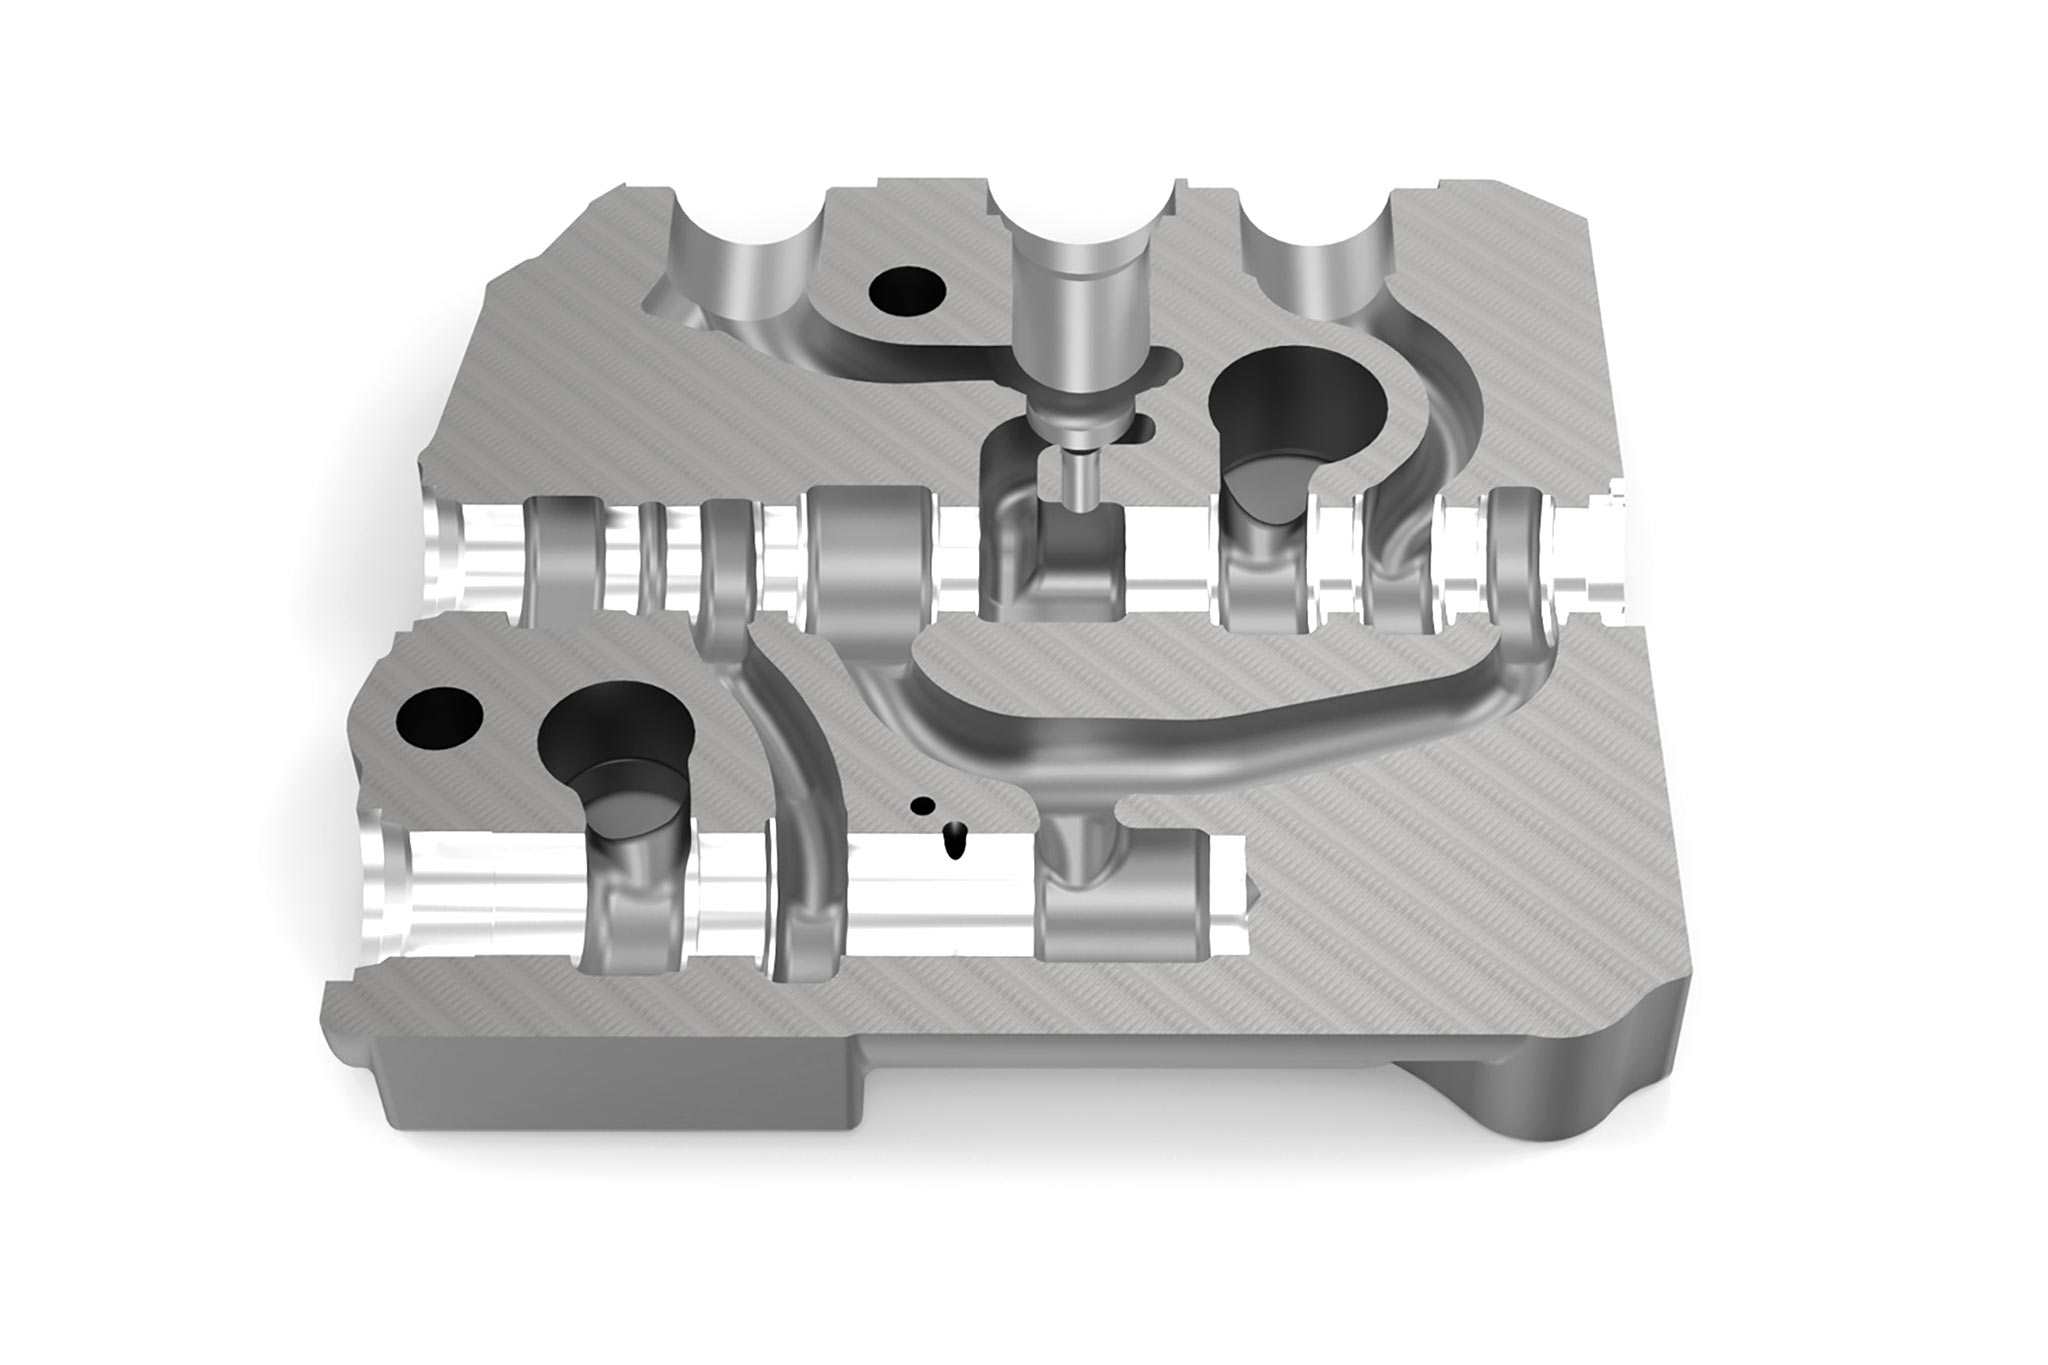
Otwór zaworu suwakowego jest centralnym elementem komponentów hydraulicznych, takich jak obudowy zaworów
lub pompy tłokowe osiowe. Ich obróbka wykończeniowa za pomocą narzędzi do rozwiercania precyzyjnego
od zawsze należy do podstawowych kompetencji firmy MAPAL. Dzięki nowym rozwiązaniom narzędziowym do obróbki wstępnej
specjalista w dziedzinie narzędzi umacnia swoją pozycję jako kompleksowy partner technologiczny. Klienci korzystają z kompletnej koncepcji obróbki z jednej ręki – od pilotowania
po obróbkę precyzyjną.
lub pompy tłokowe osiowe. Ich obróbka wykończeniowa za pomocą narzędzi do rozwiercania precyzyjnego
od zawsze należy do podstawowych kompetencji firmy MAPAL. Dzięki nowym rozwiązaniom narzędziowym do obróbki wstępnej
specjalista w dziedzinie narzędzi umacnia swoją pozycję jako kompleksowy partner technologiczny. Klienci korzystają z kompletnej koncepcji obróbki z jednej ręki – od pilotowania
po obróbkę precyzyjną.
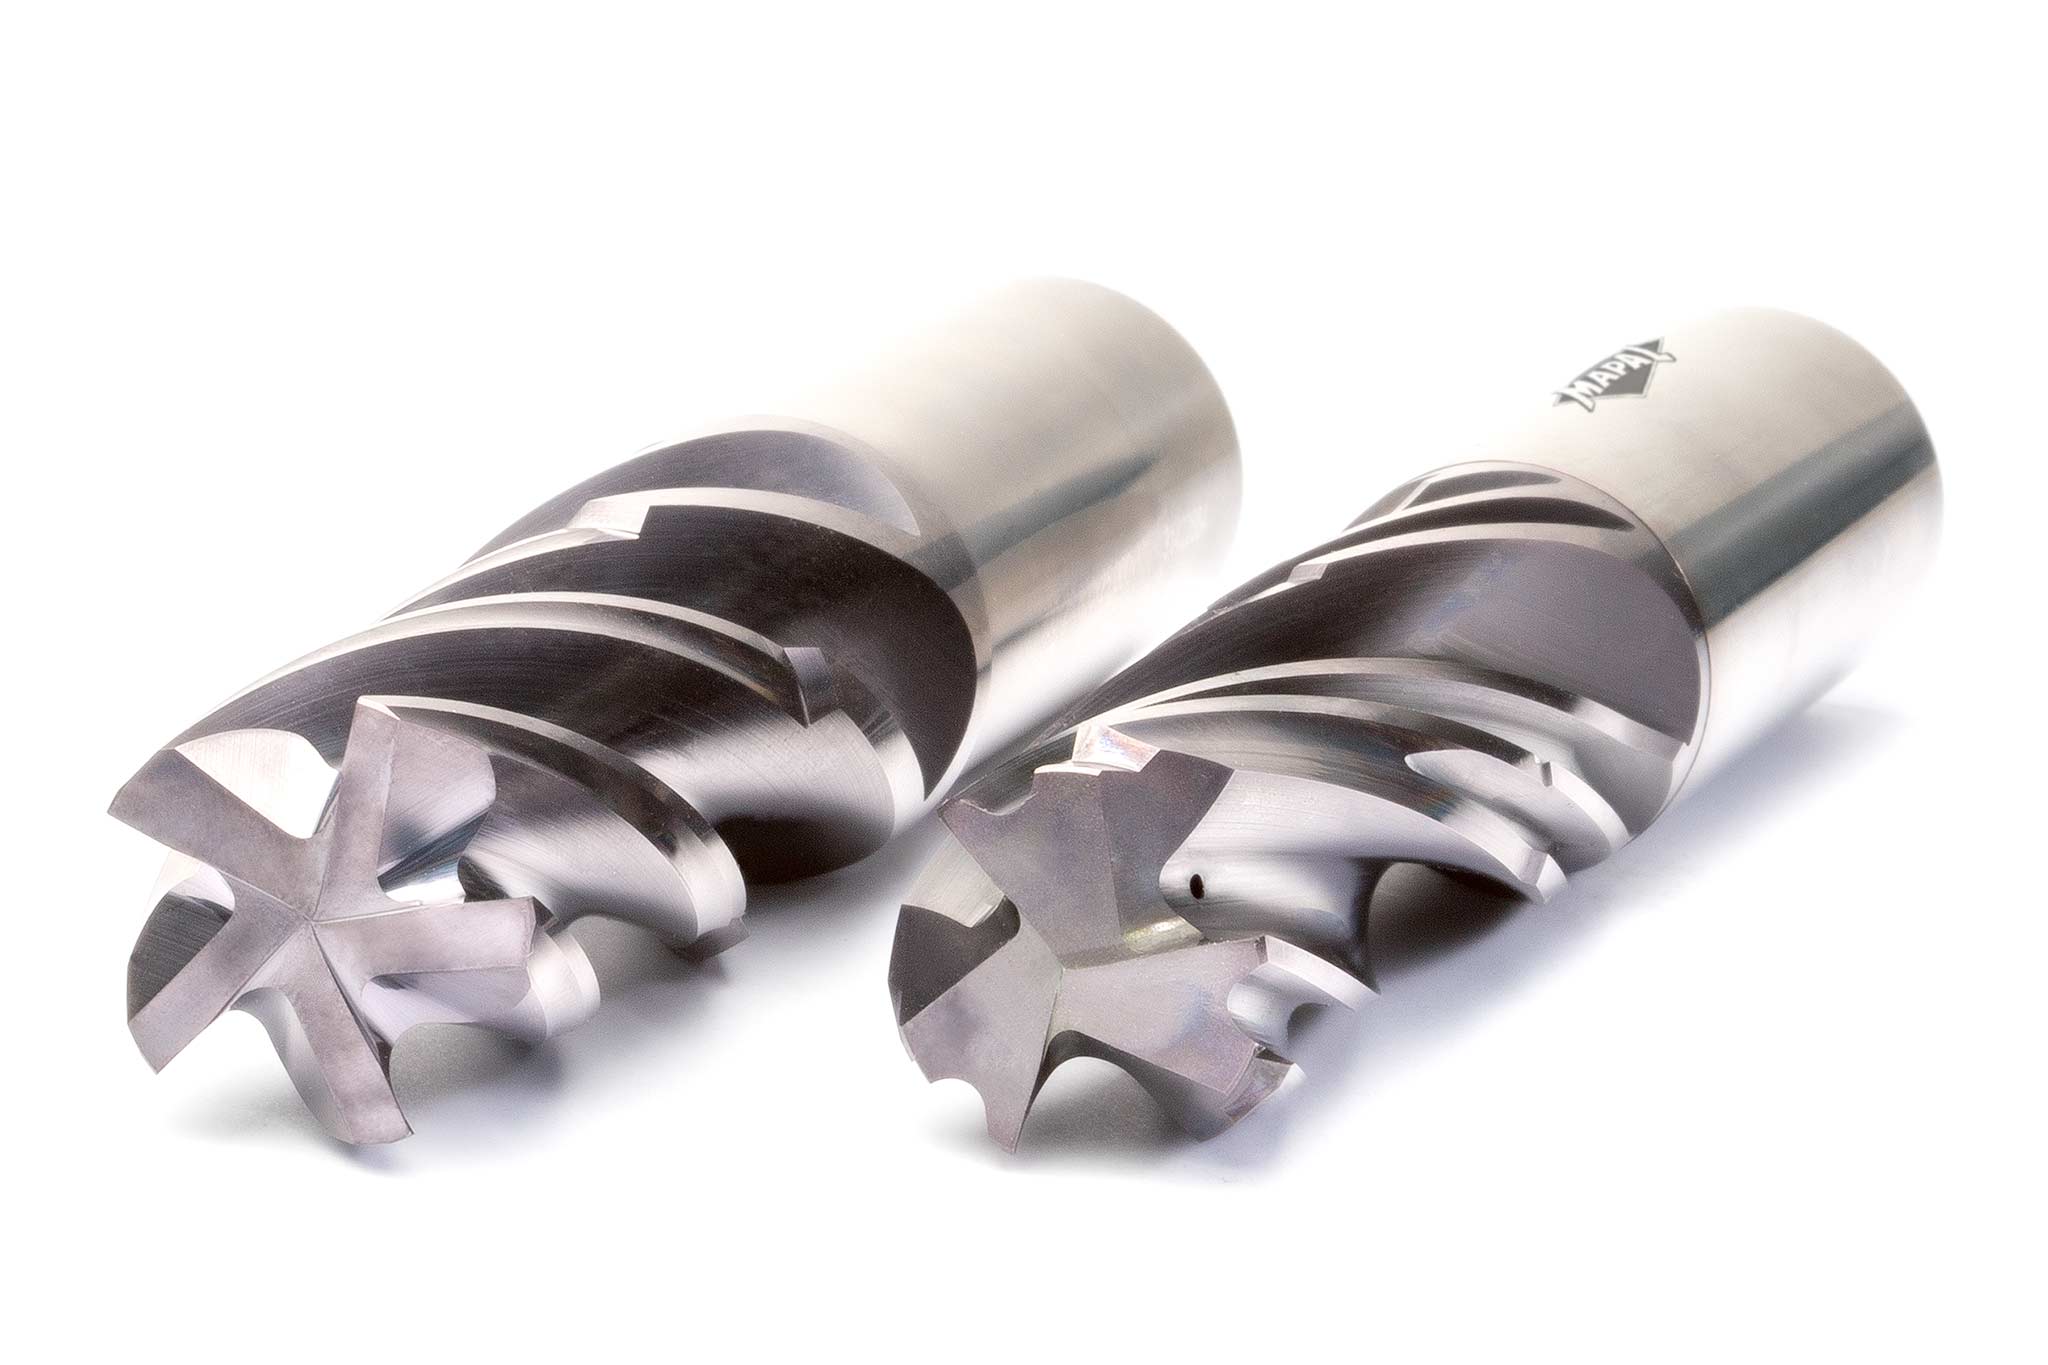
La atención se centra en dos herramientas recientemente desarrolladas: La broca piloto con tres o cinco insertos para diferentes tipos de fundición permite realizar una perforación piloto eficiente y muy económica, lo que reduce las operaciones y evita el cambio de herramientas. Mientras que la fresa de tres filos se utiliza con piezas brutas estables, la fresa de cinco filos destaca en condiciones de fundición inestables por sus resultados precisos en avances elevados.
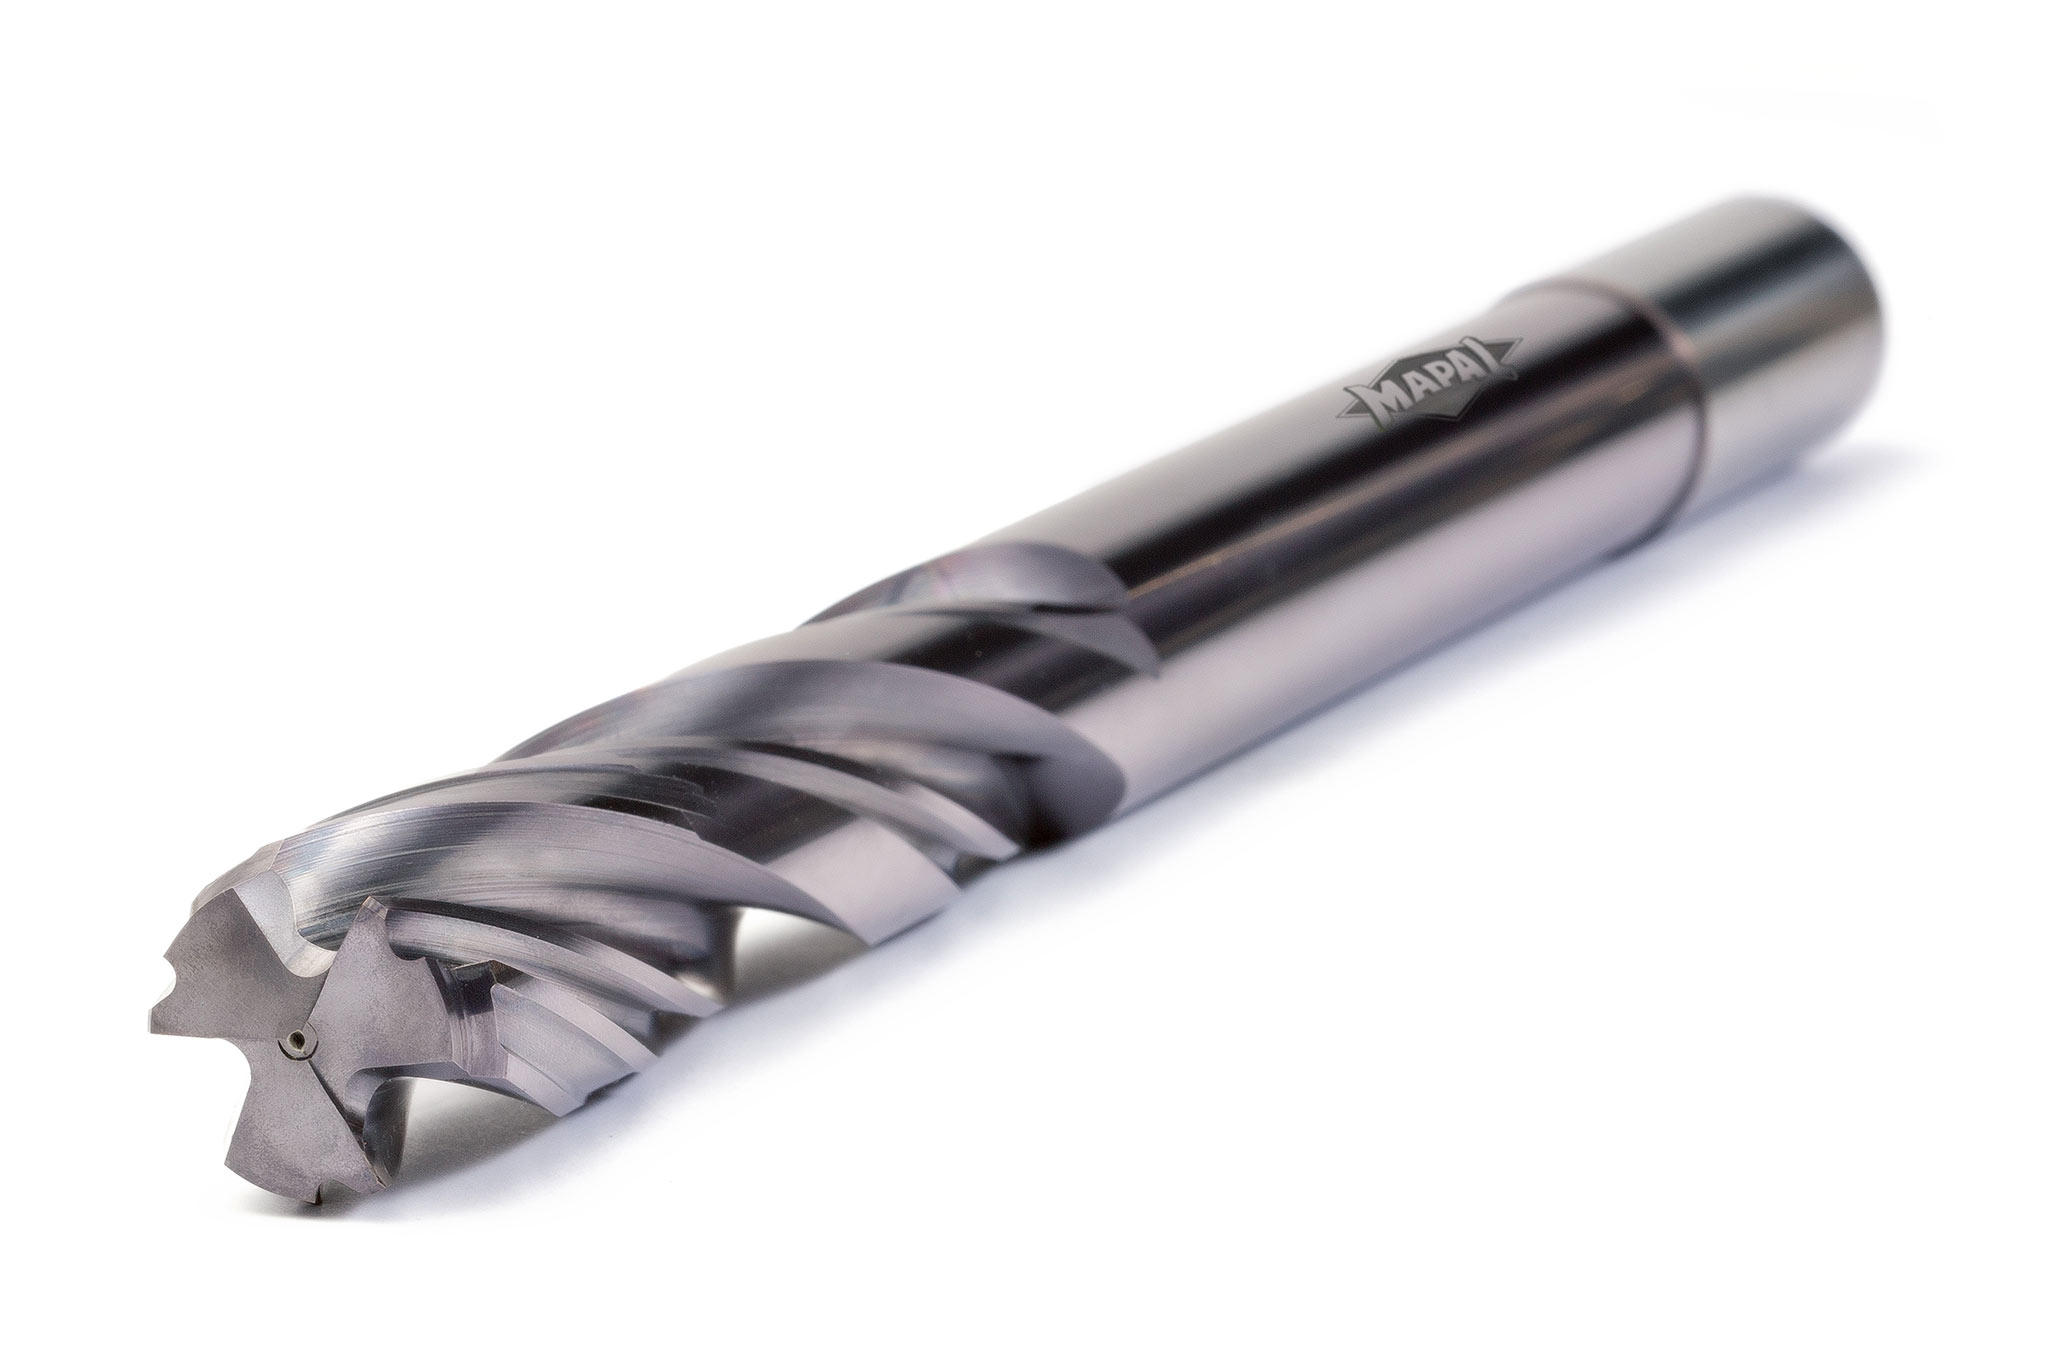
La herramienta de barrenado integral de metal duro macizo con tres filos se basa, al igual que la broca piloto de tres filos, en la tecnología de biselado múltiple patentada de MAPAL. Esto garantiza una separación limpia de las virutas y evita que se formen remolinos durante su eliminación, incluso con profundidades de taladrado de hasta 10xD. Una refrigeración interior dirigida permite vidas útiles largas y eleva adicionalmente la seguridad de proceso.
Both tools are optimally tailored towards subsequent fine machining. Coordinated processes,
reduced scrap rates and maximum cost-effectiveness help create innovative solutions for fluid power – with measurable added value for the customer.
reduced scrap rates and maximum cost-effectiveness help create innovative solutions for fluid power – with measurable added value for the customer.