
全刃PCD - 胜任严苛要求 的航空零部件加工
现代飞机和直升飞机大部分使用铝合金或复合材料制成的零件,或者是这些材料组合成的材料。这样的材料的使用主要是为了预防材料疲劳,同时确保机身整体重量更轻。在飞机零部件的切削加工中,主要的焦点首先在于工艺的安全性。MAPAL公司的PCD刀具(聚晶金刚石)在很大程度上完全满足了这些要求,并且由于其长的使用寿命和极佳的加工效果而使得用户极其信服。
在钻削复合材料时,刀具寿命延长了60 %
在飞机制造中,由于复杂的装配过程需要在结构部件和复合材料上钻削上千个用于铆接的孔。这些加工通常使用带有金刚石涂层的整体硬质合金钻头。然而, 整体硬质合金钻头并不适用于特殊应用。特别在使用寿命、过程安全和钻孔质量上有特别高的要求时,相应对刀具也有进一步更高的要求。
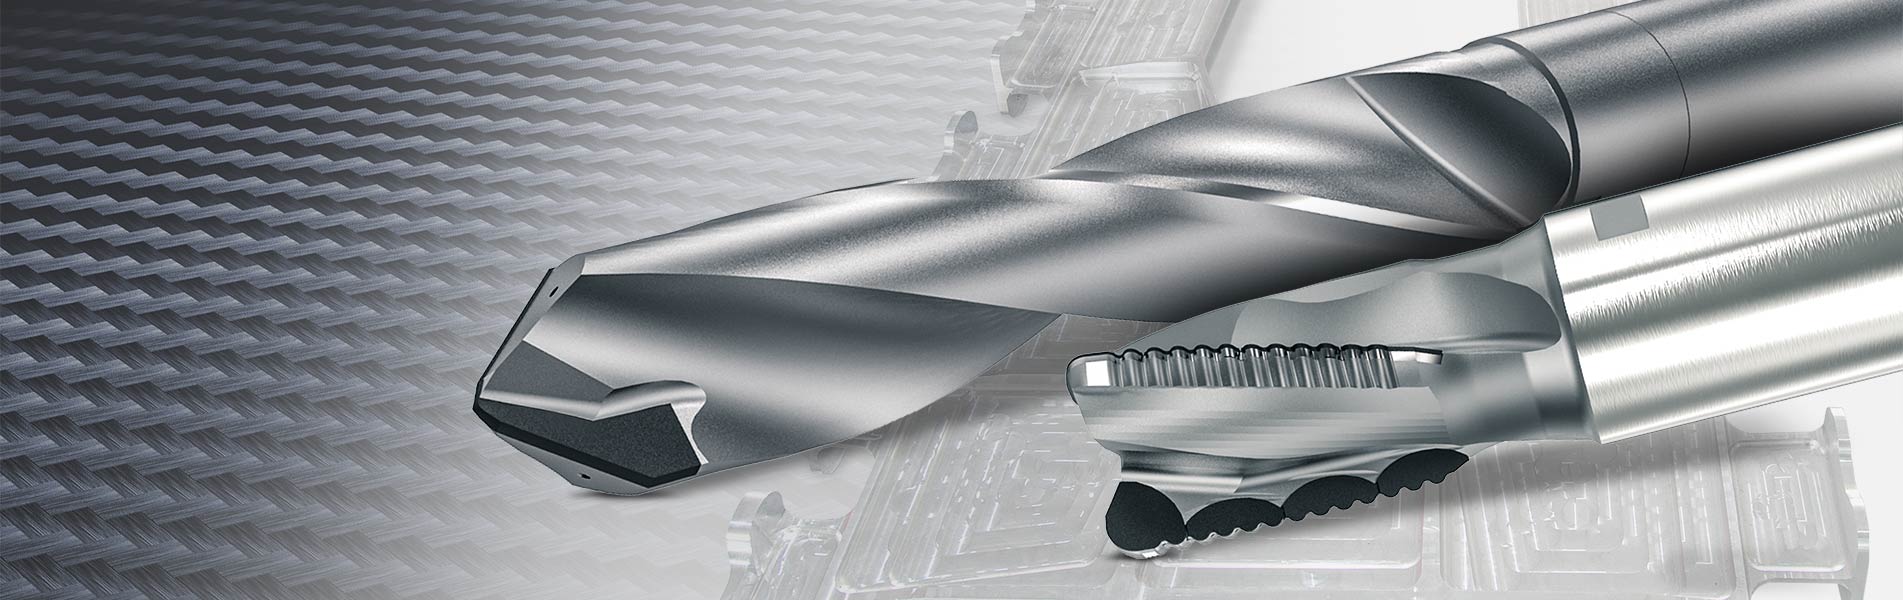
MAPAL公司对于复合材料的加工,特别开发了新型PCD钻头,用于诸如CKF(碳增强塑料)、铝和C F K的涂层的加工。该钻头主要由于它整体使用的P C D而著称。至今为止,大多数刀具在钻尖中心使用整体硬质合金,只有侧面为PCD。然而刀片材料的不连续使在此过渡处的不稳定性增加,同时钎焊缝隙也更容易破裂。MAPAL 公司在新推出的新型刀具上则消除了这种不稳定因素。
在开槽的整体硬质合金基体上插入双面抛光的PCD。由此使得整个系统稳定性得到极大提高。由于115°的钻尖刃角, 钻头具有非常好的自定心特性。80°的第二钻尖刃角确保钻孔无毛刺或脱层。
在用户应用过程中,该钻头不仅由于极高的工艺安全性令人印象深刻。同时由于其极长的使用寿命而大受用户欢迎。因此在直升飞机零件制造中,该刀具多用于螺栓孔的加工。该部件由 50 mm 厚的CFK制成。之前使用的刀具,在经过 50次钻孔后就已经达到了其使用寿命。而用户采用MAPAL公司直径为19 mm PCD钻头,不仅获得了更高的切削值,同时加工孔质量得到大幅提升,并实现了超过80次的钻孔次数 - 与仅在侧面装有 PCD刀片的刀具相比提高了60 % 。
PCD roughing cutter for dry machining
When machining the structural components of aircraft wings made of aluminium, a large portion of the existing material is removed by machining. For roughing the chambers or pockets inside the wing MAPAL has a solid carbide milling cutter, the OptiMill-SPM-Rough, in its portfolio, and this has already proven its performance many times over. However, this roughing cutter is only suitable for wet machining. Because: Solid carbide tools reach their limits when dry machining long-chipping aluminium alloys, such as those used in aircraft construction. Built-up edges quickly form, and the tools are subject to significant excessive wear.
There was an increasing demand for a tool for dry machining corresponding to the PCD-tipped milling cutter from MAPAL so that the chambers and pockets on the wing do not fill up with the cooling medium.
The geometry of the new milling cutter is in many ways identical to that of its solid carbide counterpart. The specially designed knurled roughing geometry ensures a soft cut and reduces process forces. It also gives the tool excellent plunging properties. The heat input into the component is minimal.
Due to the considerably longer tool life of the PCD tool when dry machining long-chipping aluminium alloys compared to that of its solid carbide counterpart, its use is significantly more economical. The higher tool costs are quickly amortised.
There was an increasing demand for a tool for dry machining corresponding to the PCD-tipped milling cutter from MAPAL so that the chambers and pockets on the wing do not fill up with the cooling medium.
The geometry of the new milling cutter is in many ways identical to that of its solid carbide counterpart. The specially designed knurled roughing geometry ensures a soft cut and reduces process forces. It also gives the tool excellent plunging properties. The heat input into the component is minimal.
Due to the considerably longer tool life of the PCD tool when dry machining long-chipping aluminium alloys compared to that of its solid carbide counterpart, its use is significantly more economical. The higher tool costs are quickly amortised.