
26.08.2025
Putting heads together for the last diesel engine
Fine boring tools from MAPAL for MAN diesel tools
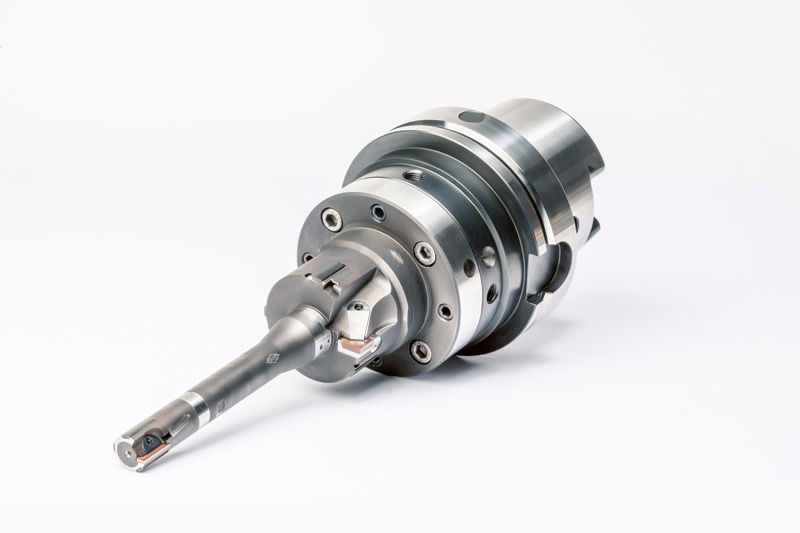
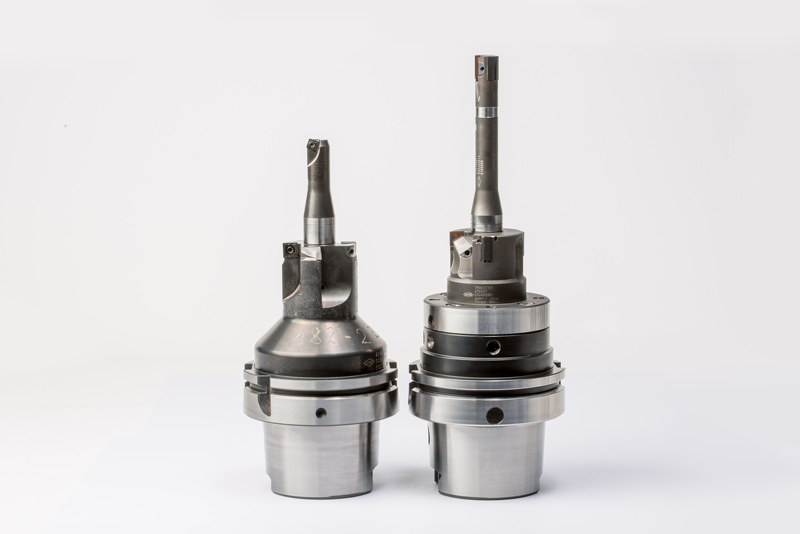
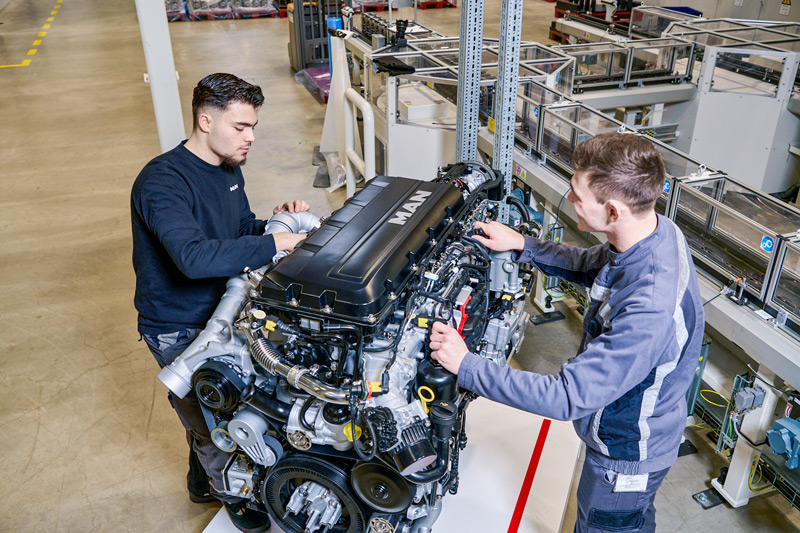
At commercial vehicle manufacturer MAN Truck & Bus’s Nuremberg plant, production of an ultra-efficient new 13-litre diesel engine has begun. As a joint engine platform, it is intended for use across the group. Fine boring tools from MAPAL are used for the cylinder heads. These machine valve guide and valve seat blind bores.

An engine for all brands
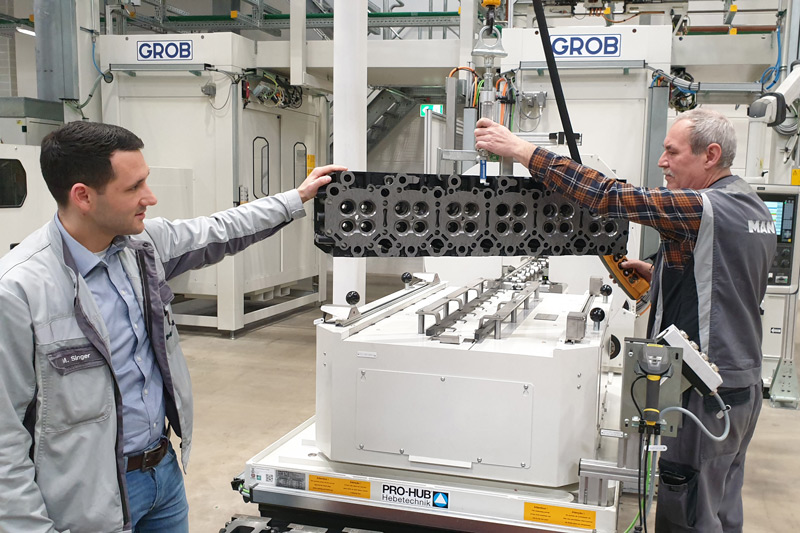
MAN has invested around EUR 220 million in the production of the new engine, which will see up to 160 highly qualified employees work in three-shift operation. Technical capacity enables production of around 50,000 engines per year. “The actual production volume is based on demand. Whether this is used to its full potential is ultimately decided by the customers”, says Singer. They have been somewhat reserved in recent years. For commercial vehicles, like for passenger cars, discussions on the shift to the electric drive have also caused uncertainty. As production starts up, work will initially be carried out in one shift.
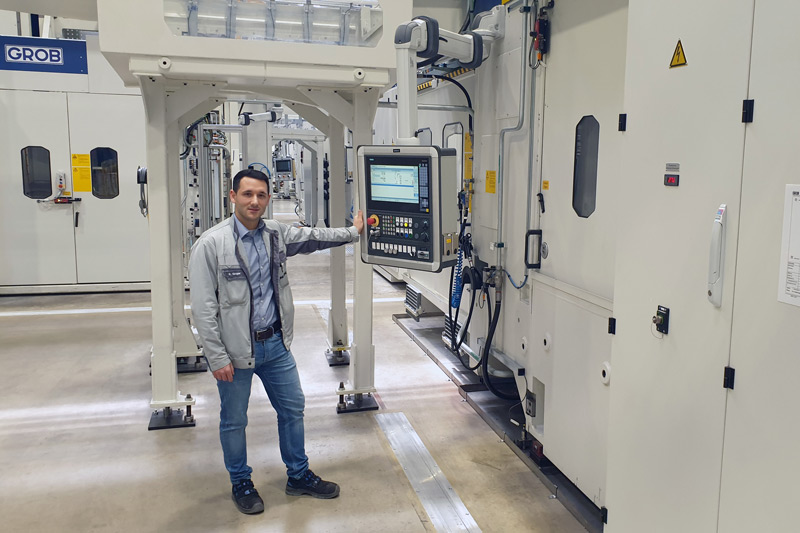
MAN has been working with MAPAL for decades. When tendering for the D30 project took place in 2019, the Aalen-based tool manufacturer was again awarded the contract for the fine machining of the valve guide and valve seat bore. This was down to the years of shared experience and a recommendation from the machinery manufacturer Grob, which is responsible for the complete process and tool design.
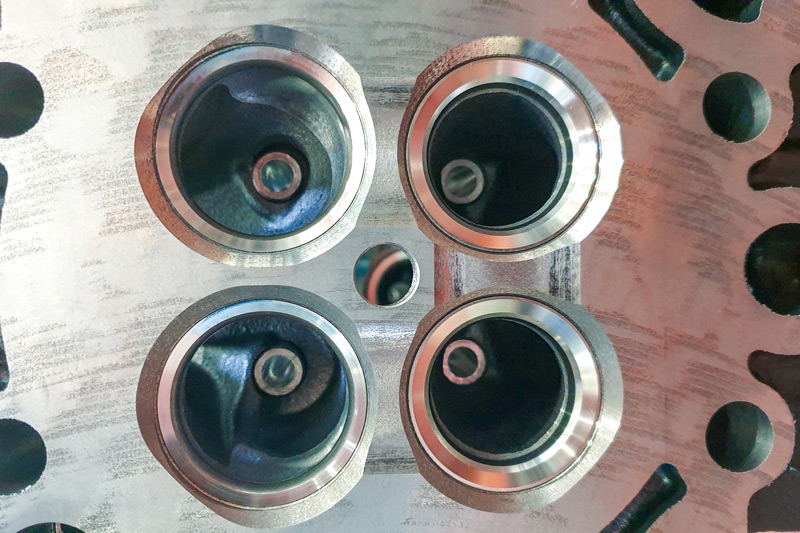
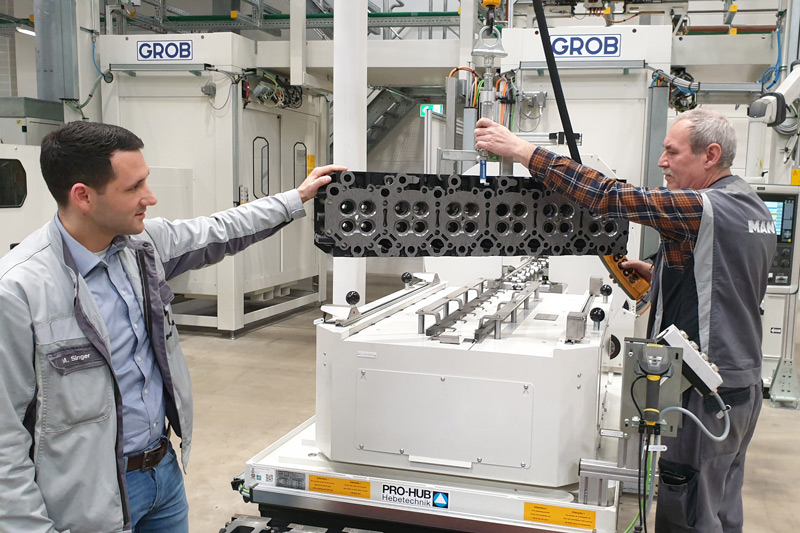
The engine’s six cylinders each have two inlet and outlet valves. This means 24 bores must be drilled into the cylinder head bank. As the inlet and outlet diameters vary, tools of different sizes are required for their machining. Machining takes place on a double-spindle machine. It is embedded in a linked system with individual Grob machines that are loaded using linear gantries.

Proven technology produces reliable process
A further tool manufacturer was entrusted with fine machining in the project’s initial phase. As a stable and cost-efficient process was not possible with its tools, however, MAN ultimately shifted its full focus to the collaboration with MAPAL. The Aalen-based company’s first contribution was a fine machining system which has run on many machines in two production halls at MAN for many years. In close coordination with the client, however, the partners continued to develop the system and achieved significant progress.
Singer hails the achievements: “The machining changed fundamentally. For instance, we saved a semi-cut and were able to do without pilot friction. Instead, we simply moved to our pre-machined diameters with the indexable insert tool, ensured a good bore entrance for the reamer, and then ultimately reamed through once. Experience helped us design the process in the best possible way.” The production concept achieved a good machining quality and complied with the specified cycle time of around five minutes in total for fine machining of the valve seat and valve guide. The desired reliable and economical process was achieved. “This was accomplished despite the increased quality requirements for manufacturing the new engine”, says Markus Meyer, who works closely with MAN as a technical consultant at MAPAL. For the valve and both valve seat blind bores, the tolerances are less than 20 µm. A tolerance of approximately 50 µm must be maintained from the seat to the guide. There must be no offset between the valve seat and the valve guide that could lead to undesirable shear forces. The surface finishes required are specified at an Rz of less than 20 µm. The cylinder head bank consists of GJV 450 cast iron into which more wear-resistant materials for the valves are pressed in the form of a ring and a guide.

Moderne Technologie senkt Stückkosten weiter
Eine Reihe gemeinsamer Workshops hatte weitere Optimierungen im Blick, insbesondere in Sachen Stückkosten. Sie sollten vor dem Anlauf der Serienfertigung weiter gesenkt werden, und in partnerschaftlicher, professioneller Zusammenarbeit konnten MAPAL und MAN signifikante Verbesserungen erzielen.
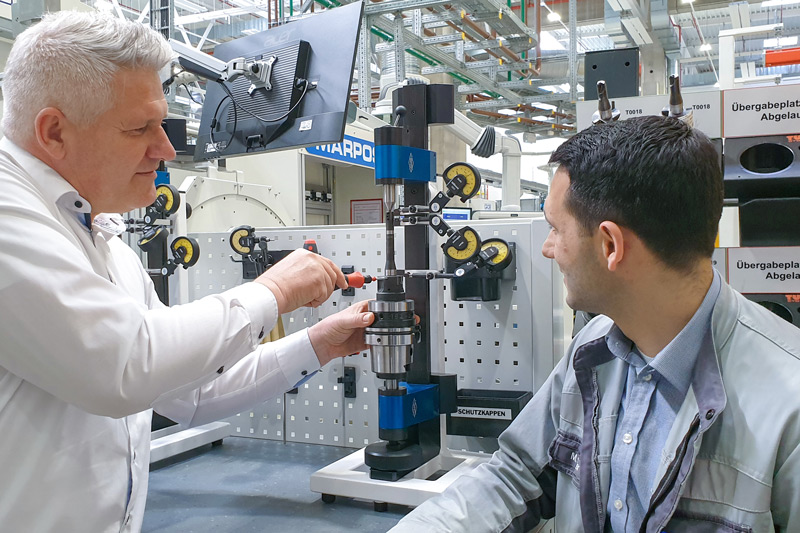
Als Hebel für niedrigere Cost per Part erwies sich die Vereinfachung des Werkzeughandlings – konkret die Reduzierung der Einstellzeit und dadurch eine Vereinfachung für den Bediener. MAPAL brachte dafür sein EA-System (EasyAdjust) ins Spiel, das für das Ventilsitzwerkzeug verbaut wurde. Bei diesem System ist die Verjüngung der Schneide bereits in die Kassette, die als Aufnahme für die Schneide dient, integriert. Damit entfällt der Einstellvorgang für die Verjüngung der Nebenschneide komplett, es muss lediglich der Durchmesser justiert werden. Thomas Teuber, Leiter Produkt- und Anwendungsmanagement Feinbohren bei MAPAL, bringt den Praxisnutzen auf den Punkt: „Der Bediener muss nicht mehr zwei Messuhren im Blick haben. Er konzentriert sich auf nur eine Messuhr, mit der er den Überstand der Schneide zu den Führungsleisten einstellt. Das geht wesentlich schneller.“ Mit dem EA-System geht auch eine Verbesserung bei den Schneiden einher: Die im EA-System verwendeten TEC-Wendeschneidplatten weisen vier, und damit doppelt so viele, Schneidkanten auf wie eine herkömmliche MAPAL Reibschneide. Ein optimierter Schneidstoff und eine innovative Beschichtung steigern die Standzeit und sorgen damit für einen noch stabileren Prozess.

Die Modifikationen zeigten Wirkung: Gegenüber dem ursprünglichen Bearbeitungskonzept konnten die Kosten der Bearbeitung von Ventilsitz und Ventilführung um rund 40 Prozent gesenkt werden. „Mit dem erreichten Meilenstein bin ich sehr zufrieden“, sagt Marco Singer und lobt ausdrücklich die kompetente Zusammenarbeit mit MAPAL. Den kontinuierlichen Verbesserungsprozess will der ehrgeizige Prozessplaner weiter vorantreiben.
Bei MAN geht man davon aus, dass der D30 der letzte vollständig neu entwickelte Diesel-Nutzfahrzeugmotor des Unternehmens sein wird – nach mehr als 100 Jahren Dieselmotorenbau am Standort Nürnberg. 2030 soll jedes zweite Fahrzeug, das an Kunden ausgeliefert wird, einen emissionsfreien Antrieb haben.

Kontakt
Kathrin Rehor Public Relations Kathrin.Rehor@mapal.com Tel.: +49 7361 585 3342


