
小批量 - 通过使用组合型刀具减少刀具更换次数
阀门外壳 EN-GJL-300 – 滑块钻孔
客户的初始情况
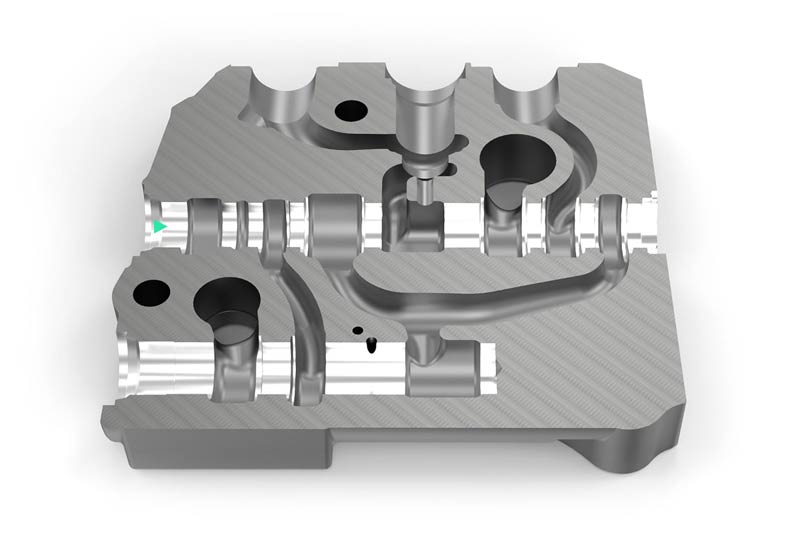
- 小批量
- 可以设置刀具
- 刀具更换次数过多/太频繁
- 每小时的机床费率高
- 由于刀杆珩磨流程而需付出较高的费力
Special features of this solution
- Tool change reduced due to multi-stepped boring tool with indexable inserts
- The contour can be completed in one processing step
- The fine boring tool creates highest bore quality and compensates the axial offset of the bores with pre-machining from two sides
Spool bore
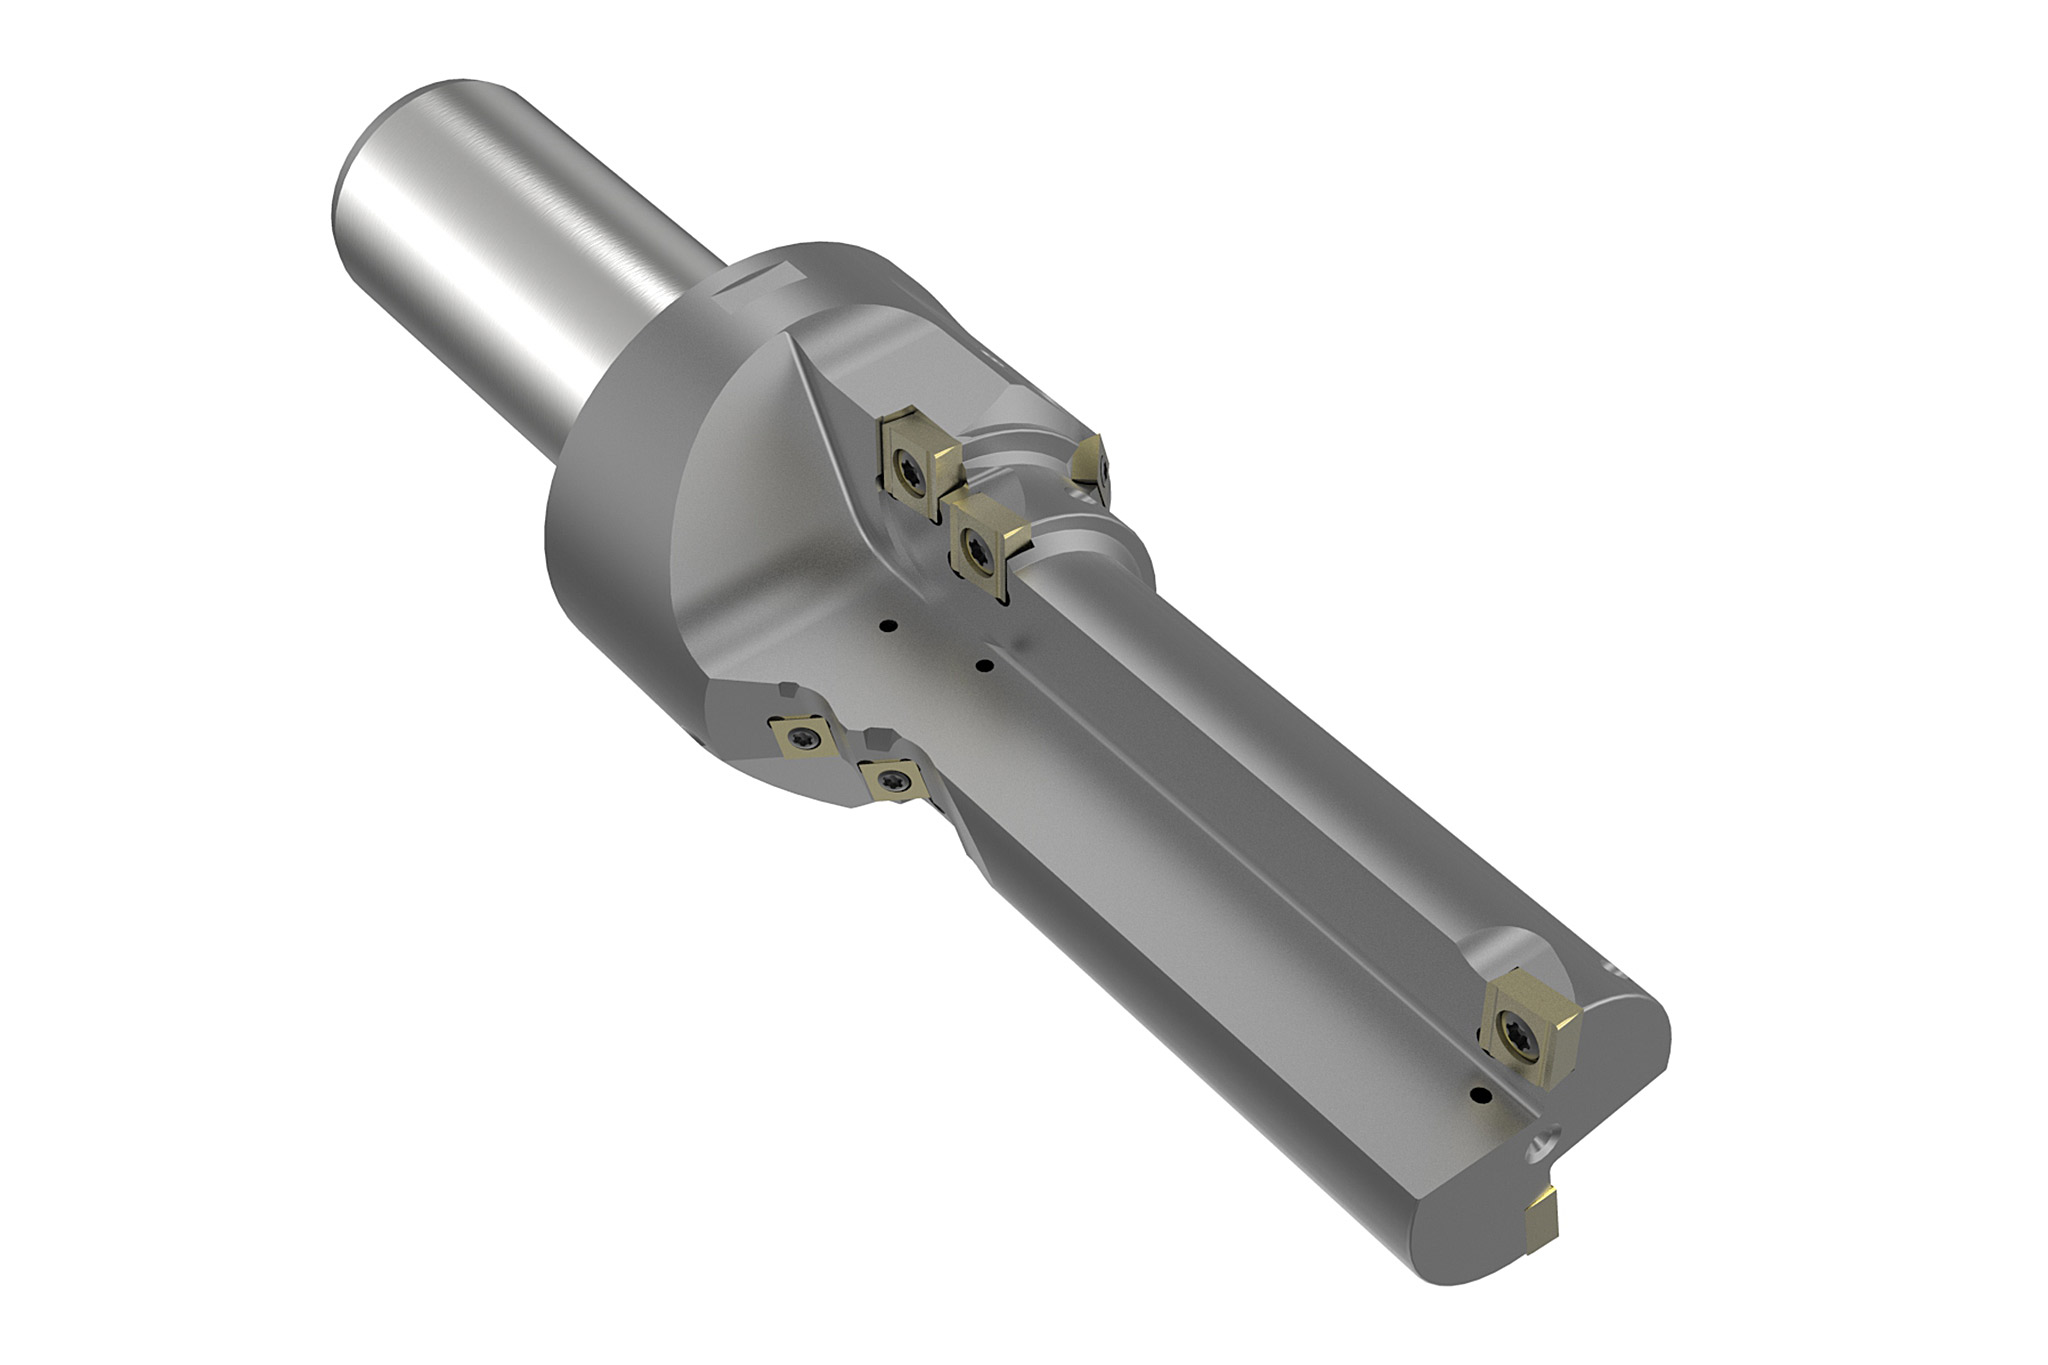
1. Piloting and boring
- Multi-stepped boring tool with radial and tangential indexable inserts
- Pre-machining spool bore and completion of contours in one processing step
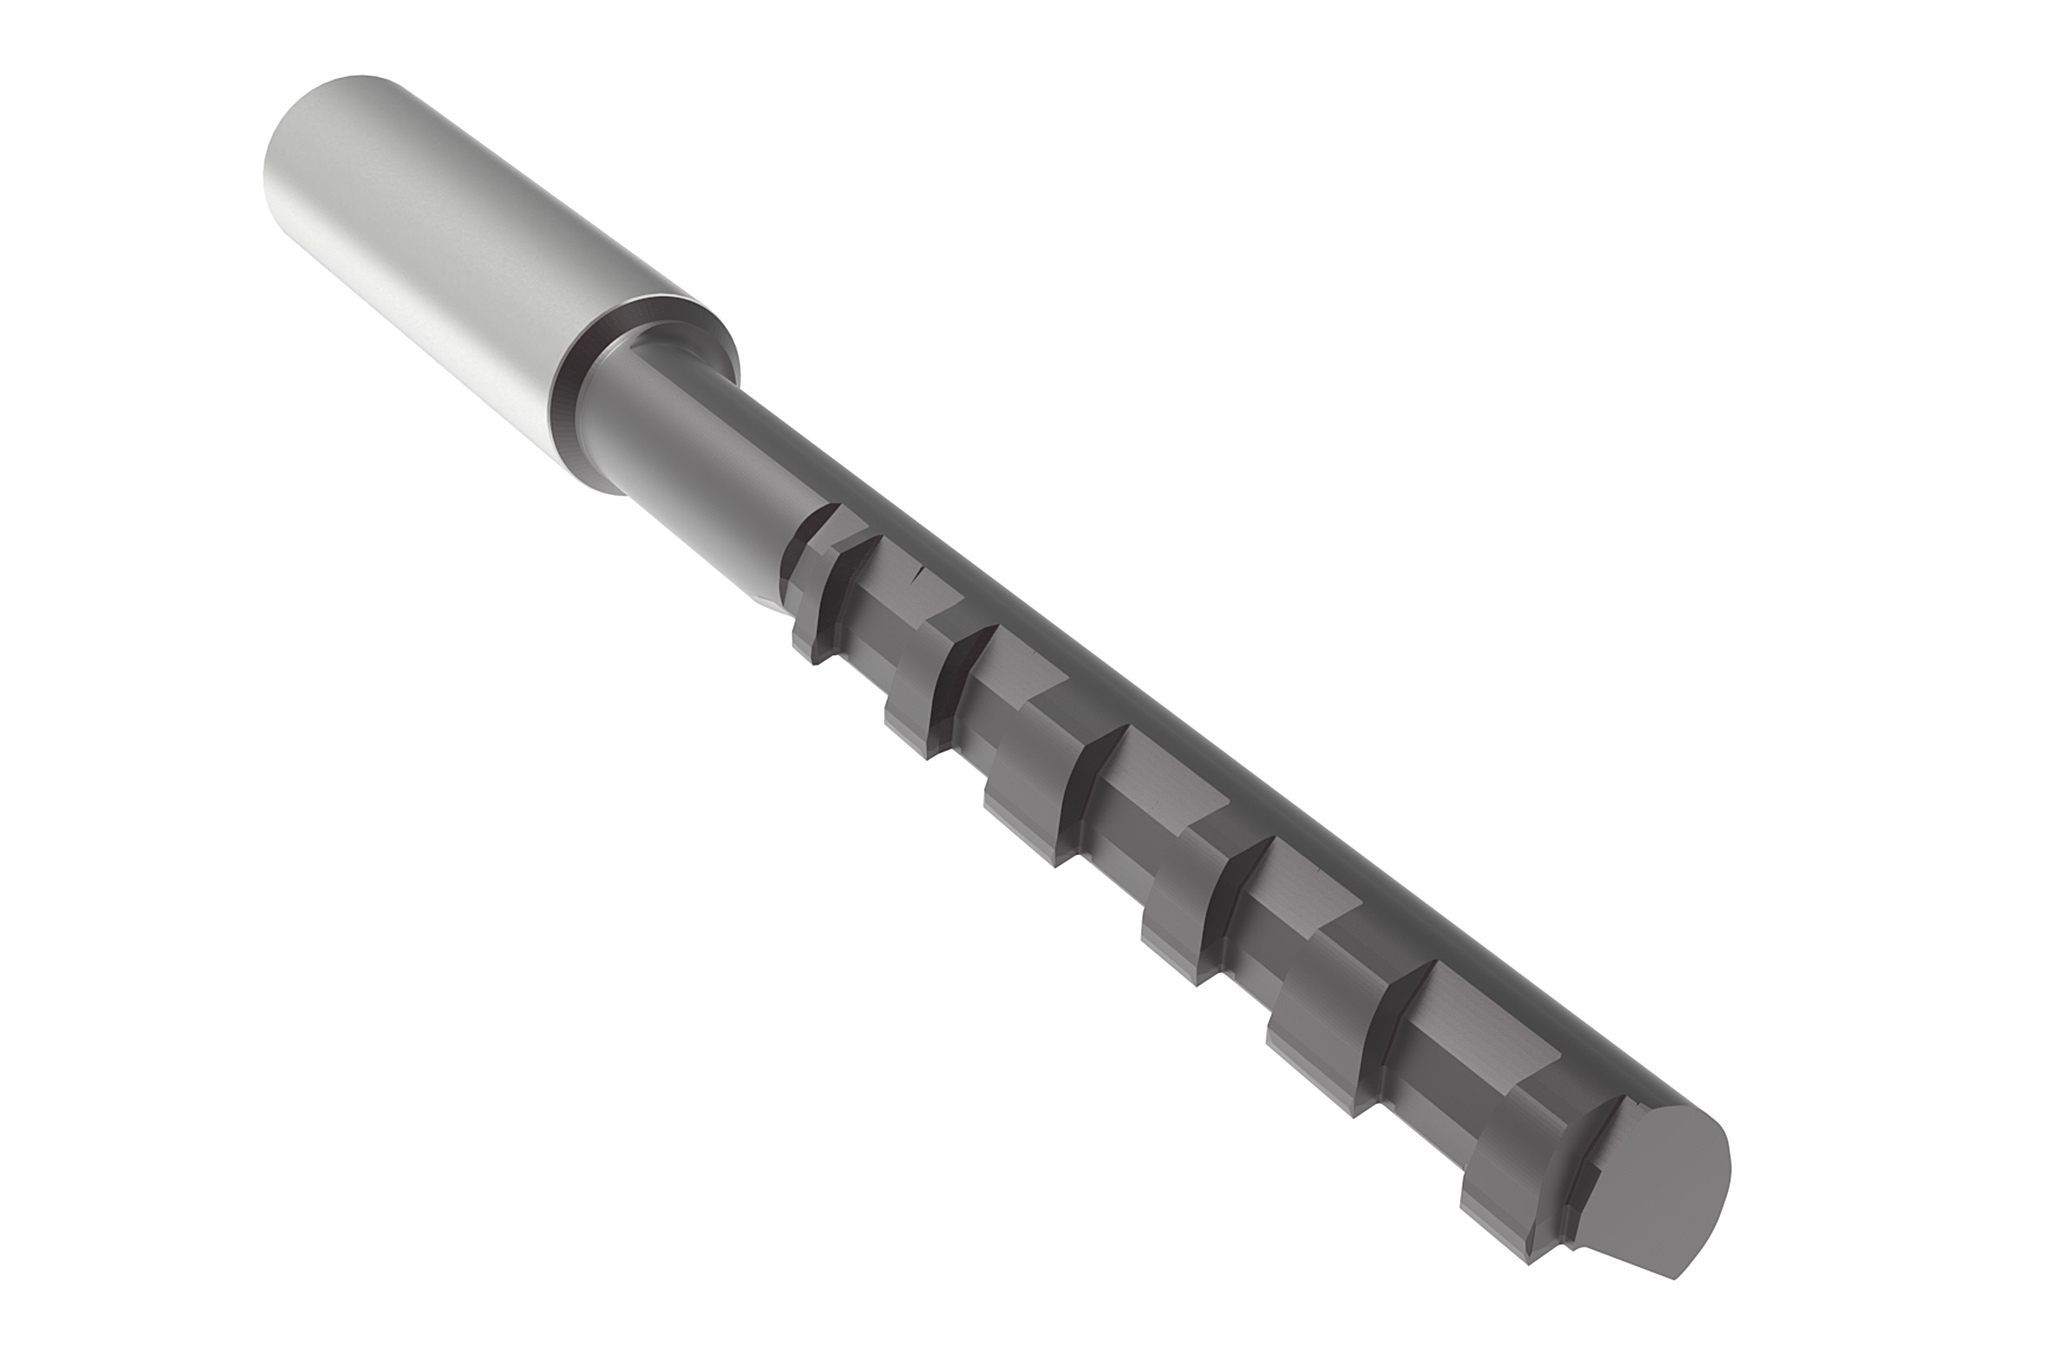
2. Control edge machining
- Solid carbide profile tool
- Highest accuracy and surface finish of control edges
- Defined control edges without macroscopic flaws
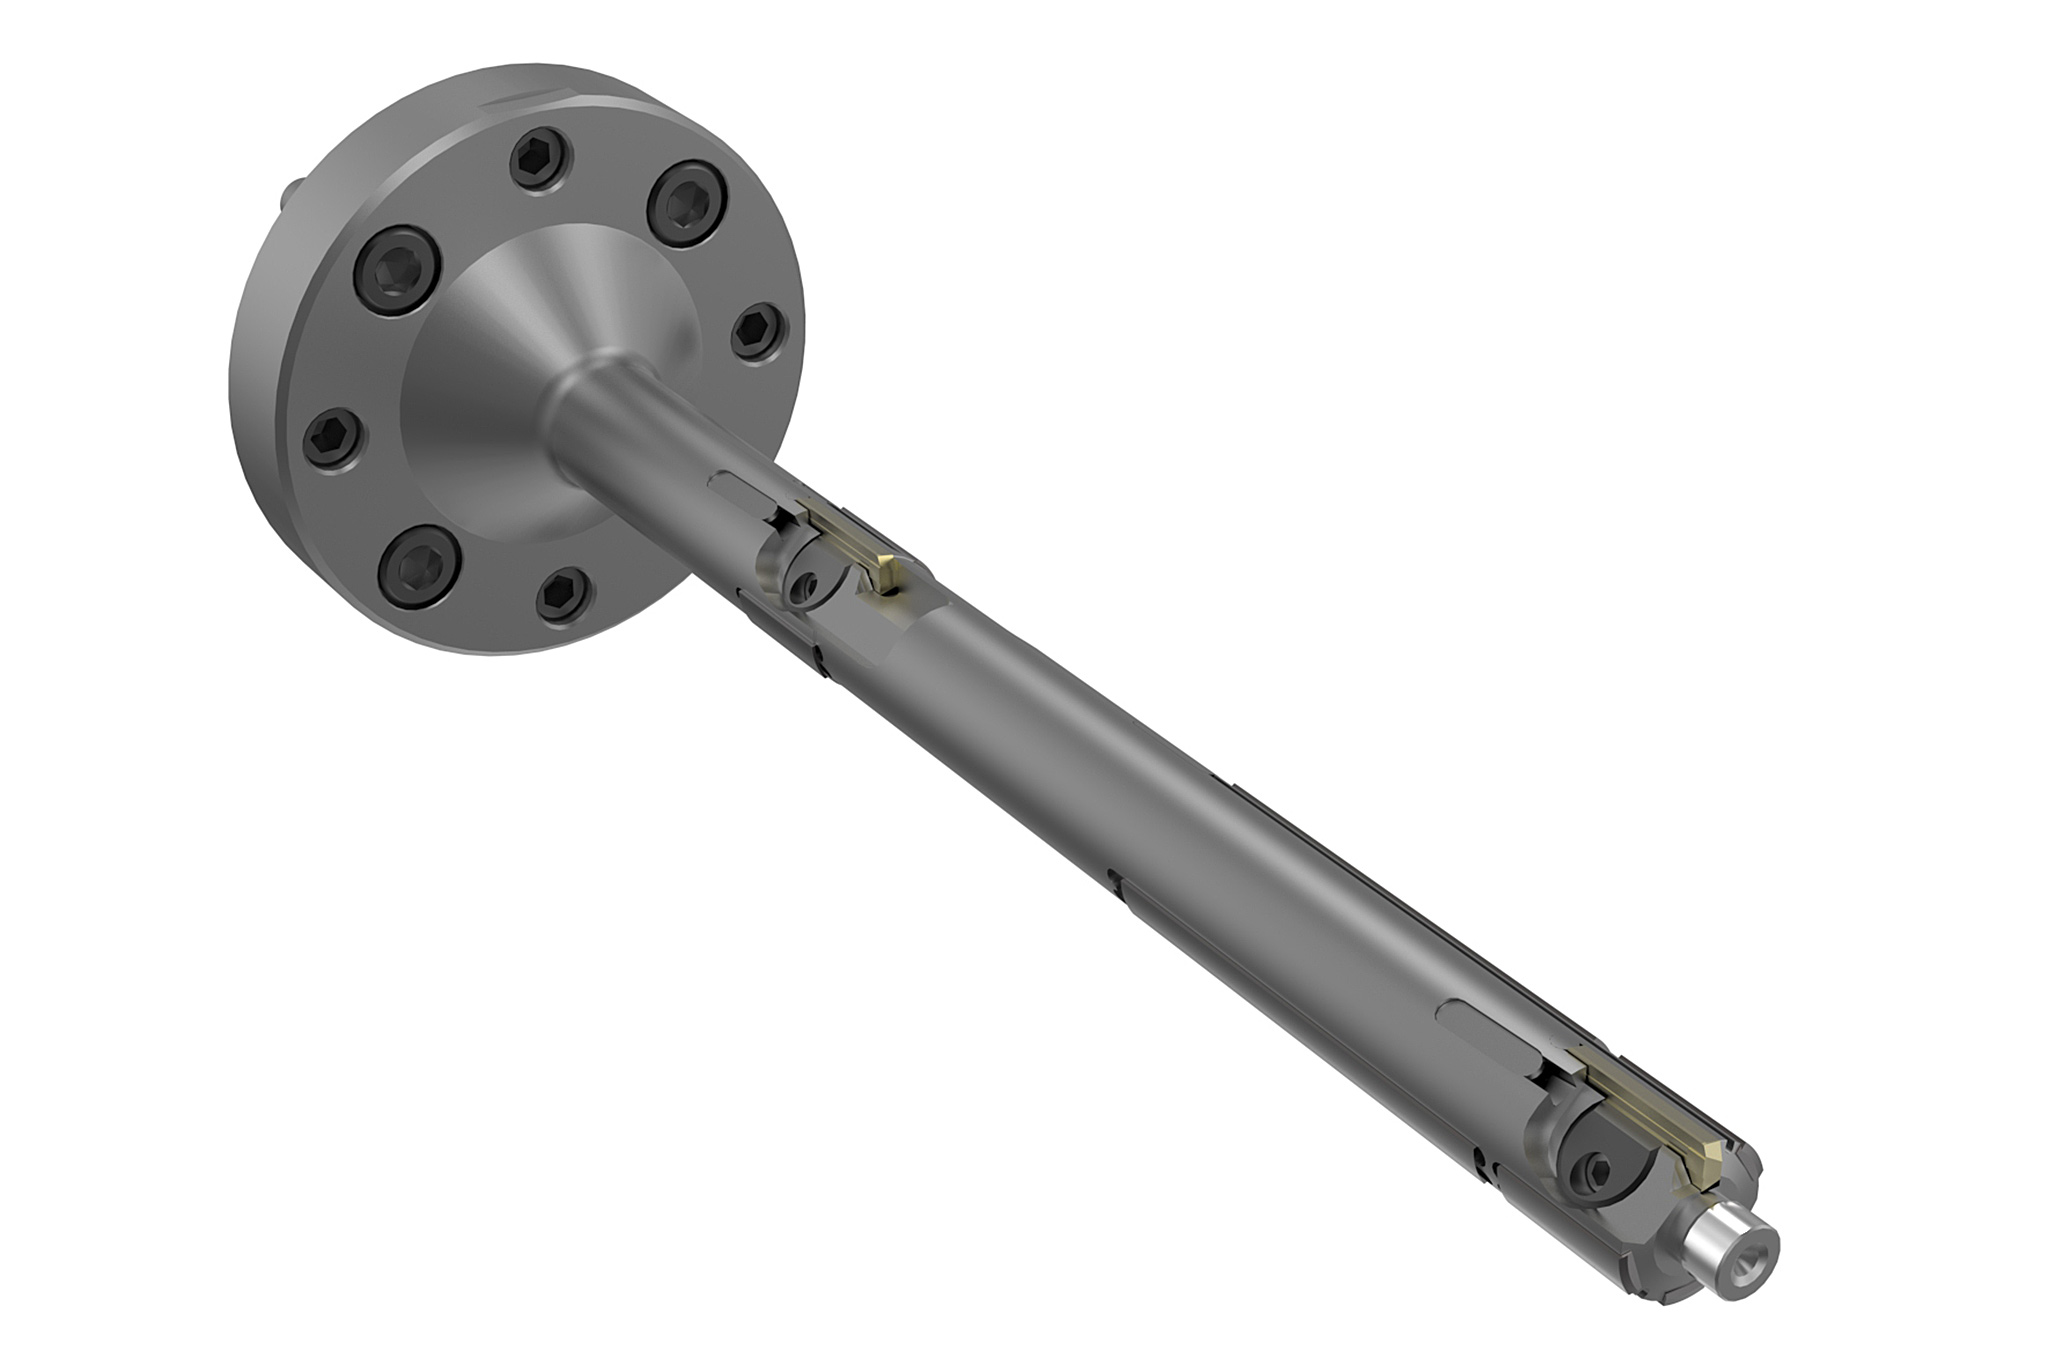
3. Fine boring
- Fine boring tool with indexable inserts and guide pads
- Ideal for bar machining of highly accurate and long bores

Advantages
- Optimally matched process due to solution with multi-stepped boring tool with indexable inserts, control edge machining and fine boring
- Best accuracy and process reliability
- Reduced effort when honing, resulting in cost savings